Hood design-Week 2
Design of Hood
Introduction: Bonnet is an important component of the front portion of the car which is used for many purposes. Bonnet is used to decorate front portion of the car and to add luxurious look. It is made aerodynamic in shape to reduce air effect. Generally, it is used to cover car engine, radiator and many other parts, therefore bonnet must be designed in such a way that all the maintenance parts should be ease of access and it should give a minimum impact of external disturbance on the engine. They serve a great deal of purpose in protecting the passengers inside the car and the pedestrians in the event of an accident, when car come across any accident from the front portion most of the time bonnet system gets damaged and absorbs some part of impact energy resulting from crash.
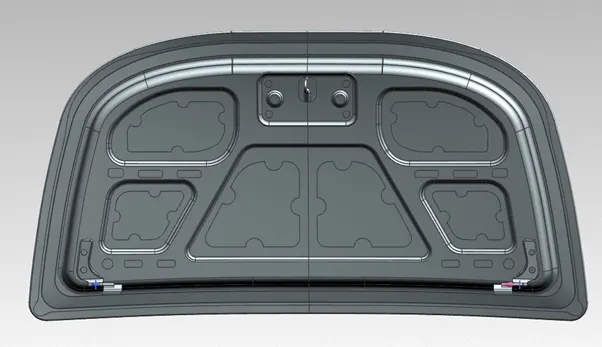
Hood
Objective: The main objective of this project is to come up with a design idea for the bonnet or hood BIW that satisfies the manufacturing requirements, functional requirements, and as well as Euro NCAP standards.
The hood or bonnet have following components:
- Hood outer panel
- Hood inner panel
- Latch & striker re-enforcement
- Hinge re-enforcement
Design consideration:
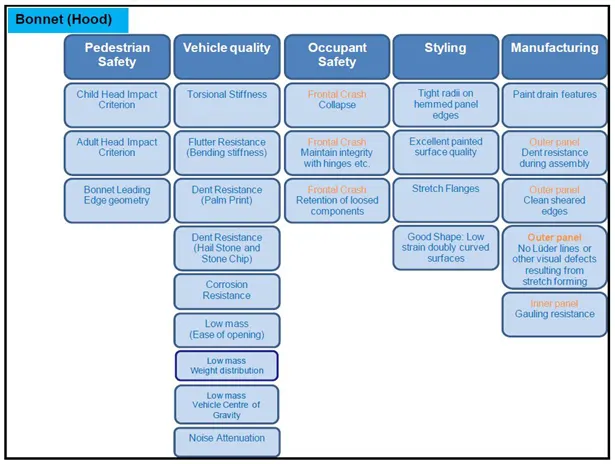
The first and most important safety requirement to be considered while designing the bonnet is the pedestrian safety from frontal collision. The European New Car Assessment Program (Euro NCAP) is a European car safety performance assessment program which has developed test specifications and rating systems for assessing pedestrian injuries during impacts with the front of vehicles such tests include a series of tests using impactors designed to mimic a collision at a speed of 40km/h. They describe a situation in which a pedestrian is situated laterally and a car first hits one of his legs. Tests are conducted on the leg, upper leg and, most importantly, the head, as head trauma is most commonly responsible for casualties.
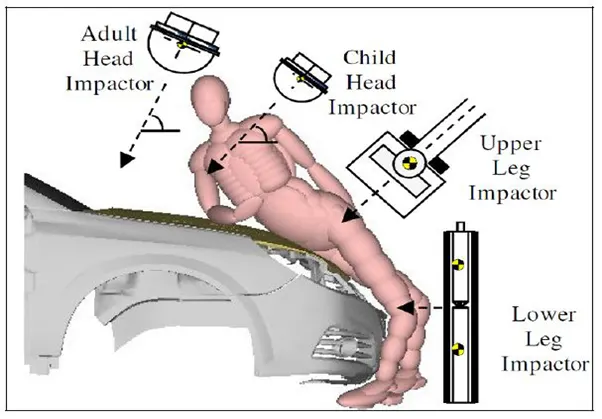
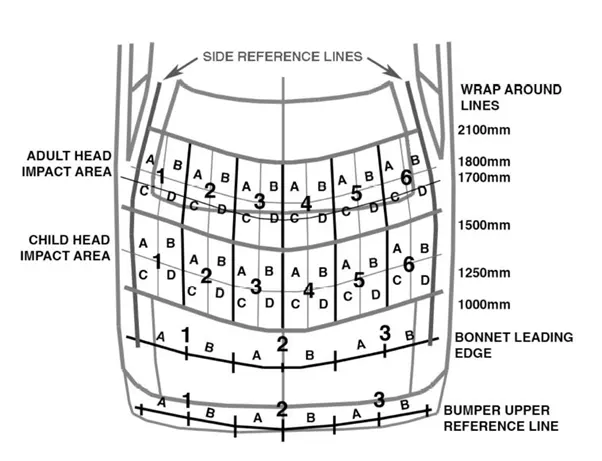
Thus, to avoid severe injuries to the head, the high impact area for adults and children are subjected to less thickness. Also, no reinforcement should be provided in that area as during the head collision, the hood will absorb the head impact energy leading to collapse of the hood and thus protecting severe head injury. Another important criteria for the hood design is the protection of the occupants inside the car during the front collision. The design of the hood should be in a such a way that the during the collision, the force should travel in the upward direction through the embosses and directed towards the body of the car. Thus, protecting the occupants inside.
WAD: WAD (Wrap-Around Distance) is the geometrically traced distance from the contact point with the Ground Reference Plane, vertically below the front face of the bumper, to any point on the vehicle front structure.
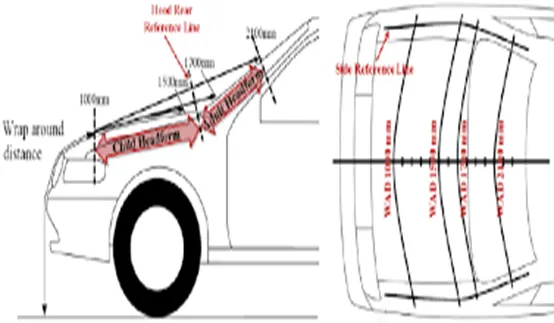
Bonnet Side Reference line: The geometric trace of the highest points of contact between a straight edge, held parallel to the lateral vertical plane of the vehicle and inclined 45 deg. is traversed down the side of the front structure, and the side of the front structure.
Manufacturing requirements:
- Deep drawing process is used for the manufacturing of the inner panel.
- Material used is aluminium as it can absorb twice the crash energy of mild steel, lighter, dent free and can make body panels thicker while still lowering weight.
- No sharp corners inside the panel.
- No negative draft.
- Provide appropriate corner relief on the area of curvature.
- Outer panel thickness = 0.75mm
- Inner panel thickness = 0.75mm
- Reinforcement thickness = 1.5mm
Design of inner panel:
Master section: The master section is created based on the requirements received from the marketability team and the manufacturing requirements that we saw before. Below are the images of the master section used for the design.
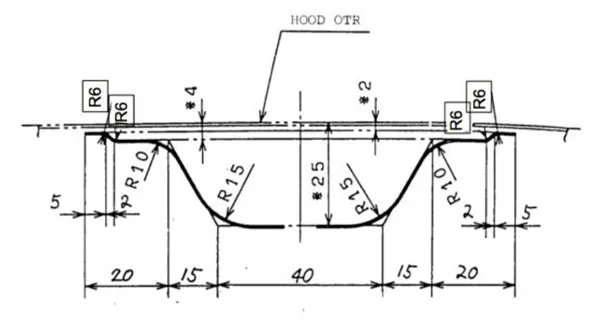
Master section
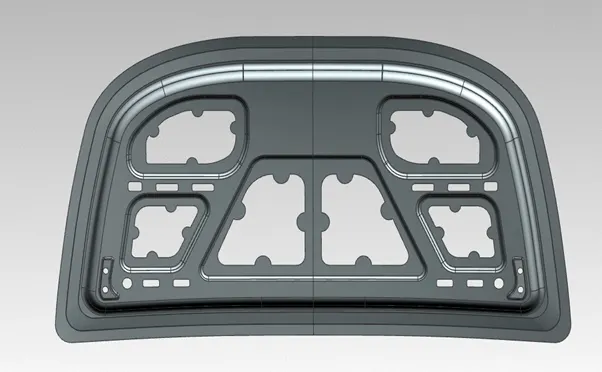
Hood Inner panel
Initial design was created from the master section that was already provided. Embossing is a metal forming process for producing raised or sunken designs or relief in sheet material by means of matched male and female roller dies, theoretically with no change in metal thickness. Embosses are created to provided addition strength and to direct the forces from the front collision towards the hinge and body of the car.
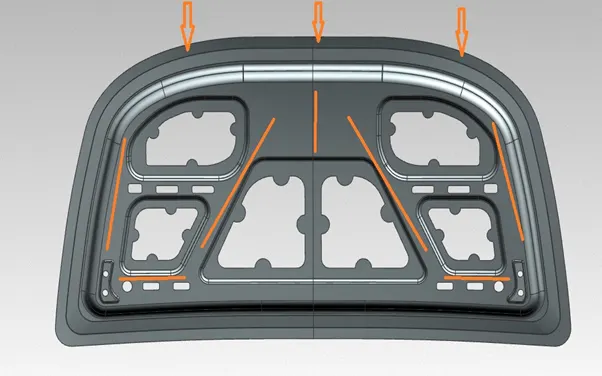
Forces distributed
The embosses in the inner panel are made according to the diversion of the load path. The emboss depth is kept at a maximum of 5mm to be on the safer side so that the part is manufacturable.
Fine tuning the emboss: To make the component easy to manufacture, all the sharp corners from the embosses are removed. The curvature intersections from different nearby embosses are blended out to produce a smooth transition.
Position of hinge and striker: -For the proper opening and closing of the hood, the striker should be perpendicular to the trajectory of the hood. For this, hinge is assembled at its position. Once it is placed, hinge axis is drawn, using the hinge axis as the center we draw a big circle to the position the latch in such a way that it is perpendicular to the hood trajectory.
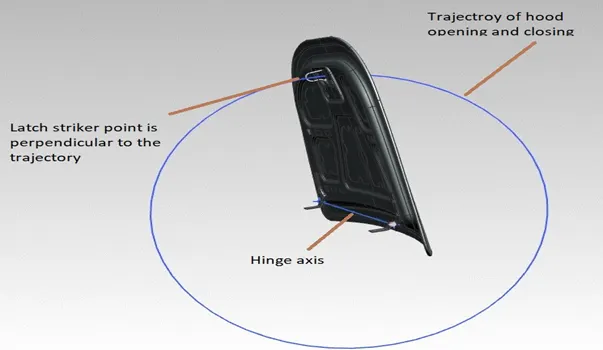
Latch and hinge axis
Latch and Hinge Reinforcement: To furthermore reduce the impact to the occupants inside the car additional latch and hinge reinforcement to the hood. When latch and striker are placed, there is drop in strength at that position thus reinforcement is required. Also, stiffness pads are placed to reduce Noise vibration and hardness (NVH). Hinge and latch reinforcement thickness is kept at 1.2 mm but it may vary.
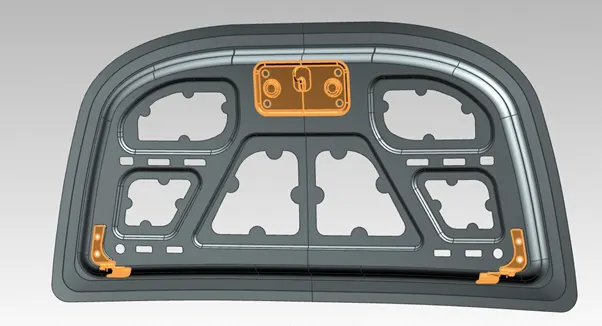
Latch and Hinge reinforcement
Mastic Data: As we know that the main purpose of the outer panel is for the aesthetic looks. Thus, we cannot use bolts or welding. This has to be done with the help of the hemming and mastic sealants. Mastic sealants are elastic compound that behaves like the rubber. It is placed between the outer and inner panel. The mastic points are defined on the hood inner panel where the hood can easily deform. They help the hood outer panel to come back to its original shape after it gets deformed. Initially is it in paste from, but after the hot furnace bath it gets hardened thus joining the outer and inner panel. Mastic sealant has the tendency to increase the strength of the panel and has influence of 80mm diameter.
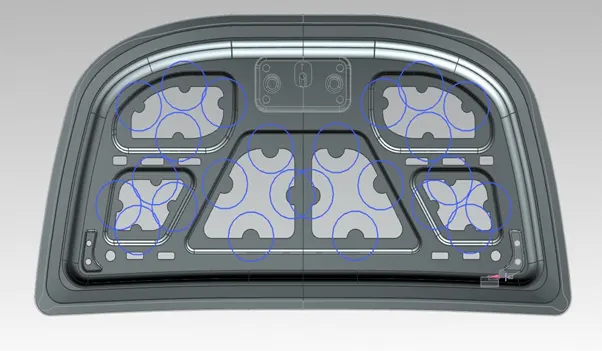
Design of Outer panel:
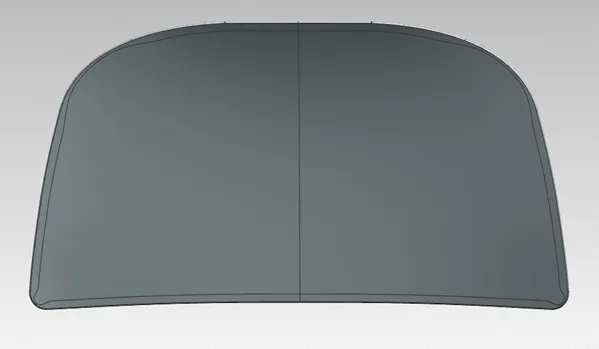
Hood outer panel
Hemming: Hemming is the process in which the edge is rolled flush to itself, while a seam joins the edges of two materials. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges. In hood design. Hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together.
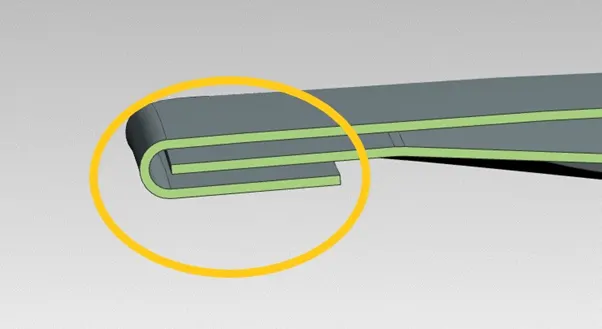
Hemming
- Deep drawing process: The deep drawing process is a forming process which occurs under a combination of tensile and compressive conditions. A flat sheet metal blank is formed into a hollow body open on one side or a hollow body is formed into a hollow body with a smaller cross-section. [DIN 8584]
Deep drawing processes are divided into three types:
- Deep drawing with tools
- Deep drawing with active means
- Deep drawing with active energy
In the automotive industry, deep drawing is usually carried out using rigid tools.
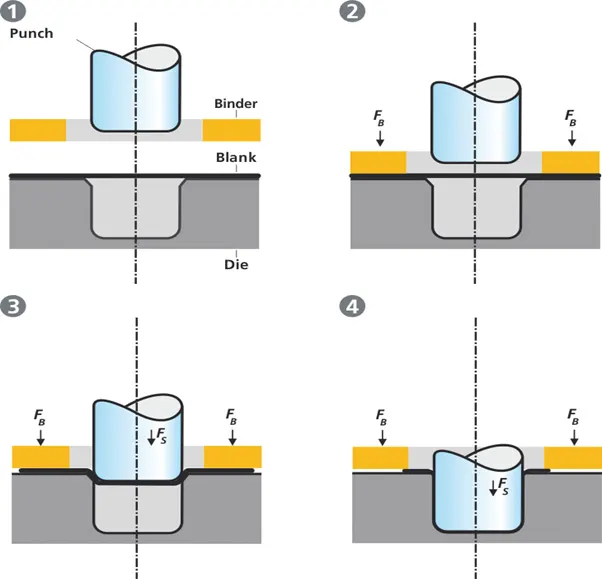
Illustration of the deep drawing process
The figure illustrates the deep drawing process. The rigid tools consist of a punch, die and binder. In deep drawing, the plate holder closes after the metal sheet blank has been inserted.
Next the sheet is clamped between the die and the binder. This process slows down the flow of the sheet while it is being drawn and thereby prevents wrinkles from forming under the binder. The punch stretches the sheet over the die radius and forms it in the die. The amount of punch force necessary for forming is thereby continually increased up to the lower dead center of the punch.
Whereas in pure deep drawing there is no reduction of sheet metal thickness, forming is achieved in stretch forming purely as a result of a decrease in sheet metal thickness. Stretch forming is extensively used for the forming of only slightly curved parts with low depth of draw (e.g. roofs, doors).
When drawing complex car body parts in practice, there is usually a combination of stretch and deep drawing involved. It is necessary that the sheet metal is stretched as well as possible without reaching the material’s limits (e.g. splits, wrinkles).
There are approximately 300 to 400 sheet metal parts which fit together to form the body of a car. In order to manufacture high quality sheet metal parts optimally for their particular use, specialized software simulates the complete deep drawing process.
2. Trimming: Trimming is a finishing operation in which shearing off of burrs from the cut edges is carried out in order to make the edges smooth and also impart dimensional accuracy. Cut off operation involves removal a blank from a sheet metal by cutting on opposites sides, sequentially.
3. Flanging: Flanging is a manufacturing process which is used to form flanges around holes by using sheet metal. A brief and concise review of the contributions made by the previous researchers in the area of hole-flanging process has been presented.
Relief Data: Relief is provided onto the part or component in order to remove any stresses developed in a particular area i.e. sharp corners that takes place during the hemming process is carries out. Thus, corners are rounded or chamfered.
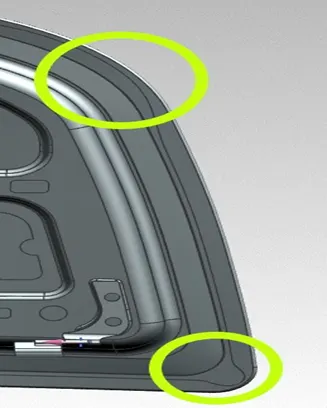
Relief angle
Draft analysis: Draft analysis is carried out to see that the panel can be drawn or not. For this I can choose Y-axis is vector. It also helps to find the negative draft present in the component which can cause difficulty in manufacturability.
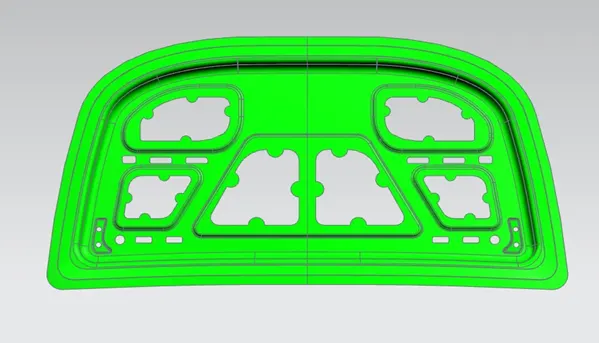
Thus, from the above image we can conclude that the part can be drawn without any problems.
Conclusions: Thus we have designed the hood of the car that satisfies the industry’s manufacturing requirements, functional requirements and as well as Euro NCAP standards using NX CAD