Design of backdoor
BACK DOOR DESIGN:
Objective:
To develop the car back door by using given surface method by automotive sheet metal design.
Intoduction:
A backdoor is located at the rear end of the car which gives access for the boot space to store luggage, spare wheel, etc. These doors can be operated manually or electric powered. In most of the luxurious cars it is electric powerd.
Back door is also called as hatch, tailgate, trunk-lid or boot door is basically the 5th door in a 4-door car. It's the rearmost part of the vehicle which gives access to the trunk and has mounts for wiper motor, tail lamps, hinges for supporting it's weight in opened position, gas stays which helps with it's opening and keeping it open, radars and cameras, etc.
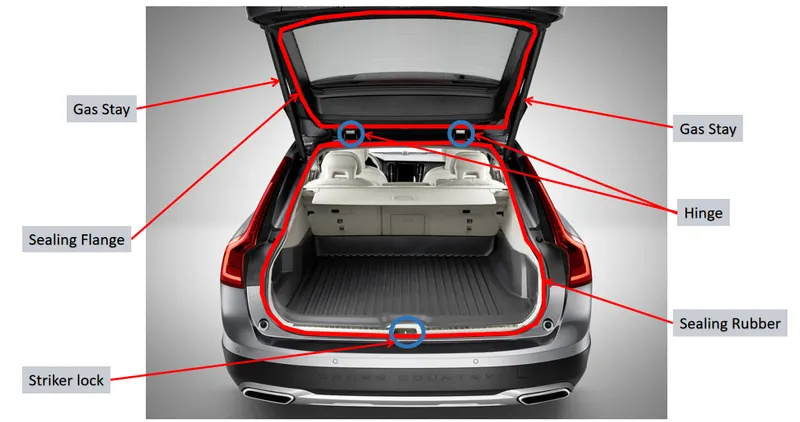
A backdoor is usually made up of one inner panel and two outer panels joined together by hemming and spot welding wherever necessary.
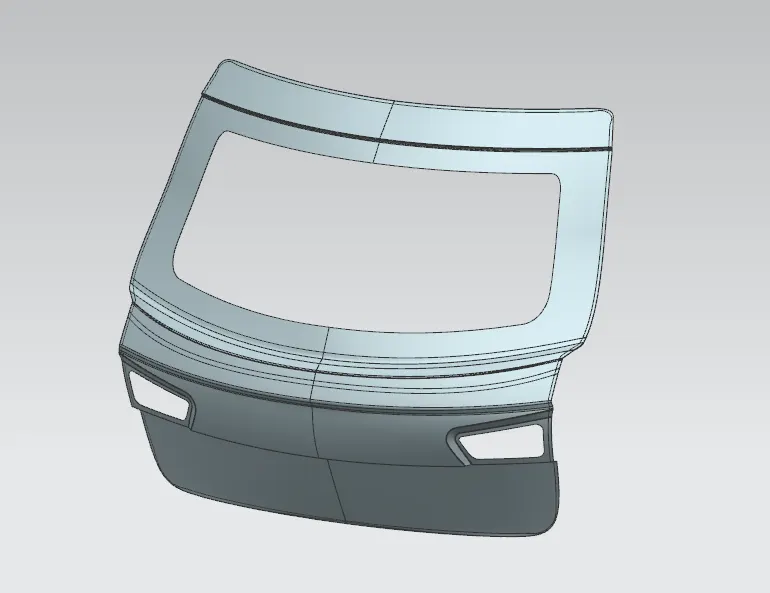
The material used for backdoor varies as per the price range of the vehicle. Most of the low cost vehicles use steel as it is cheaper and use parts that are stamped using moulds. These parts are usually of uniform thickness and reinforcements are added to improve local strength wherever required. The premium vehicles use aluminium parts which are usually die casted and hence can have variable thickness. This eliminates the need of reinforcements hence keeping the weight even lower as aluminium parts are lighter in comparison. On the contrary aluminium is more expensive than steel hence it's applications are limited in cheaper vehicles. Currently due to the extensive use of platic trims and plastic parts the cost of aluminium is affordable for the manufacturers in all price brackets. Use of aluminium reduces the overall weight of the component and hence the vehicle improving it's fuel efficiency.
Reinforcements:
As mentioned for local strengthening reinforcements are usually provided. Instead of making the whole panel of a thicker sheet, a thinner sheet with thicker local reinforcements are usually 1-1.15 mm thick whereas the panel itself is of 0.55-1 mm thickness.
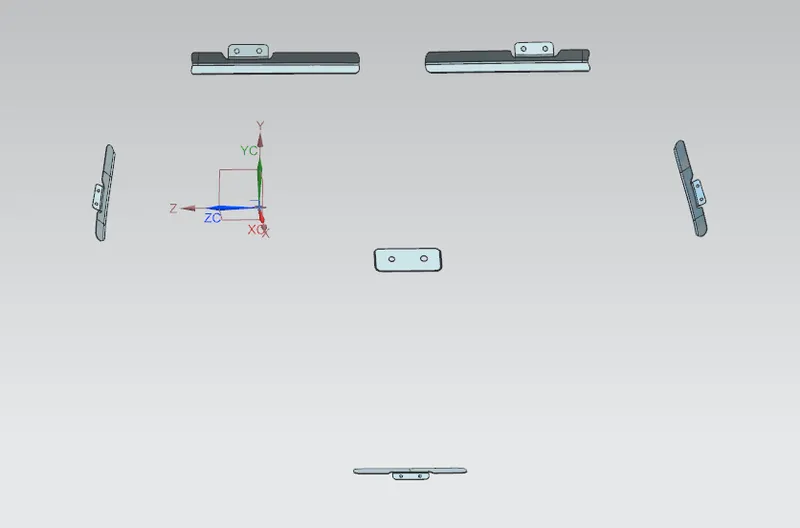
Thickness value for backdoor panels:
Outer panel: 0.75 mm
Inner panel: 0.75 mm
Reinforcements: 1 mm
Design considerations for back door inner panel:
01.
Rear visibility criteria.
02.
Support structures like hinges and gas stays.
03.
Mounts for wiper motor, tail lamps and other wiring loops.
04.
Fit and clearances.
05.
Boot space.
06.
Rear crash regulations and requirements.
07.
Sealing and it's functions.
08.
Joining techniques like hemming, spot welding, etc.
Components of back door:
• Inner panel.
• Outer panel upper.
• Outer panel lower.
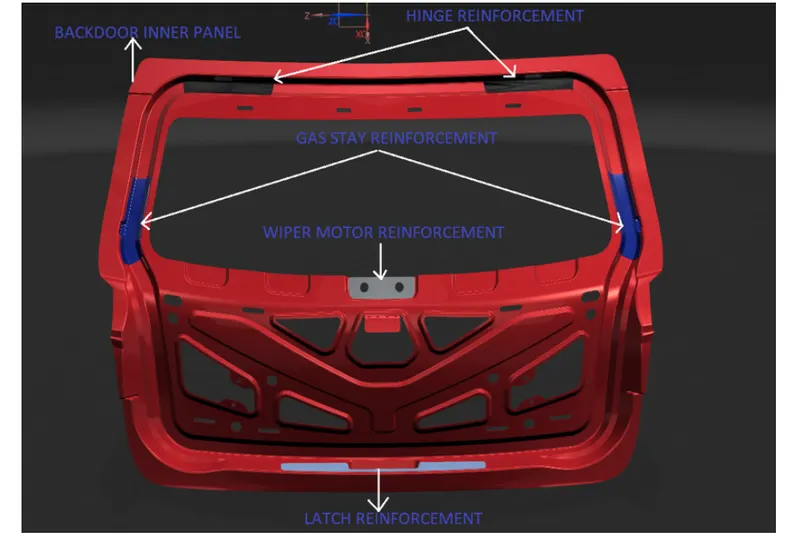
• Hinge reinforcement LH.
• Hinge reinforcement RH.
• Gas stay reinforcement LH.
• Gas stay reinforcement RH.
• Wiper motor reinforcement.
• Latch reinforcement.
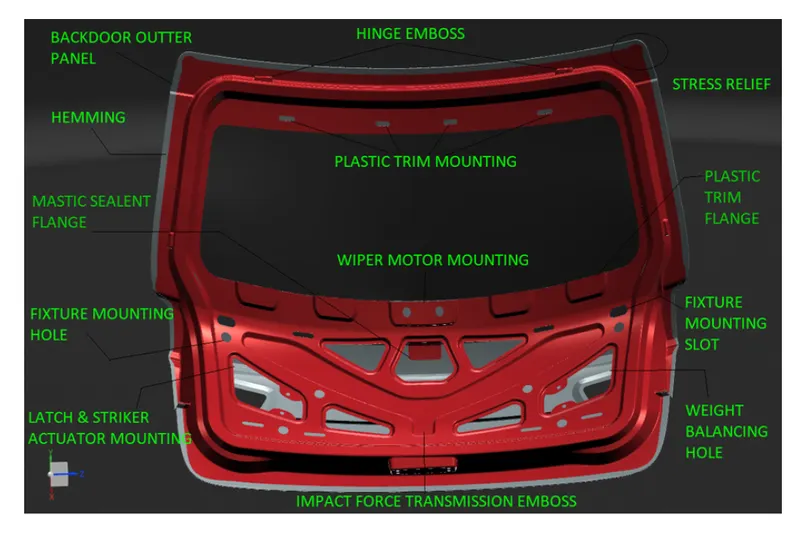
Inner panel:
Car back door inner panel is made of either steel or aluminium. Most of the luxurious car's panels are made of aluminium because of it's properties. But the cost of aluminium is high.
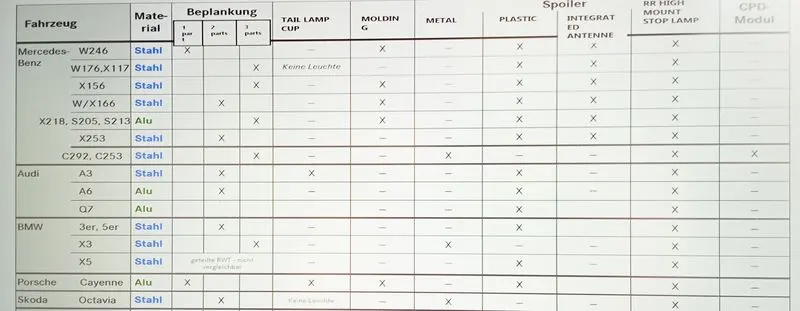
STEEL VS. ALU TABLE:
Benchmark between companies using steel and aluminium inner panel.
Wiper motor, latch reinforcements, hinge reinforcements and gas stay reinforcements are mountes on the inner panel of back door only.
The embosses in the inner panel helps stiffening the inner panel and act as a local reinforcement. Another purpose of giving embosses is to distribute impact forces towards hinges.
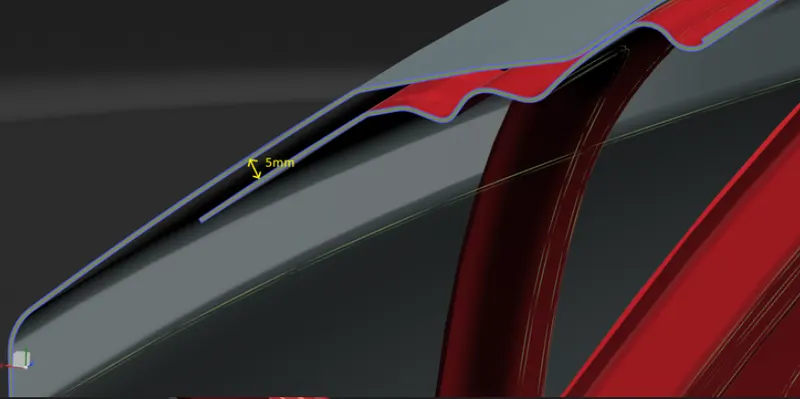
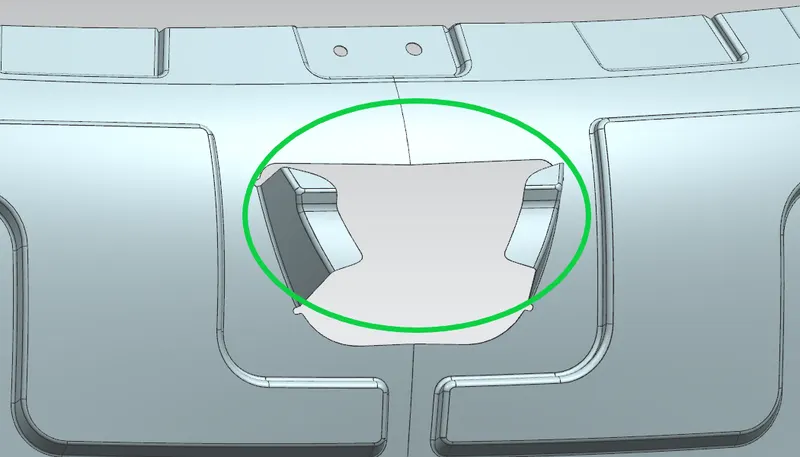
From the above figure it is seen that the extension is for mastic sealant. In bottom of the panel, there is more gap between the inner panel and outer panel to give strength and rigidity we should give those extensions and joined using mastic sealant and the gap between the extension and the outer panel is minimum of 5 mm for mastic sealant.
Inner panel draw direction:
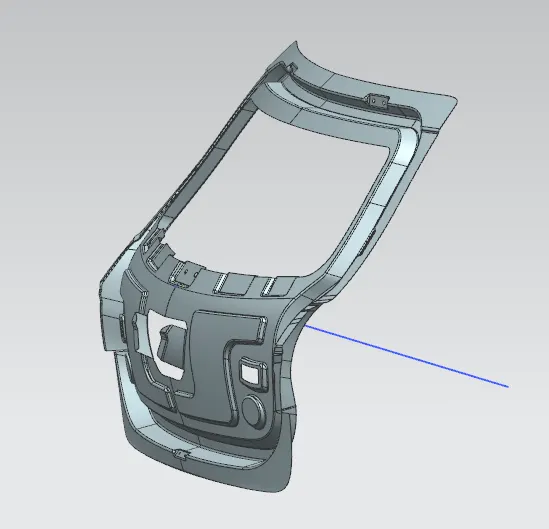
The inner panel is produced by either casting or through deep drawn method. Mostly aluminium panels are casted, steel panels are made by deep drawn process only. If it is deep drawn, then there must be a tooling direction through which that direction the panel is deep drawn.
Draft analysis:
Draft analysis of inner panel is carried out through the tooling direction only. Only the green areas are acceptable and in worst cases yellow regions are accepted but the blue and red regions are accepted only in a specific cases.
The draft angle for aluminium casted panel is 2 to 3 degrees is enough but if it is steel then the angle is more than 7 degree.
In this study we considered it as steel and 7 degrees as a draft angle and direction chosen as a tooling direction which is the deep drawn direction.
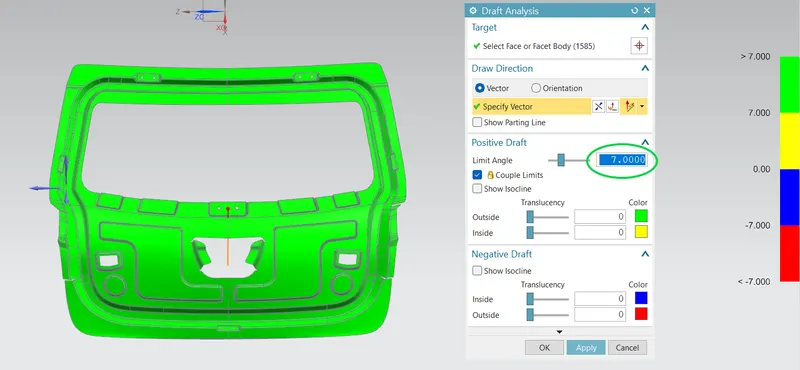
From the above figure it is clear that all areas are in green colour so our design is satisfying the draft analysis criteria.
Outer panel upper and lower:
Outer panel is the styling surface of the back door. Glass for gear visibility is mounted on the outer panel upper also rear lights are mounted on the outer panel upper.
Number plate is mounted on the outer panel lower. Spot welds and other manufacturing process should be done only on the inner panel because the outer panel is the styling surface which should not have any scratches or welds. Because it affects the style of the car which leads to bad impression on the customers.
Hinge reinforcement:
Hinges support the weight of the whole back door. Hence, the reinforcements must be provided there too. The emboss is designed in such a way that the hinges should operate freely. The hinge is connected to the rear roof of the car.
Gas stay reinforcement:
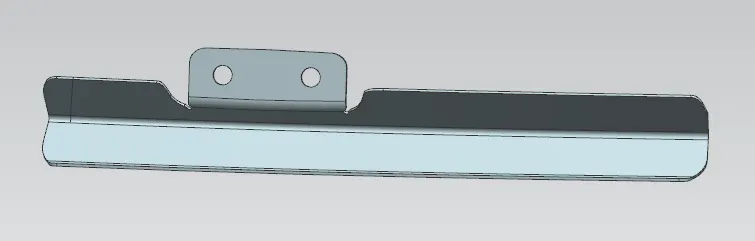
Gas stay is used to lift the backdoor automatically. There are two types of gas stay one is semi-automated and another one is fully automated. In semi automated type the back door needs little force to lift after that it lifts the back door automatically. In fully automated, it has power spindle which lifts the backdoor automatically.
Wiper motor reinforcement:
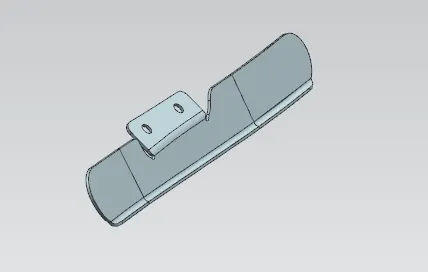
Wiper is used to wipe out the rain water falls on the back door window. It is actuated by the motor which is mounted on the inner panel. Due to the vibration and heat created by the motor the inner panel where the motor is mounted gets deform and the parts attached to the motor starts to vibrate which leads to poor NVH. So we have to provide the reinforcement where the wiper motor is placed.
Latch reinforcement:
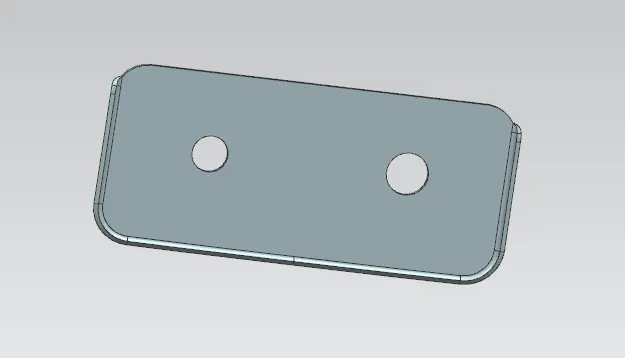
At bottom of the panel, reinforcement and embosses are given to accommodate the latch and striker assembly. Generally key operated or automatic remotly controllable
mechanism is used to keep the door open or close. The actuators, receivers and other electronic devices are mounted on the inner panel only.
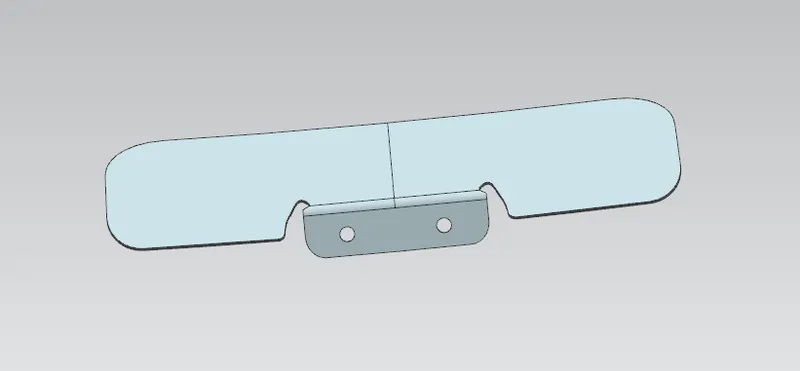
Plastic trim:
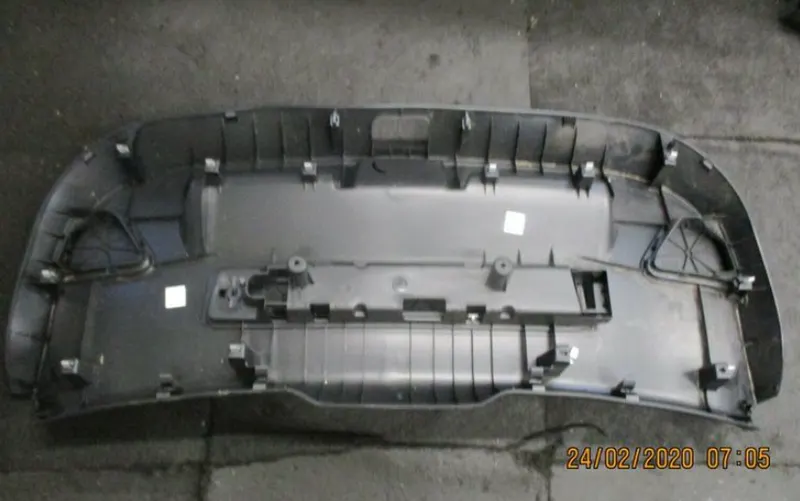
Plastic trim is the part which covers the ugly part of inner panel. There are holes given in the inner panel of the back door in which the plastic trim is mounted.
Hemming:
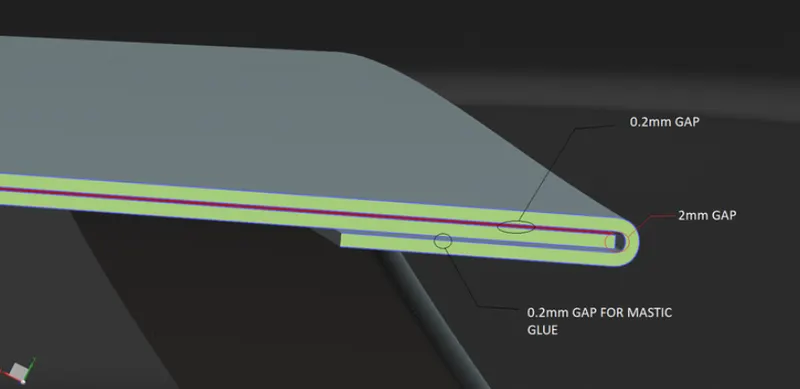
Hemming is the metal working process in which a sheet metal edge is rolled into itself. The outer surface of the panel is rolled 2 to 3 times over the inner panel. In first roll the panel is bent slightly and in the second roll the sheet metal is rolled even more and in the last roll it completely fits or covers the inner panel. There must be a 0.2 mm gap between outer and inner panel during hemming operation in order to executive the hemming glue operation.
Spot welding:
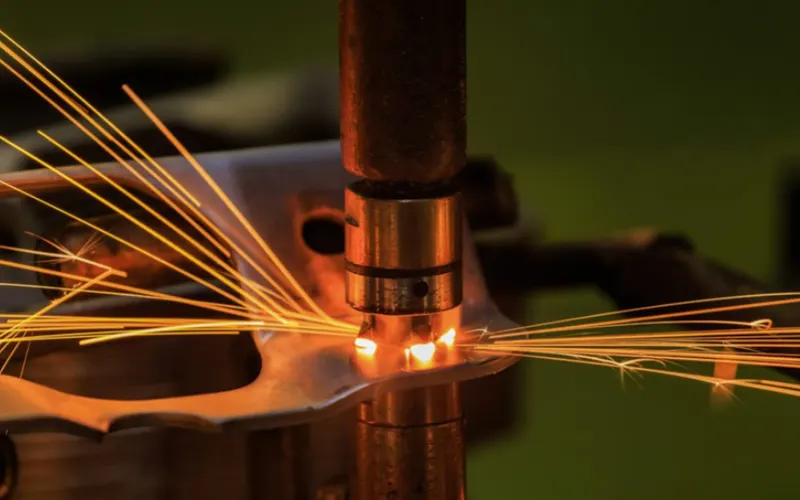
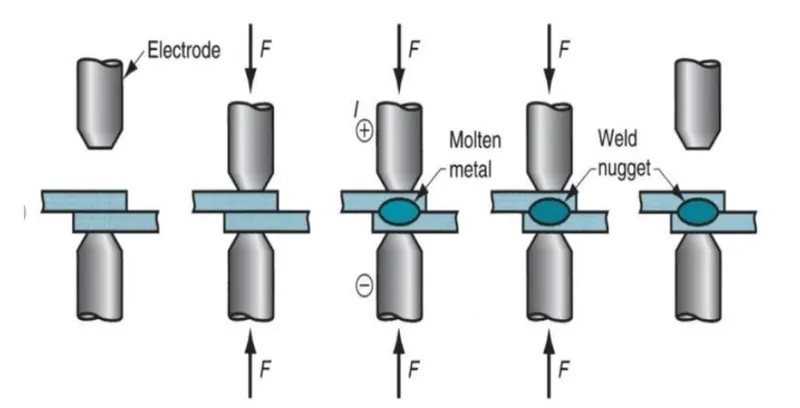
Spot welding is a form of resistance welding also known as Resistance Spot Welding (RSW). Spot welding is done using heat produced by resistance to an electrical current to join materials together. The current heats the materials to a point where they become malleable. The use of strong pressure bonds them together.
Another form of resistance welding is Projection Welding. This process involves fusing a fastner's embossed or coined projections to the metal base material to form a weld. As the materials never melt, they do not intermix. This means the resulting weld is more like a forging of the materials.
Spot welding is only suitable for a small selection of base materials. Low carbon steel is the most suitable material for spot welding. This is because it is more resistant to electricity and has a lower thermal conductivity than the copper electrodes used to create the required electrical current.
High carbon steels and aluminium alloys can form brittle welds that don't last with the spot welding process. Pure aluminium can qualify for spot welding but requires higher current levels. This is because it has a lower resistance to electricity than low carbon steel.
The outer panel upper and outer panel lower are joined through the spot welding. So there must be no gap between the outer panel upper and outer panel lower.
Conclusion:
So as per the objective the back door is designed for the given panel.