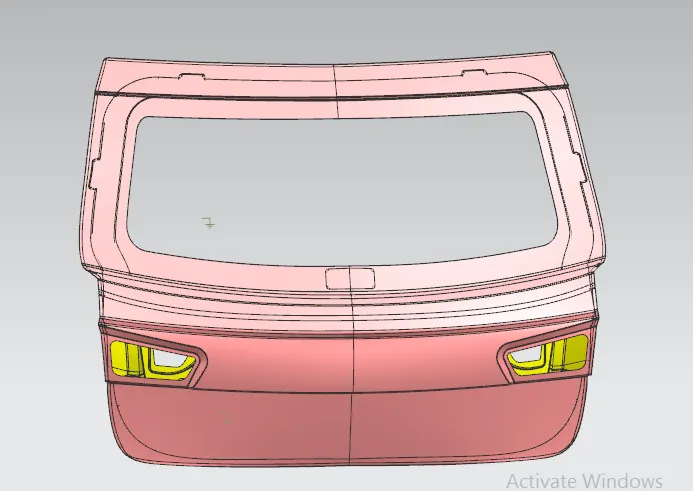
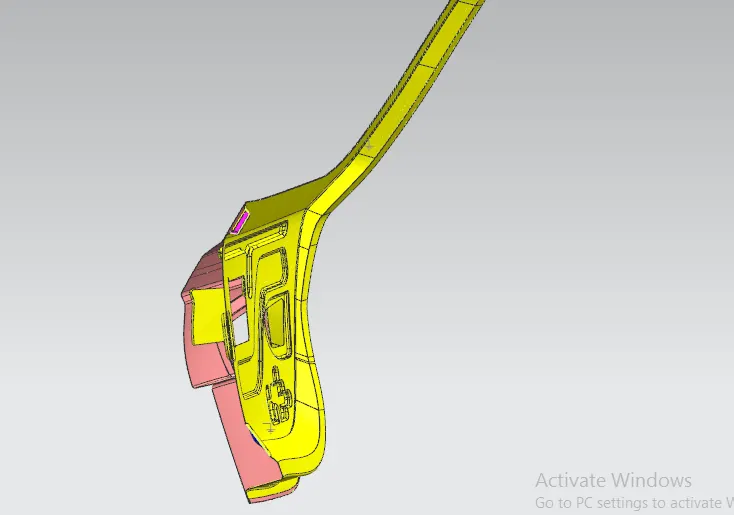
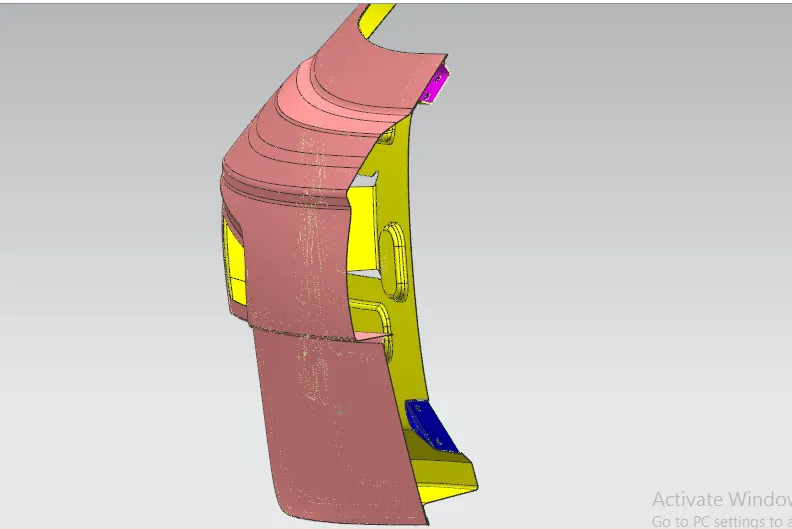
Design of backdoor
BACKDOOR CHALLENGE
OBJECTIVE
- TO CREATE PROPER STYLING SURFACE WITH THE GIVEN CLASS A SURFACE
- CREATE THE SEALING FLANGE WITH RESPECT TO THE INNER PANEL.
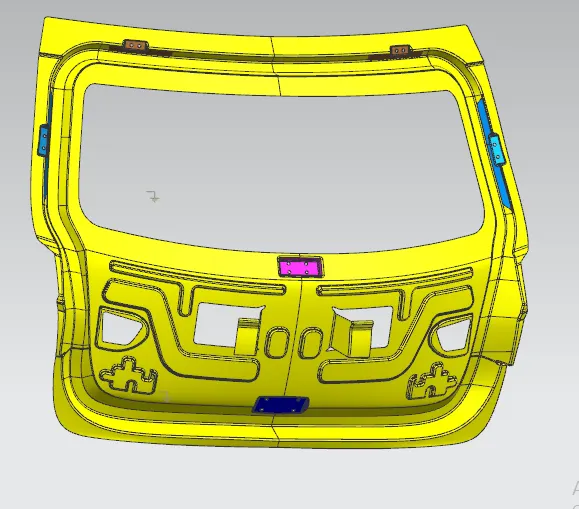
- PROVIDE THE EMBOSSES FOR THE GAS STAY,WIPER MOUNTING,HINGE AND LATCH &STRIKER.
- CREATE SEPARATE PARTS FOR THE REINFORCEMENTS.
- DRAFT ANALYSIS OF THE PANEL.
- HEMMING OPERATION FOR CONNECTING OUTER TO INNER PANEL.
- HEMMING RELIEF AT THE EDGES.
- THICKENING OF THE COMPONENT.
BACKDOOR
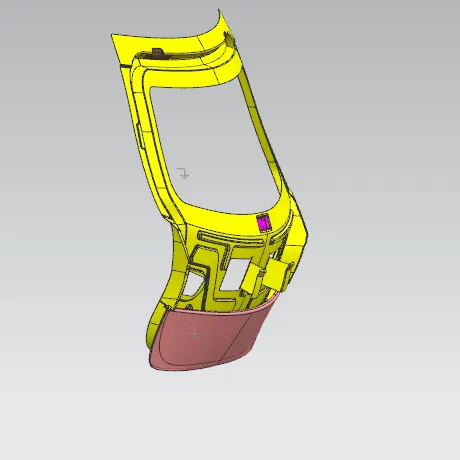
A car backdoor is similar in functioning as to the basic door which is responsible for opening and closing operation.A car backdoor is the gateway towards the luggage compartment of the vehicle.The caar backdoor comprises of the outer panel ,inner panel and sealing flange.
The space of the luggage compartment is governed by the size of the inner panel of the backdoor and its design specifications.Backdoor are one of the type of door of the vehicle which are located next to the passanger seat which provides access to the luggage compartment. In the most of the cars, these back door are operated with the help of gas stay which in turn reduces the effort required to lift the door.
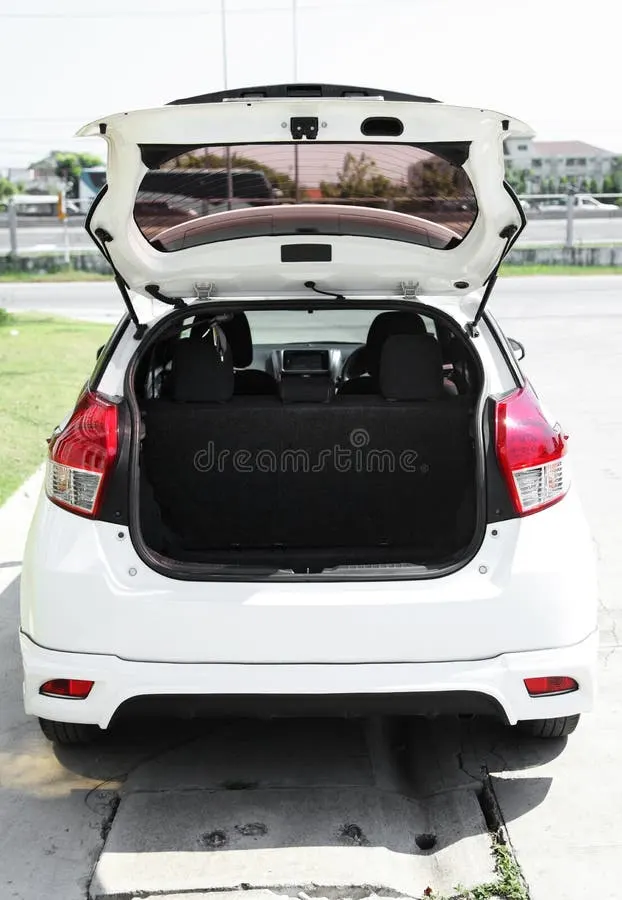
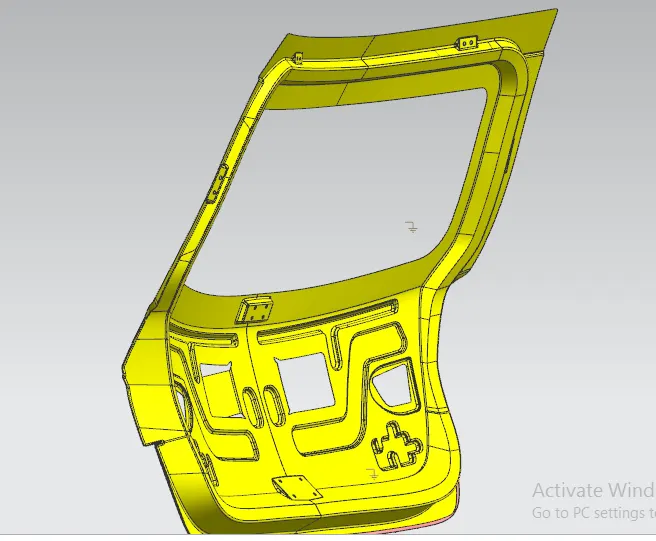
- INNER PANEL- The inner portion of the backdoor is the inner panel or the functionality like strengthening of backdoor, embosses for various mountings is carried over the inner pane of the backdoor.The backdoor inner panel is joined by sealing flange with the upper panel and also mastic sealant is there bewteen the center portion of the panels.The panels are also connected or joined by means of hemming.
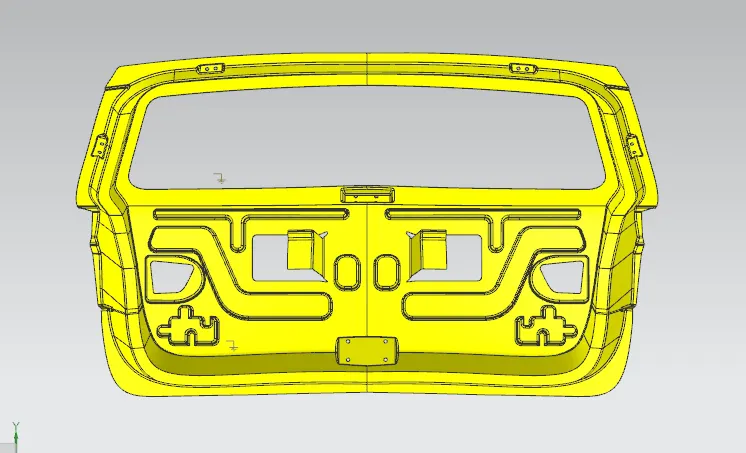
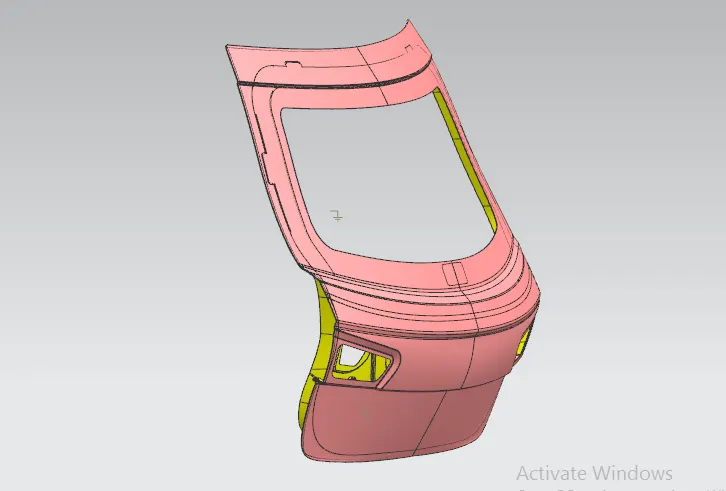
- OUTER PANEL-The outer panel is the aesthetic surface where you cannot create any of the embosses or any other feature than styling surface, it is connected with the inner panel through mastic and hemming operation.
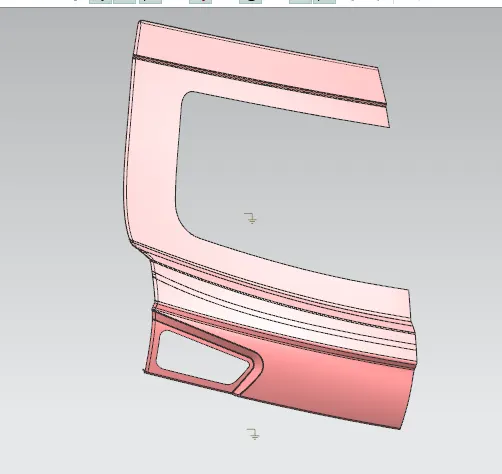
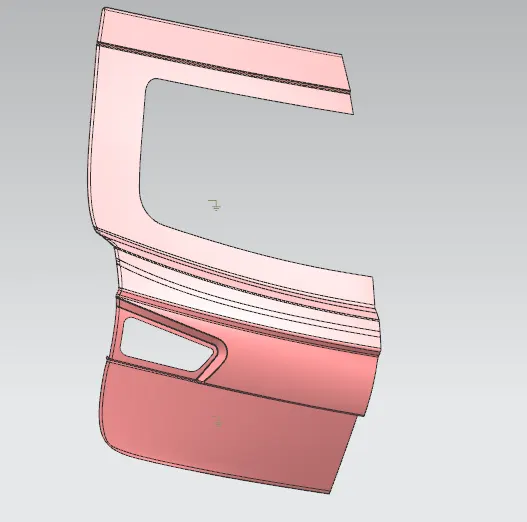
- SEALING FLANGE-It is the flange between the outer panel and inner panel.the seal fits over the sealing flange , so while creating any embosses make sure it doesnt affect the sealing flange and seal can be fitted precisely,the sealing flange is created by offsetting the outer panel by 25mm- 70mm for both upper and lower sealing flange.
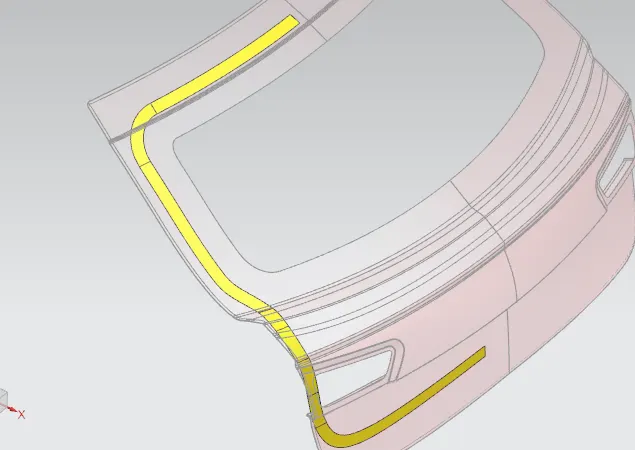
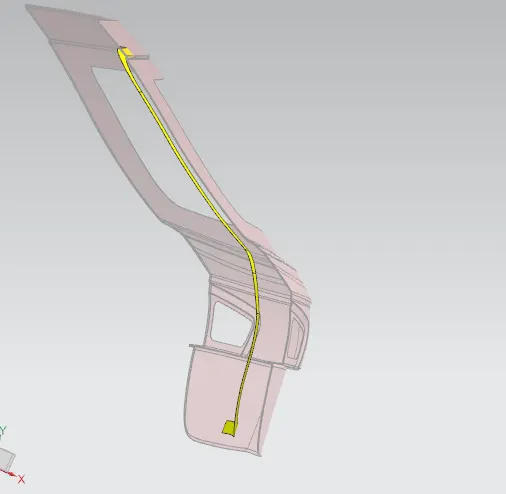
EMBOSSES AND REINFORCEMENT
EMBOSSES ARE GIVEN TO STRENTHEN THE COMPONENT AND IT SERVES THE DISSIPATION OF THE ENGERGY AT THE TIME OF CONTACT OR COLLISION.
1)EMBOSS ON LOWER INNER PANEL
The y-emboss and v emboss are given to disssipate the impact engery away from the vehicle at the time of the collision,the cut-out cannot be given directly over the inner panel as it loosens the strength of the inner panel, so we provide the emboss first and made cut-out for the assembly of the light mounting over the panel.
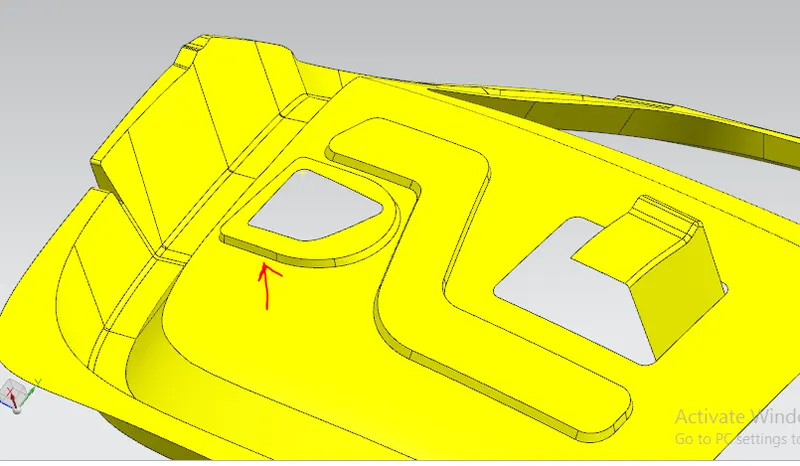
2)EMBOSS FOR THE HINGE MOUNTING
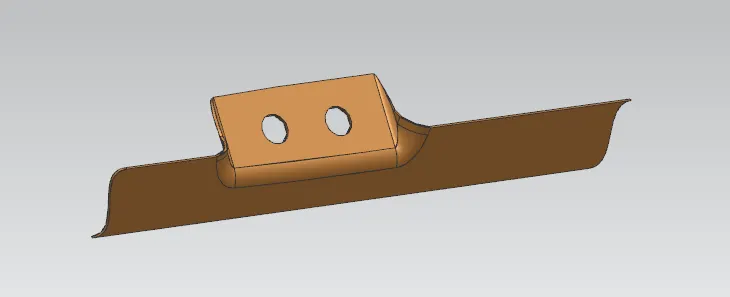
The hinge is the component which is responsible for the opening and closing action of any door of the vehicle, hinge emboss is given on the inner panel outer side, without disturbing the sealing flange as proper space must be provided in order to apply seal over to the flange.There are two hinges installed in the backdoor inner panel for working.
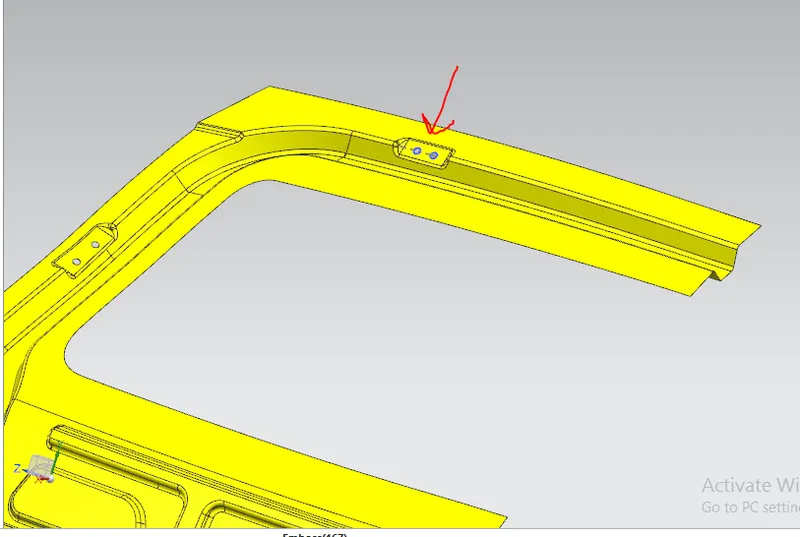
3)EMBOSS FOR THE GAS STAY
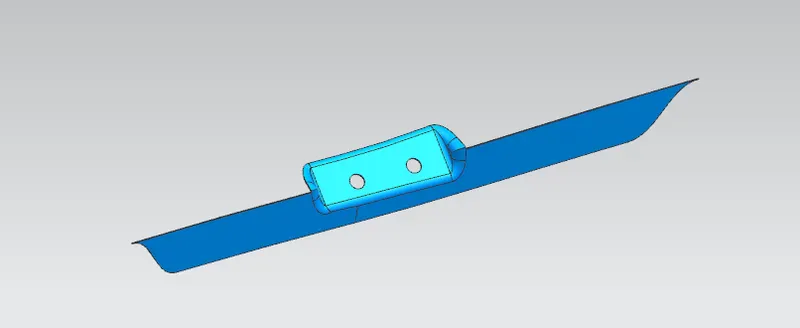
The motion of the door is governed by the gas stay installed over the inner panel, the embosses are created for mounting of the gas stay, the gas stay system is generally preffered in order to reduce the cost of the vehicle and few vehicles are incorporated with automatic control over the key.
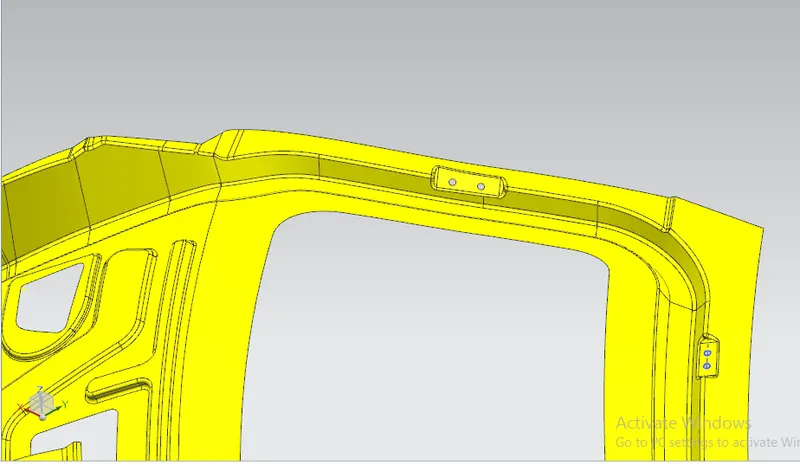
4)EMBOSS FOR THE VIPER MOUNTING
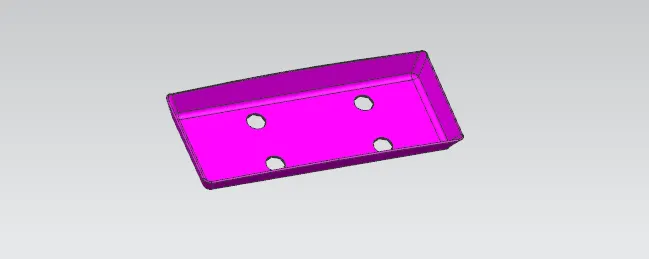
The viper motor need to be installed in the inner panel so emboss is required in the inner panel for the mounting of viper motors.
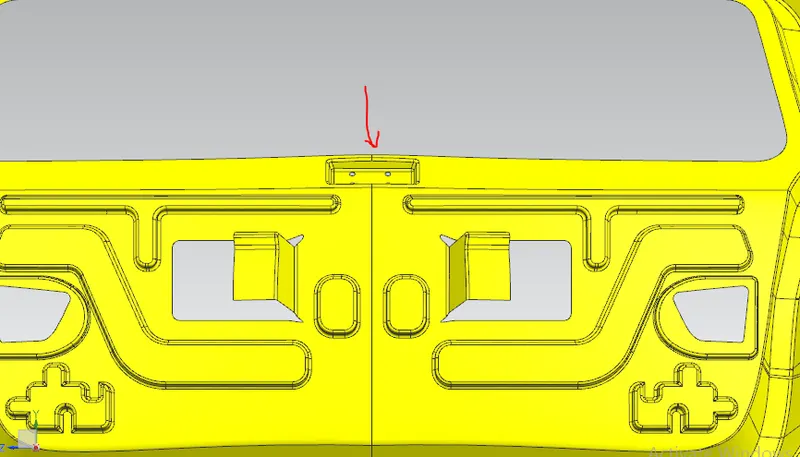
5)EMBOSS FOR LATCH AND STRIKER
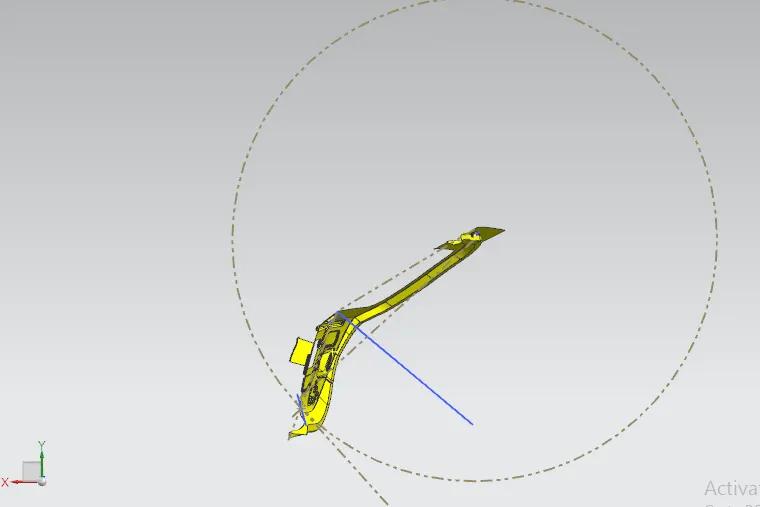
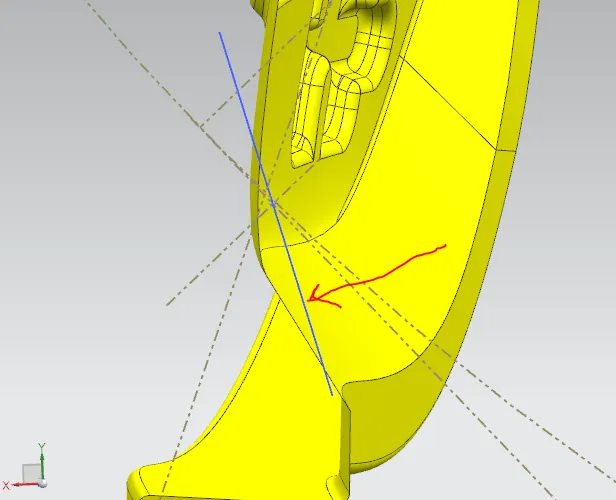
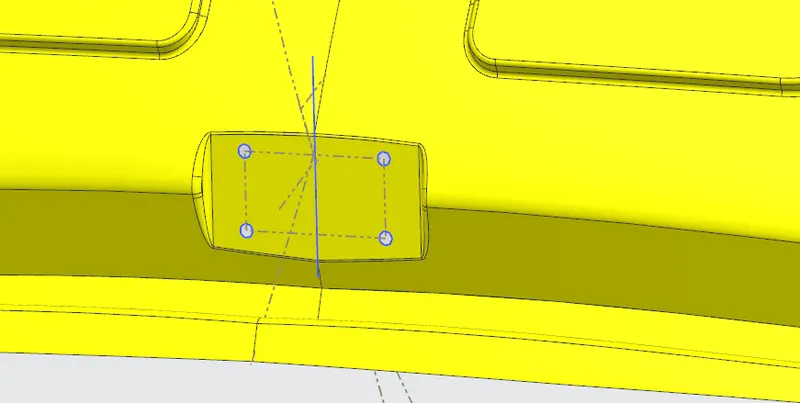
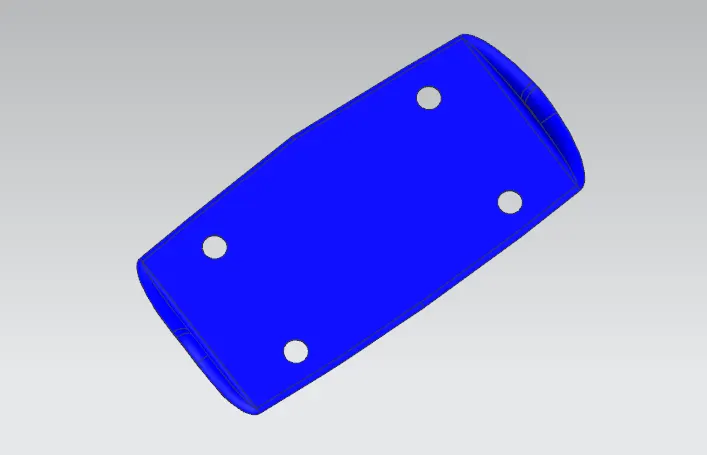
The striker emboss is required in order to mount the striker , the striker in mounted in relation with the hinge axis, the circle is created from the mid point of the hinge axis and 45 degree line is created from the tangent and perpendicular line.
REINFORCEMNETS ARE GIVEN FOR PROVIDING EXTRA STRENGTH
1)HINGE REINFORCEMNET
2)GAS STAY REINFORCEMENT
3)VIPER MOUNTING REINFORCEMENT
4)LATCH AND STRIKER REINFORCEMENT
HEMMING OF THE OUTER PANEL.
Hemming is a sheet metal forming process in which sheets are joined by bending it to 180°. Automotive body panels and automotive parts such as deck-lids, trunk-lids, doors, hoods and tailgates are formed by hemming process. In this process, usually a sheet is bent with the help of inner sheet in three different stages.
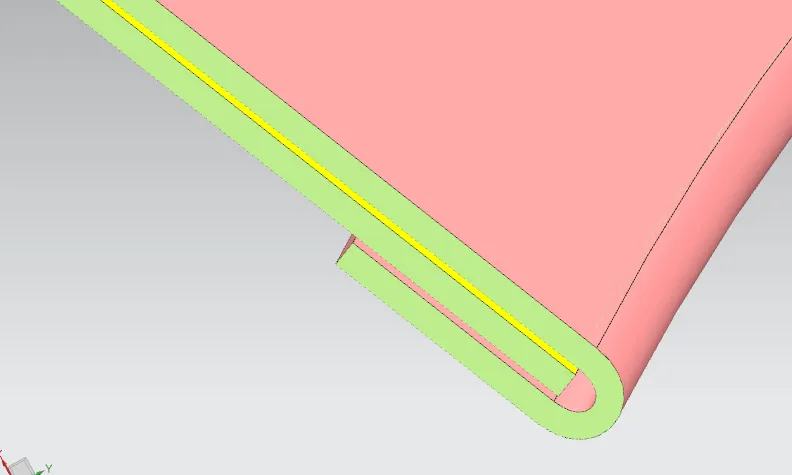
hemming relief is provided at the corners.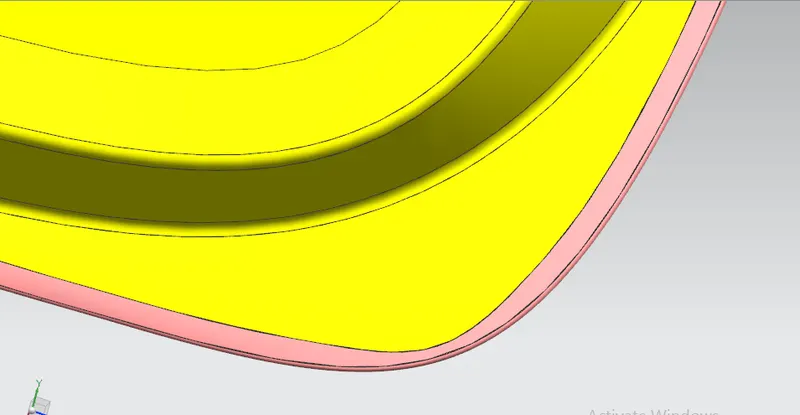
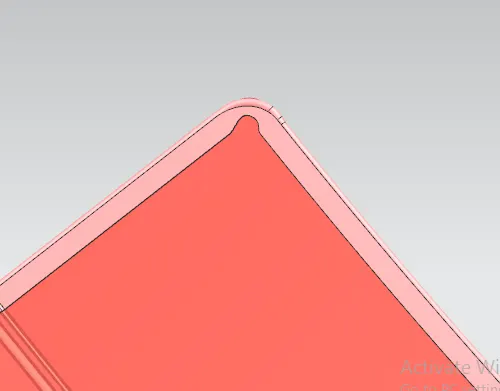
MASTIC REGION
Mastic is commonly used on construction projects as an adhesive and sealant. It is a popular choice where one surface needs to be adhered to another in a durable bond, or where the area needs to be protected
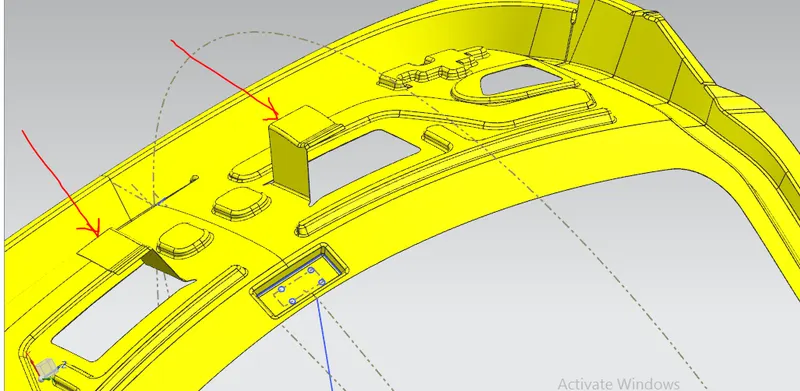
DRAFT ANALYSIS OF THE COMPONENT
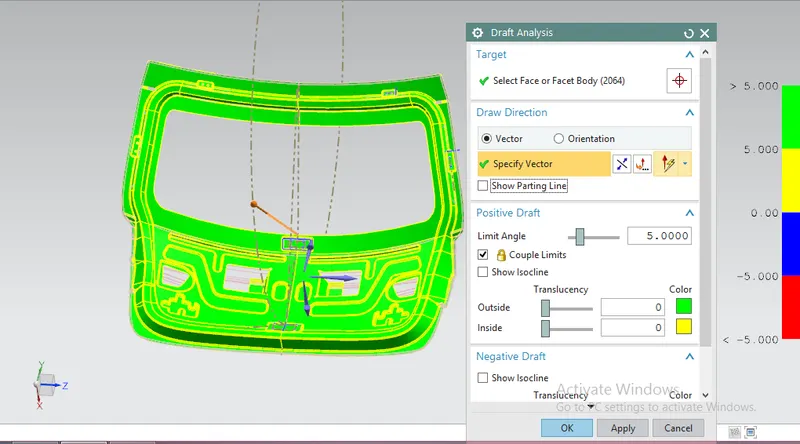
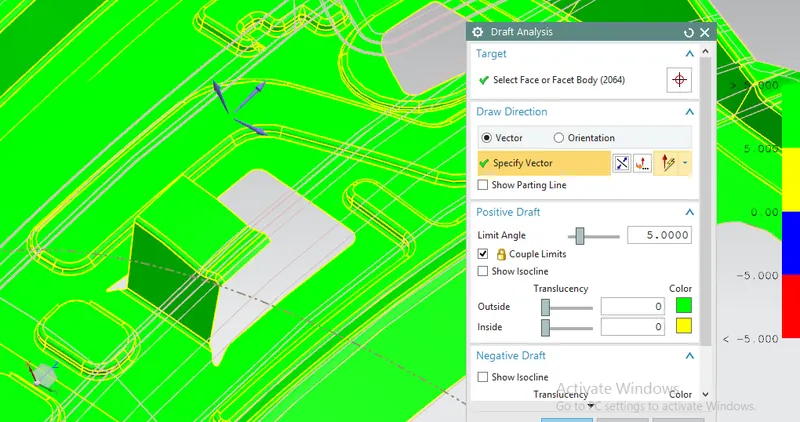
VIEW OF BACKDOOR