Design of backdoor
Design Back Door(Tail gate) Inner Panel, Outer Panel(upper and Lower), Creating Sealing flange, Embosses, Reinforcements and Perform Draft Analysis
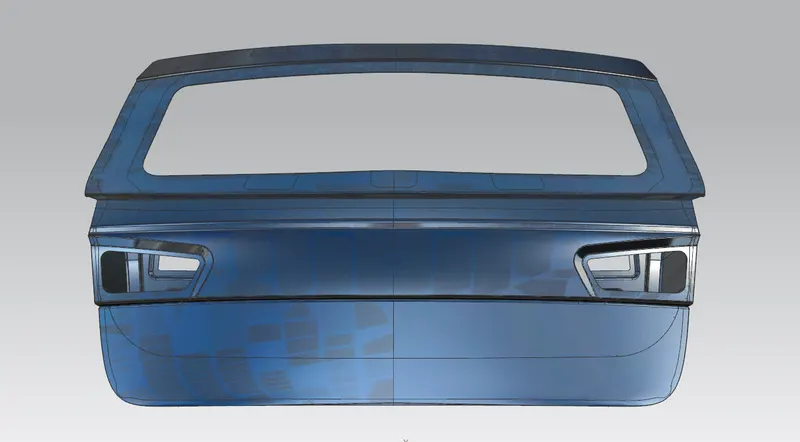
Back door is also known as Tailgate and important Biw Closure component, The Design of Back door is very important because of Rear Visibility Criteria, Support structure like Hinges and Gas stay, Mounting for viper motor, tail lamps, Boot space, Fit and clearance.
Objective-To Design Back Door Inner panel,Outer panel(upper and Lower) Using Styling Surface, Creating sealing flange, Embosses, Reinforcements and perform draft analysis.
Software Used-Siemen NX CAD
Major Parts of Back Door
- Inner Panel
- Outer Panel(Upper & Lower)
- Reinforcements
- Embosses(Hinges, Latch, Wiper motor, Gas stay embosses)
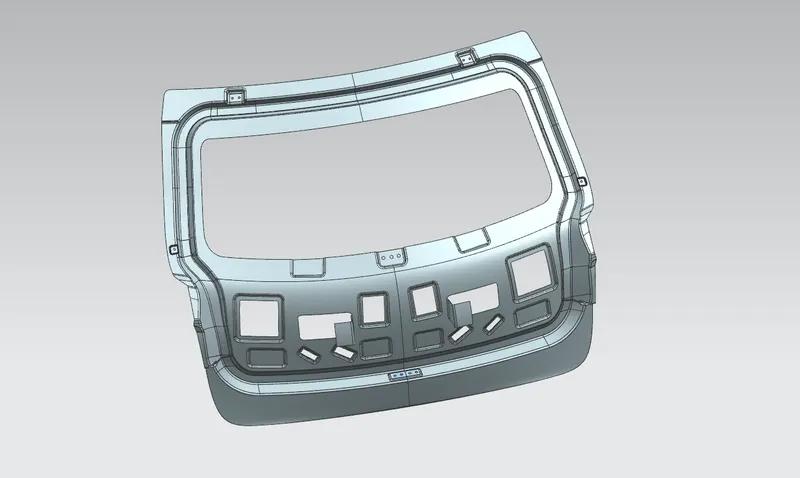
Inner Panel-The Inner Panel is made from part file of Outer panel upper which is a styling surface and Has Good Aesthetics, First I make Sealing flange(It is a flange which prevents Entering of liquids inside the car) of Inner panel then Embosses is created to increase Strength of panel, Hinges emboss, Gas stay emboss, Latch striker emboss and Wiper motor emboss is Created also hole is created for Mounting.Thickness of 0.75mm is provided and Tooling axis is created to Check draft analysis.
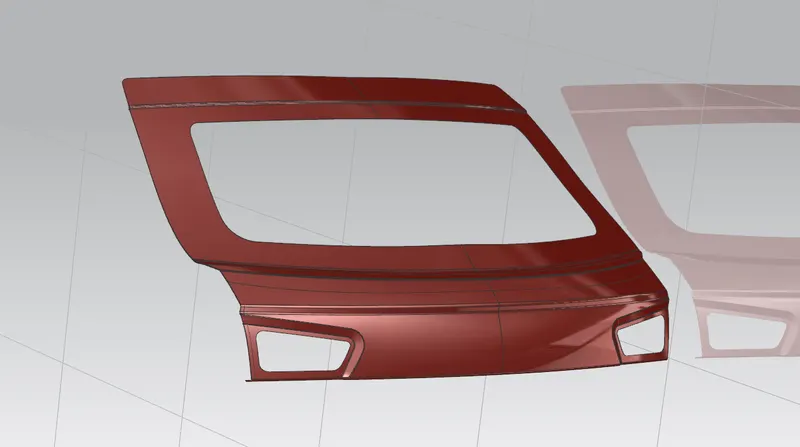
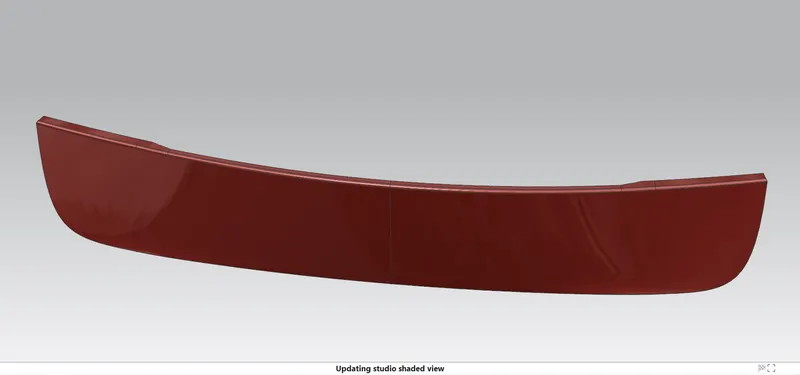
Outer Panel-Outer panel of Back door has good aesthetics and styling surface so It is not possible to Join it by Spot weld method Because It Affects the Aesthetic of panel, The thickness taken is 0.75mm. It is hemmed with inner panel by Hemming Process.
Upper part Lower part
Reinforcements
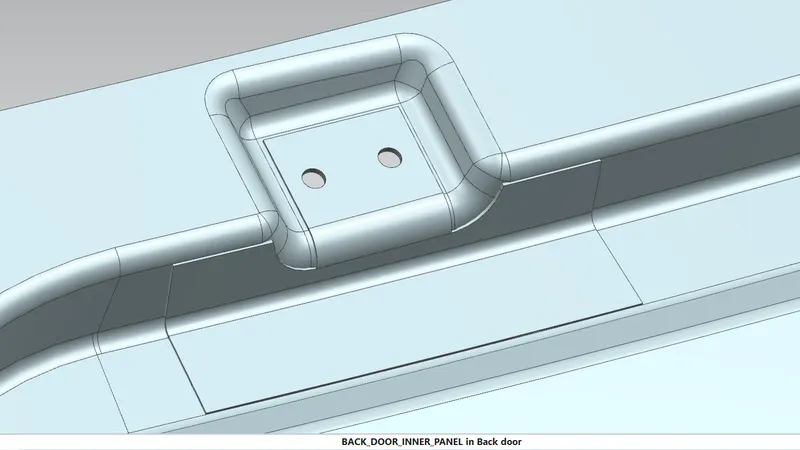
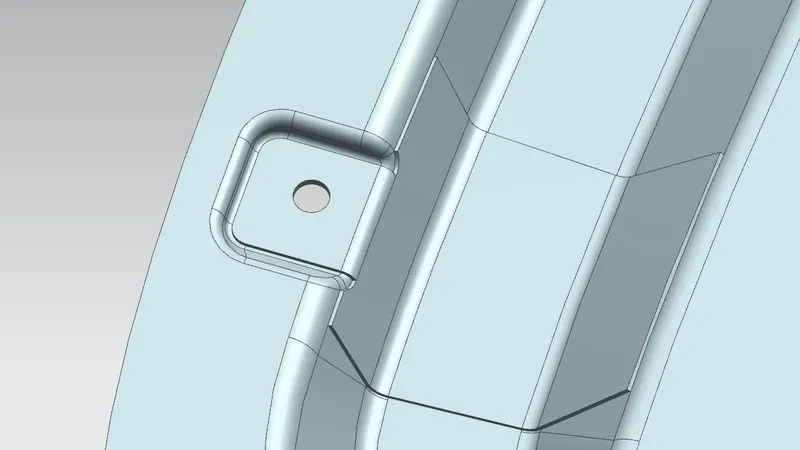
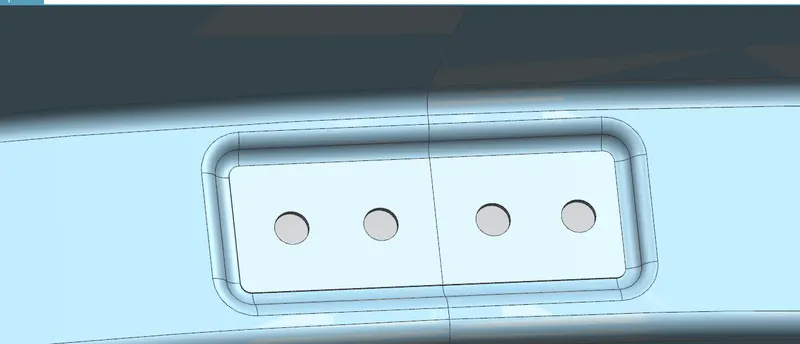
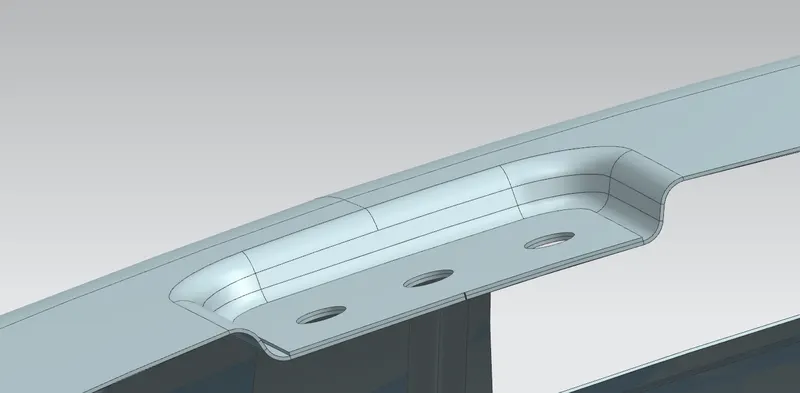
Reinforcement is provided for local strenthening the parts, It is provided on Hinges emboss, gas stay emboss, wiper motor emboss and latch embosses. the thickness of 1.5mm is given for Reinforcements.
Hinge Reinforcement
Gas stay Reinforcement
Striker Reinforcement
Wiper Motor Reinforcement
Embosses-Emboss is a feature in Nx cad which is given on Sheet metal parts to Increase the strength. A V and Y shape emboss helps to deviate force outside the panel when vehicle collide.
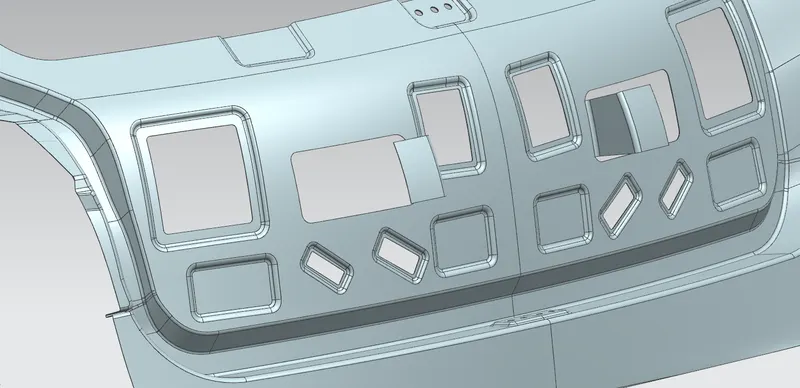
Here I Create more embosses to get better strength
Mastic Sealants- A mastic sealant is applied to Join panels, Because outer panel has Good Aesthetics and also styling surface so we did not apply spot welds to join.I create Flanges and embosses which is joined by mastic sealant which is 5mm minimum distance.
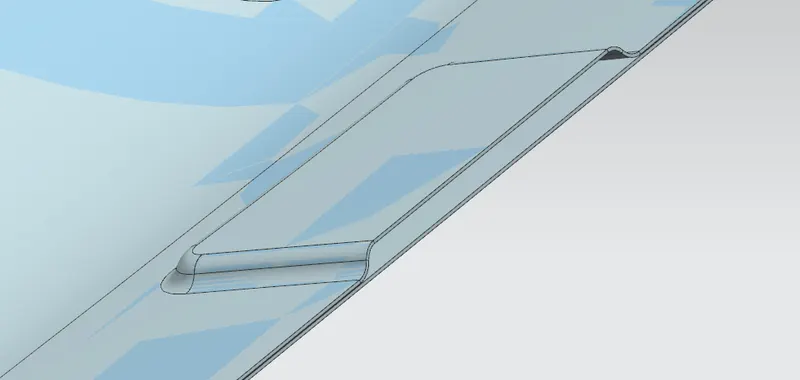
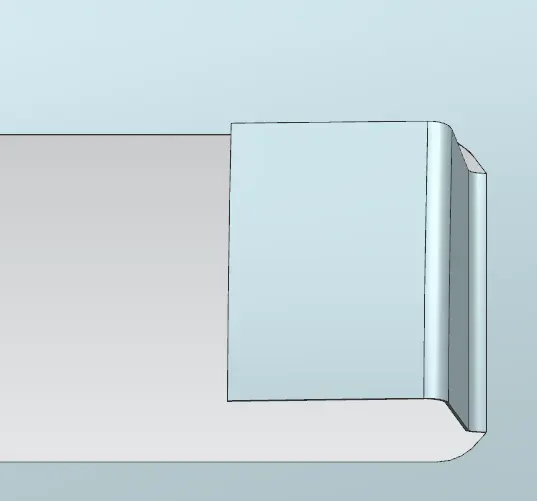
MANUFACTURING METHODS
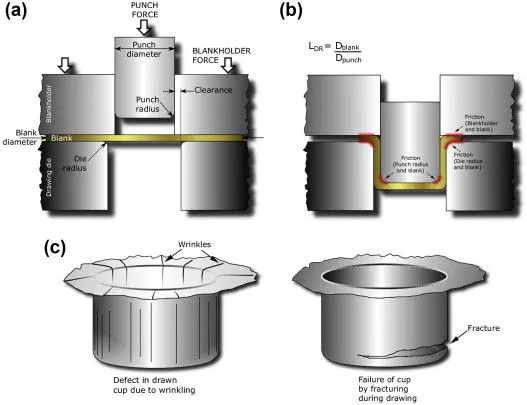
Deep Drawing-Deep drawing is a sheet metal forming process in which a sheet metal blank is radially drawn into a forming die by mechanical action of punch. It is thus a shape transformation process with material retention. The process is considered "deep" drawing when the depth of the drawn parts exceed its diameter.It is used in various industry like packaging industry, automotive industry, aviation and construction industry.
Hemming-Hemming is a technology used in the automotive industry to join inner and outer closure panels together (hoods, doors, tailgates, etc.). It is the process of bending/folding the flange of the outer panel over the inner one. The accuracy of the operation significantly affects the appearance of the car’s outer surfaces and is therefore a critical factor in the final quality of a finished vehicle.
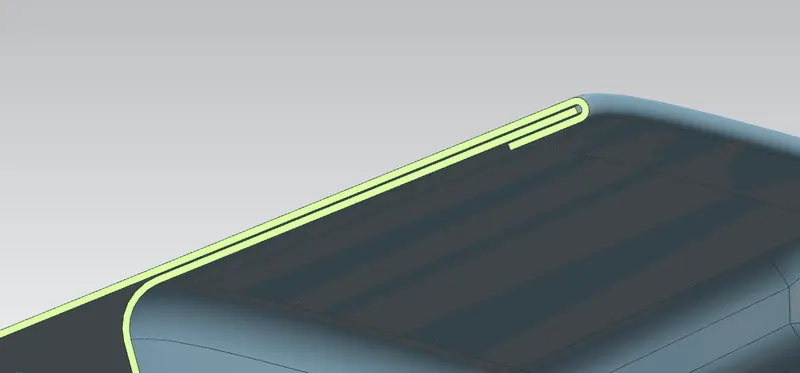
Process of Hemming
- Conventional die hemming
- Roll hemming
- Press Hemming
- Table top hemming
Press Hemming
Hemming presses are widely used in automotive manufacturing for hemming of sheet-metal body components. The process uses traditional hydraulically operated ‘stamping presses’ to hem closure parts, and, being the last forming process in stamping, it largely determines the external quality of such automotive parts as doors, hood and trunk lid.
Table top hemming
Tabletop hemming machines are utilised for the manufacture of medium to high production volumes, with the ability to achieve cycle times as low as 15 seconds.
Robot(Roller Hemming)
Robot hemming is utilized for the manufacture of Low to medium production volumes. It uses a standard industrial robot integrated with a roller hemming head to provide a flexible method for forming closures. The flange of the outer panel is bent over the inner panel in progressive steps, by means of a roller-hemming head.
One advantage of this process is that it can use the robot-controlled hemming head to hem several different components within a single cell. Another is that minor changes or fluctuations in panel-hemming conditions can be quickly and cost-effectively accommodated. If equipped with a tool-changing system, the robot could serve a variety of additional functions within the same assembly cell, such as operating dispensing equipment for adhesives and sealants, or carrying out panel manipulations, using a gripper unit.
In Conventional die hemming, the flange is folded over the entire length with a hemming tool.
Relief-A Relief is given on Corners of Upper Outer panel and Lower Outer panel to reduce Stress generated during hemming.
Outer panel upper
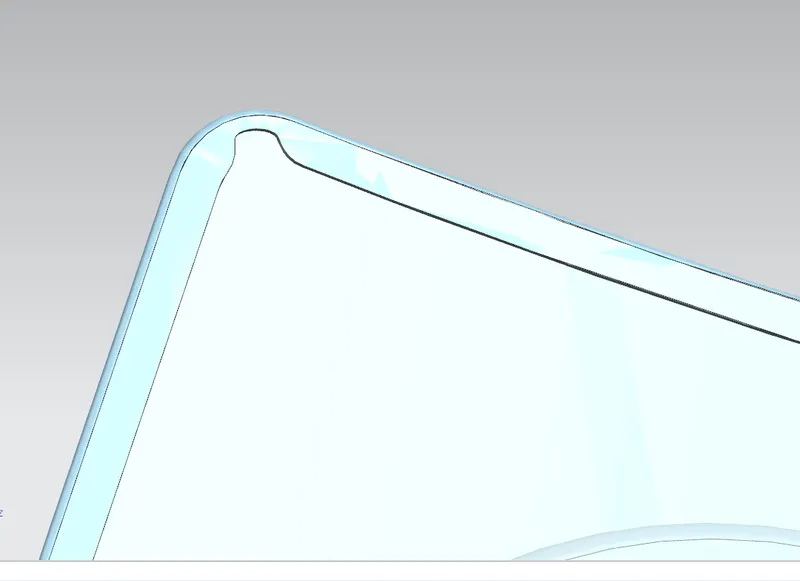
Outer panel Lower
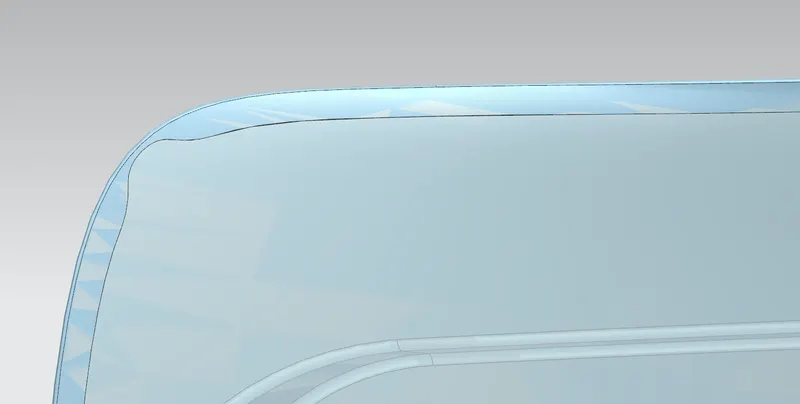
Draft Analysis-Draft analysis is Very important to check if Parts we created is Manufacturable or Not, There are 4 Criteria Green, Yellow, Blue and Red. If Our parts Comes Under Green then It is safe and can be Manufatured, If comes yellow we consider It in some cases but if Blue and Red comes then No chances. The angle we take for Analysis is 7degree. and I do draft analysis on two tooling direction.
Direction 1
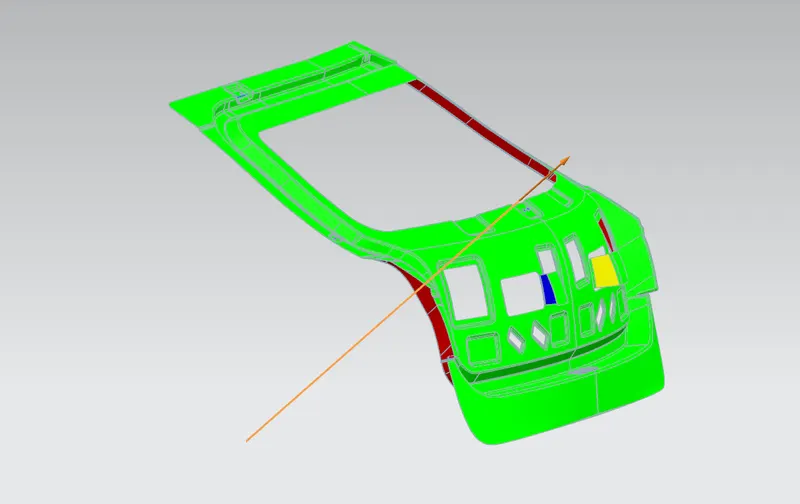
Here I use this tooling direction for draft analysis, the upper part is manufactured using this by Deep drawing method, I get all green portion so my ready for manufacture.
Direction 2
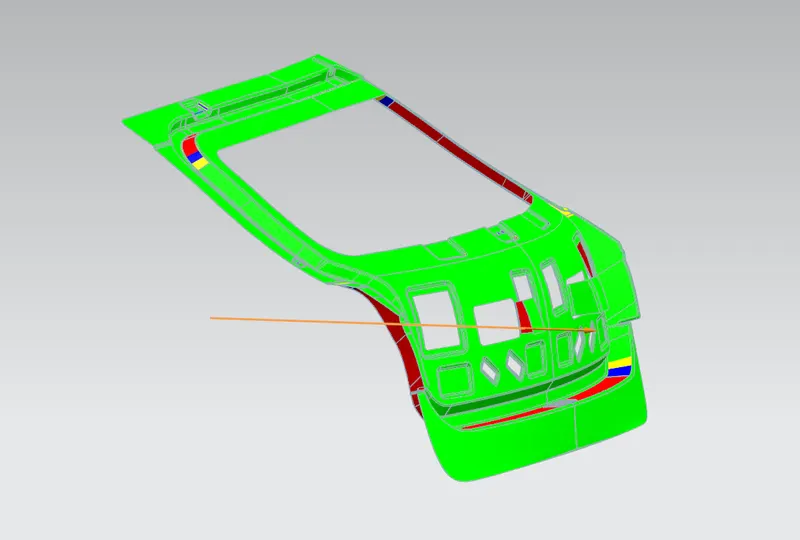
This direction is for Lower portion, in which Embosses, Flange, sealing flange comes. I apply draft analysis and get Green potion on all embosses Blends so this parts also manufactured.
Conclusion-Design of Back door completed successfully, In which Inner panel is designed(embosses, Sealing flange, and Reinforcement is created), Outer panel is joined with inner panel using Robot hemming technology, Thicken of 0.75mm is provided also Relief and draft analysis is perform.