Master Section Development
Master Section Development
Aim:-
To Design B-Pillar Through Master Section Development And Write a Detailed Report.
Given:
- A-Surface
- Master Sections
- Distance Between Ribs Should Be 50mm
B-Pillar
The B-Pillar Is The Central Pillar Of The Car. This Pillar Is Actually a Sheet Metal Part Which Is Welded In The Biw Of The Car. The B-Pillar Trim Is Attached To The B-Pillar And Improves The Aesthetic Look Of The Car. Mostly The Trims Are Manufactured By The Injection Molding Process. The Design Of The B-Pillar Is Carefully Done To Make The Part Manufacturable And Usable In The Interior. While Manufacturing a Part Through Injection Molding a Lot Of Defects Can Occur On The Plastic Part Which Will Destroy The Look Of The Panel. The Design Has To Made In Such a Way That All The Errors Can Be Rectified.
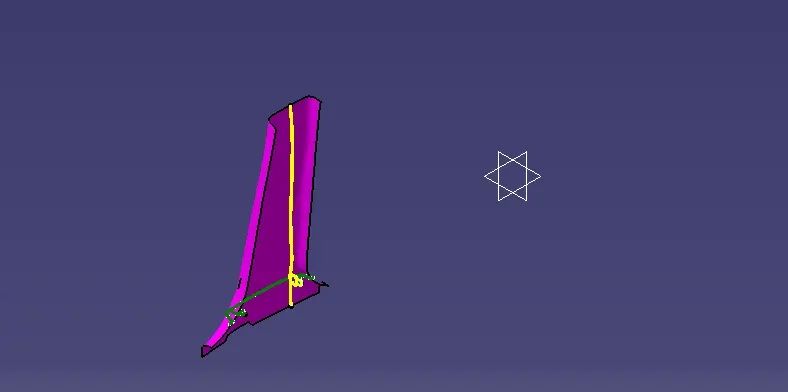
Master Section:-
- Master Sections Are The Guides For Design Requirements Which Shapes The Component After Technical Styling Of Class A Surfaces
- -The Body Frame Is Mainly Composed Of Floor Longitudinal Beams, Upper Side Beams, Door Sill Beams, And Front Cover, The Rear Beam, A-Pillar, B-Pillar, C-Pillar, And Other Load-Bearing Beam Structures Are Composed.
- Master Sections Are Parameterized Model Of The Vehicle Body That Outlines The Guide For Npd Team
- In This Report, B Pillar Cover Creation With Detailed Procedures Of Surface Development And Attachment Features Are Covered
Concept Sketches:
Concept Sketches Are Rough Idea Of Free Hand Sketch Obtained Through Styling Team And Will Be Used To Prepare The Model. It Is Usually Done Through Pen And Paper And Through The Painting Software. This Is Will Be Used To Generating The Concept For Preparing The Model By Incorporating Various Styles And Information Obtained Through The Stakeholders
Class A Creation:
After Finalizing The Concept The Sketches Are Usually Worked In Software’s Such As Auto-Desk Alias To Create Class A Surface
Tooling Axis:
The Given Class A Input Is Analyzed To Envision The Part To Manufacture And Tooling Axis Or Tooling Direction Or Die Line Is The Direction That Molds Pull Apart In Injection Molding. There Are Two Mold Pieces Names Core And Cavity. Thus Tooling Direction Determines Mold Separation And Also Becomes Vital In Developing The Plastic Product Which Is Drafted To Desired Nominal Angle For Feasible Clearance And Ejection Of Final Part From The Mold.
The Steps Followed In Creating Tooling Axis
- A Reference Point Is Created Along The Surface Zero And New Axis System Is Created
- The X Direction And Y Direction Along The Class A Were Used To Create Tooling Direction
- Finally, The Tooling Axis Is Created By Bisecting The Two Lines And It Is Published. Class A Surface As Input Using Surface Operation Commands Class B Is Developed
- The Tooling Axis Determines The Direction Of Class C Boundary Swept With Draft Direction.
- When Viewing From Tooling Direction Normal All The Parts That Are Drafted Should Be Visible So It Gives An Rough Idea To Determine Product Manufacturing In Injection Molding
- In B Pillar Model There Are Two Tooling Directions One On Main Tooling And the Other On Lifter Side That Is Used To Eject The Parts During Injection Modeling
- Lifter Axis Is Used Because The Attachment Feature Is Bounded By Close Walls
A Surface Improvement.
Before We Start Creating The Closed Body For The B-Pillar We Need To Check The Quality Of The Given A-Surface. The A-Surface Needs To Be Free Of All The Patches Or Error Elements. For This First, We Need To Disassemble The Given Styling Surface And Join It With The Merging Distance Of 0.001mm.
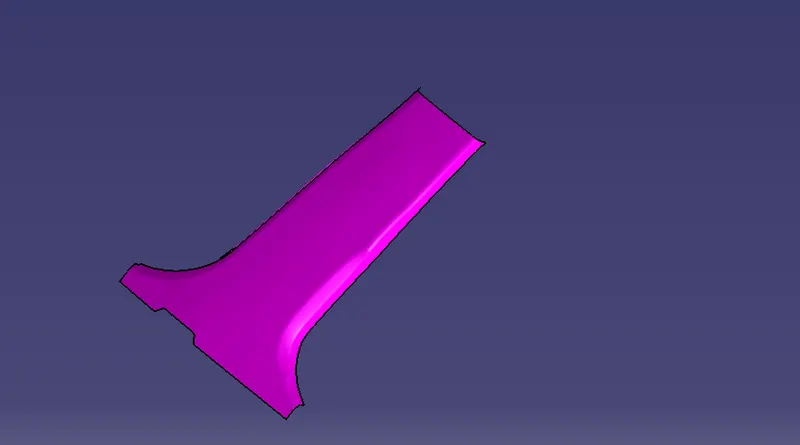
B Surface Creation
- The Next Step Is To Design B Surface For The Input Which Is Usually The Surface Where All Engineering Aspects And Support Creations Are Done.
- The B Surface Creation Is Performed Using Surface Operations In Catia Which Is An Offset From Class A With Dimension Proportional To The Thickness Of The Part
- In B Pillar Design The B Surface Is Offset 2mm From The Input Which Is The Thickness Of The Part
- The Offset Surface Leads To Surface Degenerations If Rapid Change In Curvature Or Surface Continuity
- Low Radius Of Class A
- Conic Or Styling Fillets
- The Remedy Is To Untrim, Extrapolate And Trim Or Create Surfaces Using Multi-Surface Option And Join
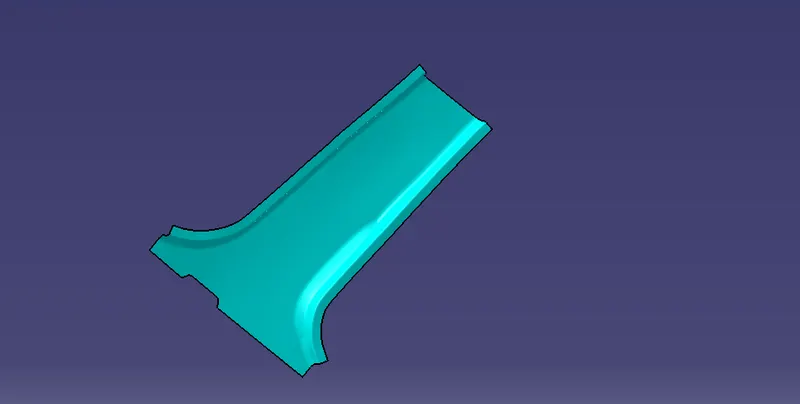
Flange Creation
-According To The Master Section, The B-Pillar Has Flanges On Both Sides. The Flanges Have To Be Included In The Design And The A And B Surface Has To Be Modified. The Surfaces Should Match The Master Section.
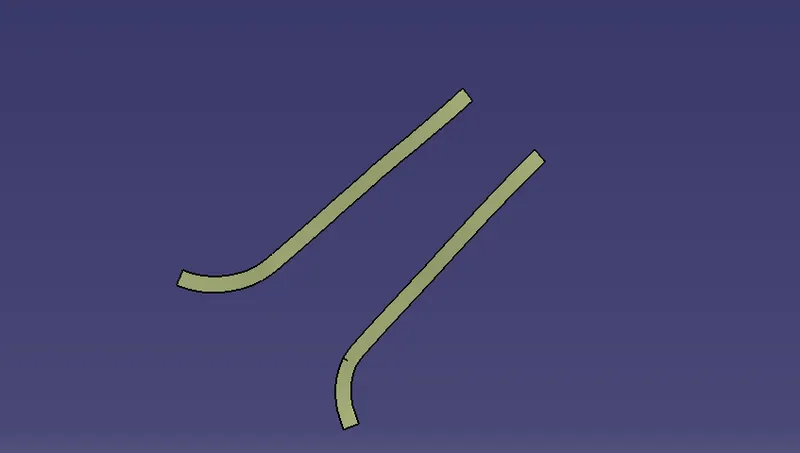
Main Tooling Axis Creation:
The Tooling Axis Is The Direction In Which The Core Moves. During Injection Molding The Core Is Moved Into The Cavity And Molten Plastic Is Injected. When This Molten Plastic Is Cooled Down Then The Core Is Moved Away From The Cavity. The Direction In Which The Core Moves Is The Tooling Direction For The Part.
To Find The Tooling Direction We Use The Master section For The Engineering Feature. Here We Take The Two Boundaries And Find a Bisecting Line Between Them.
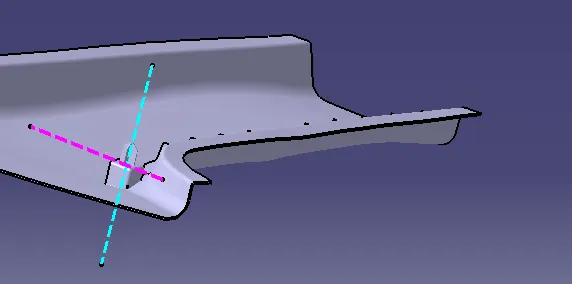
Manufacturing Feasibility Of The A-Surface (Draft Analysis):
Draft Analysis Is Used To Check The A-Surface Manufacturing Feasibility. The Tooling Axis Is Used As a Reference. Draft Analysis Checks The Angle At Which The Surface Is With Respect To The Tooling Axis. As We Know For Injection Molding The Draft On The Surface Should Be Positive And Greater Or Equal To 3 Degrees. Areas With The Draft Less Than 3 Degrees Are a Bit Difficult And Costly To Manufacture.
C Surface Creation
- The Next Step Is To From The C Surface Which Is An Intermediate Surface Between A And B And Is Used To Give The Closed Surface Appearance To The Design
- The C Surface Is Swept Using The Profile As Boundary Line Of Class A Which Is The Guide Curve With a Subtype Along Draft Direction.
- The Direction Of The Sweep Is The Tooling Direction Formed Earlier.
- The Draft Angle For The Sweep Operation Is Provided Which Is 3 Degree And Surface Is Swept For Length Above The Thickness Of The Specified Part.
- The C Surfaces Must Be Drafted Outwards From The A-Side To Avoid The Parting Line Along The A Surface.
- The C Surface Is Refined Using Smooth Curve Options To Remove The Complexity And Patches Along The Swept Surface.
- Finally, The Class A And Class C Surfaces Are Joined Together And the Connexity Of Surfaces Should Be Less Than 0.003mm And The Surfaces Are Merged.
- C Surface Merged With Class A
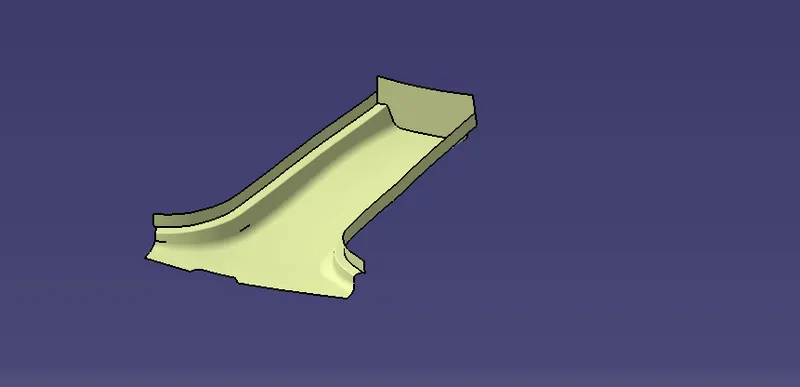
Closed Body Creation
- The Merged Surface Is Then Trimmed With B Surface To Form The Closed Surface.
- The Closed Surface Is Then Validated To Find The Irregularities Along The Edges And Imperfections Along The Edges Was Then Corrected Using Operation Like Extrapolate And Surface Trim
- This Closed Surface Is The Outer Skin And Finally The Part Is Formed By Closed Surface In Part Design Workbench
- The Final Part Is Measured To Validate The Uniform Thickness Of The Part Especially Along The Filleted Edges.
- The Uniform Thickness Ensures That The Part Created Doesn't Form Sink Mark And Flow Lines Along with Class A
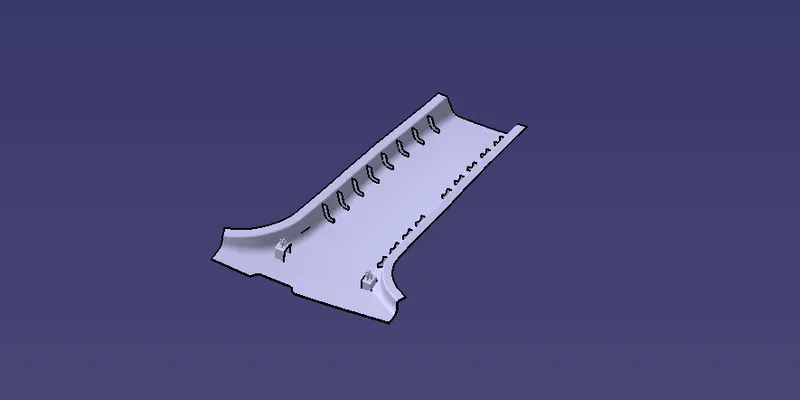
Attachment Features
The Attachment Features Are The Fixation And Location Features That Fixes The Components The Common Attachment Features Used In B Pillar Are
- Doghouse With 4 Way Locator
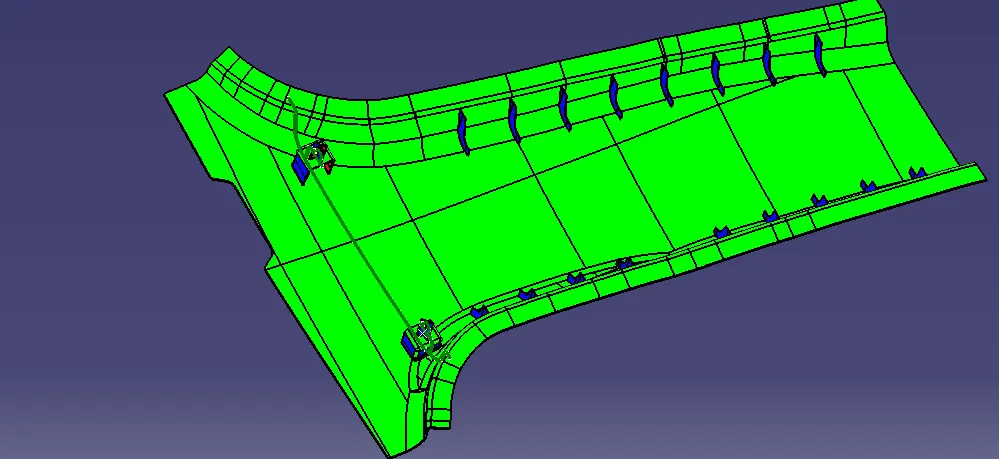
- Ribs
Doghouse
- Using The Master Section The Doghouse Is Created And Then Part Modelled Using Thickness Option
- The 4 Way Locator Is Formed Above The Dog House Which Locates The B Pillar Towards The Mating Surfaces
- The Dog House Design Rules Are
- The Thickness Of The Connecting Surface Towards B Side Should Be 40% Off The Main Thickness
- The Walls Are Drafted With Min 0.5 Degrees Along The Main Tooling Direction
- The Attachment Feature Created Needs a Separate Tooling Axis To Clear The Part Hence a Lifter Axis Is Used
- The Surfaces That Are Cleared Along The Lifter Axis Are Also Given a Minimal Draft
- The Height Of The Attachment Walls Should Be a Minimum Of 3 Mm
- This Avoids The Plastic Defects On The B Side And Maintains The Texture Of A Side
- The Dog House With Four Way Locator Are Shown Below
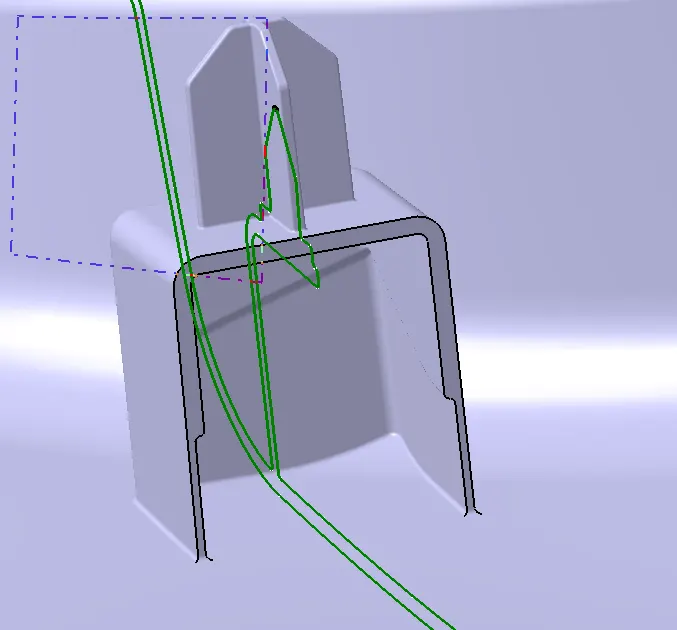
Ribs
Ribs Provide Stiffness To The Parts And Can Be To Impart Thougness Without Increasing The Part Thickness And Are Locators And Provide Alignment To The Mating Parts
Draft Analysis Procedure
- The Part Created Has To Be Changed To Material Mode In-Display Frame
- Then By Enabling Compass Definition The Axis System Is Pan Along The Direction Of The Part And Aligned In Line With The Tooling Direction
- Lock Direction Is Applied That Fixes The Compass And Then The Mode Dialog Box Is Formed By Snapping At Any Point On The Part
- The Color Codes Are Classified And Draft Angle Are Applied
- Then The Running Point Analysis Is Used To Hover Around The Part To Analyze The Permissible Draft Angles And The Analysis Is Saved
Draft Analysis Report
- The Draft Report For B Pillar Model Is Shown Below
- The Min. Draft For All A-Side Surfaces Are 3 Degrees
- The Surfaces That Are Below 3 Degree Are Shown Below
- The B Side Surface Analysis Is Shown Below
Conclusion
Thus a Tooling Axis Is Created And an Open Aesthetic Class A Surface Is Developed Into a Closed Surface With All Plastic Design Rules And a Final Part Body Is Created Out Of It In Catia Surface Work Bench. The Design Is Then Validated With Master Section And Understood The Use Of Master Section Development In Product Design Through Development Of B Pillar Cover Used In The Car Interiors.