Week 8 - Challenge 6 - Core & Cavity Design
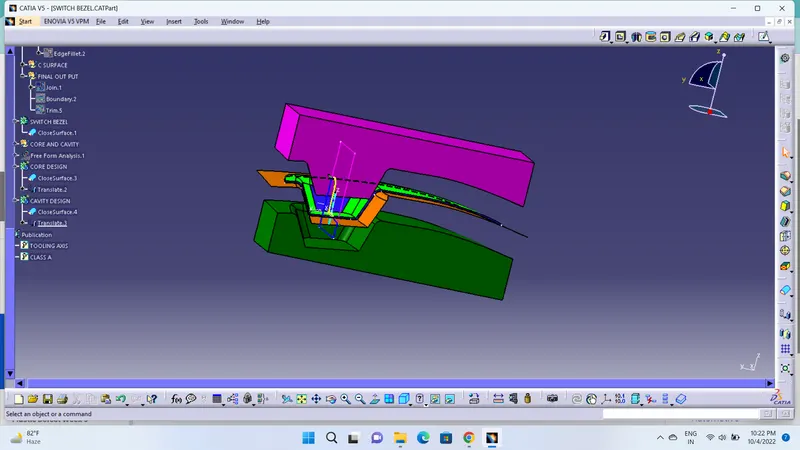
AIM :To Create the Core and cavity blocks for the switch bezel component
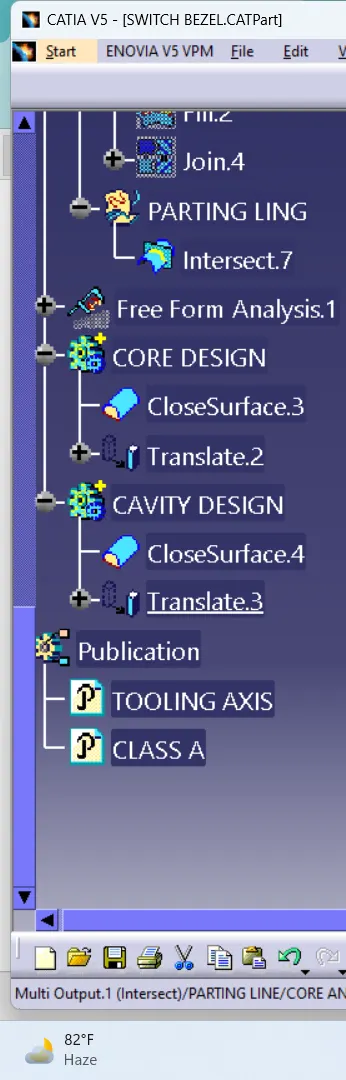
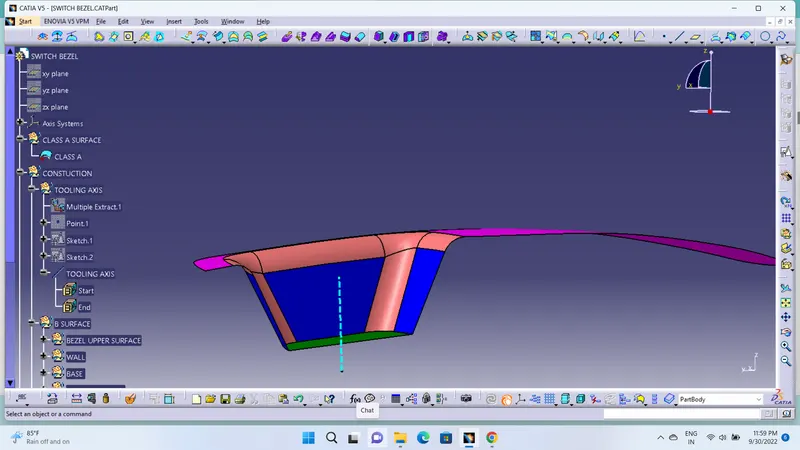
TOOLING AXIS:
The Tooling Direction is basically the direction that the mold pulls a part. The mold is built in two separate pieces, basically. You have a Cavity side and you have the Core side. The Core pulls apart from the Cavity and that's the Dye line or the Tooling Direction.
- Open the given CAT part file.
- Check for gaps between surfaces for that click on join and then preview.
- If theres any gap between the surfaces join them with a maximum tolerance of 0.003 mm.
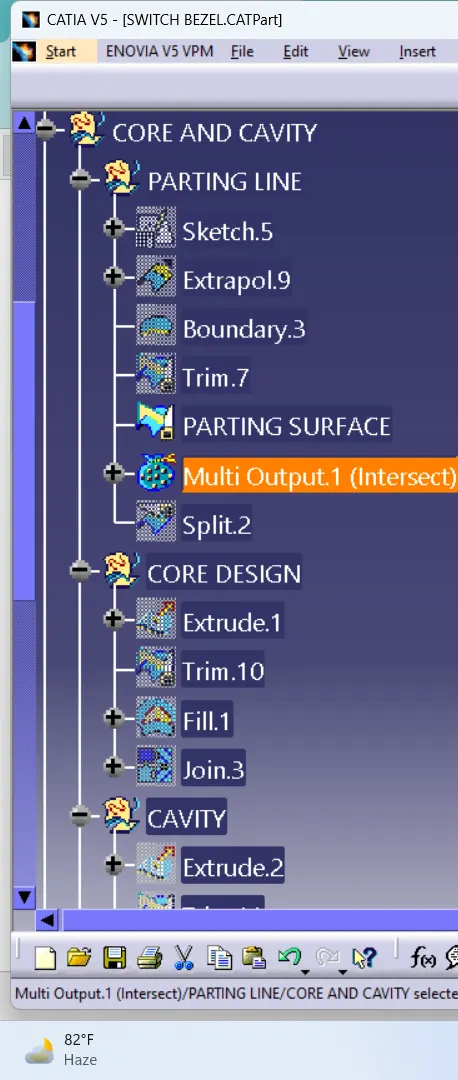
PARTING SURFACE:
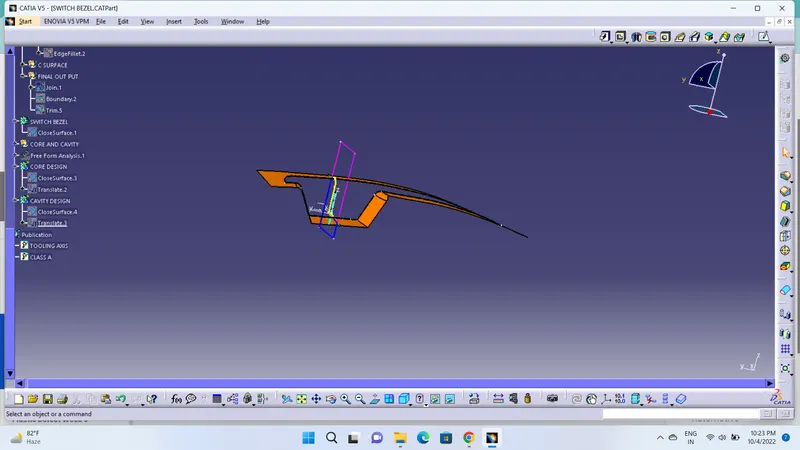
- Generally injection mold has two major components : the movable half and the fixed half, during the injecction molding process, these two halves are pressed tightly from a sealed hollow to avoid the melt flow leakage and maintain certain holding pressure, the pressed surface are called parting surface , usually parting surface are the biggest projection outline of the part.
PARTING LINE:
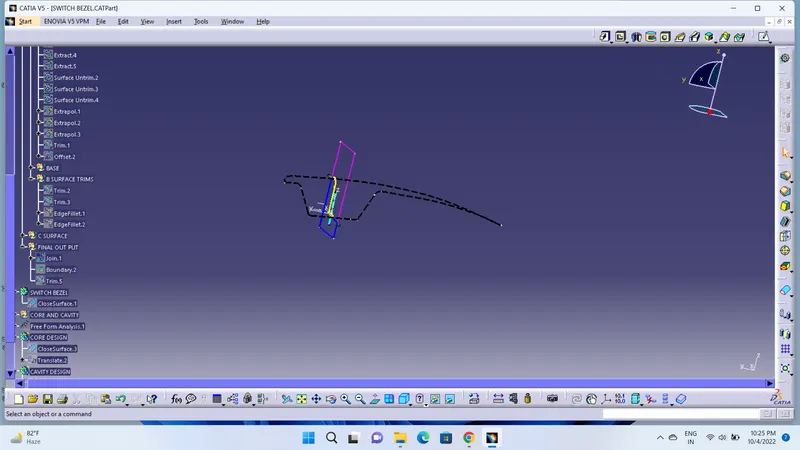
A parting line is an inevitable part of injection molded products.It is the line of separation between where two halves of a mold meet.It manifests itself on injection molded parts as a line that runs the entire perimeter of the part.In most parts, it is just a line that runs straight down the middle.
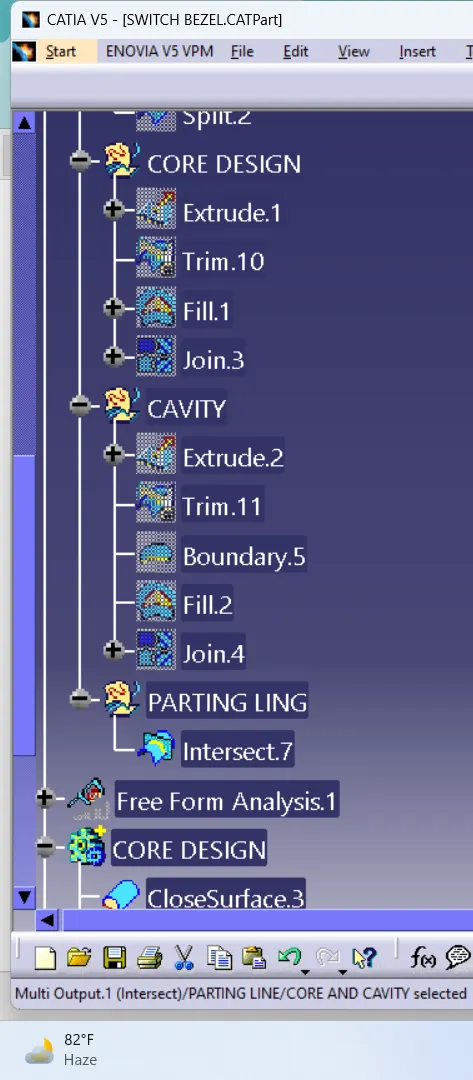
CORE:
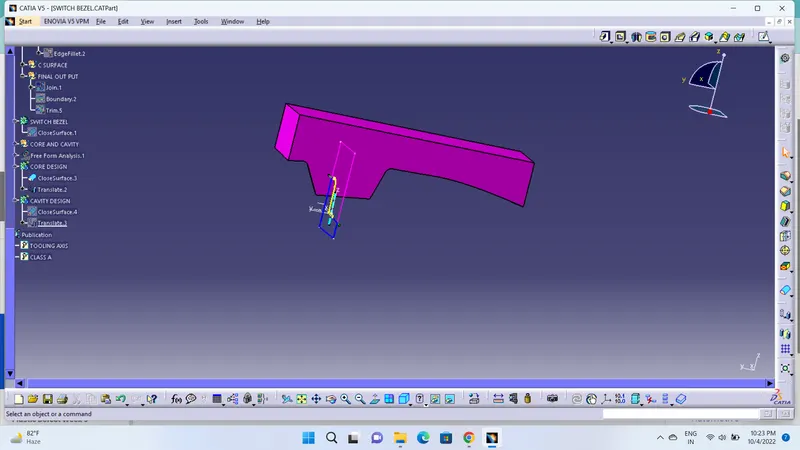
Fusible core injection molding, also known as lost core injection molding, is a specialized plastic injection molding process used to mold internal cavities or undercuts that are not possible to mold with demoldable cores.
CAVITY:
The sequence of events during the injection mould of a plastic part is called the injection moulding cycle. The cycle begins when the mould closes, followed by the injection of the polymer into the mould cavity.
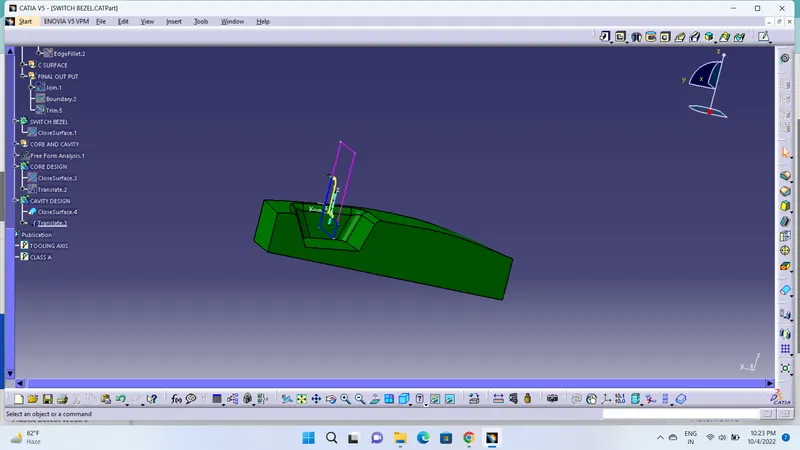
CORE& CAVITY: