Week 8 - Challenge 2 - Base Bracket Design
Introduction
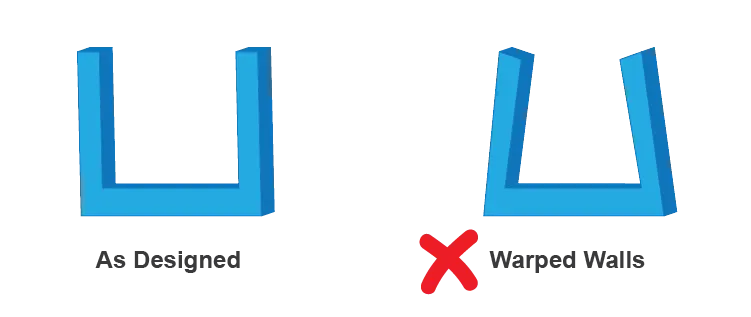
Having easier ejection from the mold may seem like a minor concern, but draft is crucial to manufacturing parts that meet your quality standard. Without draft, major problems can arise in the injection molding process that increase the time and cost of production.
When no draft is designed into the part, problems can come from friction and vacuums. These issues can damage both your part and even your mold in extreme cases. These problems are a direct result of having insufficient draft. Because plastic shrinks as it cools, portions of the part may pull away from the mold while others grip the core. If there is no draft angle that allows a simple push from the ejector pins to pop the part out of the mold, the part’s surfaces will often drag along the mold as it is being ejected. This friction between the two surfaces can cause scratches or gouges in your part and affect the appearance. This is particularly troublesome if your part is being molded with a surface finish or texture. The friction will scrape away texture and leave you with many rejected parts.
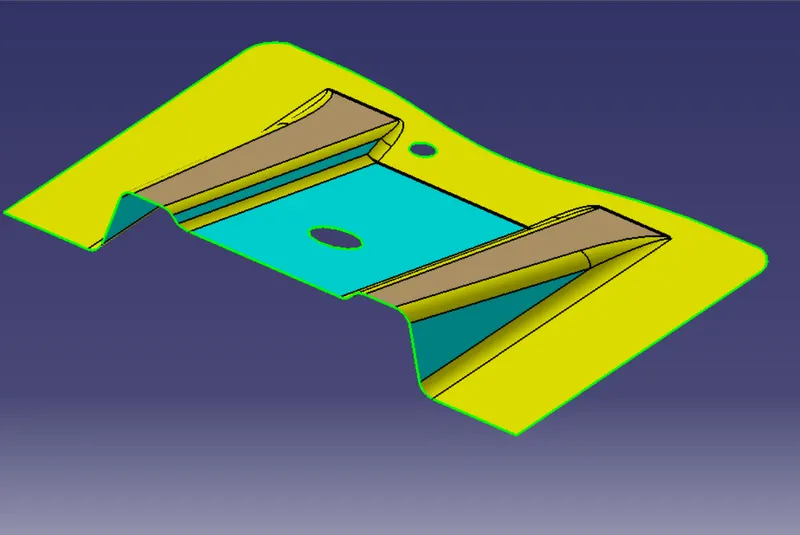
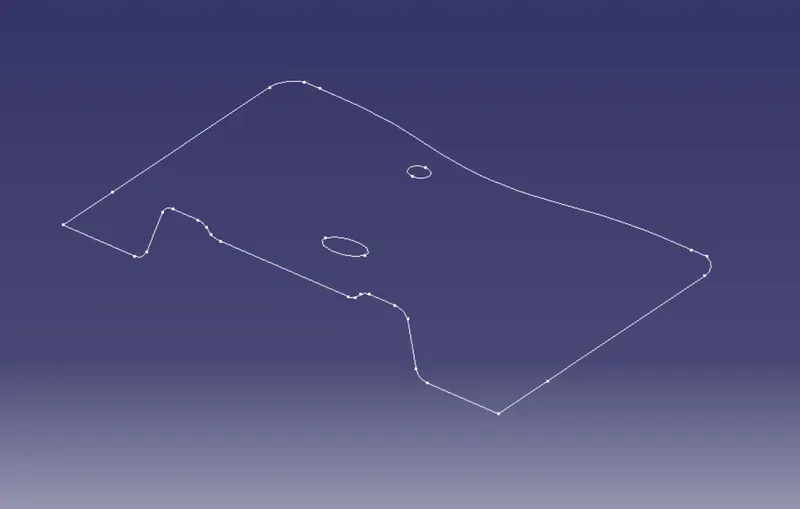
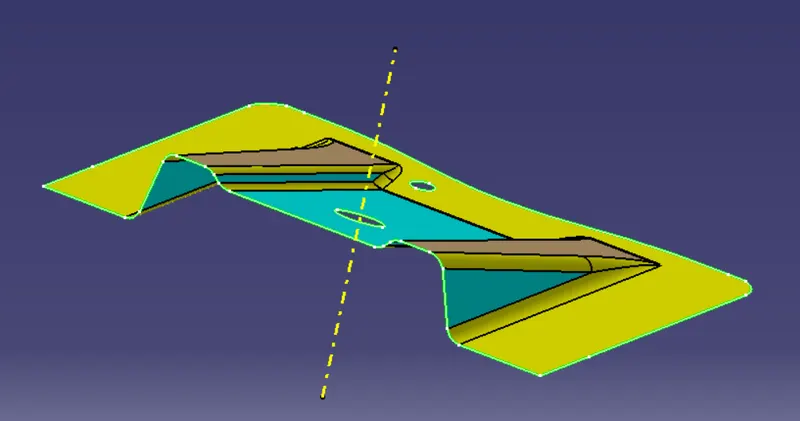
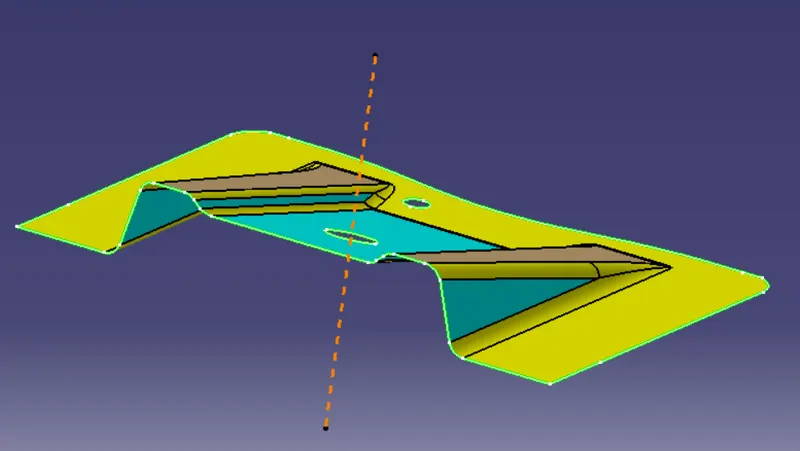
Analysis of the Class A surface
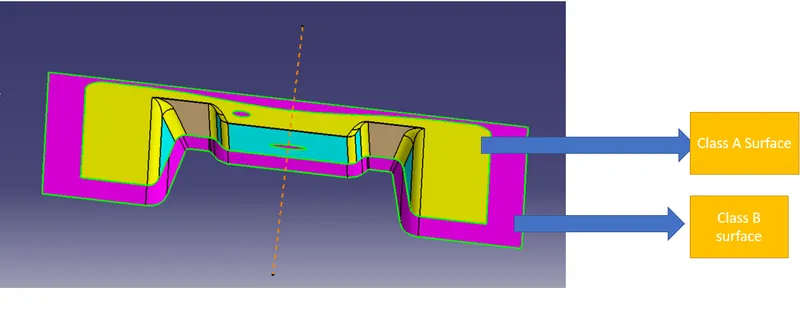
Before starting of with the designing the Class B and C surface it is necessary to check if there is any undercut and also if proper draft is given to the given class A surface
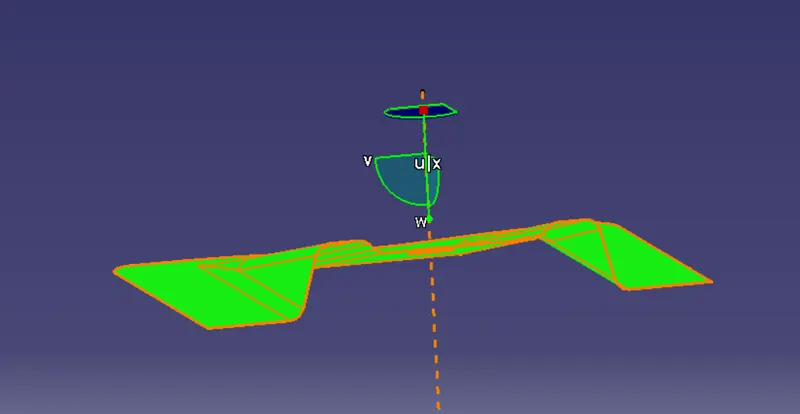
Creation of class B surface
considering the thickness of the component 2.5 mm we offset the Class A surface to 2.5 mm neglecting the fillets as fillets causes problems during thickening and also do not form a smooth surface
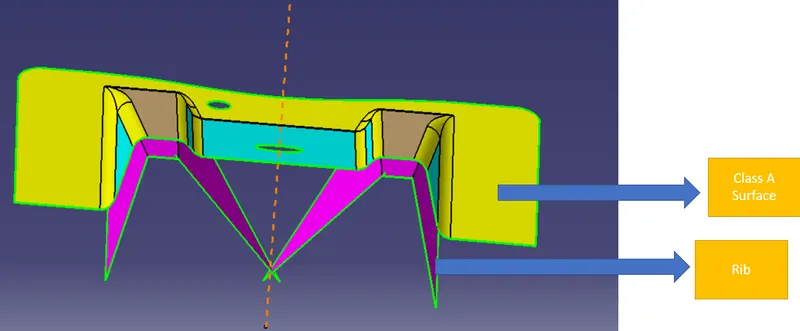
Class B Rib
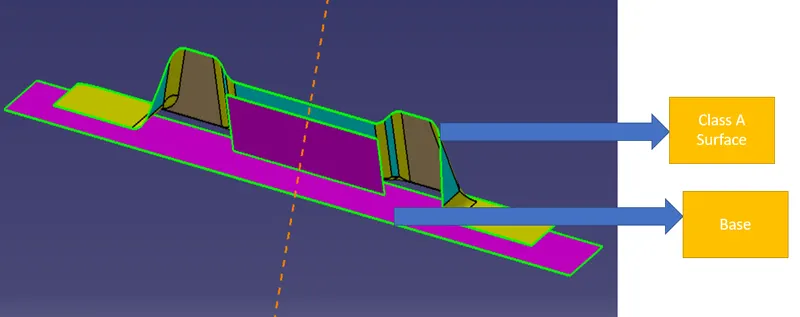
Class B base
After the Final trim and fillets of Class B surface
The fillet provided on the class B surface has certain calculation in order to maintain uniform thickness of the product.
example say The class A surface fillert radius is 3 mm the corresponding fillet at class B should be 3±(the offset value)
Defects of non uniform thickness
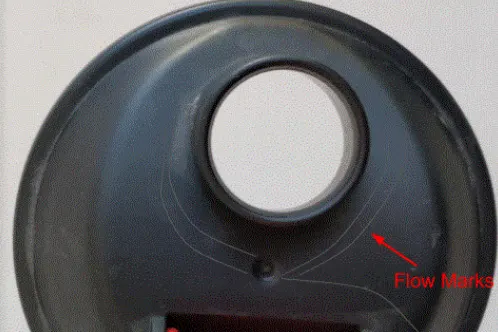
Flow lines in plastic parts appear when molten plastic flows through variable thickness section with low injection speed . which results in the solidification of plastic at different speed.
Creation of Class C surface
To have the parting line on the Class B surface we give the draft angle outwards as shown in the image below
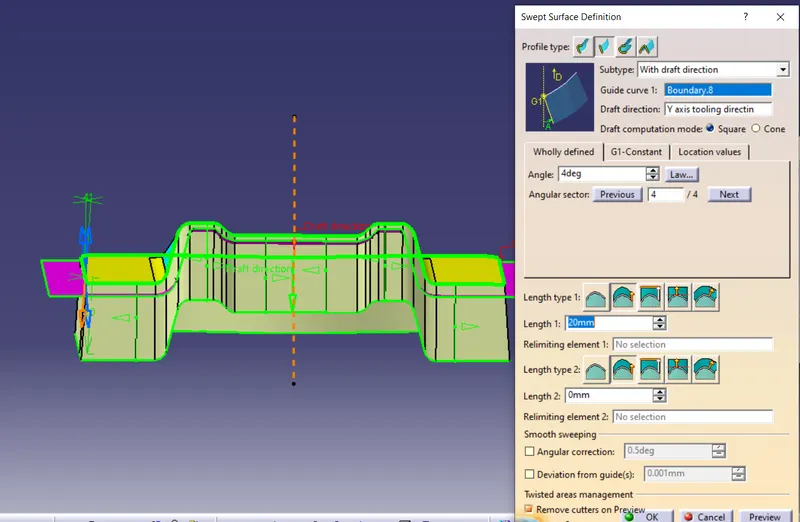
After smoothing the boundry curve we get much smoother class C surface
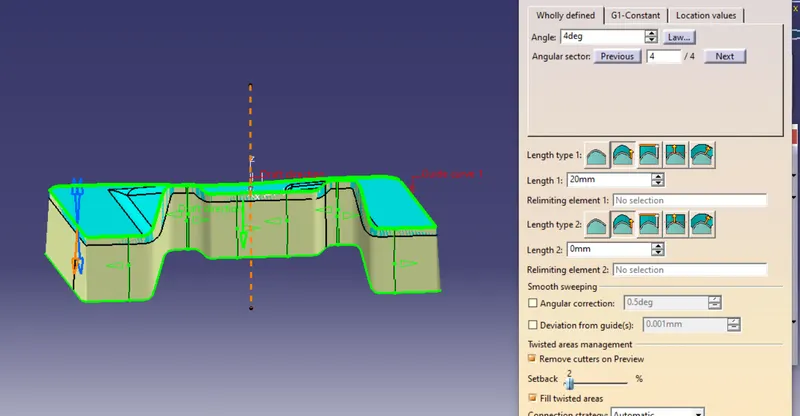
Similarly to have the parting line on the class B surface we give draft to the holes in wards
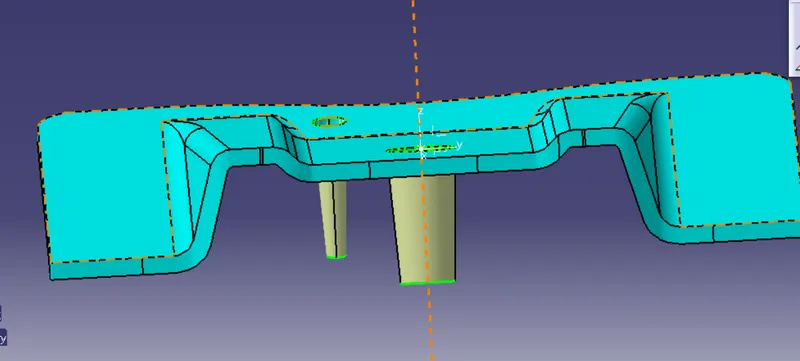
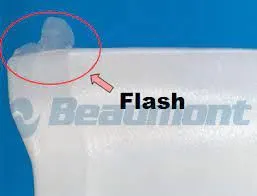
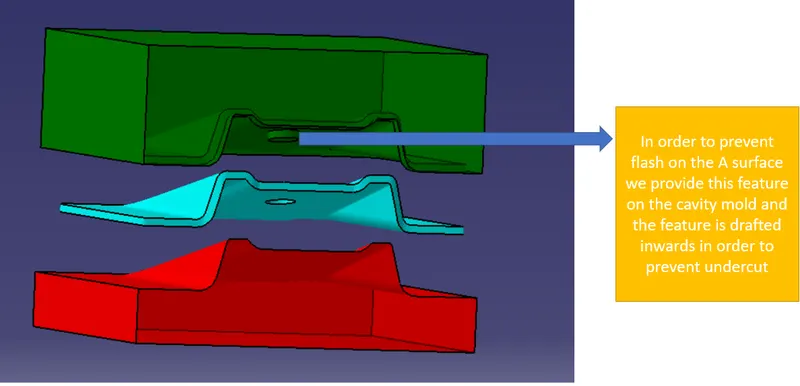
The main advantage of keep the parting line or parting surface on class B surface is to prevent the Flash defect in the class A surfce
Flash defect Example
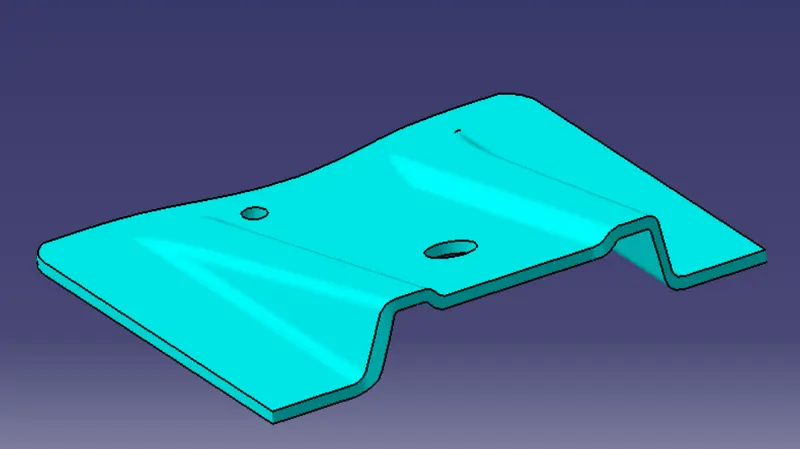
Base bracket designed from the given Class A surface
Analysis of the final component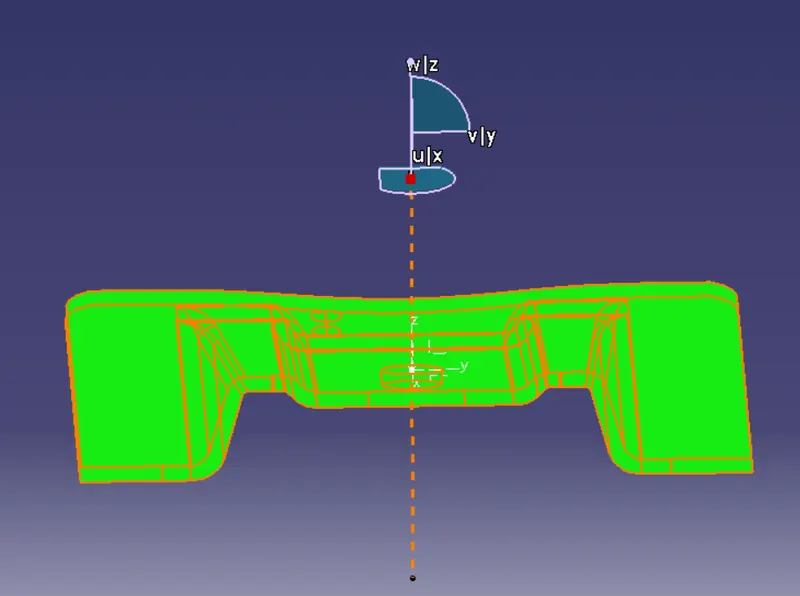
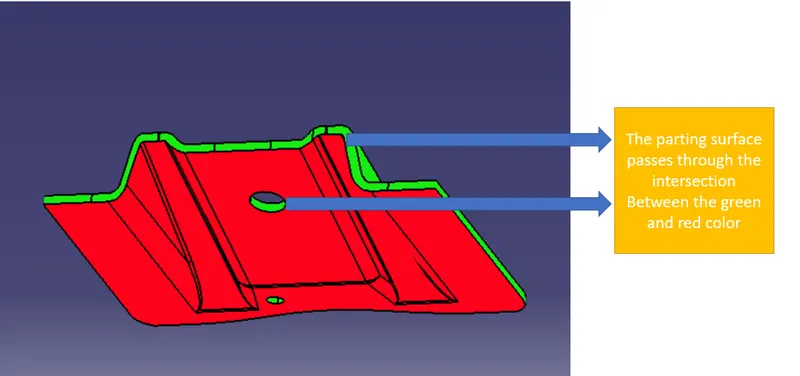
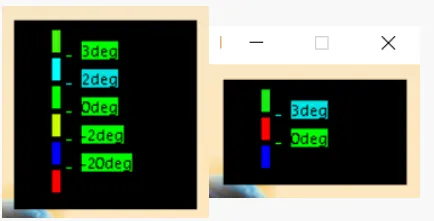
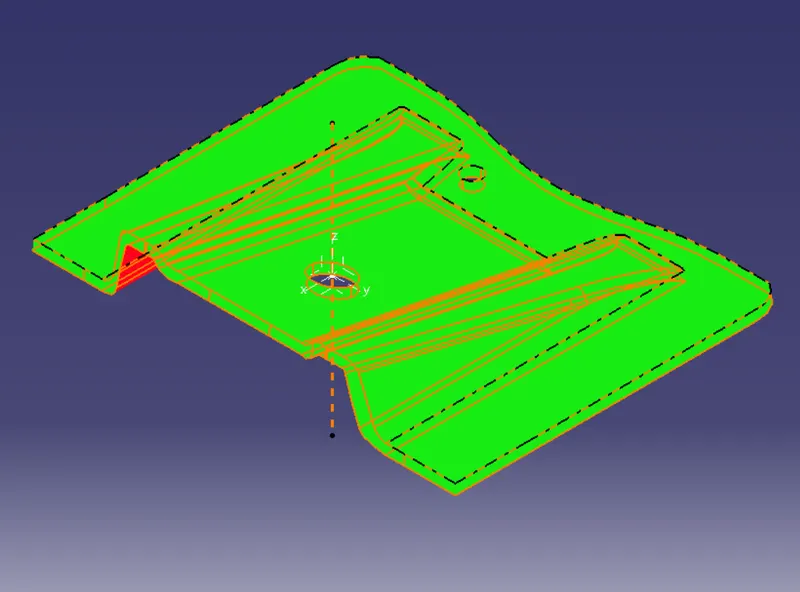
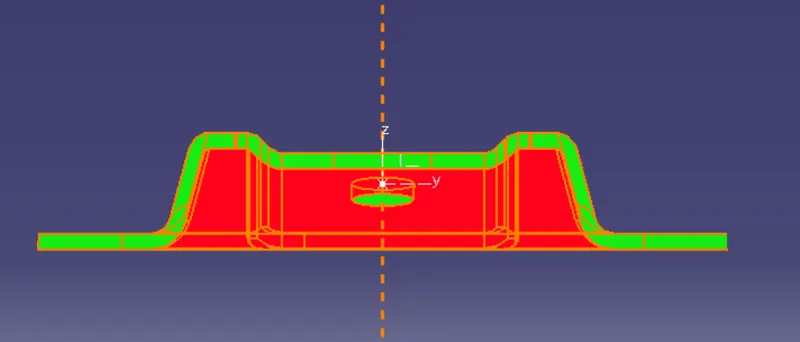
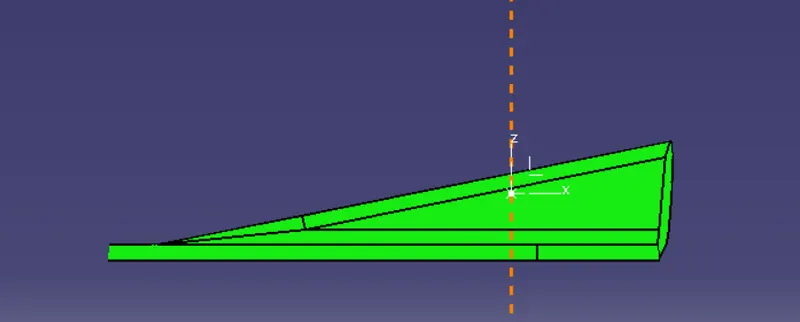
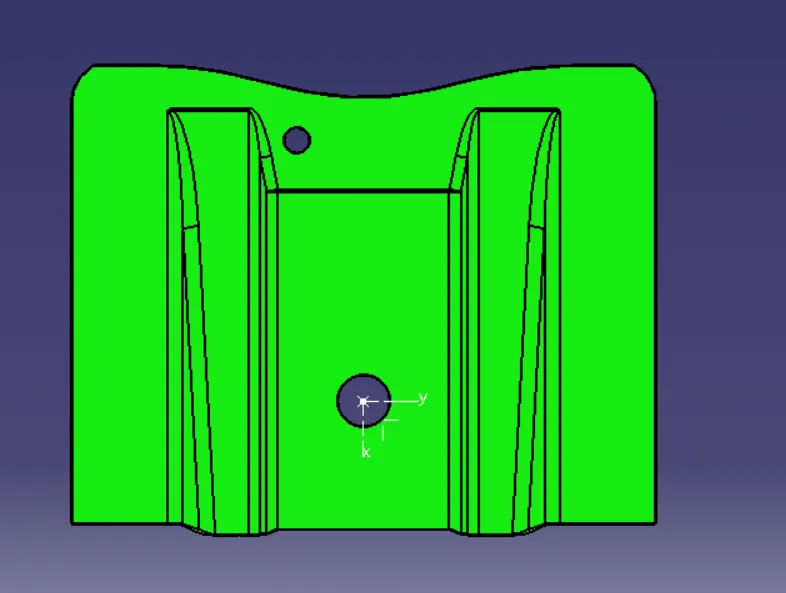
All the top and side region of the Base Bracket are of the same colour which indiactes that it is draftable and it has more than 3degree draft
colour scale which indiactes the degrees at sepecific location
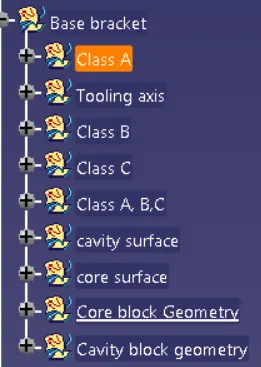
Tree Structure
Geometrical set
Part Body
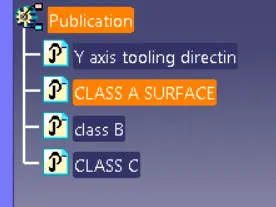
Publication is done as it is easy to access the tooling axis and the Class A surface
draft angle in various orientations
Isometric
Front
side
top
Mold design designed for the Base Bracket
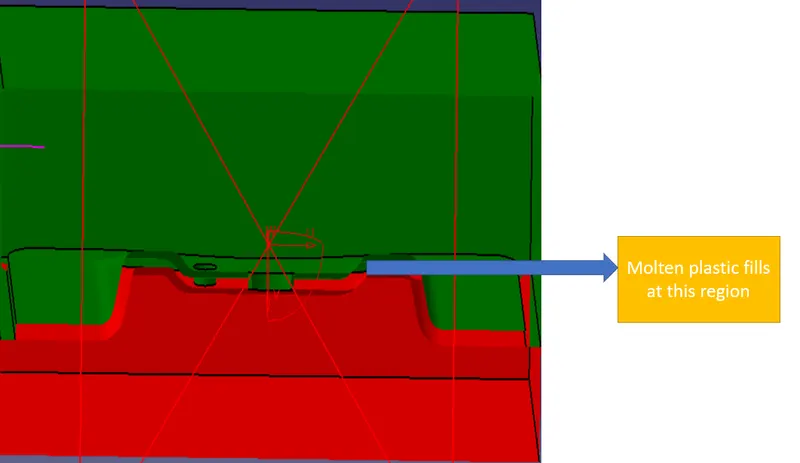
sectional Veiw
Conclusion
The Base bracket was designed successfully for the give Class A surface and the mold was designed for the same