Week 8:- 3D Finishing Challenge 2
AIM:
To design Rough locators for the fixture and to perform 3D finish for all the units (Clamping and Pin unit) for the given panel.
Software Used:
CATIA V5
Introduction:
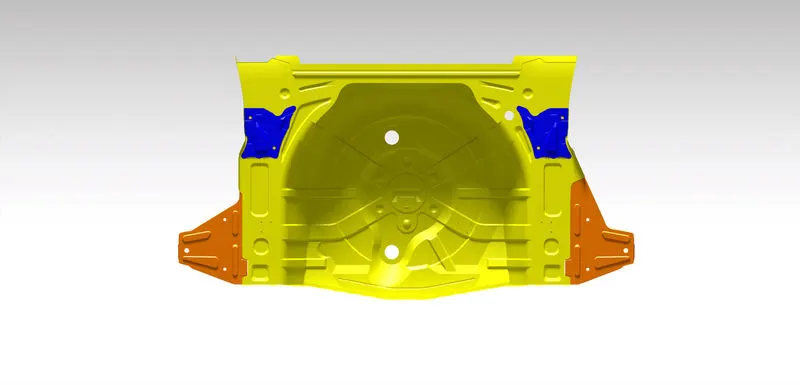
Fig . Panel
3D Finish:
- 3D finish is the process where design is being completely finish & to be ready for final simulation & 2D detailing.
- While finishing the design the nominality of holes is checked which ensures the easy assembly of all the units.
- The hole concentricity & holes sizes are checked which ensures the easy assembly of different parts.
- The gaps between the different units are used to ensure the proper in working units.
- Fasteners are implemented as per the hole size & the standard color codes as per the customer requirements are applied to differentiate the type of hole whether it’s a simple hole, threaded hole or counterbore hole.
- Renaming the assembly & the part is done to give every part a different identity. So everyone can identify in which assembly the particular part is going to be fit.
- After doing all these things the model is sent for to simulation department to Simulate the design with robots whether the gun is clashing or not & 2D detailing.
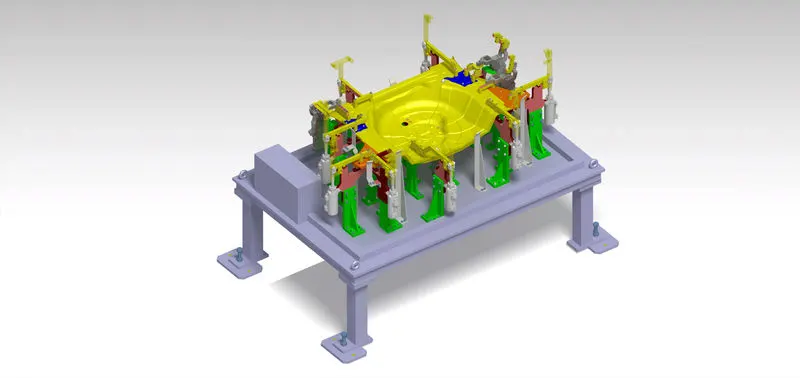
Fig . ISO VIew
Rough Locators and its use:
- A rough locator is a part designed to guide the operator, to locate the car panel on to the pins accordingly. A rough locator can be of standard part or make part.
- Rough locators are used to help locate work pieces in the automation process. Locating refers to the desired location where we want the work piece to be sitting. when it is getting on either worked on either by a person, team, or a robot.
- Body part rough locators are provided to assist manual part loading to the tool.
- The following are general guidelines for rough locators:
- It is not required to finish cold/hot rolled steel for rough locator mounting. Use NAAMS standard rough locators when possible.
- If possible, do not place rough locators in positions that force the operator to lift and load, or unload the part over the rough locators.
- Rough locators must be designed with slots for ease of adjustment.
- Rough locators should have minimal part contact so that the operator can load the part to work location with ease. Excessive part contact may cause difficult part loading and unloading.
- Rough locators must never touch the part when it is nested or controlled by the primary tool locators.
- If the rough locator requires a unique design, use the design parameters for the standard NAAMS rough locator as a guide.
- A rough locator is a part designed to guide the operator, to locate the car panel on to the pins accordingly. A rough locator can be a standard part or make part.
- It is used to identify the correct orientation of the panel.
- It can be called as fool proofing method also. Because due to the rough locator the part cannot be loaded in incorrect position. The rough locators are set according to the angle of the respective panel hence part can only be loaded in defined orientation.
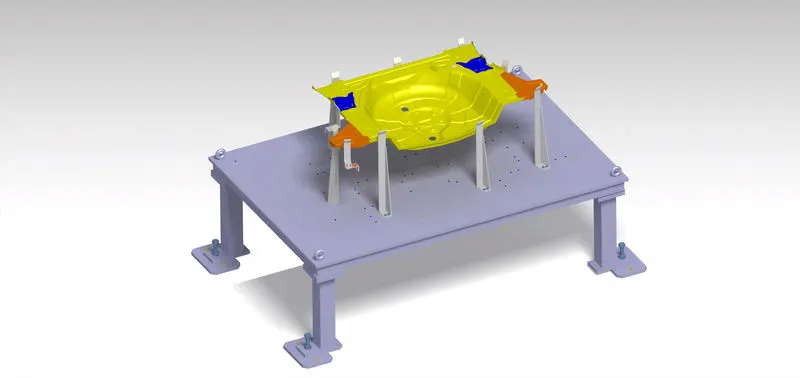
Fig . Rough Locators
Gun Study:
- Welding is mostly used in automobile industries and their requirements for fixtures that ease the welding process is a continuous developments task in any industry.
- In weld study process, the major procedure is insert the gun in the tool assembly and place the gun on the weld spots. Adjust the weld gun for not getting any clashes from the fixture. Once the gun study has been finished with the requirement of robot. It will move onto the fixture designers to develop the concept.
- The most important thing to consider while gun study is how many panels are going to weld at a station whether it is 2 layer panel or 3 layer panel, we have to verify that, because the panel will not weld more than 3 layer.
- Once all the weld spots are cleared without any clashes and it will be moved on to next procedure of simulation.
- In simulation, first we have to check with the reach with respect to the weld spots. Because robots are also having some limitions. it exceeds the limits of robot, the robot will not work properly effective. So first we have check with reach check whether it has been reaching the all weld spots or not. If it should not reach the spot we have to change the robots orientation with consideration of clients requirements and we will not move robots placement without clients approval.
- In simulation we have to check the spot with the developed fixture to know all the weld spots cleared with clashes or not. If any clashes get caught in simulation, we have to get cleared with design team and have to modify the fixture with simulations output.
- Car Body In White (BIW) is a complicated steel structure including 300-500 sheets with complex shape and are assembled by means of welding in a high rhythm through 55-75 robotic work stations.
- The fore most step taken before starting the welding fixture design, we must declare weld spots location for each and every panel. The location and orientation of other critical units of the fixture including clamps, locators., etc are decided based on the weld spot distribution.
Now coming to the point, in weld study, first we have to choose which gun has to be used for welding process. Gun have two different types, they are
- C – Type gun.
- X – Type gun.
C – Type gun:
In C – type gun one arm side is fixed and another arm is movable in linear direction of perpendicular to other arm (Horizontal direction with respect to other arm).
X – Type gun:
In X – type gun one arm side is fixed and another arm is movable in angle position like (it moves like an arc).
- It includes the study of the weld matrix & the weld point positions. There are two types in weld point one is Geo weld which ensures the geometry of the assembly & second is Re-spot weld points which adds strength to the welded parts.
- The fixture is designed for the car panel to hold it on the position, so we ensures all the weld spots and weld gun do not across or any clashes with fixture tool.
- If any clashes defined while designing fixture, then we will only move on to redesign the tool. We have no permission to change a weld spot or clamping position without considering clients.
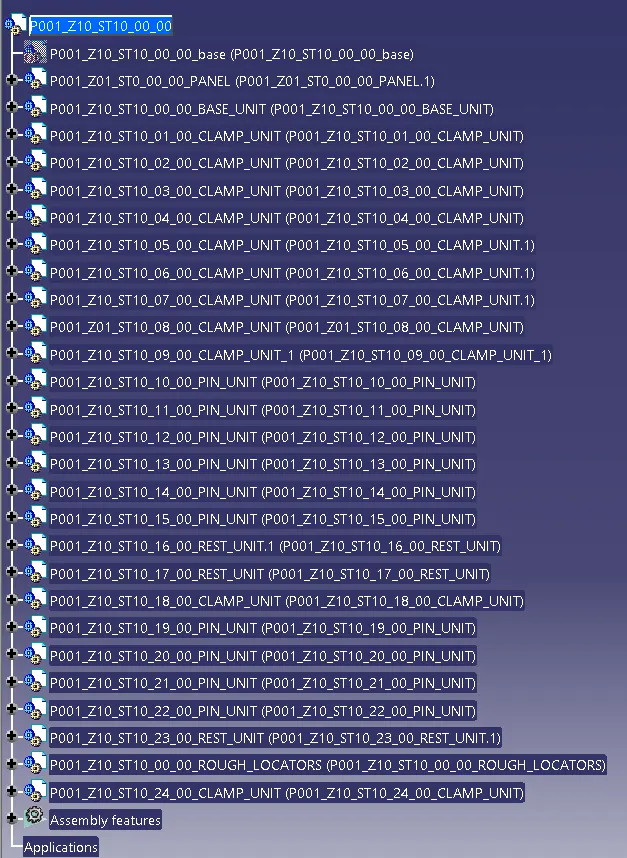
Design Tree:
Naming of design tree has been done and structuring the design tree in a simple way to identify the units. If some parts are use multiple time those will easy to identify by its name.
1. Pin Units:
Holes are make to the nominal and concentric to each other. Proper butting of two parts is done. Rough locators and fastners are implemented. colour coding is done as per the standards. Mylar splitting is done. Open position is shown in yellow colour.
- P001_Z10_ST10_10_00_PIN_UNIT
- P001_Z10_ST10_11_00_PIN_UNIT
- P001_Z10_ST10_12_00_PIN_UNIT
- P001_Z10_ST10_13_00_PIN_UNIT
- P001_Z10_ST10_14_00_PIN_UNIT
- P001_Z10_ST10_15_00_PIN_UNIT
- P001_Z10_ST10_19_00_PIN_UNIT
- P001_Z10_ST10_20_00_PIN_UNIT
- P001_Z10_ST10_21_00_PIN_UNIT
- P001_Z10_ST10_22_00_PIN_UNIT
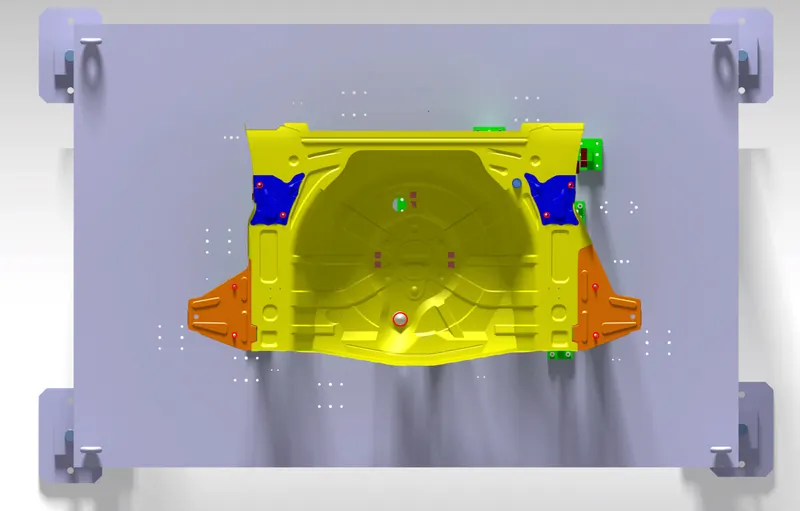
Fig . Top view of Pin units
Design of Pin Units:
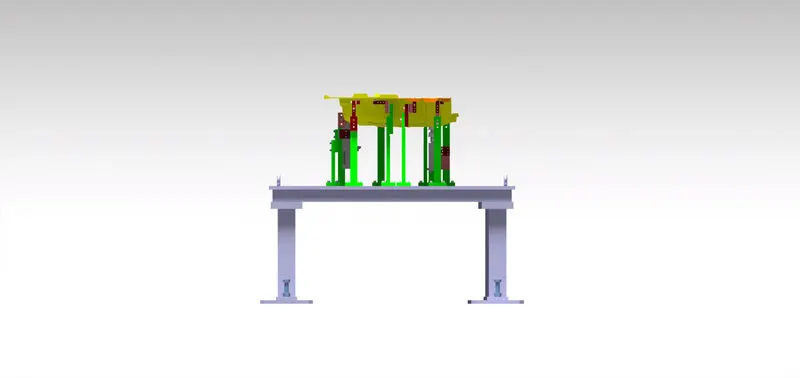
Fig . Side View
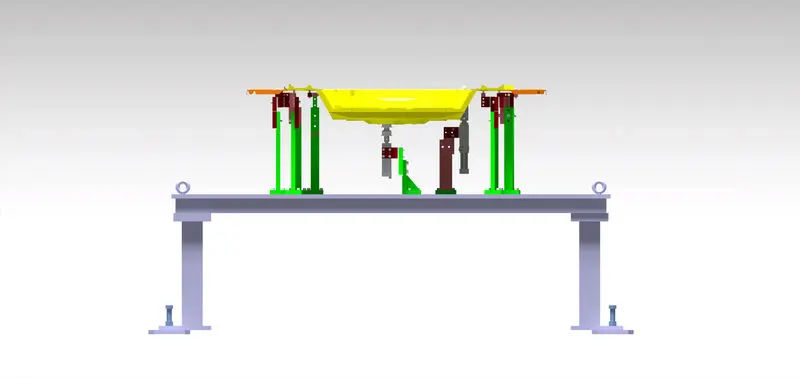
Fig . Front View
Swivel Clamp Units:
Holes are make to the nominal and concentric to each other. Proper butting of two parts is done. Rough locators and fastners are implemented. colour coding is done as per the standards. Mylar splitting is done. Open position is shown in yellow colour.
- P001_Z10_ST10_01_00_CLAMP_UNIT
- P001_Z10_ST10_02_00_CLAMP_UNIT
- P001_Z10_ST10_03_00_CLAMP_UNIT
- P001_Z10_ST10_04_00_CLAMP_UNIT
- P001_Z10_ST10_08_00_CLAMP_UNIT
- P001_Z10_ST10_09_00_CLAMP_UNIT
- P001_Z10_ST10_18_00_CLAMP_UNIT
- P001_Z10_ST10_24_00_CLAMP_UNIT
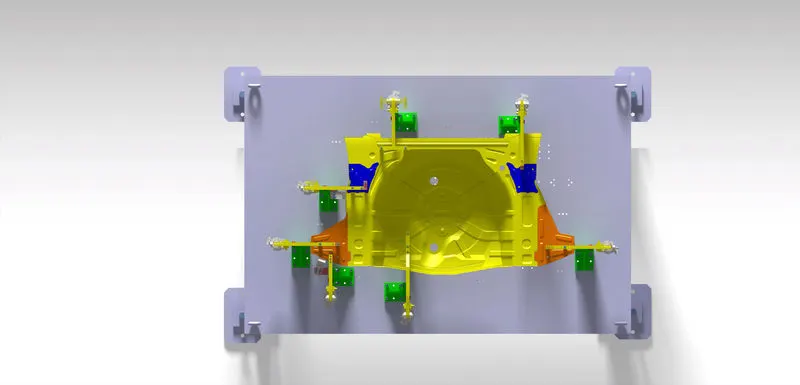
Fig . Top view
Design of Swivel Clamp Units:
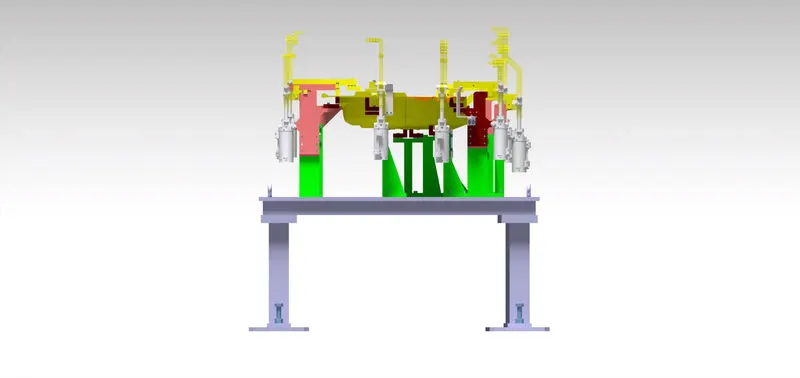
Fig . Side view
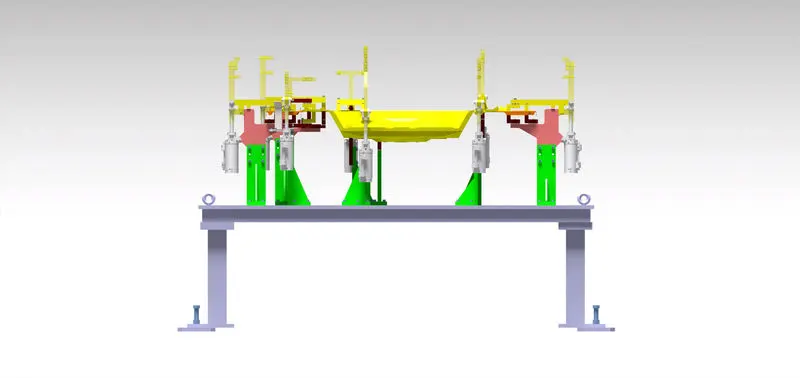
Fig . Front view
Power Clamp Units:
Holes are make to the nominal and concentric to each other. Proper butting of two parts is done. Rough locators and fastners are implemented. colour coding is done as per the standards. Mylar splitting is done. Open position is shown in yellow colour.
- P001_Z10_ST10_05_00_CLAMP_UNIT
- P001_Z10_ST10_06_00_CLAMP_UNIT
- P001_Z10_ST10_07_00_CLAMP_UNIT
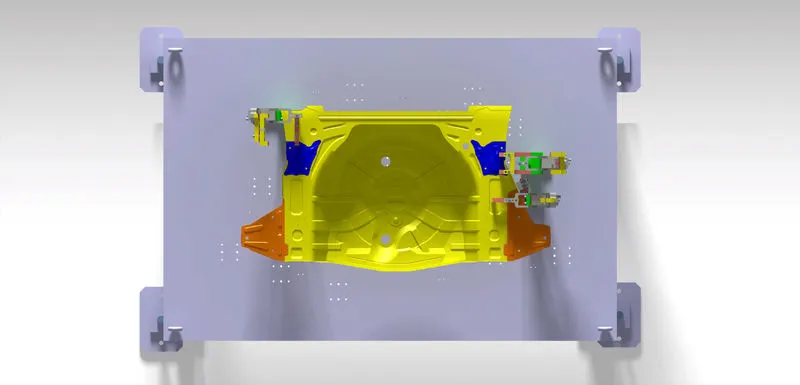
Fig . Top view
Design of Power clamp units:
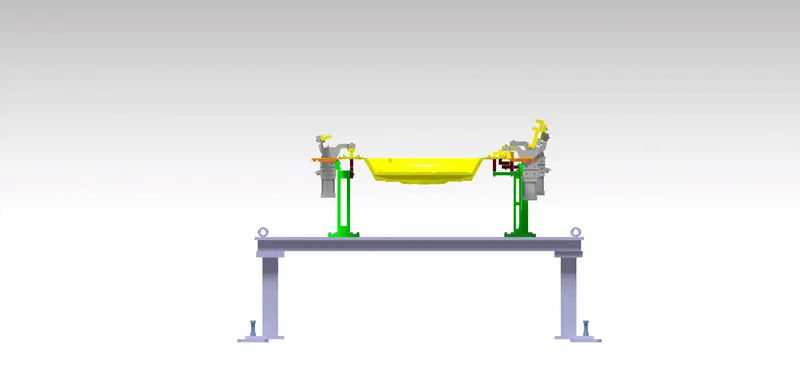
Fig . Front view
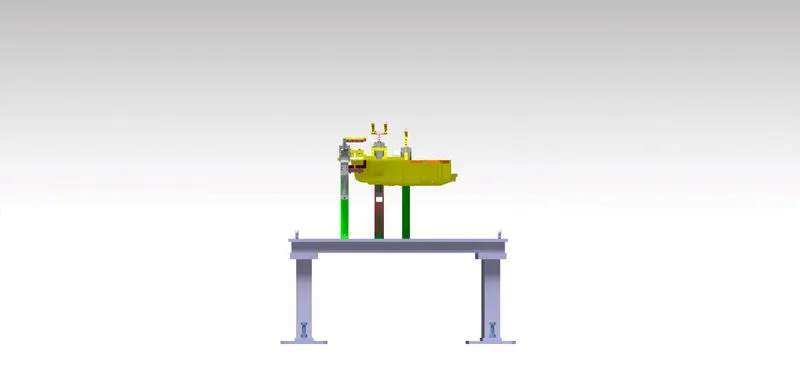
Fig . Side view
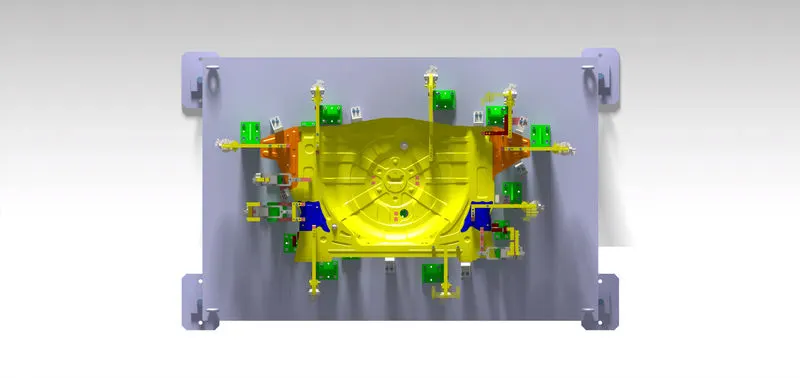
Fig . Render view with open position
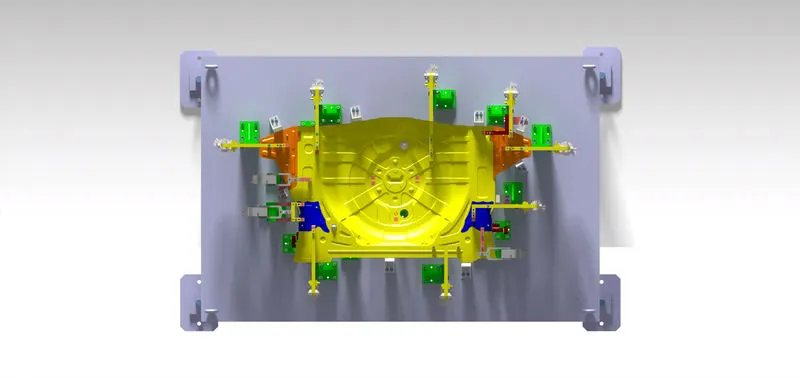
Fig . Render view without open position
Design Procedures:
- If we are going to design a part. we must now how the procedure works on production side.
- The design should be simple because we could reduce the cost and time.
- For example, if a part going to produce in manufacturing site the fixture designer must know how the machining process works and the designer think like an production engineer also at the time of concept developing.
Changes in Design:
- When compared to week 7, i have made some changes. Added a entire new unit in the assembly.
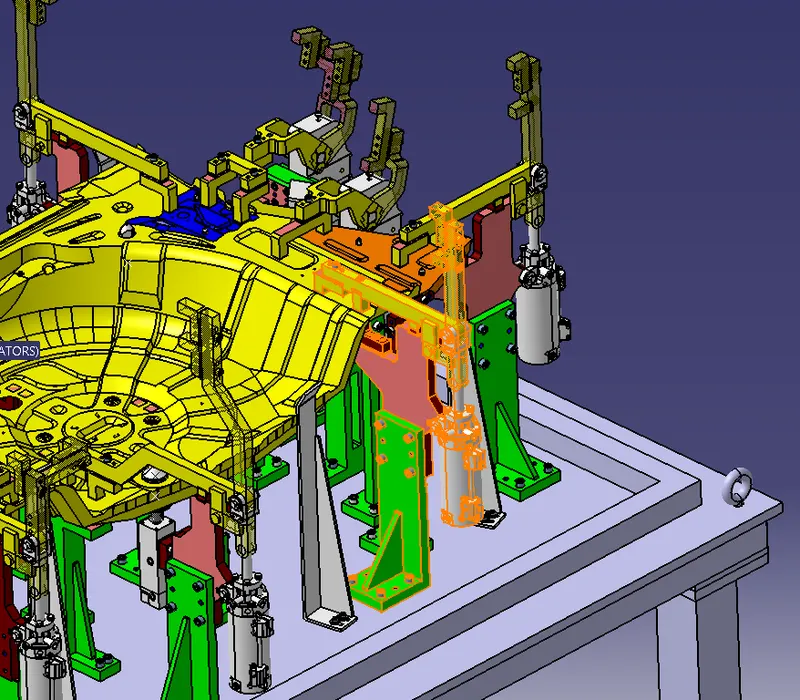
- In some units mylars have been changed because of previous assembly has not effective compared to the NAAMS and it has been corrected.
- On previous challenge, retractable cylinders are used on 6 pin units and its been reduced to only two and the reason why i reduced the retractable cylinder in pin units are majorly used on angle surface panels and these are the major changes i have made.
Final Render image of Fixture:
Fig . ISO View
Conclusion:
Here as per the objective to design rough locators for the assembly and performed 3D finish for the fixture has been done.