Week 7- Base Unit Design Challenges 2
TYPICAL PARTS OF BASE UNIT:
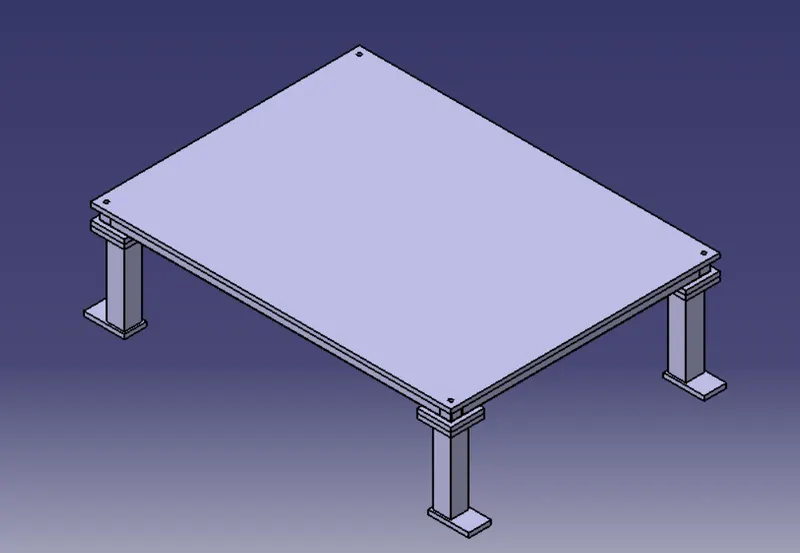
BASEPLATE:
The base plate is a plate of 25mm to 40mm thickness.
The base plate has no of holes on it which will act as mounting points for clamp unit, pin unit, etc of a tool.
PEDESTAL:
It is used to connect the base plate with a floor plate.
The pedestal can be a standard part or a make part, depending on the size and height of the fixture.
Standard pedestals are available in different heights.
Pedestals are also available in different inclinations.
Depending on the size of the base plate, the number of a pedestal for a fixture can vary for load distribution.
TRUNKING CHANNEL:
Trunking channel is a duct that carries all the electrical and pneumatic connections (wres and pipes) for units of the tool.
It has a thickness of few millimeters.
VALVE BOX:
Valve box is a standard part which will accommodates all the pneumatic valves for the unit.
The valve box is the box which includes different solenoids valves.
The trunking channel includes all the pressure inlet cables going to pneumatic parts of the fixture & protects them from damaging while operation is in process.
EYE BOLT:
Eye bolts are the bolts that are used to lift fixture for transportation by inserting hooks into them.
For example, usually we use M20 bolts that are bolted on the base plate.
Used for transportation purpose, sometimes forklift holes will be provided.
FLOOR PLATE:
Floor plate is grounded to the floor with fixed bolt on the ground.
Floor plates are also called as foundation plates.
There will be a clearance of 10mm maintained between the pedestal base plate and the floor plate.
This clearance will be used by the leveling screw, for leveling the entire tool.
Weld bars are used to weld the positions permanently, after leveling is done.
A weld bar is a plate along the sides of the base plate of the pedestal.
BASIC NEEDS TO DESIGN A BASE UNIT:
Working height:
It depends on the nature of the manual or robotic welding fixture.
- For manual fixture we need to consider the working height 850-1100mm, depending upon the working height of the worker standard of a specific country will apply.
- If base structure is made With base palte having tubular structure welded below it. We can reach to height 100mm to 250mm. in this case to reach the working welding height we need to provide additional some leg structure which may have top & plate welded to the tube.
- As designer it is important to know how big base plate or bigger base welded structure will be handled during the fabrication & handling process. Special case needs to take care of flatness if the base size is very long.
- Depending upon the weight eyebolts size is selected for lifting holes on base plate. Generally 4 eye bolt provision is made. You also need to select the location of eye bolt considering the rope / belts used while shifting the structure or complete fixture are not damaging any units nearby.
- Most of the OEM makes 4 dowel holes & put small aluminium plate marking X, Y, & Z coordinates of dowel holes. If the base length is too long few OEM's follow the methodology of having holes at 500mm distance.
The best unit of the fixture must be strong enough so that deflection of the fixture is as minimum as possible. This defection of a
fixture is caused because of forces of welding, clamping of the work piece. The base unit of the fixture should have the mass to prevent vibration & chatter.
- The base unit may be built from simple section so that other units may be fastened with screws or welded necessary. Those parts of the fixture that remain permanently with the fixture may be welded. those parts that need frequent changing may be held with screws.
- The base unit should be parallel to the floor, to adjust this there should be provision of the height adjusting mechanism.
Fundamentals of Base unit:
- A base plate size should cover all the units With its outer periphery including opening.
- A base plate is always preferred to be designed with respect to BCS coordinated.
- A base plate should be drilled with datum holes / measuring holes in line with a pitch of 1000m in general.
- Number of datum holes is depend on the size of the base plate
- .Datum holes should be drilled at nominal valves of coordinates and in terms of 50 and 100. Example X=IOO, Y: -600, Z=250.Datum holes should be covered With cover plates.
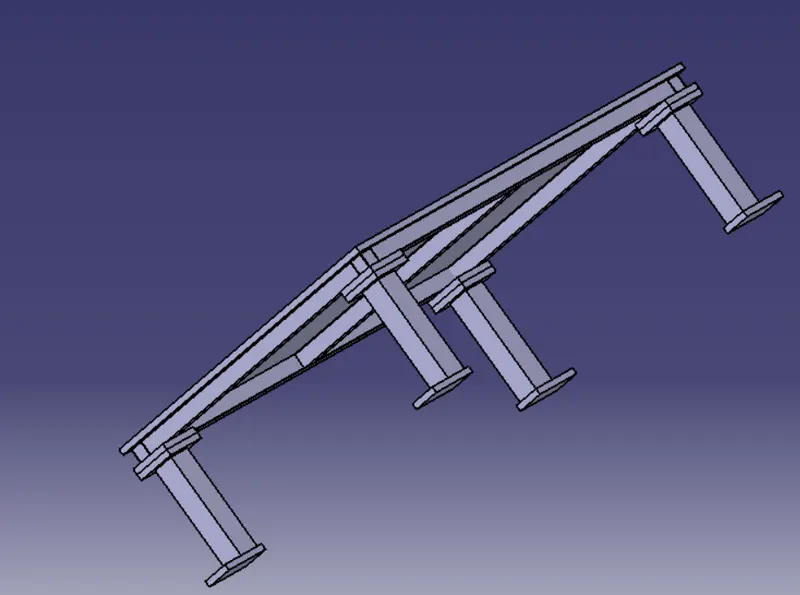
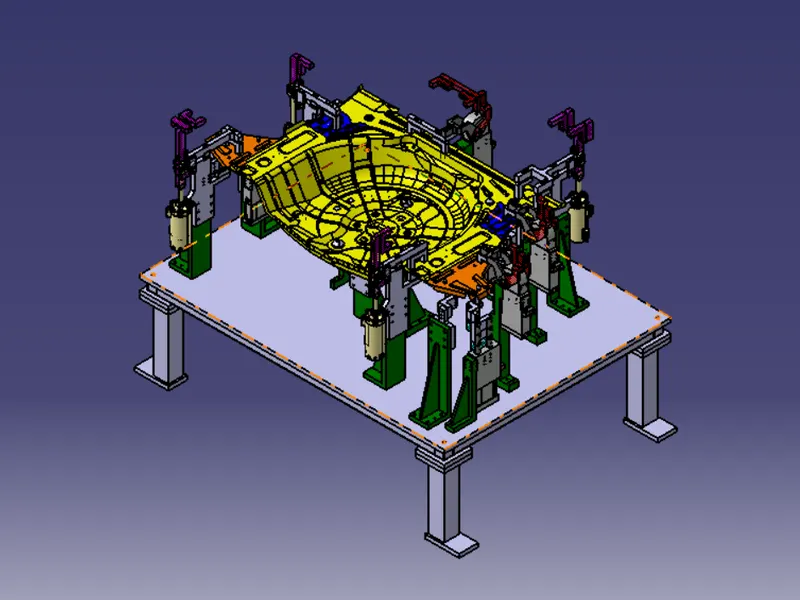
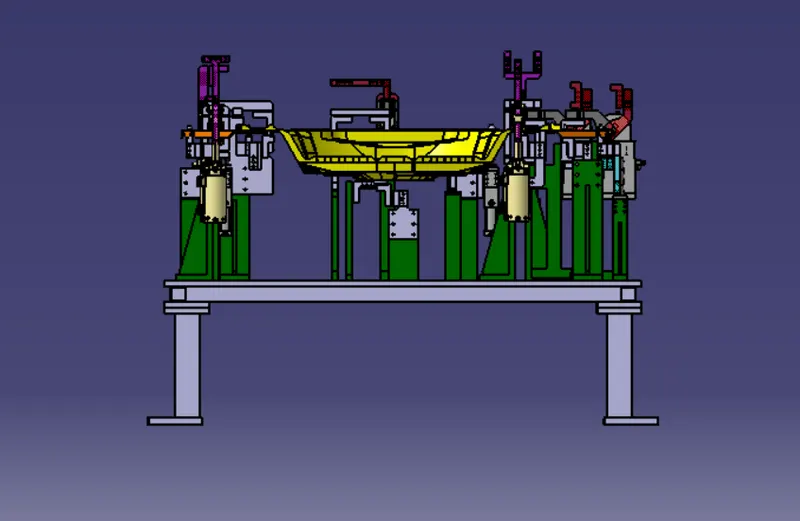
HERE THE FULL ASSEMBLY DRAWING OF FIXTURE ;
ISOMETRIC VIEW;
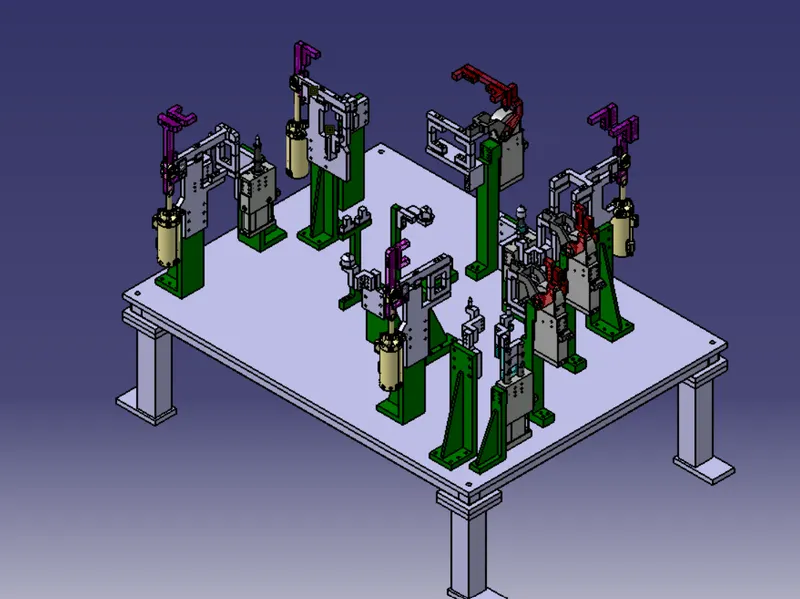
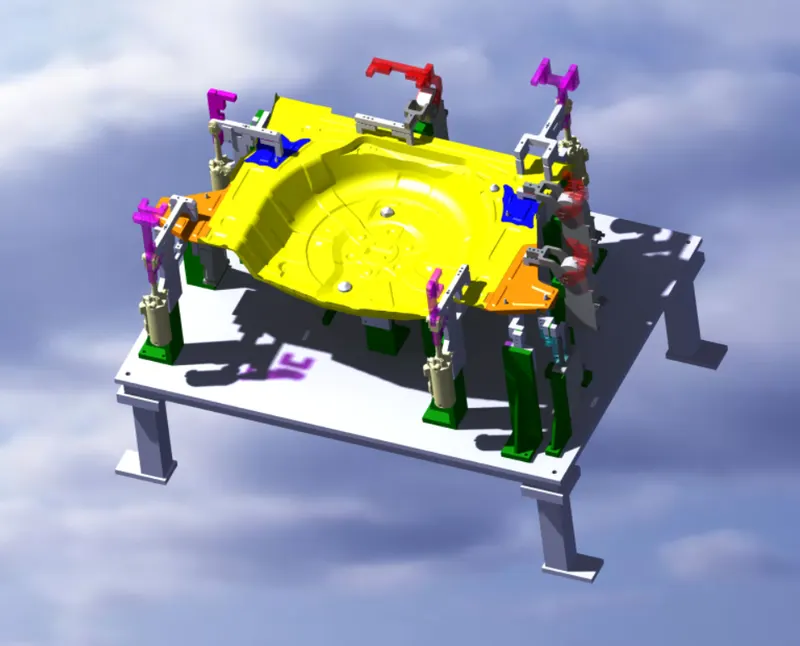
FRONT VIEW;
3-2-1 PRINCIPLES;
- 3-2-1 Principle is the most effective and better costing methods of part locating in fixtures.
- By using 3-2-1 principle we arrest all 12 degrees of freedom in workpiece to locate the fixture.
- 3 referas to three locating blocks.
- 2 refers to two locating round pins.
- 1 refers to one locationg round pin in slot.
- Three locating blocks are used to arrest five degrees of freedom ,thats in four radial movement(clockwise and anticlock wise rotationof X,Y axis) and one axial movement that is downward movement
- Two round locating pins are usd to arrest the four axial movement (X+,X-,Y+,Y-)
- One round locating pin in slot are used to arrest the two axial movement(Z+,Z-)