Week 7:- Base Unit Design Challenges 1
1.What is the Base Unit? What are the typical parts of the Base Unit?
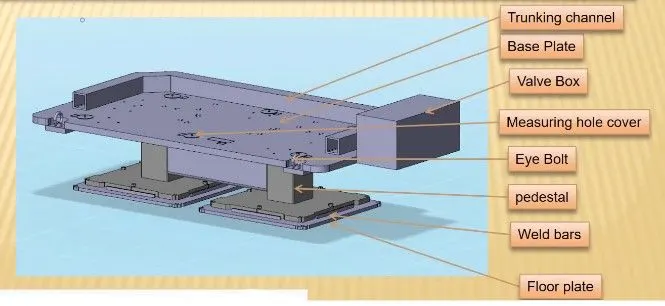
A base unit is the unit designed to mount all the other units(Clamp unit, Pin unit, rest unit etc,) of the tool, also other parts necessary for a tool like pneumatic valve box, trunking cable path will also be mounted on to a base unit.
Base unit is the fundamental component of the fixture because all other components are mounted over it,so every fixture have base unit, The base unit design is different according to the panel, Design of clamp system, location system etc,
Floor plate;
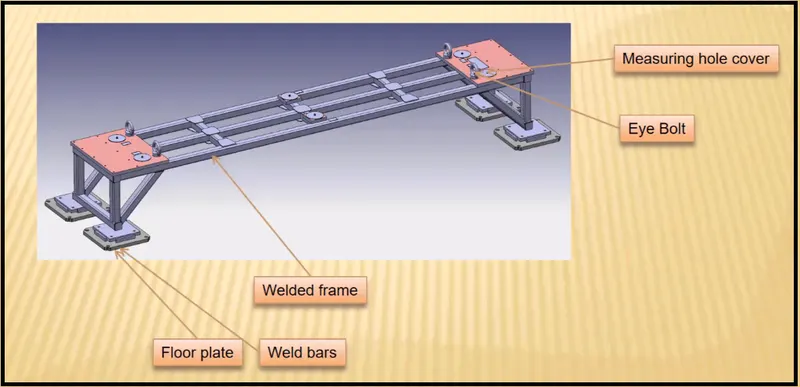
Floor plate is grounded to the floor with fixed bolt in ground.floor plates also called as foundation plates
- There will be 10mm clearance between pedestal plate and floor plate
- The clearance is used to leveling the entire fixture
- Weld bars are used to weld the position permanently after finished the leveling
Weld bars & pedestal plates;
Pedestal is the base or support on which a The fixture is mounted.
EYE BOLT;
An eye bolt is a bolt with a loop at one end. They are used to firmly attach a securing eye to a structure, so that ropes or cables may then be tied to it. Machinery eye bolts are fully threaded and may have a collar, making them suitable for use with angular loads up to 450. Eye bolts without a shoulder should not be used for angular loads.
Heavy forged eye bolts with a continuous eye may be forged with an integral shoulder, allowing their use for heavy off-axis loads.
Depending upon the weight eye bolt size are selected for lifting holes on the base plate. Generally 4 eye bolt provision is made,
You also need to select the location of eye bolt considering the rope/ belts used while shifting the structure or complete fixture are not damaging any or location units) nearby
Measuring hole cover ;
The base plate have some hole to mount various units like clamp, rest, pin etc. & every hole have some coordinates to define the exact location of the hole.
Due to irregular shape of the car panel the holes coordinates are not nominal like 110.0, 150.0 But it like 110.62,150.84.
The maesuring hole is drilled over the base plate which having exact cordinates so that all other holes can take reference from it.
The measuring hole no. depends on the size of base plate.
These holes are covered by using some plate to protect against dust, damage etc.
Valve box & trunking channel;
The valve box is the box which includes different solenoid valves.
The pneumatic fixtures work on air pressure provided to it. So the arrangement of air pressure inlet & outlet is done within this valve box.
The trunking channel includes all the pressure inlet cables going to the pneumatic parts of the fixture 8 protects them from damaging while operation is in process.
Base plate;
Base plate is the heavy plate of large thickness becuase it carries all the weight of the mounted parts.So it must be able to bear the load.
Base plate is machined to maintain the parallelity within the tolerance.
It also consist some drilled holes to mount the different units over
2. What are the points need to account while designing a Base unit?
Followng points need to be taken into account whike designning the base unit
- working height:-
It depends on the nature of the manual or robotic welding fixture.
For manual fixture we need to consider the working height 850-1100 mm, depending upon the working height of the worker standard of specific country will apply( In few countries human height is higher or lower e.g. US Japan).
If base structure is made with base plate having tubular structure welded below it we can reach to height 100 mm to Q50 mm.
In this case to reach the working welding height we need to provide additional some leg structure which may have top and plate plate welded to tube.
- As designer its is important to know how big base plate or bigger base welded structure will be handeled during the fabrication and handling process. Special care needs to be taken care for flatness if the base size is very long.
- Depending upon the weight eye bolt size are selected for lifting holes on the base plate. Generally 4 eye bolt provision is made, You also need to select the location of eye bolt considering the rope/ belts used while shifting the structure or complete fixture are not damaging any units(rest,clamp or location units) nearby
- Only Base plate or welded structure
- Depending upon the component size and weight of the total units you can decide whether you need fabricated base or just plate. Mostly fabricated bases are used made of square or rectangular tube with plate
- Most of the OEM makes 4 dowel holes at 4 corners and put small aluminum plate marking X Y &Z coordinates of dowel holes.lf the base length is too long few OEM's follow the methodology of having dowel holes at 500mm distance
- The base unit of fixture must be strong enough so that deflection of the fixture is as minimum as possible. This deflection of fixture is caused because of forces of welding, clamping of the workpiece.
- The Base unit of the fixture should have the mass to prevent vibration and chatter.
- Base unit may be built from simple sections so that other units may be fastened With screws or welded whenever necessary. Those parts of the fixture that remain permanently with the fixture may be welded. Those parts that need frequent changing may be held with the screws.
- The base unit should cover all the units with its outer periphery including opening.
- The base unit should be parallel to the floor, To adjust this there should be the provision of height adjusting mechanism.
-
Fundamentals of base plate design:
- A base plate size should cover all the units with its outer periphery including opening.
- Abase plate is preferred to be designed with respectto BCS coordinates,
- Abase plate should be drilled With datum holes/measuringholes in line with a pitch of 1000 mm in general, Numberof datum holes isdepends on the size of the base plate,
- Datum holes should be drilled at nominal valuesof coordinates, & in terms of 50 & 100 (In general) ex,1:100,Y:600, Z:250 Datum holes should be drilled with dial 100 mm awayfrom other units,
- Datum holes should be covered with coverplates,
3.What is a Dump unit?
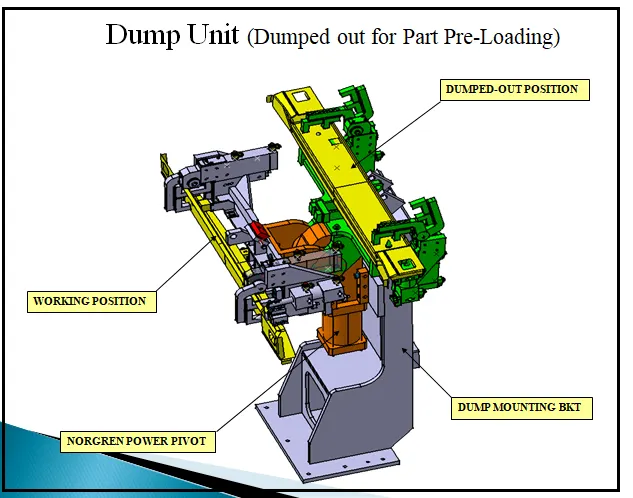
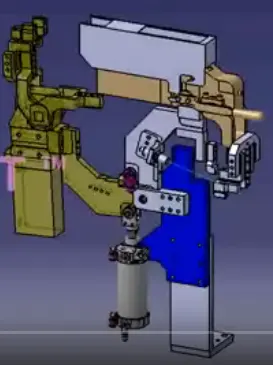
- When we have some geometrical constraints then we can not mount normal units like clamp unit, pin unit etc. In this case the dump unit is used.
- Dump unit is the complex unit to design due to space constains there is less space avilable & have to adjust all the parts in available space.
- It consist of dump cylinder to perform the operation of clamping & unclamping car panel.
Dump unit is a unit to assemble the component which have certain constrain or geometrical constrain
Functions;
Dump unit is very complex to design
dump unit contains pin unit,retract unit ,rest unit,clamp unit are there
Dump unit functions with the help of dump cylinder
dump is very rare to use which the part have more constrain then only we prefer dump unit
4.What are the points you need to consider while designing a Dump unit?
Following points are need to while designing Dump unit
- Dump units are used when we can not use normal units like clamp unit, pin unit etc, Due to some space constraints, The designed parts should be small in size but can do their functions effectively,
- It contains the dump cylinder which will be the heavier part in all the unit, The riser & blade should have enough strength to bear the load of the cylinder & all the unit as well, The riser & blade thickness should be more in this type of units.
- The parts should be designed by considering the open condition of the unit. In the open condition of the unit the parts should not fall to another unit.
- We can use any cylinder in this case which suits our requirements. In the below image of the dump unit Both clamp cylinder & hinge cylinders are used.
5.What is a Slide unit?
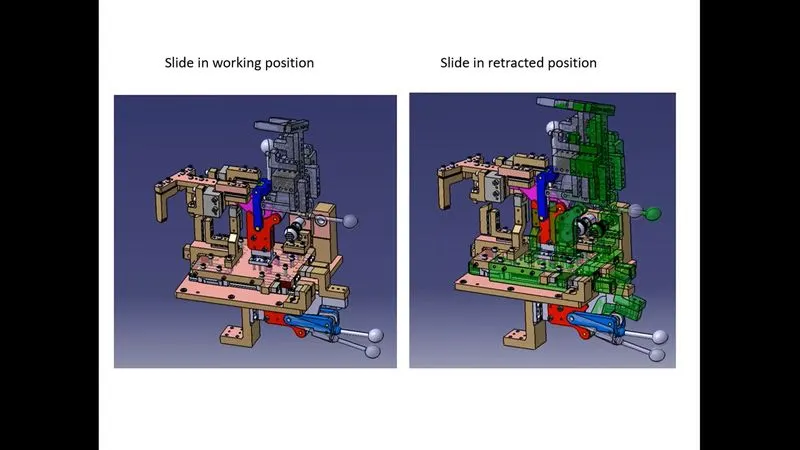
- Slide unit is a unit desgin the fixture which has more units to perform alternatively we use slide units
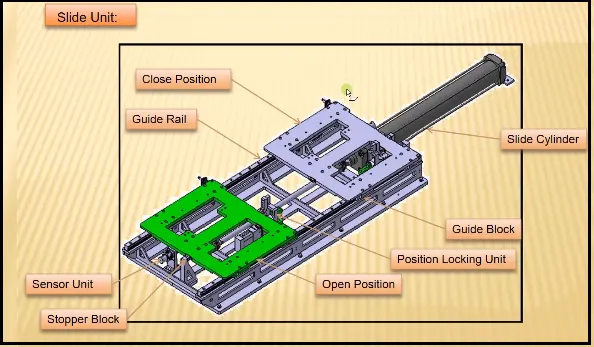
- It has cylinder which pushes the assembly forward. For precision operation ball screw with servo motor is used to move slide forward & backward. Also at the both ends shock absorber are provided.
- Assembly is mounted on a plate which is attached to guide rails.
- There are sensors on the extreme ends of the slide to sense the position of the slide
- It has stop docks on either side of the slide to stop the cylinder at required position.
- It has locking mechanism which ensures that the slide does not move in particular position as it may affect the welding quality & may damage the panel.
- Slide units are used in places where there is space constraint.
- The opening & closing of slide should not foul.
- Slide units are positioning units which are used to position the fixture, weld gun units, robots into position for further operations.
- Slide units are used when we have some space constraints. So we don't have space to design different special unit & to assemble it in those case we use sliding unit. Sometimes there are too many small panels near each other & there is not enough space as each panel requires resting, location using 2 pins, clamping & sensing. Thus becomes more difficult when the panel is at angle. To solve this problem slide unit mounts rest, clamp or pin unit or all of them on slide using guide rails, guide block, a cylinder, locking mechanism, stop blocks, sensors. When particular panel is to be welded, then this slide moves forward & after completion moves back. & get locked at its position.
- Guide rails should be lubricated well.
The lubricant has following function.
- Minimizes friction in travelling unit to prevent seizure & reduce wear.
- Forms oil on the face way to decrease stress acting on the surface & extend rolling life.
- Cover the metal surface to prevent rust formation.
6.What are the points you need to consider while designing a Slide unit?
Points needs to consider while designing the Slide unit
- LM guide ways are preffered over hardened guide ways due to least co-eficient of friction
- Slide unit essentially consist of LM guides, Linear cylinder ,front & rear stoppers, front & rear shock absorber, two proximity switches/reed switches for sensing the two end position, bellows or protection cover for rails.
- Center trunnion/rear clevis mounted cylinders are ideally used for slide unit application as this allows for some float to take up misalignment.
- Reverse stroke of 10mm to be considered in both forward & retracted condition.
- Cylinder & LM guides to be validated for load & stroke.
- LM guide rail length should be standard and should be more than the actual stroke.
- Mechanical hard stop to be considered for both extened & retracted condition.
- Shock absorber to be used for both extended & retracted condition to reduce impact load.
- The two end limits to be sensed externally by a proximity switch.
- The shock absorber should be mounted such that it is perpandicular to the pivot at mid stroke or within i/- 5degree.
- Slide units are used when we have some space constraints. So we dont have space to design different special units & to assemble it. In those case we use sliding units.