Week 3:- BiW Fixture Design Methodologies Challenges
1.What is Design methodologies?
DESIGN METHODOLOGIES:
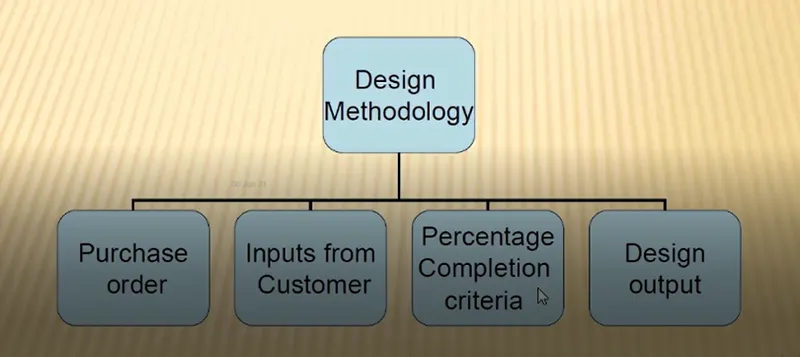
Design methodologies is nothing but the steps followed during the concept designing stages of fixture design. The various stages of design methodologies are,
- Purchase order.
- Inputs from customer.
- Percentage of completion criteria.
- Design outputs.
1.Purchase Order
A purchase order (PO) is a commercial document and first official offer issued by a buyer to a seller indicating types, quantities, and agreed prices for products or services. It is used to control the purchasing of products and services from external suppliers. Purchase orders can be an essential part of enterprise resource planning system orders. Purchase order is a order from customer for start of the work. After offer has been finalized customer will be releasing the LOI/PO(Purchase Order).
Once PO is released we have to start the work.
After PO from the customer we have to prepare the schedule.
Purchase order is the confirmation document from customer to proceed the committed work for them.
2.Inputs from customer
The inputs from the customers are as below,
Functional Requirements: The purpose or the function of the fixture will be given as inputs from the customers like what are the process the fixture is going to do i.e welding, riveting, gluing or whether it is a checking fixture, etc.
Preferred standards: As we know different companies follow different standards, we will be following the standards, we will be following the standards followed by the customers. By following standards the time of designing and manufacturing of parts will be saved, which will be automatically minimizing the time of the projects. As for the standards parts, it can be easily replaced from the used fixture to the new fixture which reduce the cost.
Car products: The inputs we get from car products are GD&T, part list, cad files of car part, clamp plan, product assembly process sheet.
Layout: Layout shows the entire assembly plan to understand the process. Layout provides the information of flow of parts, station pitch, robot stations, accessories like tool changers & tip dressers, sub assembly links, plat form height, loading/unloading sequence/height.
Ergo Data: As same as preferred standards, different companies follow different standards of ergo data. We have to follow the customer standards of ergo data. The inputs of ergo data will given by the customer mostly in case of manually operated fixtures/manual fixtures. The ergo data is mainly used to make the operator comfortable which may lead to improve the efficiency in cycle time& production. Ergo data provides inputs like platform height, maximum & minimum reach from operator to fixture, maximum & minimum height of the fixture, whether the child parts/assemblies are visible while clamping or loading & unloading. Also provises information like loading height, working safety zone of operator, etc.
Weld study: Weld study is the important inputs given by the customer. It gives details about the study of particulars gun that we use for welding. Also the dates like no/ of weld, position of weld in the components will be given. In short, weld study includes weld gun details, weld matrix & weld points.
Standard detailing templates: This inputs include the detailing templates of 2D cad drawing as per the customer standards. So, we have to follow the detailing templates as per the customer standards.
3.Percentage of completion criteria
It is followed in the designing stages & dispatch stages of welding fixtures.
It helps to track or identify how much task completed & how much to go further for completing a fixture.
Inputs & concept design – 0 to 25%
Concept approval & simulation check – 25 to 40%
Design freezing & detailing – 40 to 85%
Check & final dispatch – 85 to 100%
The above mentioned percentage are the percentages of stage wise completion criteria of the projects.
4. Design Output
- Output consist 3D models,2D drawing which is the detailing part, BOM & other related documents.
- There are some tools which are multiple units on common base are called inutized tools for ex. fixture which includes no. of units on the same base.
- They required two types of drawing sheet as follows,
1)key sheet- It shows the index of the unit & their placement on tool base
2)Layout sheet- It is the detailed drawing individual unit to include all their components.
- Non unitised tools which can be completely detailed on layout sheet.
2.What are the inputs required from the customer to start designing a Fixture?
The inputs required from the customer to start designing a fixture are as follows,
- Fundamental requirements.
- Preferred standard components.
- Car products.
- Layout.
- Ergo – data.
- Weld study.
- Standard detailing templates.
A.Functional Requirements:
The purpose or the function of the fixture will be given as inputs from the customers like what are the process the fixture is going to do i.e welding(spot or seam weld), gluing, riveting, hemming or whether it is a checking fixture or a storage racks etc.
It is one of the basic requirements to get from the customer to start designing a fixture.
B.Preferred standards:
As we know different companies follow different standards, we will be following the standards, we will be following the standards followed by the customers. By following standards the time of designing and manufacturing of parts will be saved, which will be automatically minimizing the time of the projects.
As for the standards parts, it can be easily replaced from the used fixture to the new fixture which reduce the cost.
Some of the preferred standard components used in BIW fixtures are given below,
- Standard like ABB, NAAMS, DESTACO, ZYTRAN, TUNKERS are used in design & manufacturing of fixtures.
- Standard parts like Risers, L-blocks, retainers, pins, NC blocks, Shims, etc.
- Components like clamps, cylinders, slides, switches, sensors, etc.
- Weld guns, Tip dressers, Tool changers, etc. tip dressers are to sharpen the tip of the tools whereas tool changes are used in robots to do various process. As robots are too costly, tool changers are used.
ABB – It is a Robots manufacturing company.
Some example of description of standard robots are, Robust IRB 7600 robots, which can, hold the panels securely and accurately in place while IRB 6640 robots perform the welding.
The below picture shows the welding line is installed at great wall motors (GWM) recently opened and internationally acclaimed automotive plant in Tianjin, china. One of the factory’s most highly publicized and productive manufacturing lines is the ABB welding line, which comprises among other things a fleet of ABB robots and patented ABB framing and hemming technologies.
C. Car Products:
The inputs we get from car products are: GD&T, part list, Cad files of car part, Clamp plan, product assembly process sheet.
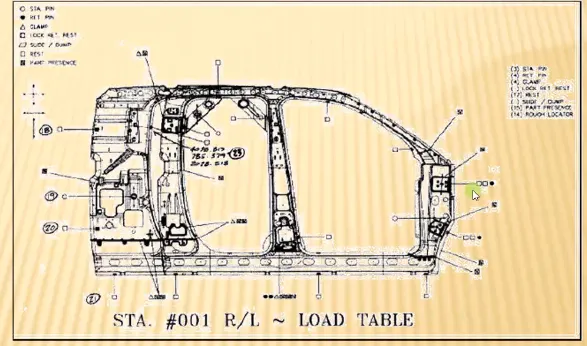
1.GD&T: It provides information of locating pins, rest, clamp, damp & slide unit informationof each station. Also includes the information of sequence of openings of clamps, dumps & slide stroke information.
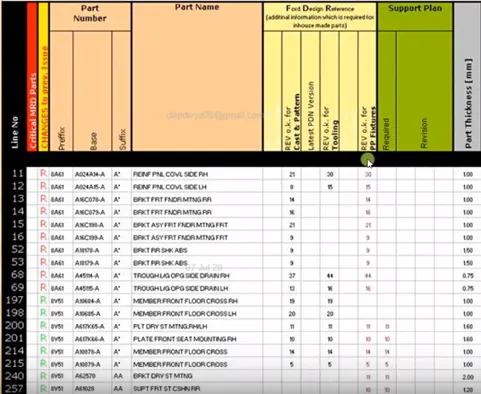
2.Part lists: It gives the lists of parts which are going to assembled in the fixture. The list contains the information of part number, part name, revision of fixture, part thickness, etc.
3.Clamp plan: Clamp plan provides the information of location of pins, Rest units, clamp unit, dump etc. It is the important input from customer. The clamp plan/position should not be changed without the knowledge of customer.
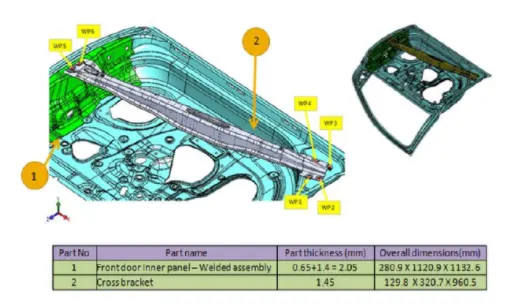
4.3D cad file: The 3D model of the car part will be given from customer. From that 3D model we will be developing our fixture design process. The 3D cad file will be in the format of step file (stp) or IGES file (igs).
5.Product assembly process sheet: It gives the information of stage wise assembly process like how the parts move from one assembly process like how the parts move from one assembly station to other after the completion of joining process.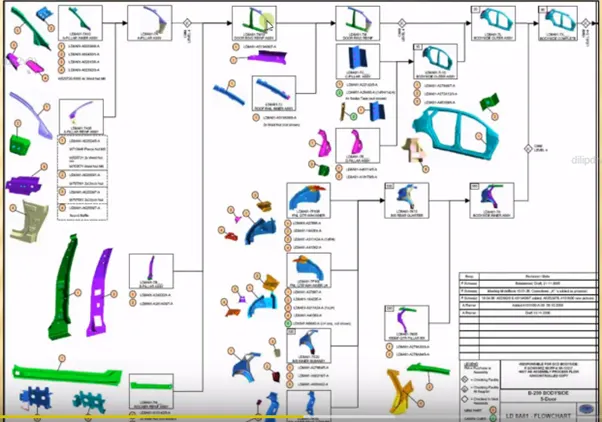
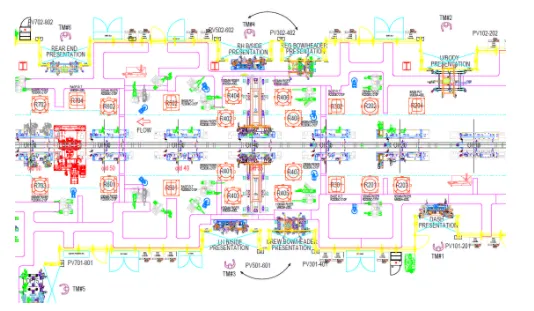
D) Layout - Layout provides information about Flow of parts, Station pitch, Robot stations, Tool changers, Tip dressers, Platform height, Sub asselmbly links & loading/Unloading sequence.
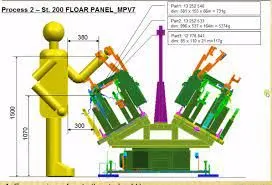
E) Ergo Data - It is the study of human behaviour & movements during the assembly work. It provides data regarding loading height, working safety zone of the operator etc.
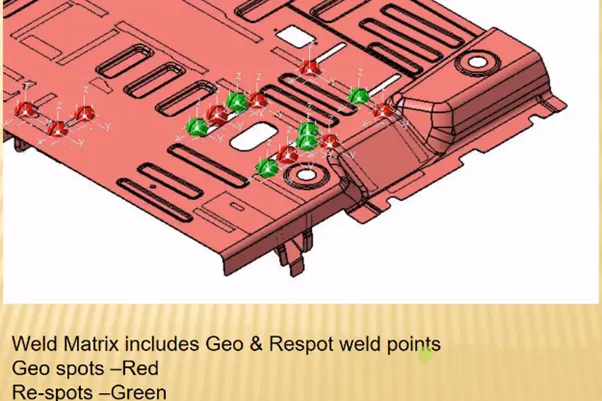
F) Weld study - It includes the study of the weld gun is going to be used for th operation depending on the size of the part, Thickness of the part etc. It also includes the study of the weld matrix & the weld point positions. There are two types in weld point one is geo weld points which ensures the geometry of the assembly & second is the Re spot weld points which adds strength to the already welded point.
G) Standard detailing templates - Every customer have their standard of detailing & the templates which are used for 2D drawing & detailing.
3.What is the input we get from "Car Products"?
INPUTS WE GET FROM CAR PRO DUCTS:
Inputs we get from car products includes;
- GD&T.
- Part lists.
- 3D cad file.
- Clamp plan.
- Product assembly process sheet.
C. Car Products:
The inputs we get from car products are: GD&T, part list, Cad files of car part, Clamp plan, product assembly process sheet.
1.GD&T: It provides information of locating pins, rest, clamp, damp & slide unit informationof each station. Also includes the information of sequence of openings of clamps, dumps & slide stroke information.
Tolerance important:
In Assemblies Parts will often fit together if their dimensions do not fall with in a certain range of values.
In Interchangeability If a replacement part is used, it must be a duplicate of the original part within certain limits of deviation.
The relationship b/w functionality and size or shape of an object varies from part to part.
2.Part lists: It gives the lists of parts which are going to assembled in the fixture. The list contains the information of part number, part name, revision of fixture, part thickness, etc.
3.Clamp plan:
Clamp plan is very important input from the customer. the Clamping plan of the part is the plan which defines the location of the clamp while doing the operation to ensure the geometry of the assembly.We can not change the clamp plan without the permission of the customer.We have to design fixture which should not required change in the clamp plan.It provides information regarding to the location of pins, Rest, Clamps, Dumps etc. The coordinates is also mentioned in the clamp plan so the design team can take the cordinates directly & start the designing of the fixture.
4.3D cad file: The 3D model of the car part will be given from customer. From that 3D model we will be developing our fixture design process. The 3D cad file will be in the format of step file (stp) or IGES file (igs).
5.Product assembly process sheet: It gives the information of stage wise assembly process like how the parts move from one assembly process like how the parts move from one assembly station to other after the completion of joining process.
4.What is the Clamp plan?
Clamp:
A clamp is a fastening device used to hold or secure objects tightly together to prevent movement or separation through the application of inward pressure.
requirements of clamps:
All clamps must fulfill four essential requirements. They are,
- The work piece must be held rigid while undergoing operations.
- The time required for loading / unloading the tool must be as short as possible, which means the clamping device must be quick acting.
- when subjected to vibration, chattered, heavy pressure the clamping must be positive.
- The clamp must not damage the work piece.
Clamp plan:
Clamp plan is very important input from the customer. the Clamping plan of the part is the plan which defines the location of the clamp while doing the operation to ensure the geometry of the assembly.We can not change the clamp plan without the permission of the customer.We have to design fixture which should not required change in the clamp plan.It provides information regarding to the location of pins, Rest, Clamps, Dumps etc. The coordinates is also mentioned in the clamp plan so the design team can take the cordinates directly & start the designing of the fixture.
.
5.What is the purpose of a Layout?
THE PURPOSE OF THE LAYOUT:
The purpose of the layout is to understand the information about where the fixture & robots are been placed, working area covered by the robot, what are the fixtures assigned for the robots to do the process, etc. layout shows the entire assembly plan to understand the process.
The circle around the robot is the swept area of the particular robot which shows the reachability of the robots particularly with the confine circle.
Layout provides the information of flow of parts, station pitch, robot stations, accessories like tool changers & tip dressers, sub assembly links, plat form height, loading/unloading sequence/height.
Flow of parts: It shows the flow of the parts/panel in the assembly line or shop floor like how component move from one station to other station after the completion of process.
Station pitch: The distance between two stations is known as station pitch. It shows the space constraints between the two stations, which shows in layout.
Robot stations: It shows the position where the robots & their accessories placed, which is shown in the layout.
Sub assembly link: Sub assembly link is nothing but the link between the assembly fixtures & the main assembly line. It shows that how the sub assembly fixtures are linked with the main assembly line.
The main purpose of the layout is to understand the entire plan of the assembly line.
The layout providing the above information like flow of parts, station pitch, robot stations, etc used to understand the working process of robots, what are the fixtures assigned for the robots, space constraint, etc.
By considering the layout, the designers can develop the concept sketches of fixtures without any clash in the assembly lines.
6.What is Ergo data?
ERGO DATA:
It is the study of human behaviour & movements during the assembly work. It provides data regarding loading height, working safety zone of the operator etc.
The final assembly of an automobile involves tasks of complex nature. These processes are on the least priority for automation. Manual labor is best suited for assembly operations with the aid of minimal level of automation. All the processes have to be improved continuously in order to reduce the costs and increase productivity .The workers attain various postures, exerts force and works continuously in cycle time to accomplish the assembly task. Working along automobile assembly lines is characterized by repetitiveness.
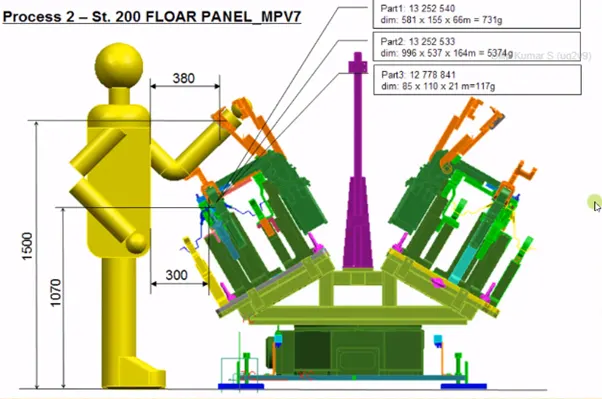
- Physical access (space) for hands or tools and clear visual viewing angle
- Eliminate obstructions in front of working area forease of access e.g. knob position
7.What do you understand by Weld study?
WELD STUDY:
Weld study is the important inputs from the customer.It gives the study of particular gun that we use for weld, No. of spots to be welded, sequence of weld, position of weld in the components. In short, weld study includes weld gun details, weld matrix & weld points.
Generally the weld points will be given in spheres.
Red sphere represents the Geo spot weld points whereas Green sphere represents the Respot weld points.
The weld points are classified as,
1. Geo weld points:
The Geo weld points are which is planned in the Geo fixture.
These weld will determine the position of the panels as per the given data in drawing.
The geo weld points are represents in red sphere in the weld study inputs given by the customers.
2. Respot weld points:
The respot weld points are planned in the respot tool.
These weld will determine the strength/stiffness of the panel/components.
The Respot weld points are represent in green spheres in the weld study inputs given by the customers.
8.What are the criteria for percentage completion in the designing stage? Explain it in detail
THE CRITERIA FOR PERCENTAGE COMPLETION IN THE DESIGNING STAGE:
The percentage completion criteria is followed in the designing stages & dispatch stages of welding fixtures.
This percentage completion criteria is followed to trace the project whether it matches the committed date given to the customer for hand over the projects to them.
Also it helps us to identify the stages in the projects like how much the project is completed and what are the further stages are in pending, to complete which helps us to complete the projects on the committed time and date.
The percentage completion criteria is divided into four stages to identify the percentage of the completion of work.
The four stages of percentage completion criteria are as follows,
- Input & concept design.
- Concept approval & simulation check.
- Design freezing & detailing.
- Check & final dispatch.
(a) Input & concept design- 0 to 25%
The design inputs from the customer & after studying those inputs the concept fixture designs are created.
(b) Concept approval & Simulation check- 25 to 40%
The concept design approval from the customer after study of simulation.
(c) Design freezing & detailing- 40 to 85%
After the simulation result if no any changes are required then the design is freezed. After freezing the 2D drwaing which is the detailing part is started.
(d) Check & final dispatch- 85 to 100%
After detailing the quality checking team start inspection of all the data & it will dispatch to the customer if everything is ok.
9.Brief about "Output" in design?
Each manufacturer shall establish and maintain procedures for defining and documenting design output in terms that allow an adequate evaluation of conformance to design input requirements. Design output procedures shall contain or make reference to acceptance criteria and shall ensure that those design outputs that are essential for the proper functioning of the device are identified. Design output shall be documented, reviewed, and approved before release. The approval, including the date and signature of the individual(s) approving the output, shall be documented.
The outputs of design and development shall be provided in a form that enables verification against the design and development input and shall be approved prior to release.
Design and development outputs should
- meet the input requirements for design and development,
- provide appropriate information for purchasing, production, and for service provision
- contain or reference product acceptance criteria, and
- dspecify the characteristics of the product that are essential for its safe and proper use.
For unitized tools (multiple unit in a common base) requires two types of drawing sheets.
Example of the unitized tool: a tool with multiple unites like rest unit, clamp unit, sensor unit ,etc. in a common base
The two types of drawing sheets are,
- key sheet
- Layout sheet
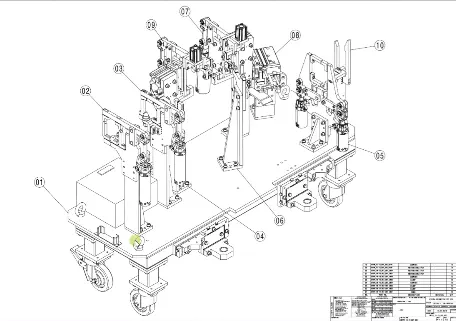
1. Key sheet
key sheets gives or shows the index of unit & their placements on the tool base.
It will have an orthogonal view of the fixtures including a numbered balloon drawing mentioning the units.
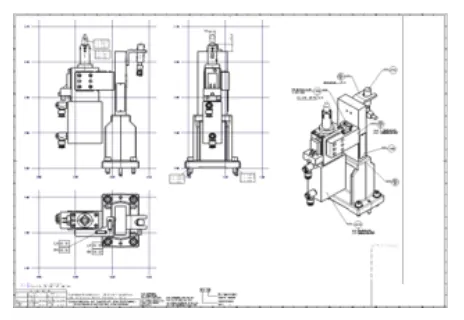
2. Layout sheet:
Layout sheets shows as detail drawing of individual unites to include all of components.
For the Non unitized tool no need of key sheets. As they can stand alone, the drawing can be detailed completely on a layout sheets.
THE DESIGN OUTPUT SHOULD COMPILE FOLLOWING POINTS:
- Approved standard components are to be used wherever possible.
- Design must be as simple & economics as possible.
- Design must be comply with all current safety & ergonomic requirements.
- Design must provide for controlled & damage free handling of product.
- Adequate error proofing provision must be incorporated into each design by proving proximity switches, rough locators, etc.
- The weight of the moving parts must be kept to a minimum while maintaining maximum strength.
- Frames & structures are to be simple & study.
- Design clearance & accessibility for routine maintenance & service.
- Motion control must be considered on any moving equipments.
- Designer is responsible to validate clamps & weld guns.
10.What do you understand by structuring a design tree? How does it reduce errors during the design process?
Structuring a design tree implies to a process where all the assemblies & parts are named in a specific standard. Diffrent customers have their different set of standards to structure a design tree.
- It is an important process which helps us to identify a specific part or assembly as to which project, tool or unit, it belongs to.
- This helps us to avoid the errors during design study, manufacturing, assembly, inspection etc.
- If the parts or assemblies are not properly or the design tree is not structures properly, it will create confusion to understand the design & may create major possibilities of making an error.
- Naming of a fixture or a unit or a part, ives the information as to which project or zone or assembly do they belong.
- It can help us to identify the quantity of items of same type or differnet types are being used in assembly.
Steps for structuring the design tree:
- Create new à Product à click OK (by clicking ok now you will enter into a product window)
- Then right click product in a structure tree à go to properties à rename in part number (As we created a product we have to mention the total assembly name of the fixture) à click ok.
- The naming of the assemblies / parts / units have certain standard procedures, which I have clearly explained below.
- The product name is title of the fixture. The renamed titled should be à P001_Z03_ST09_00_00_RP001 – represent the project name.
Z03 – Zone name.
Panel name will also be mentioned in some case.
ST 09 – Station name / J03 – Jig name will be mention sometimes.
00 – unit name.
00 – Part number.
R/L – is representing the right hand side / left hand side of the panel.
The other renamed title explained in video is
H1L_19A_RRFRA_JG3_00_00_R.
H1L_19A – Project name.
RRFRA – Panel name.
JG3 – Jig name/number.
00 – unit name
00 – Part number.
R – Indicates right side.
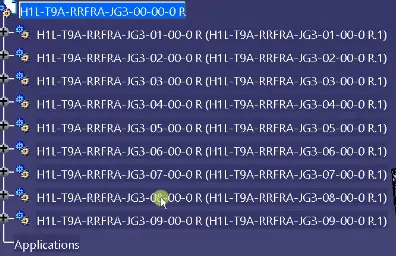
and the most thing is you should places the designed parts are at top position of the tree and standard parts are at bottom position of tree.so it ill helps to easy finding of differentiating the designed and standard parts.
11.What are Units? Mention 5 types of units.
UNITS:
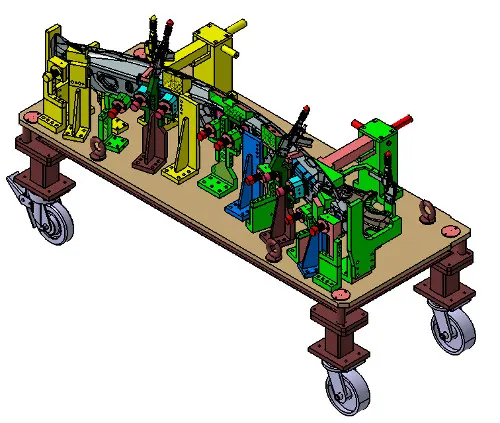
A unit is a device that has a specified function, especially one forming part of a complex mechanism. A welding fixture is assembly of different types of units.
As name refers, the different units will be only seen in the unitized tool.
units are classified into two, they are,
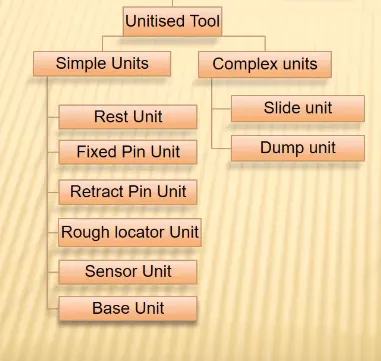
1. Base unit:
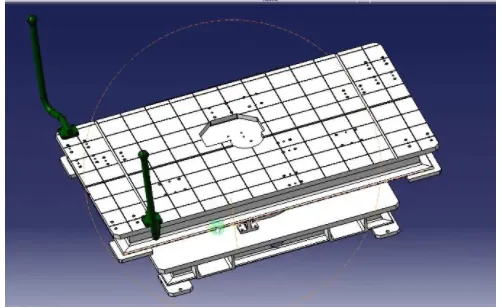
Base unit is the unit designed to mount all other units such as clamp unit, pin unit, rest unit etc., of tool, also other parts necessary for a tool like pneumatic valve box, trunk cable path will also be mounted on to be a base unit.
2. Fixed pin unit:
Fixed pin unit is a unit designed to locate the car panel using pins.table
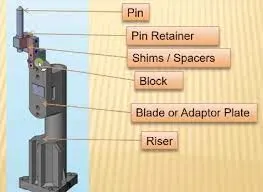
Pin, pin retainer, shims, blocks, blade, riser are the part of fixed pin units.
Pin retainer is used to hold the pin firmly.
Typically, the locating pins are used to locate a body part in a position sufficiently accurate to execute a welding process.
The body part is constrained by a set of appropriately locating pin so total constraint by locating pin should be fully constrained at all times to prevent any movement.
3. Retractable pin unit:
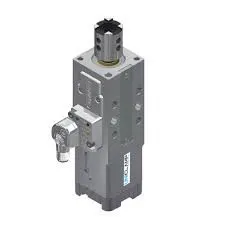
retractable pin unit is unit designed to locate the car panel using pins, but the entire pin package parts will be mounted on the retractable pneumatic cylinder as shown in below fig 3.
Retractable pin unit is the opposite of fixed pin unit which can be moved up & down also which can be retracted till certain distance.
It is mainly used for unloading the complex panel after welding.
4. Clamping unit:
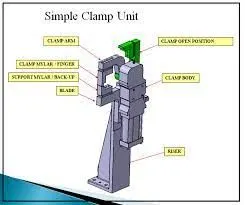
Clamp unit is a unit designed to clamp or hold the car panel with NC block / Mylars by using a pneumatic clamp cylinder.
Clamping unit is used to clamp the part which is to be welded after location using pin unit.
Clamping is achieved with the help of pneumatic cylinders and clamp arms.
Clamping arm, finger, rest, shims, standard riser, pneumatic cylinder are the parts of clamping unit in general.
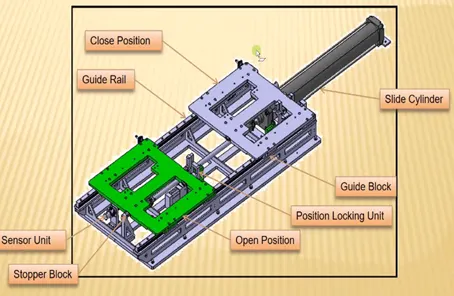
5. Slide unit:
Slide unit is found mostly in complex fixture, where the sliding mechanism will be involved.
This type of unit used when there is some space constraints.
Guide block, guide rail, position lock unit, stopper block, sensors are the parts of slide unit in general.
Guide block & guide rail helps to the guide the slide unit. The rail should always be covered to protect against weld spatter & dust by a bellow or a sheet metal cover.
Position lock unit helps the slide to be locked/clamped in the working position.
Stopper block helps to stop/control the entire moving of a slide unit from certain distance, which is placed at the end of the guide rail.
Sensors – The two end limits to be sensed externally by a proximity sensor.
12.Describe Fixed Pin units & their purpose?
- Fixed pin unit consist of riser, blade, block, shims or spacer, pin retainer & pin.
- Riser is the standard part which is used to rise up the height of the while unit. Blades are plates mounted on the riser. Other parts like cylinder, arms etc are mounted on the blade.
- Shims are the small part which comes with the thickness of 0.1mm, 0.2mm, 0.5mm etc. These will compensate the stackup tolerance which reflects at the panel holding part called Mylars. In fixed pin shims are used to adjust to traslational motions.
- Pin retainer will support the pin & the locating pin which restricts movement of the car panel.
Purpose of fixed pin unit-
- Fixed pin unit is a unit designed to locate the car panel using pin.
- The fixed pin unit is the part of the 3-2-1 principle. It restricts 6 degrees of freedom of the car panel.
- It is necessary to have 2 pins to locate car panel. one pin must arrest 4 way (4 translational ) & other must arrest 2 way (2 rotational ) of a car panel.
13.What are the different parts of a fixed unit?
DIFFERENT PARTS OF THE FIXED PIN UNIT:
The different parts of the fixed pin units are as follows,
- Pin.
- Pin retainer.
- Shims.
- Blade.
- Riser.
1. pin:
It is used for the location purpose of the panel.
Typically, the locating pins are used to locate a body part in a position sufficiently accurate to execute a welding process.
The body part is constrained by a set of appropriately locating pin so total constraint by locating pin should be fully constrained at all times to prevent any movement.
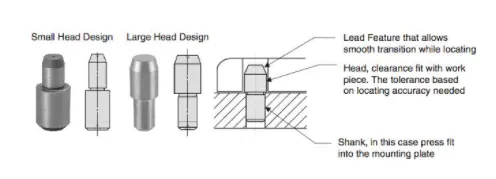
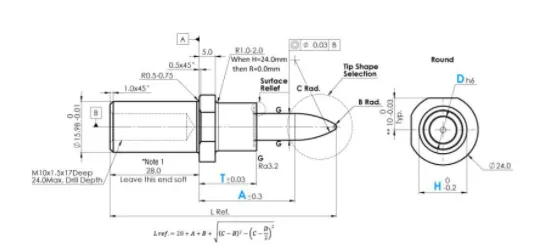
There are dozens of styles of locating pins that can be utilized in a design. Below I have shown the commonly used pins.
One of the most common pins is a stepped pin with either small or large head.
2.Pin retainer - It will support the pin.
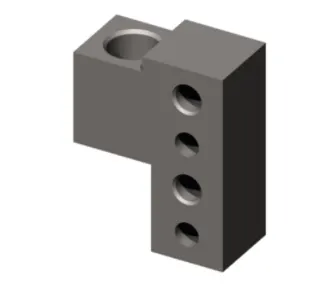
3.Shims- These are the small part which comes with the thickness of 0.1mm, 0.2mm, 0.5mm etc. These will compensate the stackup tolerance which reflects at the panel holding part called Mylars. We give tolerance to all the parts of the fixture. Due to this tolerance the Mylars will either lift up or goes down from its defined position. If the Mylars goes down from the defined height it will make impression or dent on the panel. If the Mylars lift up then there will be a distorsion due to welding stress. To adjust the Mylars At its defined position we use shims so the panel won't deformed & also dont get any impression on it.
4.Blades - These are plates mounted on the riser. Other parts like cylinder, arms etc are mounted on the blade.
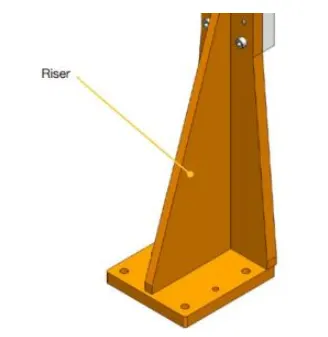
5.Riser- Riser is the standard part which is used to rise up the height of the while unit.
14.What is the purpose of making a Rest unit & describe its parts?
- The rest units are designed to rest/support the car panel by using NC blocks/Mylar/Rest
- It is the simplest unit to design because it have less parts to design & the purpose is only resting of the car panel.
- Because of this simplicity the rest unit is combined with other unit to reduce the cost of the overall project.
It can be combined with clamp unit to clamp as well as to rest the car panel. It can be combined with locating unit to locate as well as to rest the car panel. also locating, clamping & restunit can be combined together in one unit to reduce cost.
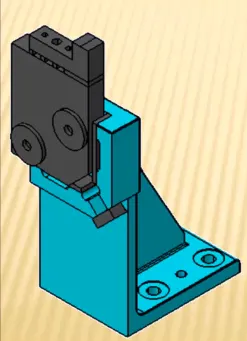
PARTS OF REST UNIT:
The parts of rest unit are as follows,
- NC block/mylars.
- Risers.
- Blades.
- shims
1. NC blocks/mylars:
Mylars are the part which are holding the panel from top & bottom.
It is a jaw type, during welding it wont deforms from its position. It is also known as fingers.
It wont allow the deformation of the part due to welding stresses.
Mylars are of two types, they are
- Clamping mylars
- Resting mylars
Only resting mylars can be seen in rest unit.
The panel which rests on the part is known as resting mylars.
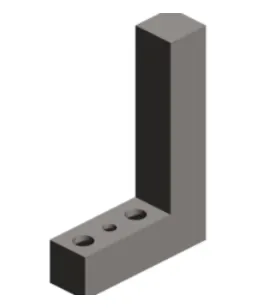
2.Riser- Riser is the standard part which is used to rise up the height of the while unit.
3.Blades - These are plates mounted on the riser. Other parts like cylinder, arms etc are mounted on the blade.
4.Shims- These are the small part which comes with the thickness of 0.1mm, 0.2mm, 0.5mm etc. These will compensate the stackup tolerance which reflects at the panel holding part called Mylars. We give tolerance to all the parts of the fixture. Due to this tolerance the Mylars will either lift up or goes down from its defined position. If the Mylars goes down from the defined height it will make impression or dent on the panel. If the Mylars lift up then there will be a distorsion due to welding stress. To adjust the Mylars At its defined position we use shims so the panel won't deformed & also dont get any impression on it.
15.What are the basic fundamentals to design a Sensor unit?
Sensor is a device which detects or measures a physical property and records, indicates, or otherwise responds to it.
A unit designed to sense car panel using electrical sensors is called sensor unit. The from the sensors is send to the PLC so the next process is executed by this signal. The sensor is very sensitive & easily damagable part so sensor cover is provided to the sensor for safety purpose.
There are different types of sensors
a)proximity sensor
b)laser sensor
c) photo electric sensor
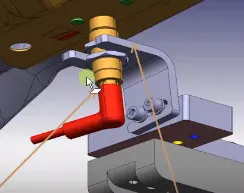
FUNDAMENTALS TO DESIGN A SENSOR UNIT:
- Every single loose panel which are being welded in a tool should be sensed.
- Each panel should be sensed by 1 or 2 sensors depend on the size of the panel, preferred to be in diagonal opposite ends of panel.
- Every sensor should be mounted in a 3 direction adjustable way in general.
- We should try to minimize the size of sensor as much as possible.
- Some major sensor manufacturers are IFM, Pepperl – fuchs, sick, OMRON, etc.
16.What is a Rough locator unit & what are the basic fundamentals to consider while designing it?
ROUGH LOCATOR UNIT:
Rough locator unit is a unit designed to guide the operator to locate the car panel on the oins accordingly.
A rough locator can be standard part or make part.
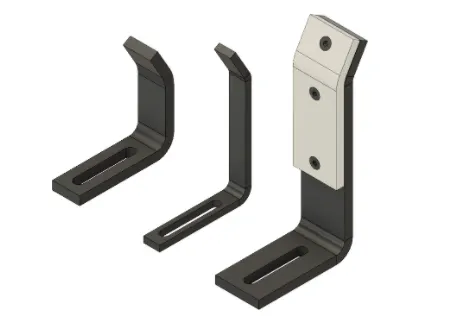
THE BASIC FUNTAMENTALS TO CONCIDAR WHILE DESIGING A ROUGH LOCATOR:
- Rough locator should be placed at the edges of the car panel, which has to guide.
- Rough locator should be placed in the same angle of the car part edge with a minimum distance of 2 – 5 mm from the edge of car part.
- Rough locators should guide the panels in a pin assemble direction in general.
- Rough locators should start guiding the panel before 10 t0 15mm to the start of the pin engagement.
- Rough locators should be designed with entry angle for car part entry as shown in the above figure.
- Rough locators should be designed with two slots to mount for easy adjustment in general.
- The slots should be in the direction of car part guiding.
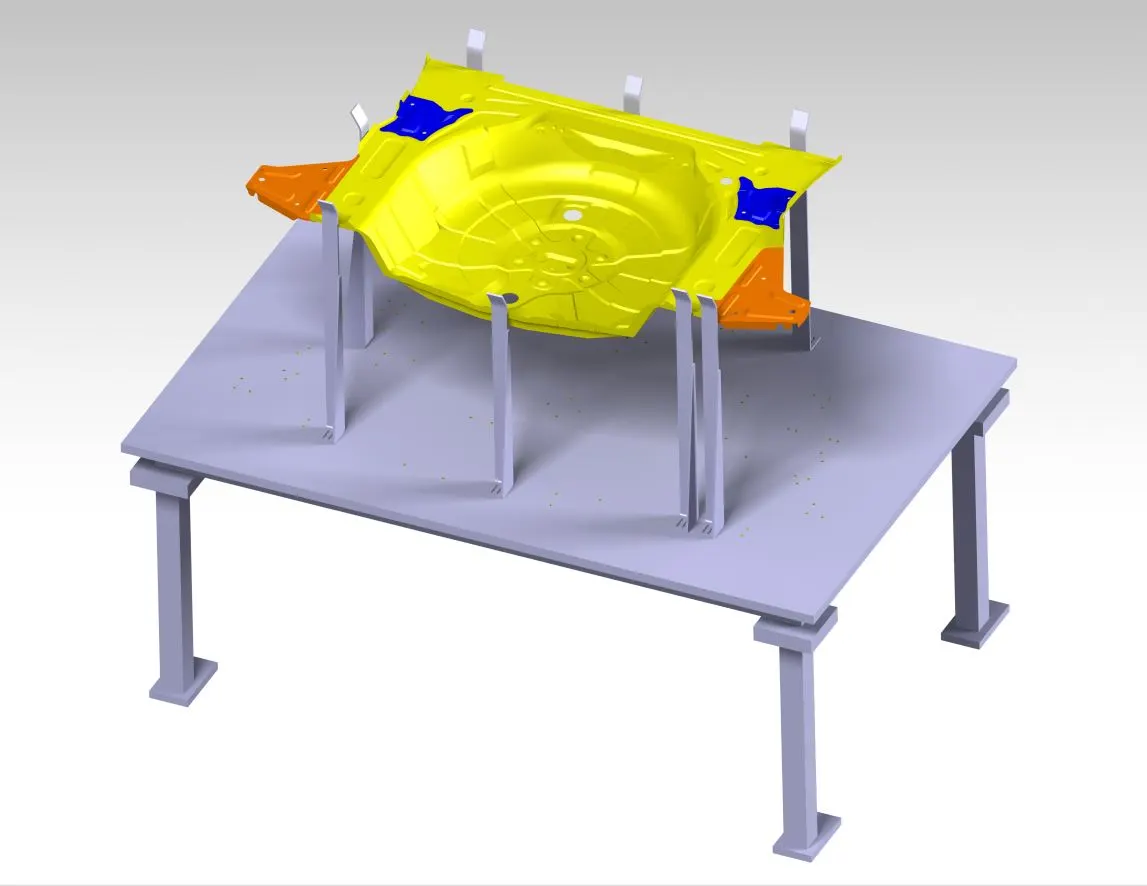
17.What is a Base unit and describe it's parts?
A base unit is the unit designed to mount all the other units(Clamp unit, Pin unit, rest unit etc.) of the tool, also other parts necessary for a tool like pneumatic valve box, trunking cable path will also be mounted on to a base unit.
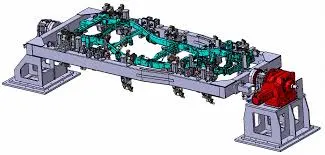
Base unit is the fundamental componet of the fixture because all other components are mounted over it.so every fixture have base unit. The base unit design is different according to the panel, Design of clamp system, location system etc.
parts included in base plate are described below
1)Floor plate- It is the plate which join the fixture to the floor by using some nut bolts. This plate surface is machined for maintaining the horizontal position of the fixture.
2)Weld bars & pedestal- Pedestal is the base or support on which a The fixture is mounted.
3) Eyebolt- An eye bolt is a bolt with a loop at one end. They are used to firmly attach a securing eye to a structure, so that ropes or cables may then be tied to it.
eye bolt with nut
Machinery eye bolts are fully threaded and may have a collar, making them suitable for use with angular loads up to 45°. Eye bolts without a shoulder should not be used for angular loads.
Heavy forged eye bolts with a continuous eye may be forged with an integral shoulder, allowing their use for heavy off-axis loads.
4) Measuring hole cover - The base plate have some drills to mount various units like clamp, rest, pin etc. & every drill have some coordinates to define the exact location of the hol. Due to irregular shape of the car panel the drilled holes coordinates are not like 110.0, 150.0 But it like 110.62,150.84. The maesuring hole is drilled over the base plate which having exact cordinates so that all other holes can take reference from it. The measuring hole no. depends on the size of base plate. These holes are covered by using some plate to protect against dust, damage etc.
5) Valve box & trunking channel- The valve box is the box which includes different solenoid valves. The pneumatic fixtures work on air pressure provided to it. So the arrangement of air pressure inlet & outlet is done within this valve box. The trunking channel includes all the pressure inlet cables going to the pneumatic parts of the fixture & protects them from damaging while operation is in process.
6) Base plate- Base plate is the heavy plate of large thickness becuase it carries all the weight of the mounted parts. So it must be able to bear the load. Base plate is machined to maintain the parallelity within the tolerance. It also consist some drilled holes to mount the different units over it.
18.What is a Dump Unit and what are its functions?
DUMP UNIT:
Dump unit is found in complex fixture.
Dump unit is used when there is any geometrical constraints while placing a panel.
Dump unit consist of dump cylinder to perform clamping & unclamping.
FUNCTION OF DUMP UNIT:
Dump unit plays as a vital role when there is any geometrical constraints while placing a panel.
19.What is a Slide unit? Mention where Slide units are commonly used.
A slide unit is basically used in space constrains in assembling a part. This unit is also a complex unit. It contains sliding bed, cylinder, open position, close position, guide box, position locking unit, sensor unit, stopper block.
Components of a slider unit:
Sliding cylinder
Sliding cylinder has One open position and One closed position, which has to guide rails direction to the entire panel is going to move.
position locking unit
Position locking unit which will lock the position at that particular point doesn't allow the entire plate to move.
Sensor Unit
Sensors need to sense whether this entire component has reached here or not.
Stopper blocks
Stopper blocks as I said initially to control the entire panel moving and it's a moving part.