Week 12- Final project
AIM:
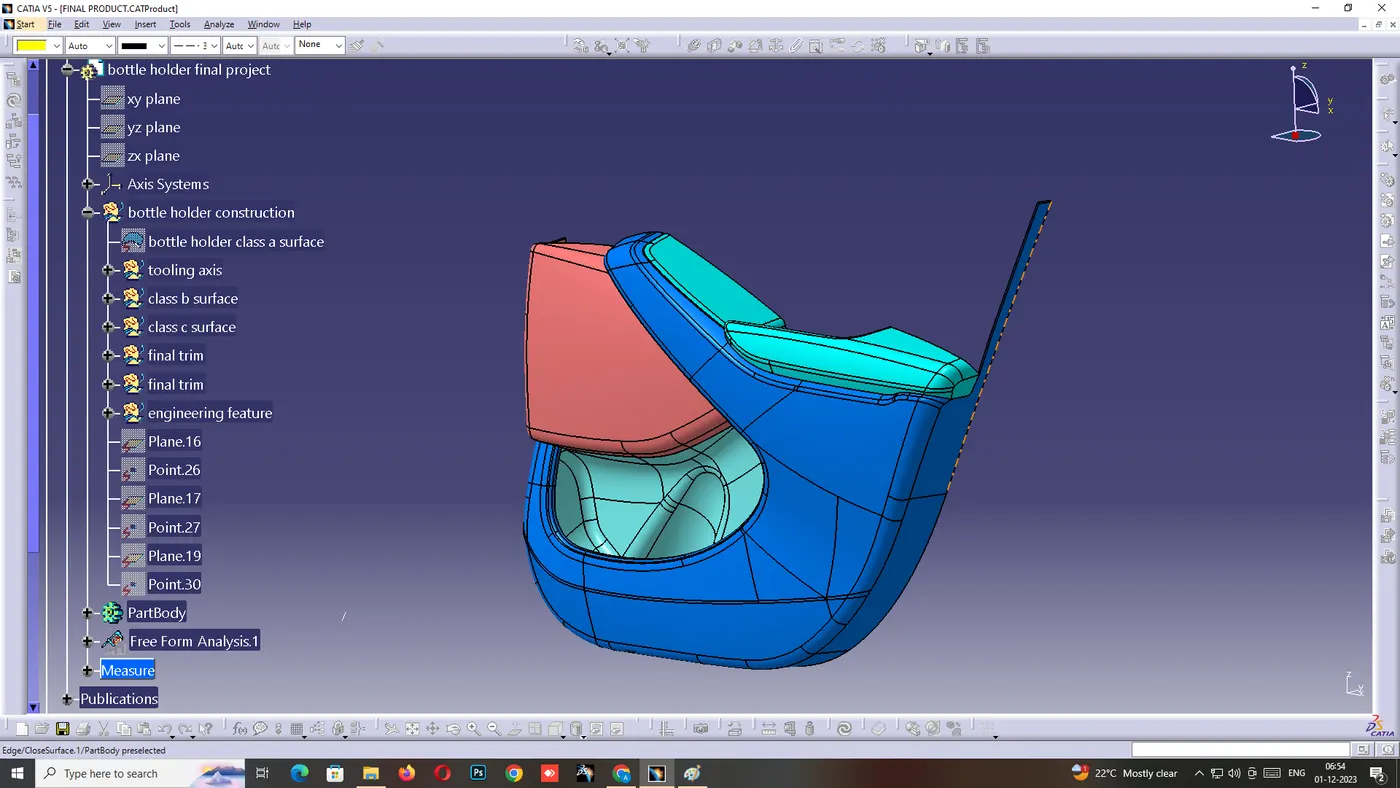
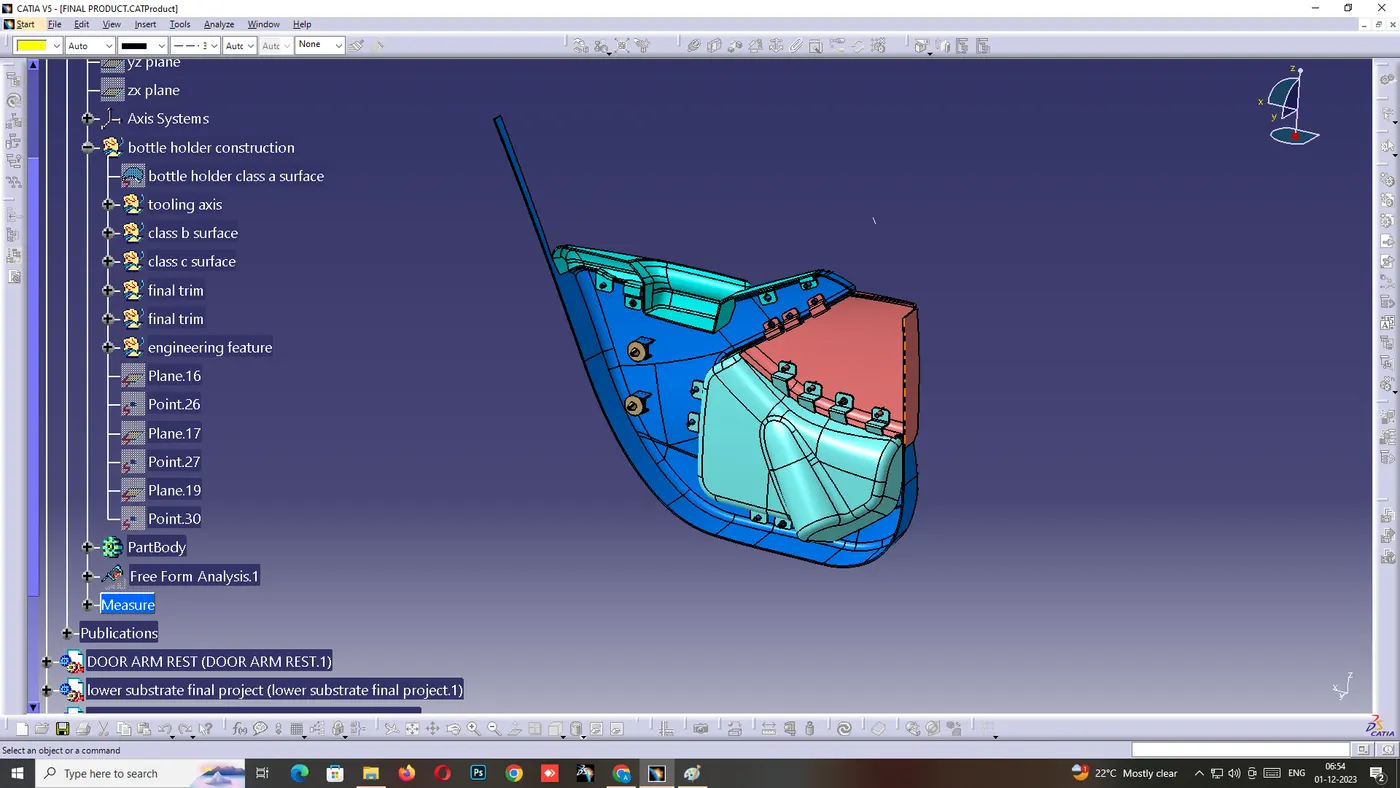
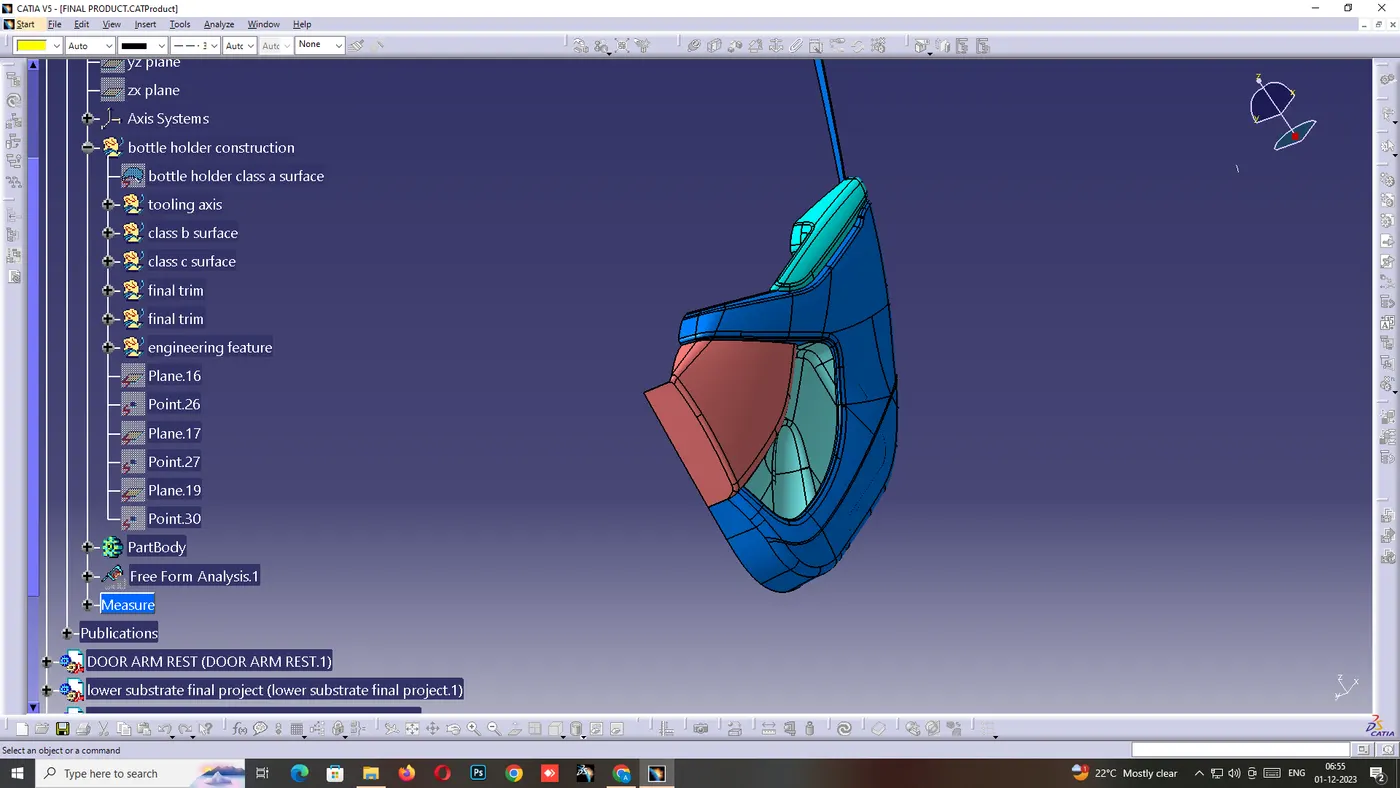
To design and development of vehicle interior door trim using Catia V5 with given class A surface along with Master section. Also create the Side Attachment features as per design rules.
OBJECTIVE:
- To create thickened part using master section for reference
- To create the mounting features as per design guidelines in the industry and with master sections
- To perform Draft analysis & Tooling analysis
The door panel is the interface between the interior of the car and the inner workings of the door. Generally the door panel is divided into parts for easy designing like arm rest, map pocket, lower substrate. These require one of the toughest requirement among the interior parts of the car. This should be designed to with stand the load while being less than 2mm in thickness and also to protect the occupants during collisions.
Door currently have an inner full width panel consisting of electronic windows, central locking system and speakers. These panels typically consists of a foamed core covered with either textiles or plastics.
- Tooling Axis
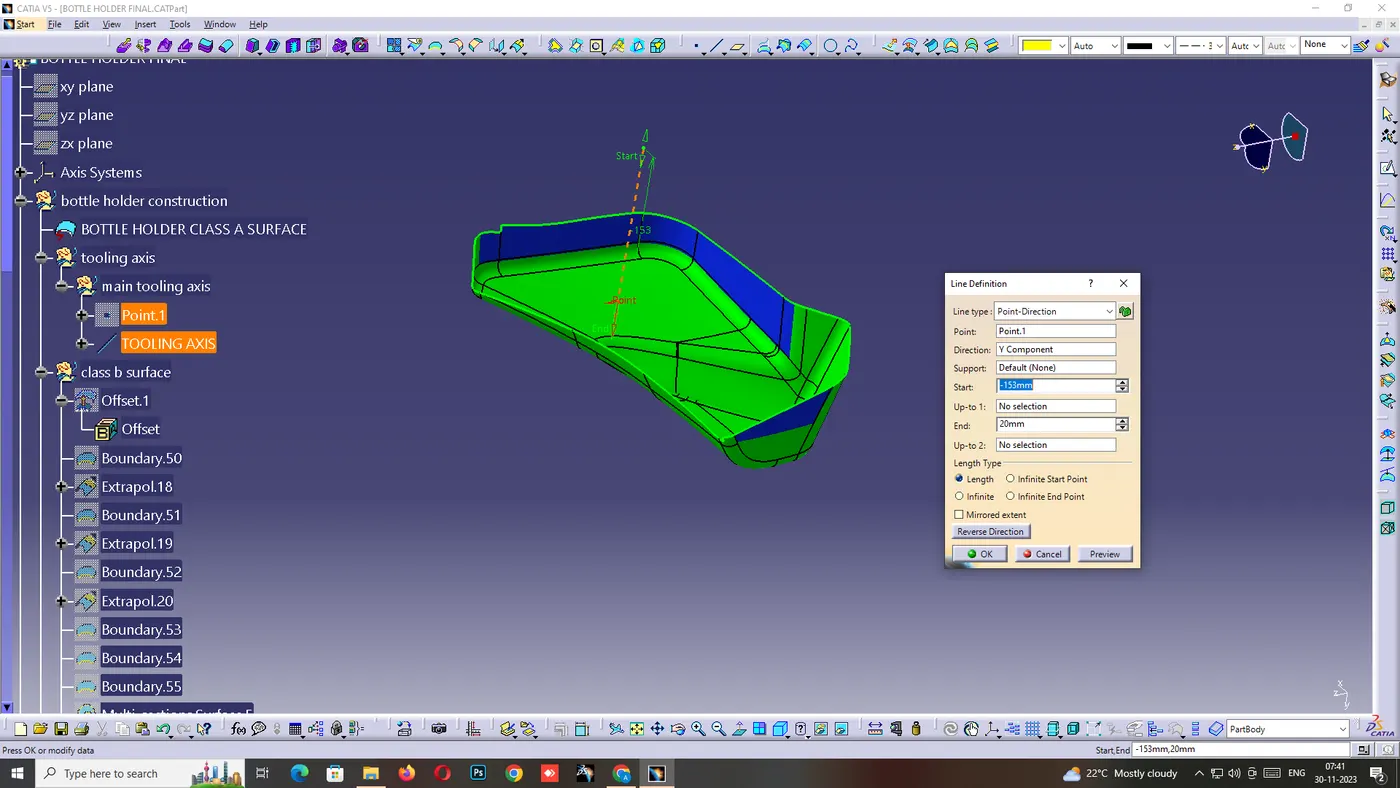
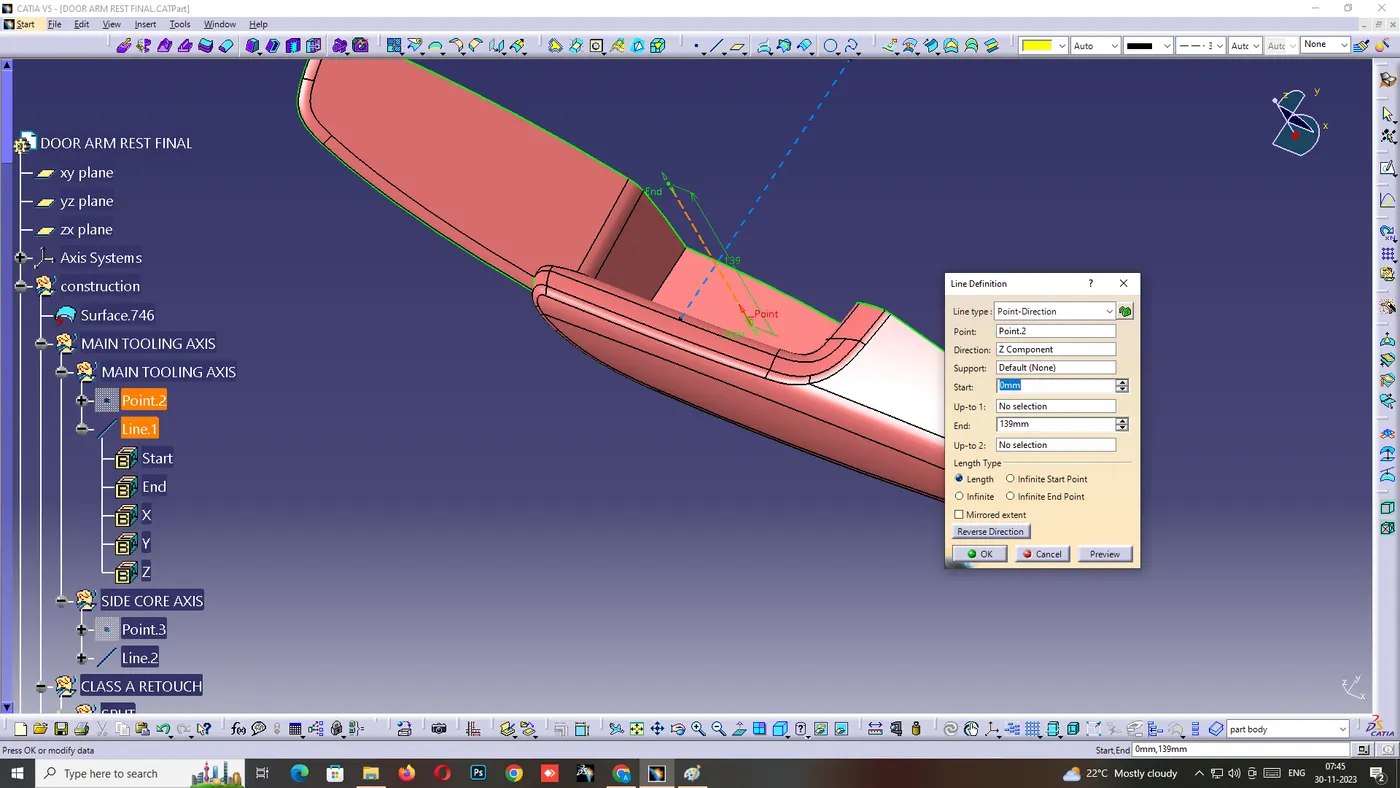
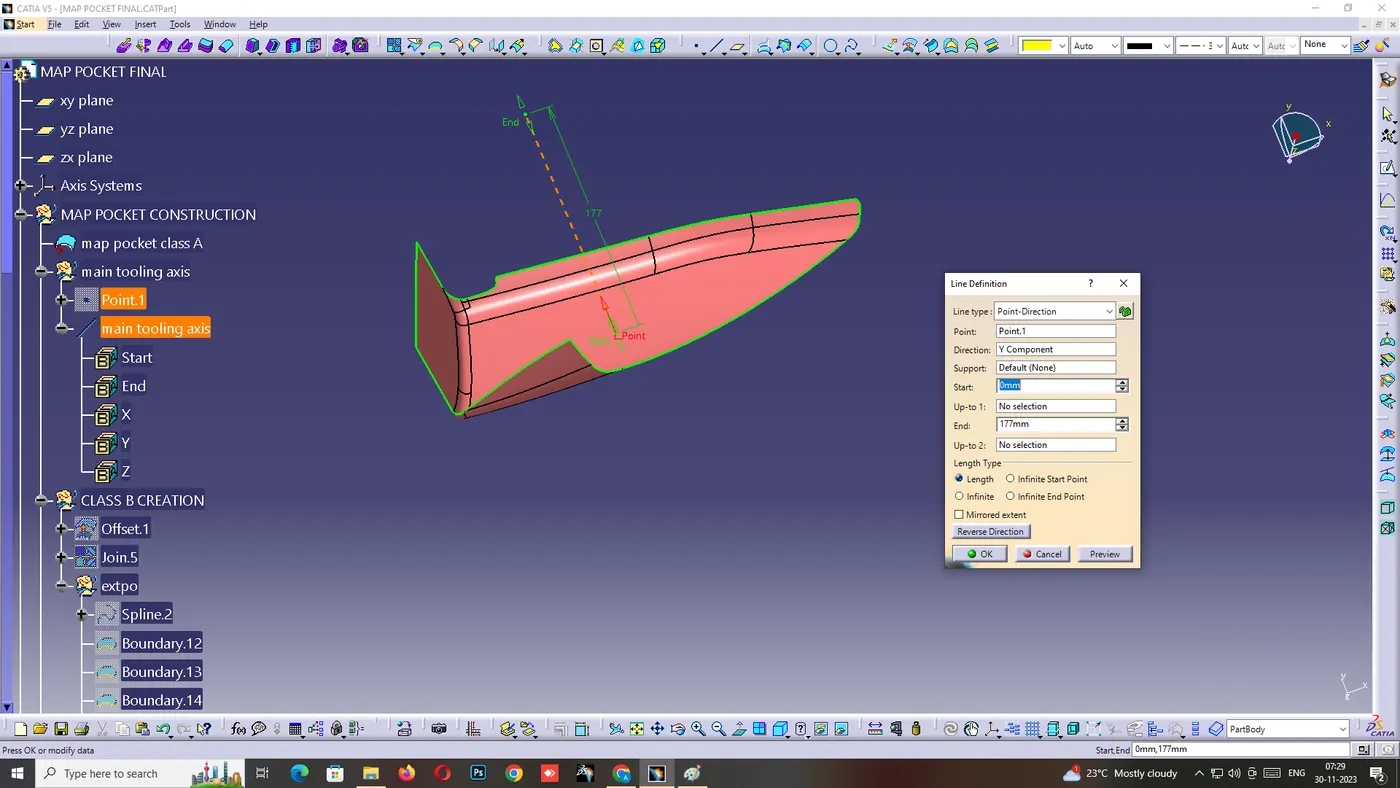
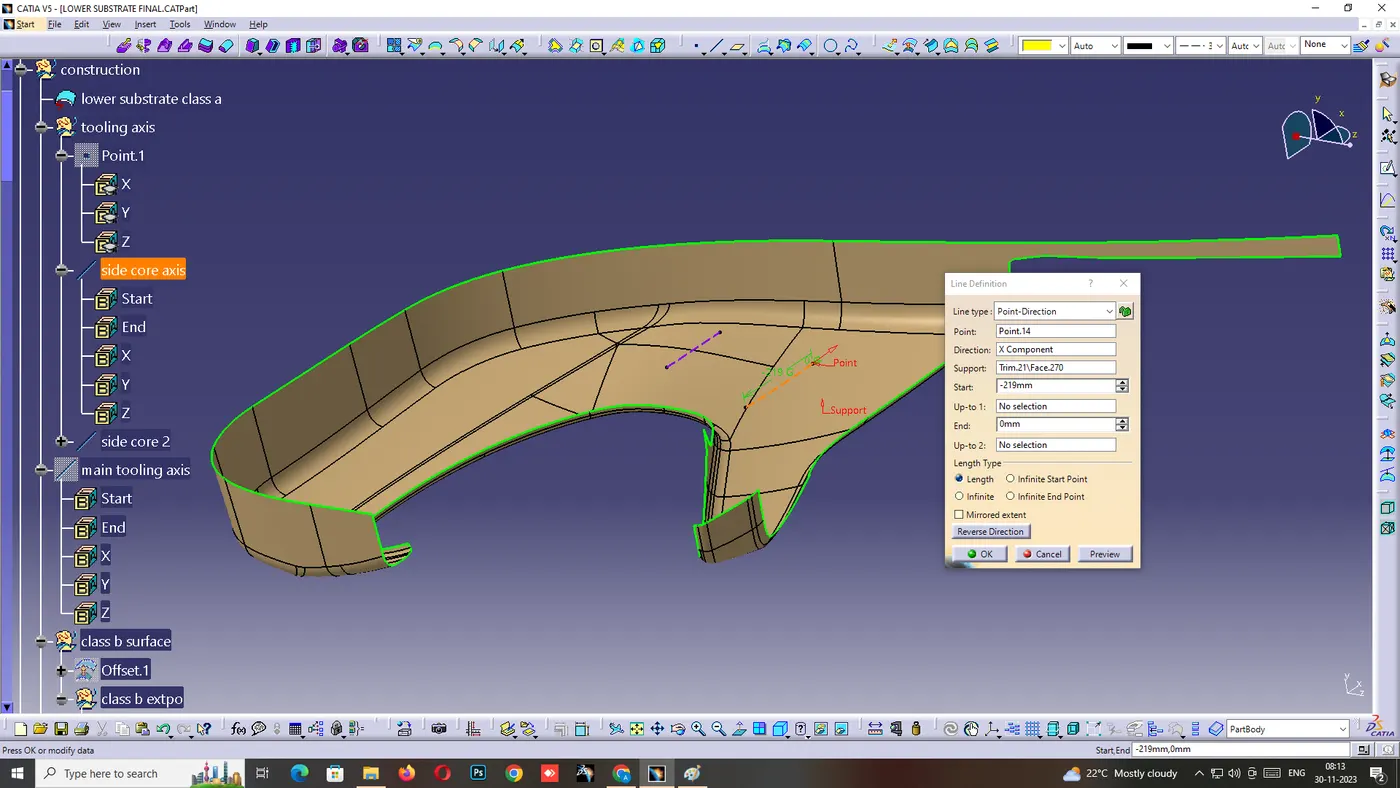
The tooling direction is used to find the direction in which the part is removed from the core and cavity. The draft angle should be positive to the tooling axis to manufacture the component easily. The step by step procedure of creating the tooling axis is given below.
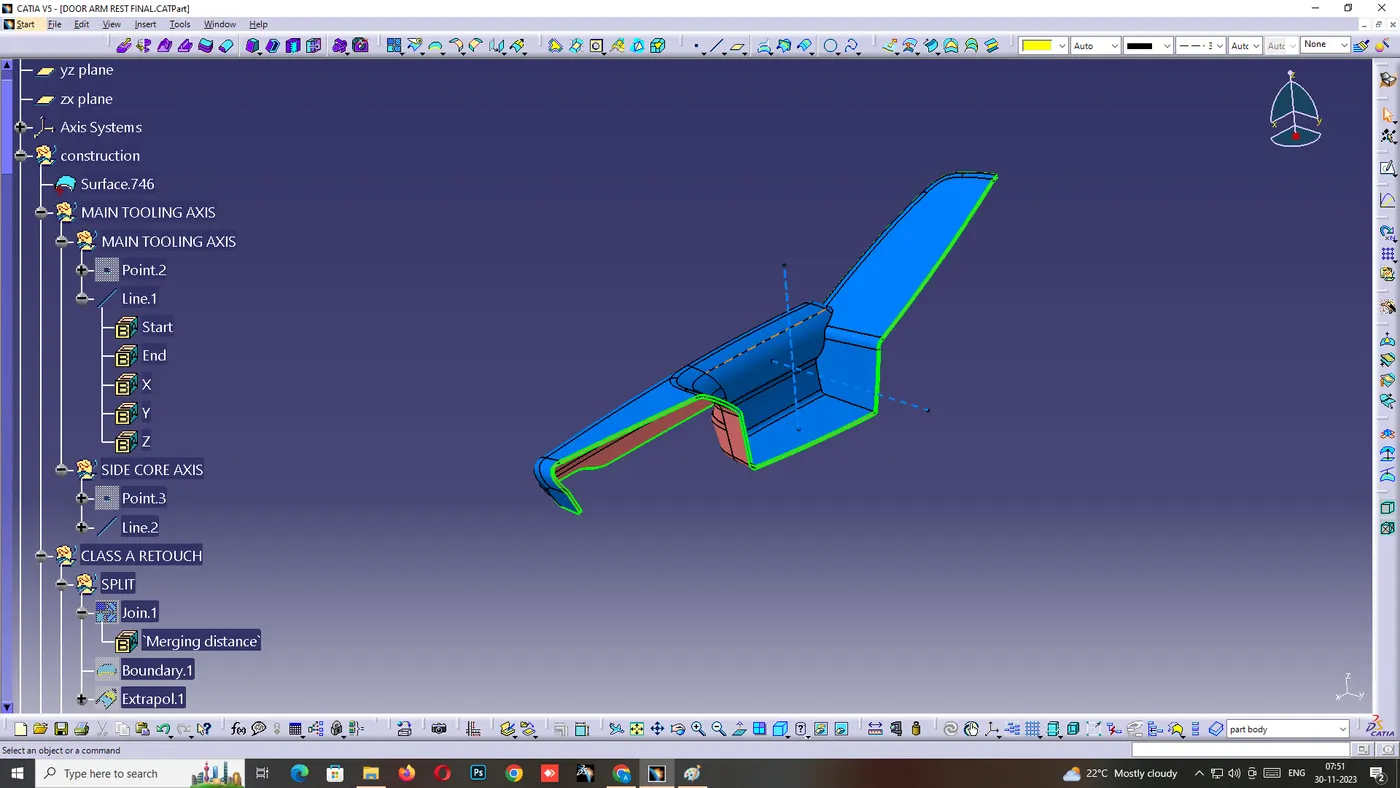
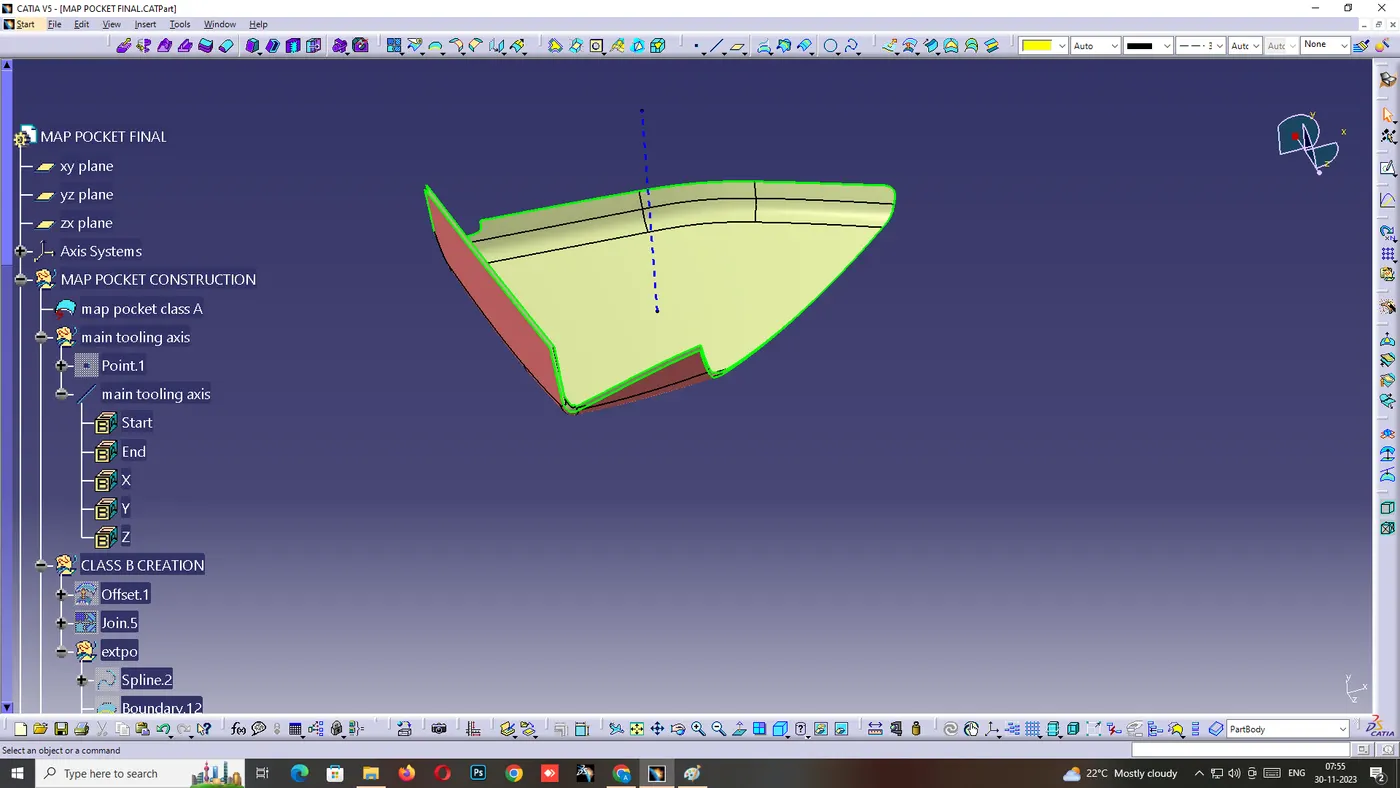
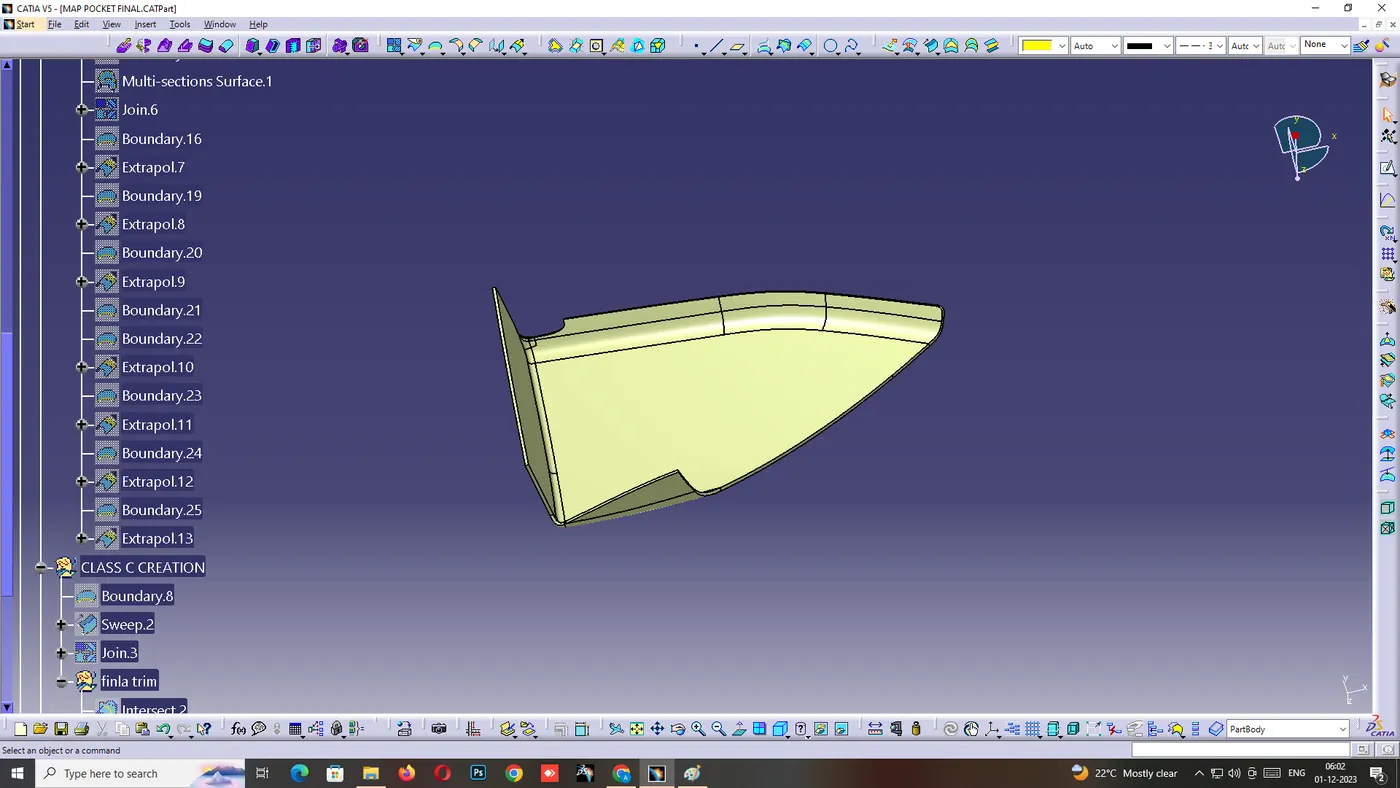
Creating the tooling axis for Map Pocket by create a point on surfaces respectively to the 0 value. It automatically create at mid surface and generate the line to the direction of y axis.
- Creating the B surface.
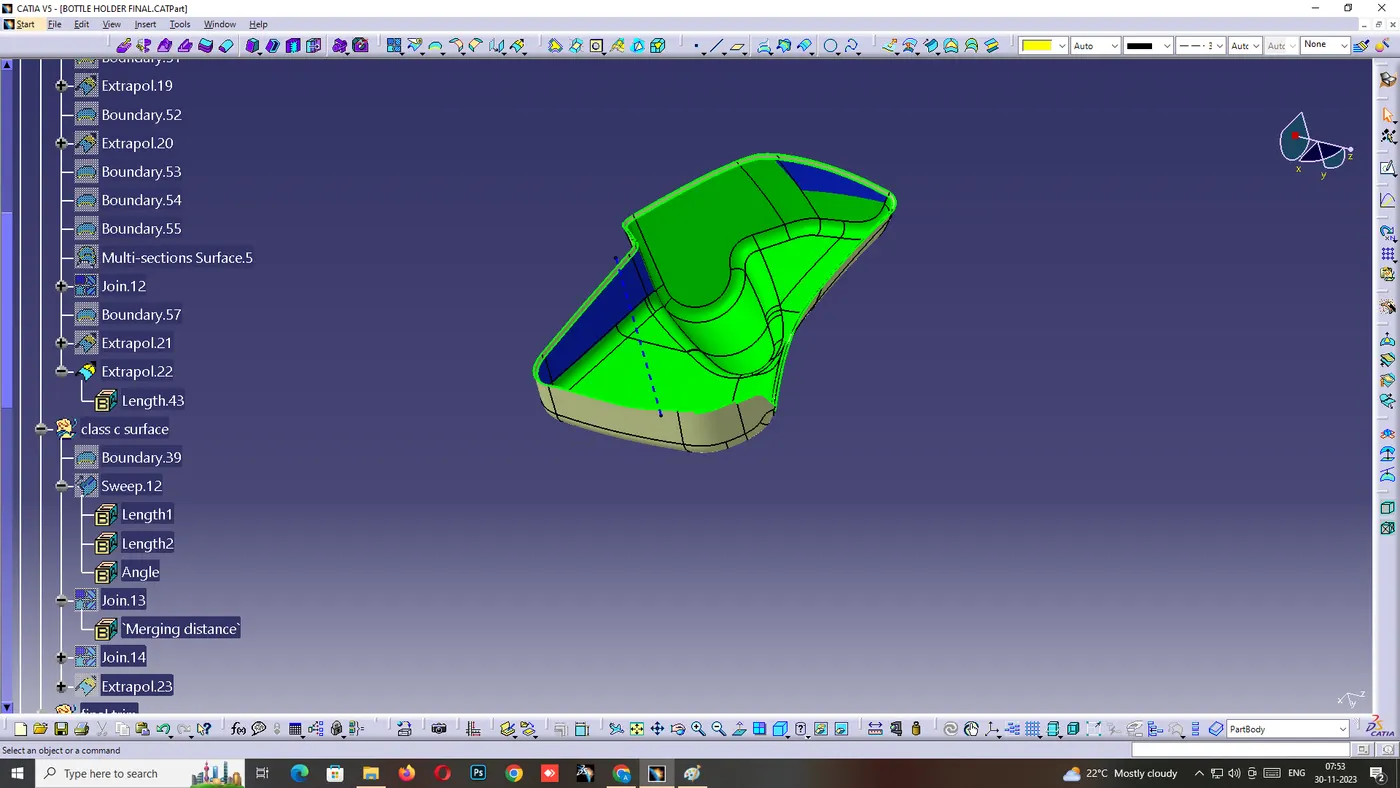
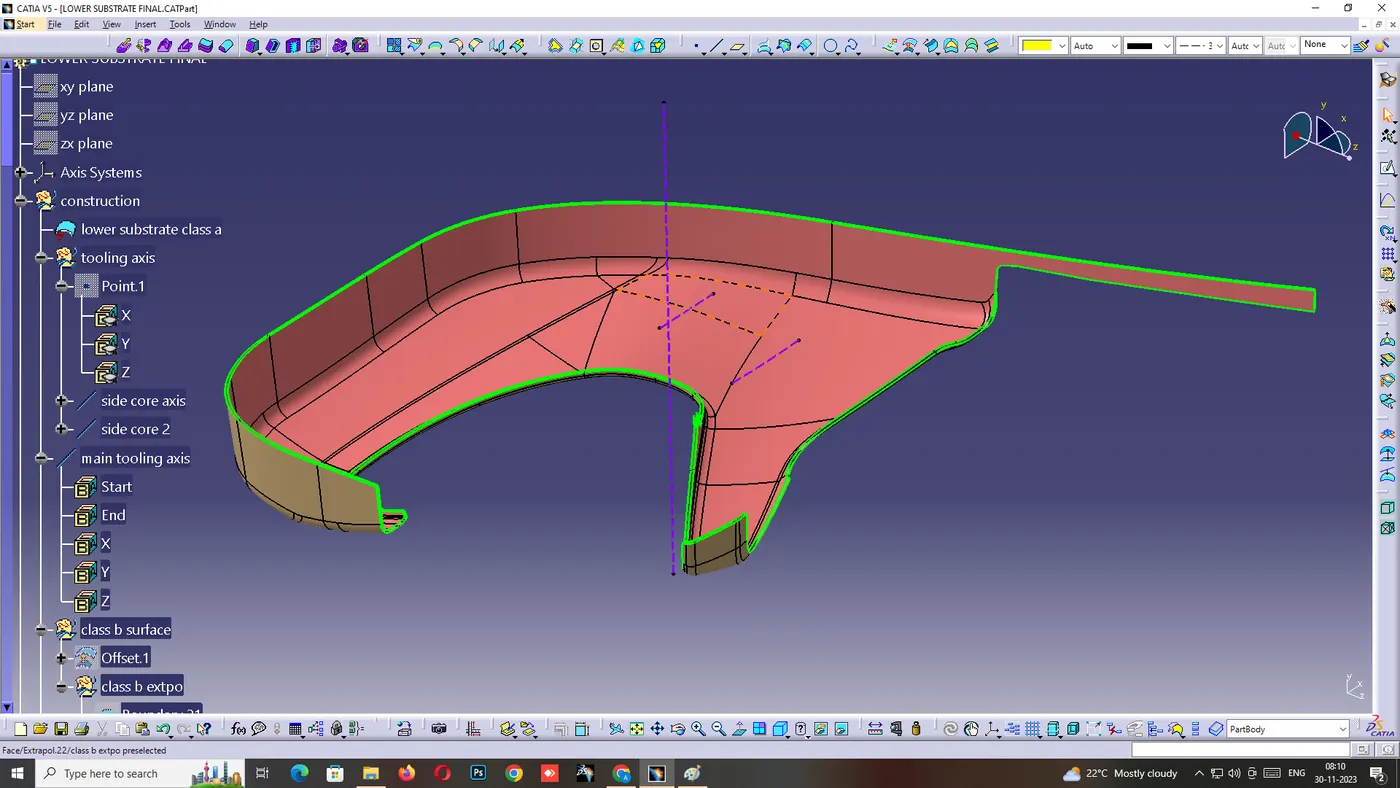
Creating the B-SURFACE by extracting the class A surface, by each surfaces separately, it is offset to certain distance, making point on the master section to get the intersection as shown below.
- Creation of C Surfaces:
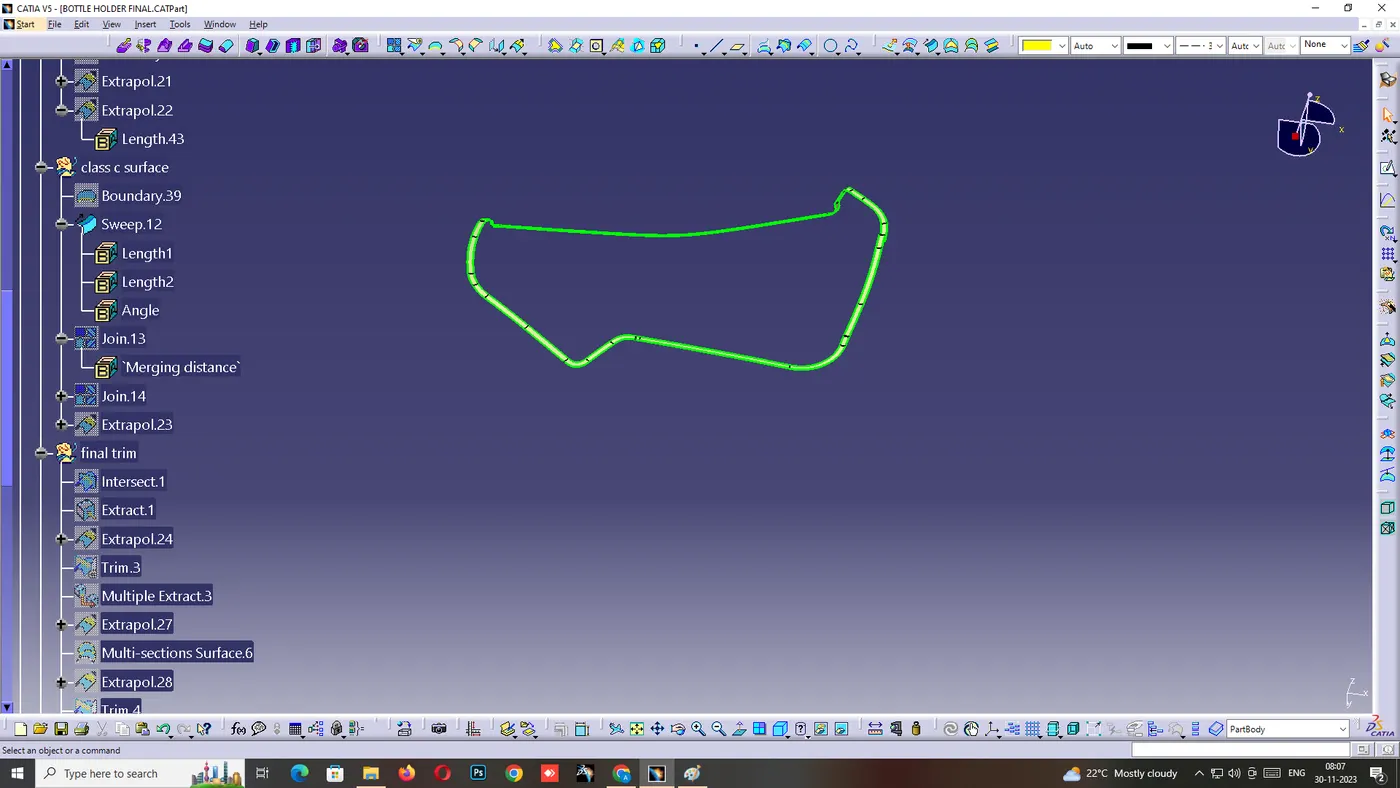
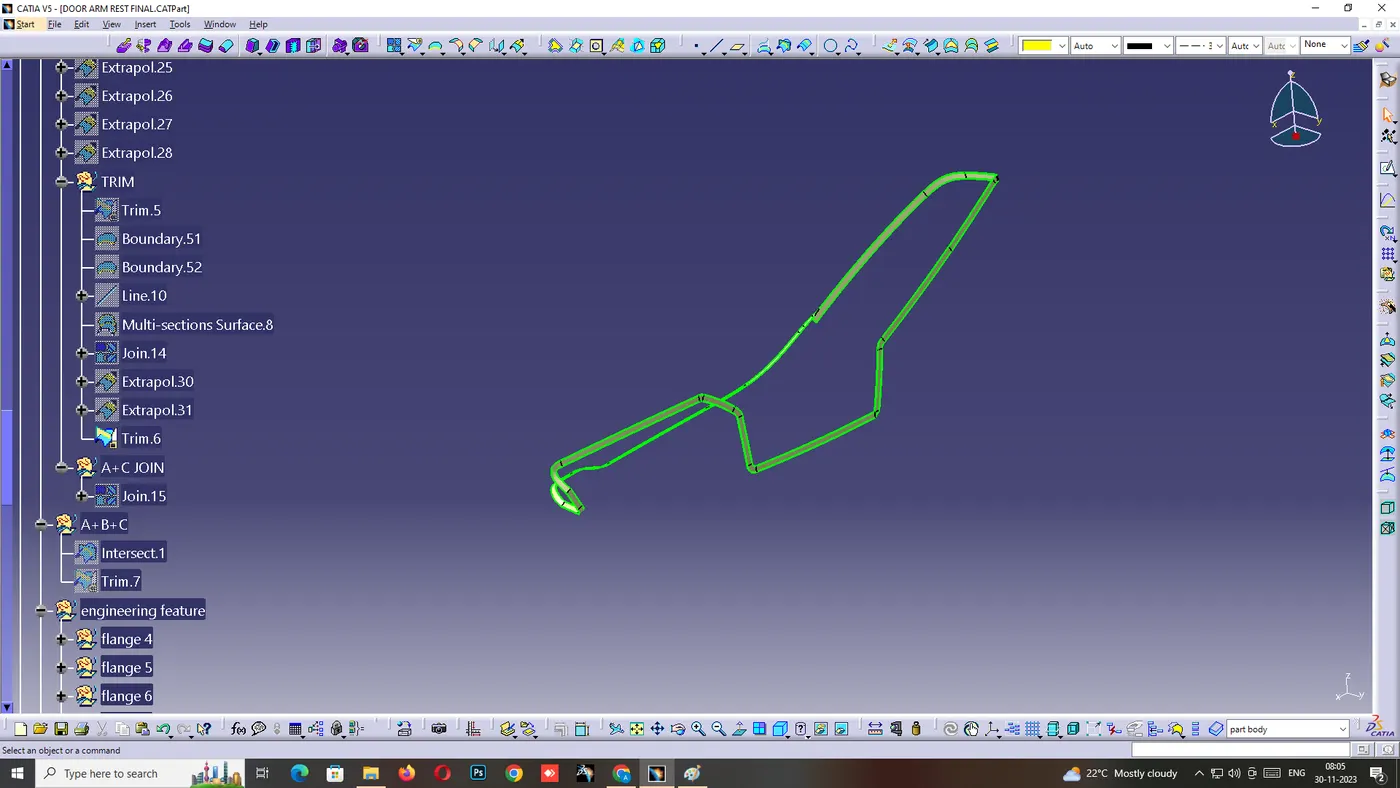
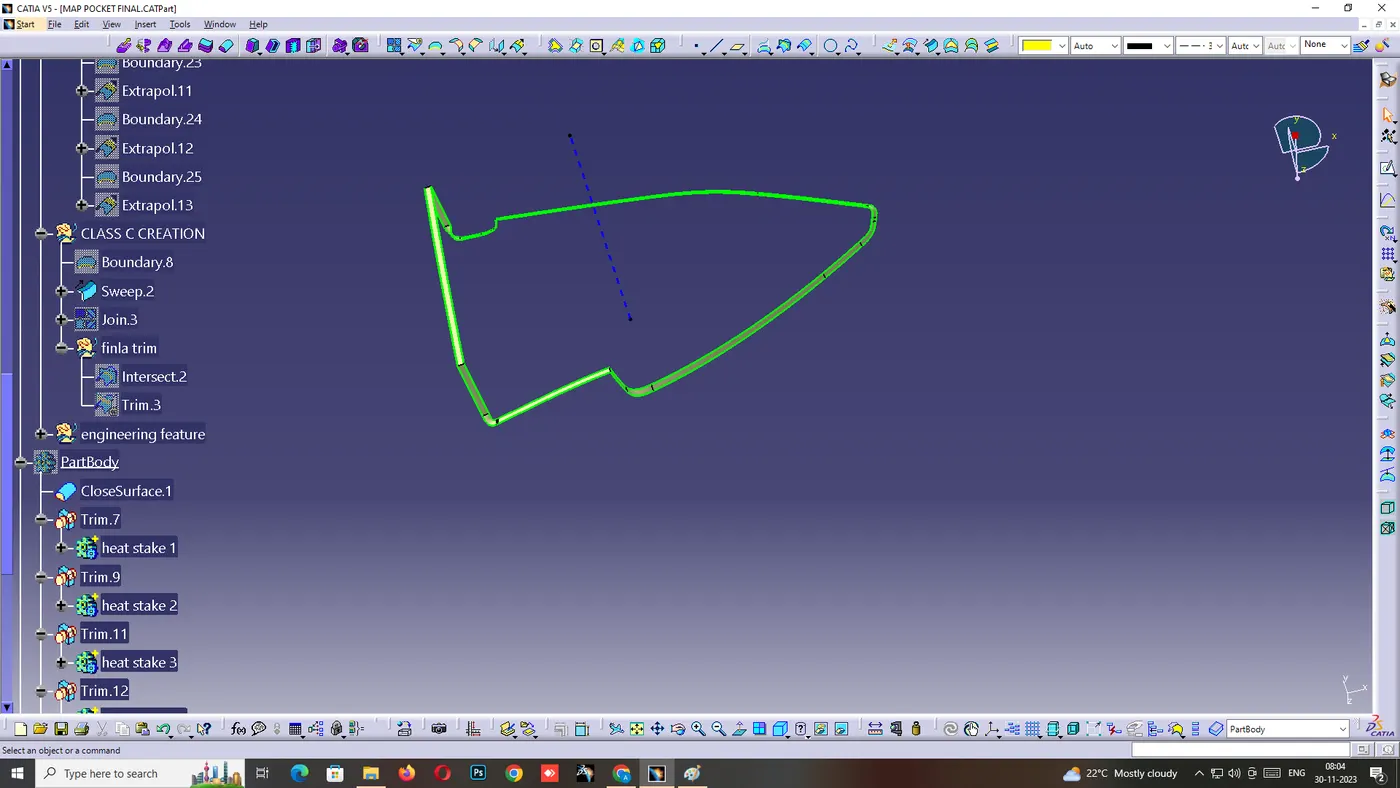
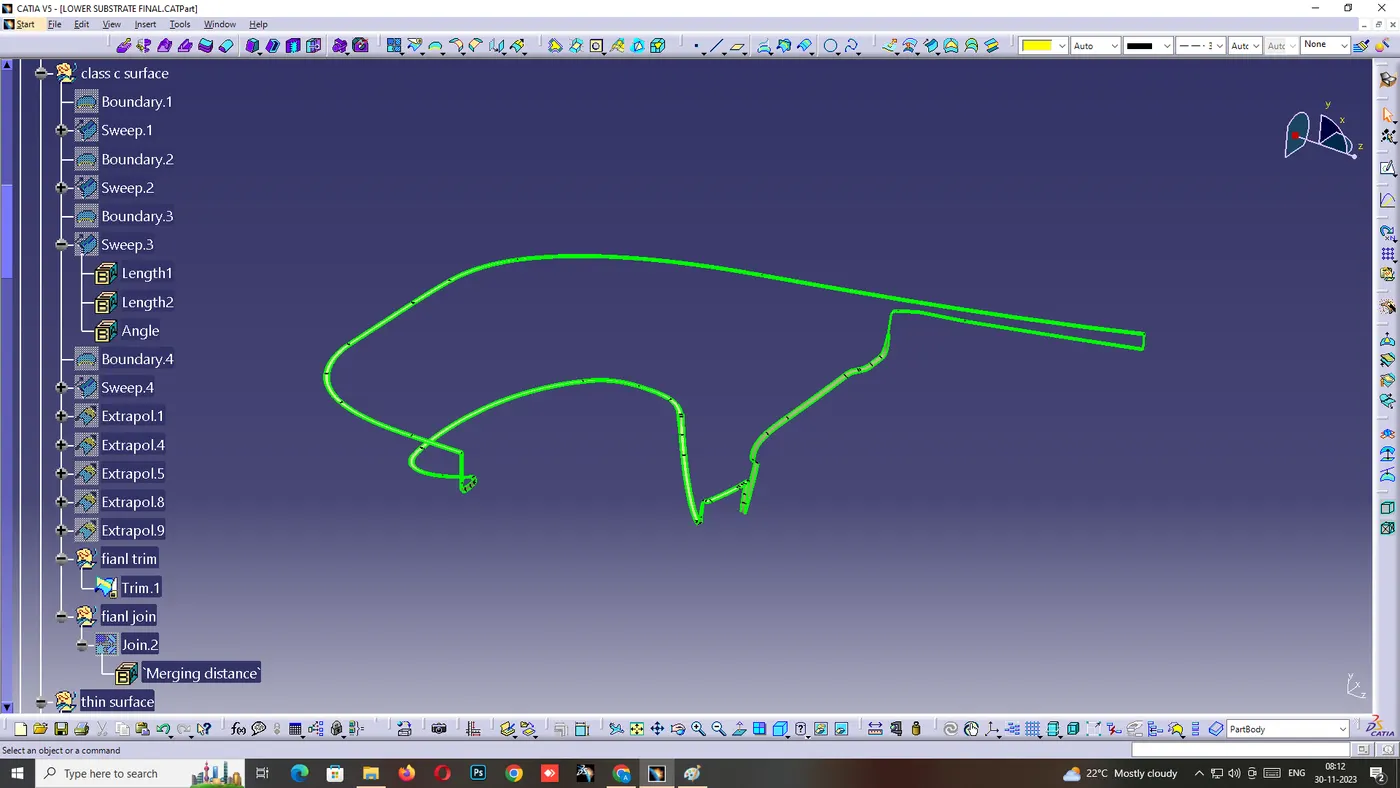
Extracting the boundary of Class A surface and it is make into smooth curves to sweep the curves by using support surface to the 90 degree respectively.
Once the all surface joined together it extrapolated to certain distance to trim with A Class surface to C surface. Finally we created Class C surface.
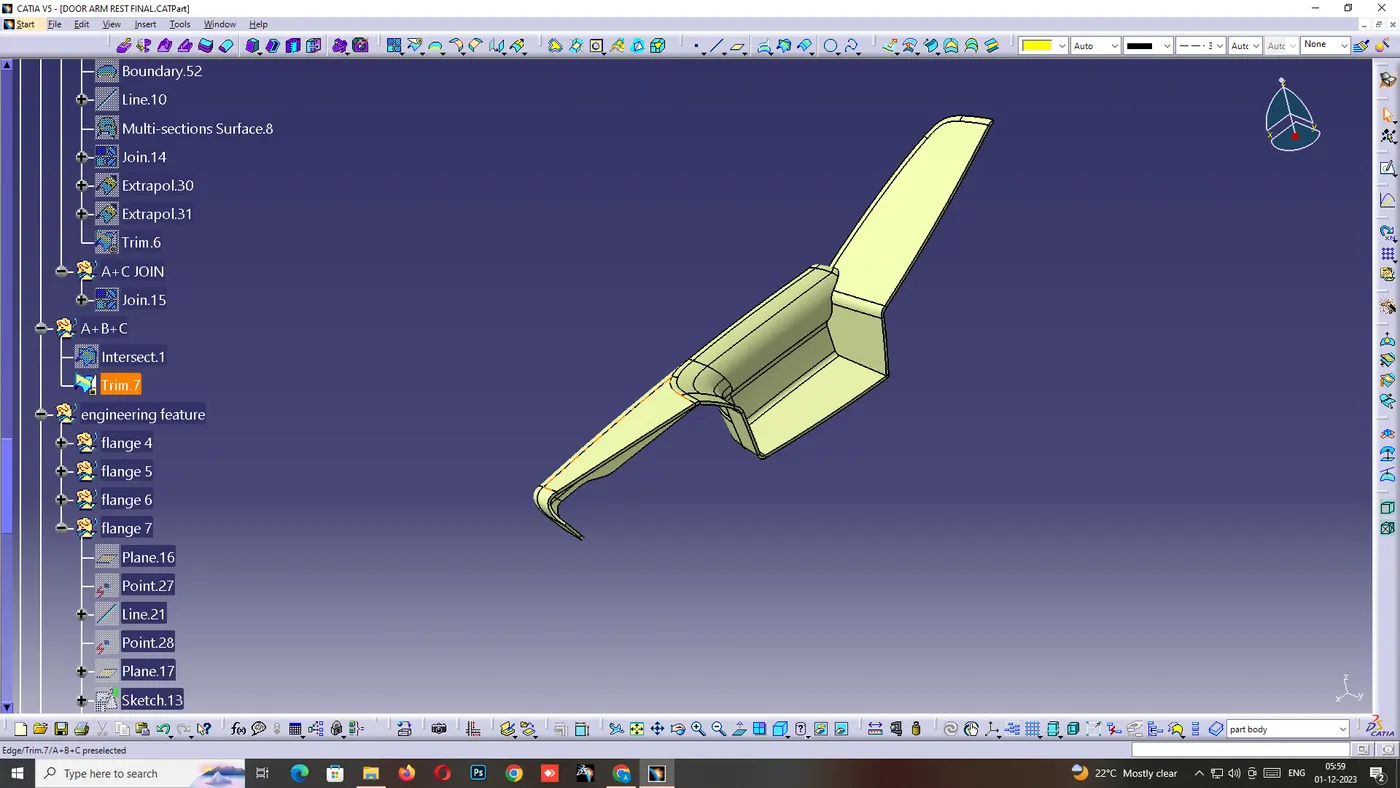
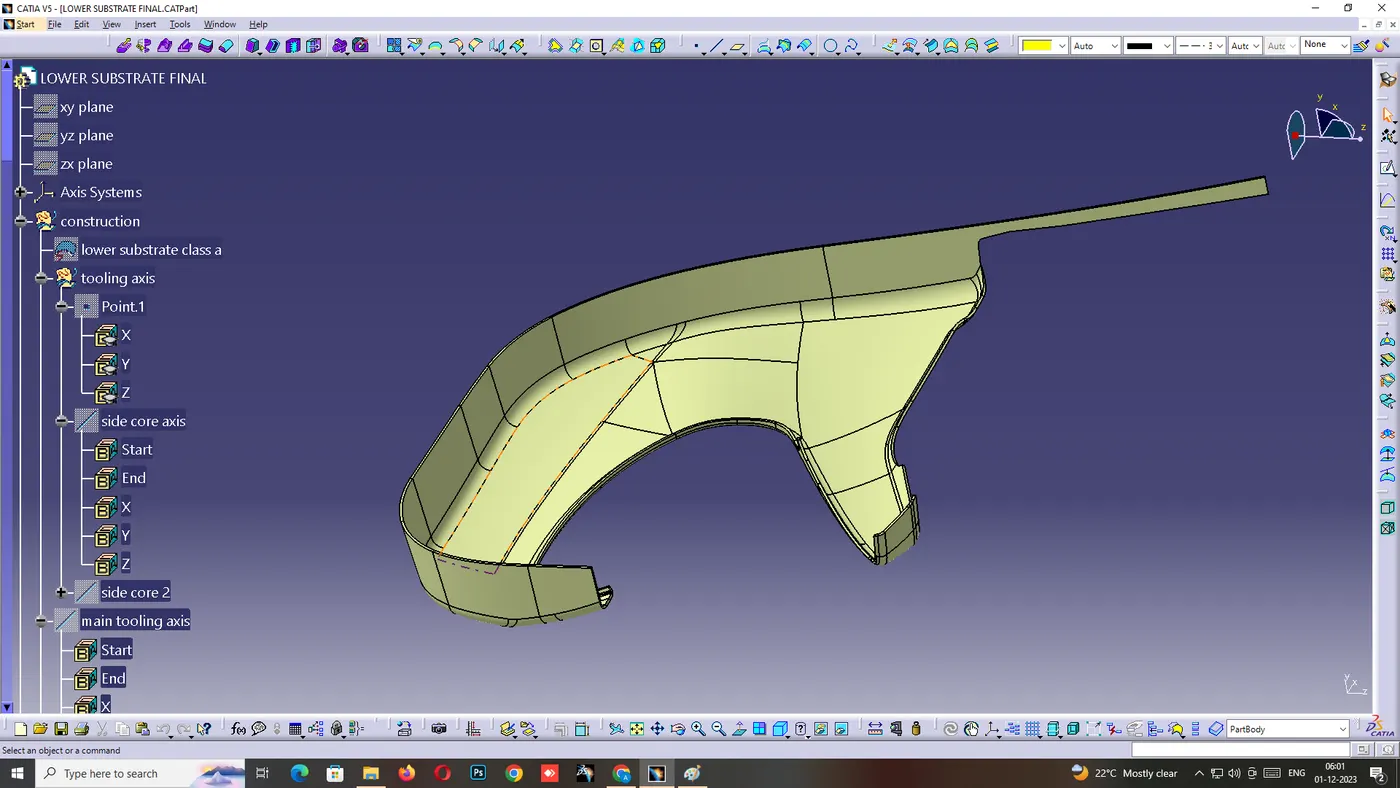
To make the final component the Class C surface is trimmed with Class B surface, the output will get the component with 2 mm thickness of surface and it is converted into solid body using insert body option in part design as shown below.
Making the Final plastic Component:
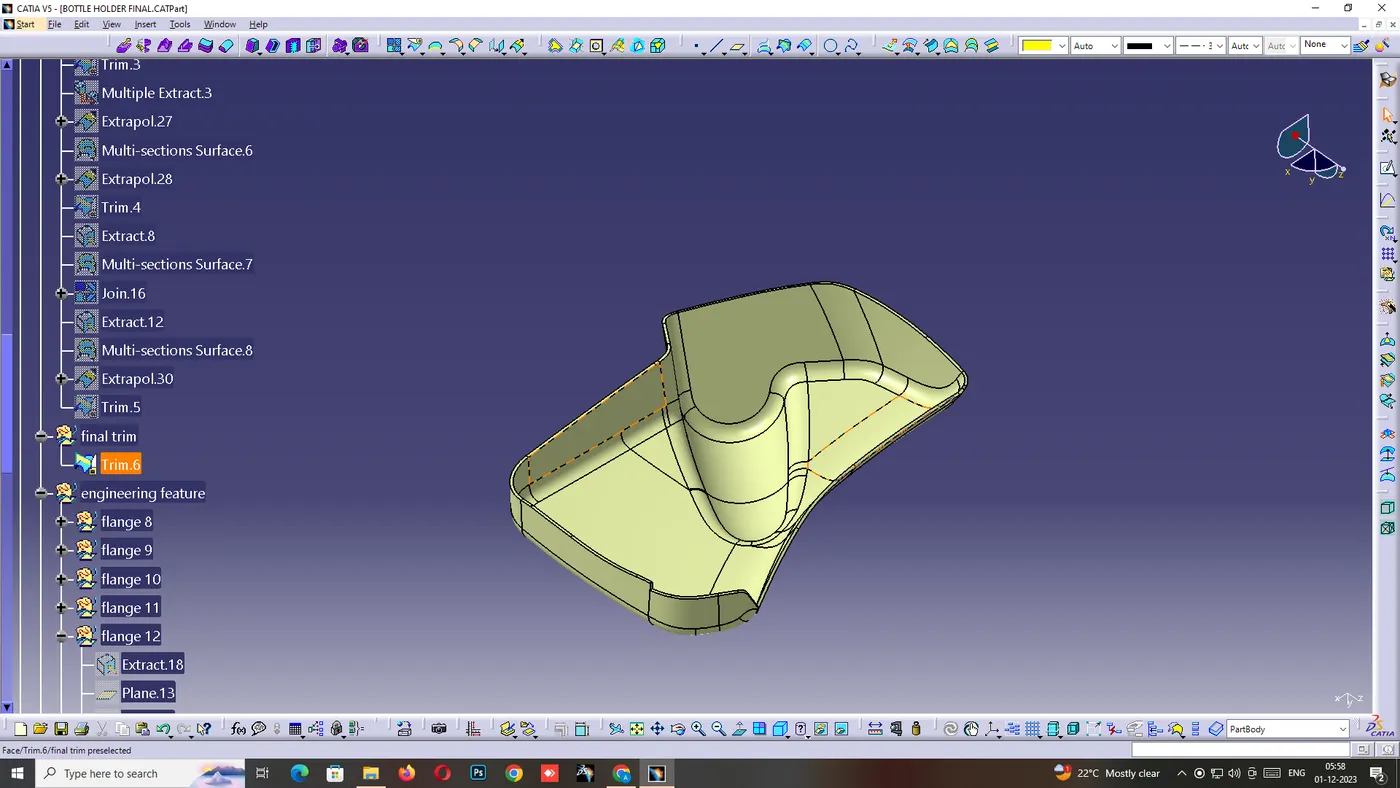
Once the all surface joined together it extrapolated to certain distance to trim with A Class surface to C surface. Finally we created Class C surface.To make the final component the Class C surface is trimmed with Class B surface, the output will get the component with 2 mm thickness of surface and it is converted into solid body using insert body option in part design as shown below.
DOG HOUSE:
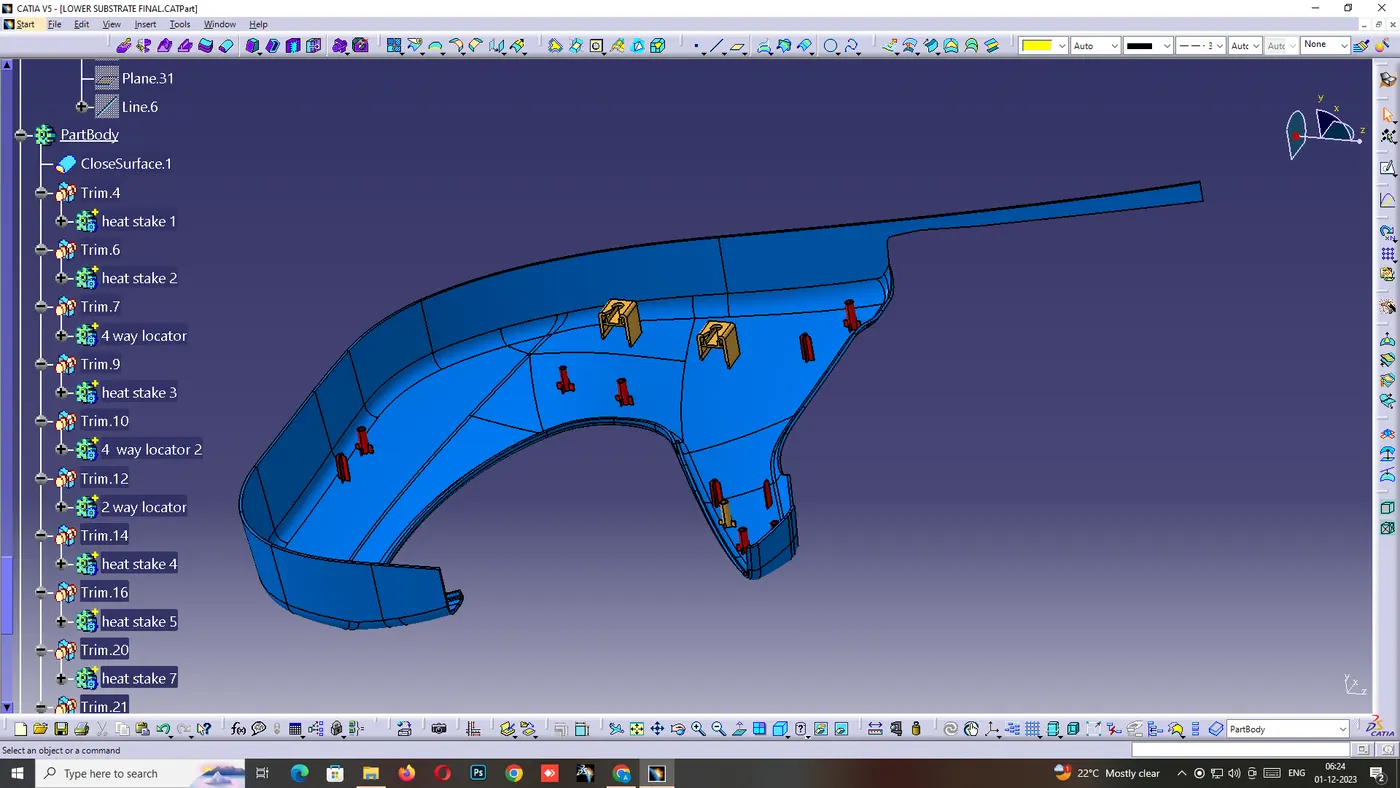
Dog house is an engineering feature used in plastic trim design. Dog houses are used as supporting feature. Sometimes other engineering features like snaps; locators etc. are mounded on them to increase their strength. Dog houses are subjected to draft analysis to prevent breakage of the component during ejection from mould cavity. Dog house and other engineering components are built on B-surface.
HEAT STAKE:
Heat staking is a pulsed – heat process to join two or more parts out of which one at least is made of plastic . The plastic is to deform the plastic material using the heat and foam at a set process time. The bond is made by partially de forming the plastic part in order to fix the other. Heat stakes makes it easily to bond metal to plastic is commonly used in high volume and low cost application such as Automotive, IT and consumer appliances.
AND OTHER ENGINEERING FEATURES:
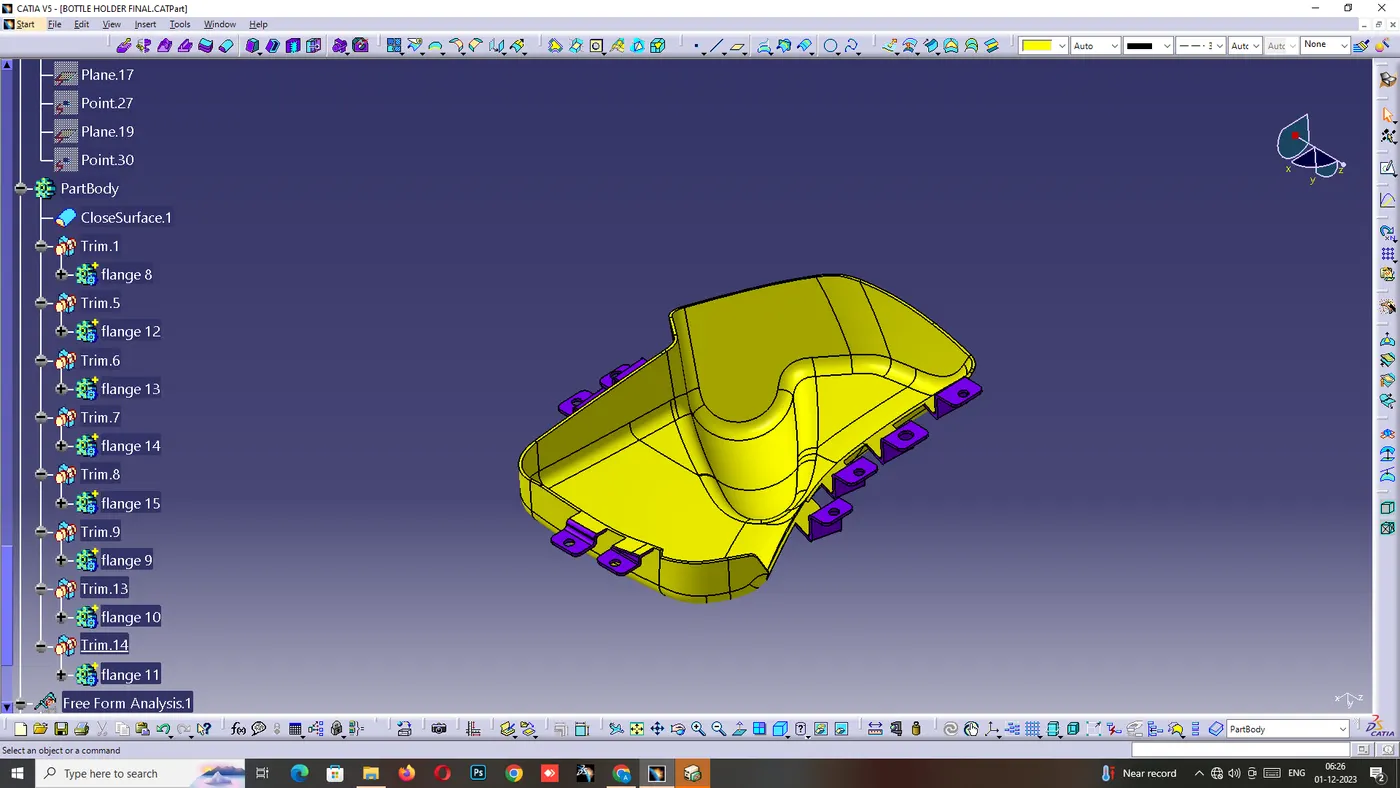
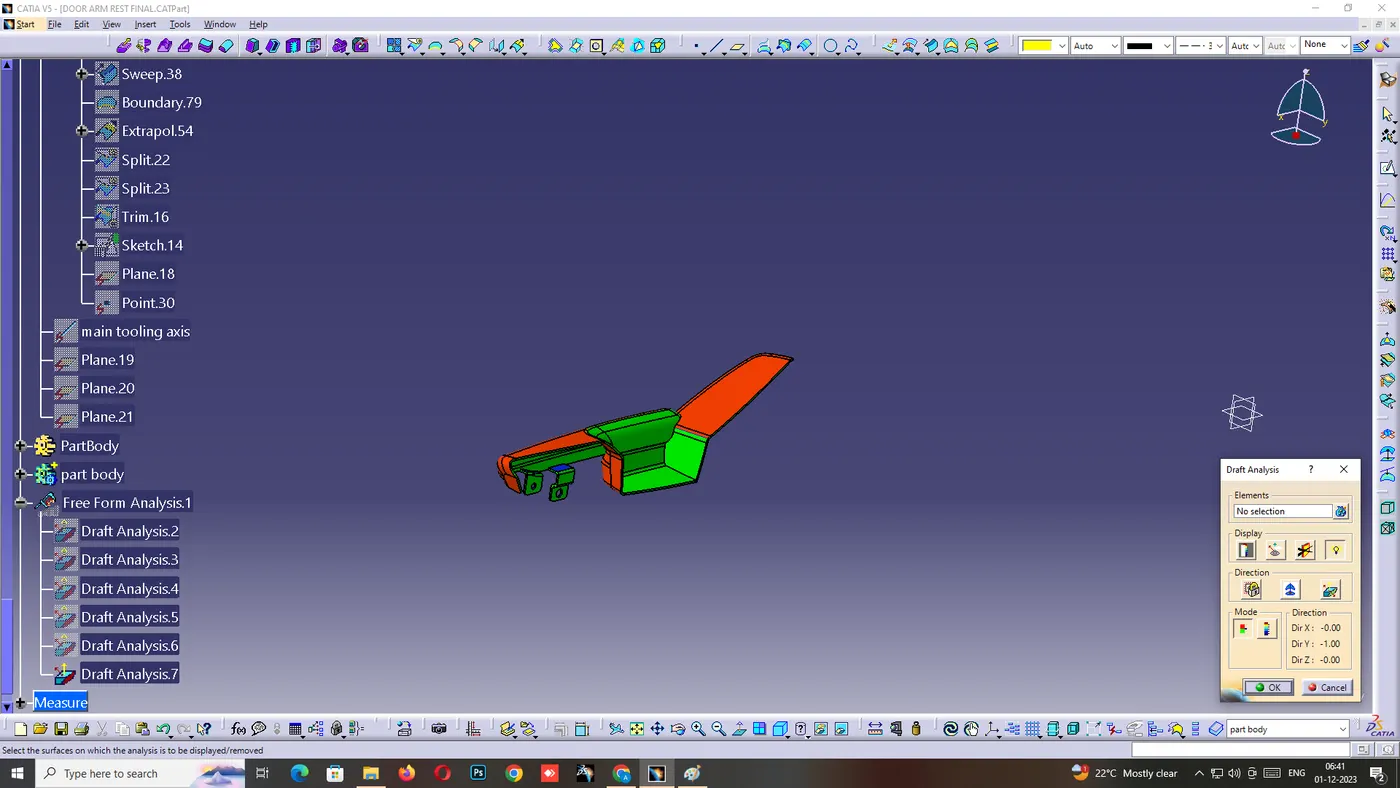
.Performing Draft Analysis:
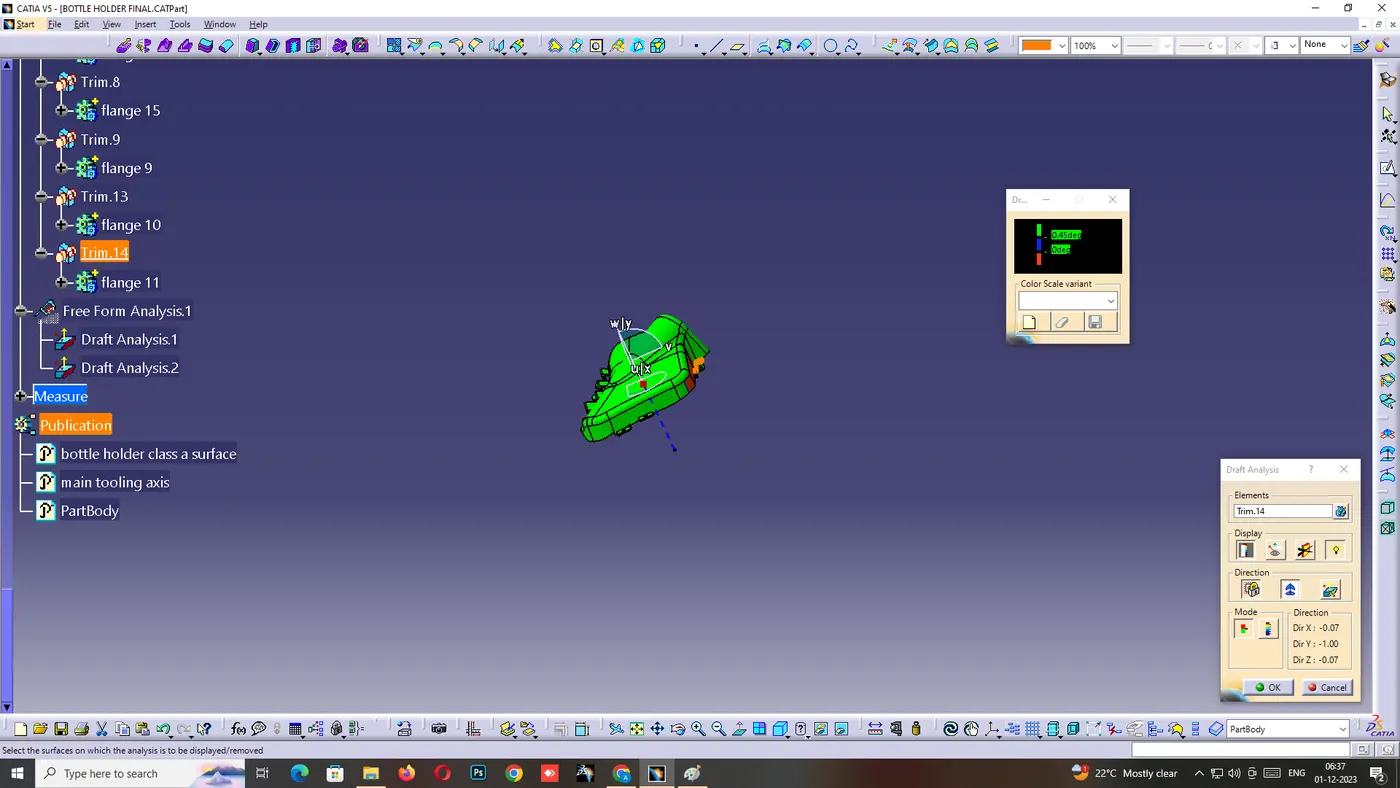
The Draft Analysis command enables you to detect if the part you drafted will be easily removed. This type of analysis is performed based on colour ranges identifying zones on the analysed component where the deviation from the draft direction at any point, corresponds to specified values. This rule of thumb applies to parts with mold depths of up to 2 inches. At this size, draft as low as 1½ degrees will allow for an easy, non-damaging release from the mold when the expected shrinkage of the thermoplastic material occurs.
It’s also important to remember that draft angles are just one component of an effectively designed injection molded piece. Design for manufacture is one of the easiest ways to improve the quality and efficiency of your injection molding process, and it never hurts to stay up to speed on all injection molding best practices.
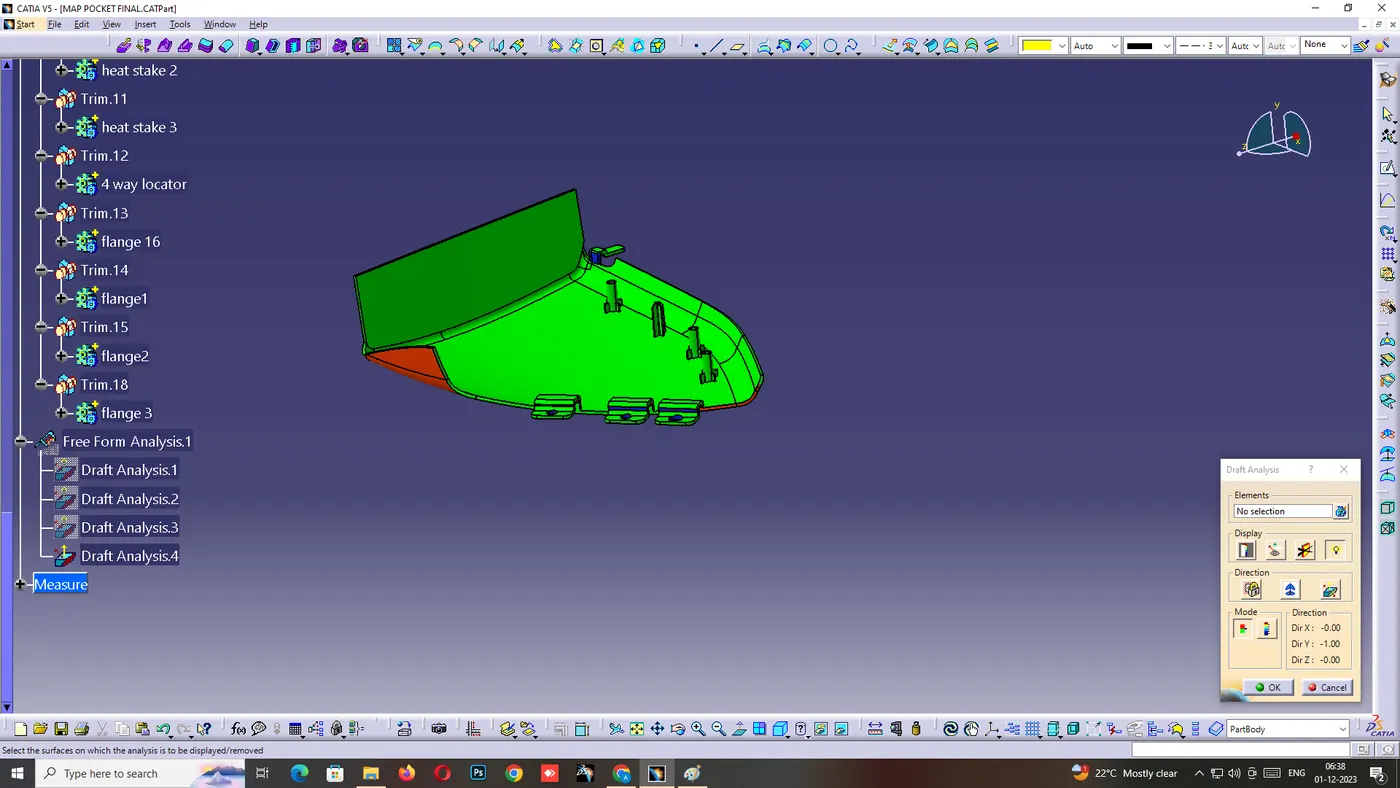
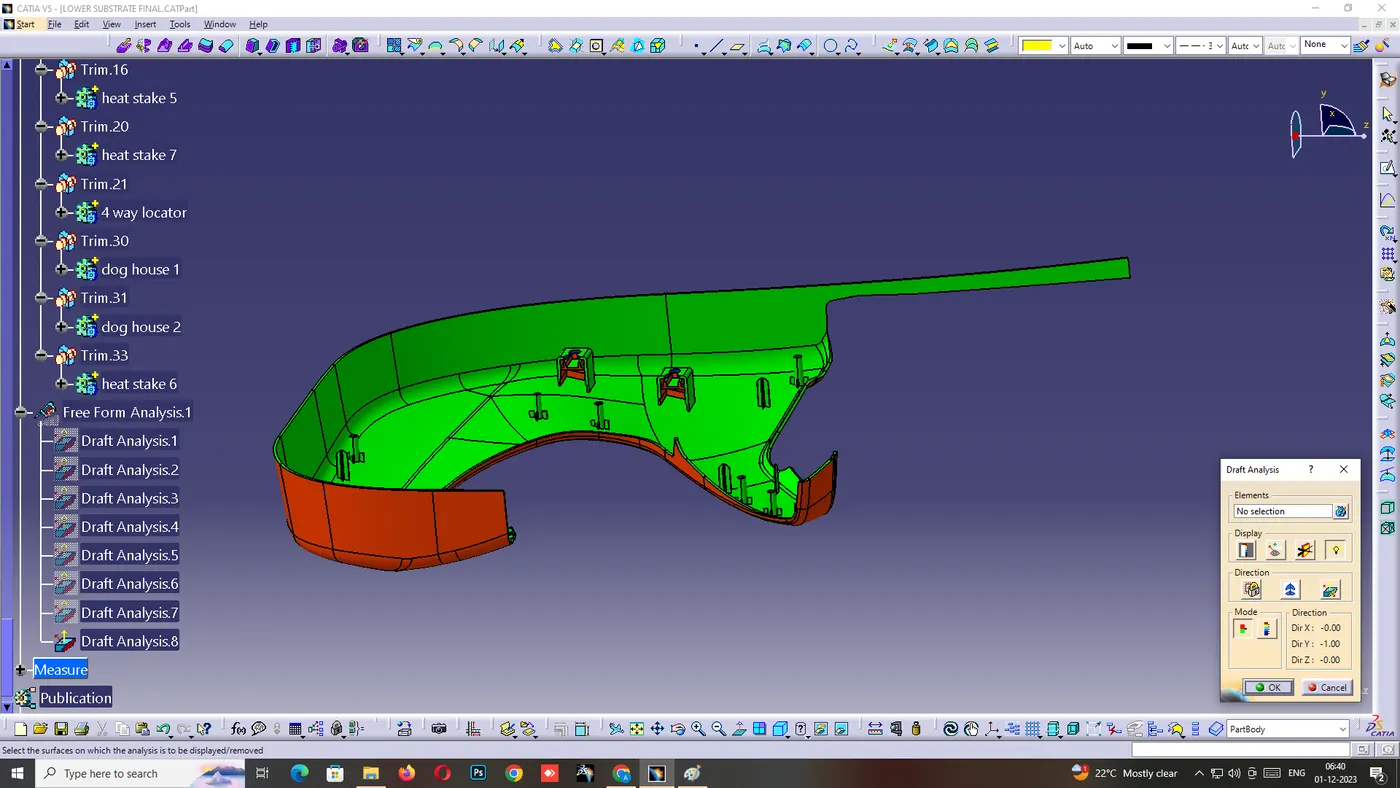
FINAL PRODUCT: