Week 1:- Introduction to BiW and Fixtures Challenge
Q-1 What is BIW and define its parts?
A-1 Body in white is that stage in which a car’s body frame has been joined together before painting and before the motor, chassis sub-assemblies, or trim(glass, door, seats, upholstery) has been integrated into the structure.
Assembly involves different techniques such as welding(spot, MIG/TIG), riveting, clinching, bonding and laser brazing
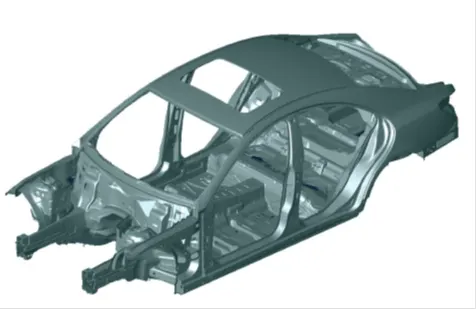
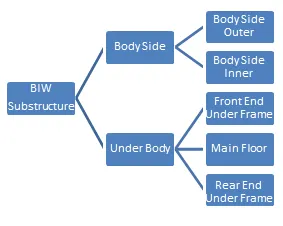
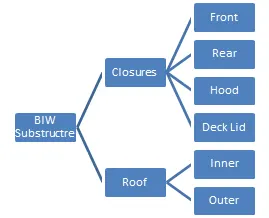
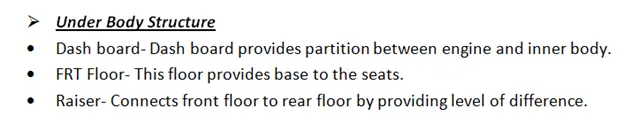
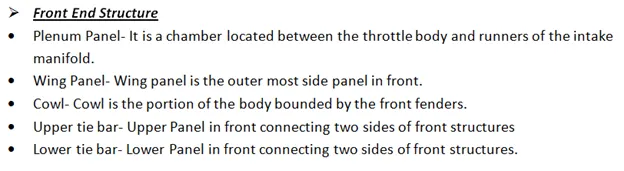
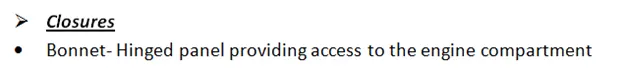
BIW parts are further categorised as
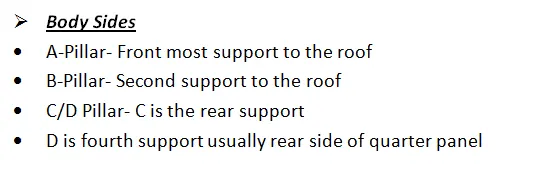
Q-2 What do you understand by BIW nomenclature?
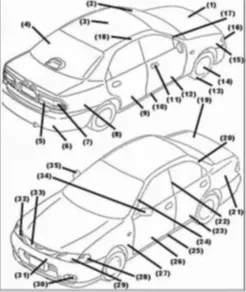
A-2 BIW has number of parts in it, different parts are known by different names
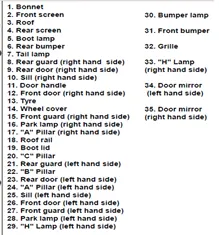
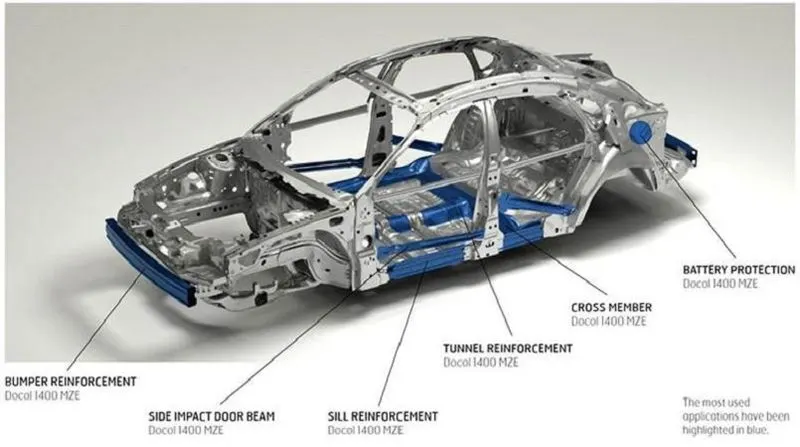
Q-3:- What are fixtures and its types?
A-3:- The fixture and its types are as follows
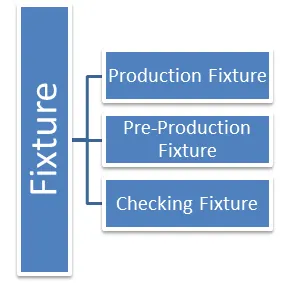
- Production Fixture
Basically used for mass production, the fixture where car body will get assembled, therefore the materials which are placed in this unit should be very well tested according to the criteria and every single unit as well as sub-assemblies should match with drawing sheet provided.
The main reason of matching with drawing sheet is that it becomes easy for maintenance purpose which should be cleaned and checked according to routine.
- Pre-Production
The first step towards visual impact of entire automobile body, about how the product will look is performed at this stage.
The basic fixture which sets the parameter and satisfies the mechanical properties.
Due to this fixture, one can easily rectify errors which will be further avoided during production.
More involvement of manual operations
- Checking Fixtures
To check or to inspect the assembly.
The geometry of welded parts in checked to ensure that the product meets required dimensions.
Very much similar to geo fixtures expect no operations will be performed such as welding, gluing
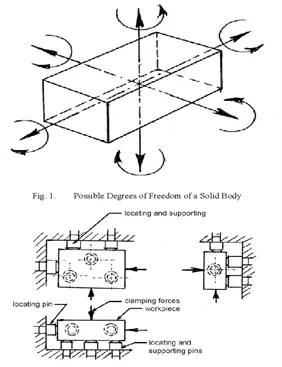
Q-4:- What is the basic principle of fixture design?
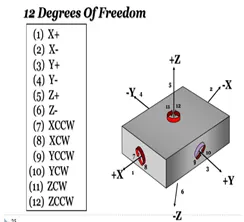
A-4:- In every free body there are total of 12 Degree of Freedom
Translational-6
Rotational-6
Need to fix 12 DOF to locate the workpiece.
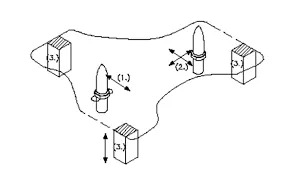
Q-5:- Elaborate types of BIW fixtures?
A-5:- BIW stations are categorised as follows
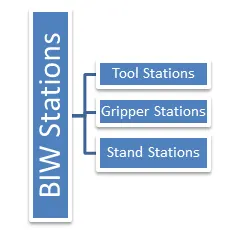
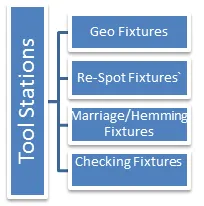
- Tool Stations
- Geo Fixtures
The panels are welded together and their profile is maintained, the geometry of that assembly is formed in that geo tool. The jigs involved in assemblies will be having tight accuracy. The geo pin will have tolerance up to 0.15mm.
- Re-Spot Fixtures
The spots which are not considered in geo tools are welded at this station in order to increase cycle time. The pin tolerance provided will be -0.28mm
- Marriage/Hemming Tool
Hemming is the technology used in automotive industry to join inner and outer panel together (doors, hoods, tail gates). It is the process of bending/folding the flange of the outer panel over the inner one. Hemming processes includes :- Press hemming, Table top hemming, Robot(Roller hemming)
- Checking Tool
Checking stations where all the dimensions, co-ordinates, quality of the objects are tested. Checking station can be of gauge type, fixed type and automated checking fixture.
-Fixed type is used where work piece is fixed with clamps and pins and a CMM machine is used to check parameters and co-ordinates.
-Automatic fixtures where automatic settings are done with the help of PLC and sensors.
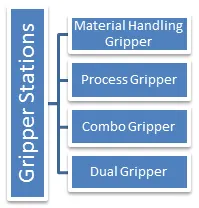
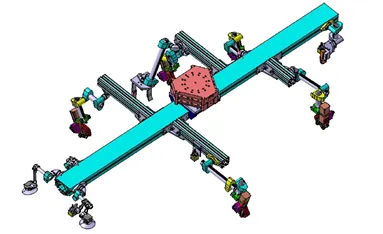
- Grippers- Gripper is basically a fixture but with less number of parts. Gripper should be kept as lower weight as possible and it has to be mounted on hand of robot.
- Material Handling Gripper
The main process includes transferring car panel from one station to another, basically pick and drop system.
- Process Gripper
It is similar to material handling gripper except that the robotic arm will pick up the body from one station transfer it to another station where a process will be performed such as welding at pedestal welding stand. Depending upon requirements different operations such as welding, riveting, gluing and sealing will be performed.
- Combo Gripper
Where more than one operations are performed from material handling and other process such as welding.
It forms a combination of Weld gun + Gripper
- Dual Gripper
As the name suggest, these will be having right hand & left hand gripper to carry each process simultaneously
It forms a combination of Gripper+Gripper
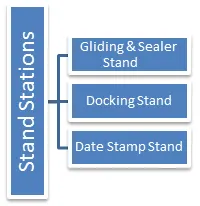
- Stand Stations
- Gluing and Sealer
They are fixed to floor permanently, gluing gun or sealer gun is welded to a fixed stand.
- Dockyard Stand
The docking stand will have the gripper or gun mounted on it.
The robot cannot perform multi-tasking due to limitations, so when one process gets finished the robot will pick gun after completing previous task.
In other words the dockyard stand is another helping hand for robot to supply the required equipment when needed.
- Date Stamp Stand
Every manufactured product will have date stamp from day of purchase, batch number, serial number for traceability for future reference.
Q-6:- What are the basic terminologies used in the BIW fixture?
A-6:- The Basic terminologies used for BIW fixtures are as follows
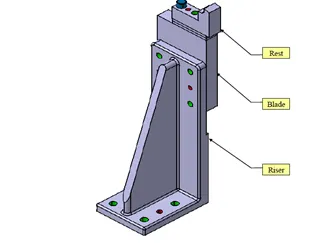
- NC/ Mylars/ Fingers
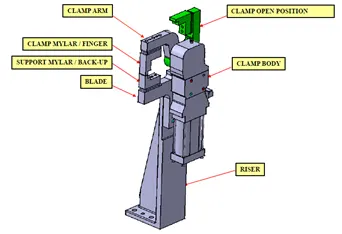
Mylars are also known as rest clamp which is used for holding 2/3 BIW sheet metal parts. Mylars play an important role in BIW welded assembly.
- PLP
The principle locating pins are the one used for locating panels.
- Blade
Blade is the one which are attached to risers.
- Riser
The riser is that manufacturing part which gives height to all assemblies such as L-type, welded square type. On the riser the blade will be mounted
- Shims
In order to avoid stack up tolerance due to every relatable assembly or sub-assemblies shims are used, so that it can be easily adjusted. The entire tolerance(±0.2) can form distortion and will create possibility off-center condition, in order to make center to center assembly shims became necessity.
- Rough Locators
Rough locators are generally used in manual fixtures, the main focus is to provide guidance for the panel to be adjusted for the operator.
- Hardware
Bolts, Fasteners and nuts are hardware used in the fixture station, available according to standard sizes.
- CMM
Co-ordinate measuring machine used to locate co-ordinates of an assembly as per drawing, or information provided in CAD sheets.
- Units
The assembly of different components aligning together to give an output is known as units. The unit can be different such as base, pin unit and clamp unit.
- Number Plate
In order to give identification to a single unit for easiness in remembering different units are given number order wise which helps in assembly. Basically it is aluminum embossing
- Co-ordinate Plate
On every fixture, tooling hole is provided through which every hole in measure with the help of CMM. Generally the bed is main reference through which the distances are calculated.
- Name Plate
Marking where basic information will be provided such as name of company, name of jig, name of fixture and other necessary information.
- Clamp Arm
The arm which moves at specified distance or rotates at specified angle is known as clamp arm.
- Pivot
The pivot is point of reference through which the clamp arm will move about its axis.
- Class A Surface/Skin Surface
The area of BIW that is visible to customers like outer body of car which should be very well designed and aesthetically good is known as skin surface.
- Reed Switches
Reed switches are basically the electrical part which
- Sensors
The main aim of sensor is to detect whether the part is available or not and to give signal.