Week 1:- Introduction to BiW and Fixtures Challenge
1.What is BIW & define its parts?
BIW is the stage in automoble manufacturing in which car body's sheet metal components have been weled together.
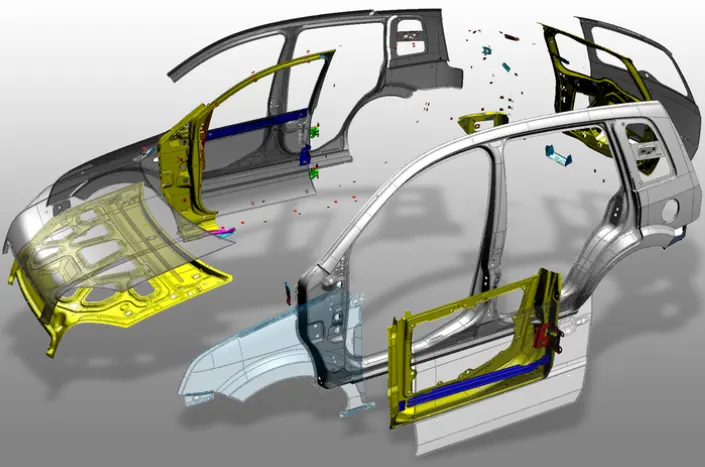
There are two types of Body structures in use, They are:
- Monocoque Body structure.
- Frame Mounted Body structure.
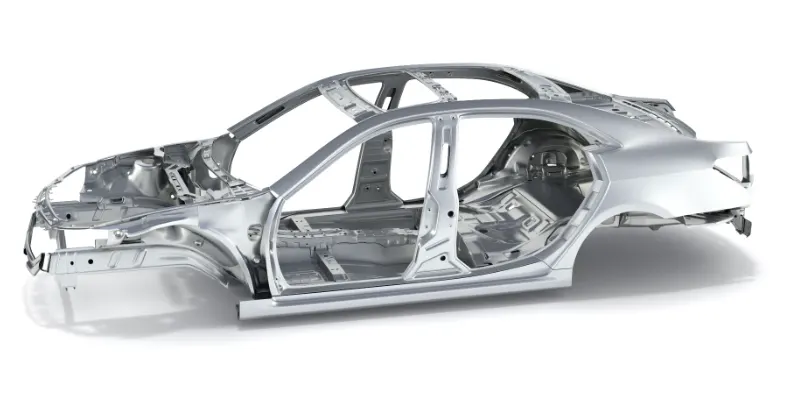
a)Monocoque Body structure.
In this type of Body structures, Chasis is in built in the BIW itself and there is no seperate chasis. Wheels are directly mounted to the BIW with the help of suspension system.
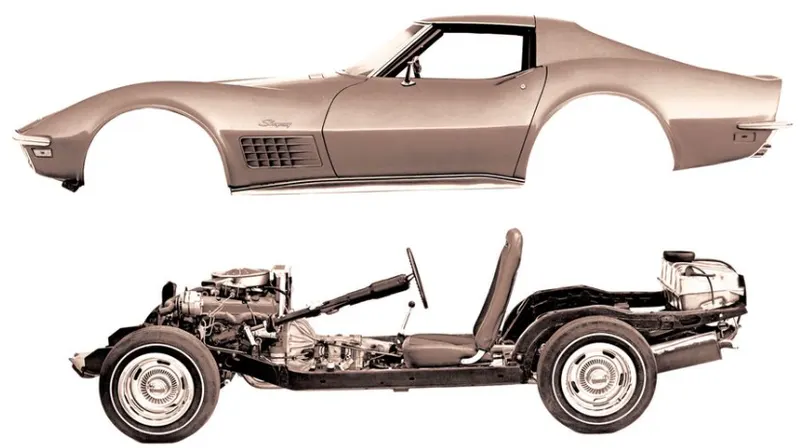
b)Frame Mounted Body structure.
In this type of body structures, Body is mounted on seperate chasis or frame & wheels are mounted on the chasis not to the body.
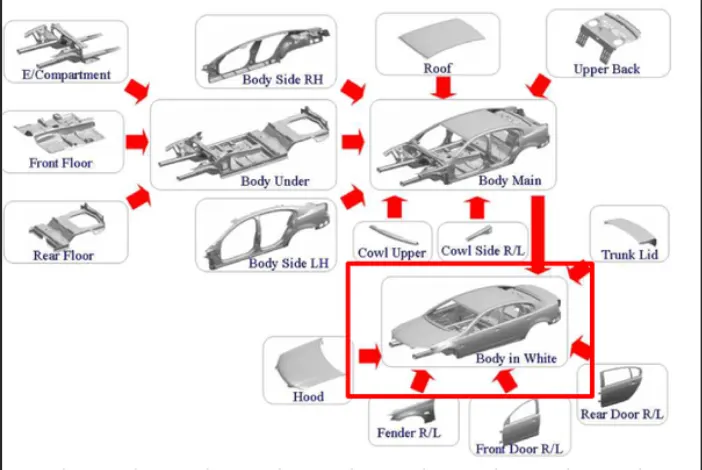
BIW structures can be divided into following sub-structures:
- Underbody structure.
- Front End Structure.
- Body side structure.
- Closures.
- Roof.
2.What do you understand by BIW nomenclature?
- The devising or choosing of names for things, especially in a science or other discipline.
- In formal, the term or terms are applied to someone or something.
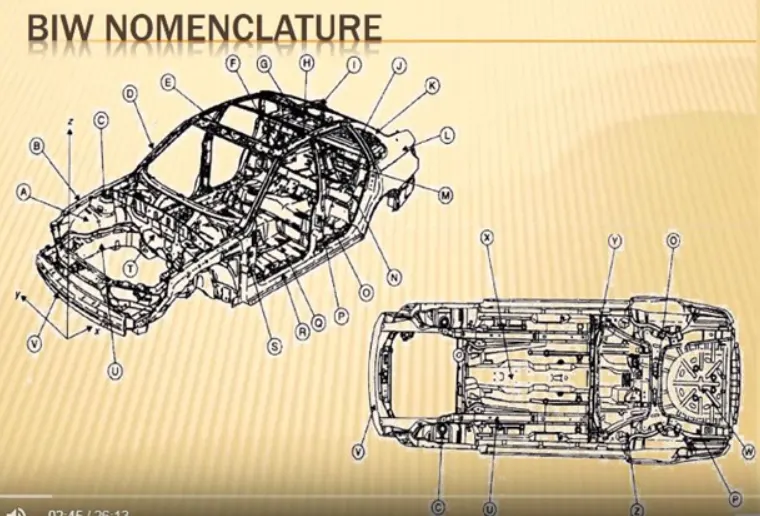
| item | UK description | US description |
| A | Inner wing panel | Motor compartment side panel |
| B | Upper wing member | Motor compartment upper rail |
| C | Suspension tower | Shock tower |
| D | Upper 'A'-pillar | 'A'-pillar or windshield pillar |
| E | Windscreen header rail | Windshield header or front heade |
| F | Roof stiffener | Roof bow |
| G | Rear parcel tray | Package shelf |
| H | Cantrail | Side roof rail |
| I | Backlight frame | Backlite header or rear header |
| J | C'-pillar | "C"-pillar |
| K | 'D'-pillar | 'D'-pillar |
| L | Rear quarter panel | Rear quarter panel |
| M | Boot floor panel | Rear compartment pan |
| N | Rear seatback ring | Rear seatback opening frame |
| O | Rear seat panel | Rear seatback panel |
| P | 'B'-pillar | B-pillar or center pillar |
| Q | Floor panel | Floor pan |
| R | Sill | Rocker or rocker panel |
| S | Lower 'A'-pillar | Front body hinge pillar (FBHP) |
| T | Dash panel | Dash panel |
| U | Engine (longitudinal) rail | Motor compartment lower rail |
| V | Front bumper | Front bumper |
| W | Spare wheel well | Spare tire well |
| X | Centre (longitudinal) tunnel | Tunnel |
| Y | Rear seat cross-beam | 4 crossbar |
| Z | Rear suspension support beam | 5 crossbar |
3.What is fixture & its types?
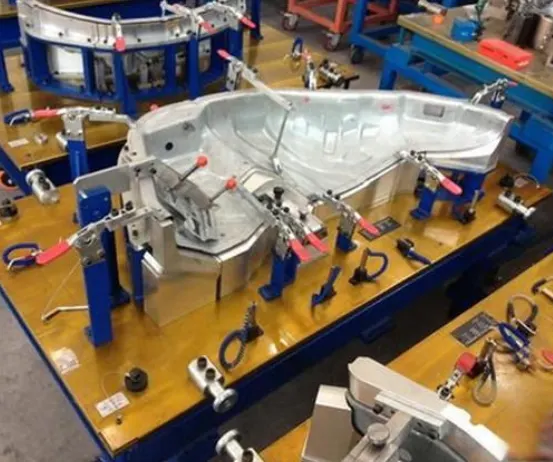
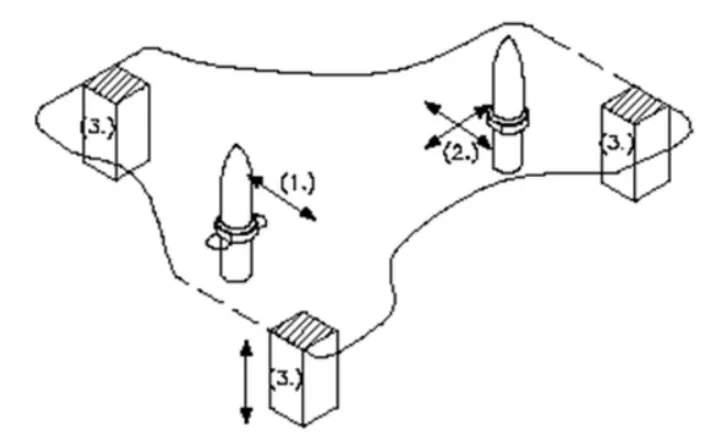
A fixture is a device which holds the work piece to be processed (welded) by using 3-2-1 Principle, Fixture has to be quite stable and rigid to withstand the welding stresses.
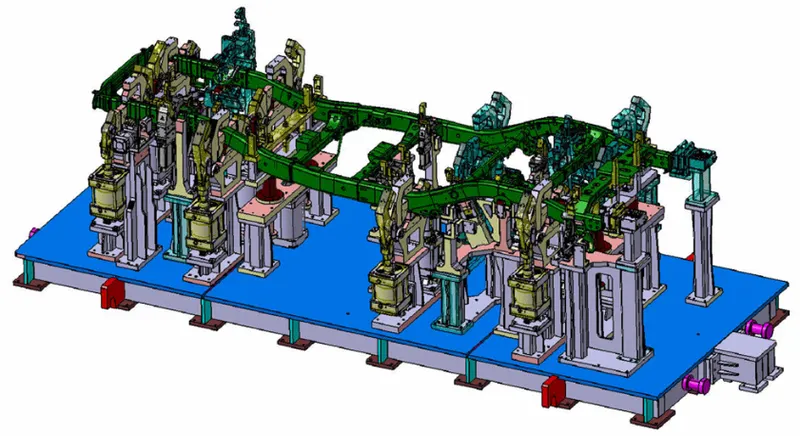
Type of Fixture:
- Pre-production fixture.
- Production fixture.
- Checking fixture.
a)Pre-production fixture:These fixtures is also called the prototype fixture to check & study the feasibility of initial batch production.
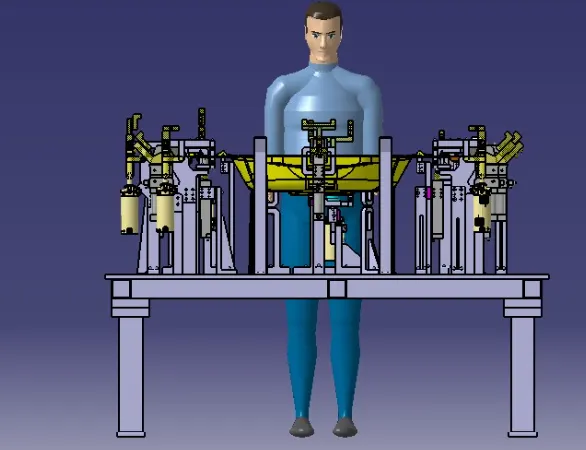
b)Production fixture: This type of fixture are used for Mass production purpose.
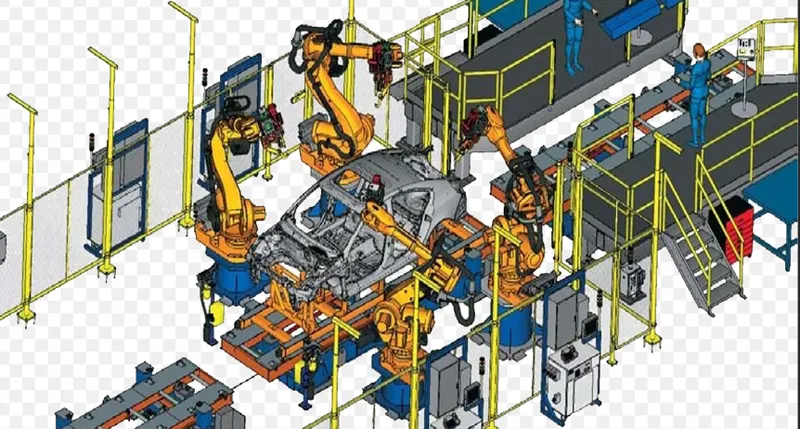
c)Checking fixture: These type of fixtures are used for the checking purpose of the part or assemblies.
4)What is the basic principle of fixture design?
A fixture is a device which holds the work piece to be processed (welded) by using 3-2-1 principle
Principle of Fixture Design:
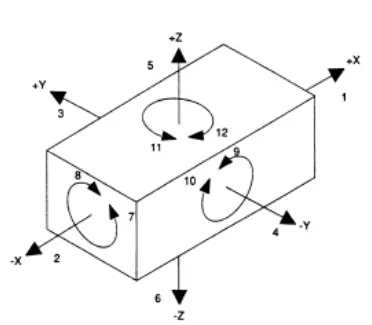
For any free body there are total 12 degrees of freedom as below, 6 translation degree of freedom And 6 rotational degree of freedom. we have to fix all 12 degrees of freedom in order to locate the work piece in the fixture.
- Clockwise around X axis (CROT -X)
- Anticlockwise around X axis (ACROT - X)
- Clockwise around Y axis (CROT -Y)
- Anticlockwise around Y axis (ACROT - Y)
- Clockwise around Z axis (CROT -Z)
- Anticlockwise around Zaxis (ACROT - Z)
5.Elaborate types of BIW Stations?
The BIW assembly line is divided into zones & these zones are again divided into stations.They are:
- Tool stations
- Gripper stations
- Stand station
- Miscellaneous stations
a)Tool Stations
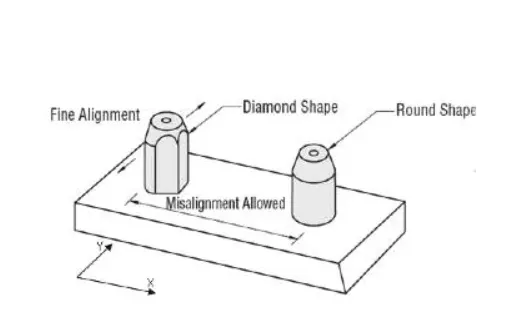
- Geo Fixtures: In geo fixture the geometry of the panels which are welded together is defined accurately. The pin tolerance for a geo pin will be of closer tolerance i.e. -0.15 in general.
- Re-spot Fixtures: In re-spot fixture the remaining weld spots which are not achieved in geo tool are weld.The pin tolerance for a re-spot pin will be of tolerance with -0.28 in general.
- Marriage/Hemming Fixture: In this tool inner panel assembly and outer panel assembly are joined together.
- Framer Fixture: The final panel from subassemblies of Under body, Body sides and Roof are welded together
- Checking Fixture: These are used to check the assembled parts.
b)Grippers Stations
A gripper is a device that holds a object to be manipulatating end of a robot or end effectore.
- Material handling gripper: These gripper are used to designed for handling the car panel from one Station to other Station.
- Process grippers: These grippers are used to carry out some specific operation like gluing, welding, riveting in addition to material handling.
- Combo Gripper: These gripper are used to designed for handling the car panel from one Station to other
Station, Also with combination of weld gun at another side of the gripper for welding. - Dual Gripper: These gripper are used to carry two panel same time, In case when we want one LH & one RH part, these grippers are used.
c)Stands Stations
Stands are used to hold the part when not in use or also it is used to mount some parts or bodies on it.
- Pedestal stands: Weld gun is mounted on the fixed stand which is ground on the floor, The gripper can carry the panel to the stand for weld operation.
- Gluing & sealer stand: It is used to fixed the welded or a standard stand which is grouted to the floor.
- Docking stands:The robots have some limits such as the payload,when robots are selected for multi tasking like material handling & welding it cannot carry both at a time because it have some load capacity, so the robot will drop and pick the gripper after completing the respective task.
- Date stamp stand:Every manufactured product has some data to stamped on it for identification.
d)Miscellaneous stand
- Curing: After gluing it needs some time to cool down, so we put the assembly on some belts & it will take the panel to another station & meanwhile gluing will cool down.
- Buffer stand: After some operation, we stack the min 10-15 panel and it can be transported from one station to another station in easy.
- Take out trolleys: It used to take out the some panels for inspection in between the cycle.
- Conveyor: The conveyor is used to transfer panel from one place to another.
6.What are the basic terminologies used in the BIW fixture?
- Principle Locating Point: These point on the panel is used for the location strategy like clamp, pin, pin retainer and rest are decided to support and hold the car panel.The positional dimensions or relative dimensions are very precise.
- Tool Nominal Locating Pin: These pin have no shimming adjustments, It is used to reference for measuring the other pin locations of the tool.
- NC Block: These are Numerically controlled machined parts, It is direct contact with the car body (0,0,0 )to hold and support them. NC blocks are also called as Mylar, Locator, Finger and Rest
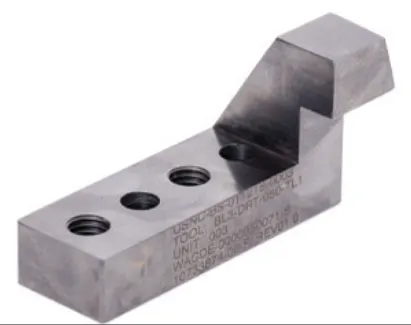
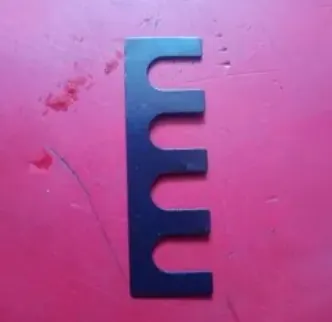
- Shims and Spacers: Its used for adjustments of locators NC Blocks and Pin retainers for obtaining the desired values for the precise working of a unit with respect to panel. Shimming should be parallel to BCS.
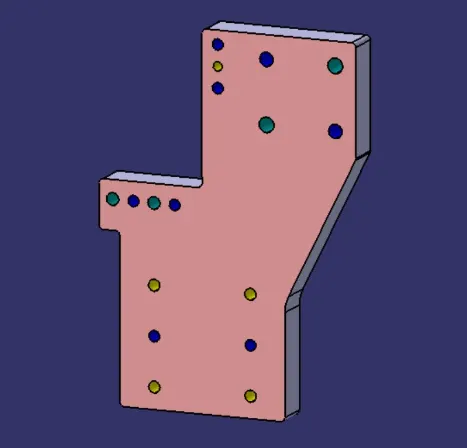
- Blade: Its a plates, Other parts like cylinder, arms, etc are mounted on the blade.
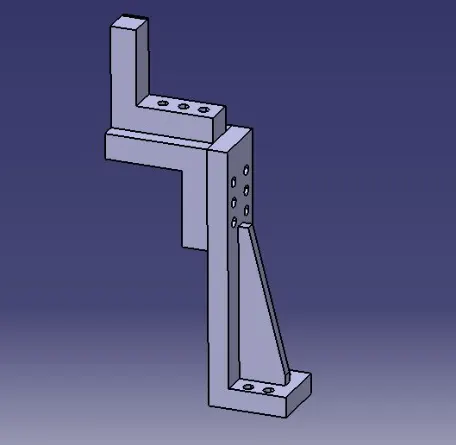
- Risers: There are different types like L-typer, Square tube ,T type etc is the manufacturing part which gives height to the assemblies.
- Trihedron Point: This is a point mentioned on the intersection of the butting surface and dowel hole of a NC block for the purpose of measuring and validation during tool assembly.