Week 1:- Introduction to BiW and Fixtures Challenge
1) What is BIW & define its parts?
-Body in white(BIW) is basically refers to a stage in automobile industry where car body is assembled and joined as a single unit by means of various techniques such as welding,brazing,riveting,soldering,adhesive, etc.
Body in white is a frame structure of car that takes place before painting,installing motor ,sub- assemblies,electronic components,wiring,seats,etc.
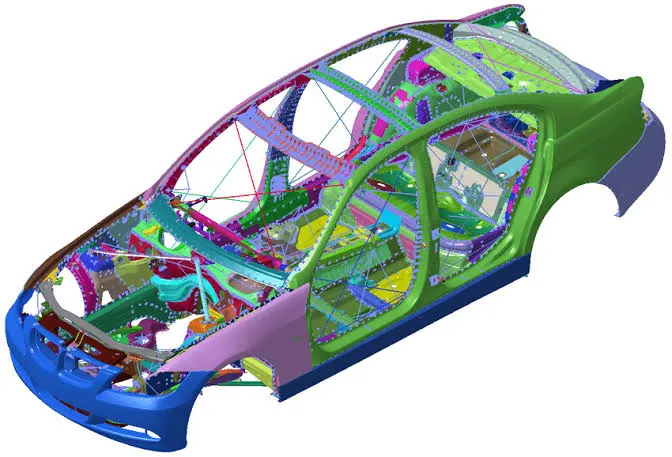
Fig: BIW components of vehicle
BIW consists of five parts that is
- Underbody Structure
- Front end structure
- Body side structure
- Closure
- Roof
Underbody structure further consists of
- Dash Panel: It provides division between engine and the driver/passenger of the front seat inside the car.
- FRT Floor: It is the the base floor on which seats will be mounted and also it separates the transmission assembly and the cabin.
- Riser:It provides the connection between front floor and the rear floor with some level difference.
- Rear Floor:It is the floor which provides base for mounting seats at rear of the car and also ground clearan.
- Rear Wheel House
Front end structure consists of
- Plenum Panel:It is placed between the runner and the intake manifold, it provides the extra charge which is stored in this chamber panel which ensure efficient working of engine.
- FRT wheel house/Fender:It is a casing around the FRT wheel
- Wing Panel:It is the outer side panel in the front of car.
- Cowl:It is the space between the base of the windshield and the rear edge of the hood.
- Upper tie bar:It is the outermost side panel in the front structure of car.
- Lower tie bar:Its is the lower side panel in the front structure of the car.
Body side structure consists of
Closures consists of
- All Doors
- Hoods/Bonet: It is front panel with a hinge that provides access to them engine.
Roof structure consists of
- Roof
- Headers
- Bows
2)What do you undertand by BIW Nomenclatures?
-Nomenclature is giving a term or name for things in different fields. BIW has number of parts to form the frame so all parts has different names.
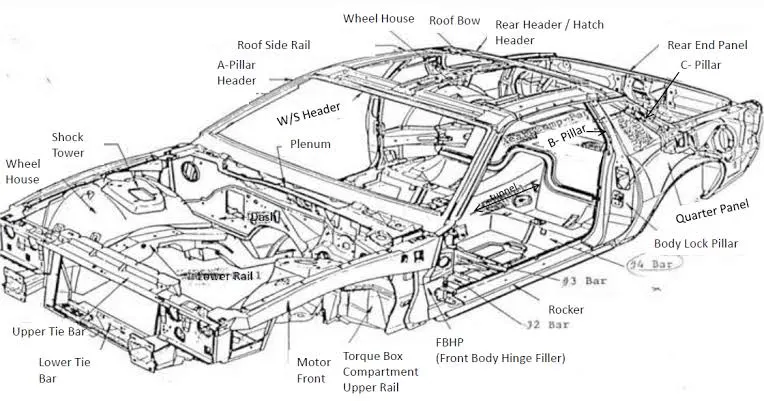
Fig: BIW nomenclatures of vehicle
-Since an automobile industry is spread through entire world , as a result the BIW parts naming also changes due to language change.
-As an example , for one part of BIW is called as Roof Stiffener in UK and for the same part is called Roof Bow in US.
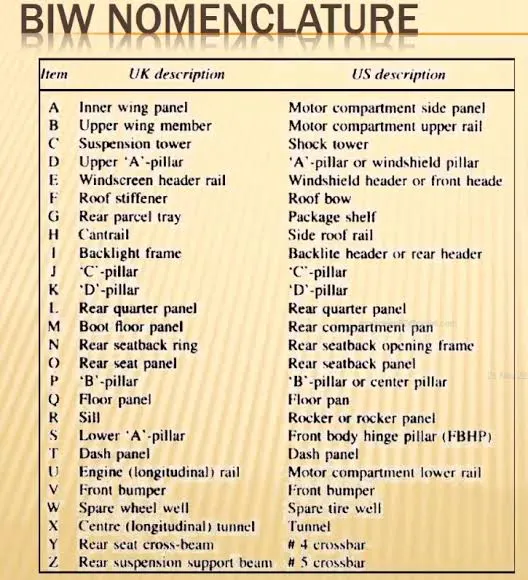
Fig: BIW
3) What is fixture and its types?
-A fixture in BIW is an equipment that holds Workpiece which will undergo through various process(welding) by using 3-2-1 principle. It is use to hold the work piece in proper location so as to avoid any distortion and also without affecting the geometry of the work piece.
-BIW fixture requirements are
- It should hold the part properly and prevent distortion during welding operation.
- Clamping should be light wrt workpiece but it also hold it firmly such that it maintain the required position throughout the process.
- Clamping should be such that it is clear from the welding area.
- It should be stable from the welding stresses and maintain its consistency throughout the process.
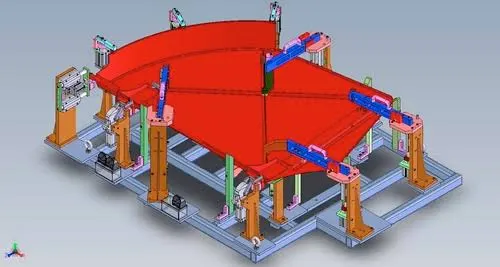
Fig; BIW fixture
Types of BIW fixtures
- Production Fixture: It is generally use for mass production. Since it is used where the production scale is very high it has to maintain the consistency throughout the process with maintaining the geometry of the part. The quality is maintained by checking the dimensions and tolerances in between the process. Maintenance required for these fixture is very less as it will increase time for production also maintaining these fixture is easy which further increases productivity. Time required for assembly and disassembly is very low contributing to increase in production time.
- Preproduction operation fixture: These are the base fixture which seats the benchmark and will fix the issue or errors that might generate from pre-production operation fixture. It is a base fixture as it will set benchmark which will help to eliminate issue or errors that will generate during preproduction operation fixture. It requires large number of quality engineers to set up as the operation is manual as a result it is time consuming than Production fixture. It is more time consuming and also costly.
- Checking Fixture: These fixture are used for checking purpose. It undergoes a number of joining processes (Welding,hemming,glueing,etc). Gauges are used to check the dimensions and tolerances of the work piece and its compared with the actual dimensions of the design part if it is ok or not. After process the part geometry is checked whether fixture maintain its geometry and tolerances.
4)What are the basic principle of fixture design?
- For a designer, major amount of time is spent on deciding how to locate the part in the fixture. A free body has 12 degrees of freedom, 6 translation degree of freedom and 6 rotational degree of freedom .
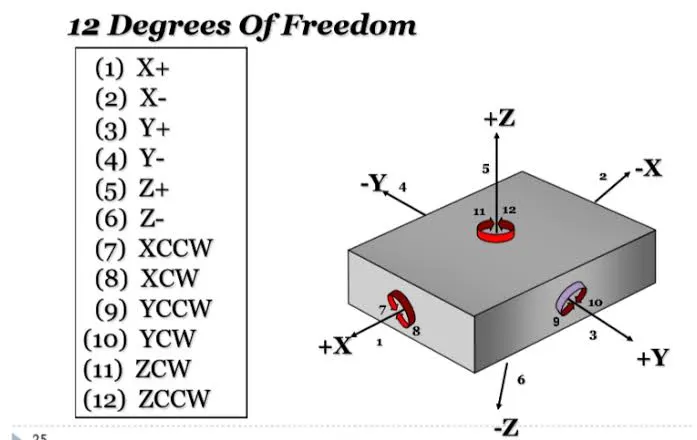
Fig: 12 degrees of freedom
- Clockwise around X axis (CROT-X)
- Anticlockwise around X axis (ACROT-X)
- Clockwise around Y axis.( CROT-Y)
- Anticlockwise around Y axis (ACROT-Y)
- Clockwise around Z axis (CROT-Z)
- Anticlockwise around Z axis (ACROT-Z)
It is very important to fix part properly such that it should restricted all 12 degrees of freedom. For a BIW fixture designer most of the time is spent on deciding to fix all 12 degrees of freedom.So to hold this work piece properly jigs and fixture are used for production. There are various types of fixture used in industries like welding fixture, milling fixture, drilling fixture ,etc.
5) Elaborate types of BIW Station?
- In BIW assembly line parts are moved from one section to another, the section is called Station.
BIW station is categories as follows
- Tool Station
- Gripper Station
- Stand Station
- Miscellaneous Station
- Tool Station
a)Geo Fixture
-A Geo fixture is one which defines the geometry of the part. In this fixtures tack welding is done on all the parts which will be assembled in the fixture.
All the parts to be assembled must be located with the help of two location pin. Locating pin may be common for two or more parts.
The jigs used in this station are of very high accuracy. In Geo fixture every machine part should be made with a tolerance of ±0.02mm and also the pin should have positional accuracy within ±0.015mm.
Spot welding or MIG welding in Geo fixture takes place in such a way that once part is removed from fixture it will have the desired accuracy and dose not get damage while transferring from Geo fixture to re- spot fixture.
b) Re-spot fixture
-In Re-spot fixture is use to complete remaining tack. Since in BIW assembly n number of tack weld required but if every tack weld is done on the same fixture a lot of time is wasted in the process and as a result other stations will be in ideal state.
So to counter this in Geo fixture the tack weld points are carefully selected in such a way that the geometry of the part is well define and it is not alter during transportation to Re-spot welding.
All the leftover tack will be completed in Re-spot fixture which ensures that the remaining stations are not ideal. The jig pin of re-spot has high positional accuracy and their tolerancissip ±0.28mm.
c) Marriage Fixture
- In this fixture the marriage of different assemblies takes place. In assembly line there are different zones where different assemblies are completed like front body, rear body , side body, etc.
- After all the assemblies are completed, all the parts brought to this station and assembled together by means of various joining processes.
d) Framer fixture
- In this fixture roof is joined to them outcome of the marriage fixture as a result it looks like frame structure so the name frame fixture.
e) Checking fixture
- These are the fixture used for checking the tolerance, dimensions and the coordinates of the assembly parts to ensure there is not deviation during the joining processes.Mostly two types of fixture are used ie Gauge fixture and the fixed type automated checking fixture.
- In gauge type fixture the work piece is hold and different gauges are used to check the dimensions and tolerances are within specified limit.
- In fixed type fixture the work- piece is fixed with the help of clams and pins and CMM is introduce which will measure tolerance and coordinates of the assembly and the data is compare with the CAD design.
- Grippers
- In BIW assembly gripper is a device which holds the object with ease and can be manipulated as per requirement. A gripper is use to do many operations like holding, handling, tightening or loosening of work piece. It can be connected to a robot or else it is fixed to automatic system.
Gripper are of different types are as follows
a) Material handling gripper
These are used for handling different materials and to transfer these material from one station to another.
b) Process gripper
- Process gripper are used for handling the work piece and along with that it can carryout various processes like welding, riveting, gluing etc on respective stand.
c) Combo gripper
- Combo gripper are used where multitasking is required like it can handle material and along with that it can perform joining processes like welding, etc.
d) Dual gripper
- Dual gripper are use to handle car panel and to transfer it from one station to another with the help of two sided gripper.
- Stand
- Stand is use to hold the
work piece when in idle condition and also use to perform different operations on the work piece when required
Different type of stands used in BIW assembly are
a)Pedestal Stand
- On this stand it has weld gun is attached to it ,the stand is permanently mounted on the floor and its fixed. Gripper will bring the part under this stand and welding operation is perform on it.
b)Gluing and sealer stand
- On this stand glue gun or sealer gun is attached to the stand which is permanently fixed on floor. When gripper brings the work piece under this stand operation will be perform.
c) Docking stand
- In BIW assembly robots use will have limitations such as load carrying capacity or short of space to perform operations. As a result the multitasking robots cannot perform their task due to such limitations.
To counter this we use docking stand on which devices can be mounted which are not in use for current operations but required for next operation.
d) Date stamp stand
- For all the products which are manufactured requires a specific identity for the reference. So a stamping device is mounted on the stand to stamp serial or batch number on every part.
- Miscellaneous Stand
a) Curing
- In some processes like gluing or sealer operation some amount of time required to cool down otherwise the part may distorted . So after gluing operation part are put on conveyor belt to transport to another station and meanwhile cooling down glue.
b) Buffer stand
- After the assembly of the parts, they are stored on this stand as a buffer and then can be transferred to other station with ease. This stand stores the parts when any machinery undergo maintenance.
C) Take out trolley
- It takes out work piece at every interval of time to check if the process is ok or not.
d) Conveyor
- Conveyor is a long rotating belt on which work piece are kept to transport from one location to another.
6) What are the basic terminologies use in the BIW fixture?
- Different terminologies use in BIW fixture are as follows
a)Myler/Finger:
- Mylers or fingers is a device which will hold the work piece during operation and dose not allow any deformations due to welding stresses.
Mylers are attached at top and bottom side, top is known as Clamping Mylers and the bottom one is known as resting Mylers.
b) Principle locating point(PLP):
- PLP is use to locate the holes accurately of the work piece so as to maintain its during assembly. During stamping operation workpiece gets large number of holes and most of them are not accurate . PLP defines in the drawing.
c)Risers;
Risers are use to increase the height of the assembly. Risers are of different shapes like square, L shape, etc.
d) Blades:
- In BIW assembly blades are mount on raisers.
e) Shims:
-Shims are thin parts with a thickness of 0.1mm or higher use to correct tolerance in mylers. Due to tolerances mylers either moves up or down from its define position. If mylers moves up from its define position it will put dent on the panel and if myler moves down it will distort the panel due to welding stresses. So to prevent such cases shims are use in the Mylers.
f) Rough locator:
- When part is loaded in the fixture it can happen that part may wrongly fitted in the fixture. So to avoid this we use rough locator which guides the work piece in desired position.
g) Hardware:
- it is all the hardware parts required in an assembly like nut,bolt, etc.
h) CMM
- Coordinate measuring machine(CMM) is is a measuring device which measures part at different coordinate with the help of probe. The measured data is then compared with the design data to give final report.
i) Unit:
- a fixture is made up of various units like clamping unit, pin unit ,base unit ,etc.
j) Number plate:
- It is an aluminum plate on which different numbers are developed using stamping or embossing operation and are put on different units to recognize easily.
k) Name plate:
- It is a plate on which fixture details are embossed or stamp to recognize easily .
l) Clamp arm:
- Clamp arm is a part of a clamping unit. Mylers are mounted on the clamp arm. Clamp arm rotates over axis.
m) Pivot:
- It is an axis over which clamp arm rotates.
n) Skin Surface
- It is the outer surface of the car generally roof , hood,door, etc which is visible to our eye . So this skin surface should be perfect without any dents or imperfections on it. So while designing the fixture for skin surface the clamp used should be soft and firm such that it holds it without damaging.
o) Reed switches and sensors
- These are the equipments used when automated fixtures are required.