Project 2
- FIXTURE DESIGN
OBJECTIVE:
- Initiate the concept of 2D detailing.
- Perform3D finish on the assembly design.
- write a detiled report describing the process(what changes are made in the design) and attach relevent images
FIXTURE DESIGN:
Fixture must correctly locate a workpiece in a given orientation with respect to the cutting tool or measuring device,or with respect to another component locating and clamping are the critical functions of any work holding fixture.
A work pice free in space can movie in an infinite number of directons.For Analysis,this motion can be restricted to ensure proper referincing of workpiece.To restrict the motion 3-2-1 principle is used .A body in space can have 12 degrees of freedom ,to restrict the motion we should achive 0 degrees of freedom.
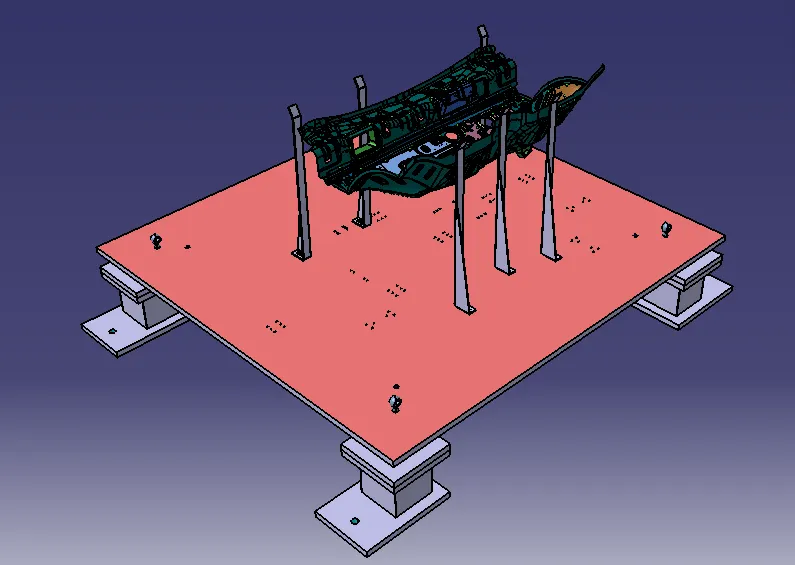
In this project, the car panel consists of many parts out of which 5 parts are taken in considertion to design the fixture.
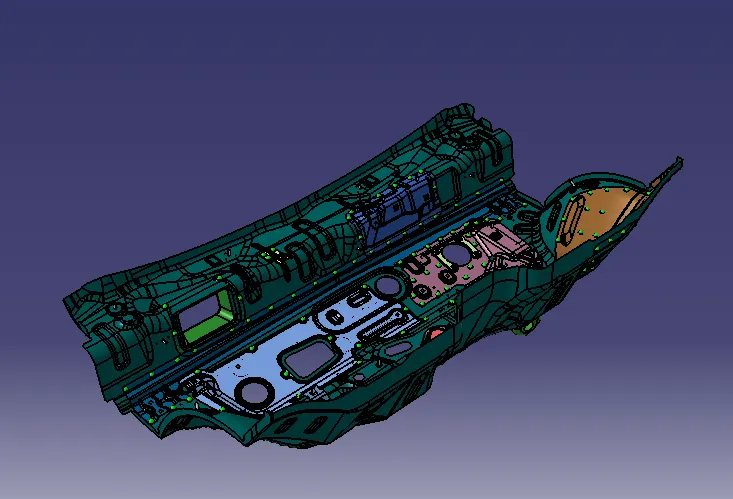
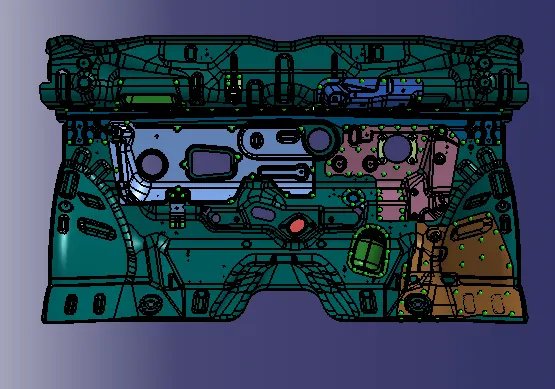
First to understand the scope of the work means what is expected by customer.Every customer has its specific requirements and it may have own raw material,electric,pneumatic,cad,dsign standards.Every customer also gives different inputs and ecpects output. e.g:2D drawing,process sheet in xls,pdf,CAD format of design,layout format,OLP.
Functional requirement is the basic requirement which defines the function of the fixture weather it is being used for welding,hemming,checking fixture or stroge racks.Depending on this design considerations are going to change while designing the fixture.
- Bill of materials of the components to be welded-spot welding
- CAD panels data or atleast 2D detaling of assembly and individual data.
- sheet metal panel thickness plays major role to decide 2 metal or 3 metal weld.
- spot detail information like total number of spots and spacing between the spots.
- weld information clarity from drawings like 2 metal or 3 metal welding.PLP(principle locating points) of indiviual and total assembly.
- Cycle time-If calculated or can be found out as per mannual or robotic welding process.
- Process sheet or process engineering is done-where locating sequence,no. of clamp data and gun data is mentioned.
- All clamping cylinder and fixture standards.
- CAD-software guidelines.
- Raw material standards.
- Design guidelines.
- Brought out item(purchased parts) standards like pneumatic item,toggle clamp,bearing,screw,dowel,etc. can be company information.
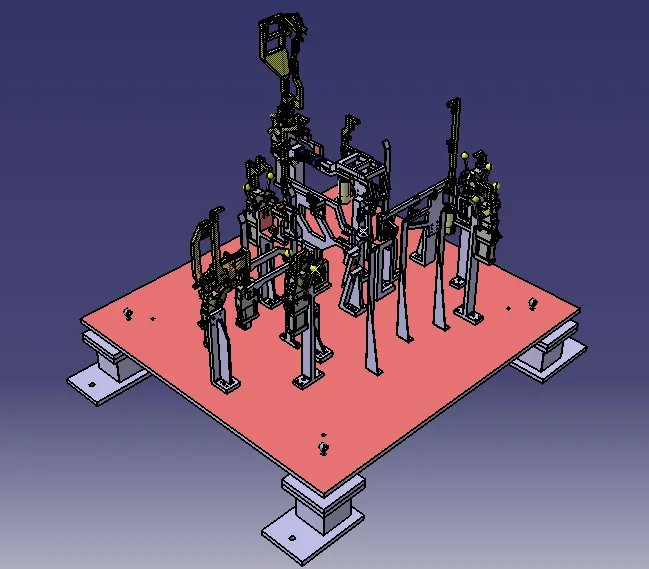
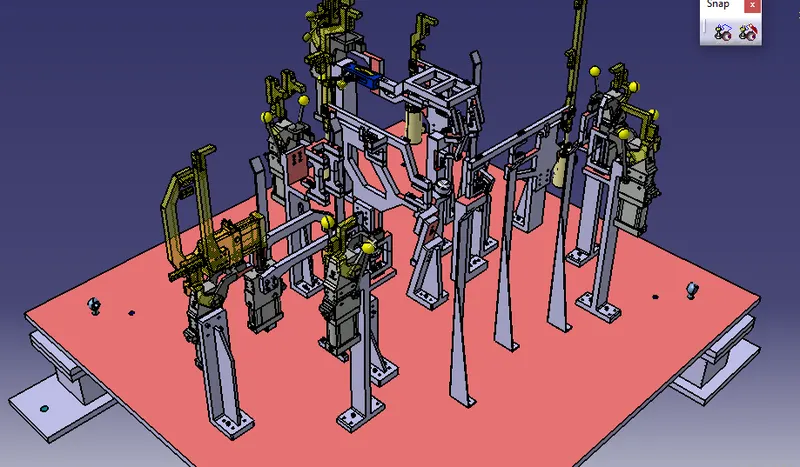
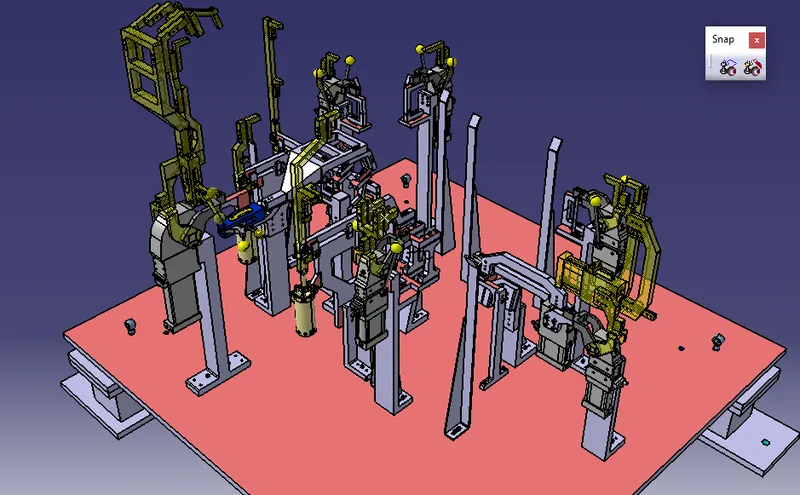
The fixture will be the spot welding fixture where robotic gun will be used for spot welding hence the fixture should have ample of space that the spot gun should be come in do its work should go out without striking to any of the part of the fixture.The green spots shown in the image are the spot weld where the spot welding will be done by the welding gun.so we have to place the fixture parts by considering the spot weld and also by doing the gun study we have to check the fouling of parts with the gun.
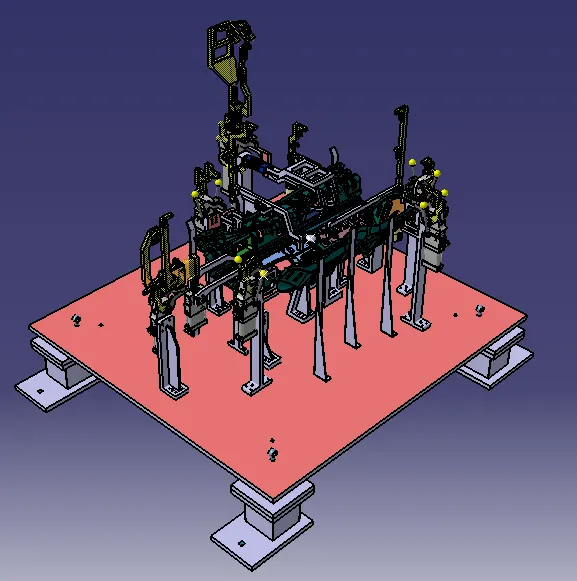
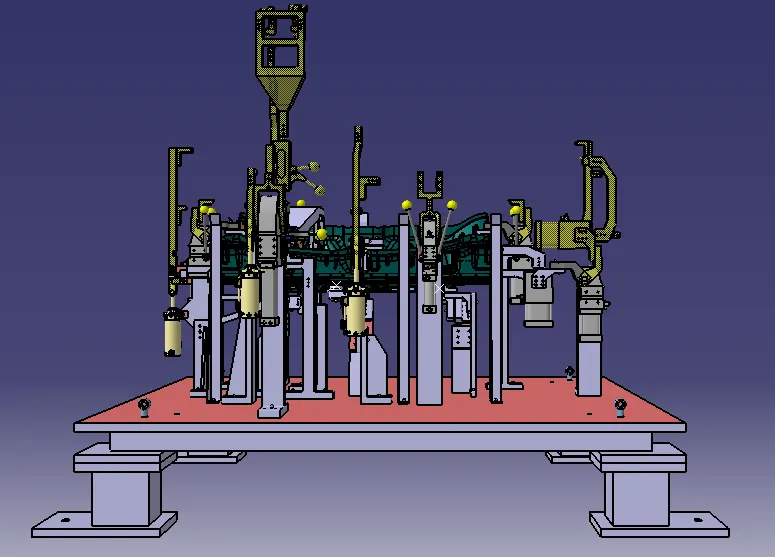
DESIGN OF FIXED PIN UNIT:
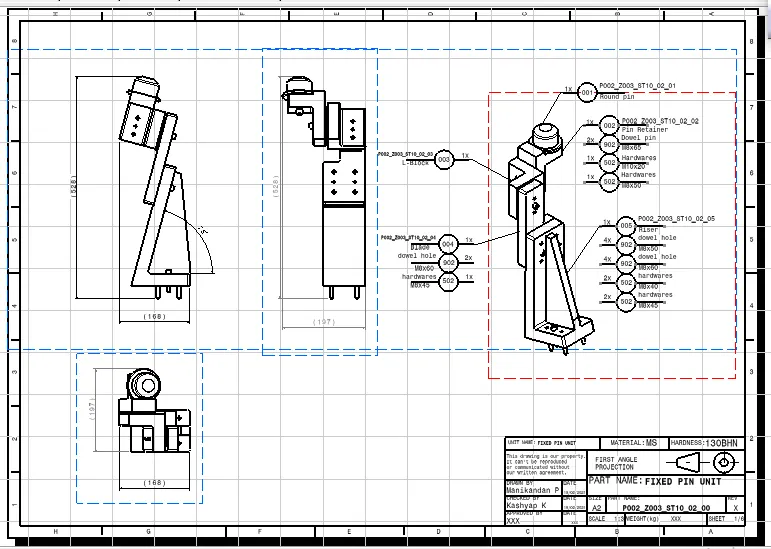
As per the 3-2-1 principle of the fixture we have to constraint degrees of freedom of part so at the time of operation there will be less chances of destrotion.For this purpose fixed pin units and retractible pin units are designed.
Retractable pin units have 3 way shim adjustable & fixed pin unit have 2 way shim adjustment.
DESIGN OF PIN CLAMP UNIT:
Some panel are complex in shape and less availability of space to place and we cannot use multiple units for one part.To solve this probles we use pin clamp unit.It is the combination of pin unit and clamp unit.
we can use either fixed pin unit or retractible pin unt depends upon the panel design.In this project the part of the given car panel is welded from upside of the main part,and also we cannot place pin on bottom of the panel.so, the pin must engage on the upper side of the panel for that we should use retractible pin unit.
Firstly, the panel is engaged on the fixed pin uits and then the retractible pin units are engaged on the upper side of the panel .After the welding process is done ,now retractible pin unit is disengaged and then the panel is free to take out.
There is a problem in using the pin unit on the upper side that is the pin is disengaged from panel but it is still stands above the panel.we cannot take the panel on this case, to solve this problem i used combination of pin unit and clamp unit.I attached clamp unit with the retractible pin unit,now the pin unit is rotated to 90 degrees and now the panel is free to take out from the fixture.
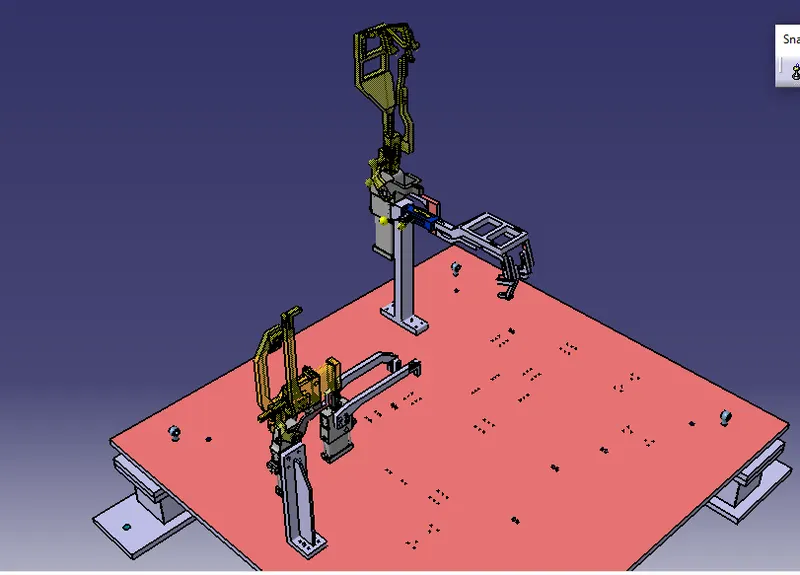
Another main thing is that, firstly the pin is retracted and then rotated to 90 degrees orelse it will damage the panel .
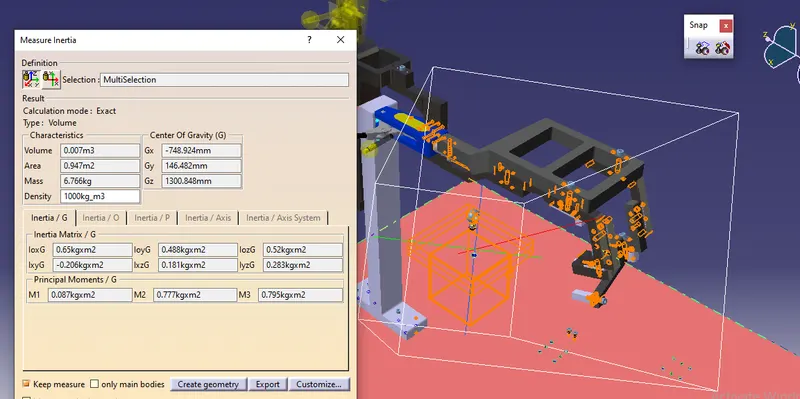
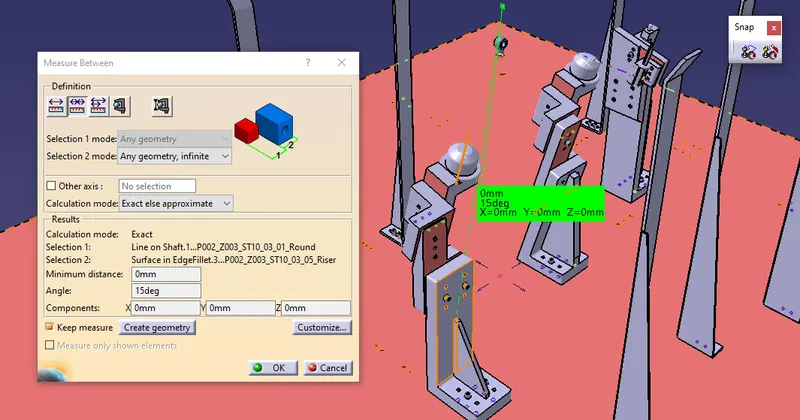
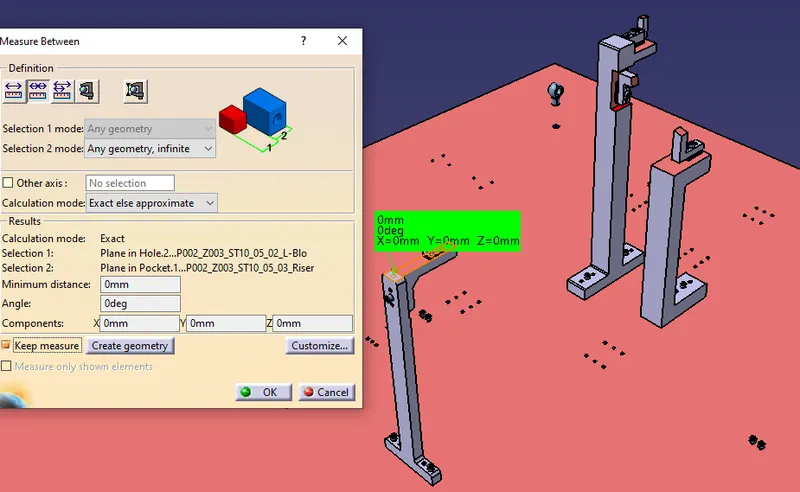
From the above picture it shows the total weight of the clamp arm and other parts attached to it.
The total weight is around 8kgs
The cylinder used is 80 bore capacity cylinder and its maximum load capacity is 14kgs
So, the cylinder can lift the parts attached to the clamp arm.
DESIGN OF SWIVEL CLAMP UNIT:
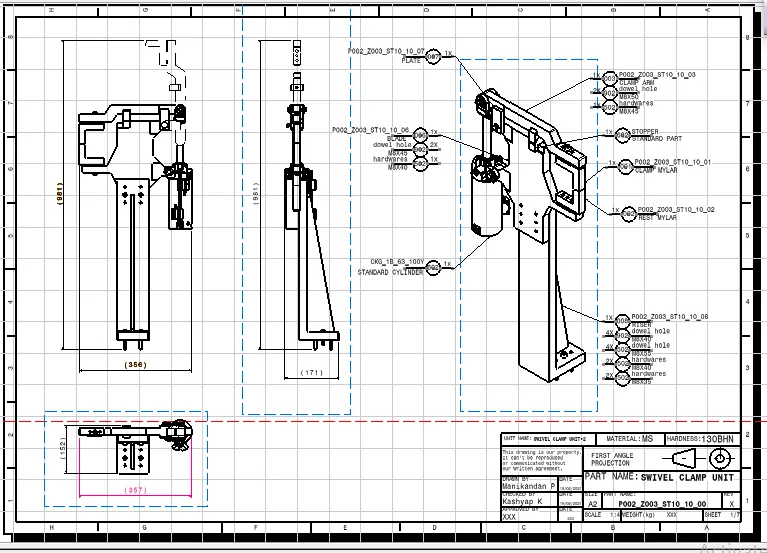
To clamp the part at the center of the panel,we should use large clamp arm,clamp mylars are fixed at the end of clamp arm.In such cases we should swivel clamp unit for proper clamping.
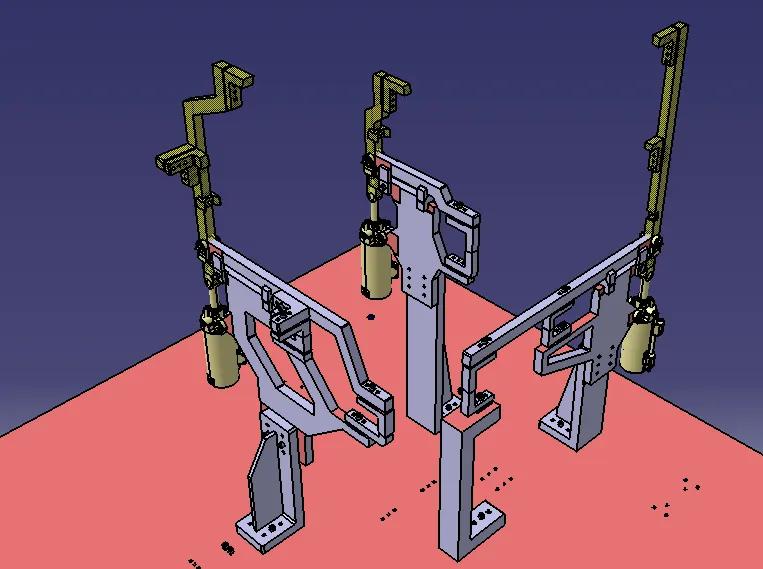
DESIGN OF POWER CLAMP UNIT:
Power clamp unit is the unit is designed to hold the car panel on the position to do some process over the part.It includes NC block/Rest/Mylar by using pneumatic clamp cylinder.The power clamping devices are utilized for positiuoning and holding product securely.It applies pressure on the product to hold it on the specified positions.The holding should be firm enough to hold part on its position & also it should not damage the part as well.
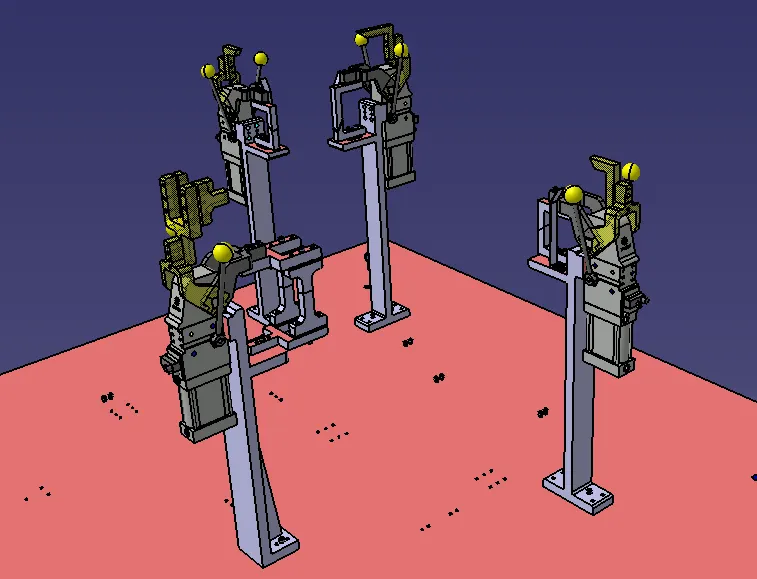
A clamp cylinder is a pneumatic device works with pressuried air.The clamp cylinder is used to open and close the parts fixed to the clamnp arm fixed to the clamp body.
- clamp cylinders are brought out part.
- They are in general 40,50,63,&80 bore capacity.
- Opens upto 135 degrees for horizontal clamp mounting.
- Opens upto 105 degrees for vertical clamp mounting.
DESIGN OF REST UNT:
Rest unit is used where the clamp arm of some unit is large.we cannot place rest mylar for those units have larger clamp arm.For that we use seperate unit to place the rest mylar called rest unit.
DESIGN OF BASE UNIT:
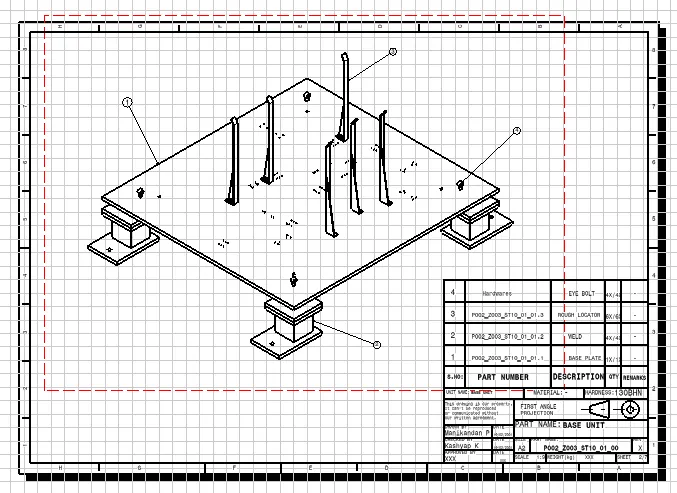
BASE UNIT unit is the unit designed to mount all the other units (clamp units,pin units,rest units etc) of the tool, also other parts necessary for a tool like pneumatic valve box,truncking cable path will aslo be mounted on to a base unit.
3D FINISH:
3D finish is the process where design is being completely finish & to be ready for final simulation &2D detailing.
Following points are taken into consideration while finishing the design.
- Hole concentricity &Hole sizes:Holes of all of the parts are checked & confirmed while finishing the parts.
- Machining area:Machining area in every part is defined & the machining area is highlighted by using orange color.
- Nominality:All units dimensions are maintained nominal to facilitate easy assembly of the unit.
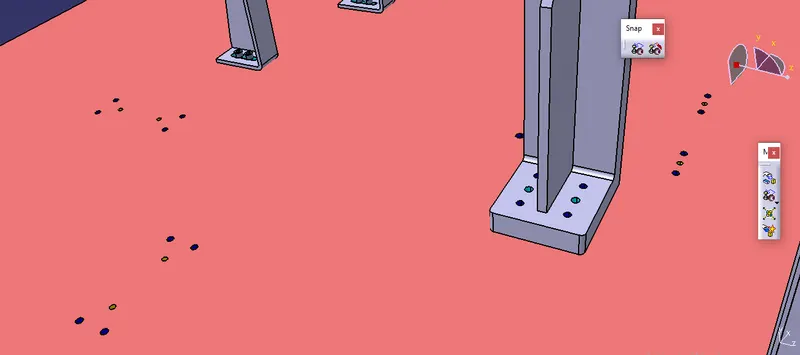
- Holes colouring standard:Color code standard used in the 3D Finishing.
1.) CYAN -Simple hole
2.) YELLOW - Threaded hole
3.) ORANGE - Machined area
4.) BLUE - Dowel pin hole
5.Fasteners Implementation:Fasteners are implemented in all unit as per the requirement and load on the part.
6.Avoid clash b/w different part:Proper gap is maintained between parts to avoid the clash.
7.Mylar splitting as per panel profile:Mylar splitting are confirmed while finishing the design.
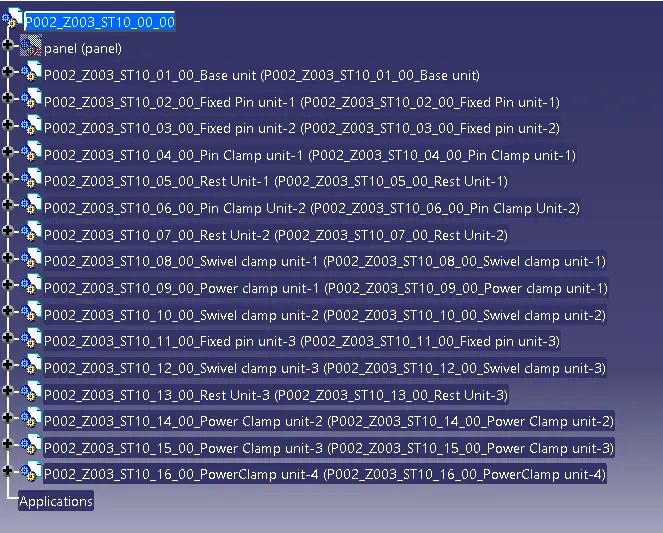
8.Proper renaming of parts/assemblies as per standard:It is done while finishing the design hence we can identify each and every part easily with unique identification.
2D DETAILING:
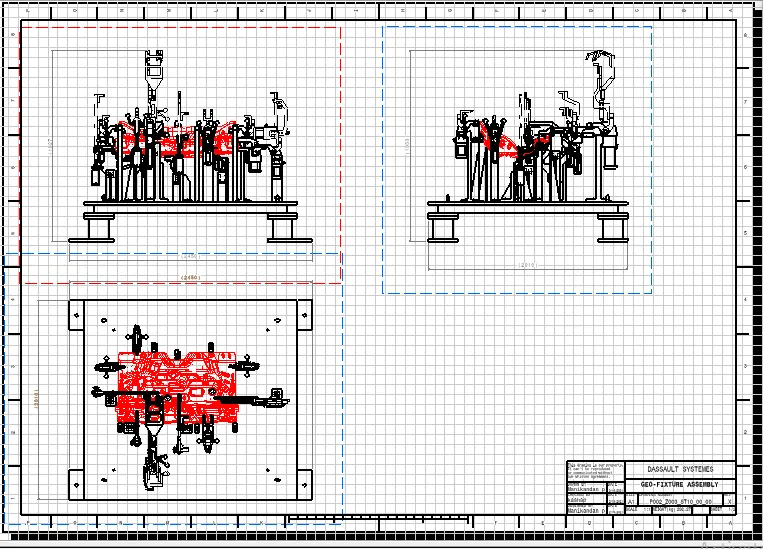
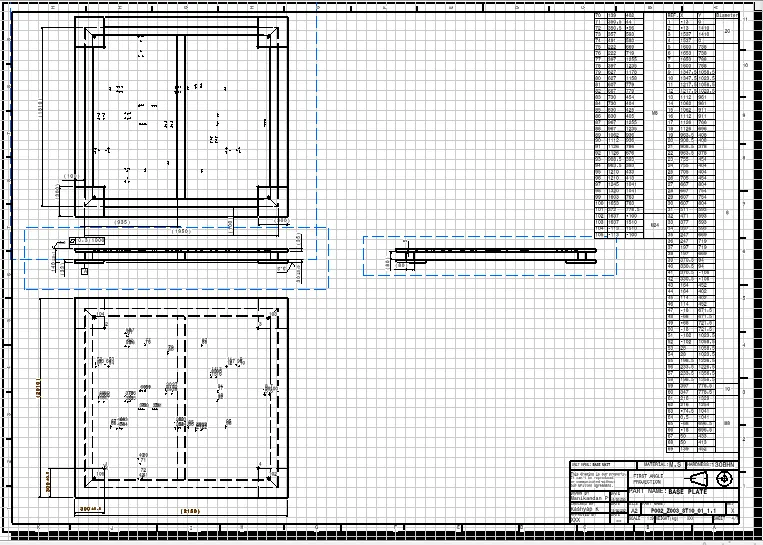
A 2D drawing view consists of two dimentional elements.A 2D drawing view allows you to quickly create or modify a drawing view without making changes to a part or assembly document.
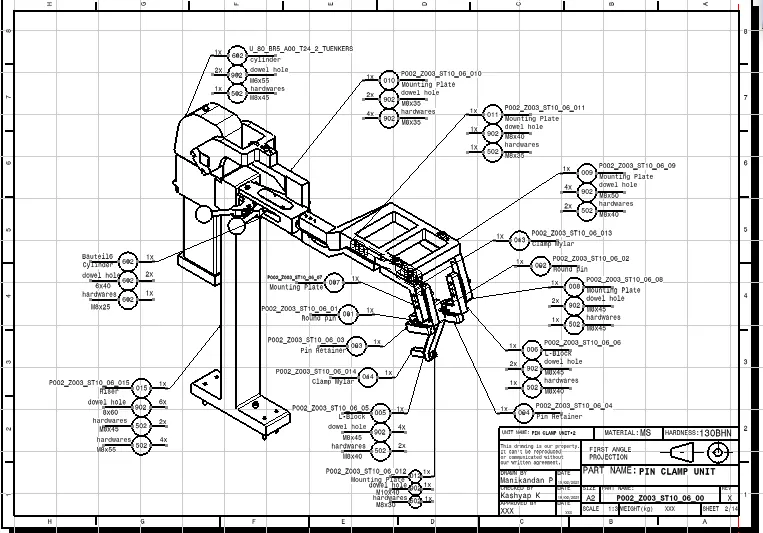
In fixture detailing key sheet detailing of every unit is done which gives the idea placing of unit in assembly.
BOM PREPARATION:
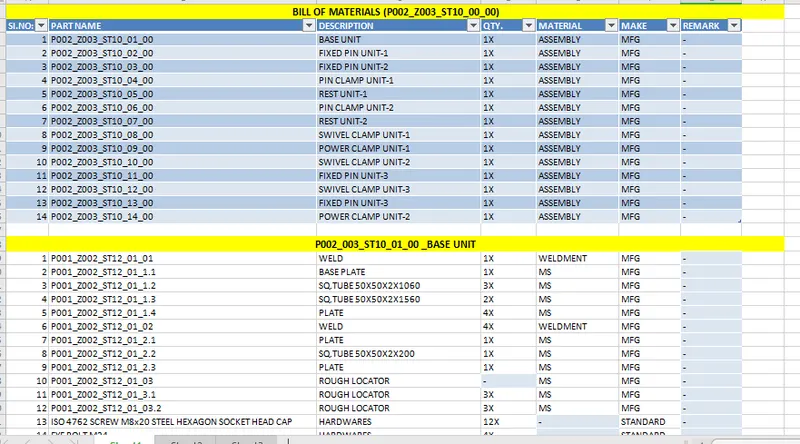
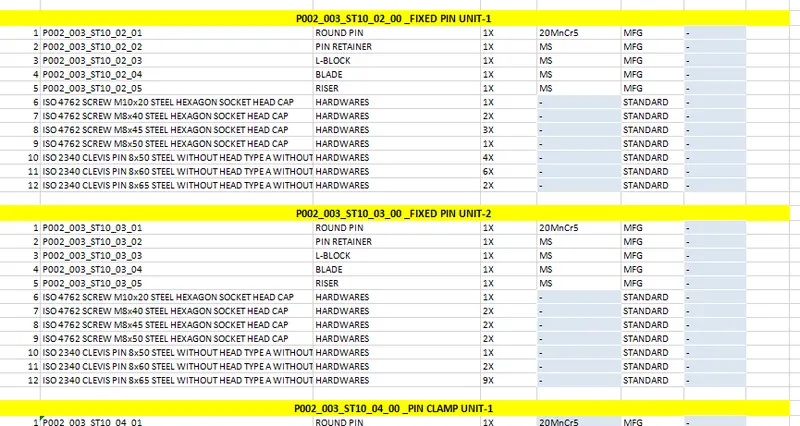
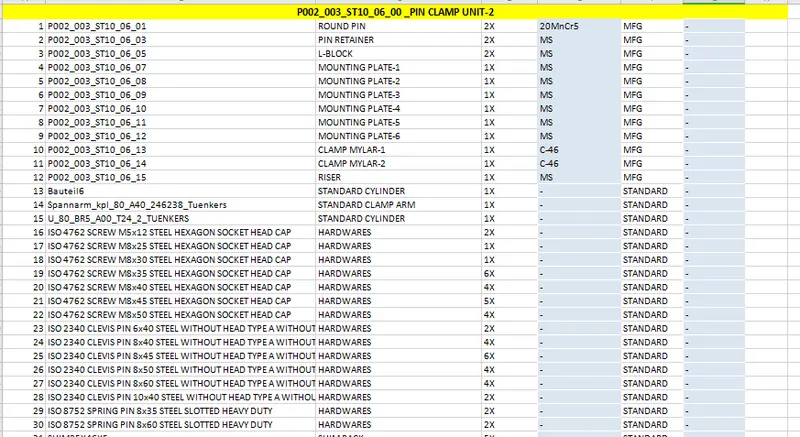
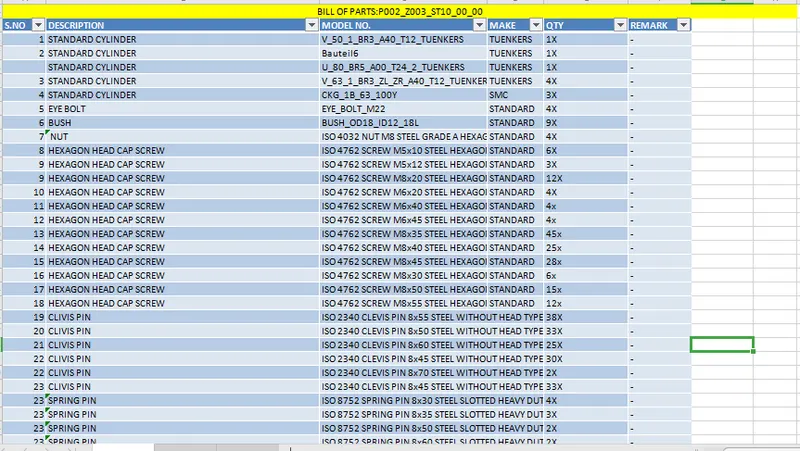
A BOM serve as the foundation of production planning systems,And the informations in it provides the basic data for other business processes,such as manufacturing resorce planning ,product costing,material provision for production and plant maintenance.
DESIGN TREE:
CONCLUSION:
As per the objective concept for fixture design is illustrated , performed and 2D finish with output documentation.