Hood design-Week 2
HOOD INNER AND OUTER PANEL DESIGN
HOOD : The hood (North American English) or bonnet (Commonwealth English) is the hinged cover over the engine of motor vehicles. Hoods can open to allow access to the engine compartment, or trunk on rear-engine and some mid-engine vehicles for maintenance and repair.
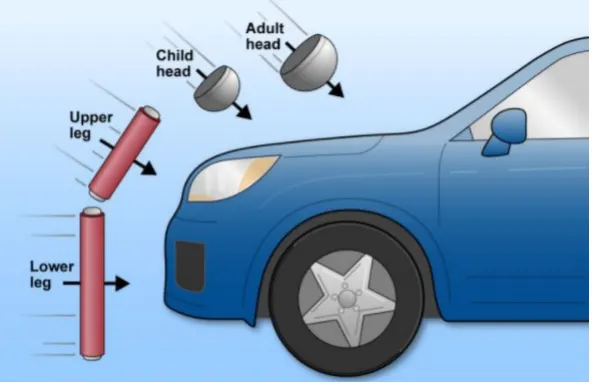
On front-engined cars, the hood may be hinged at either the front or the rear edge, or in earlier models, it may be split into two sections, one each side, each hinged along the centre line. Hoods are typically made out of the same material as the rest of the body work. This may include steel, aluminium, fiberglass or carbon fiber. However, some aftermarket companies produce replacements for steel hoods in fiberglass or carbon fiber to make the vehicle lighter.
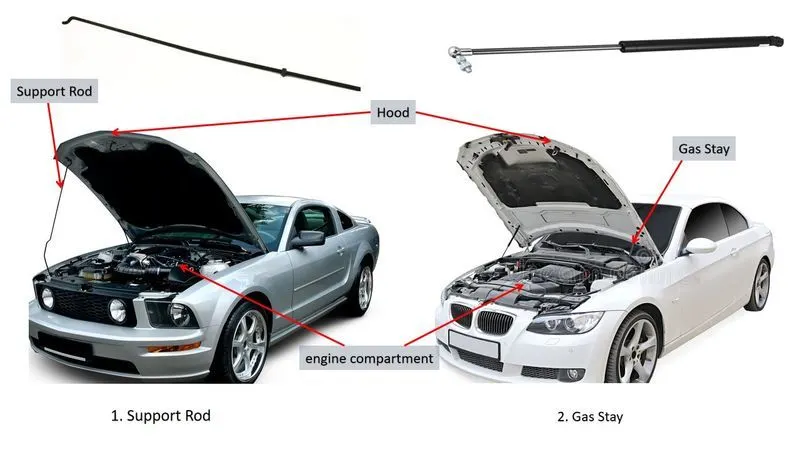
Hood is typically supported by rods or some fixtures, so that it stays at a position and a person can lean onto it hassle free and work. These includes
Support Rod : A hood rod is designed to hold your hood propped open whenever you need to do some work in your car's engine bay. When used, it must be firmly secured to ensure that it provides a stable hold on the hood. Meanwhile, when not in use, it must be kept stable in place and must not move around. The hood rod clip is the part assigned with that function. This clip clamps onto the rod and ensures that it is firm in its place when not in use. It keeps the rod from moving around under the hood and from causing trouble.
Gas Stay : This is used to open the car hood by just providing little lift force. A small effort is all it needs and other work is done by gas pressure. It is normlly found in high-end cars where the mass of hood is more than normal
Head zone for lock striker :
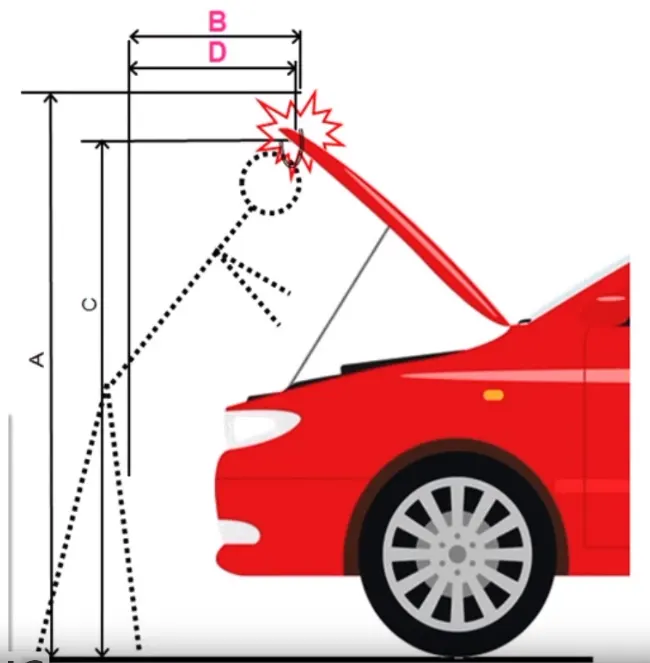
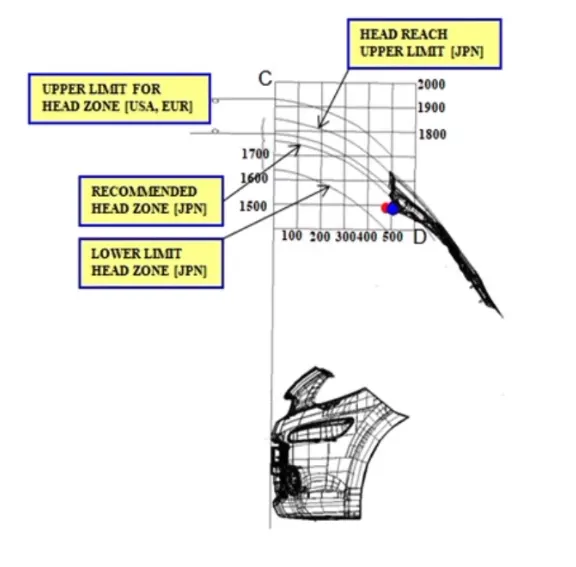
The opening of the hood should follow the circular trajectory, which circle is drawn from the mid-point of the line drawn between the both the hinge axis. In the opening condition of the hood, the head should touch the customer, means we have to design opening angle of the hood such that it does not interfere with the average height of the person in that particular region. The average height of the height of the person is varied from country to country.
Manufacturing operations
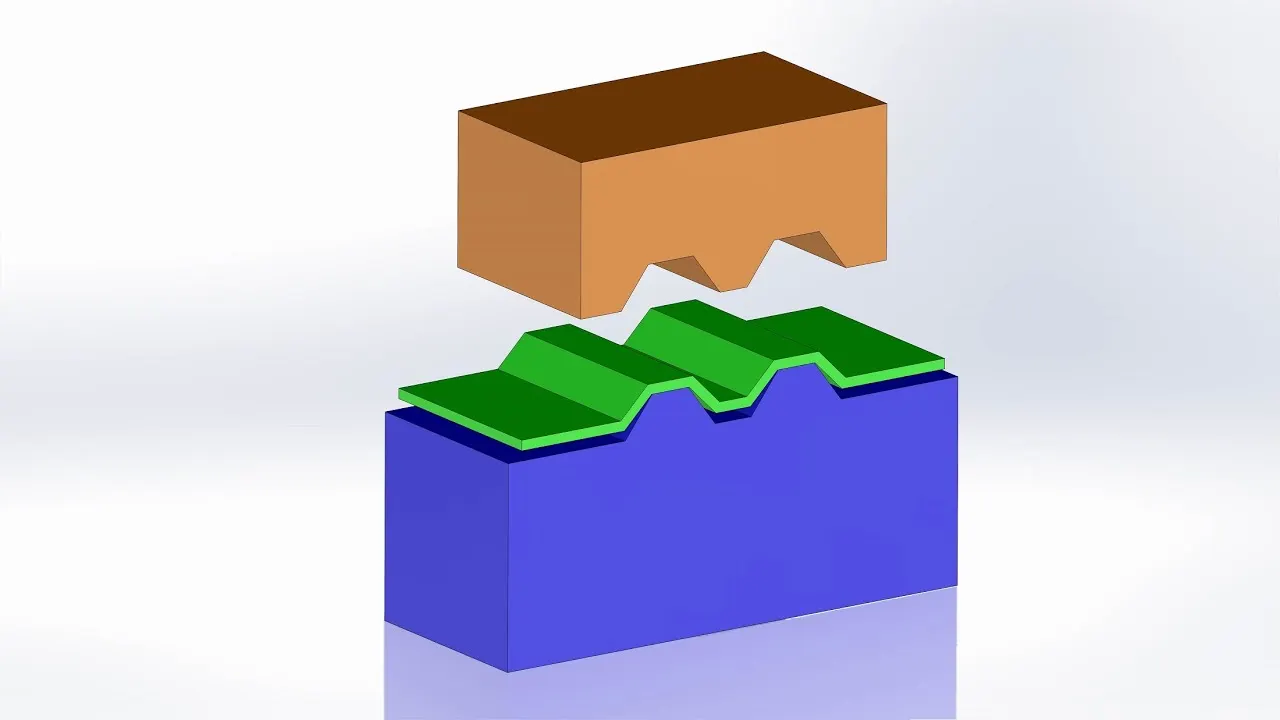
Forming operations (Deep drawing) :
It is sheet metal forming process, in which a sheet meatl blank is slightly clamped along it perimeter by a blank holder and radially drawn into a forming die by the mechanical action of a punch.
If the depth of the cup is more than half of its diameter, the process is termed as deep drawing.
The deep drawing is used to manufacture a product with seamless, complex shapes. This is tool related manufacturing process where the meatal is stretched or extended between two tool havles to create prospective shape.
Embossing :
Embossing is the process of creating the raised portion in the sheet metal. Usually, the emboss is created by stamping process for producing raised or shrunken designs or relief in sheet metal.
Blanking and piercing :
Blaking and piercing are the shearing processes in which a punch and die are used to produce parts from coil or sheet stock. The blaking produces the outside features of the component, while piercing produces internal holes or shapes.
Joining operations (Hemming) :
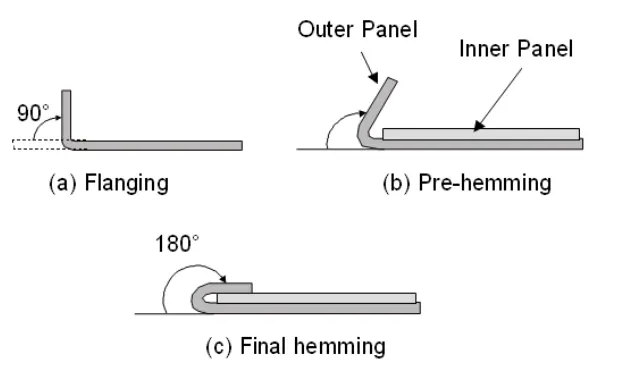
In automobile industry, the panels which are visible outside are joined with the inner panels or supports with the help of the hemming process. Hemming is comes into for outer panels because thermal joining processes leave the residual marks which are acceptable on the aesthetic surfaces.
Hemming is the technology used in the automotive industry to join inner and outer closure panels together. It is the process of bending/folding the flange of the outer panel over the inner one. The accuracy of the operation affects significantly the appearance of the car's outer surfaces, and is therefore a critical factor in the final quality of a finished vehicle.
Hemming is performed in order to achieve a better final geometry in the vehicle's part and add resistance and rigidity to the part. Also, to allow a safe handling of the part.
DATA:
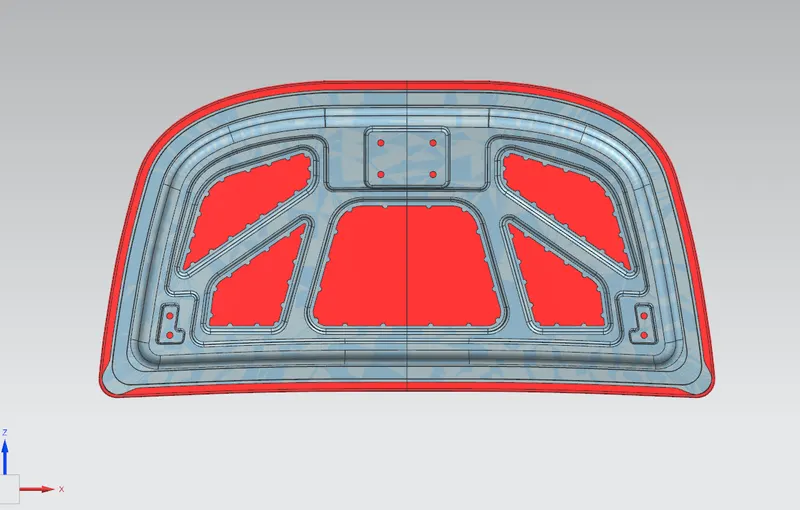
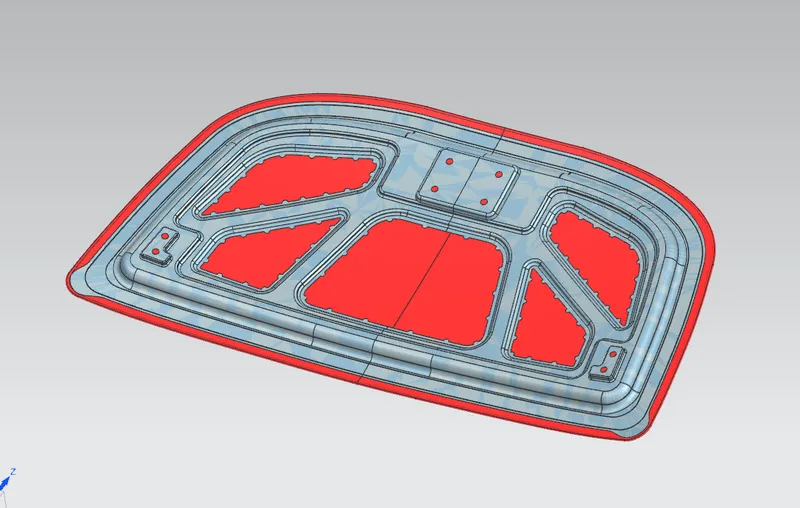
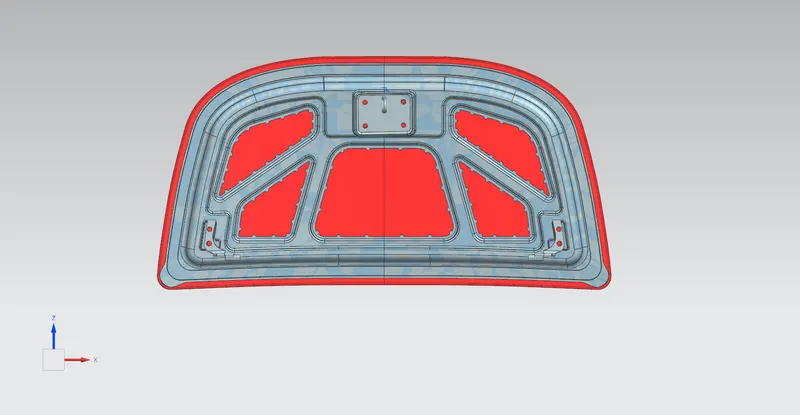
Inner hood has been designed by following the master data:-
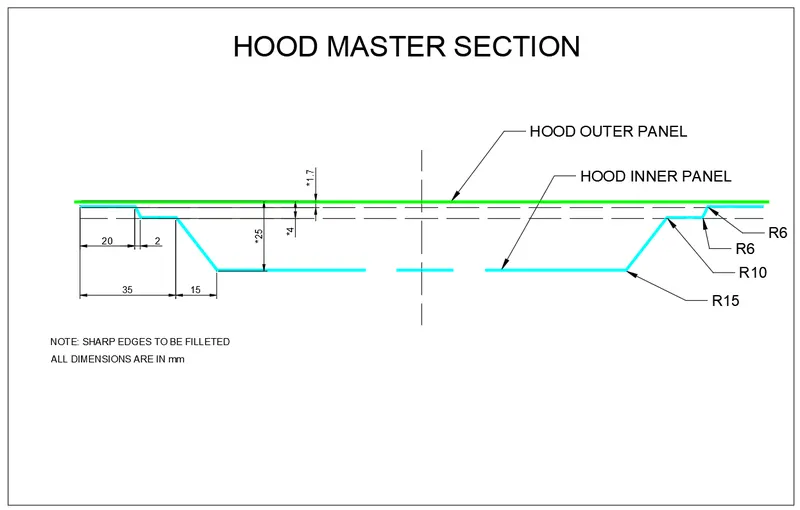
Hood thickness:-
- Outer panel thickness:- 0.75mm
- Inner panel thickness:- 0.75mm
- Reinforcement thickness:- 1.5mm
Design Procedure:
We will design the inner panel first, so lets start with the given data, a body stretched to full dimension of outer panel.
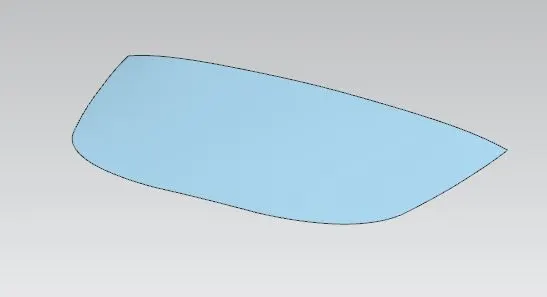
Next trim the sheet into half.
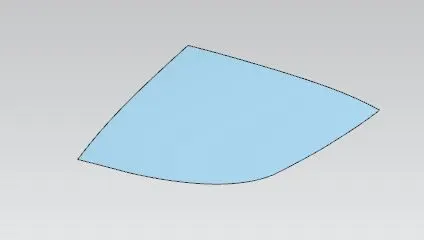
Take a topmost surface offset and keep dimensions according to master section, i.e. 2mm.
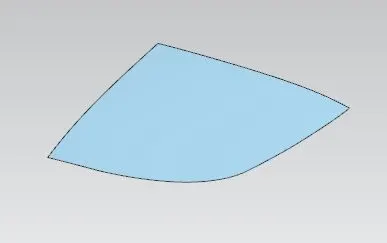
Taking curve offset on surface of 20mm.
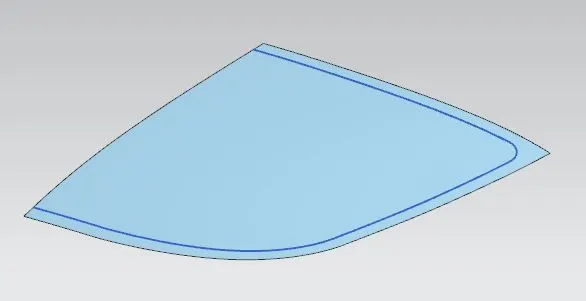
Trim sheet and keep the outer part.
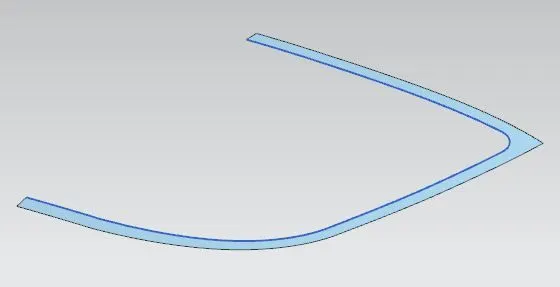
Take another surface offset of 4mm.
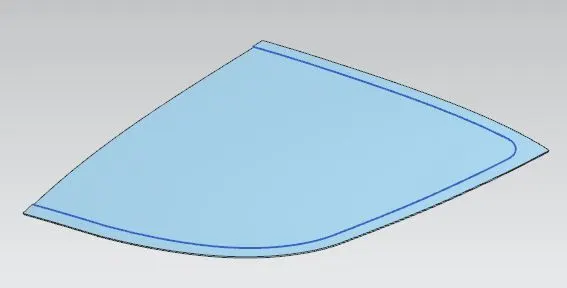
Now offset curve same way for 22mm inside.
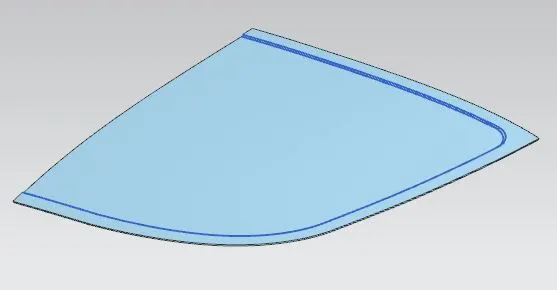
Trim outer part of sheet.
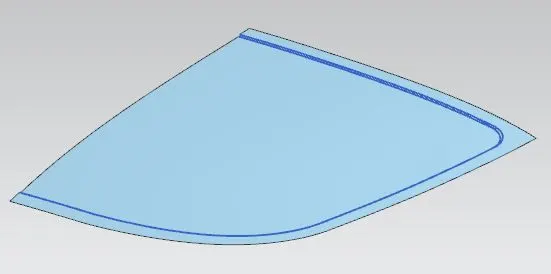
Now we add surface through curve and fill the gap.
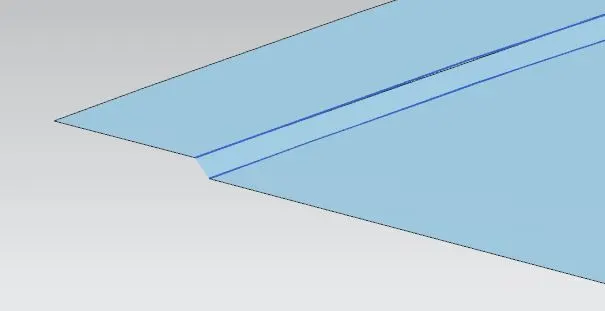
Taking another offset of same surface upto 25mm.
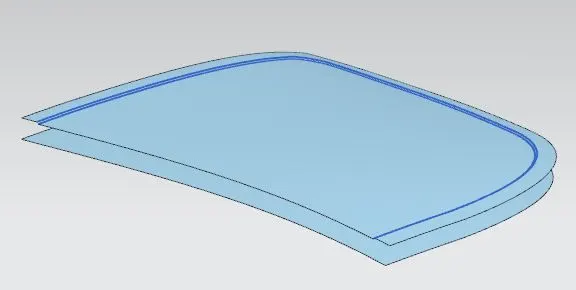
Do curve offset on surface and trim sheet.
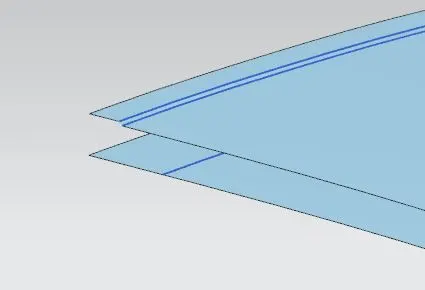
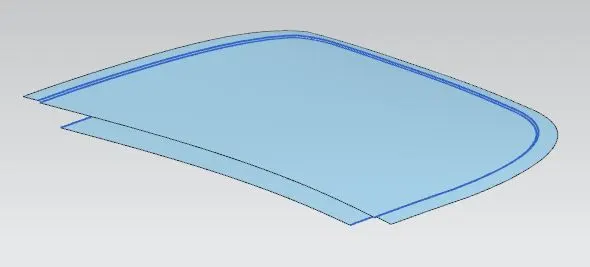
Now to fill gap, we create surface by law extension command and keep draft of 5 degrees outwards.
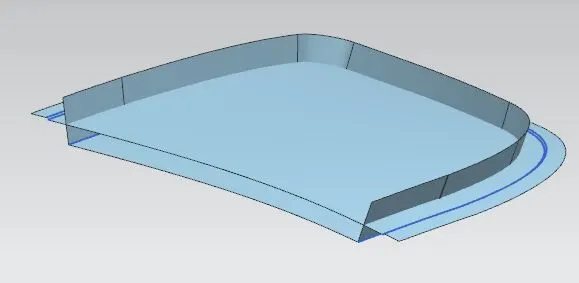
Using trim and extend feature, we eliminate some part and get this structure.
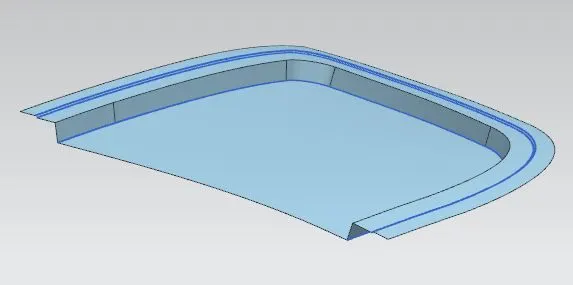
Now we will blend these sharp edges by edge or face blends and keep dimensions as said.
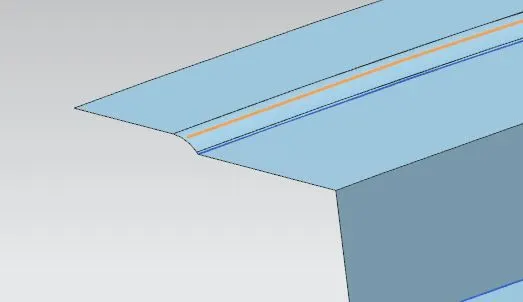
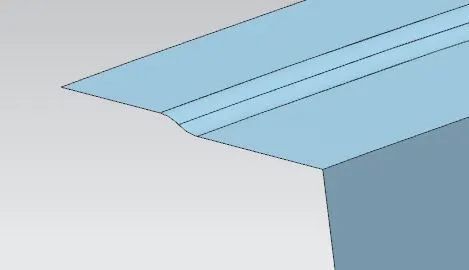
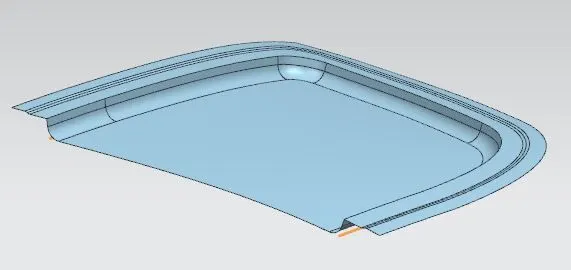
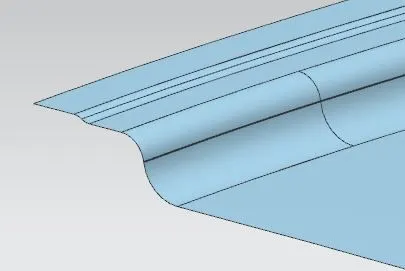
After blending, we will create a sketch and project it to the surface. We keep some space for hinge and striker reinforcement.
We follow it by Law extension surface, offset the base surface to 5mm upward and apply trim and extend to get an embossed shape for the profile.
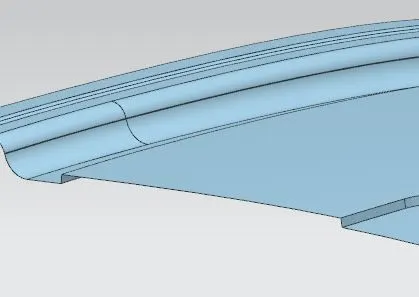
We create one more sketch and project it to the same part. Later, use law extension with draft, surface offset of 5mm, trim and extend and trim sheet to get desired output.
Another sketch we create to remove some material from the workpiece, so we can give some hollowness to the panel for safety reasons. Add spots for mastic points. Then project it in same direction as did before.
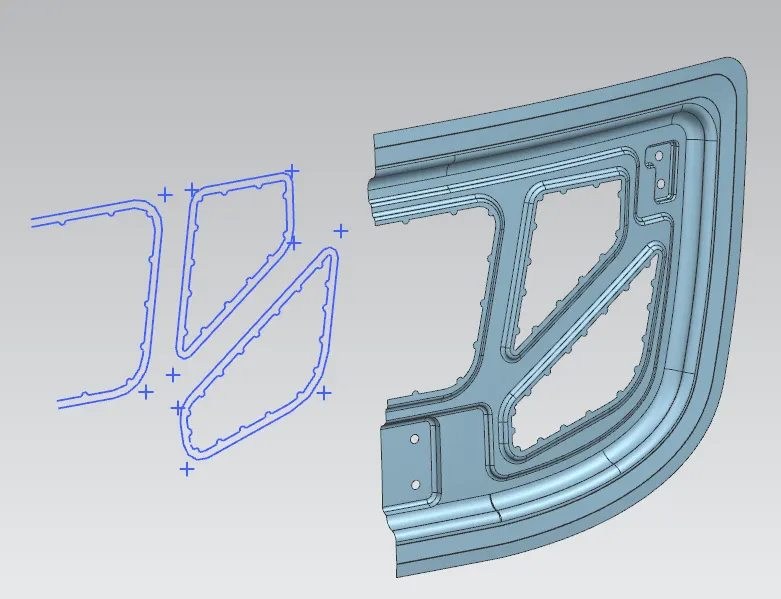
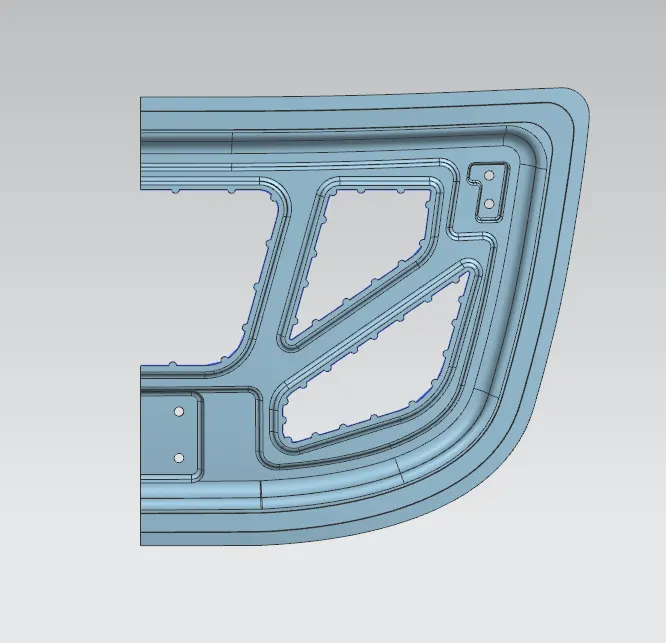
Now we adjust our hinge assembly and striker in position that we want and make profiles for their reinforcements. Project them to surface.
Keep the assembly little away from panel, so that we can add a vertical datum plane and emboss the same profile uptill that plane.
Eliminate the part that is needed for fixation. And you can see the assembly is well set to the embossed surface.
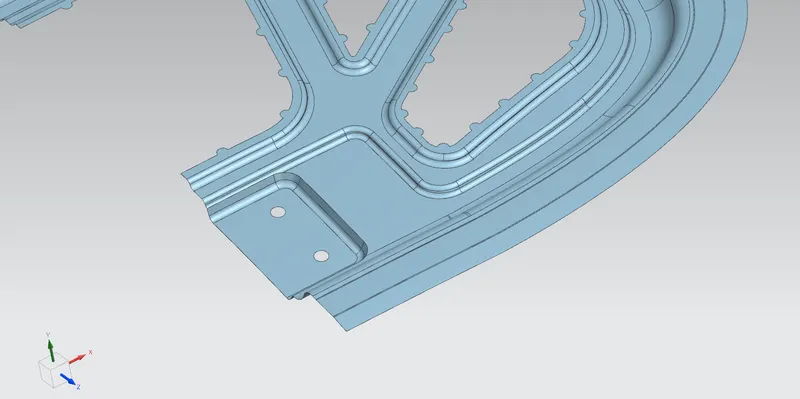
Mirror the entire model and sew it.
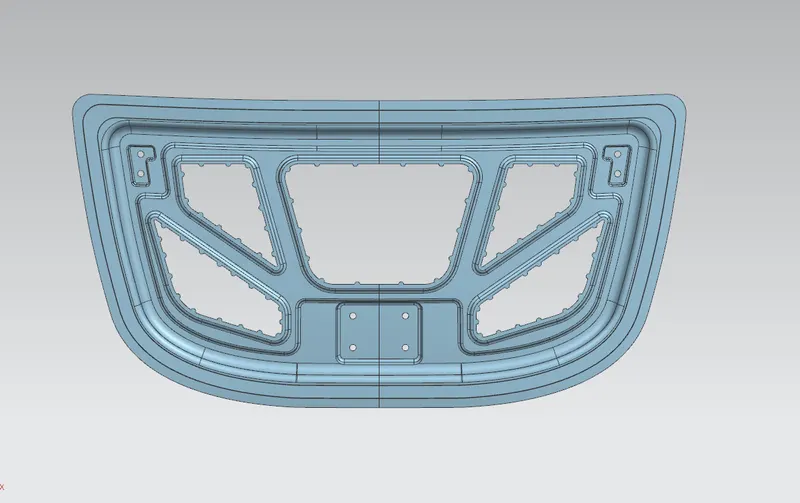
Now, finally we give thicken command of 0.75mm and we get our inner panel. Make sure the direction goes up.
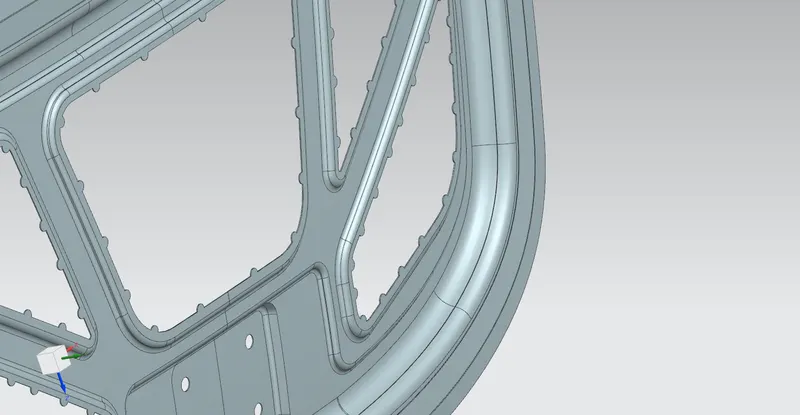
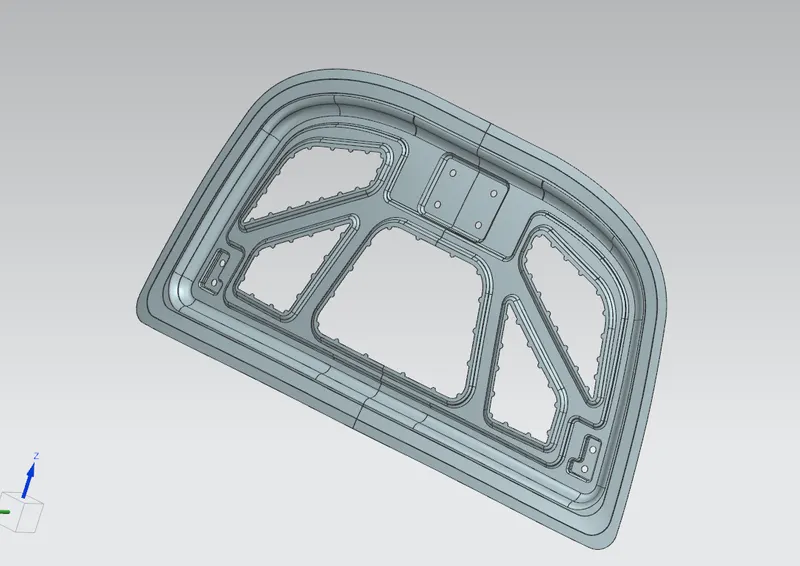
Now, we come to other part of designing the outer panel. So we start with the same body as default and trim that into half.
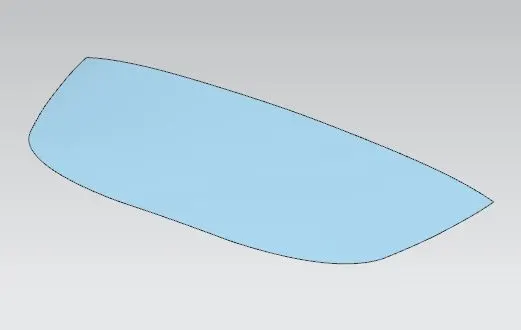
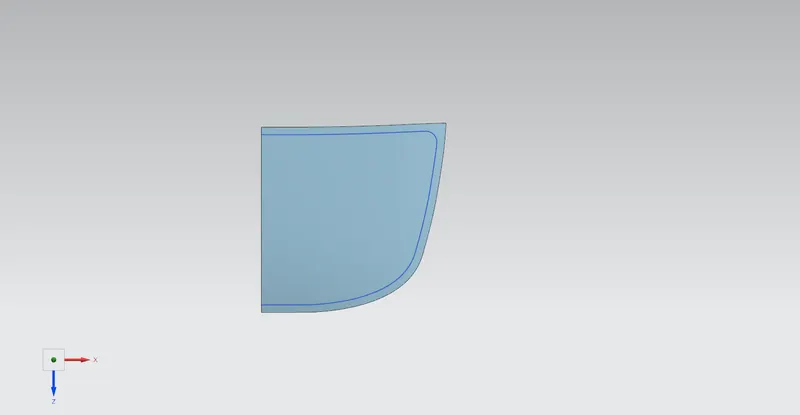
Extend the surface by law extension and keep draft of 5 degrees.
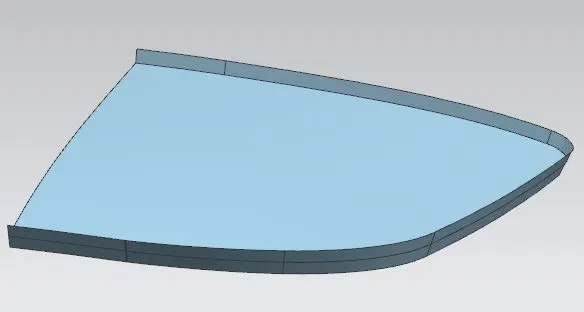
Now, take surface offsets of both the surfaces available. Here, for the law extended one we take 7.5mm inside and for the workpiece we take 2.8mm down. (keeping all the sheet thickness and gaps between them, we are taking 2.8mm)
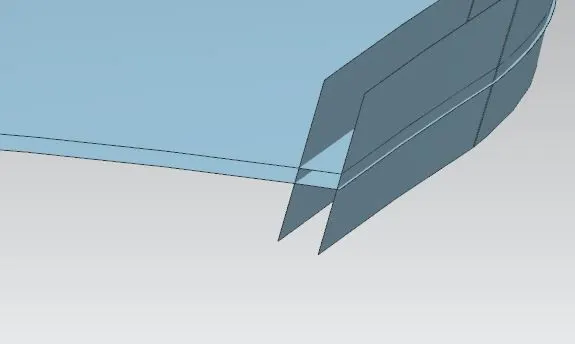
Trim the unwanted part of offsetted surface.
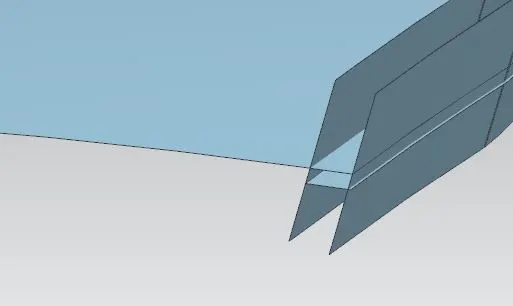
Now with the remaining three we create a face blend. The vector direction for upper surface goes down, bottom ones goes up and side ones come inside.
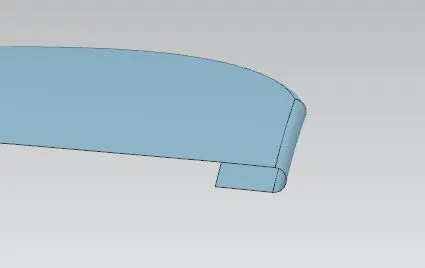
For this hemming we keep some relief at the rear end and front end too.
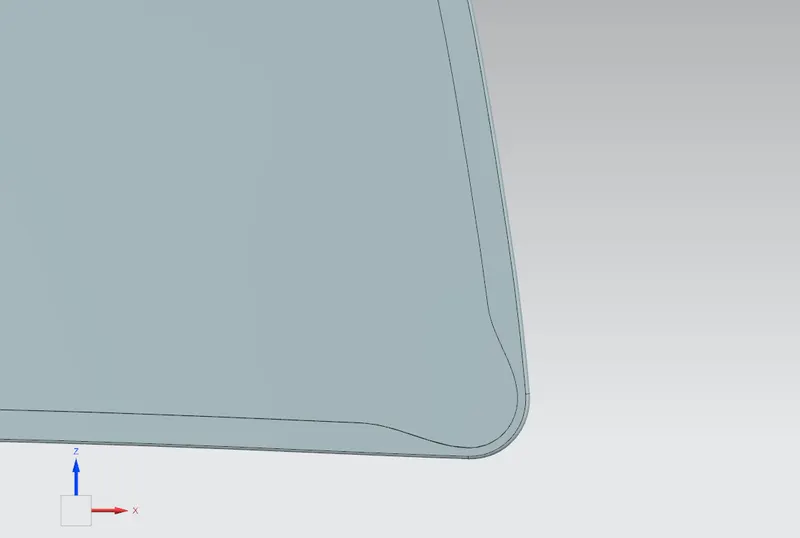
Now we can mirror the part to the plane and sew it.
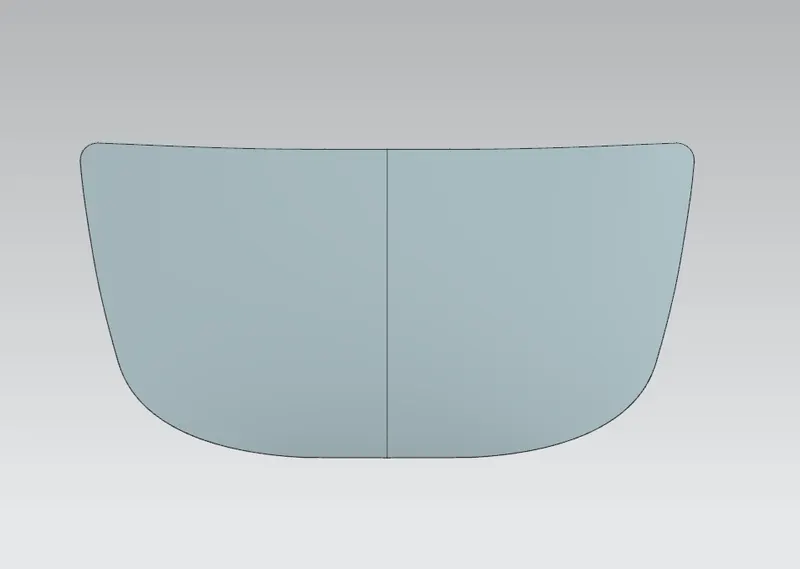
Give thickness of 0.75mm to the part. In this the direction goes down.
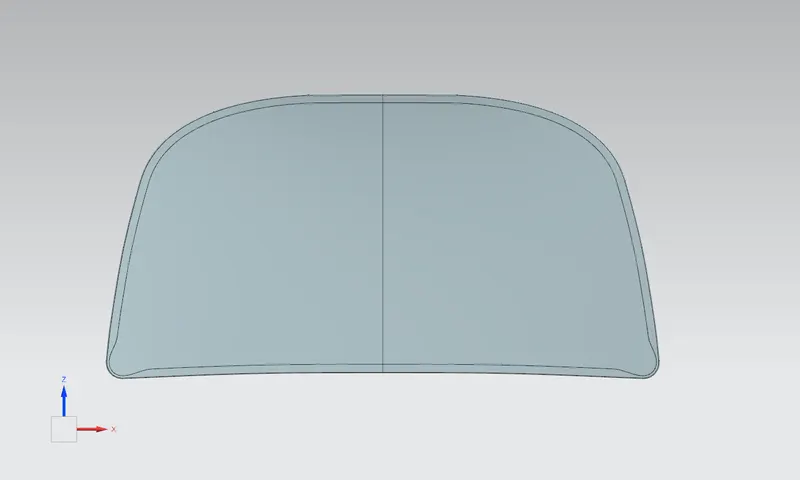
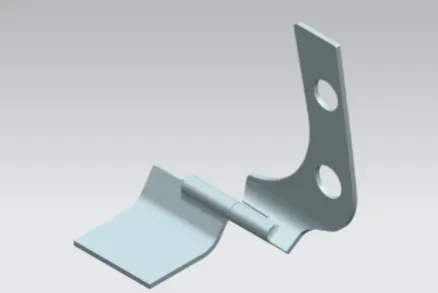
Hinge Assembly:-
A hinge is a component that connects the hood to the car's fenders. To ensure that the hood opens and shuts properly, the latch must be placed perpendicular to the hinge axis.
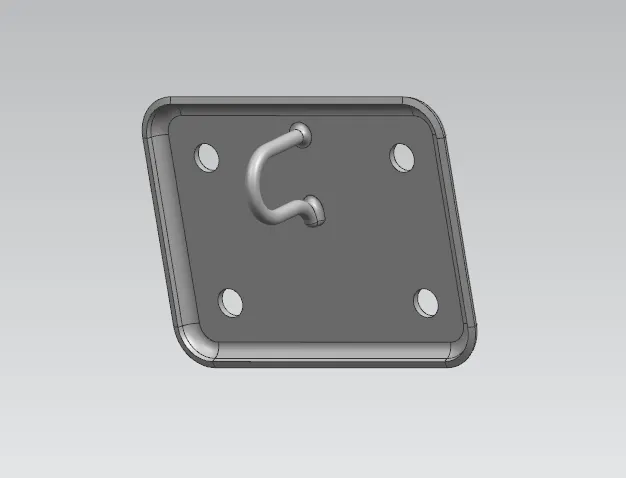
Striker:-
The latch and striker are used to secure the hood to the automobile. It is often positioned in the area given on the inner panel.
Now, we can assemble all the components together and can aslo set the contraints for striker and hinge assembly so that they dont have any freedon of moving.
Conclusion:-
The hood is designed with norms and regulations of the manufacturer's specifications.