Fender Design
OBJECTIVE
- To design a front fender from the given skin data and the master section provided with Drip mounting, A-pillar, Sill, Bumper and Baffle (splash) Mounts.
- To Prepare a report by explaining about Fender Design and its different mounts , manufacturing process and its design parameters.
INTRODUCTION
Fender
Fender is the term for the part of an vehicle body that frames a wheel well (the fender underside). Its primary purpose is to prevent sand, mud, rocks, liquids, and other road spray from being thrown into the air by the rotating tire. Fenders are typically rigid and can be damaged by contact with the road surface.Sticky materials, such as mud, may adhere to the smooth outer tire surface, while smooth loose objects, such as stones, can become temporarily embedded in the tread grooves as the tire rolls over the ground. These materials can be ejected from the surface of the tire at high velocity as the tire imparts kinetic energy to the attached objects. For a vehicle moving forward, the top of the tire is rotating upward and forward, and can throw objects into the air at other vehicles or pedestrians in front of the vehicle.
There are two types of of fenders
1. Full Bumper Type.
2. Half Bumper Type.
Full Bumper Type
Full Bumper type
This type of fender is used in olden days, it is no more in use due to its heavyweight of the structure and consumes more (RAW MATERIAL) in manufacturing.
Half Bumper Type
Half Bumper Type
Half Bumper Type fenders are widely used now, due to its mini size and the scrap or wastage is less compared to the full bumper type.
DESIGN METHODOLOGY :
GIVEN DATA :
MANIFACUTRING PROCESS OF FENDER
The manufacturing process includes the following steps that firstly, unfolding and shearing are carried out on a plate, wherein a proper cold roll specification is selected at first, a cold roll is unfolded, and then the unfolded cold roll is sheared to an iron plate of the corresponding size according to production material specifications; secondly, oil pressing and punching are carried out, wherein the iron plate is extended at first, then side shearing and punching are conducted on the iron plate, folding and shaping are carried out on the iron plate, and finally reshaping is carried out on the iron plate; thirdly, small first parts of the fender are machined, wherein first of all, the iron plate is punched to a needed outer contour blank, then the iron plate completing the outer contour blank is further shaped, and the iron plate is punched at last; fourthly, installation and welding of a metal plate are conducted. The manufacturing process for the car fender is simple and high in production efficiency; a body of the fender and the small parts can be separately machined, so waiting time is shortened; working efficiency of production is improved.
The manufacturing of the fender majorly involves these operations.
1.Embossing
2.Bending
3.Cutting and Blanking
Embossing
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet material using matched male and female roller dies, theoretically with no change in metal thickness, or by passing sheet or a strip of metal between rolls of the desired pattern.
Bending
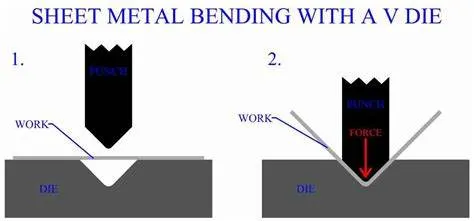
Metal bending is a process by which metal can be deformed when applying force to the subject, which causes it to bend at an angle and form the anticipated shape, which often results in it being in a ‘V’ or a ‘U’ shape. This is done through the application of force on a workpiece. The force on the work piece can be mechanical, pneumatic or hydraulic.
Cutting and Blanking
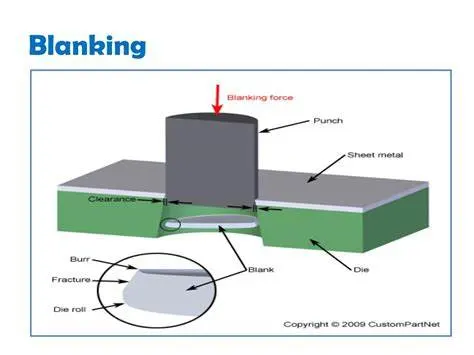
Cutting processes are those in which a piece of sheet metal is separated by applying a great enough shearing force to cause the material to fail.
Blanking is a steel manufacturing process in which a flat, geometric shape is created by feeding a coil of sheet metal into a press and die. In this process, the blank is punched out from the large metal sheet.
Fender is mounted basically on 5 important regions. They are
1. Drip Area
2. A-Pillar Mounting Area
3. Sill Mounting Area
4. Bumper Mounting Area
5. Baffle Mounting Area
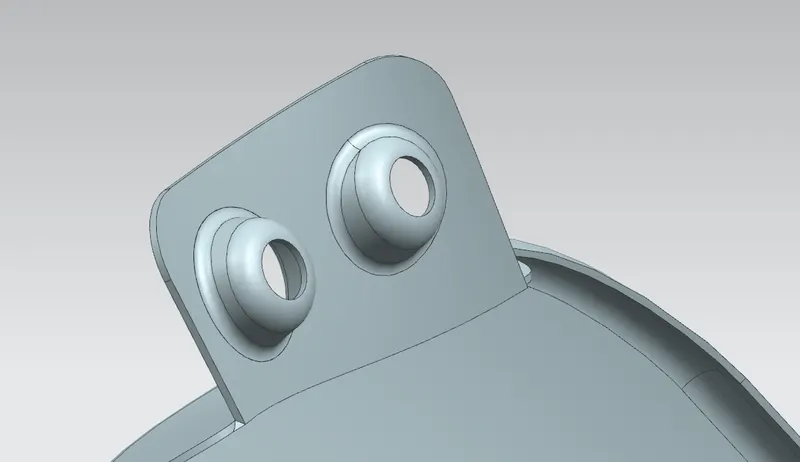
Drip Area
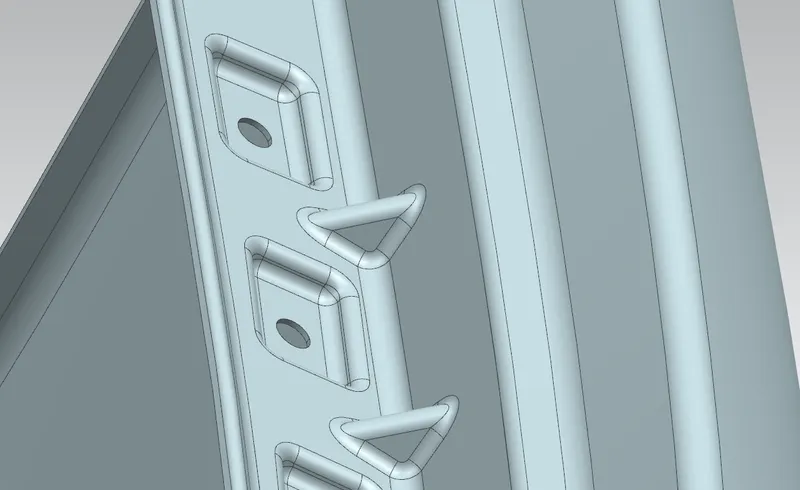
The area at which the fender gets attached to the engine housing through fasteners. It is the major mounting for the fender. Mountings at the drip area are designed leaving a clearance of 200mm from the back of the fender for the cowl setup. And clearance of 150mm from the front of the fender for a headlamp housing unit.
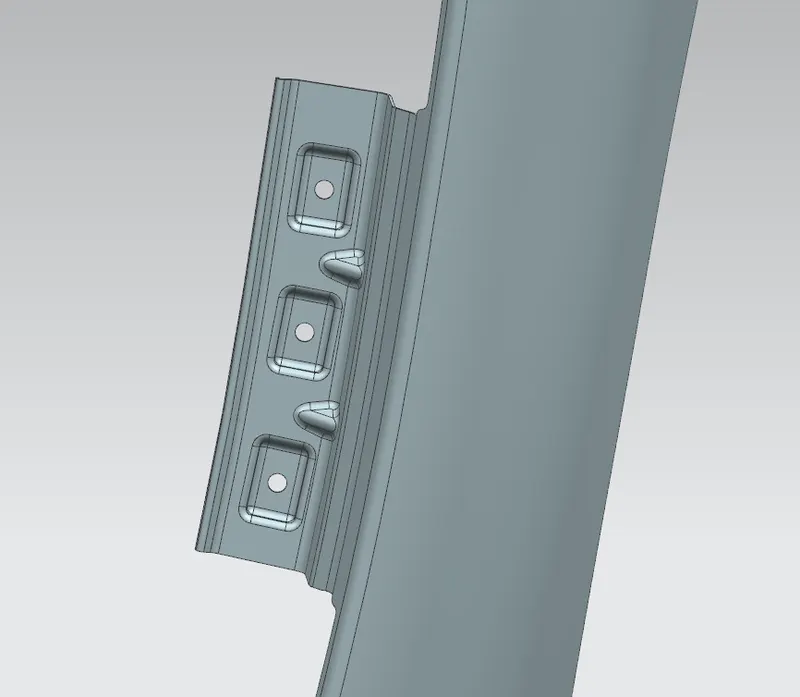
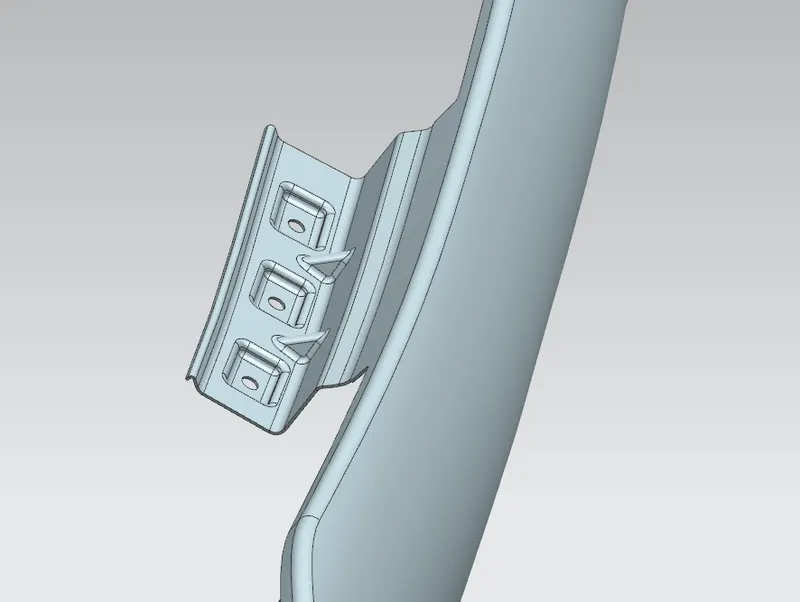
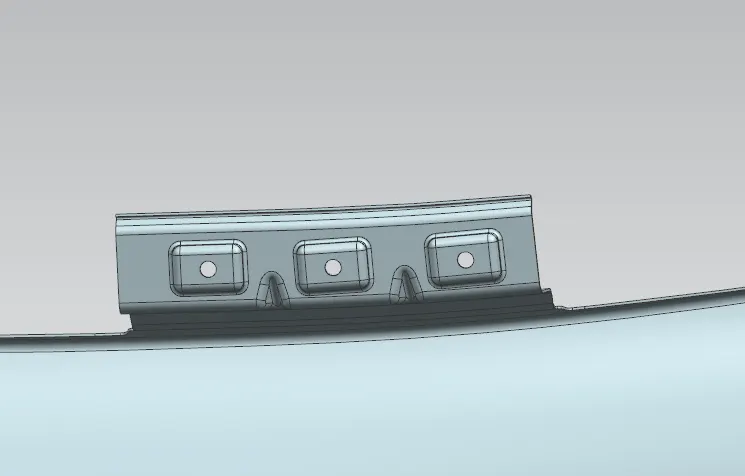
Darts are provided at the bends to stiffen the sheet metal at that region.
A-Pillar Mounting Area
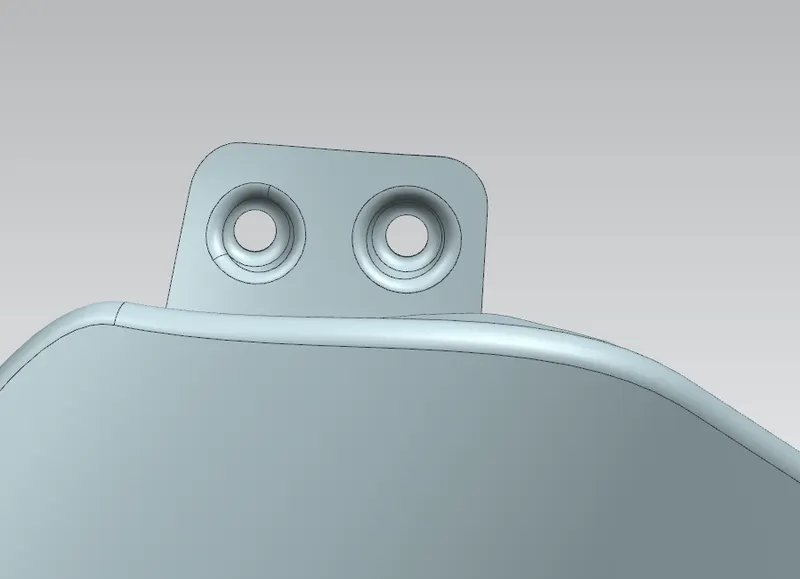
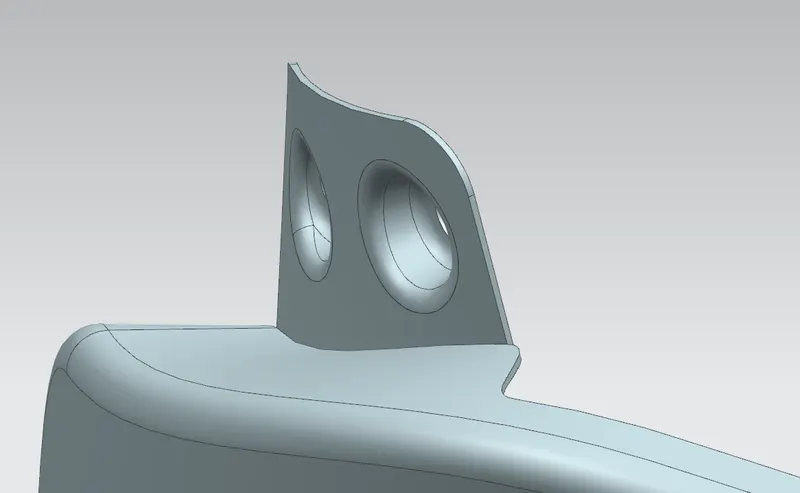
This Mounting region is located near the cowl of the vehicle where the fender is fastened with the bottom edge of the windshield. This mounting is covered with the side rear-view mirror.
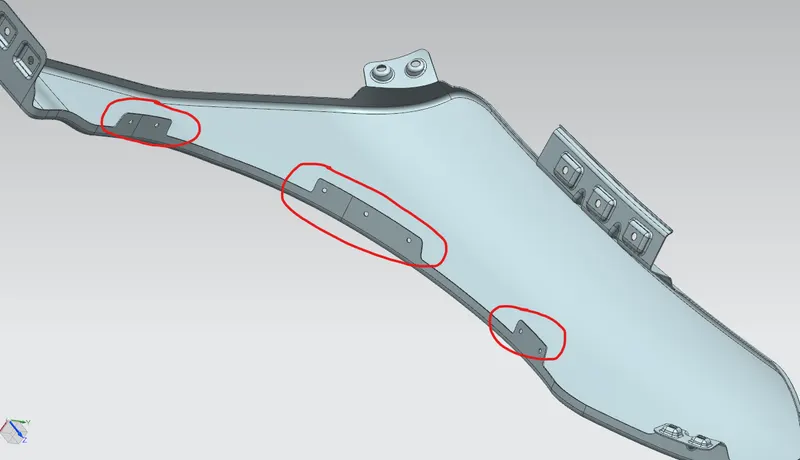
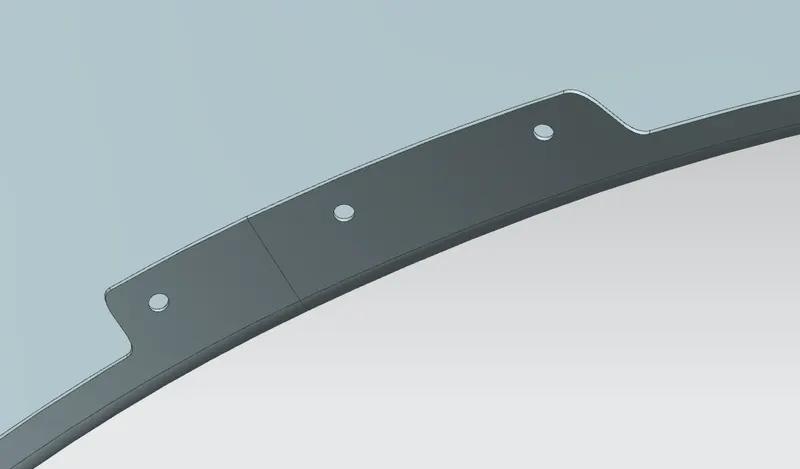
Baffle Mounting Area
In this region, the baffle gets installed to the fender with the help of clips which holds the baffle with the fender along the wheel arch.
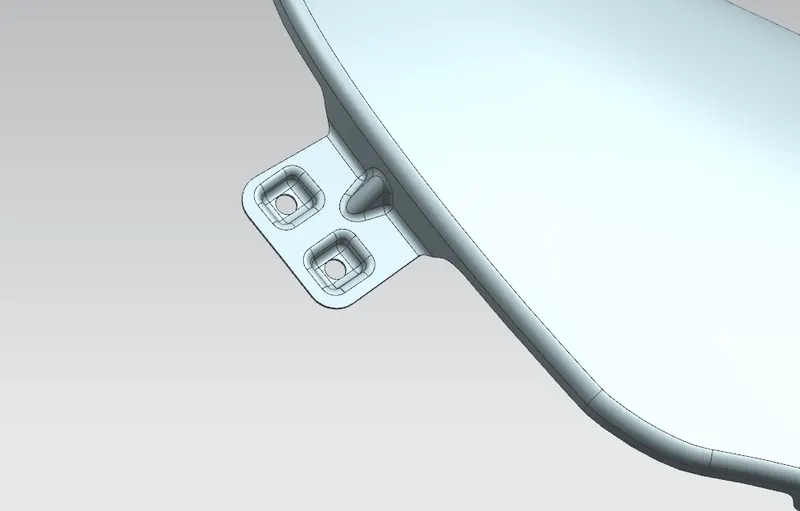
Bumper Mounting Area
The bumper mounting region is located beneath the bumper. The fender gets attached before the installation of the bumper. After fixing the fender with fasteners the bumper will cover the bumper mounting.
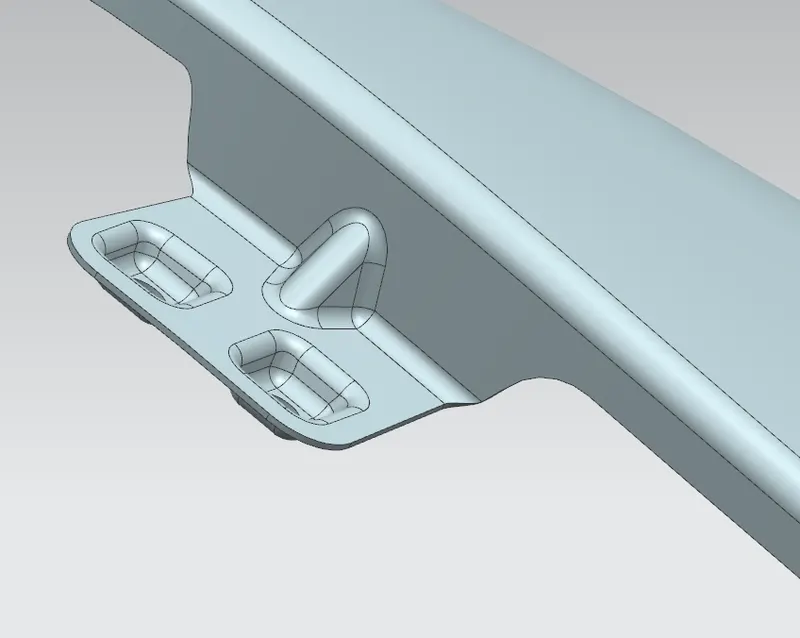
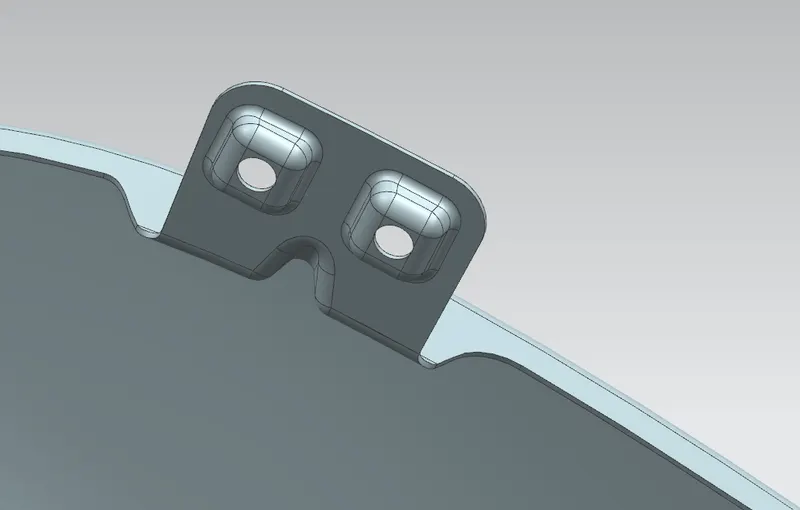
Sill Mounting Area
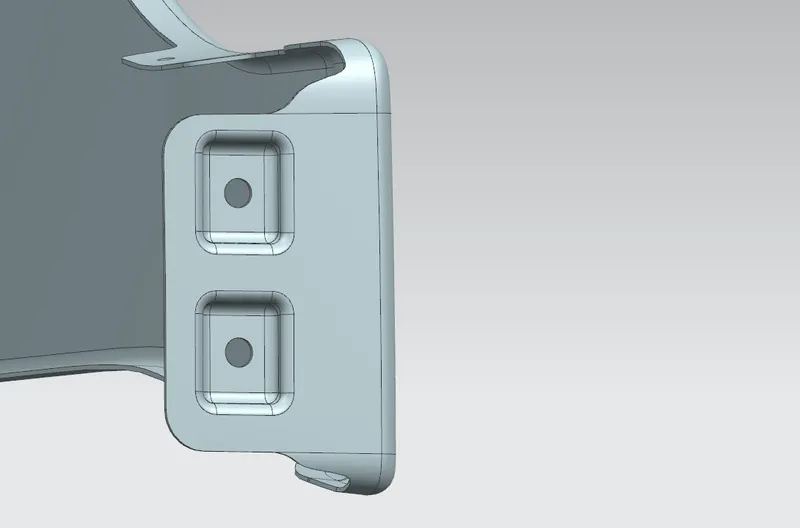
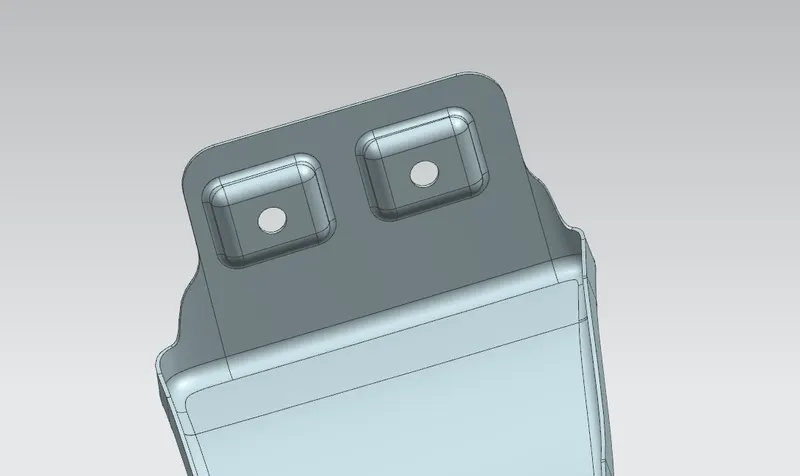
The area at which the bottom of the fender gets connected to the floor near the bottom edge of the door. The Embossed sill mounting of the fender is attached with the fasteners.
APPLYING OF THICKNESS TO THE SURFACE .
The thickness of 0.75 mm inward on the final sewed surface of the fender to the sheet metal parameters
DIFFERENT VIEW'S of a Fender
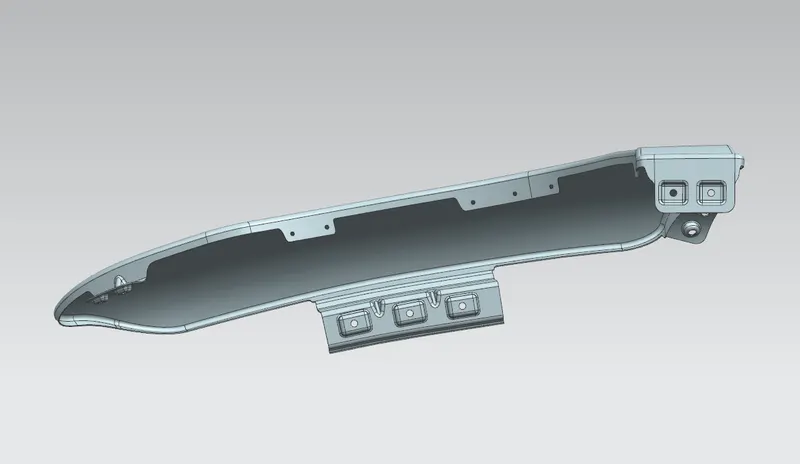
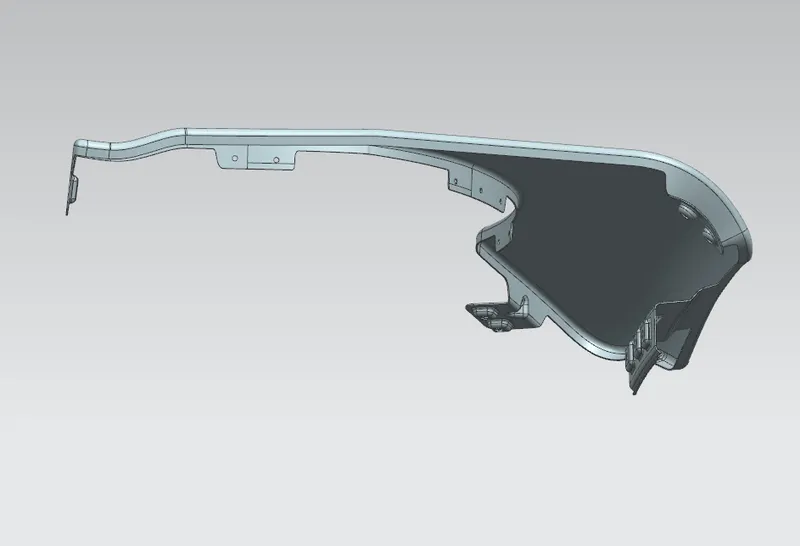
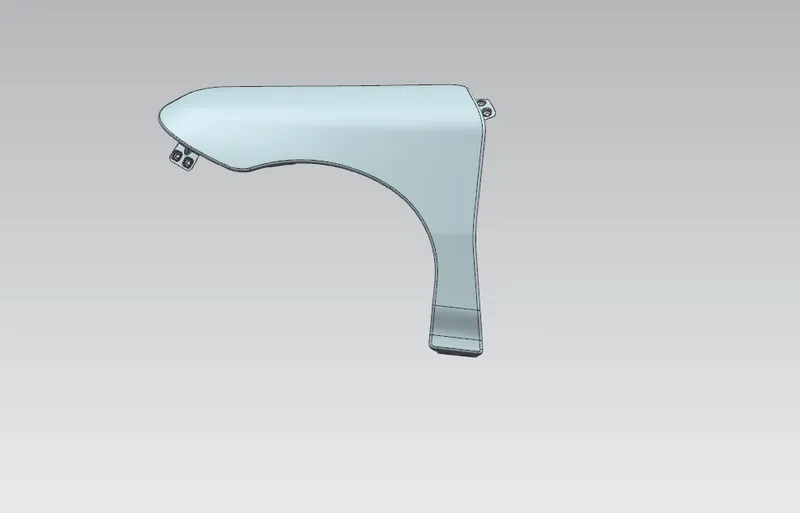
GENERAL NOTE: The PART and STP file is zipped and uploaded
Conclusion:
designed the Front Fender in NX application with proper mountings by using the Master Sketch and Design Parameters.