Design of backdoor
AIM: To design Backdoor of a Car using given class 'A' surface in NX-Cad.
Objective - The objective of the project is to use the given stylling surface to comeup with a backdoor design and use apppropriate methodology and also provide necessary reinforcements and embosses.
BACK DOOR
Introduction:
Back door is also called as tailgate. Backdoor is a hinged part which is used for entry and exit of the vehicles. Backdoor are one of the type of door of the vehicle which are located next to the passanger seat which provides access to the luggage compartment. In the most of the cars, these back door are operated with the help of gas stay which in turn reduces the effort required to lift the door. Few cars have electric motor to lift the back door when a switch is pressed. It is the rearmost part of the car and has mounts for tail lamp, hinges, wiper motor, gas stay etc. Back door is made up of 1 inner panel and 2 or 3 outer panels joined together by hemming and spot welding process.
Material used for the back door is chosen with various parameters like cost, strength required, weight, time taken to manufacture and so on. Steel is used in most of the cars as it is cheaper, these are stamped using molds and these parts will be uniform in thickness. Reinforcements are added to increase the strength locally.
Types of Back door
- Top mounted
- Side mounted
- Bottom mounted
Top Mounted:
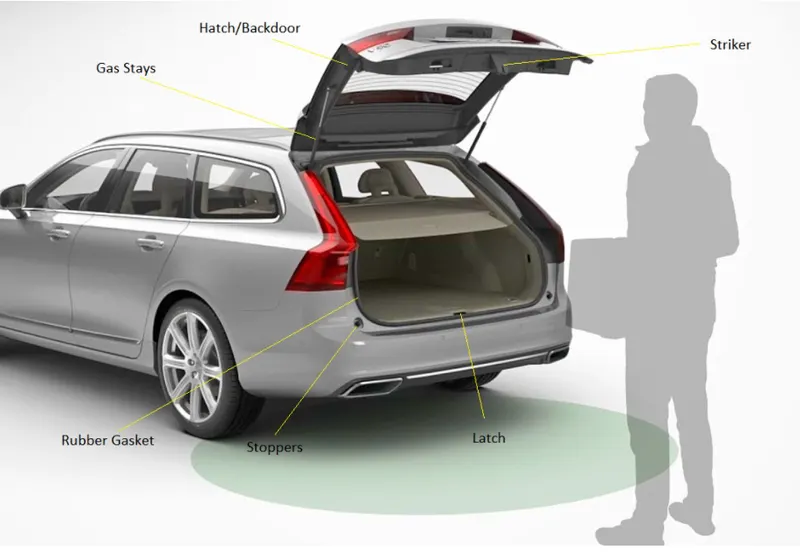
Pick up trucks, station wagon and sports utility vehicles use this type of back door. These are both gas stay supported and motor powered. Advantage of this type of back door is it provides greater rear visibility compared to others.
Side mounted:
Side mounted doors are mounted on the side of the car. Vans, SUVs, MPVs, Trucks use this type of back door. Accidental head impacts can be avoided with this type. It is easier to load and unload items using this door.
Bottom Mounted:
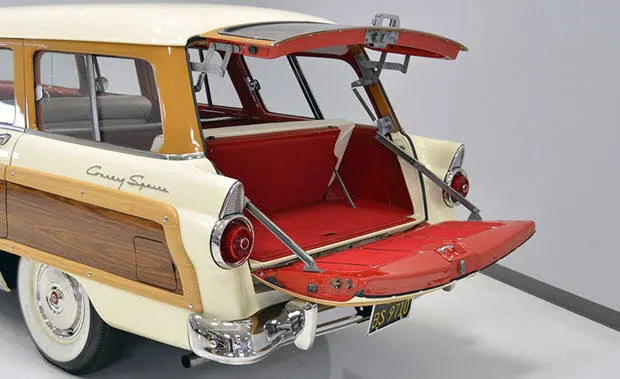
Bottom mount doors are used in estate type cars, pickup trucks and some luxury SUVs. This is the most comfortable type of back door, it can be also used as supporting table or holding long items.
Based on Working mechanism
- Gas stay type
- Powered lift type
Gas stay type:
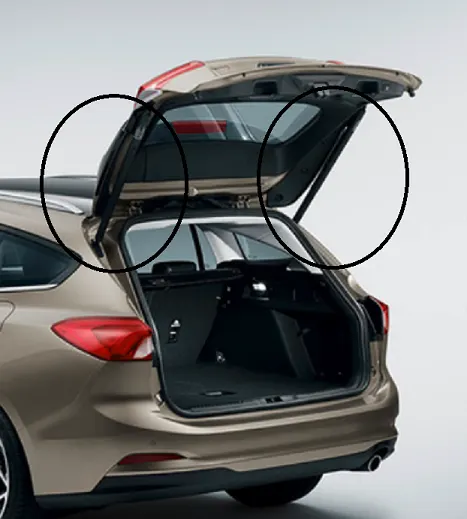
Gas stay type is the most common type used in cars for operating the back door. Components of back door are gas stay, hinge, wiper mechanism, rear light and rubber beadings for sealing of door.
Powered lift type:
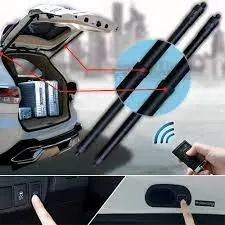
Powered lift type is also known as electric motor actuated type. It is mostly used in luxury cars. As it is the sophisticated type of operating the back door. A switch is pressed to open or close the door. This consists of power latch, anti pinch switch, PTF assembly.
Manufacturing Process:
Backdoor undergoes numerous manufacturing process, like bending, stamping, punching, deep drawing, hemming, embossing, spot welding and even more. But the main moto is to reduce the lead time, cost and increase the productivity.
Bending:
In bending the sheet metal is bent to a defined curvature. Here simple curve surfaces are produced and this becomes the base surface of the component. A Die and Press arrangement applies pressure on the sheet metal which changes the curvature of the blank permanently. And applying of pressure must be careful that the metal should not spring back to its original shape.
Deep Drawing:
Next after the bending process drawing operation is done here Complex curvature can be produced. the die and the mould create the desired shape which we predefined for the blank the pressure is applied hydraulically or mechanically that forces the punch to the die and forms the shape in the sheet metal. Negative draft angle is avoided because it cannot be manufactured.
One of the drawing process is Deep drawing deep drawing is a forming operation the is a combination of tensile and compression.
Stamping:
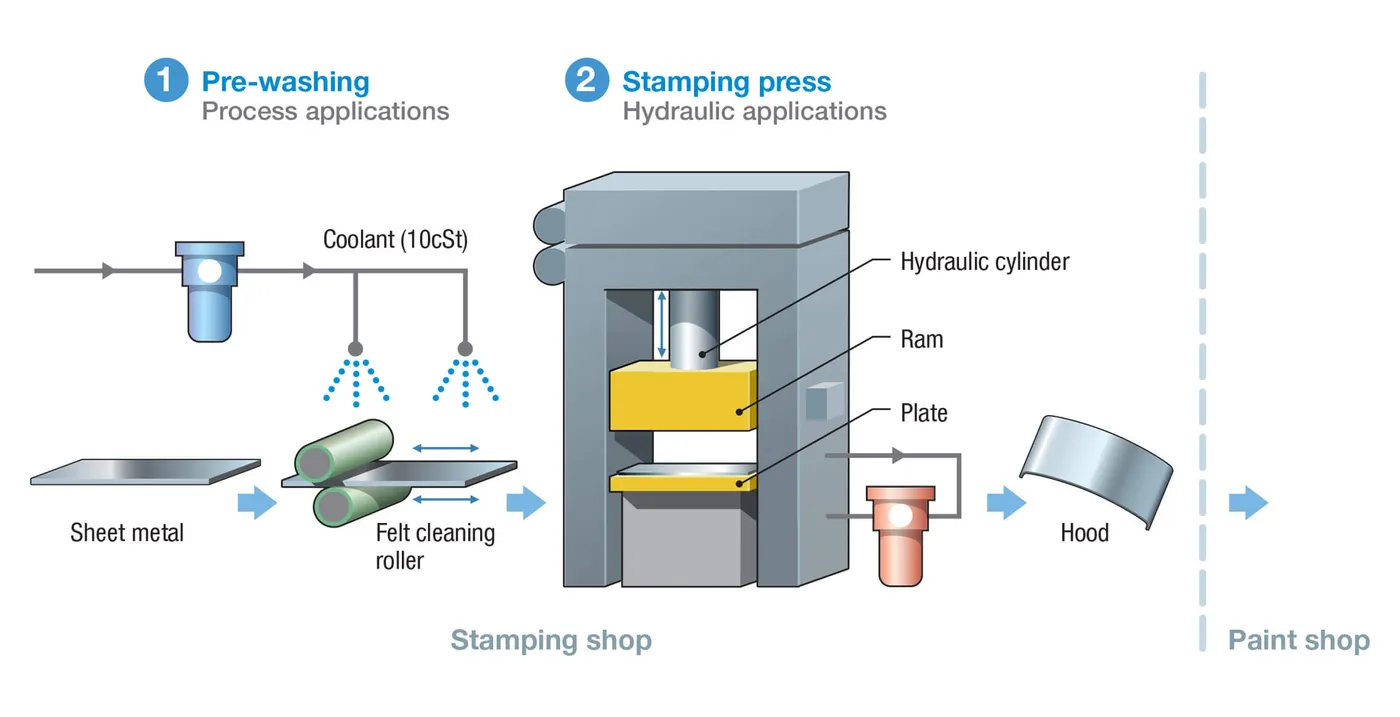
Stamping is done with the help of Stamping press machines share a series of dies or a single die with various cuts or formed on the metal.
Embossing:
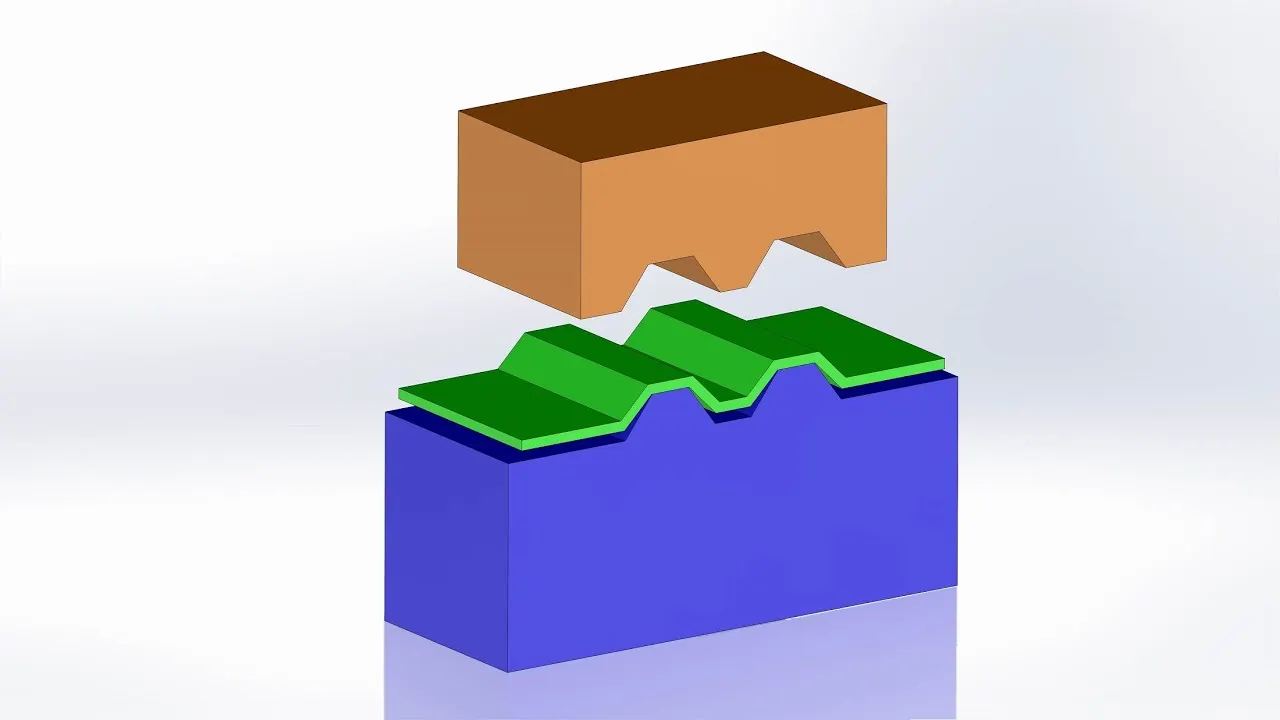
Embossing is a metal forming process for producing raised designs in sheet materials with the help of dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. Metal sheet is drawn through the male and female dies producing a pattern or design on the metal sheet. Depending on the dies used, different patterns can be produced on the metal sheet.
Lancing:
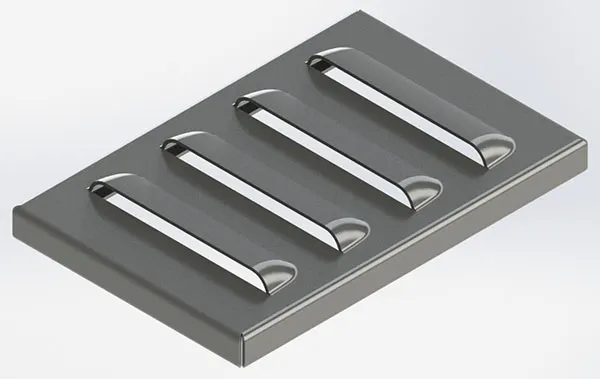
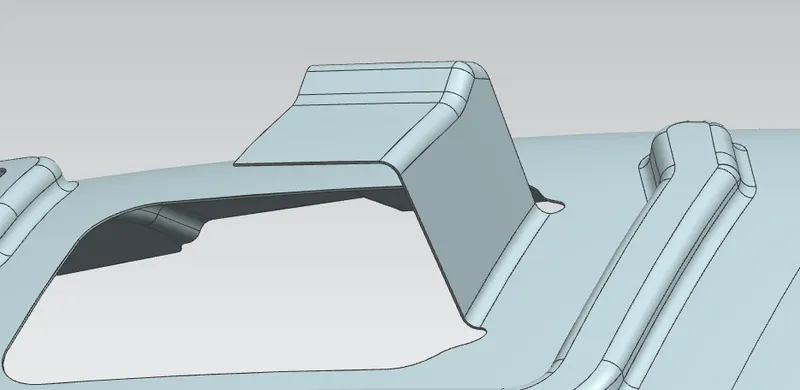
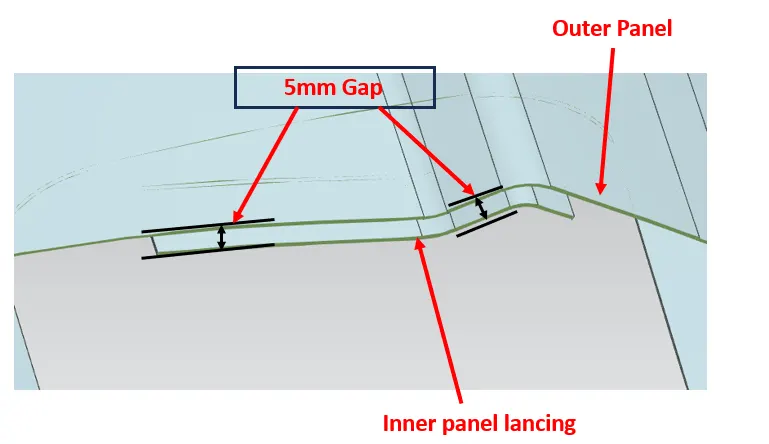
Lancing is a process in the sheet metal where the metal is cut to a sheet of metal through part of its length and then bending the cut portion. No material is removed in the lancing process. It is used to make tabs, vants, louvers in sheet metal workpiece. Here in back door inner panel we use this operation.
Reducing weight of the car is more important as it is a major red flag in cost and performance. So there will be a search for material lighter than steel. But most at times it will be costlier and can be used only in the luxury section of cars. Most automobiles use steel as it is not costlier. ULSAB - Ultra light steel auto body is used to reduce the steel weight, tailor welded blank and hydro-forming techniques are used in ULSAB.
Tailor Welded blank:
Two separate pieces of sheet metal can be welded together with tailor welded blank operation. It allows to join sheet metals at different grades, thickness and corrosive coating for giving specified properties in different areas. They also allow a high degree of flexibility in designing parts and large blanks can be formed from much smaller sheets. Weight can be decreased by using this method.
Hemming:
Hemming is a type of forming operation in manufacturing components. Here the edges of the sheetmetal are folded on the other part achieving tight fit. This joins the both parts without affecting the appearance and hence it is used in hood, doors, fenders, tailgates etc,. In tailgate it is used to join the inner and Outer panel of the tail gate.
There are various types of hemming operations
- Conventional Dai Hemming
- Roll Hemming
Conventional Dai Hemming:
This is used for mass productions. Here a hemming tool is used to fold the entire length of the sheet metal. Depending on the opening angle that will be several steps of the Hemming process. But this is an expensive process and it is restricted to flat and complicated profiles cannot be made in hemming.
Roll Hemming:
The name says rollers are used in the hamming process and industrial robots are used to get the rollers over the part to fold over the other part and hemming is done. Comparing to the conventional die hemming the tool cost are significantly low the old hemming but the cycle time is higher the roll hemming
Spot Weld:
Spot welding is a type of electric resistance welding. It is also known as resistance spot welding. The process of spot welding is sheet metals are made into contact with each other and pressure is applied on specified points. So heat is generated from the resistance and weld is formed.
Design Consideration for Backdoor/Tailgate:
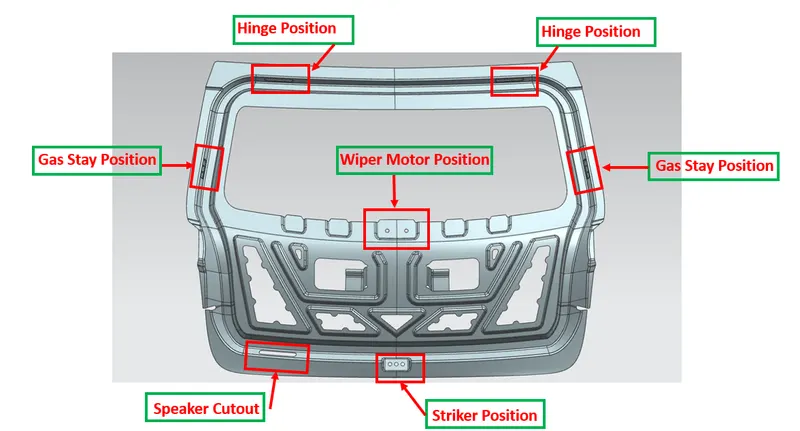
- Visibility Criteria
- Latch and Stricker Position
- Hing Position
- Gas Stay Position
- Space Avalibility
- Drain Holes
- Hemming and Relief area's
- Draft Analysis
- Gap and Flush Requirements
Door parts thickness is given below:
- Outer Panel - 0.75 mm
- Inner Panel - 0.75 mm
- Reinforcements - 0.75 mm
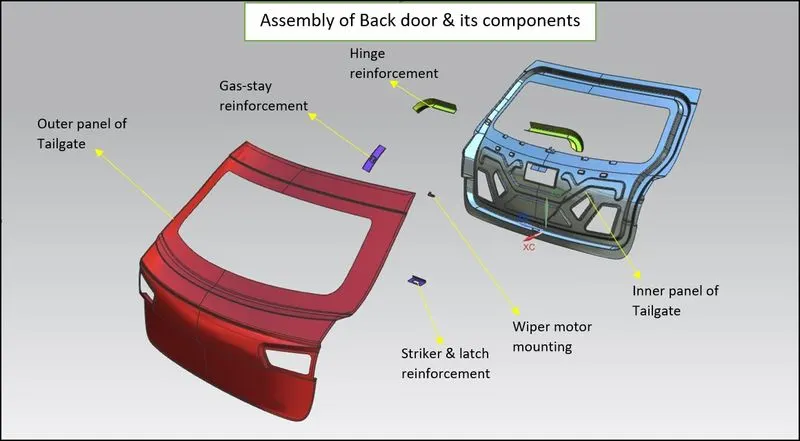
Back Door Assembly Components:
- Outer Panel
- Inner Panel
- Hinge Reinforcement.
- Gas Stay Reinforcement.
- Wiper Motor Reinforcement
- Striker Reinforcement
Given Input Data
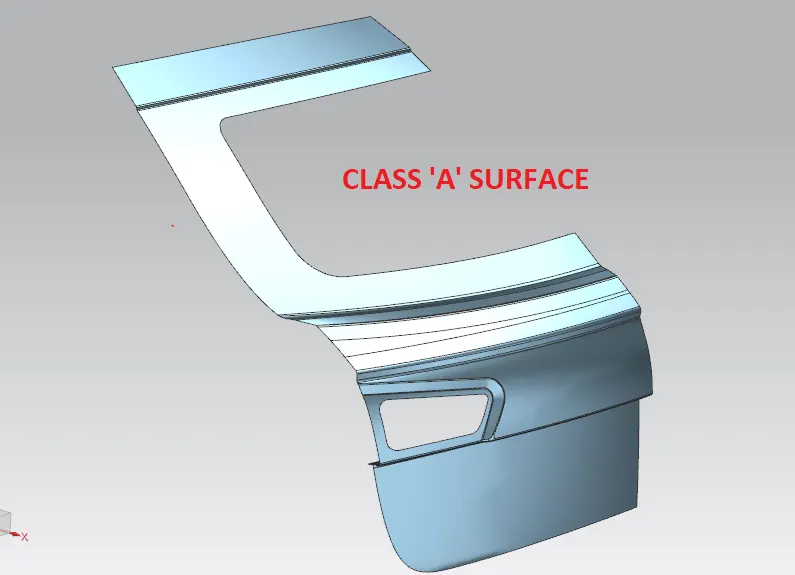
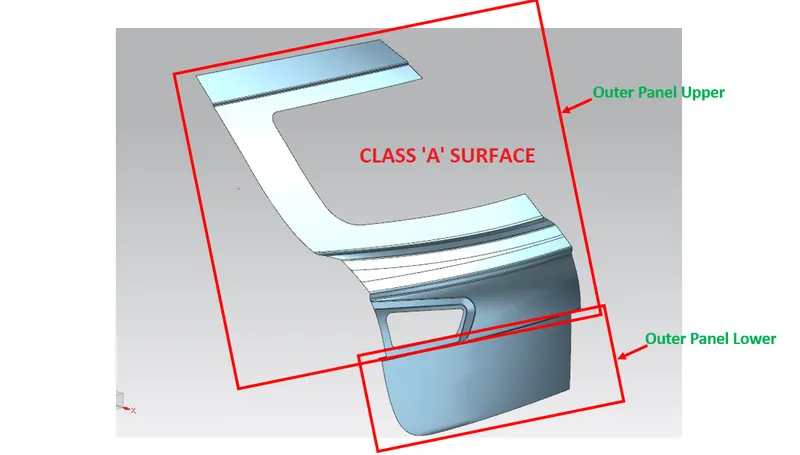
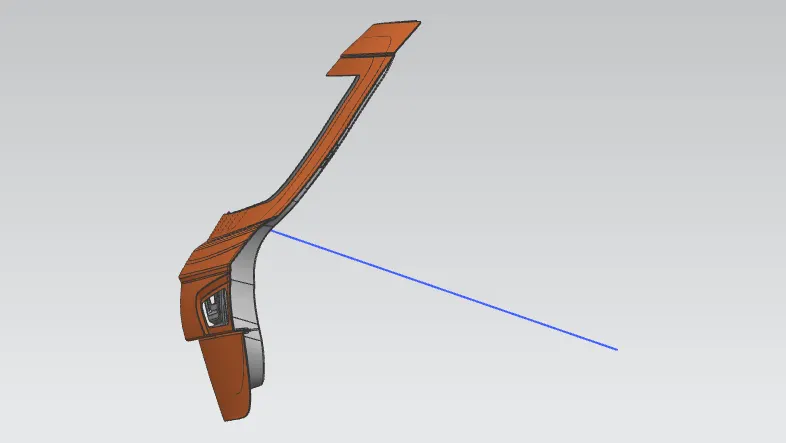
Outer panel upper and lower
Outer Panel Upper and lower:
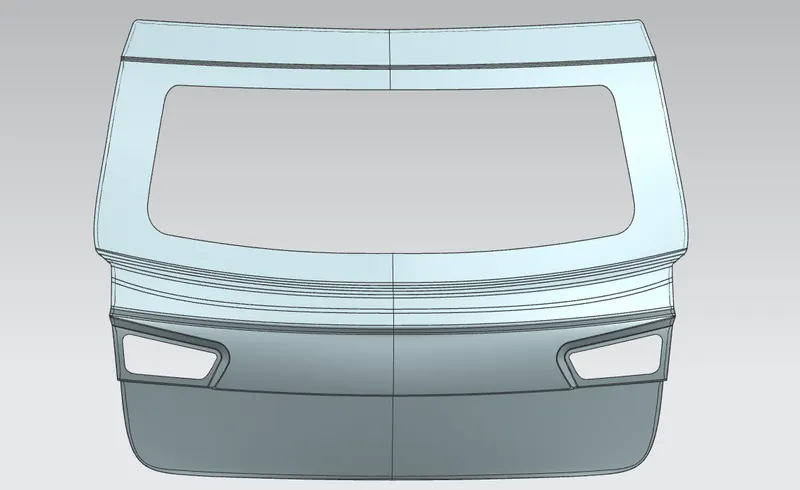
Outer panel is the asthetic part of the tail gate. It will be attractive in look. coatings are given to keep it scratch and rust resistant. The outer panel also has the provisions for the tail lamp, rear fog lamp and also has the provision for licence plate mountings. Most of the hatchback cars have the provision for wiper motor. Thickness is given 0.75mm in the above model towrards the inner panel. Hemming is done to join the inner and outer panel.
Inner Panel:
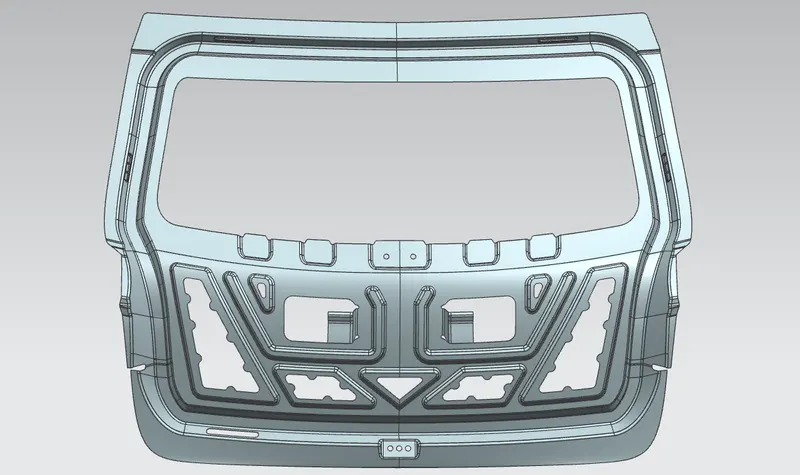
Back door inner panel has the mountings for hinges, gas stay, wiper motor, mastic area, striker and so on. The block is stamped as single part. This reduces the cost and number of tools needed to manufacture. This is the strengthening element of the back door. Inner panel is hemmed with outerpanel finally. Aluminium or steel will be used for manufacturing the tail gate inner panel. reinforcements are added whereever needed. Thickness is given 0.75mm in the above model towrards the outer panel. Flages like Connecting flange, sealing flange and inner panel flange will be present in the the inner panel.
Hinge Reinforcement:
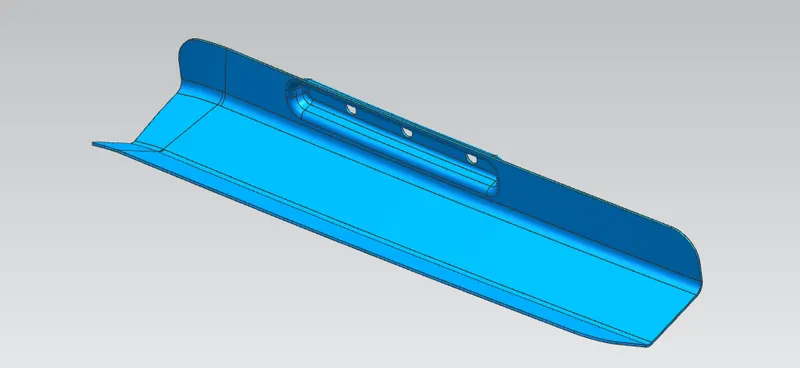
Hinges are used to opening and clsoing of the back door. Both halves of hinge on back door and roof combines to operate the door. Reinforcement is given to compensate the load acting on the region. Thickness is given 1.5mm in the above model towrards the outer panel.

Gas Stay Reinforcement:
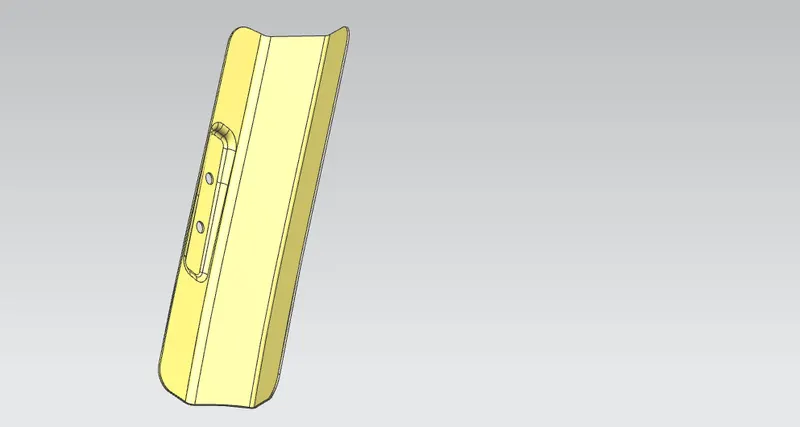
Gas stay in a tail gate is used hold open and close the tail gate. It eliminates man power by holding the back door open in position. one end of the gas stay is fixed on the door and other on the body side.
Wiper Motor Reinforcement:
Wiper motor is placed in the back door area under the glass mounting portion. It comprises of small motor and modlues that actuates the wiper. reinforcement is given to strengthen the part locally. here the thickness is given 1.5mm.
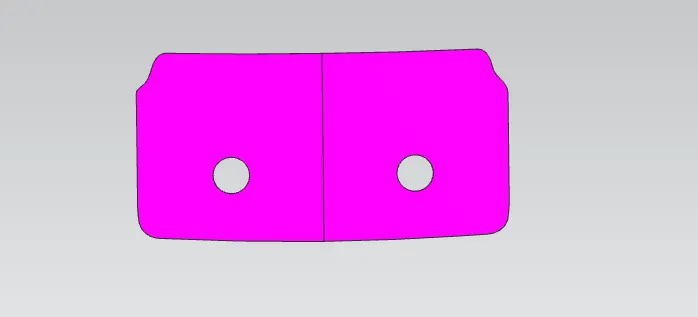
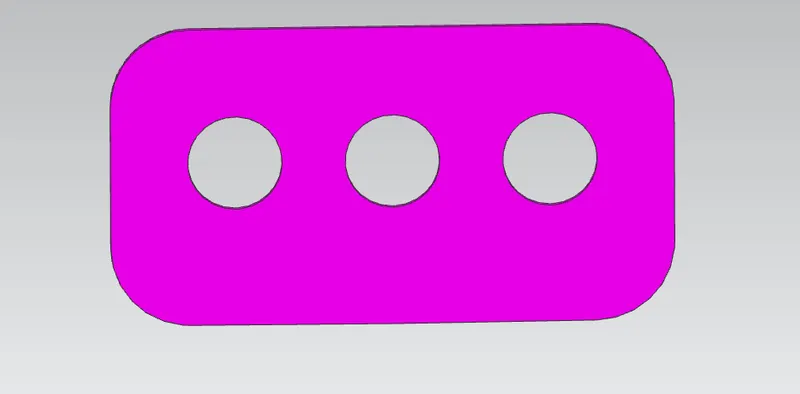
Striker Reinforcement:
Latch and striker is responsible for locking of the back door. Stress will be developed as we frequently open and close the door so adding a reinforcement will make it stronger.
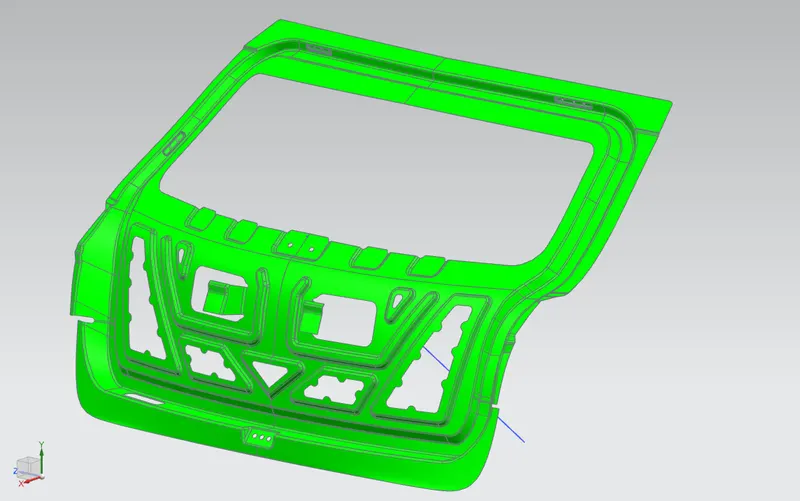
Draft Analysis:
Here are the parts that are made as per the master section and also clearing the draft analysis. Draft analysis is done in NX software. We can change the draft angle and analyze is it clearing the required criteria. It is shown is different color zones. So identifying it will be easier. It will let us know that the part can be removed easily during manufacturing or not. Minimum draft angle of 7 Degree is considered for analysis. green color infer on the parts that all face along the tooling direction has positive draft angle greater than 7 degree and passed in analysis.
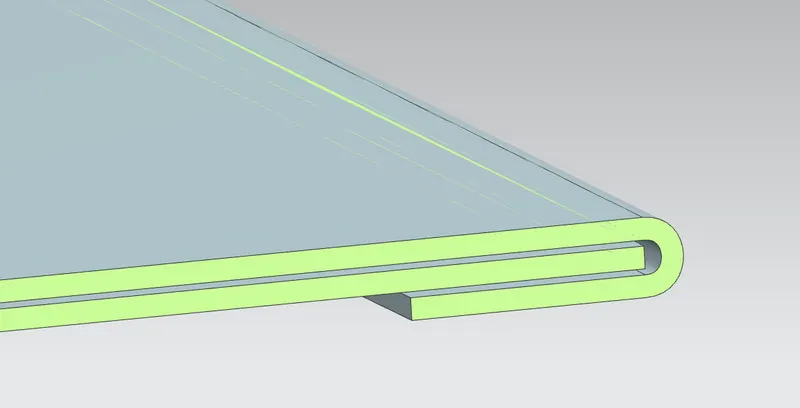
Hemming:
Hemming is a sheet metal forming process in which sheets are joined by bending it usually to 180°. Here we have used it to join the inner and outer panel of the back door. Thickness of sheet is 0.75mm and clearance between sheet is 0.2mm to provide sealant in it.
Hemming Relief:
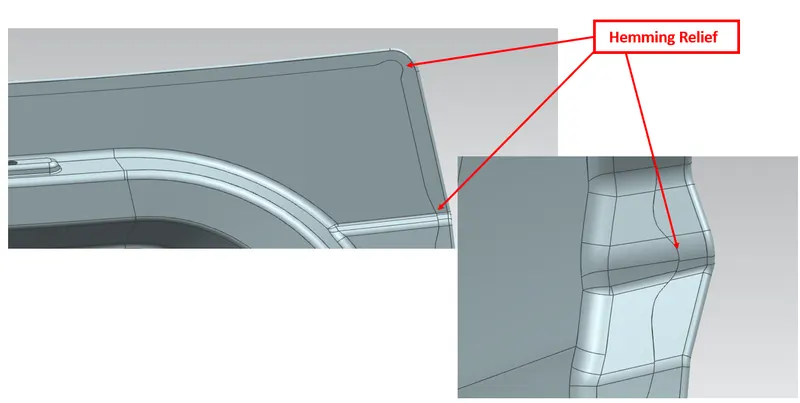
While we do hemming we give corner relief at the turns of the part because during manufacturing rolls cannot travel at the corner and it may create wrinkles while hemming at the corner. so we give a curvature for avoiding those problem.
Lancing:
As given below about the lancing process. Here we use in the inner panel of the door. It is done to join the outer and inner panel with the help of mastic sealants.
Positioning latch:
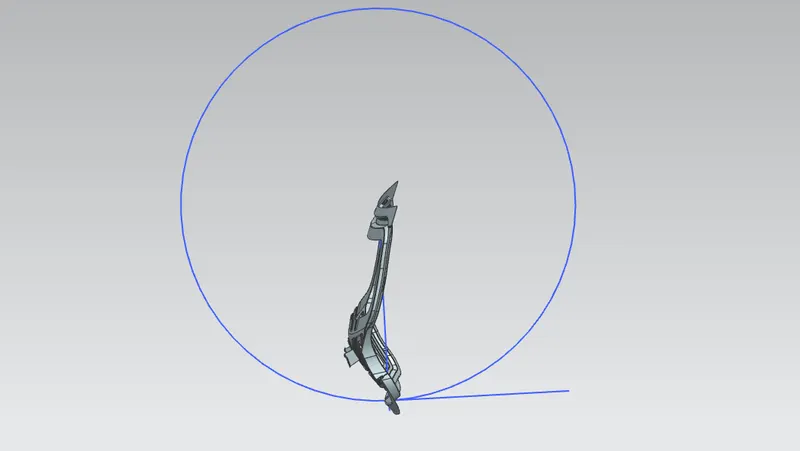
Latch and striker should be perpendicular to the hinge so only it will open and close properly. So i have made this trajectory to position the striker emboss.
Backdoor Assembly:
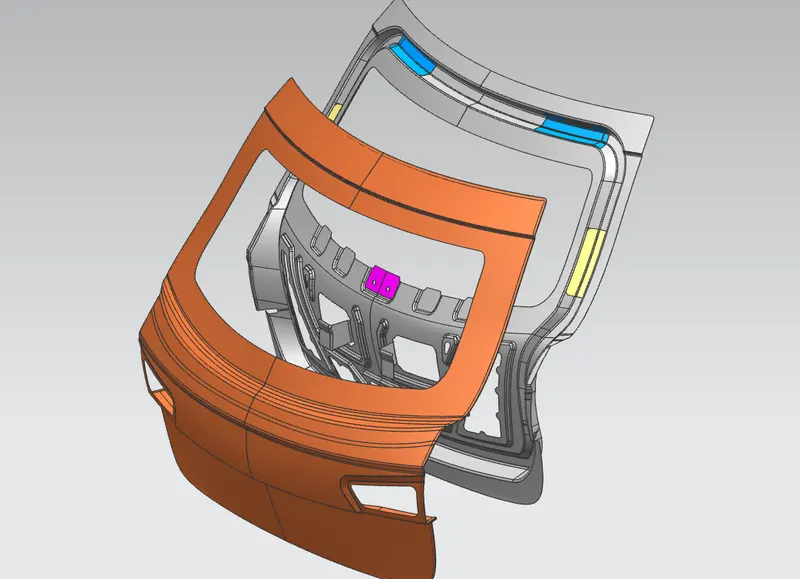
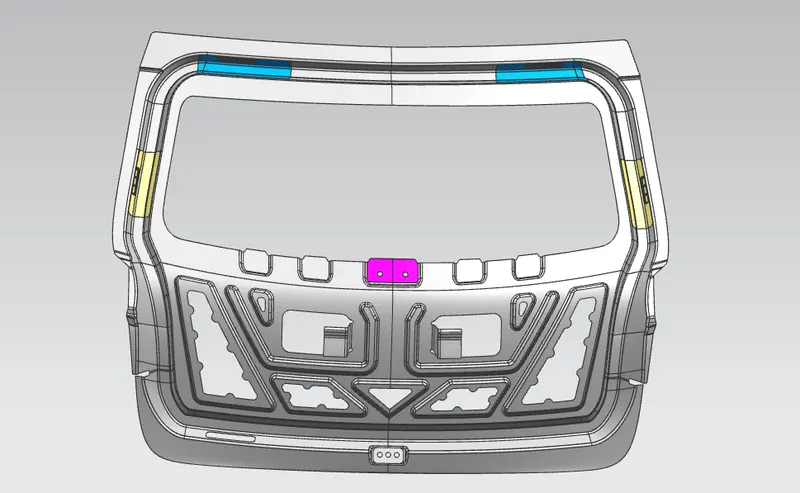
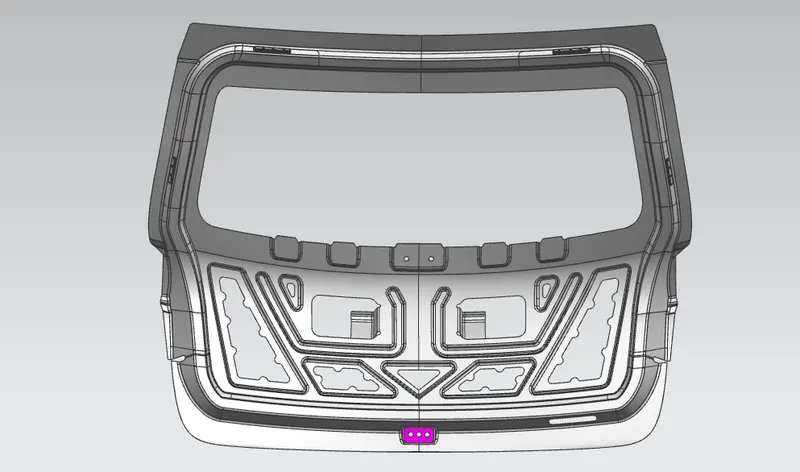
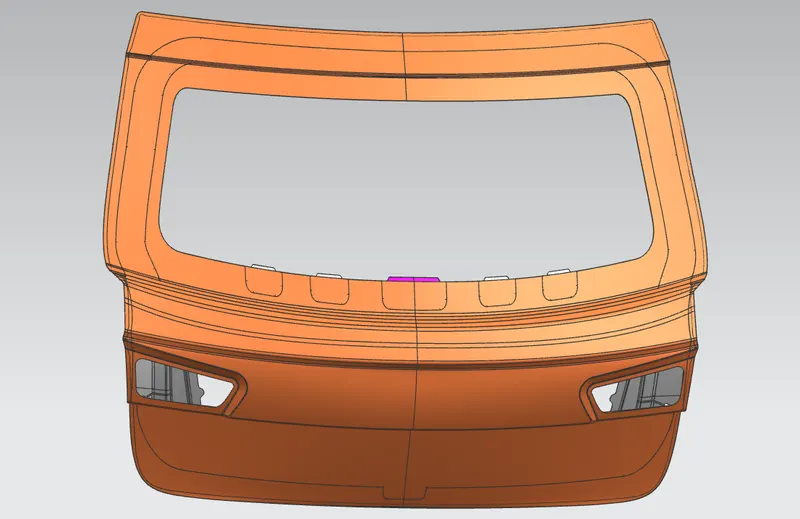
CONCLUSION:
Here, we have designed the back door by the given styling surface of a back door design, I have used appropriate design methodologies and provided the necessary reinforcements and embosses for the BackDoor design.