Design of backdoor
Design of Backdoor
What is back door of a car?
A door which is located at the rear side of a car which gives access for the boot space to store luggage, spare wheel etc.
These doors can be operated manually or electric powered. In most of the luxury cars door is electrically operated.
Functions of the Backdoor:-
- It protects the occupants and luggage from getting damaged.
- It houses assembly of tail lamps, wiper motor and other components.
- It serves as entry and exit point for luggage/passengers.
- It houses windshield glass which helps in rear visibility.
- Parking sensors, rear view camera are mounted on it.
Types of doors based on working position,
- Top Mounted Door
- Side mounted Door
- Bottom Door
Top Mpunted Door:-
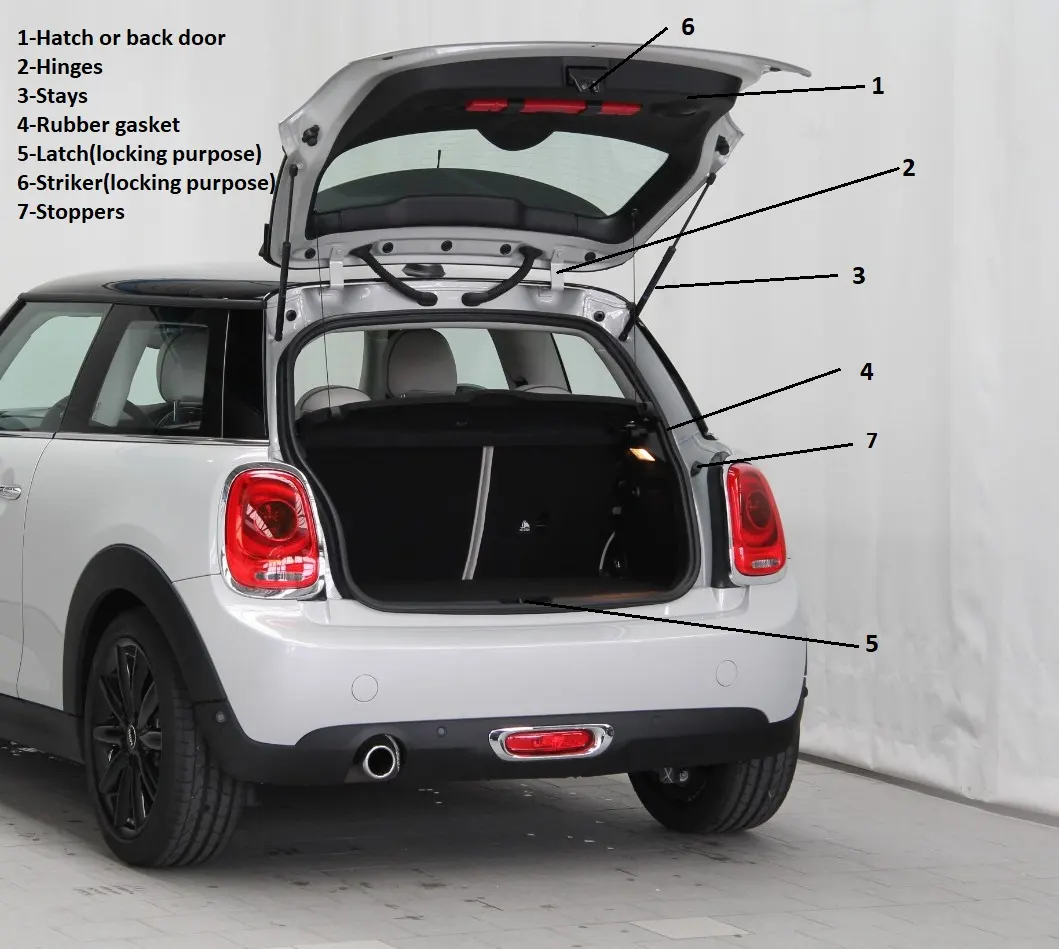
These type of back doors are used in a station wagon, pickup truck and some other sports utility vehicles. Today’s modern cars use top mounted tailgating systems which are both powered and also gas stay supported. These tailgates provide greater rear visibility compared to other types.
Side Mounted Door:-
It is generally used in van type MPVs, SUVs, pickup truck vehicles. These side mounted door/barn doors are a lot easier compared to top mounted ones. These doors are generally small in size and can be easily accessed. These doors are more convenient for the goods handlers carrying lengthy objects, long pipes where one door is kept open. It also saves accidental head impacts. It is a lot easier to load /unload things in vehicles having side-mounted doors.
Bottom Mounted:-
Bottom type or split type backdoor system is used in estate type cars, pickup trucks and some luxury SUVs. These are most convenient type of backdoor in which the bottom split is used as a support or even as a table for the touring people.
MANUFACTURING PROCESS :-
Conventional tailgate assemblies are made from stamped metal panels welded together to form a tailgate. Latches are added on either side of the tailgate to engage a striker on the pickup sides. A handle operates the latches to open and close the tailgate assembly. Steel tailgate assemblies provide a durable and secure closure for the pickup bed.
Another disadvantage of steel tailgate assemblies is the cost of the tooling required and equipment required to stamp metal tailgate components. Metal tailgate components are generally produced in a large stamping press. The stamping presses generally require finely machined tools made from hardened steel. The cost of tooling a metal tailgate is much more expensive.
MATERIAL FOR BODY PANELS :-
Materials for car body panels require certain specific characteristics to meet the industry’s challenges: rationalisation of specifications for leaner inventory, improved formability for reduced rejection rate and better quality. Higher Strength Low Alloy (HSLA) steels of thinner gauges, are getting preference for weight reduction and the resulting better fuel economy.Other quality characteristics under demand are higher yield stress (strength), toughness,fatigue strength, improved dent resistance as well as corrosion resistance in materials used for body panels for improved durability and reliability.
To obtain consistent quality of autobody skin panels without failures during stamping, the formability/ductility specifications of strip steels are the basic requirements.Most of the steels used in automotive application are aluminium-killed steels of about 0.7 to 0.9 mm thickness.
An intensive research and development are going on for alternate materials, manufacturing processes and stamping tools for sheet-metal components with the main objectives of cutting down the weight and unit cost of the vehicle. Simultaneously, the steel content of the car is falling with the use of aluminium and new materials, such as plastics. Aluminium may provide the most sought after solution to reduce the weight of the vehicles. A reduction of 30% in weight is achievable if the same strength, stiffness, and stability of the component are to be realised by substituting steel with aluminium. Possibility of significant reduction in die cost will be another advantage with aluminium. However, problems related to strength, serviceability,
manufacturability, and above all the cost, require effective solutions before the acceptance of aluminium as a substitute to steel for body panels. Plastics for bumpers,
STAMPING PROCESS :-
Stamping processes to be used for a panel depend on its design. However, normally the processes used extensively are blanking, drawing, piercing, forming, notching, trimming,hemming, etc. Blanking prepares the initial approximate form of the part in flat sheet. Drawing is generally the first operation to attain depth related form. Piercing, notching, hemming, are product design related operations. Trimming generally removes the extra material on the periphery of the panel provided for blankholding during draw operation. Decision on trim line is very important and becomes deciding factor to obtain good draw.
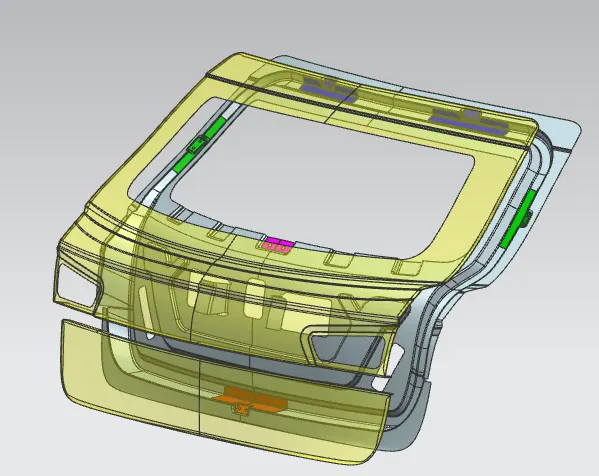
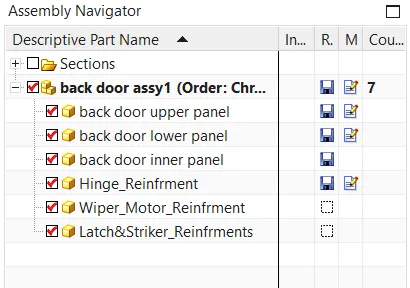
Back Door Assembly:-
- Inner panel
- outer panel
- hinge reinforcement
- wiper motor reinforcement
- latch & stricker and its reinforcement
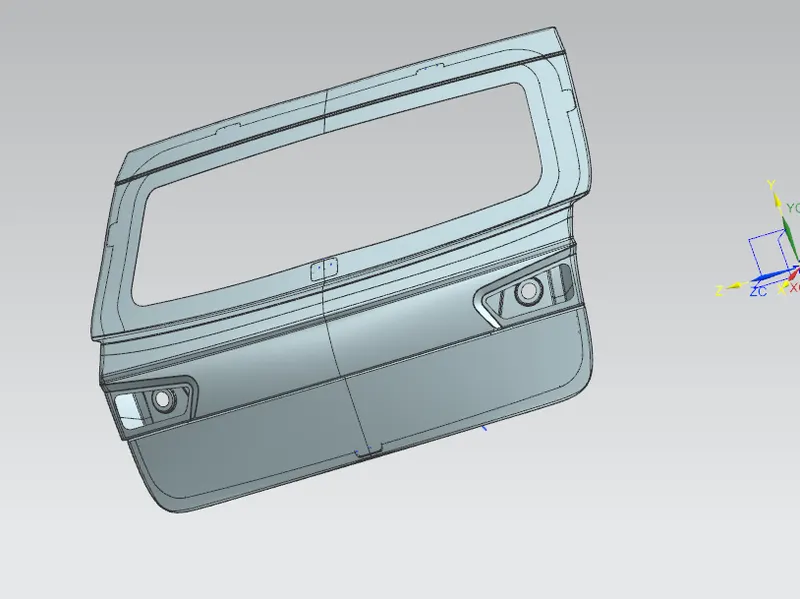
Outer panel:-
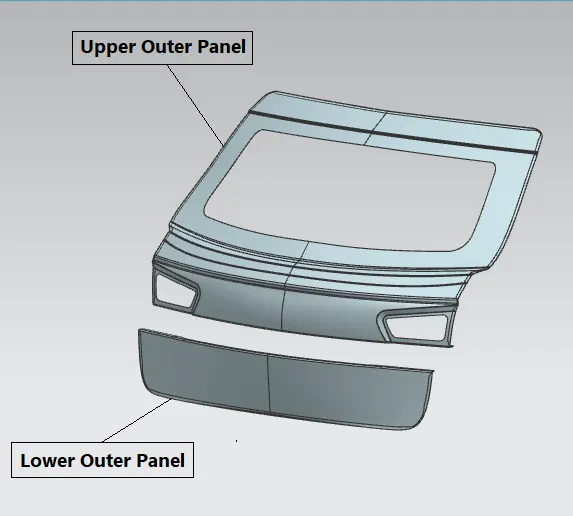
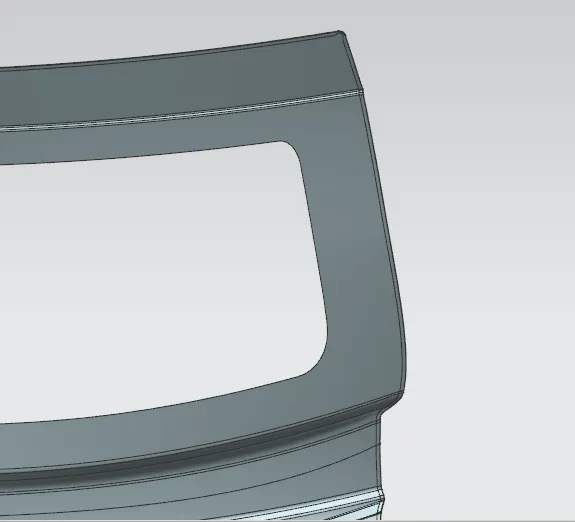
It is the outer styling skin surface of the back door. It is provided with multistage coatings which has property of scratch resistance, rust prevention etc. It is wrapped around the inner panel through hemming process.
Hemming:-
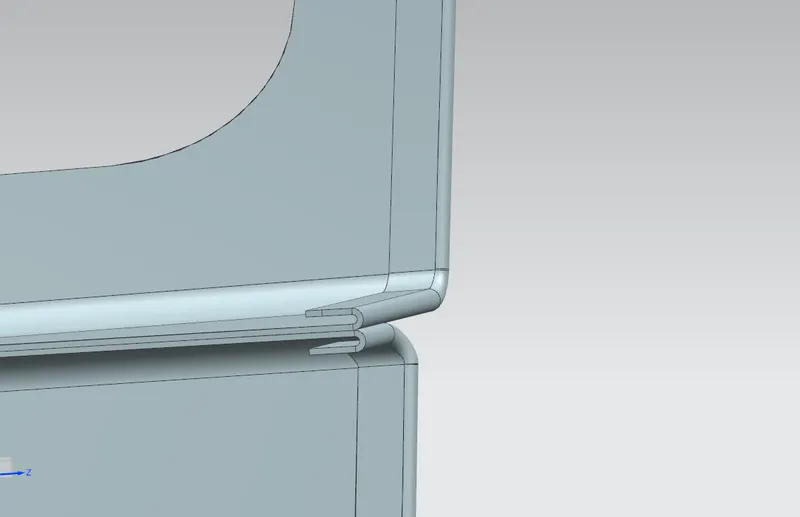
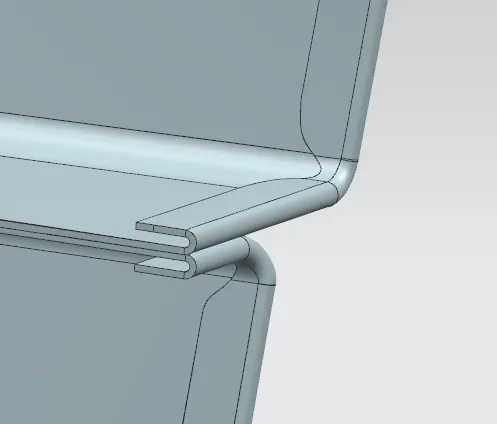
Hemming is a forming operation in which the edges of the sheet are folded over another part in order to achieve a tight fit. Usually hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges. In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
Corner Relief:-
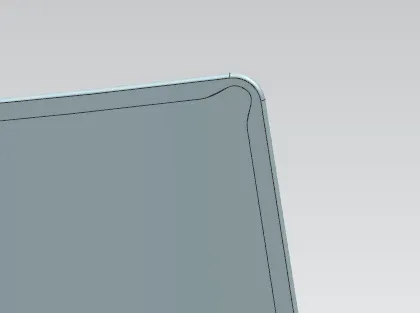
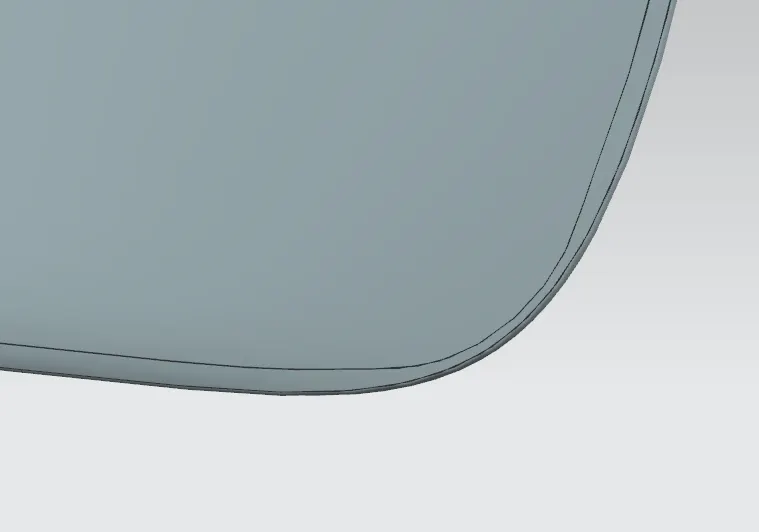
During hemming process multiple rollers are used which causes vibrations and stress concentrations at the some locations due to which design intent of the panel shouldn’t be changed (i.e the panel should spring back to original formation after roller is removed). But most of the time that is not the case at corners so to avoid that situtaion reliefs are provided at corners.
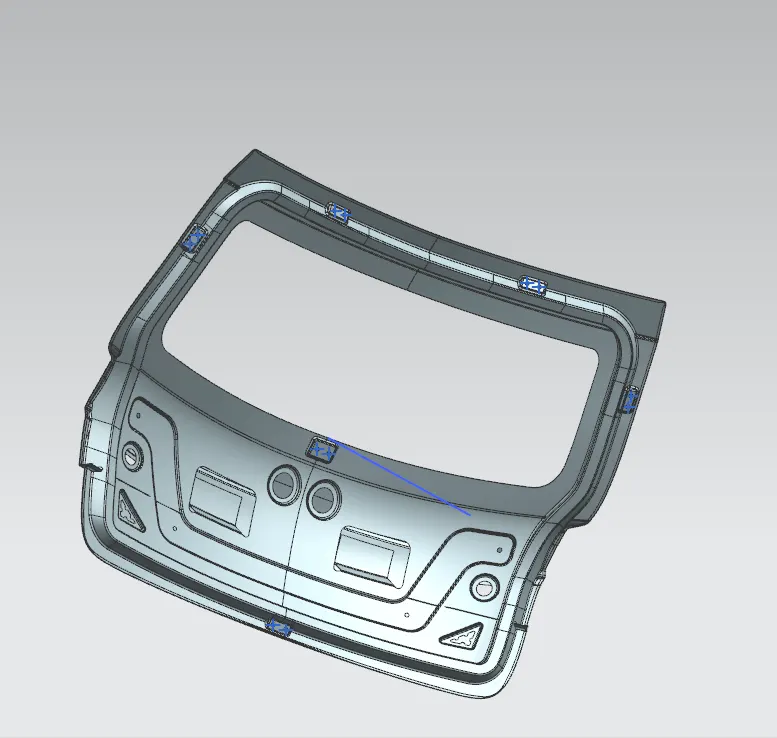
Inner Panel:-
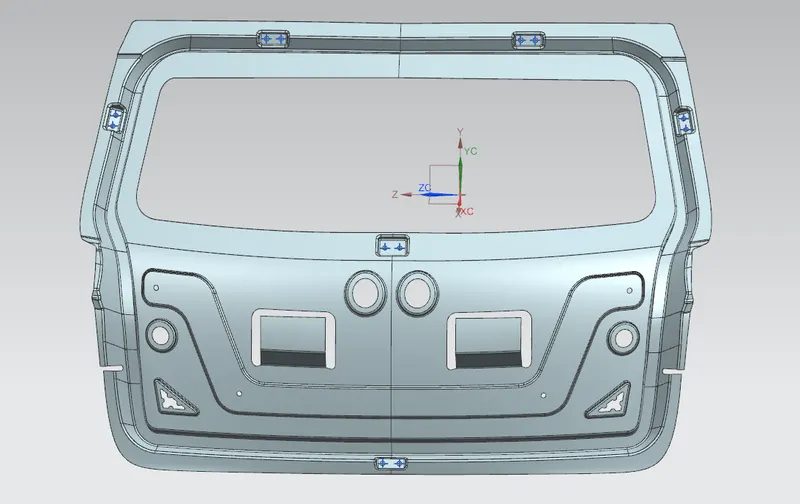
The inner panel is one of the most important components of backdoor assembly. It provides strength and helps in dissipation of forces outside the part with the help of embosses made on it. It helps in mounting of accessories like hinges, wiper motor, gas stay, latch & striker etc.
The inner panel is produced by either casting or through Deep drawing process.
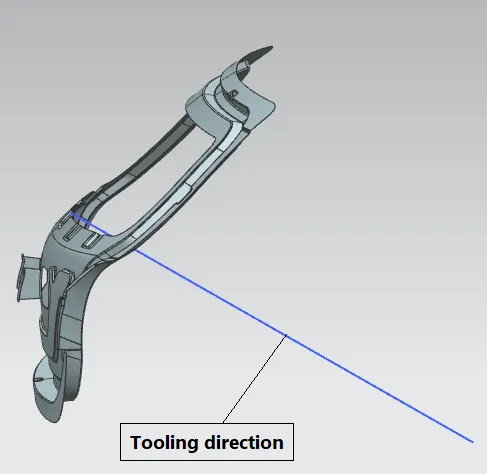
Mostly aluminum part is casted, steel inner panel are manufactured by deep drawing process. If deep drawn, there must be a tooling direction through which that panel must be deep drawn.
Sealing Flange:-
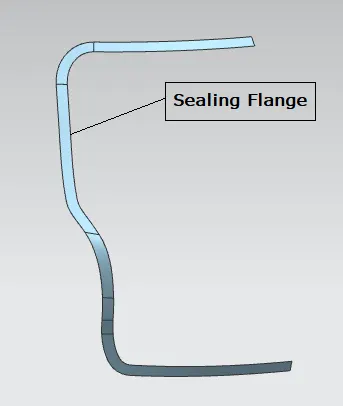
It is that section of the inner panel which enables the backdoor to sit over the rear body side of the car. Its design is important as it decides how a backdoor is mounted on the rear body side of the car and also restricts any external matter to enter inside the vehicle.
Reinforcements:-
Reinforcements are generally placed to increase the strength of the panel in localized areas which is relatively small compared to sheet metal parts for absorbing loads imposed thereon and dissipating such loads throughout the panel assembly to help maintain rigidity of the panel assembly. The reinforcements are usually 1-1.5mm thick as opposed to 0.75mm thick panel used in this part.
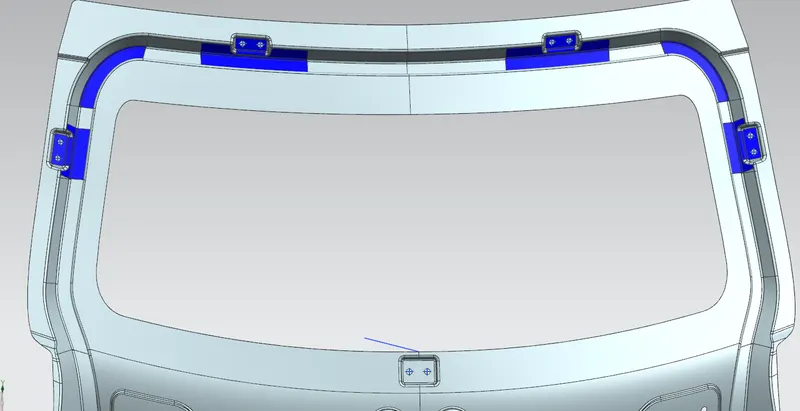
- Hinge reinforcements:-
Hinge is a pivot mechanism which supports the total weight of the backdoor. So reinforcements are added for strength and rigidity.
- Gas stay reinforcements:-
Gas stay is used to lift the backdoor automatically and is used to support the backdoor in its open position. It can be of Two types Semi-automated and fully automated.
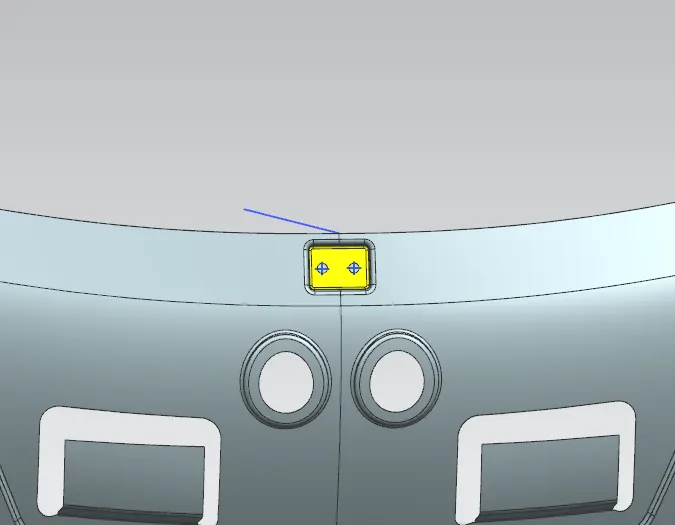
- Wiper Motor reinforcement:-
Wiper is used to wipeout the dust particles/water on the windshield glass which affects the rear visibility. It is actuated by the motor which is mounted on the inner panel. Due to vibration and heat of the motor, inner panel gets deformed which results in loss of strength & rigidity of the panel thus leading to poor NVH. So reinforcement is provided to avoid these conditions.
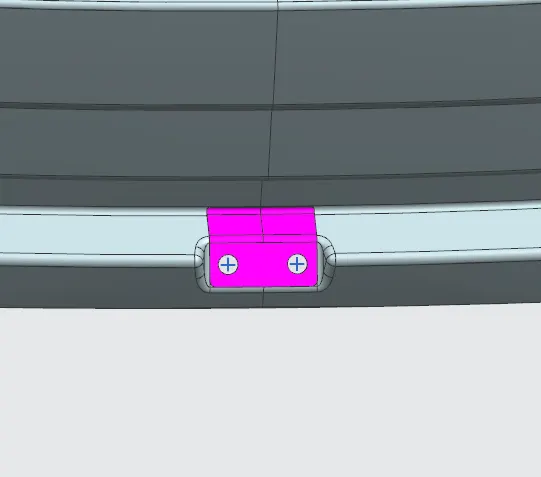
- Latch and Striker reinforcement:-
In the bottom part of the panel emboss is created for placemnet of latch and striker assembly. There is over slamming and abusing while opening and closing of the door, thus arising the need for reinforcement to be placed.
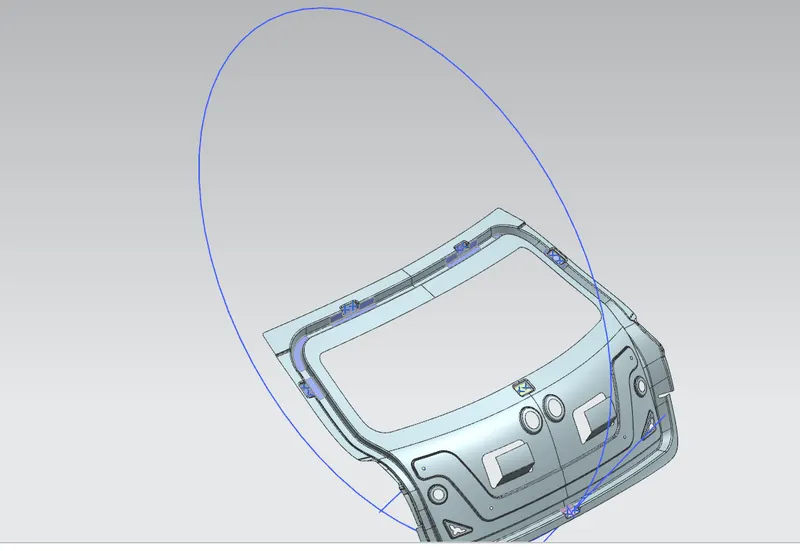
Positioning of Latch & striker/ Latch Trajectory:-
Backdoor is the swinging part which rotates about hinge axis. The position and orientation of latch striker is important for proper opening and closing of the backdoor. The positioning is done by sketching a circle with center as the axis of the hinge which passes through the striker at appropriate position with respect to inner panel.
Assembly:-
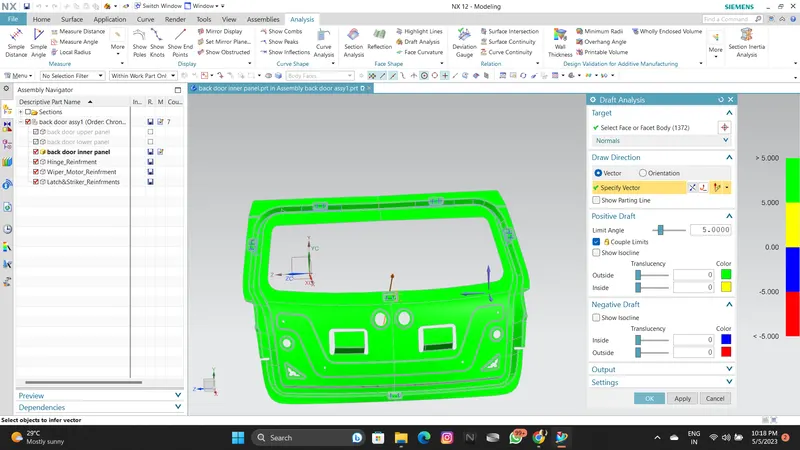
In this assembly Top down approach was followed wherein from given styling surface the inner panel was created using various tools/commands in NX. After that others parts were modelled as per the requirements one by one.
Analysis: Draft analysis:-
Every part which is manufactured from press tool or other forming tools require some positive draft on the faces which are parallel to the tooling direction. If we don’t give draft (Zero Draft) or give negative drafts on these faces it will stick to the mould surface and when the mould is in motion it will destroy surface thus reducing its surface finish. Thus Draft Analysis command enables us to detect if the part we have drafted can be easily ejected or not. It also give insights about the critical zones, so that appropriate changes in the design can be made if needed.