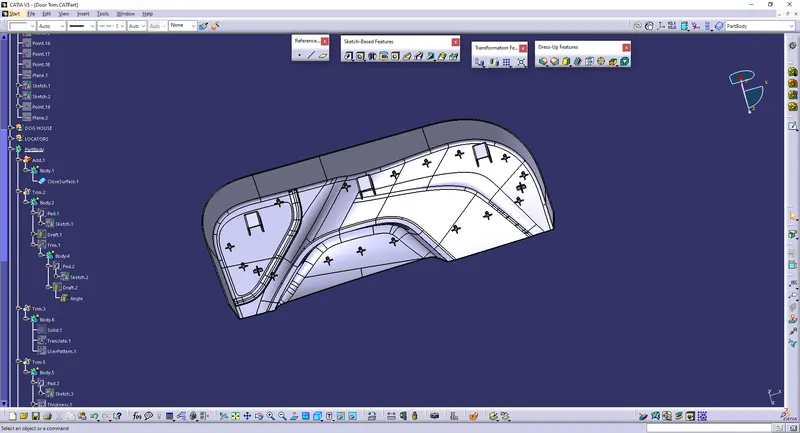
Week 9 - Project 1 - Door Trim Lower with Engineering Features
OBJECTIVE
Create the Door Trim Lower Plastic component through the given Class-A surface. To begin with, the tooling axis for the given Class-A Surface should be created meeting the requirements of the draft angle and at the end perform the Draft analysis on the model.
Create the Heat Stakes and the locators considering the design rules mentioned in the video for the door trim.
METHODOLOGY
We get the component and with the help of the design rules for 2 way & 4 way locators Heat Stakes we design the following.
Then after that we do the draft analysis.
TOOLS USED:
Boundary
Join
Multiple extract
Trim
Surface offset
Draft analysis
Intersect
Surface sweep
Close body surface
DESCRIPTION
1. CREATING TOOLING AXIS The Tooling Direction is basically the direction that the mold pulls a part. The mold is built in two separate pieces,
basically. You have a Cavity side and you have the Core side. The Core pulls apart from the Cavity and that's the Dye line or the Tooling Direction.
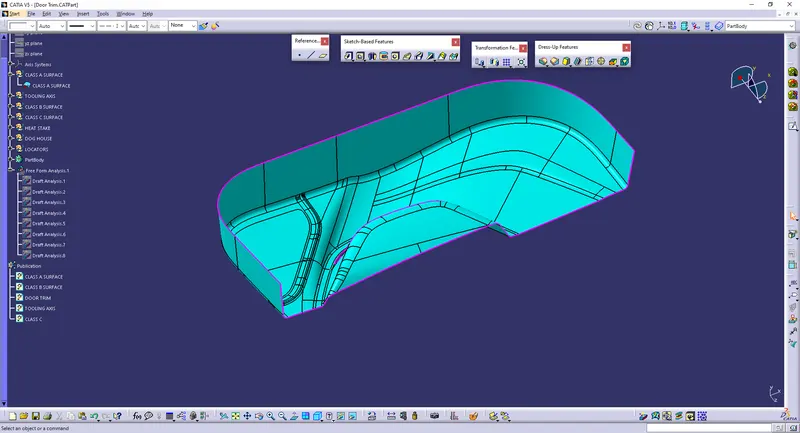
Open the given CAT part file.
Check for gaps between surfaces for that click on join and then preview.
If theres any gap between the surfaces join them with a maximum tolerance of 0.003 mm
Extract the boundary and dissemble the boundary.
2. PUBLICATION
Publication is done to the component to make it visible and navigate easily.
To publish the component go to tools > publications and then select the tooling axis and the class A surface.
A separate tree structure is formed under the main part
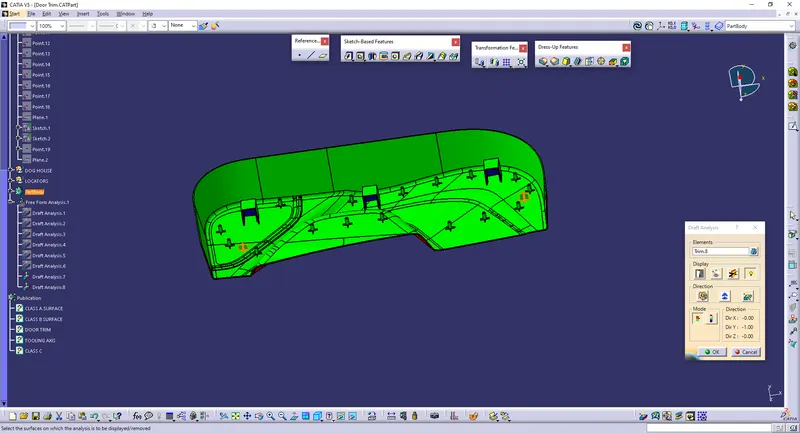
3. DRAFT ANALYSIS
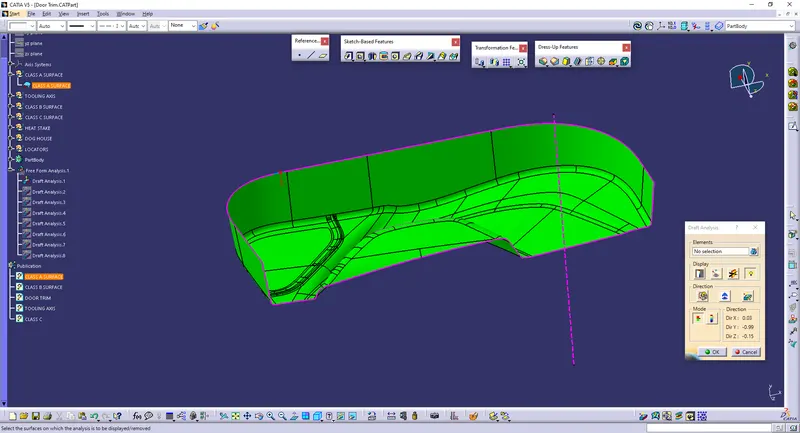
The Draft Analysis command enables you to detect if the part you drafted will be easily removed. This type of analysis is
performed based on color ranges identifying zones on the analyzed element where the deviation from the draft direction at any point,
corresponds to specified values.
Before going to drat analysis go to customized view parameter >under mesh >check material and then click ok.
Now for draft analyses go to insert » analysis » feature draft analysis.
Use the compasss to define the draft direction.
In the colour scale change the draft angle to 3 degree.
The component changes to green in indication of passing draft angle.
Use running point to check the angle on the component.
The draft analysis is complete.
4. CREATING CLASS B SURFACE
Extract the surfaces from the class A using multiple extract and untrim them.
Use Extrapolate to make sure that all the untrims are properly intersected to trim and offset the surfaces to 2.5 mm to create the thickness.
Trim the extra surfaces using trim command.
Insert them into new geometrical set and name it with respective part names.
Apply fillets to the model after creating the entire surface.
If the edges are outside the fillet value will be added to the thickness of the component and if the edges are inside, the fillet
value will be subtracted from the thickness of the component, for instance the thickness of the component Is 2.5mm the fillet
value is 15mm so the outside portion value should be 17.5mm and inner eges should be filleted 12.5mm to get uniform thickness.
Perform trims one at a time so that it will be clear to understand.
5. CREATING CLASS C SURFACE
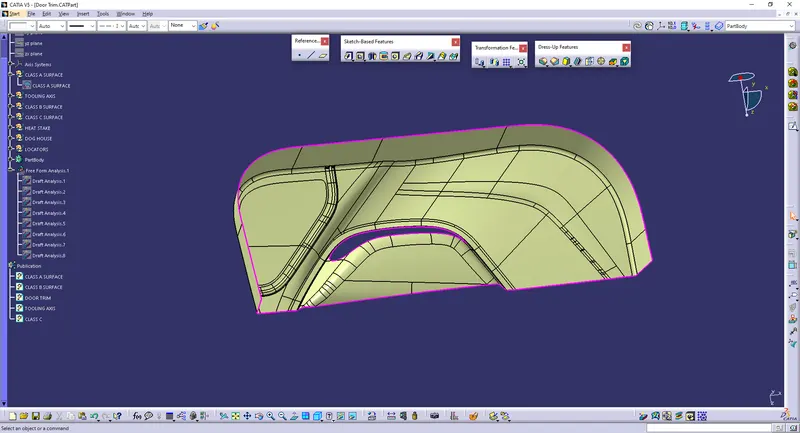
Extract the boundary from the class A surface using boundary command.
Using disassemble tool to divide the boundary as the boundary contains domains.
Use sweep command > choose profile type line > subtype as with draft direction > choose guide curve and draft direction > draft
angle as 3 degree > preview.
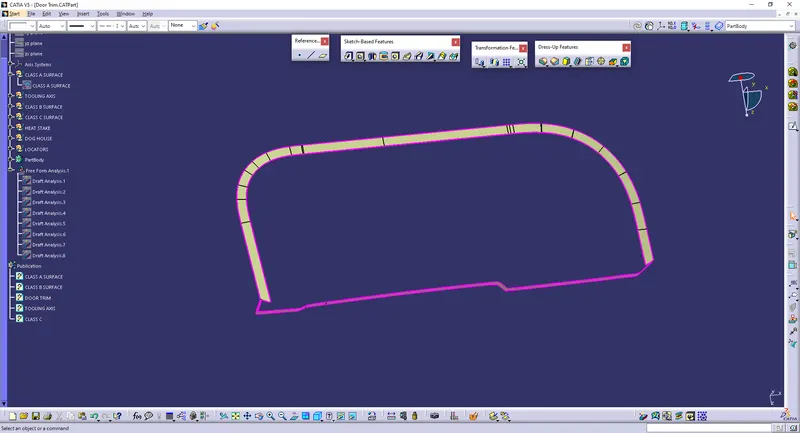
TRIM A+B & C
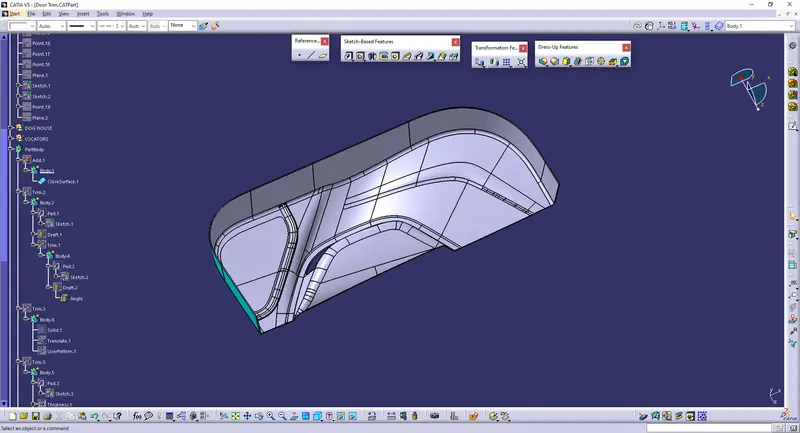
CREATING SOLID MODEL BY USING CLOSE SURFACE IN PART DESIGN
6. create 4-way locators,2 way-locators and heat stakes
INTRODUCTION:
3-2-1 PRINCIPLE:
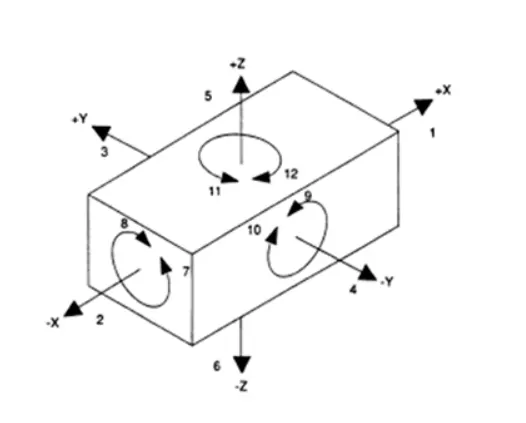
A work-piece free in space can move in an infinite number of directions. For analysis, this motion can be broken down into 12
directional movements or "degrees of freedom". All 12 degrees of freedom must be restricted to ensure proper referencing of a work piece.
As shown in Fig 1, the 12 degrees of freedom all relate to the central axis of the work-piece. Notice the 6 axial degrees and 6 radial degrees of freedom.
The axial degrees of freedom permit straight-line movement in both directions along the 3-principle axis shown as X, Y & Z. The radial degrees of freedom permit rotational movement, in both clockwise & counter clockwise radial directions around the same three axes.
Degrees of Freedom of a Rigid Body
Consider the rigid body shown below which is situated in space. It can have 12 degrees of freedom.
2-WAY LOCATORS:
A 2-way locating pin restricts motion along 1 axis (or 2 degrees of Freedom), like a round pin in a slot. Likewise, a 4-way pin restricts 4 degrees of freedom along 2 axes. A round locating pin located concentrically in a hole is a common application of a 4-way pin, and helps to further secure the piece.
4-WAY LOCATORS:
4-way mean you prevent movement at 2 axes (+X, -X, +Y and -Y) on the plane. Generally, you have cylindrical pin on the fixture and circular hole at workpiece part
HEAT STAKES:
Manufacturing operations currently use many different combinations of attachment methods to keep components together.
Common fasteners such as bolts, screws, and rivets can be used to form permanent attachments, but there are attachment
methods that don’t require secondary hardware. One of those methods is heat staking, which doesn’t require additional fasteners.
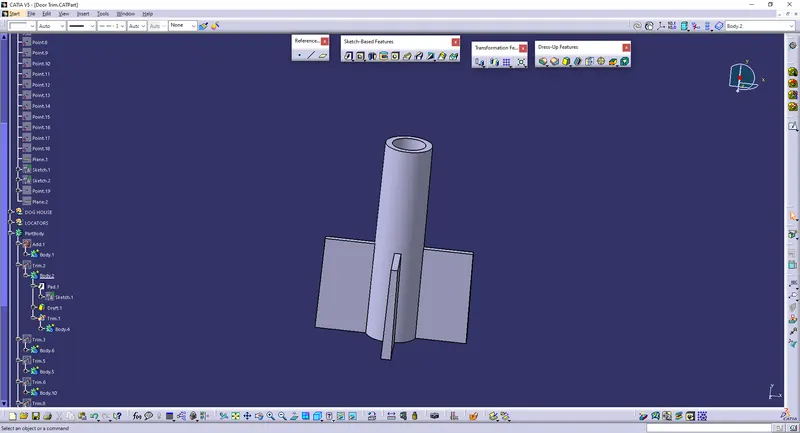
WHAT IS HEAT STAKING?
Heat staking is the process to attach two separate components together by melting the base plastic material into a shape that will hold the secondary component. It’s a permanent attachment method that does not require any additional material such as an adhesive or a solvent to make the permanent bond. The only addition is the heat applied to melt the plastic and a tool to shape the plastic to form the mechanical connection.
Heat staking can be done with a precise and rapid operation that also offers repeatable results every cycle. Manufacturing machine can be developed to complete multiple heat staking operations at once to decrease cycle time. The stakes don’t have to be parallel which makes the design options limitless.
Heat staking is a great option that is comparable in strength and durability to other operations involving secondary fasteners without extra cost. These connections can also resist corrosion in harsh environments.
REASONS FOR HEAT STAKING:
1.Mutiple staking shapes for different benefits.
2.Excellent durability.
3.No extra materials are needed.
4.Increased efficiency.
5.Easy Maintenance.
4-WAY & 2- WAY LOCATORS, HEAT STAKES CREATED ON DOOR TRIM:
CONCLUSIONS:
The 4 way and 2-way locators, heat stakes has been created following all the plastic design guidelines.