Week 8 - Challenge 6 - Core & Cavity Design
AIM:
To create a switch bezel from the given A-class surface by considering a thickness of 2.5 mm and also creating Core and Cavity blocks for it.
A class surface :
The input of the product designer is in the form of the A-class surface. The job of the product designer is to create the B and C surfaces keeping all the aspects for the mold.
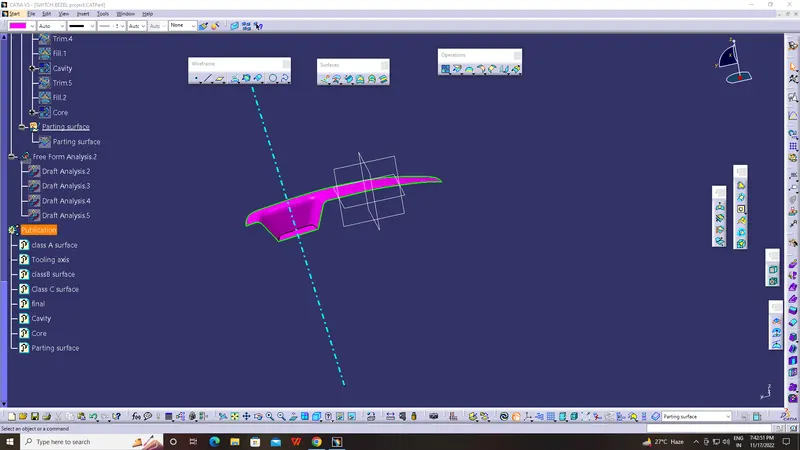
Tooling axis:
- Considering the Ejection from the cavity of the mould after manufacturing the interior trim (switch bezel) must have the
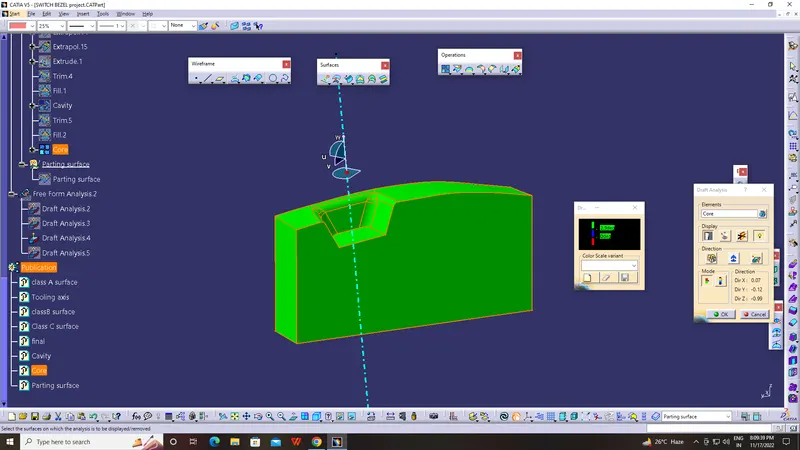
- nominal 3-degree draft angle.
- Hence the tooling direction is created by considering the above factor and bisecting method is used.
- The base surface of the class – A was extracted and a point at the centre is created and an axis system was inserted to the point with the current feature is disabled.
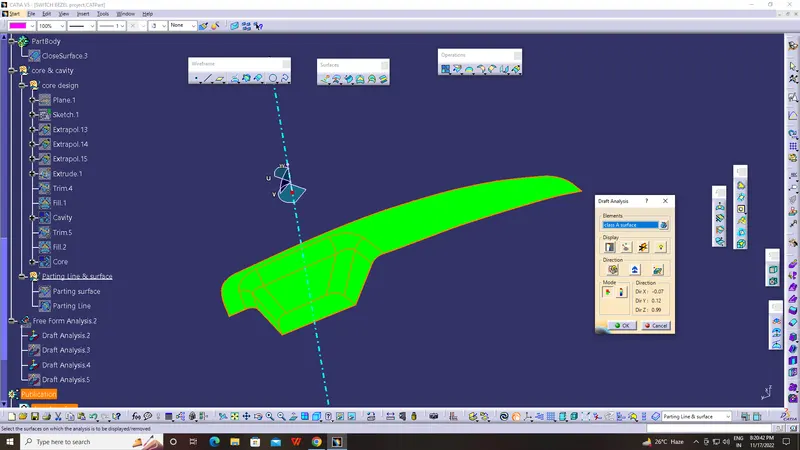
Core and cavity design:
The Mould Core & Cavity are the shaped sections in either half of the mould tool which give the plastic product its final shape.
The hot molten material is injected into the core & cavity and then sets hard into shape. The design of the core & cavity is essential in the correct formation of the product. The sequence of events during the injection mould of a plastic part is called the injection molding cycle.
The cycle begins when the mould closes, followed by the injection of the polymer into the mould cavity.
A core is usually made of the best quality sand and is placed into the desired position in the mould cavity. Core prints are added to both sides of the pattern to create impressions that allow the core to be supported and held at both ends.
Cavity :
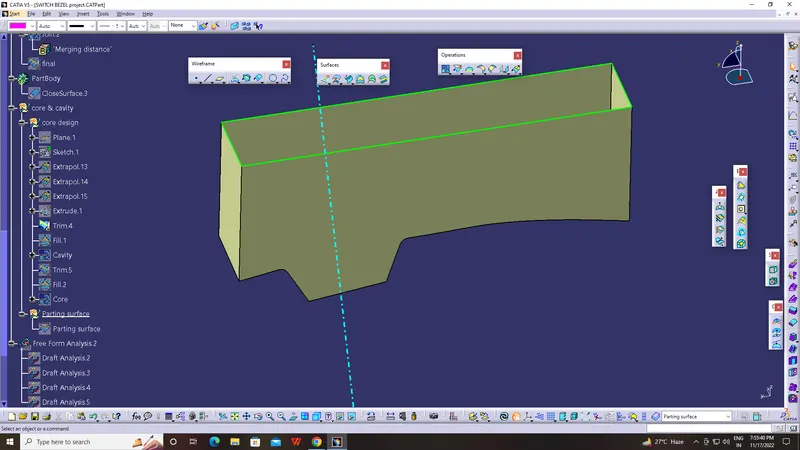
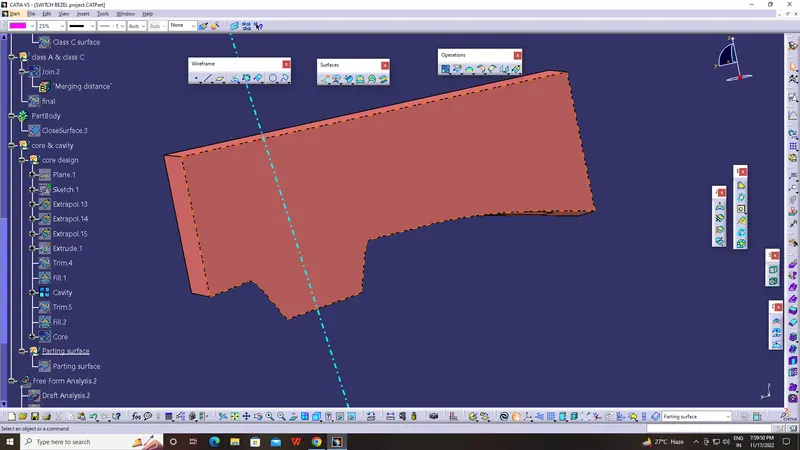
- The cavity is the part where the injector and filling of the molten plastic happens. The cavity block is prepared by first extruding the outer boundary along the tooling direction.
- The cavity design is started with extracting the parting surface that becomes the datum for the core and cavity. The parting surface in most of the cases is kept at the B class surface to avoid close and tight contact between the core and cavity.
- At first, the A-class surface is extrapolated with some length and later it is trimmed with a C surface.
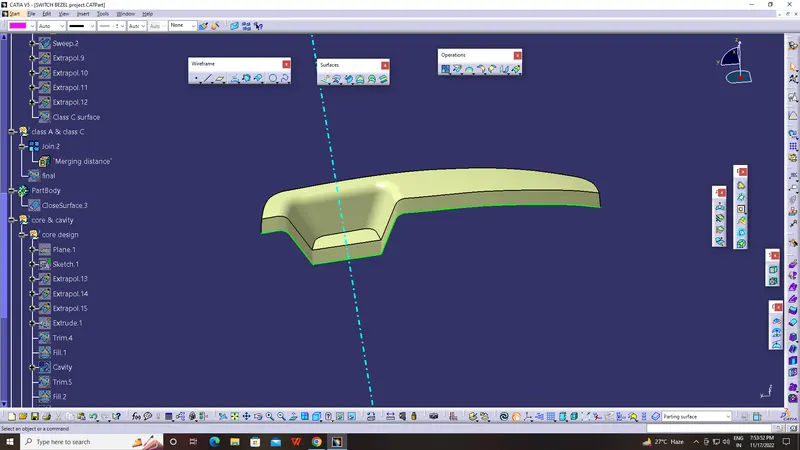
- This A and C surface again trimmed with the B surface to form the cavity face.
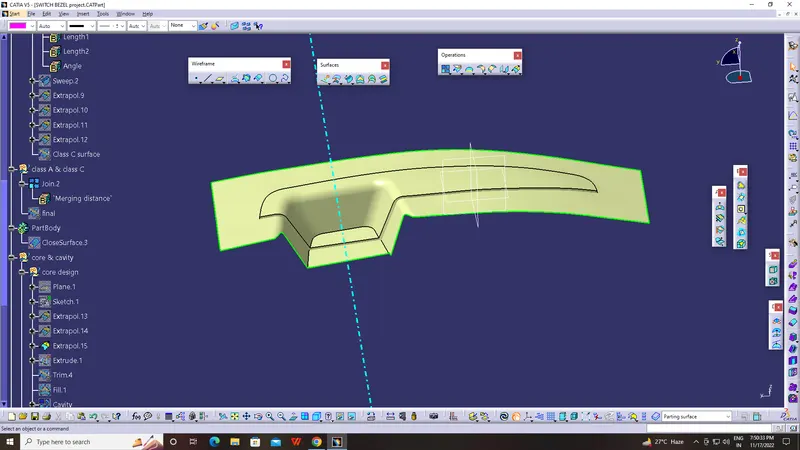
- Now, the final cavity block is made by drawing the boundary sketch and extruding it along the tooling axis direction followed by the filling and thickening.
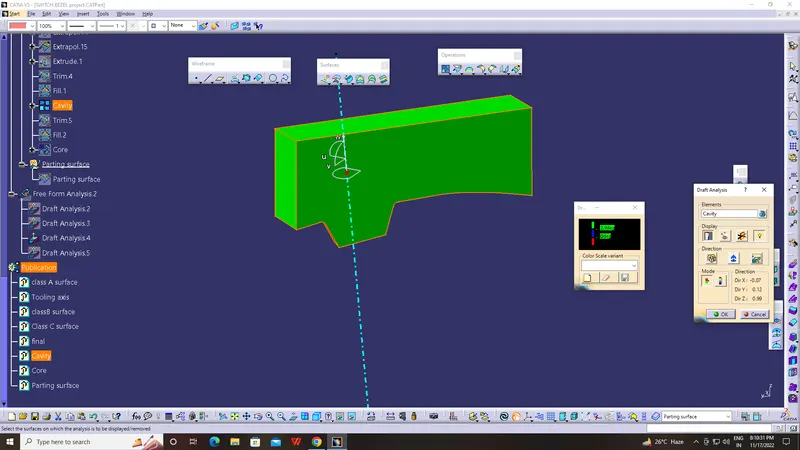
Draft Analysis of Cavity:
Core :
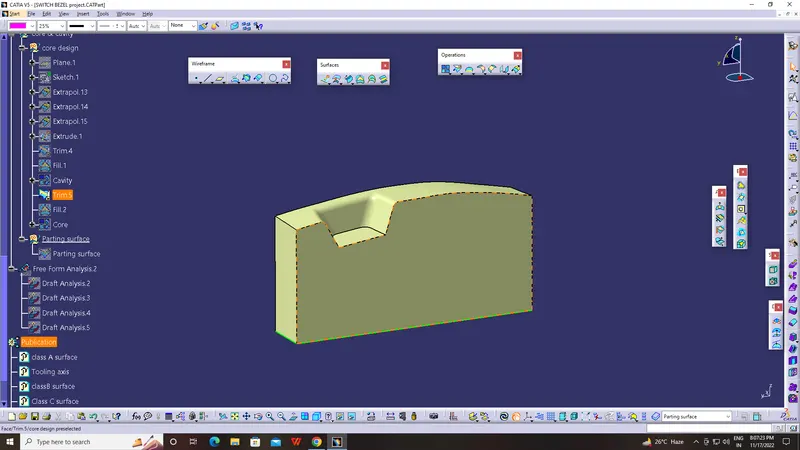
- The core design is started with extracting the parting surface that becomes the datum for the core and cavity. The parting surface in most of the cases is kept at the B class surface to avoid close and tight contact between the core and cavity.
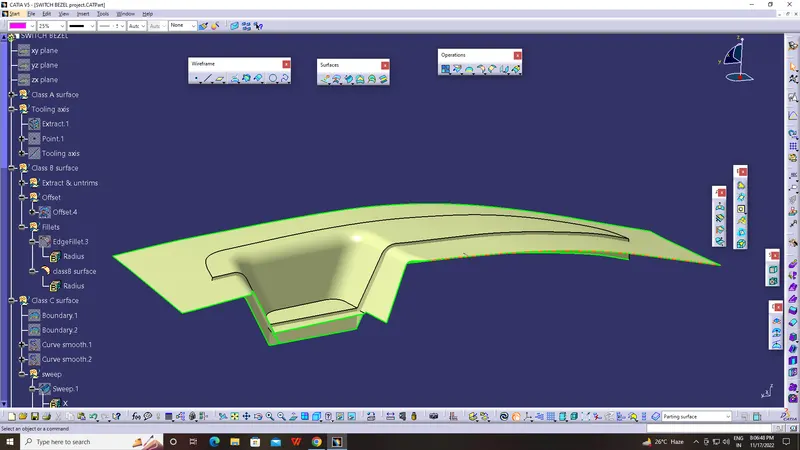
- This outer surface is trimmed with the B class surface and then it is filled and thickened.
Draft Analysis of Core :
Parting surface :
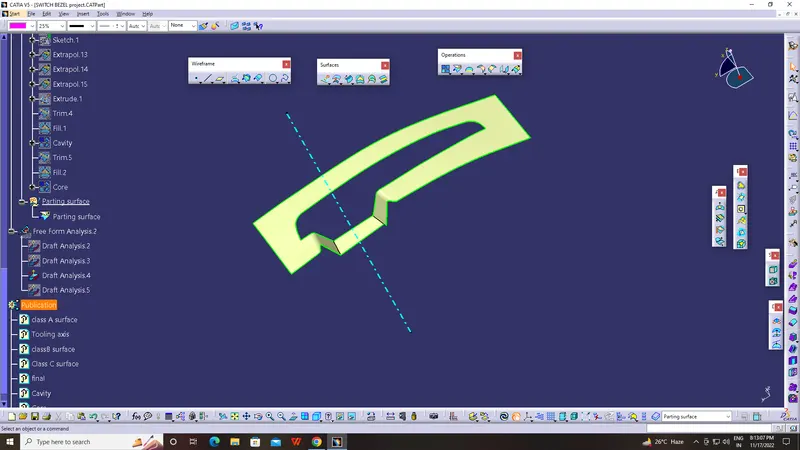
The parting surface of a mould are those surfaces of both mould plates adjacent to the impressions which butt together to form a seal and prevent the loss of plastic material from the impression. The parting surfaces of a mould are those portion of both mould plates, adjacent to the impressions, which butt together to form a seal and prevent the loss of plastic material from the impression.
Parting line :
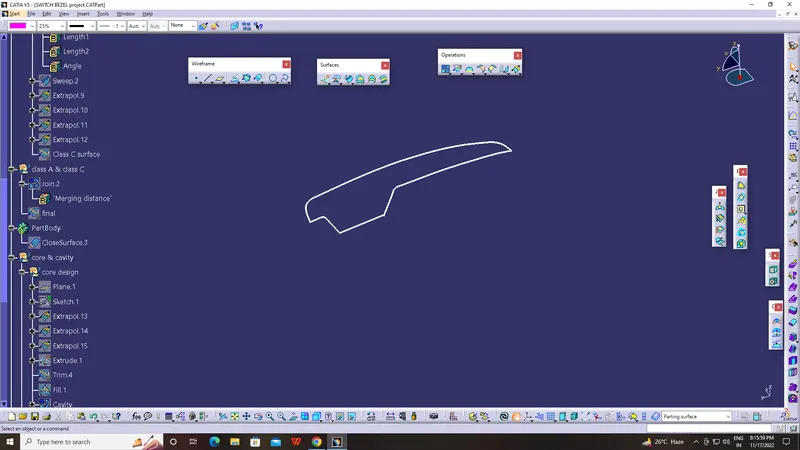
A parting line, in the industrial casting of molds, is the borderline in which draft angles change direction. That is, it is the dividing line that splits the core and cavity halves of a molded part. It is sometimes a starting point for the mold parting surface.
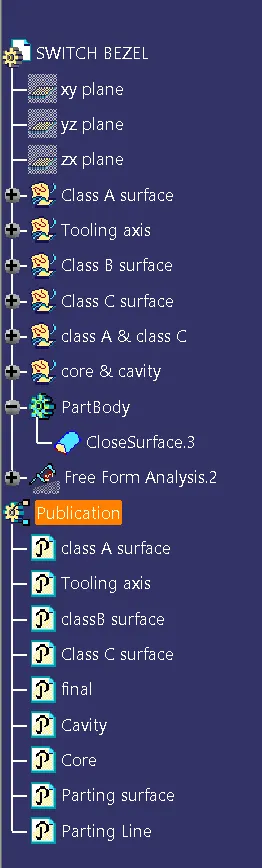
Tree Stucture:
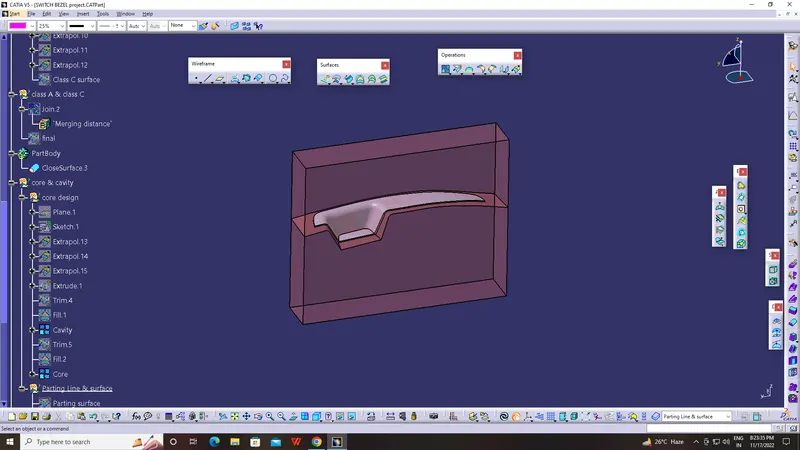
Result:
Core and Cavity blocks for the Switch Bezel have been successfully created.