Week 8:- 3D Finishing Challenge 2
Aim:-
- To create Rough locator for the fixture.
- To Perform 3D finish for all units by considering manufacturing fesibilities.
Introduction :-
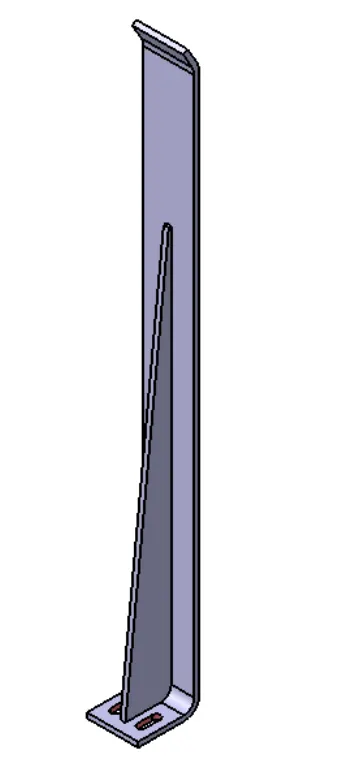
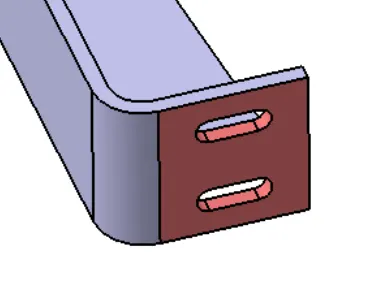
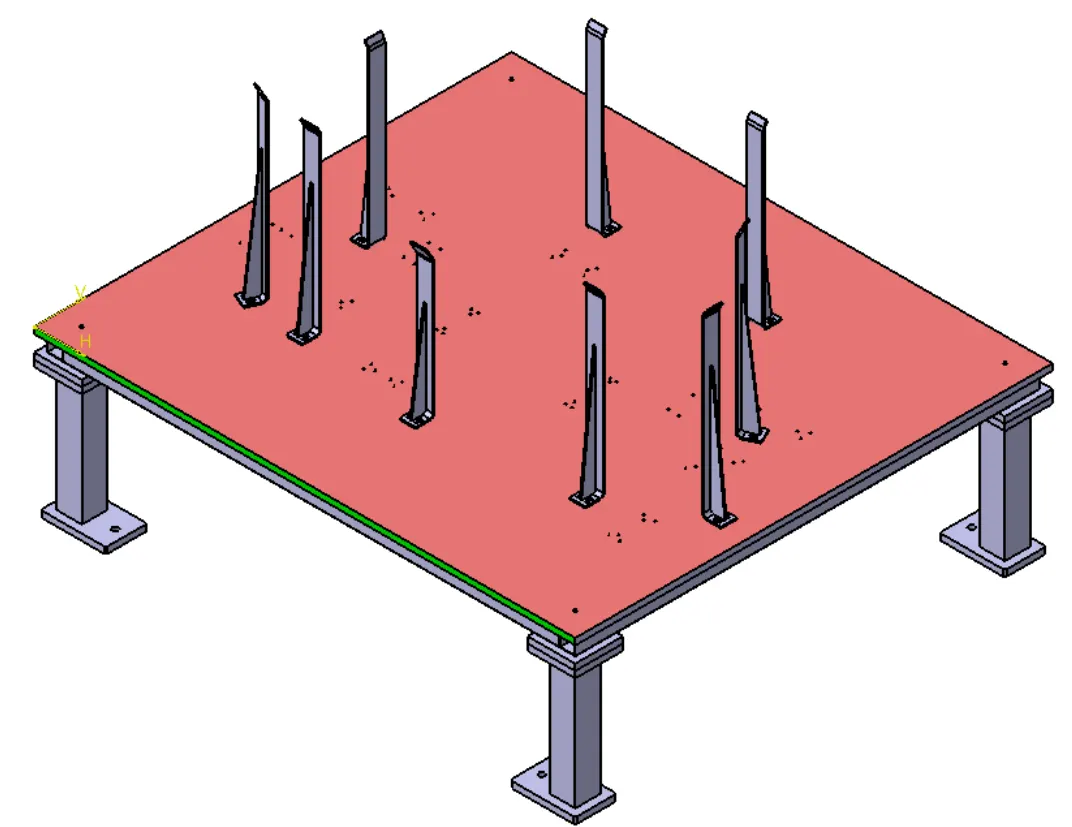
ROUGH LOCATORS
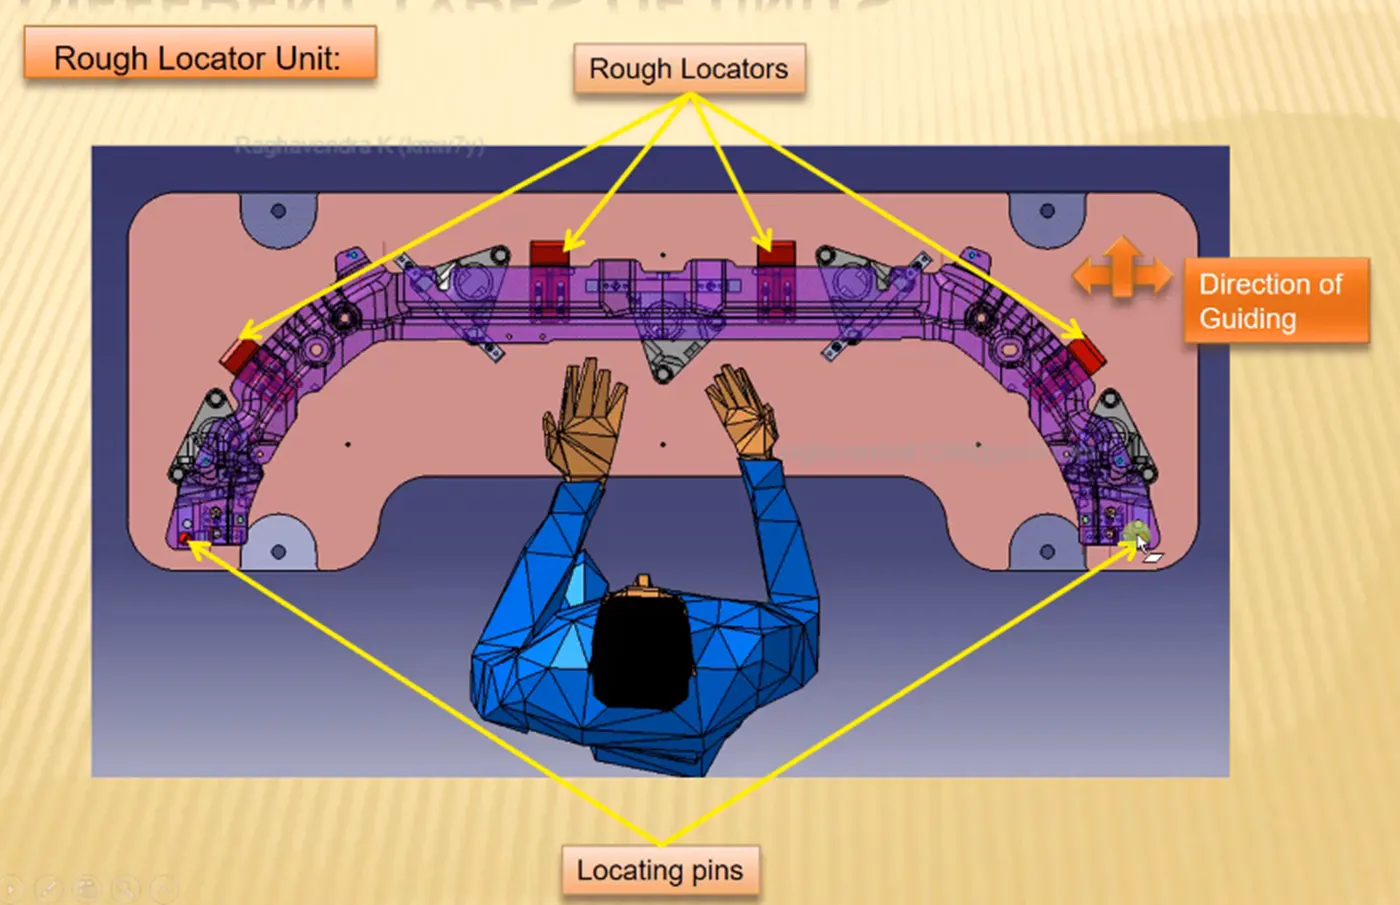
- A rough locator is a part designed to guide the operator, to locate the car panel on to the pins accordingly. A rough locator can be of standard part or make part.
- Rough locators are used to help locate work pieces in the automation process. Locating refers to the desired location where we want the work piece to be sitting. when it is getting on either worked on either by a person, team, or a robot.
- Body part rough locators are provided to assist manual part loading to the tool.
- The following are general guidelines for rough locators:
- It is not required to finish cold/hot rolled steel for rough locator mounting. Use NAAMS standard rough locators when possible.
- If possible, do not place rough locators in positions that force the operator to lift and load, or unload the part over the rough locators.
- Rough locators must be designed with slots for ease of adjustment.
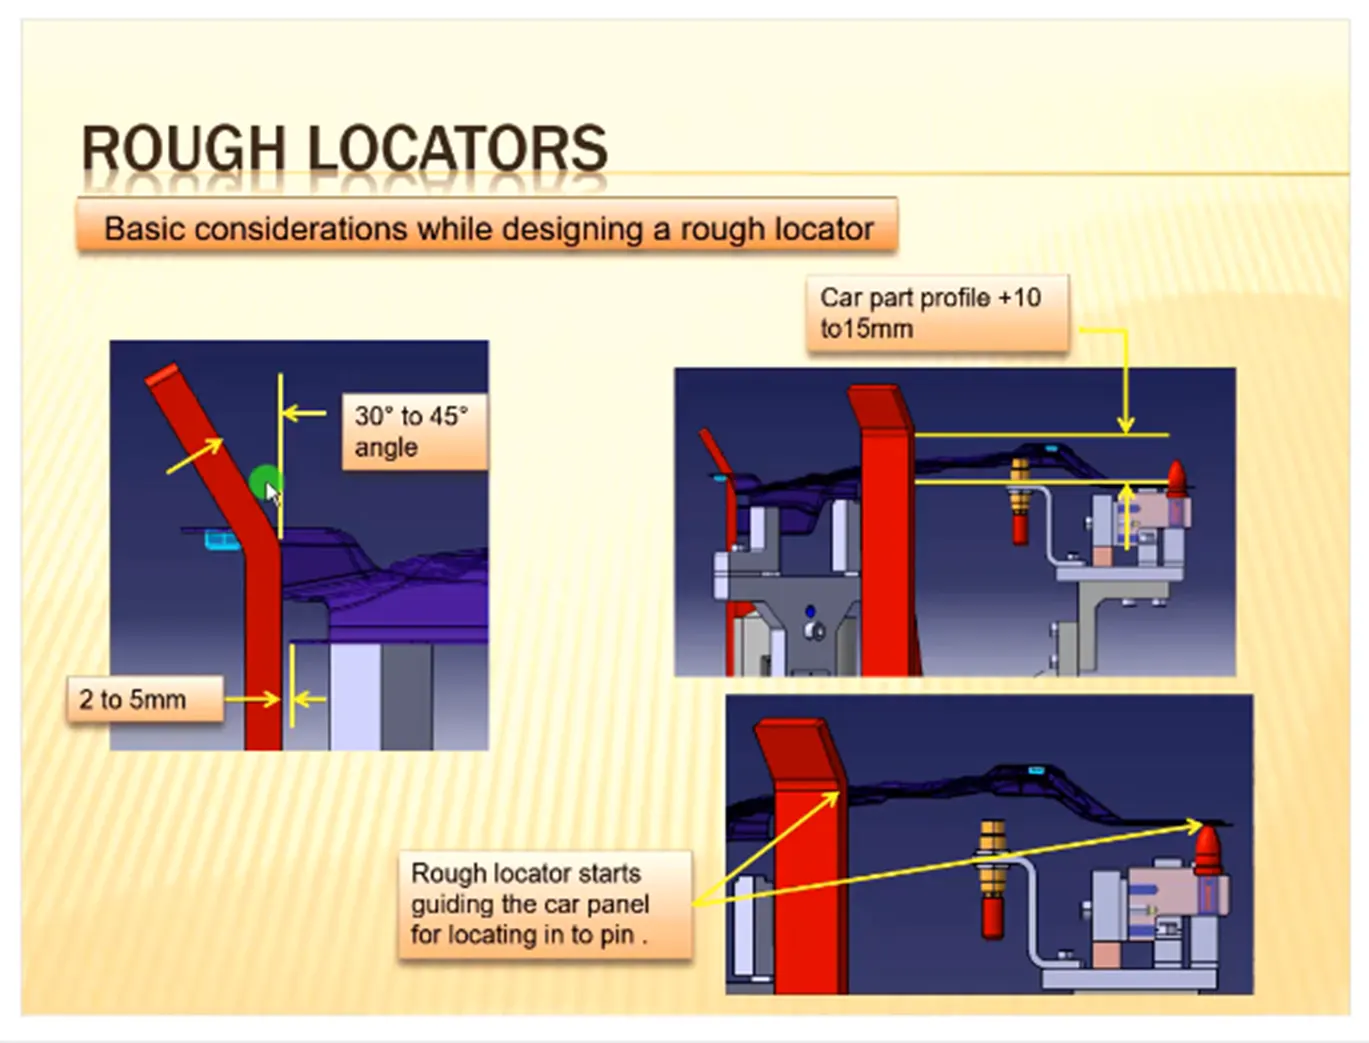
- Rough locators should have minimal part contact so that the operator can load the part to work location with ease. Excessive part contact may cause difficult part loading and unloading.
- Rough locators must never touch the part when it is nested or controlled by the primary tool locators.
- If the rough locator requires a unique design, use the design parameters for the standard NAAMS rough locator as a guide.
- A rough locator is a part designed to guide the operator, to locate the car panel on to the pins accordingly. A rough locator can be a standard part or make part.
- It is used to identify the correct orientation of the panel.
- It can be called as fool proofing method also. Because due to the rough locator the part cannot be loaded in incorrect position. The rough locators are set according to the angle of the respective panel hence part can only be loaded in defined orientation.
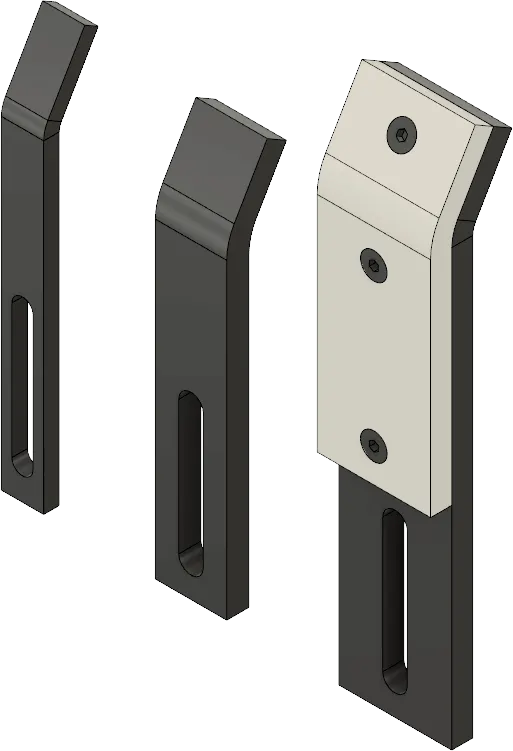
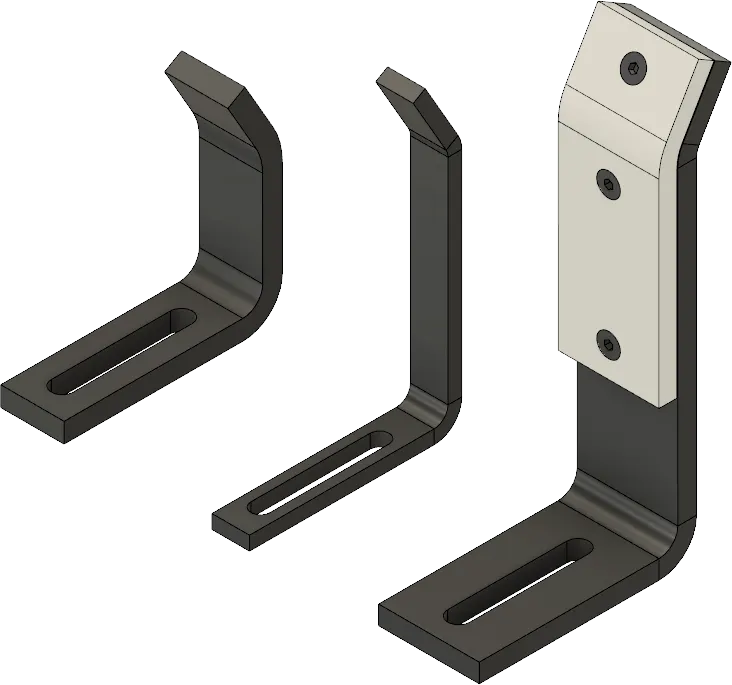
Design Considerations for Rough locators
3D FINISH
3d Finish is a process where the design is being completely finished and to be ready for final simulation and 2d detailing.
- While finishing the design the nominality is checked which ensures the easy assembly of all the units.
- The hole concentricity and hole sizes are checked which ensures the assembly of different parts.
- The gaps between the different units are checked to ensure the proper individual working of different units.
- Design the rough locators, which help to load a panel in correction orientation.
- Design the pneumatic lay-outing for pneumatic connection.
- Gun study is the major and most important part of 3d finishing.
- Selection of sensors, Solenoid valves as per the requirement and implementation in design.
- Fasteners are implemented as per the hole size and the standard color codes as per the customer requirement are applied to differentiate the type of hole whether its dowel hole, Threaded hole, or clearance hole.
- Renaming of the assembly and the part is done to give every part a different identity so everyone can identify in which assembly this part is going to be fit.
- After doing all these things the model is sent for simulation and 2d detailing.
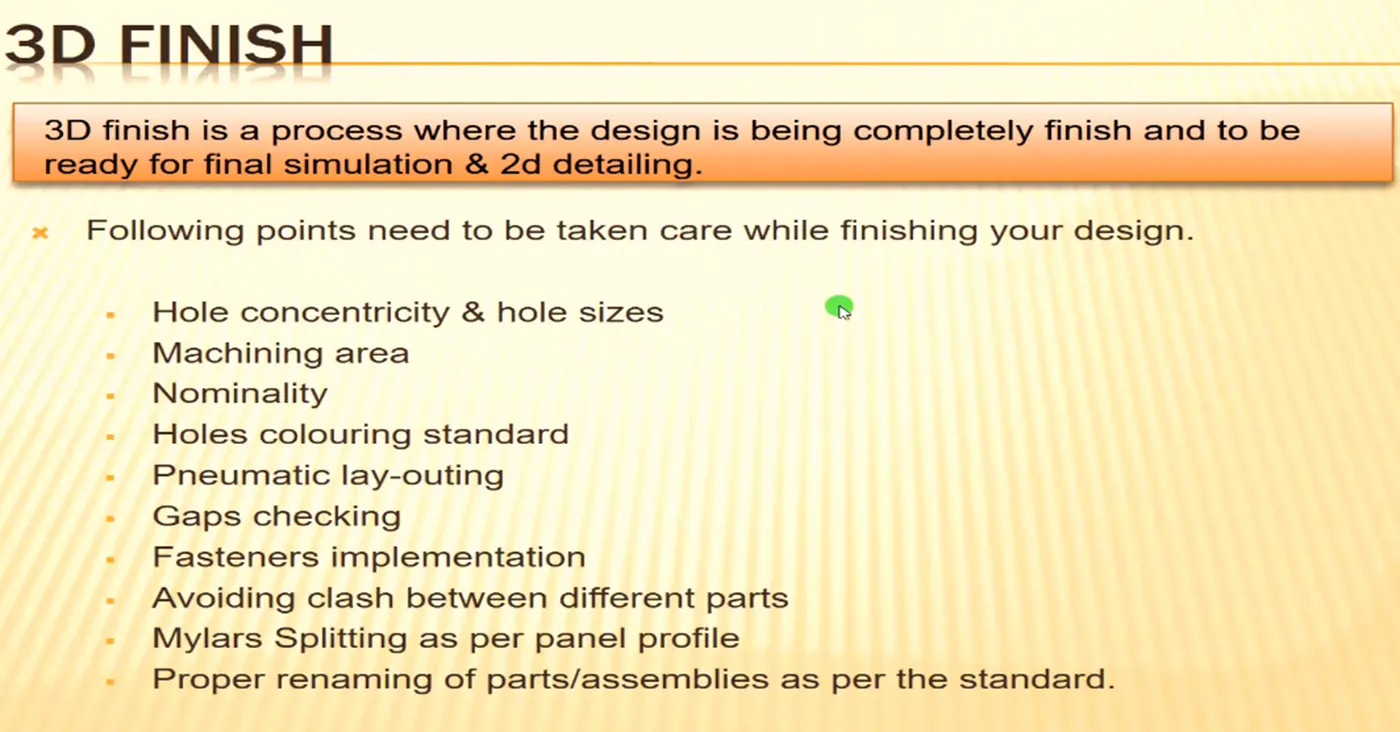
Points Need to Be Taken Care of While Finishing the Design:
The following are the points taken into consideration while finishing the design.
1.Hole Concentricity and Hole Sizes: All part holes concentricity and hole sizes are checked for easy assembly while finishing the parts.
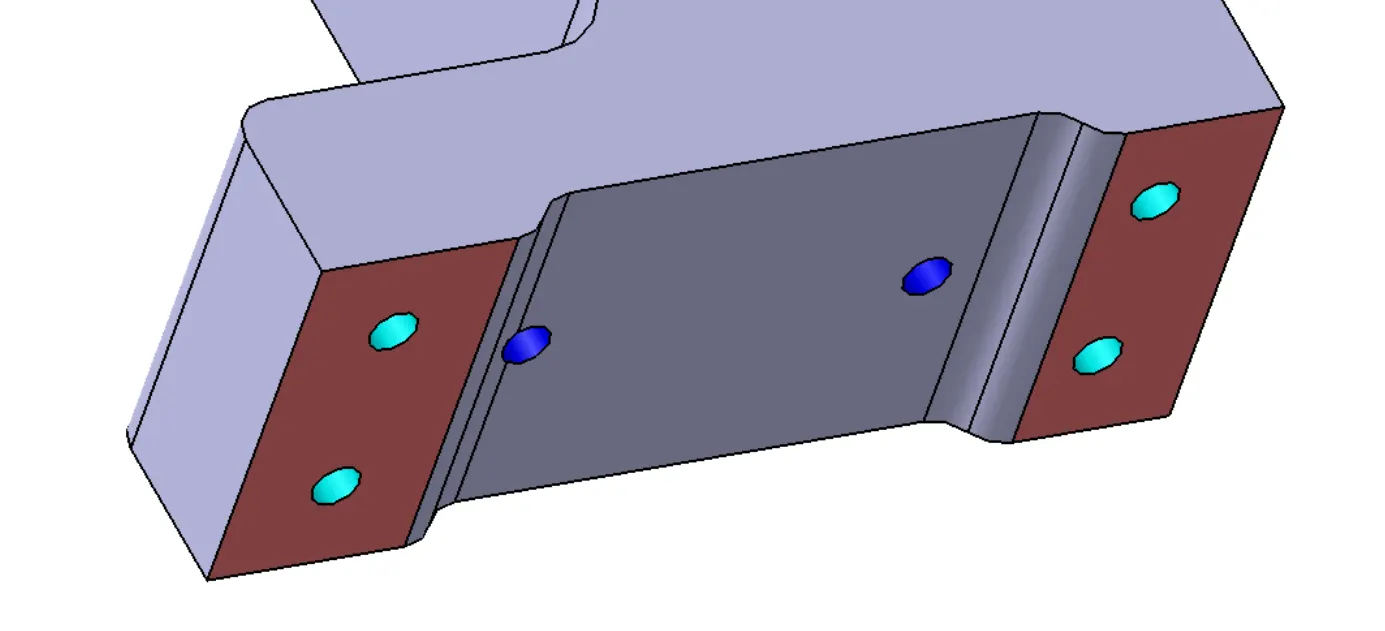
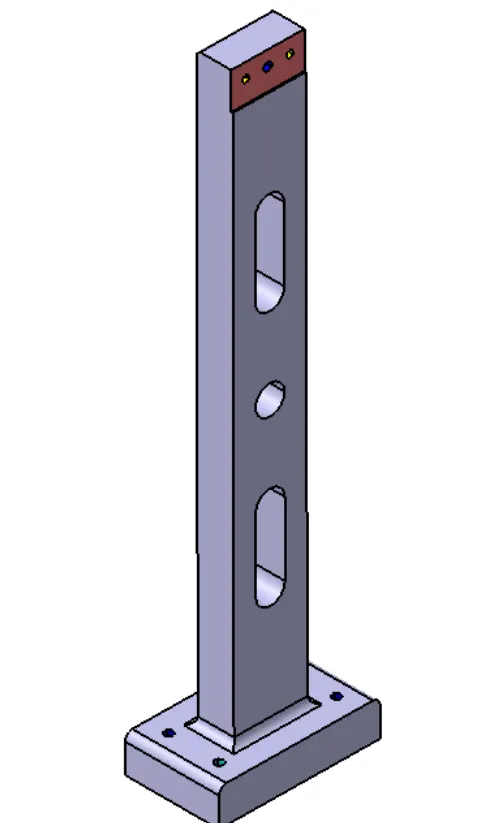
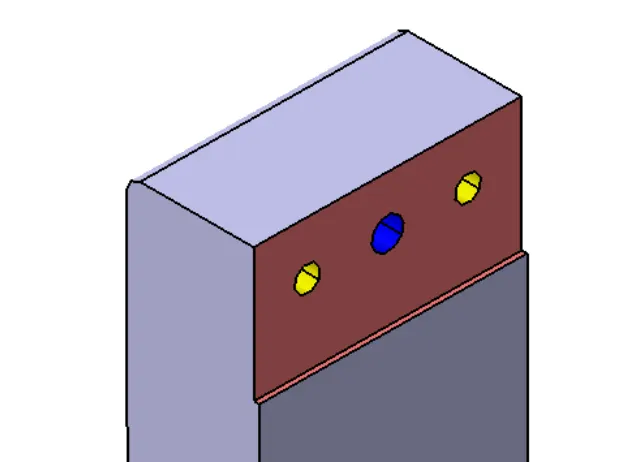
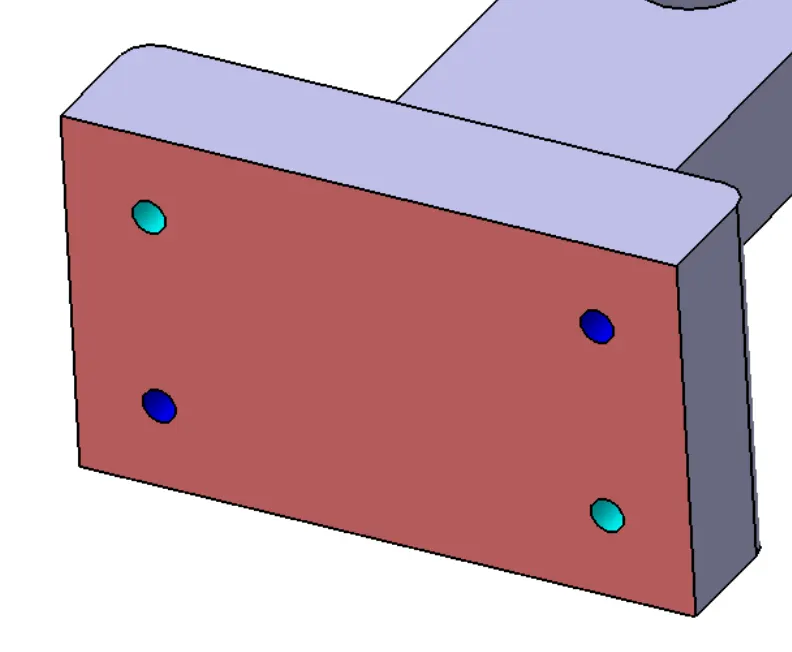
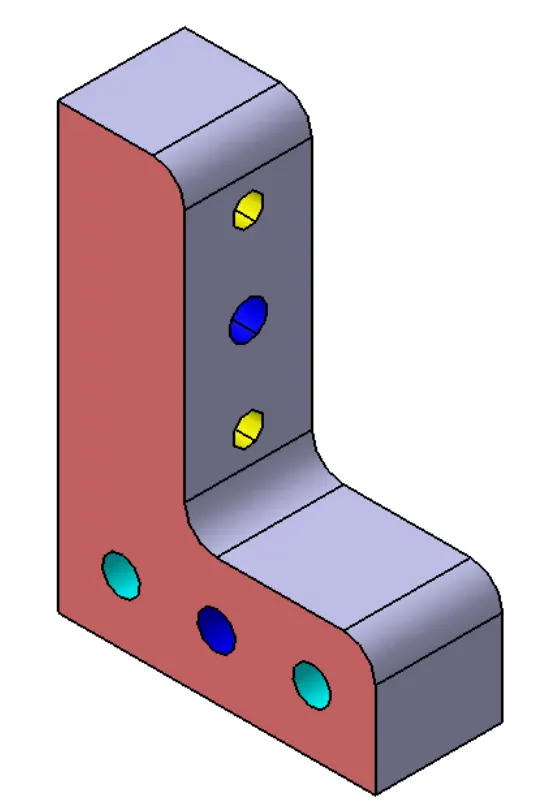
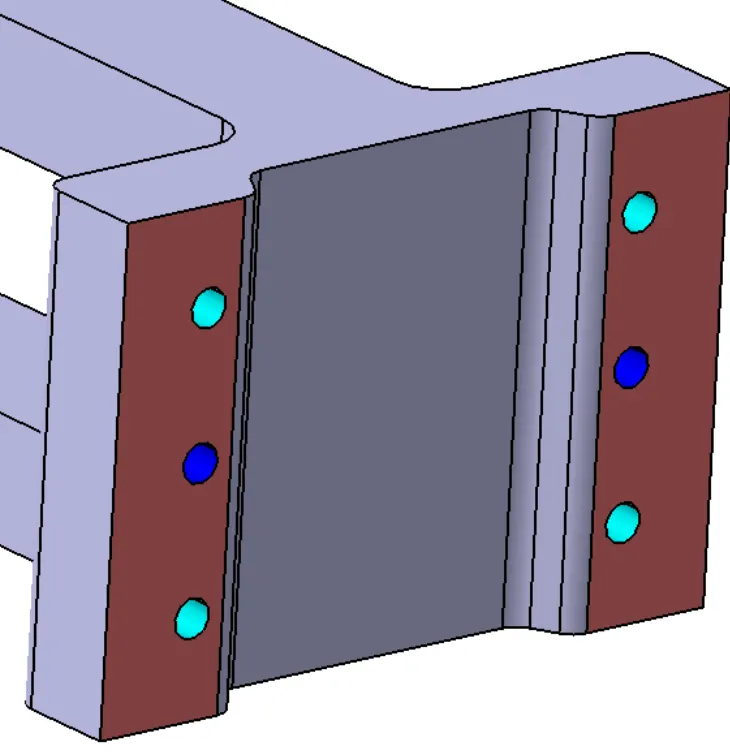
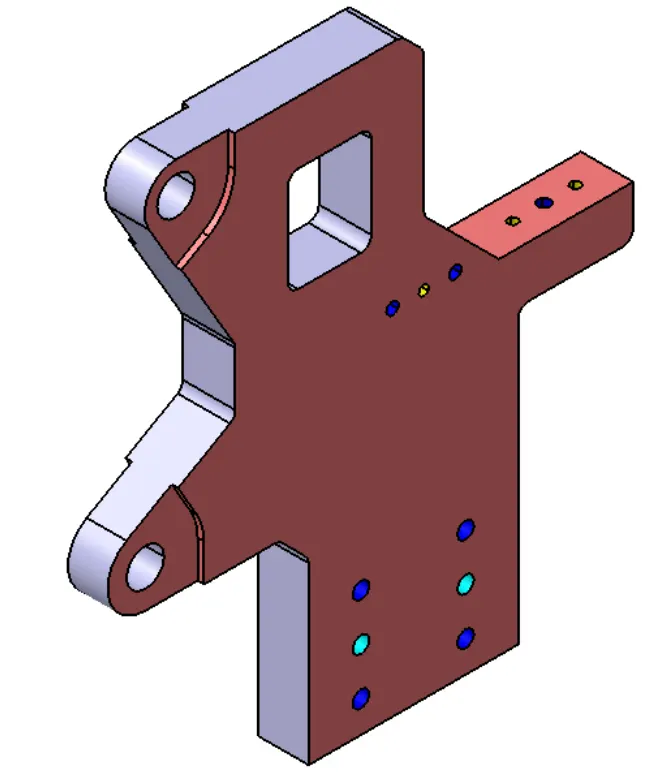
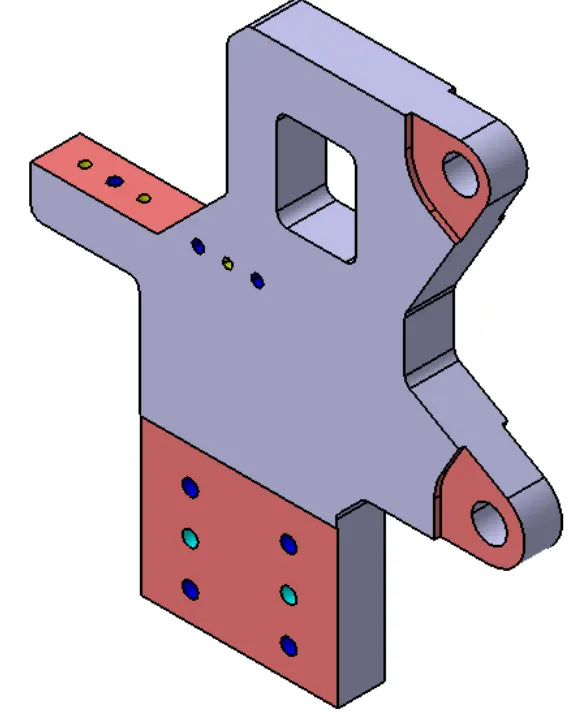
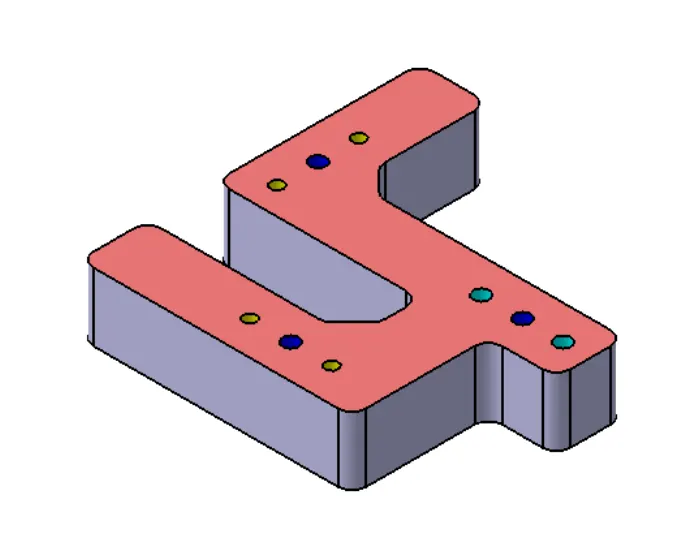
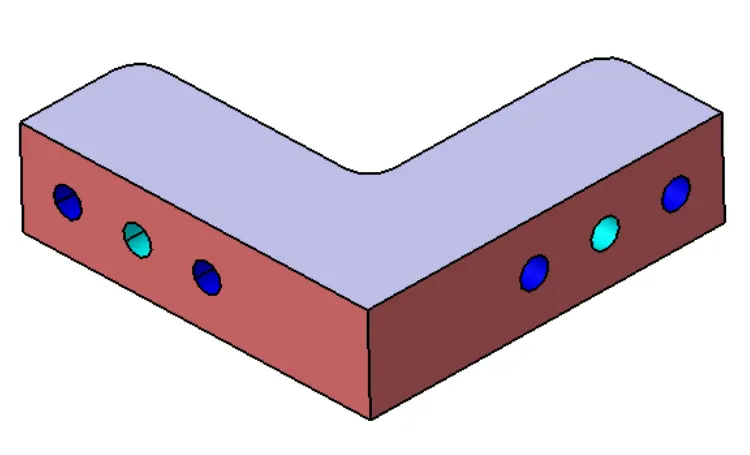
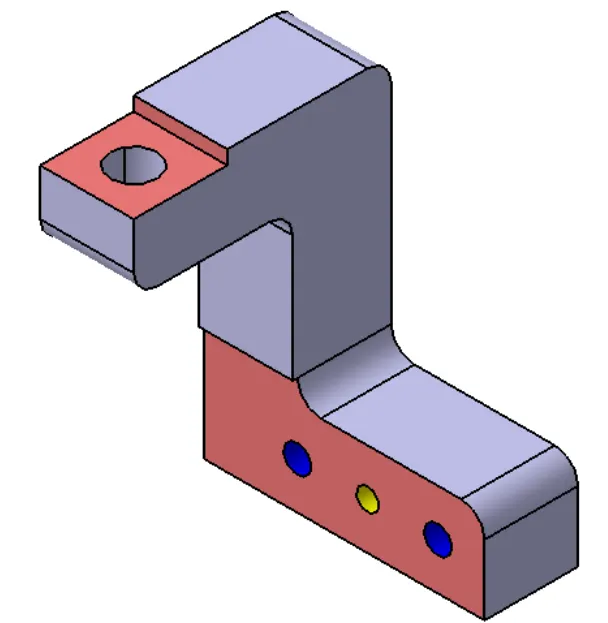
2.Machining Area:The machining area in every part should be defined and the machining area should be highlighted by using standard color code. Machining is to be done on parts to properly Mount with mating parts. Machining only on desired faces reduces cost and saves time. And also Machining increases the accuracy of dimension. So before going to simulation or detailing machining area should be defined.
3.Nominality: All unit dimensions should be maintained nominal to facilitate easy assembly of the unit.
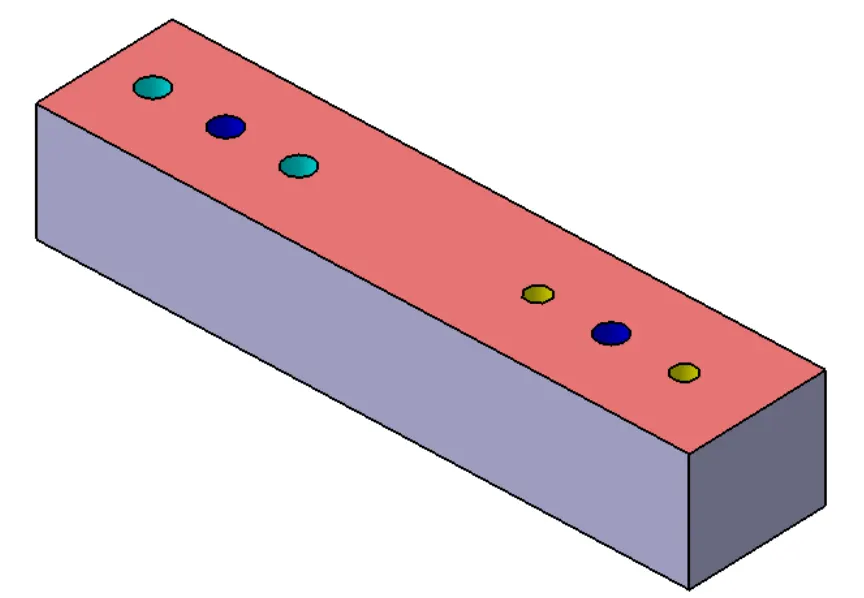
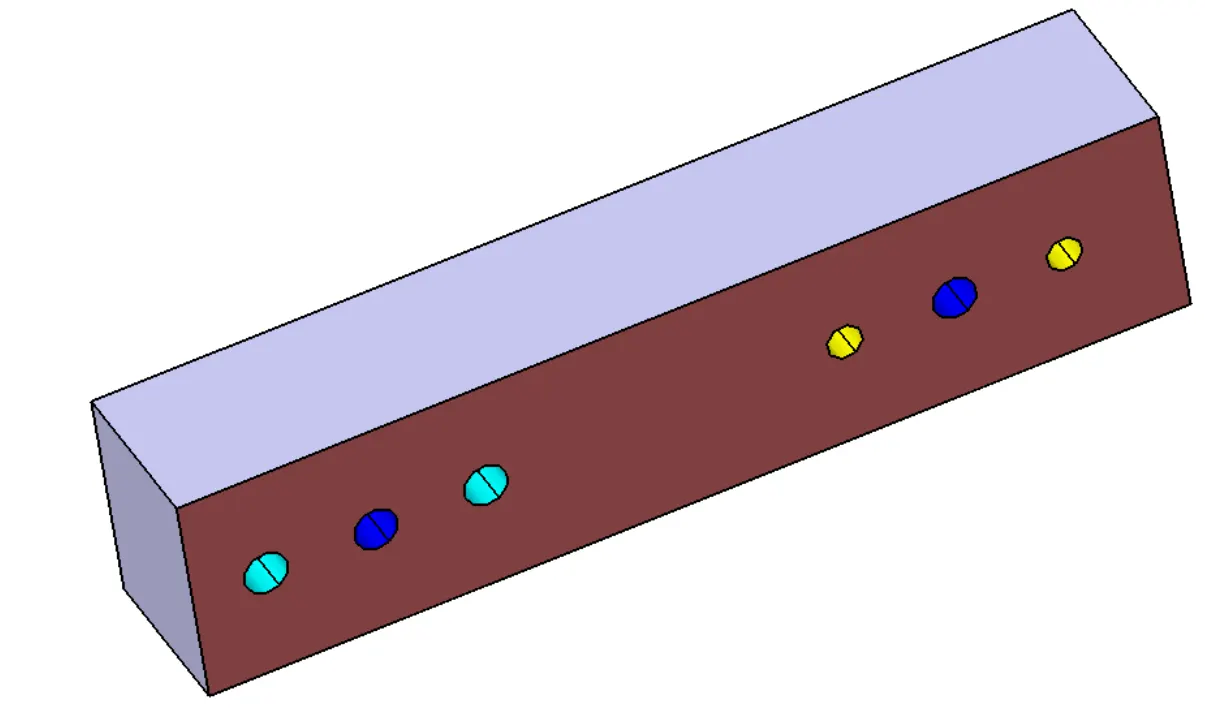
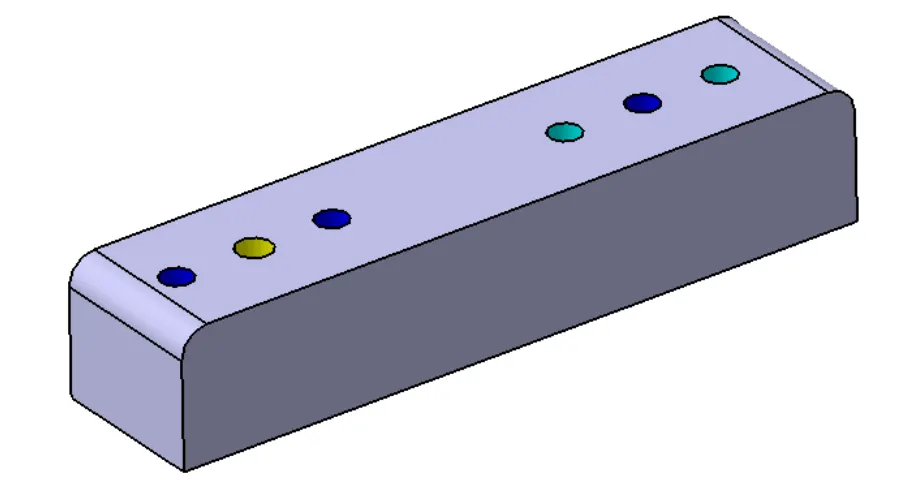
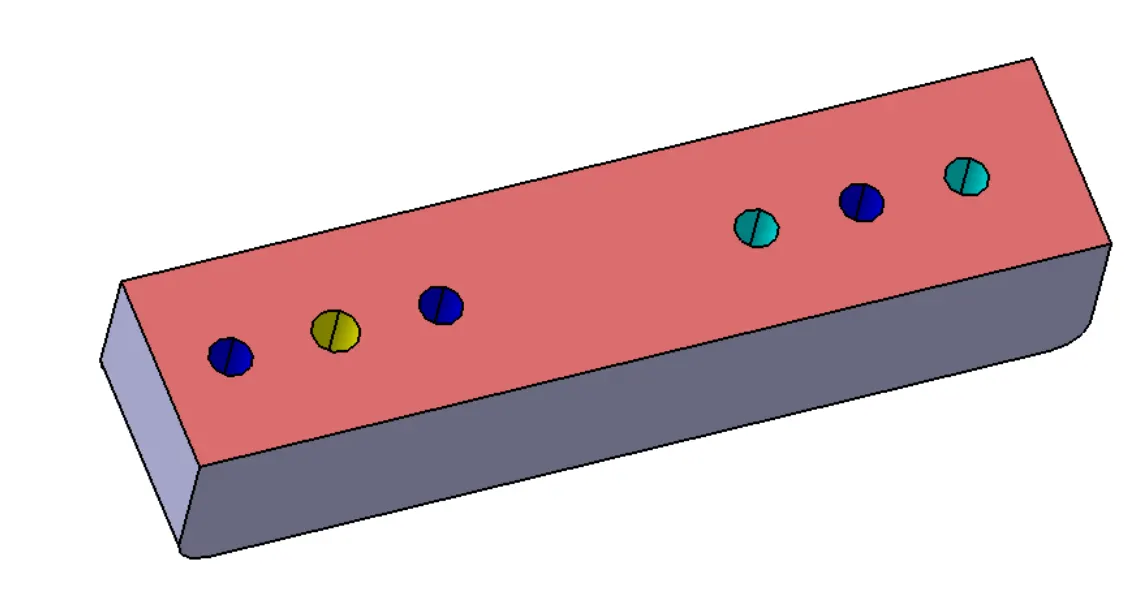
4.Holes Colouring Standard:
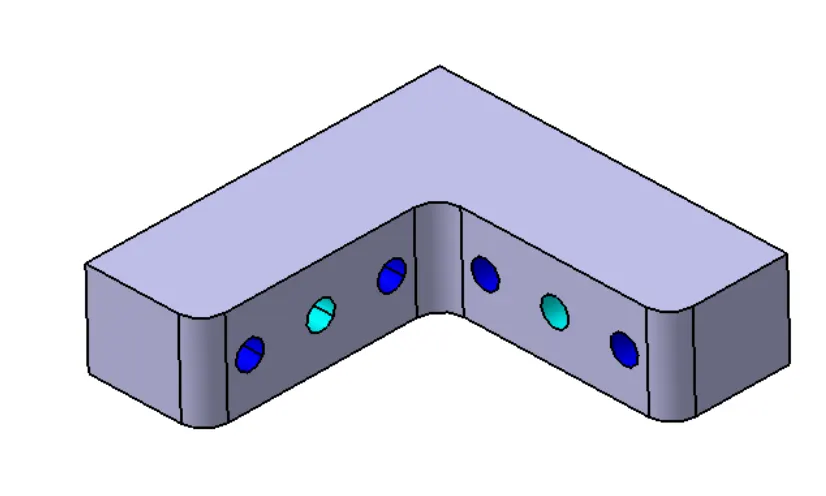
In a 3D finish, hole coloring should be done because it helps to identify what type of hole it is. It depends on customer standards. Customer-specific color like:
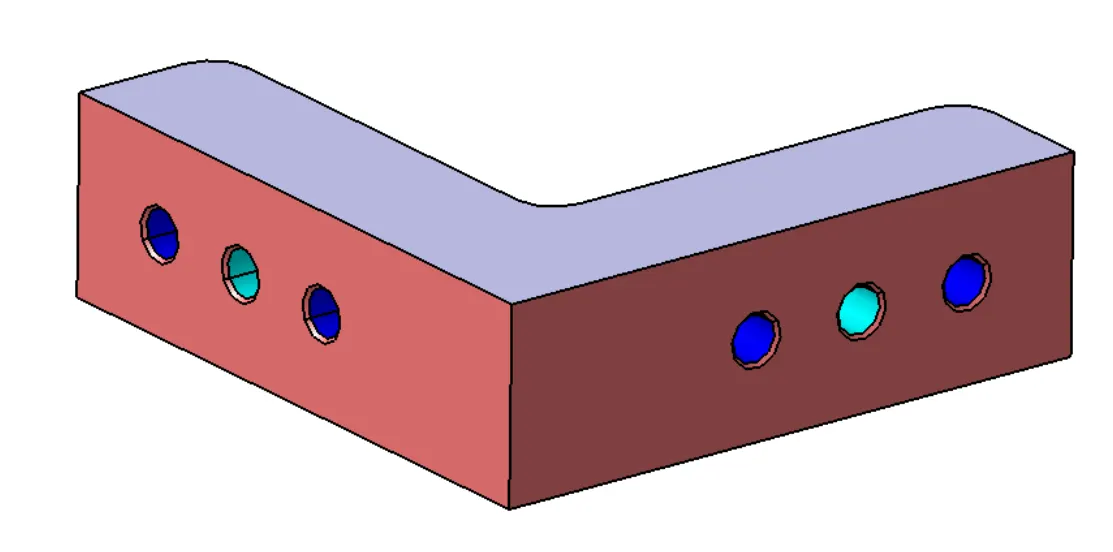
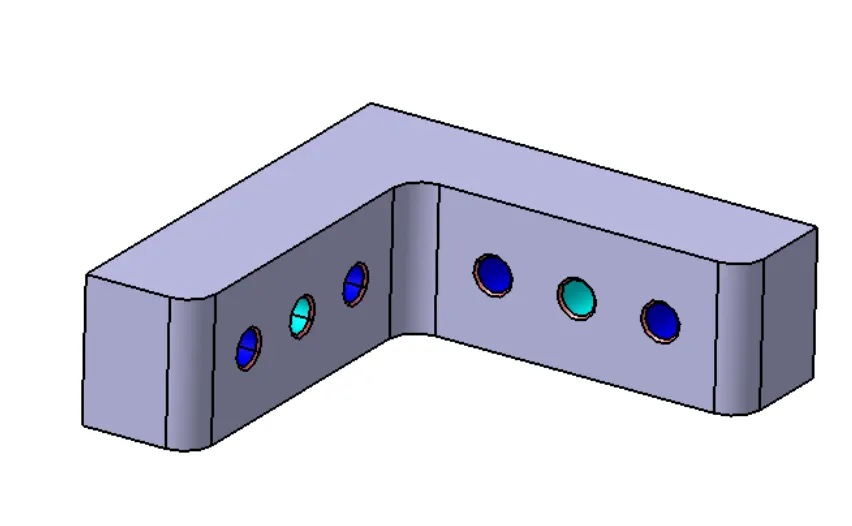
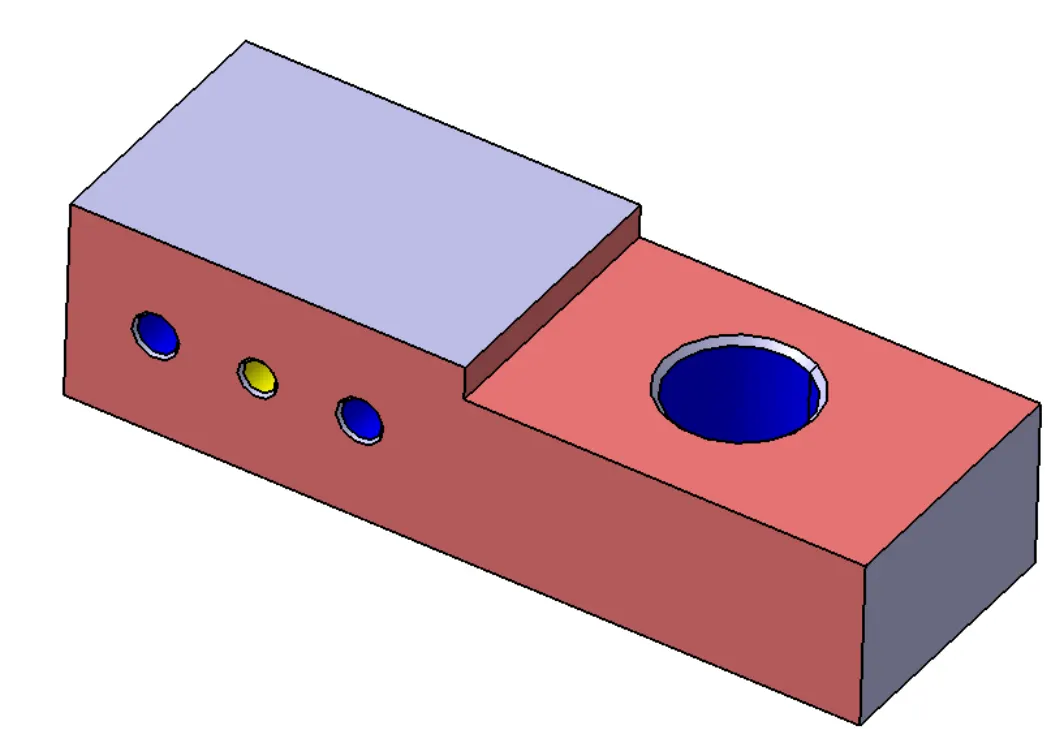
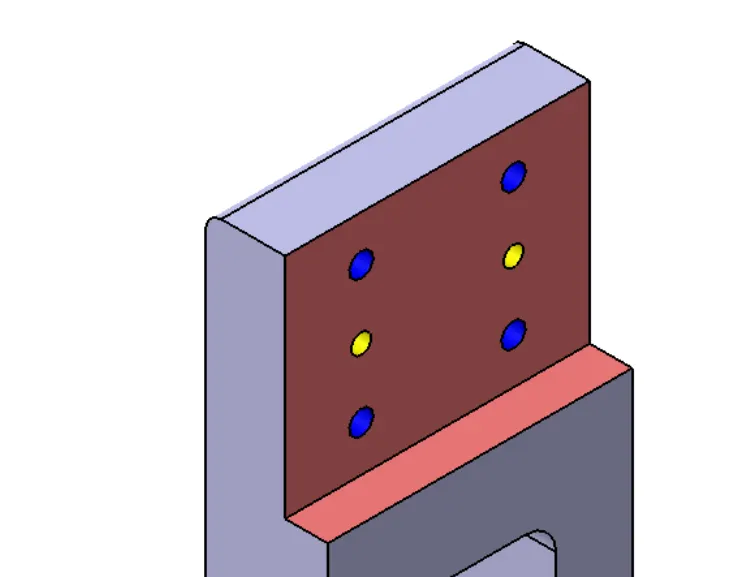
- The dowel hole should be given blue color.
- The threaded hole should be colored yellow.
- Counterbore, open hole should be given cyan blue color.
5. Pneumatic Lay outing:The pneumatic lay outing is a collection of different pneumatic pipes which work as an inlet to the pneumatic cylinder. It should be done properly for the proper functioning of the units.
6. Gaps Checking: The gaps between the different units are checked to ensure the proper individual working of different units.
7. Fasteners Implementation:Fast should be implemented in all the units as per the requirement and load on the part.
8.Avoiding Clash Between Different Parts:A proper gap should be maintained between units to avoid clashes between the different units.
9. Mylar Splitting as Per Panel Profile:Mylar splitting as for panel profile should be confirmed while finishing the design.
10. Proper Renaming of Parts or Assemblies as Per the Standards:Proper renaming of parts and assembly should be done while finishing the design and hence we can identify each and every part easily with Unique Identification.
Gun Study:
Welding is mostly used in automobile industries and their requirements for fixtures that ease the welding process is a continuous developments task in any industry.
In weld study process, the major procedure is insert the gun in the tool assembly and place the gun on the weld spots. Adjust the weld gun for not getting any clashes from the fixture. Once the gun study has been finished with the requirement of robot. It will move onto the fixture designers to develop the concept.
The most important thing to consider while gun study is how many panels are going to weld at a station whether it is 2 layer panel or 3 layer panel, we have to verify that, because the panel will not weld more than 3 layer.
Once all the weld spots are cleared without any clashes and it will be moved on to next procedure of simulation.
In simulation, first we have to check with the reach with respect to the weld spots. Because robots are also having some limitions. it exceeds the limits of robot, the robot will not work properly effective. So first we have check with reach check whether it has been reaching the all weld spots or not. If it should not reach the spot we have to change the robots orientation with consideration of clients requirements and we will not move robots placement without clients approval.
In simulation we have to check the spot with the developed fixture to know all the weld spots cleared with clashes or not. If any clashes get caught in simulation, we have to get cleared with design team and have to modify the fixture with simulations output.
Car Body In White (BIW) is a complicated steel structure including 300-500 sheets with complex shape and are assembled by means of welding in a high rhythm through 55-75 robotic work stations.
The fore most step taken before starting the welding fixture design, we must declare weld spots location for each and every panel. The location and orientation of other critical units of the fixture including clamps, locators., etc are decided based on the weld spot distribution.
Now coming to the point, in weld study, first we have to choose which gun has to be used for welding process. Gun have two different types, they are
C – Type gun.
X – Type gun.
C – Type gun:
In C – type gun one arm side is fixed and another arm is movable in linear direction of perpendicular to other arm (Horizontal direction with respect to other arm).
X – Type gun:
In X – type gun one arm side is fixed and another arm is movable in angle position like (it moves like an arc).
It includes the study of the weld matrix & the weld point positions. There are two types in weld point one is Geo weld which ensures the geometry of the assembly & second is Re-spot weld points which adds strength to the welded parts.
The fixture is designed for the car panel to hold it on the position, so we ensures all the weld spots and weld gun do not across or any clashes with fixture tool.
If any clashes defined while designing fixture, then we will only move on to redesign the tool. We have no permission to change a weld spot or clamping position without considering clients.
3D FINISH
BASE UNIT:
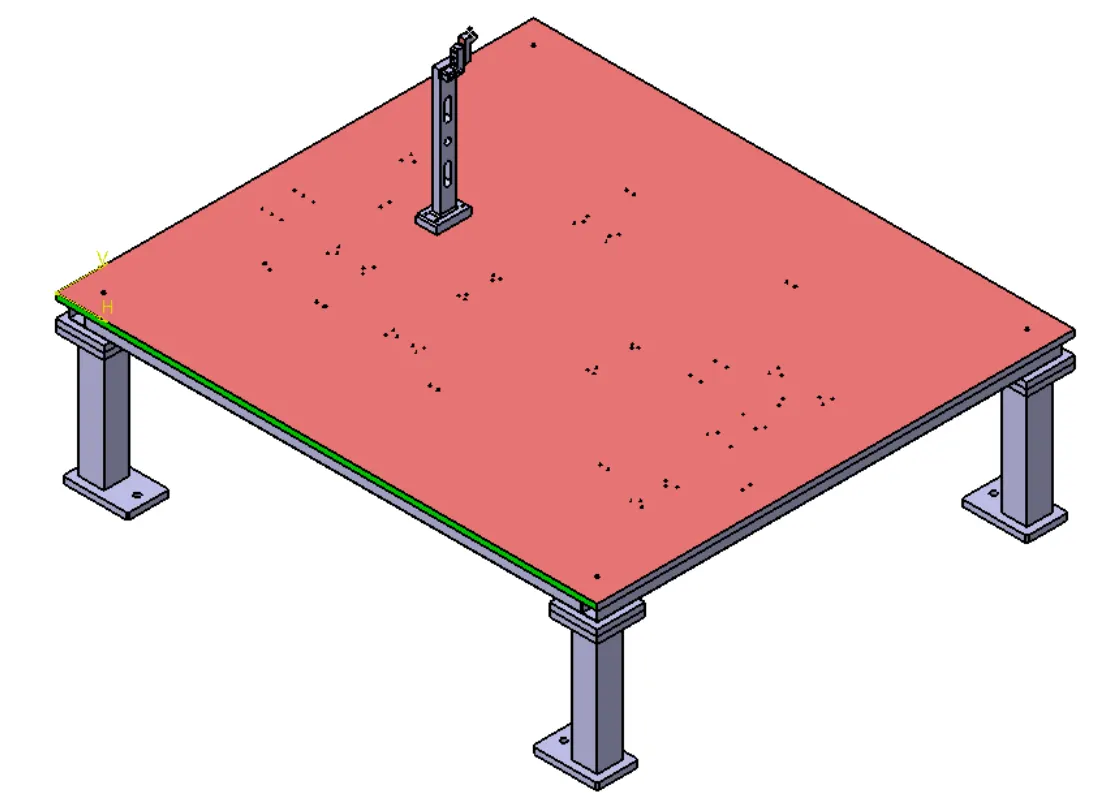
A base unit is a unit designed to mount all the other units of the tool, also other parts necessary for a tool like a pneumatic valve box, trunking cable path will also be mounted onto a base unit.
Below are some parts of a base unit in general.
- Trunking channel.
- Baseplate.
- Valve box.
- Measuring hole cover.
- Eyebolt.
- Pedestal.
- Weld bars.
- Floor plate.
Base plate:
- Base Plate is a machined plate of 25 to 40mm thickness made of steel and aluminum on to which the holes are drilled to mount the individual's units like clamp units. pin units etc of a tool.
- There are three key benefits to a Baseplate:
- They can help to quickly and accurately tram in fixtures and vises.
- They can hold large, complicated, or odd-shaped parts.
- They protect the cast iron machine table.
Pedestal:
- A pedestal is a part that connects the base plate to the floor plate. A pedestal is a standard part in general, and in some cases, it can be a welded frame integrated with the base plate.
- A standard pedestal can be of different heights and different sizes.
- Depending on the size of the base plate, the number of pedestals varies for load distribution.
- A pedestal is of different types with different inclinations.
Trunking Channel:
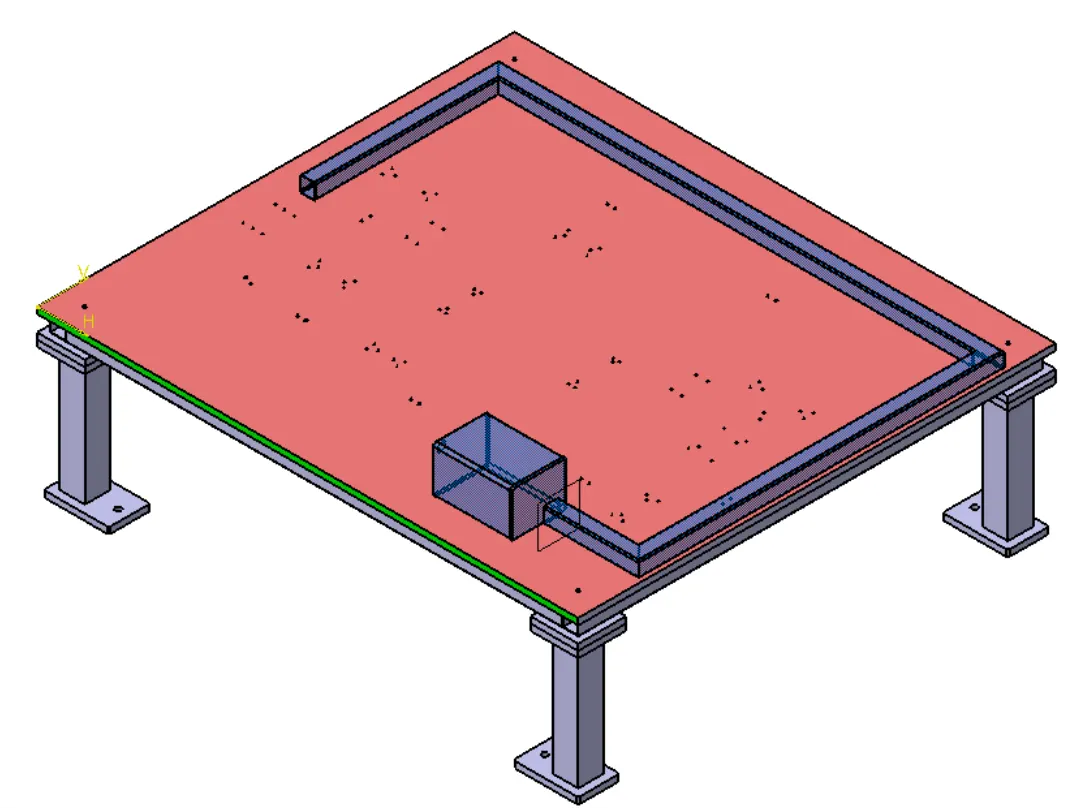
- The Trunking channel is a standard part that will accommodate all the pneumatic and electrical hoses and wires for the units. The trunking channels include all the pressure inlet cables going to the pneumatic parts of the fixture and protects them from damage while the operation is in process.
Valve Box:
- Valve Box is a standard part that will contain all the valves for the pneumatic units. The valve box is the box that includes different solenoid valves. The pneumatic fixtures work on air pressure provided to it. So the arrangement of air pressure inlet and outlet is done within this valve box. The trunking channel includes all the pressure inlet cables going to the pneumatic parts of the fixture and protects them from damage while the operation is in process.
Eye Bolt:
- An eye bolt is a bolt with a loop at one end. They are used to firmly attach a securing eye to a structure, so that ropes or cables may then be tied to it.
- Machinery eye bolts are fully threaded and may have a collar, making them suitable for use with angular loads up to 450. Eyebolts without a shoulder should not be used for angular loads. Heavy forged eye bolts with a continuous eye may be forged with an integral shoulder, allowing their use for heavy off-axis loads.
- These are used for the transporting of the tool by inserting hooks into them. Some, hooks or forklift holes are also provided in some cases for transporting purposes.
Floor Plate:
- Floor plates are grouted to the floor with fixed bolts on the ground.
- These are also called foundation plates. There will be a clearance of 10mm maintained between the pedestal base plate and the floor plate.
- This clearance will be used by the leveling screws, for leveling the entire tool.
- Weld bars are to be used to weld the positions permanently after leveling is done.
- A weld bar is a plate along the sides of the base plate of the pedestal.
Fundamentals Of a Base Plate Design:
The fundamentals of a base plate design are:
- As a designer, it is important to know how big base plate or bigger base welded structure will be handled during the fabrication & handling process. Special care needs to take care of flatness if the base size is very long.
- A base plate size should cover all the units with its outer periphery including the opening.
- A base plate is preferred to be designed with respect to BCS coordinates.
- A base plate should be drilled with datum holes / measuring holes in line with a pitch of 1000 mm in general.
- The number of datum holes depends on the size of the base plate.
- Datum holes should be drilled at nominal values of coordinates, & in terms of 50 x 100. (In general) ex. X=100, Y 600, Z- 250.
- Datum holes should be drilled with dia 100 mm away from other units.
- Datum holes should be covered with cover plates.
- Depending upon the weight, eye bolt size is selected for lifting holes on base plate Generally, 4 eye bolt provision is made You also need to select the location of eye bolt considering the rope/ belts used while shifting the structure or complete fixture are not damaging any units (rest, clamp or location units) nearby.
- Depending upon the component size & weight of the total units you can decide whether you need a fabricated base or just a plate. Mostly fabricated bases are used made of square or rectangular tubes with the plate.
- Most of the OEM makes 4 dowel holes at 4 corners & put small aluminum plate marking X Y&Z coordinates of dowel holes. If the base length is too long few OEMs follow the methodology of having holes at a 500 mm distance.
- The best unit of the fixture must be strong enough so that deflection of the fixture is as minimum as possible. This deflection of a fixture is called because of forces of welding, clamping of the workpiece.
- The base unit of the fixture should have the mass to prevent vibration & chatter.
- The base unit may be built from simple sections so that other units may be fastened with screw or Welded necessary. Those parts of the fixture that remain permanently with the fixture may be welded. Those parts that need frequent changing may be held with screws.
- The base unit should be parallel to the floor to adjust this there should be the provision of the height adjusting mechanism.
HOLE NOMINAL IN BASE PLATE :-
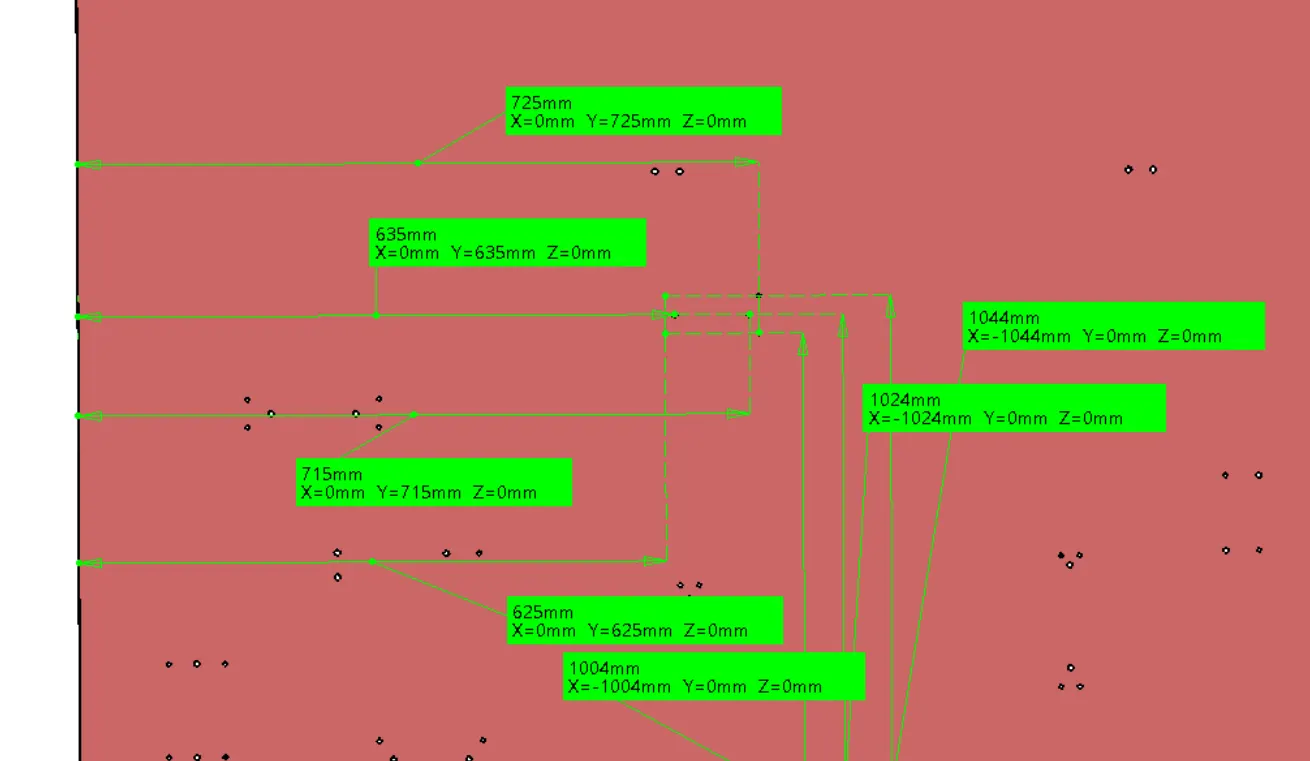
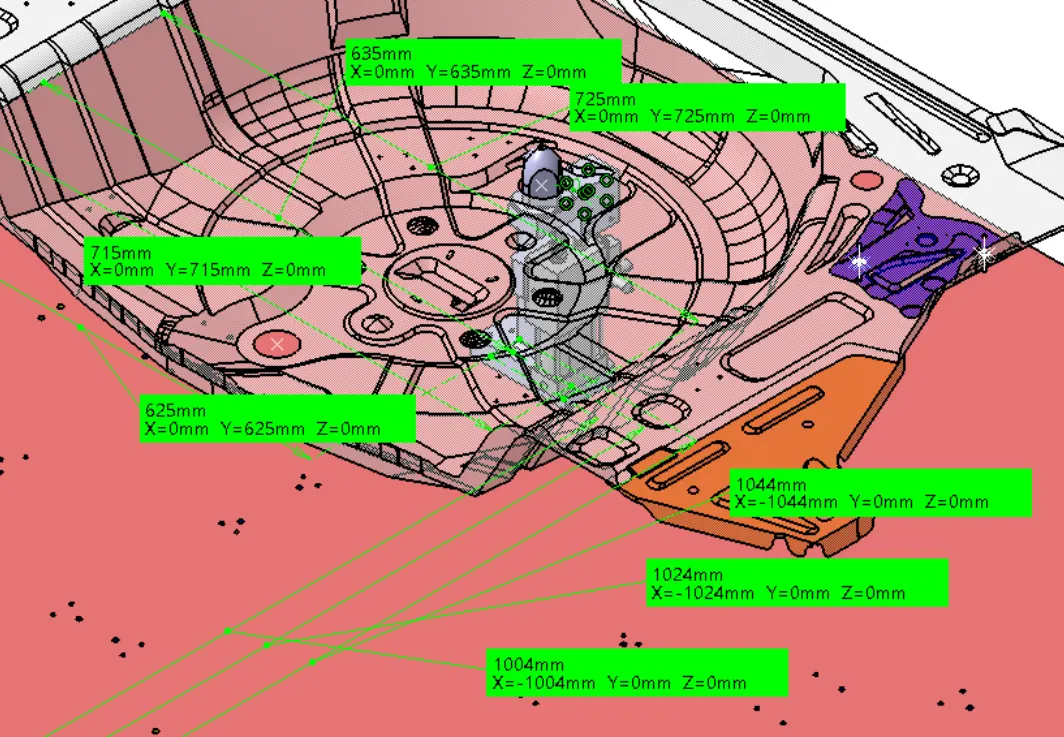
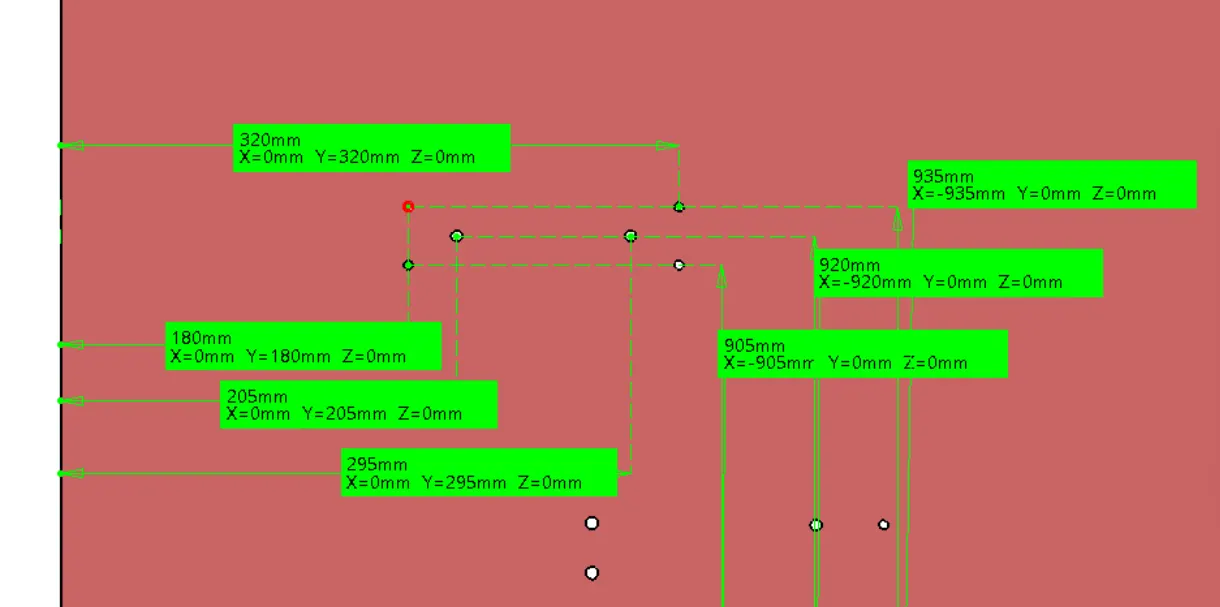
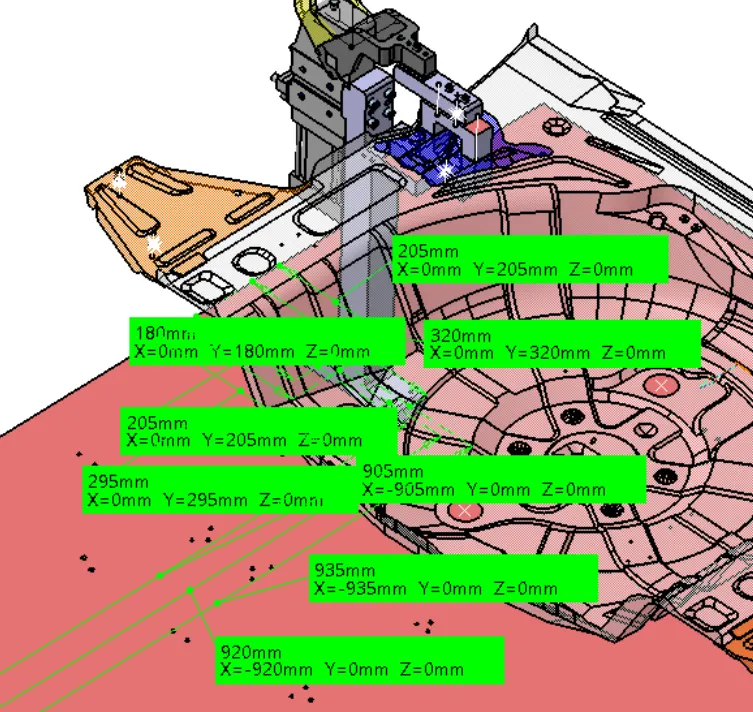
Measuring Dimensions from the Base Plate edges,
1.FIXED PIN UNIT_P00B_Z002_ST01_01_00_FIX_UNIT
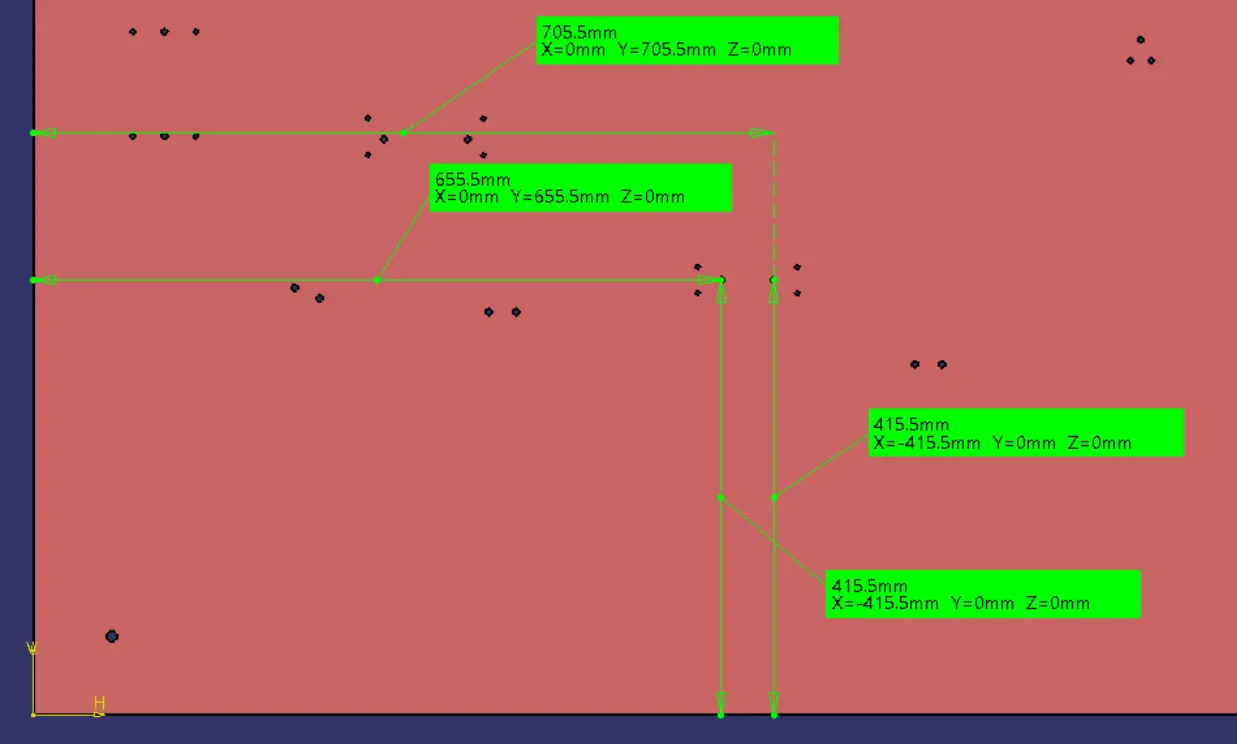
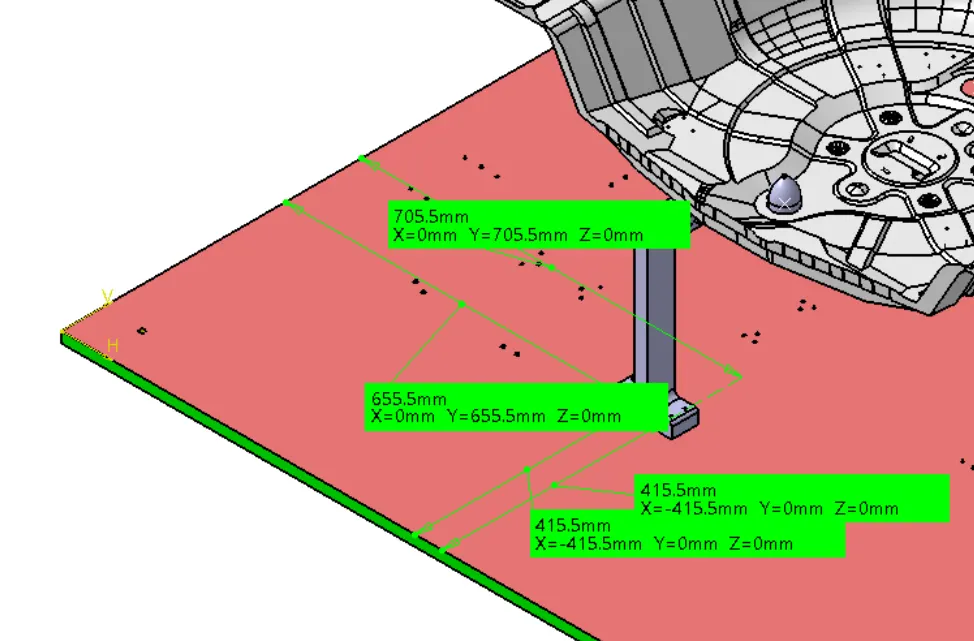
Measuring dowel hole positions from edges
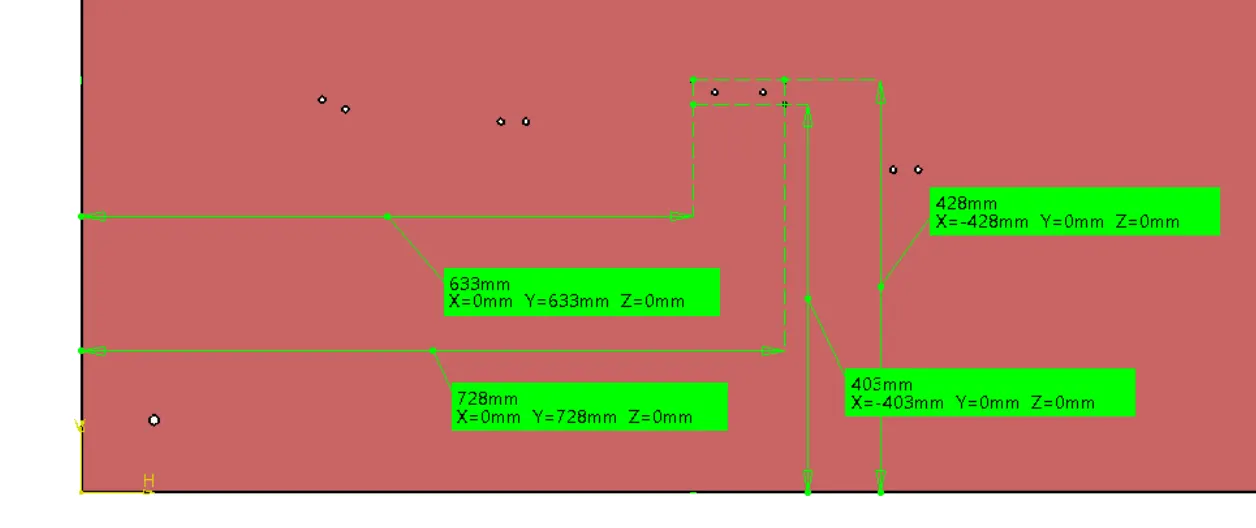
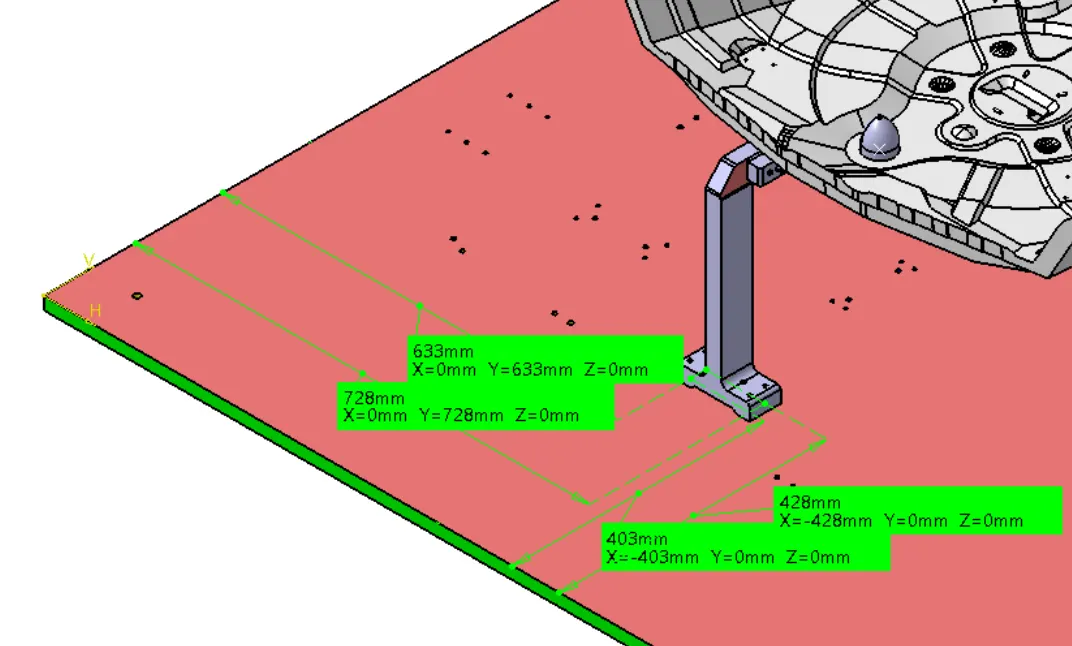
Measuring Thread hole positions from edges .
2. RECTRACTABLE PIN UNIT_P00B_Z002_ST01_02_00_RECTRACTABLE_UNIT
Hole nominality from the base plate edges
3.CLAMP UNIT AND PIN UNIT_P00B_Z002_ST01_03_00_CLAMP_UNIT_1
4.FIXED PIN UNIT_P00B_Z002_ST01_04_00_FIXED_PIN_UNIT
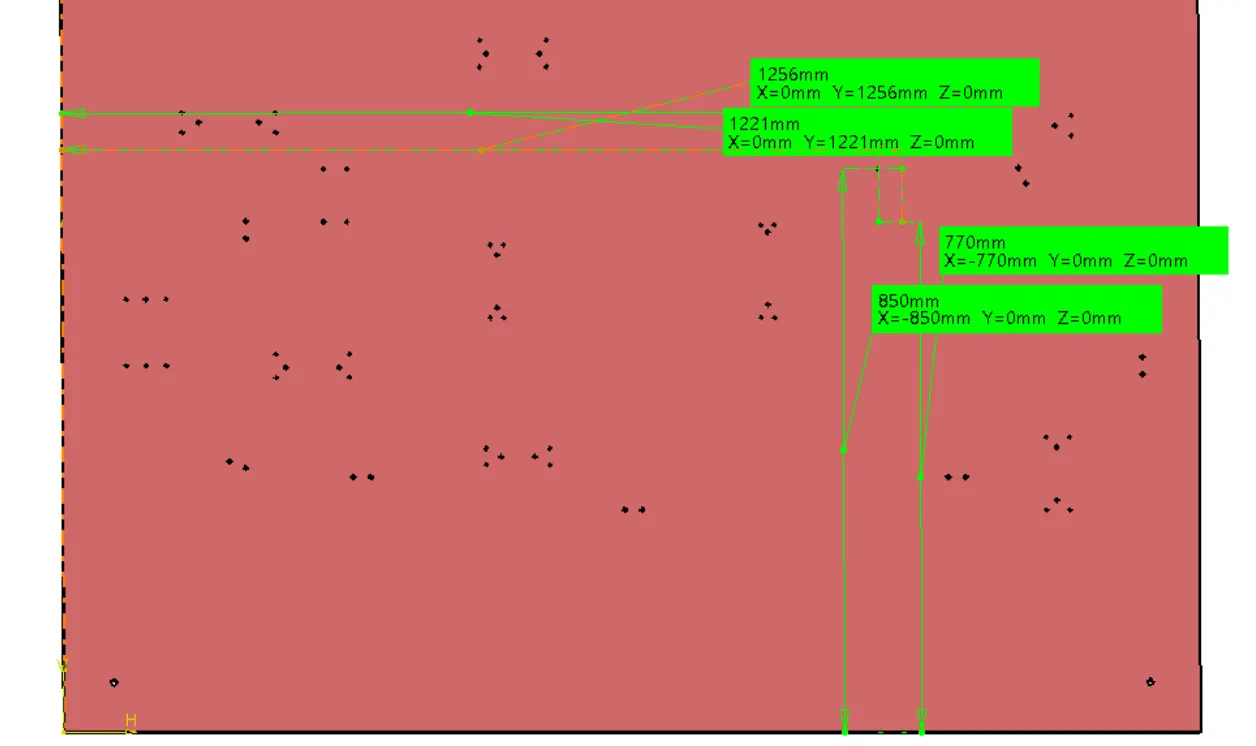
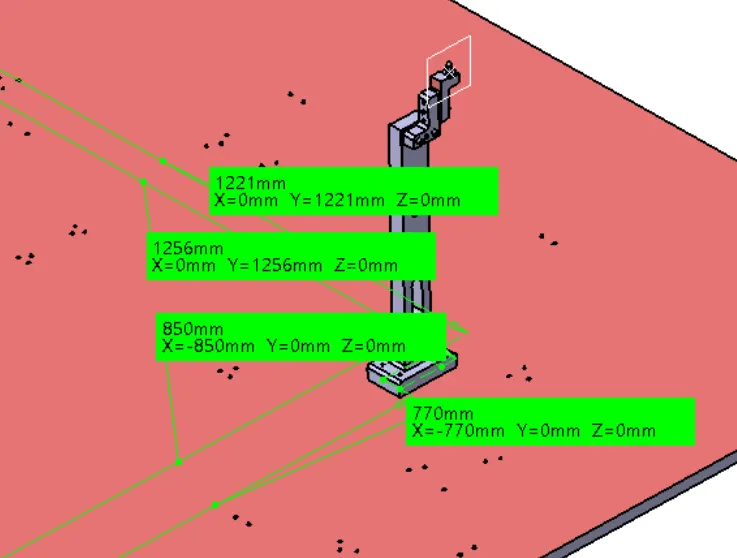
5.CLAMP AND FIXED UNIT _P00B_Z002_ST01_05_00_CLAMP_UNIT_3
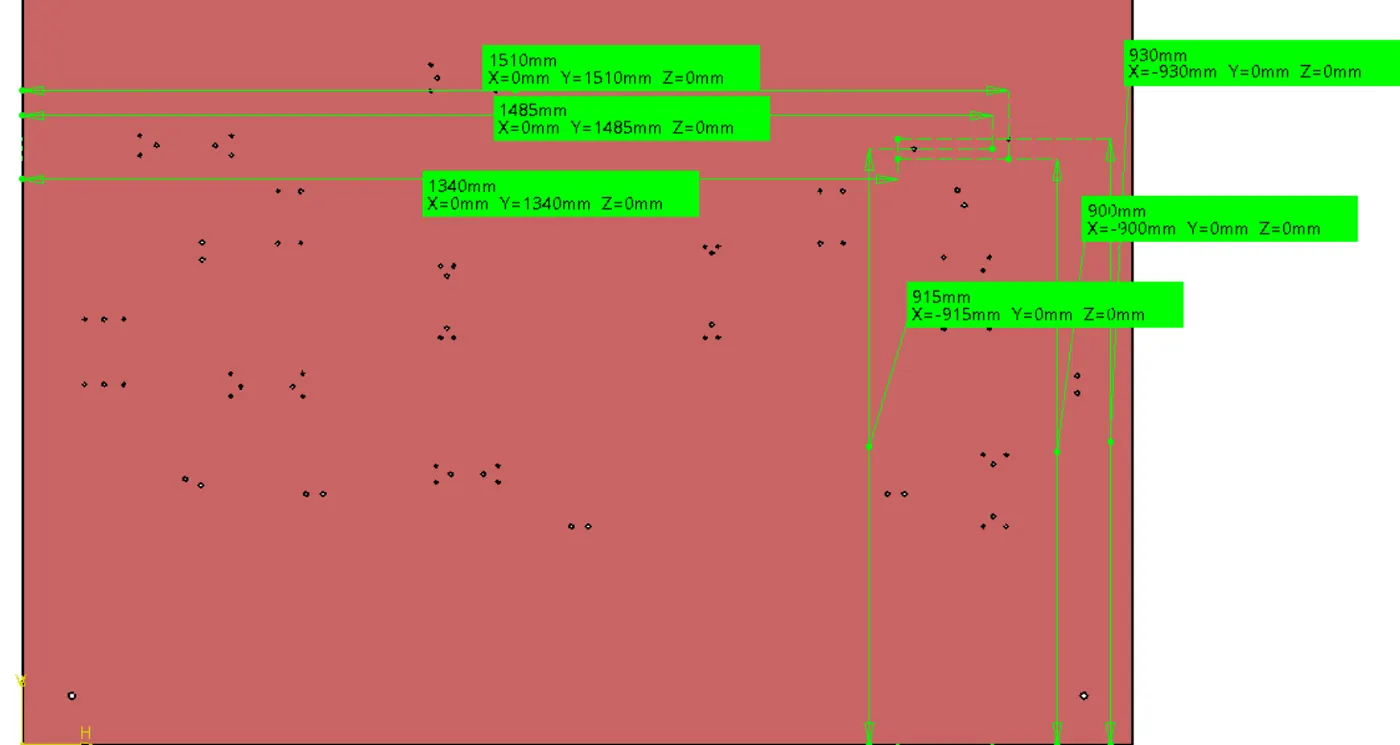
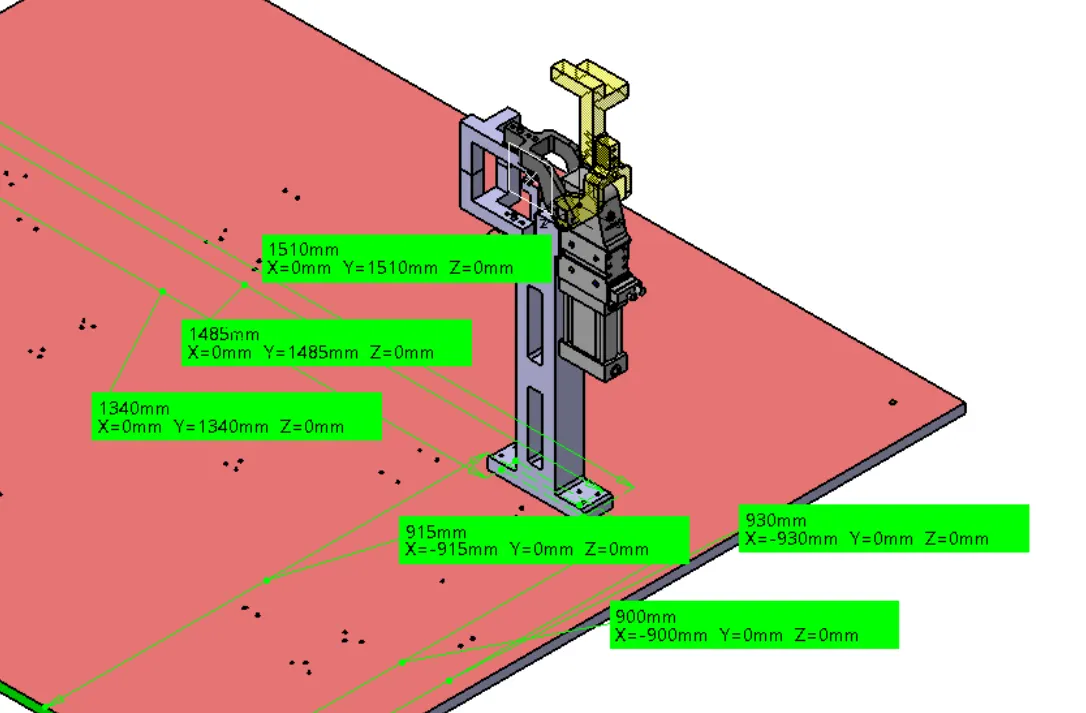
6.REST UNIT_P00B_Z002_ST01_06_00_REST_UNIT_1
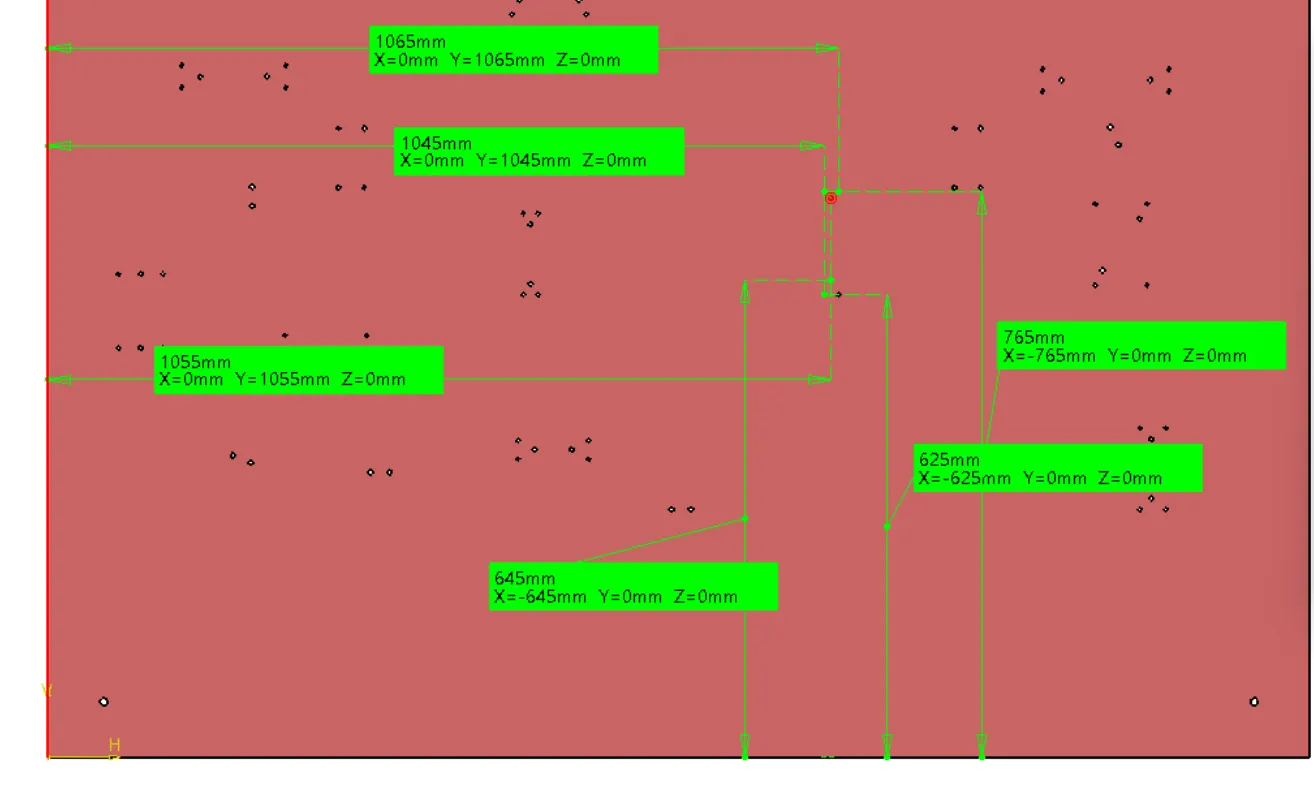
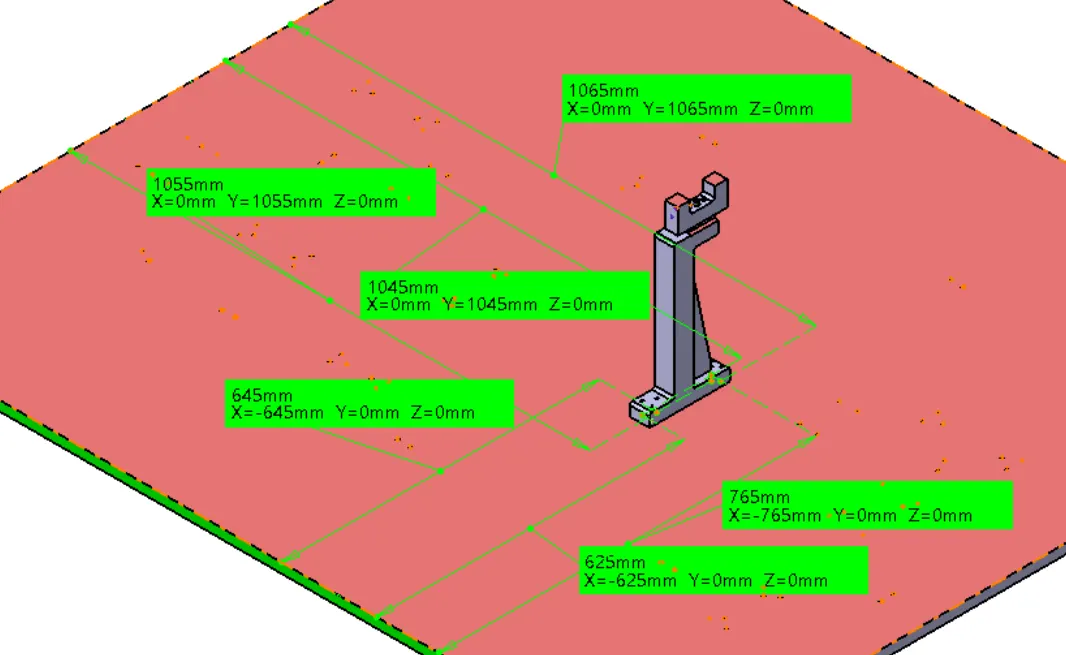
7. REST UNIT_P00B_Z002_ST01_07_00_REST_UNIT_2
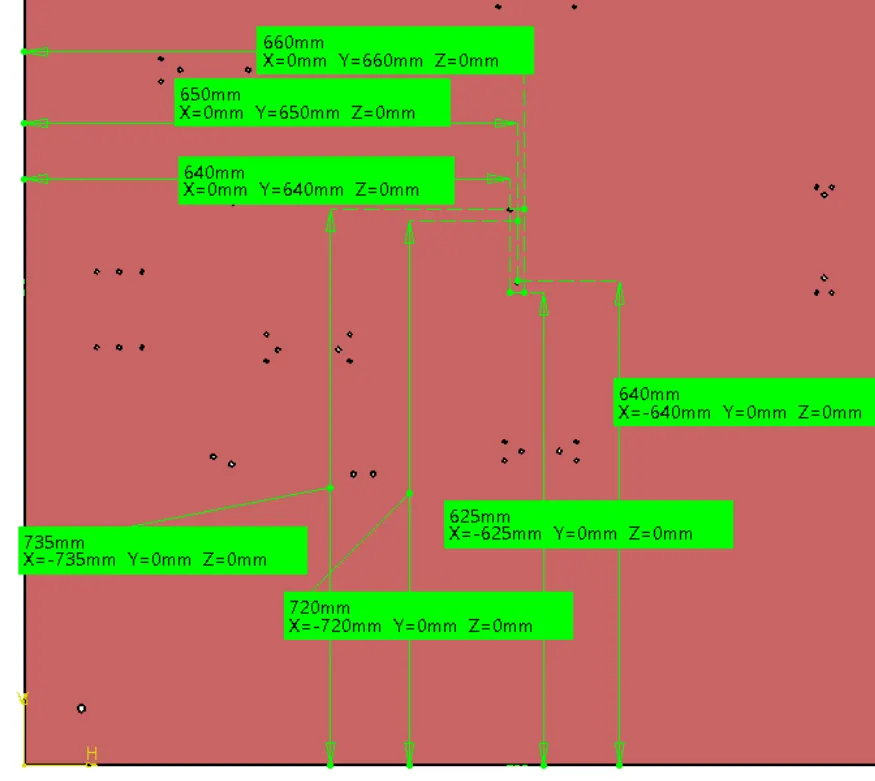
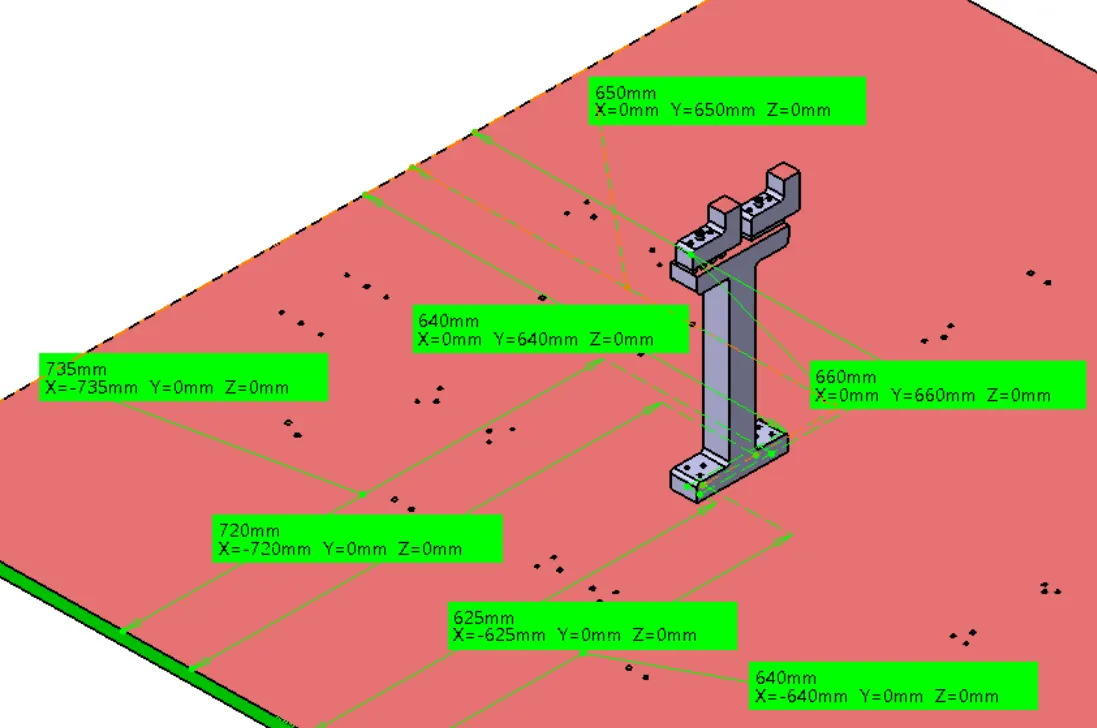
8.CLAMP AND PIN UNIT_P00B_Z002_ST01_08_00_CLAMP_UNIT_3
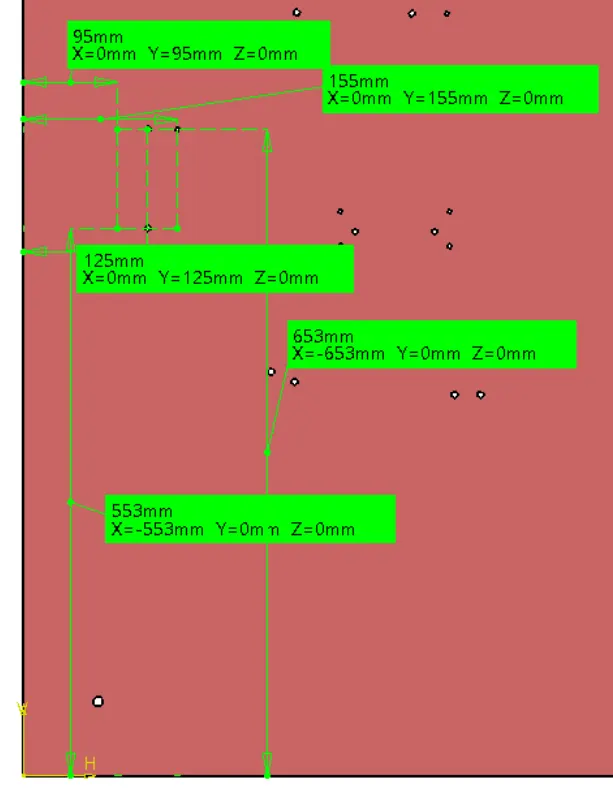
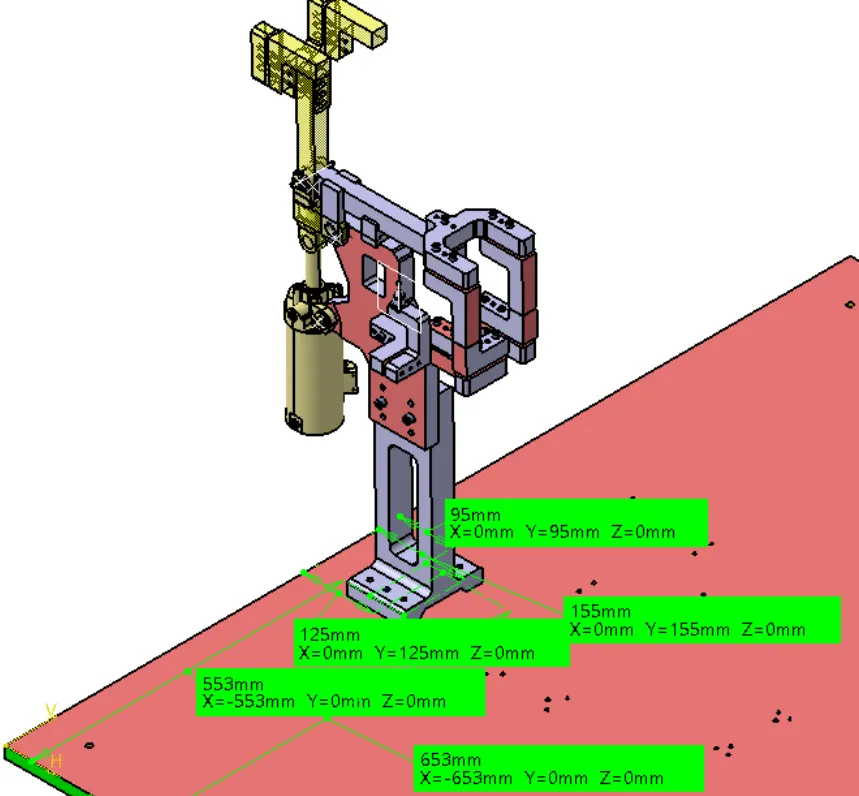
9. CLAMP AND PIN UNIT_P00B_Z002_ST01_09_00_CLAMP_UNIT_4
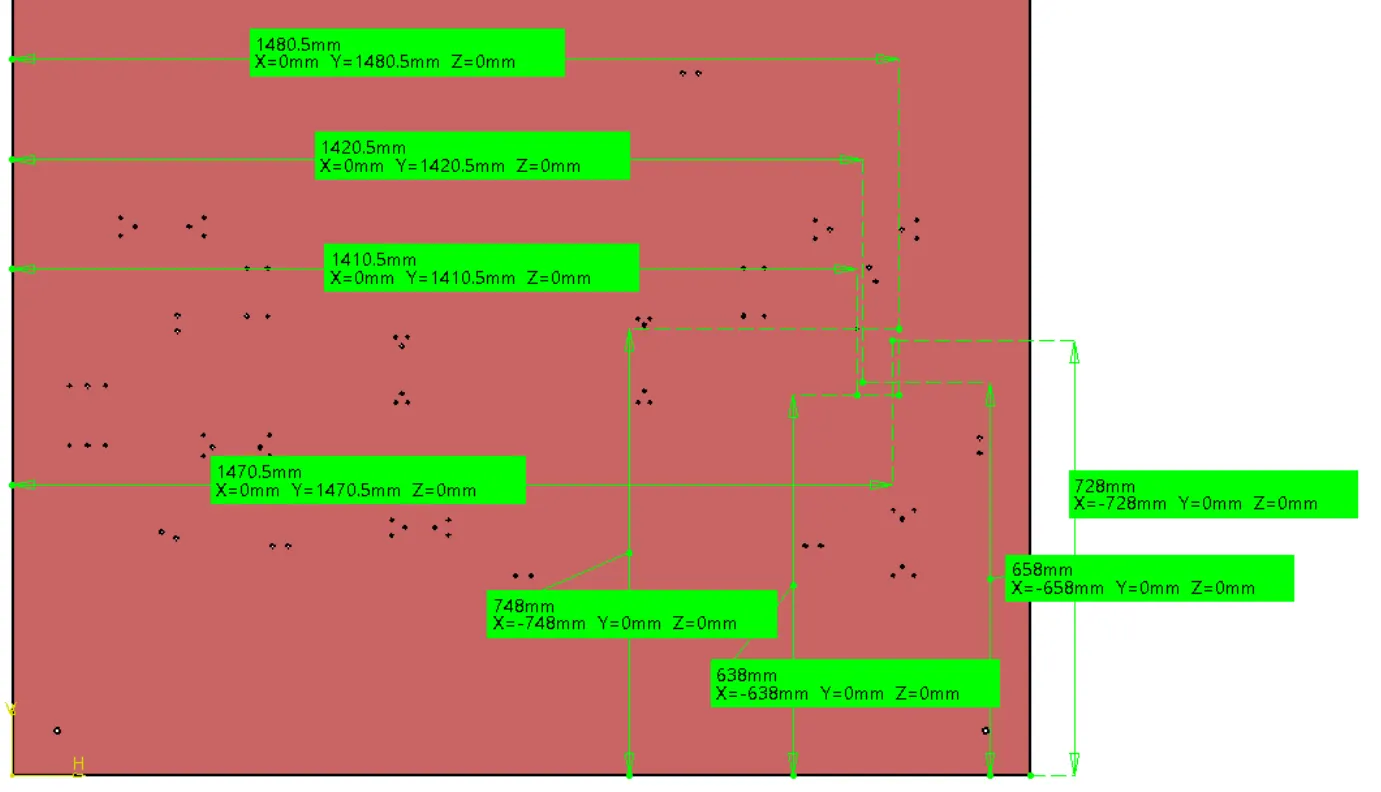
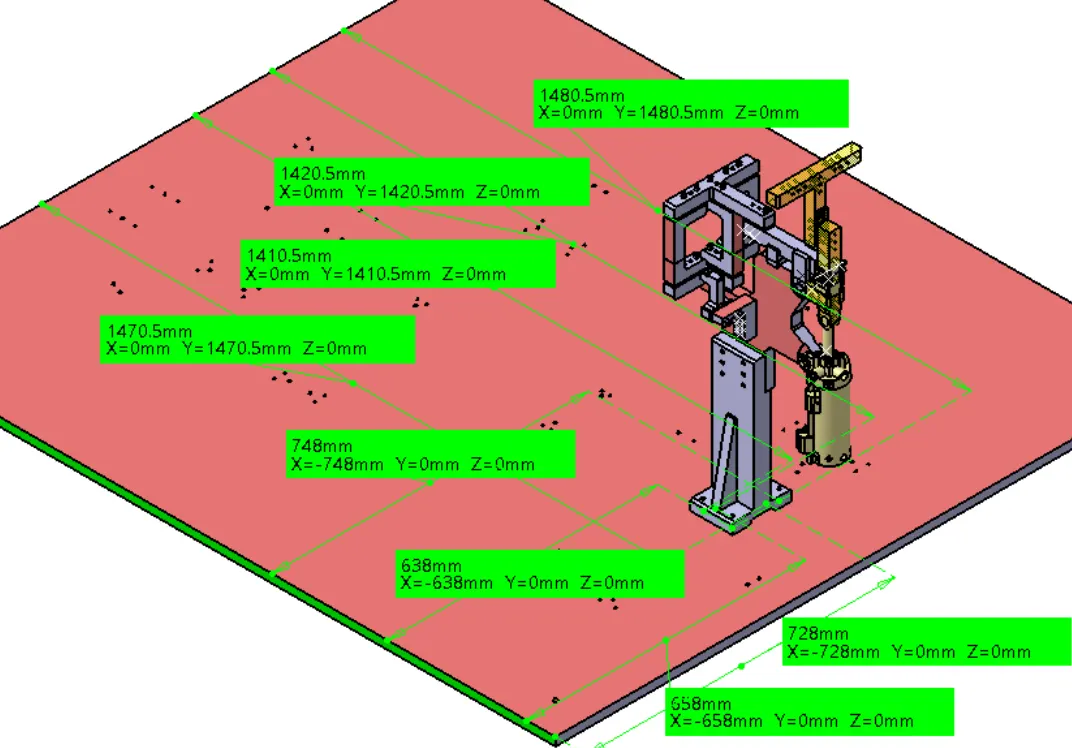
10.FIXED PIN UNIT_P00B_Z002_ST01_10_00_FIX_UNIT
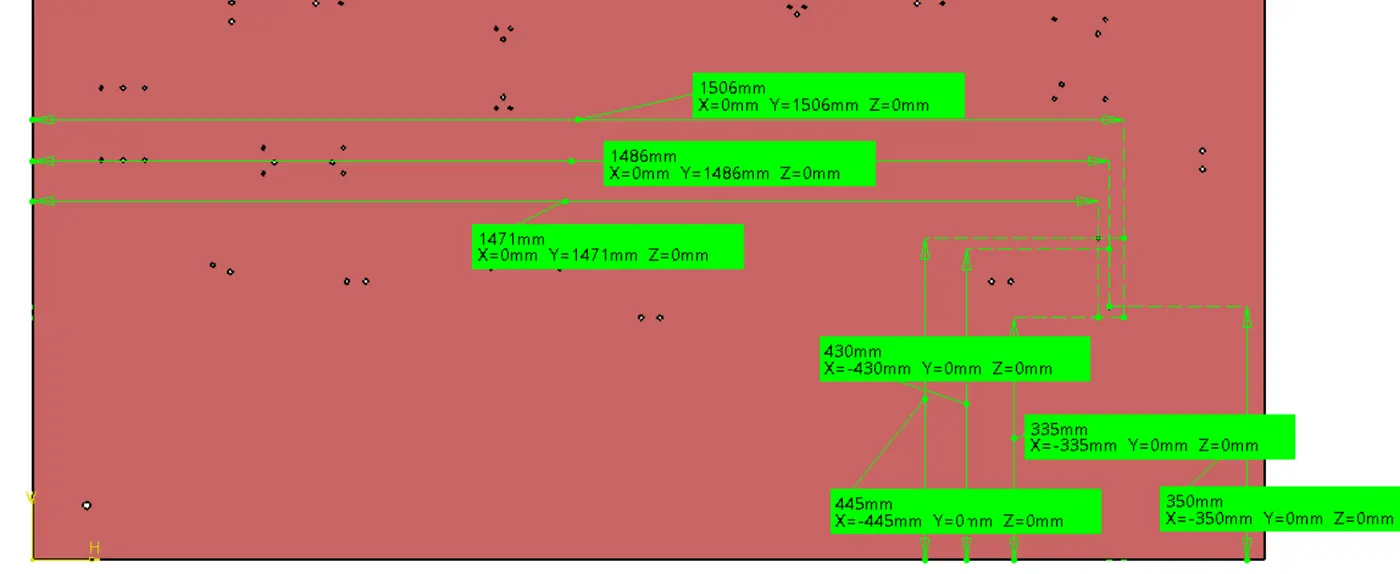
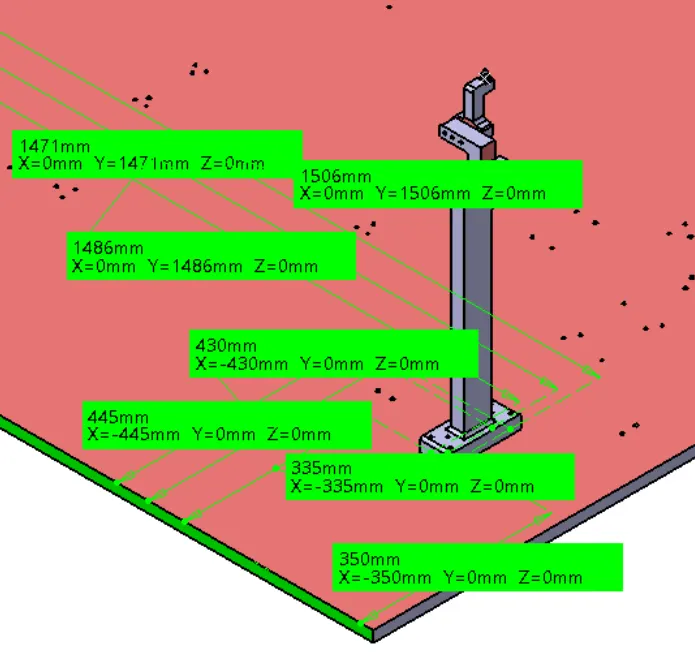
11.FIXED PIN UNIT_P00B_Z002_ST01_11_00_FIXED_PIN_UNIT
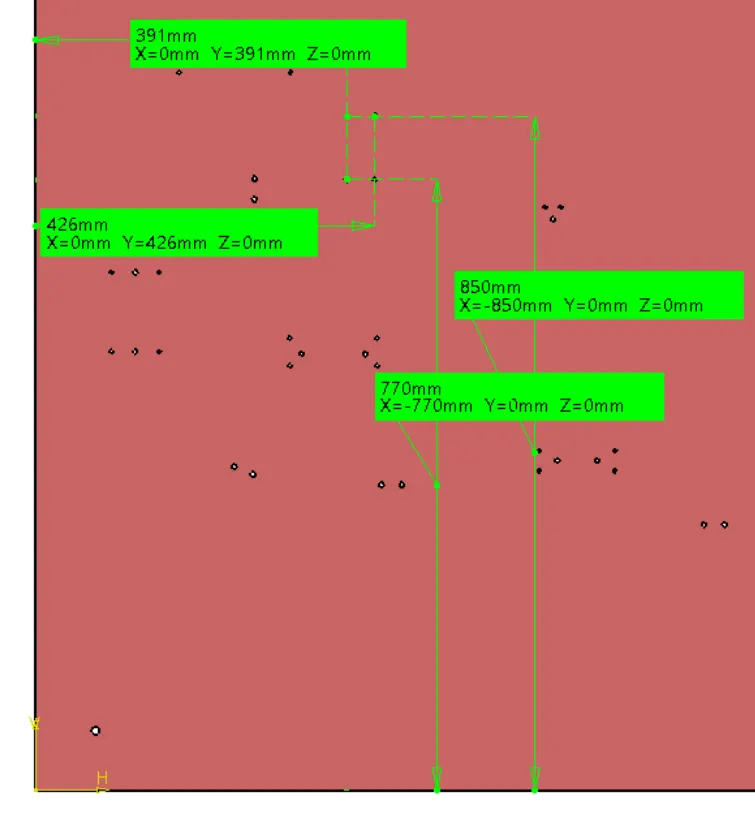
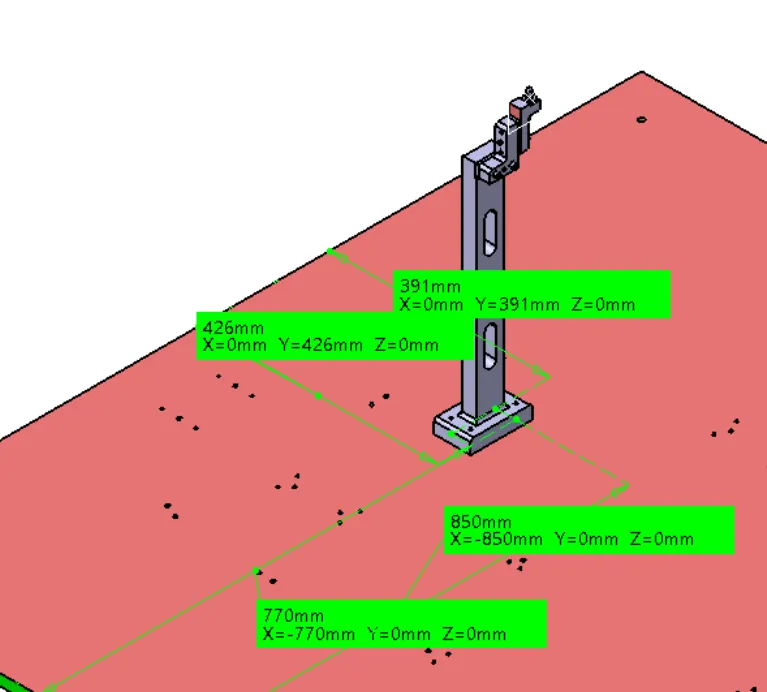
12.FIXED PIN UNIT_P00B_Z002_ST01_12_00_FIX_UNIT
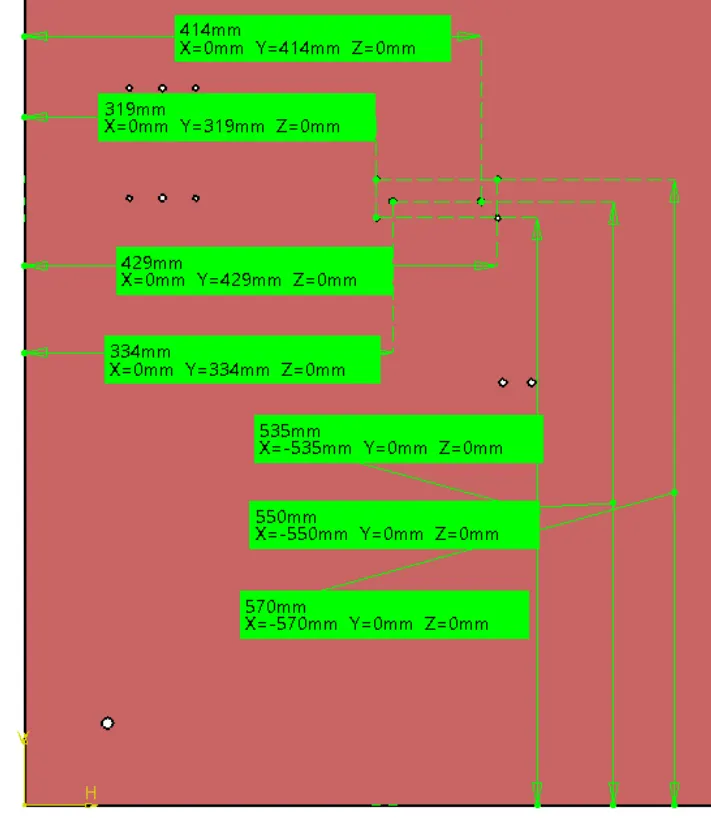
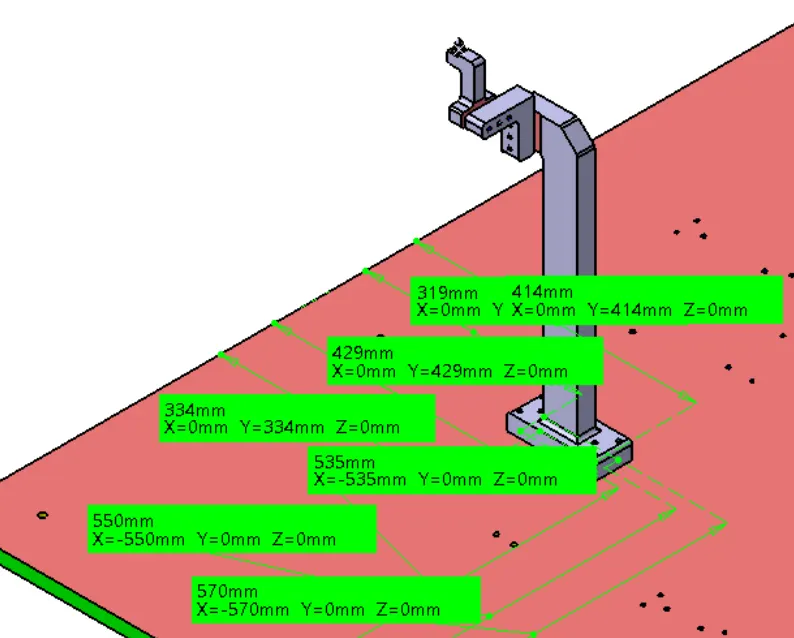
MACHINED SURFACES IN ALL UNITS
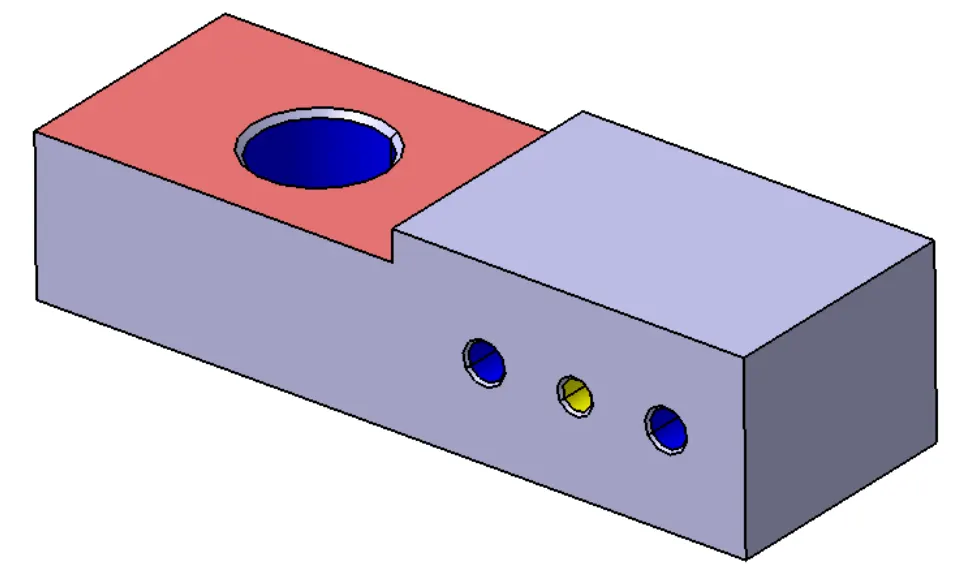
1.FIXED PIN UNIT_P00B_Z002_ST01_01_00_FIX_UNIT
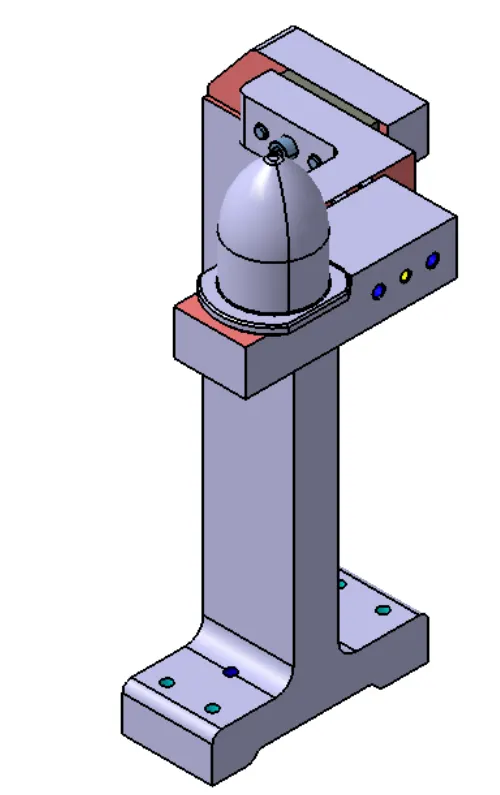
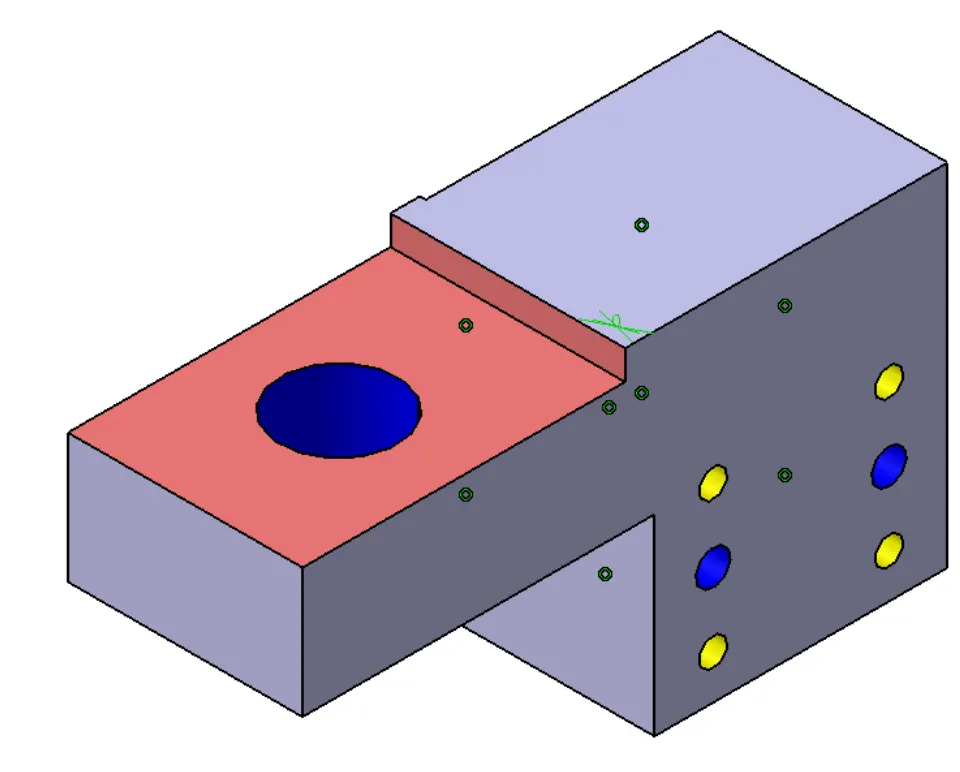
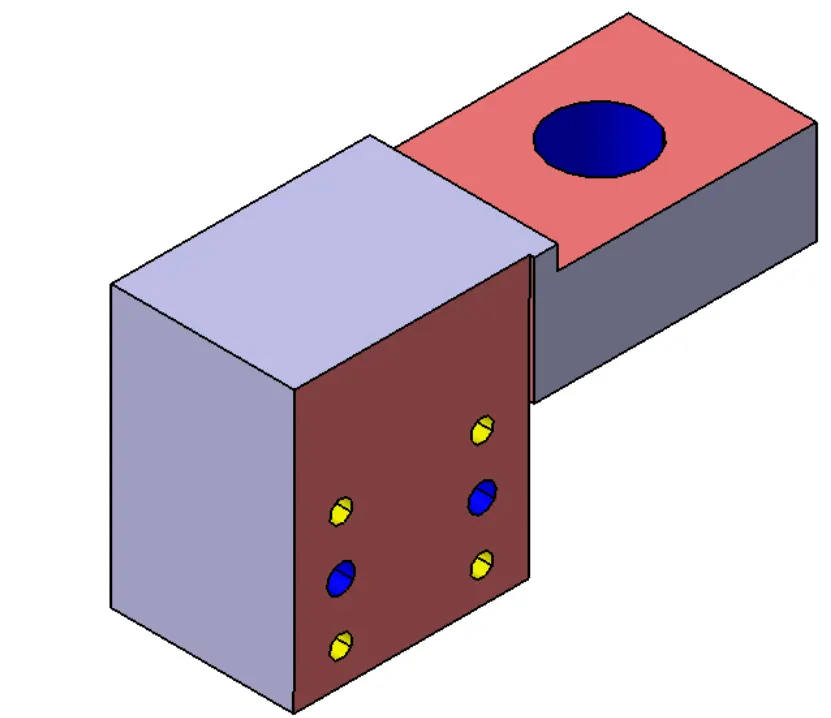
A. RAISER(P00B_Z002_ST01_01_04_RAISER)
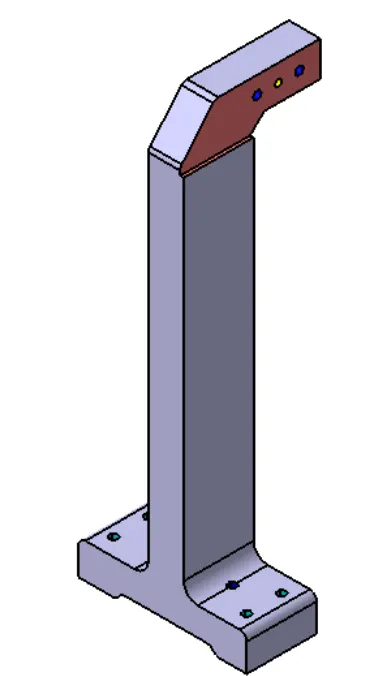
- L BLOCK MOUNTING AREA
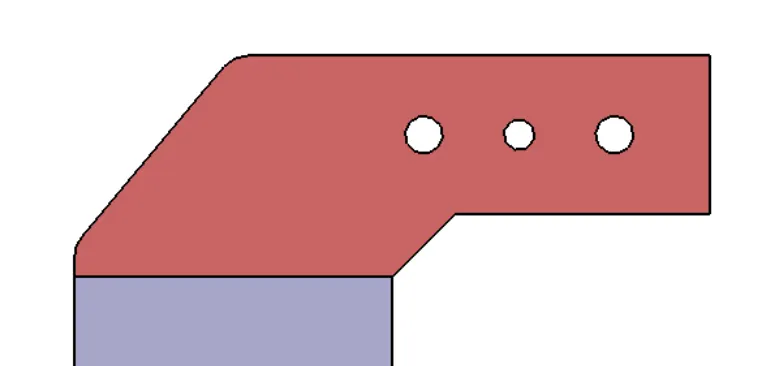
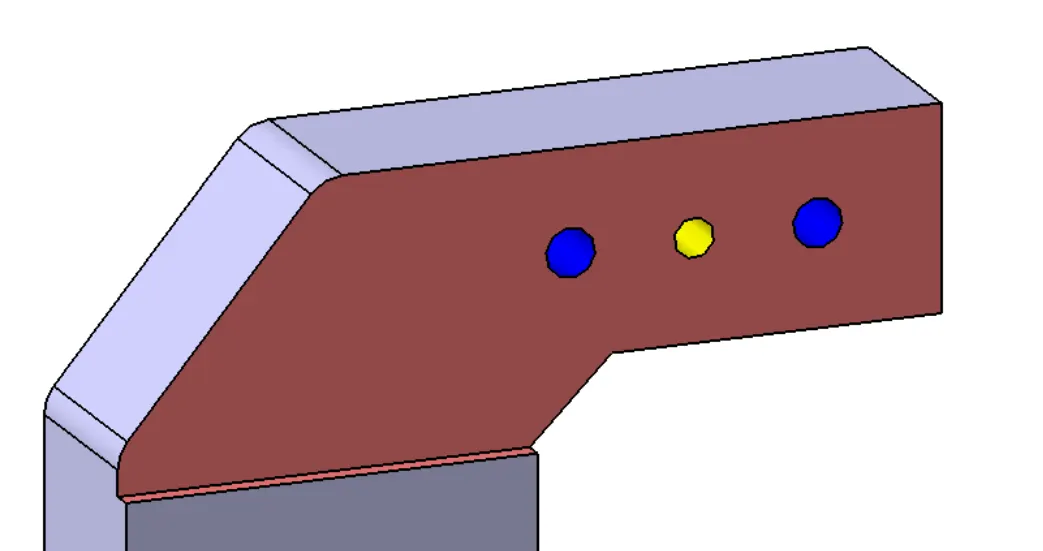
- BASE PLATE MOUNTING REGION
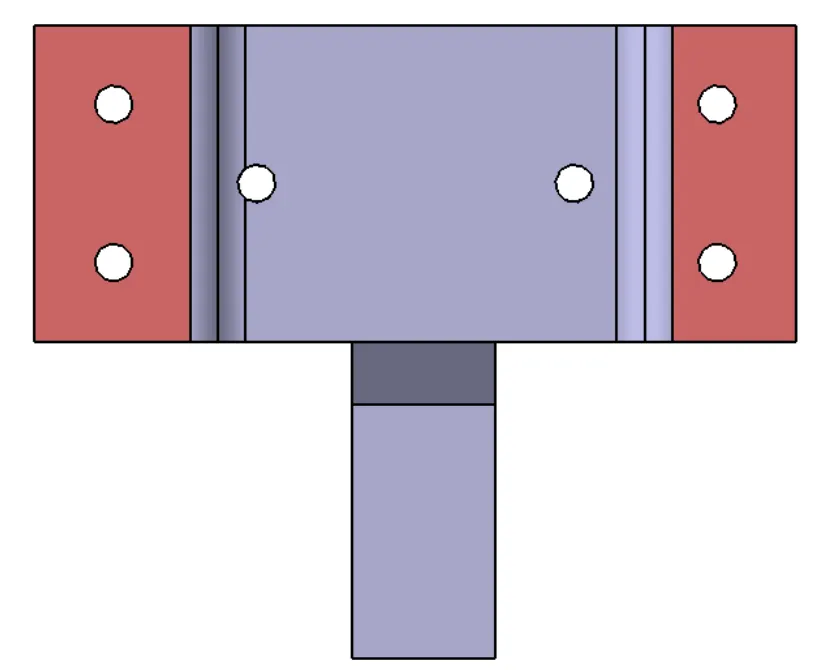
B. L_BLOCK(P00B_Z002_ST01_01_03_L_BLOCK)
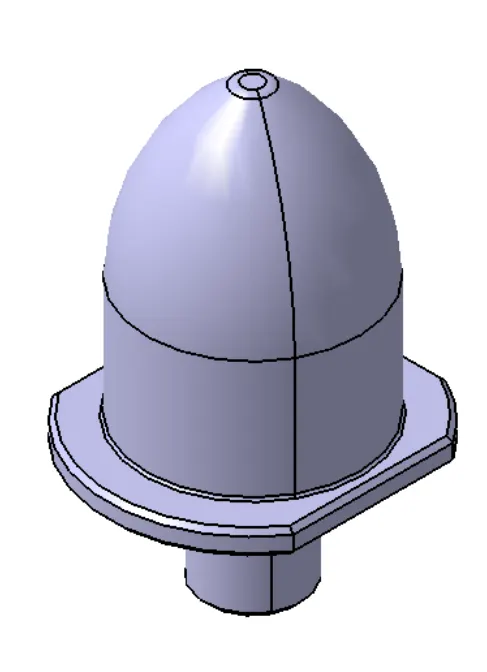
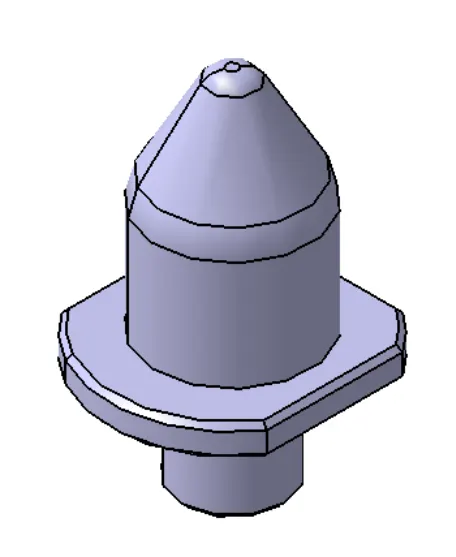
C. PIN RETAINER(P00B_Z002_ST01_01_02_PIN_RETAINER)
D. PIN (P00B_Z002_ST01_01_01_PIN)
2. RECTRACTABLE PIN UNIT_P00B_Z002_ST01_02_00_RECTRACTABLE_UNIT
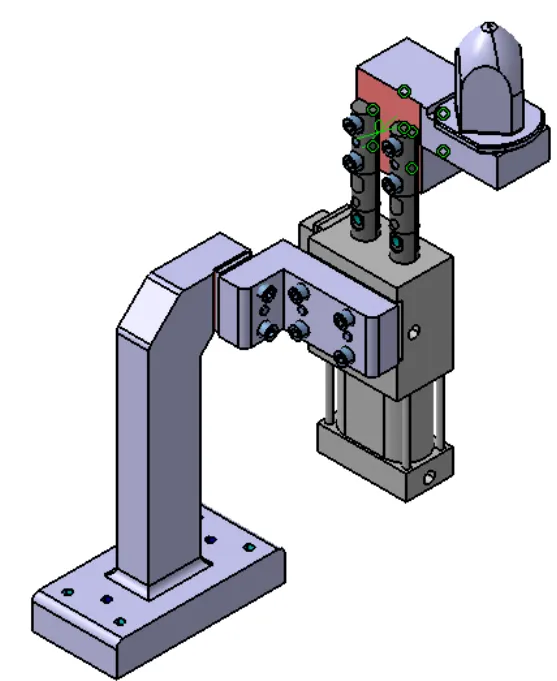
A. RAISER()
A. RAISER(P00B_Z002_ST01_02_04_RAISER)
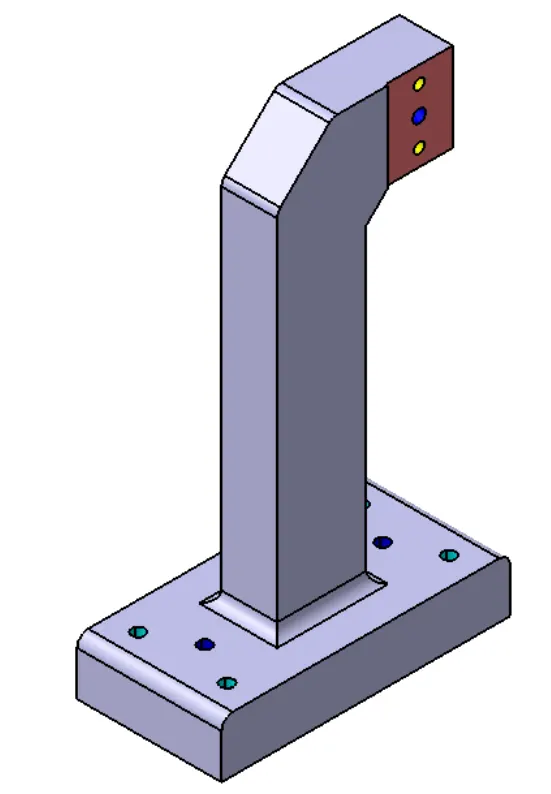
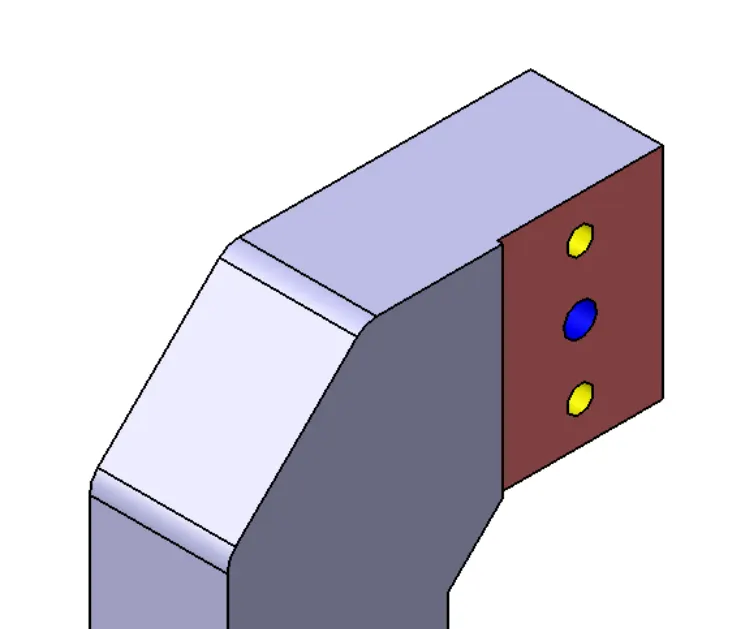
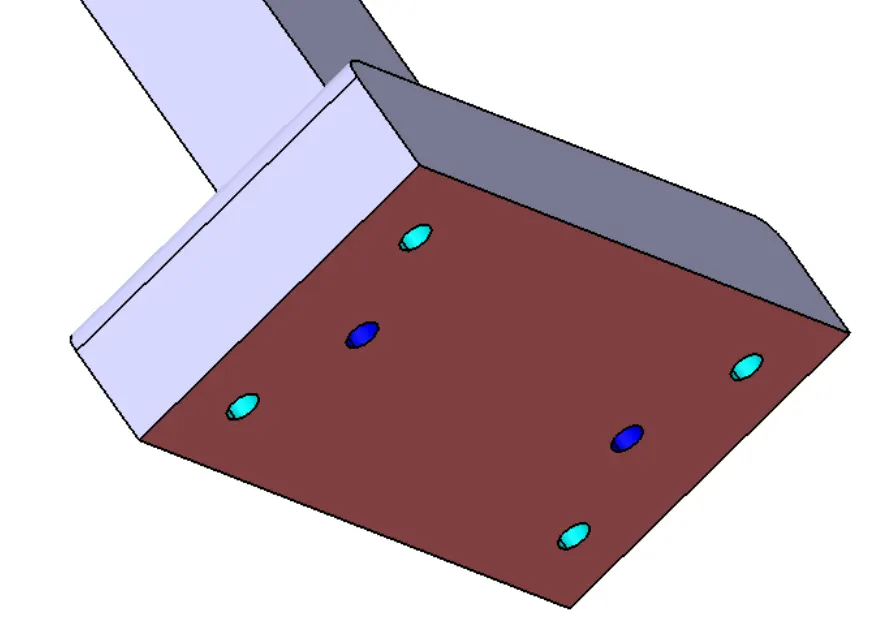
B. L_BLOCK(P00B_Z002_ST01_02_03_L_BLOCK)
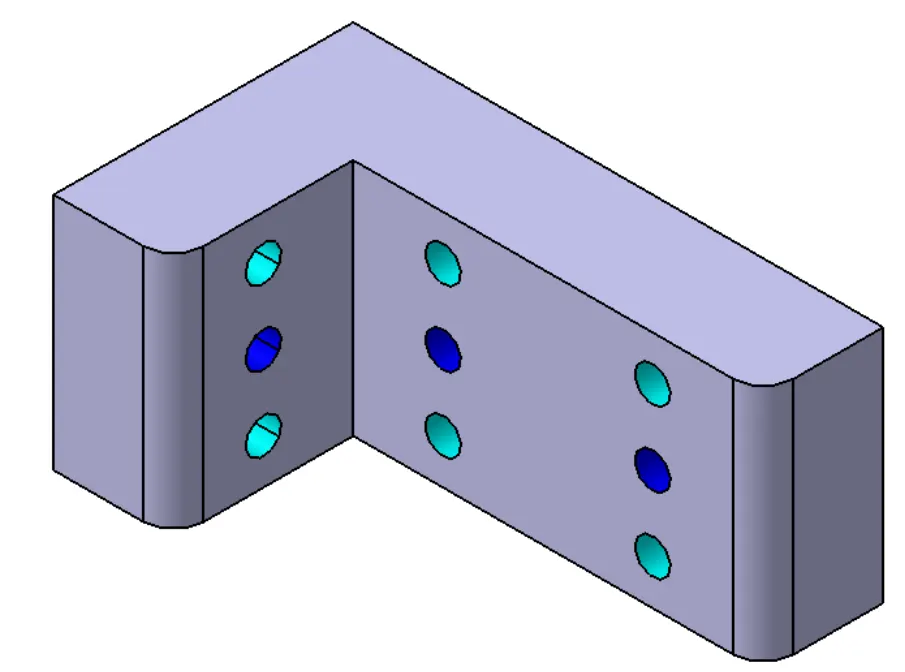
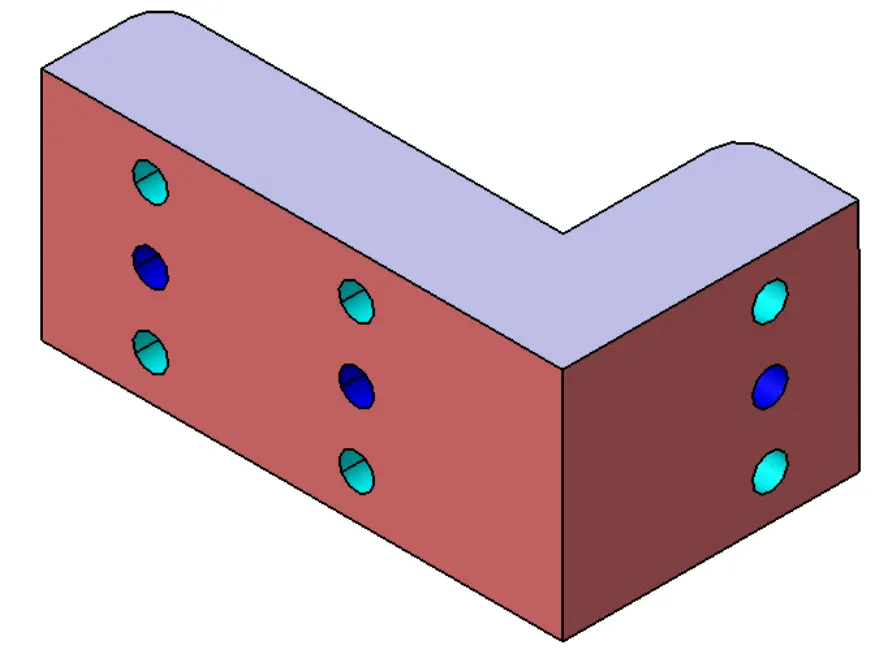
C. PIN RETAINER(P00B_Z002_ST01_02_02_PIN_RETAINER)
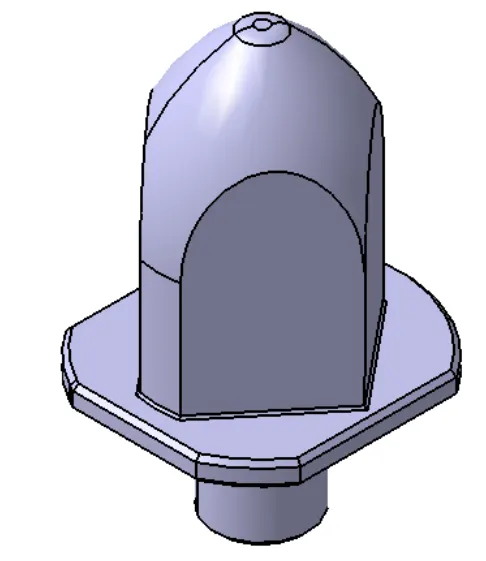
D. DIMOND PIN(P00B_Z002_ST01_02_01_PIN)
3. CLAMP AND PIN UNIT_P00B_Z002_ST01_03_00_CLAMP_UNIT_1
A. RAISER(P00B_Z002_ST01_03_02_RAISER)
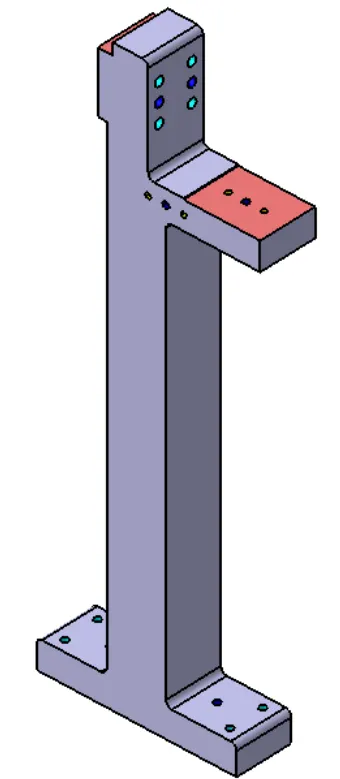
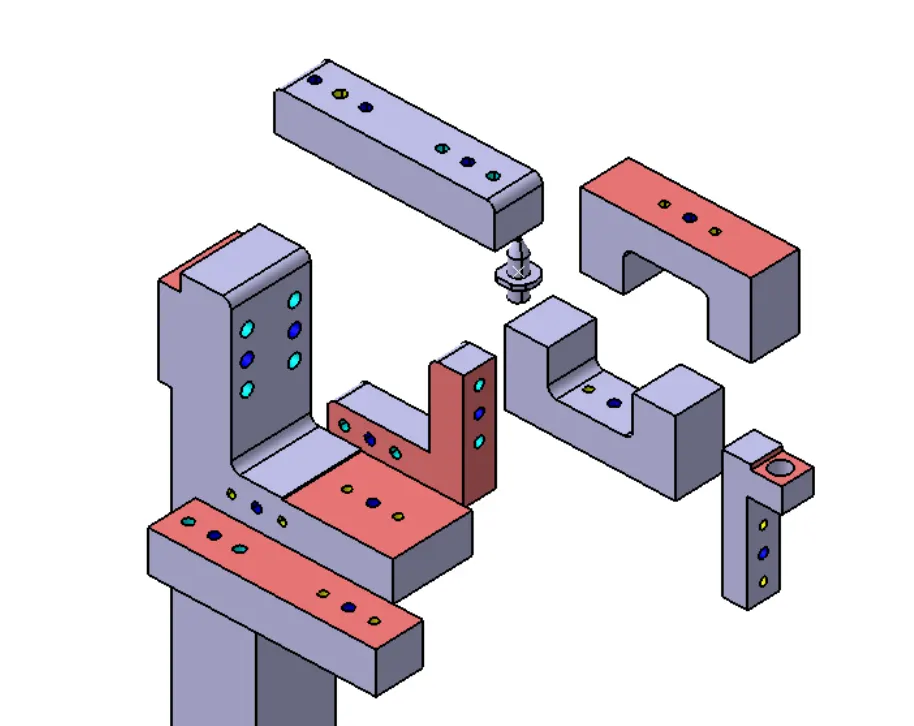
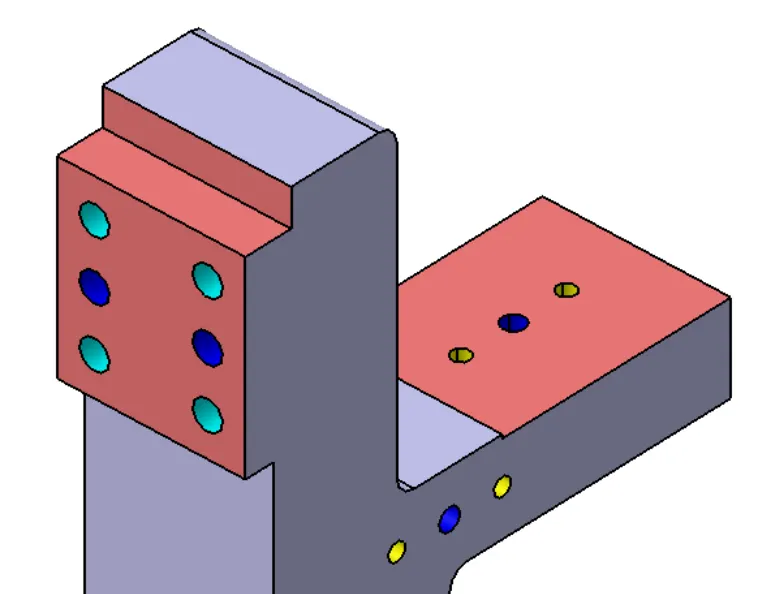
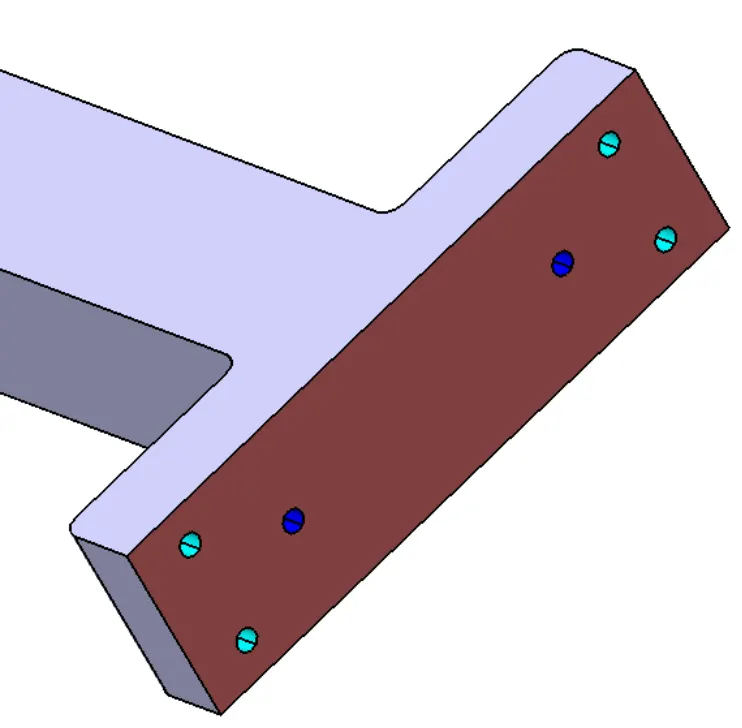
B. REST MYLAR(P00B_Z002_ST01_03_01_REST_MYLAR)
C. FINGER(P00B_Z002_ST01_03_03_FINGER)
D. L_BLOCK(P00B_Z002_ST01_03_04_L_BLOCK)
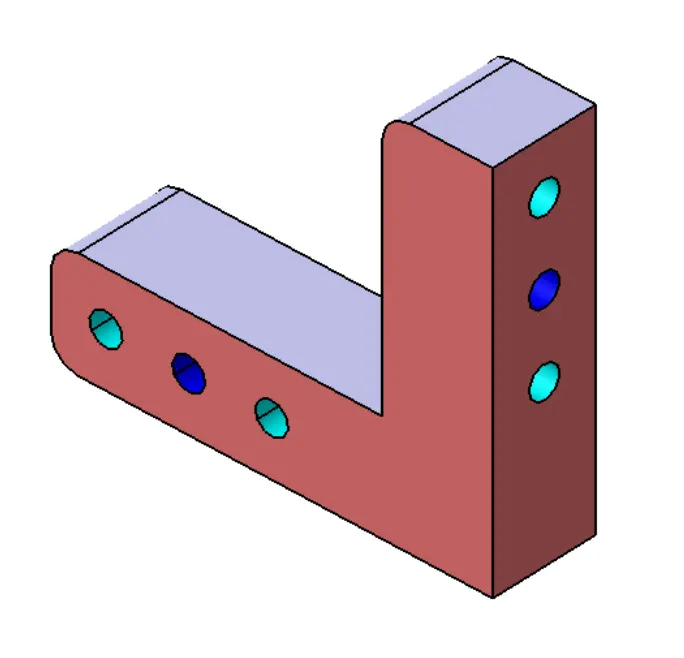
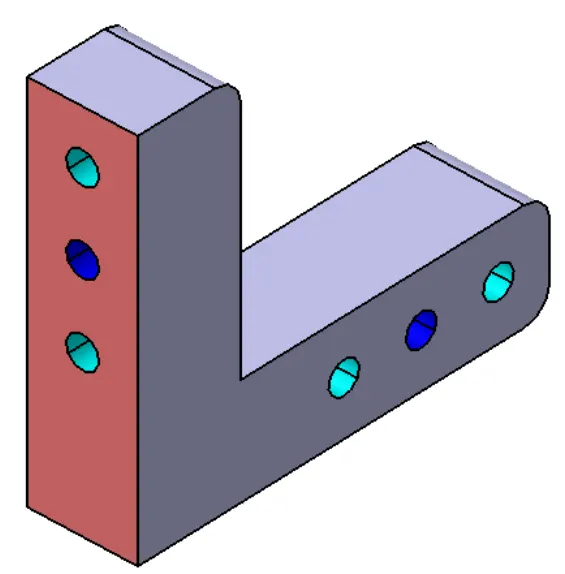
E. PIN (P00B_Z002_ST01_03_05_PIN)
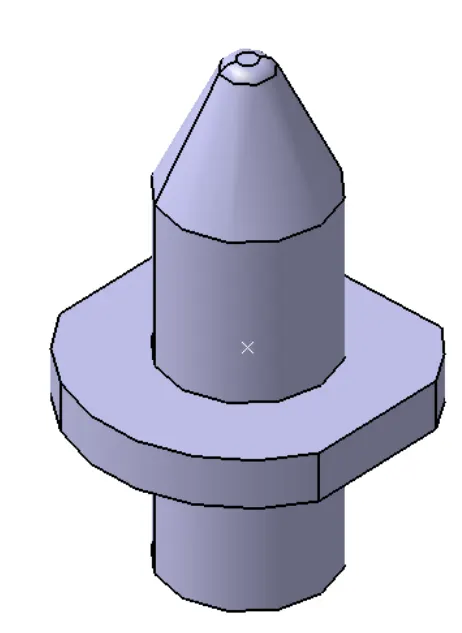
F. PIN RETAINER(P00B_Z002_ST01_03_05_PIN_RETAINER)
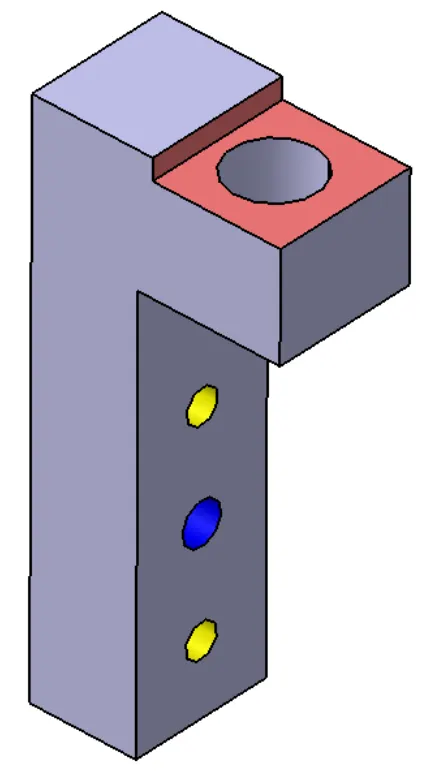
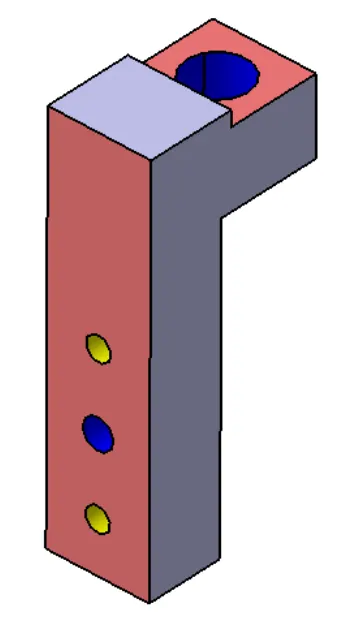
G. CLAMP MYLAR(P00B_Z002_ST01_03_06_CLAMP_MYLAR)
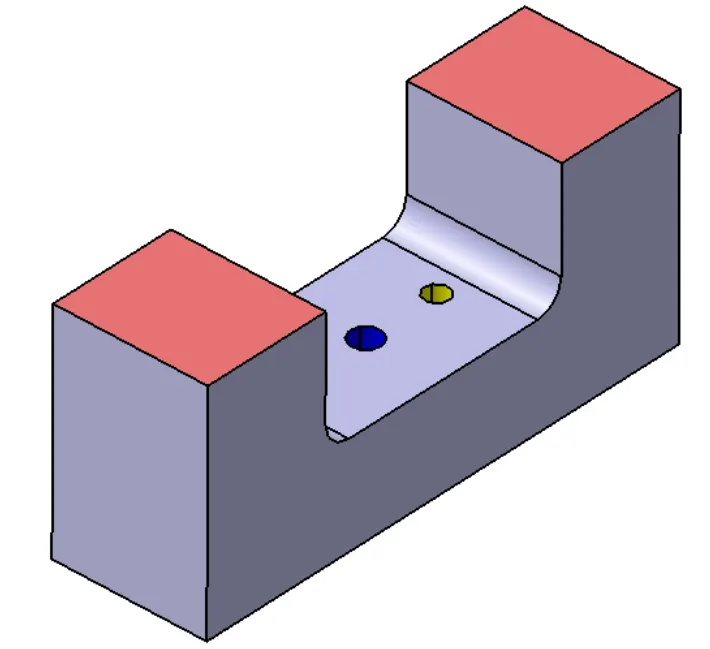
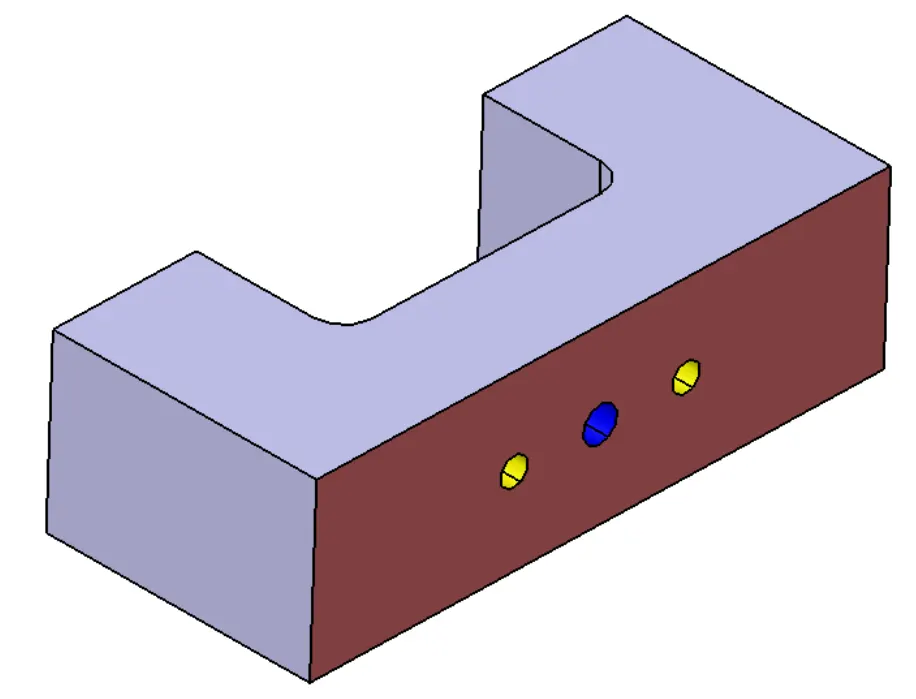
4.FIXED PIN UNIT_P00B_Z002_ST01_04_00_FIXED_PIN_UNIT
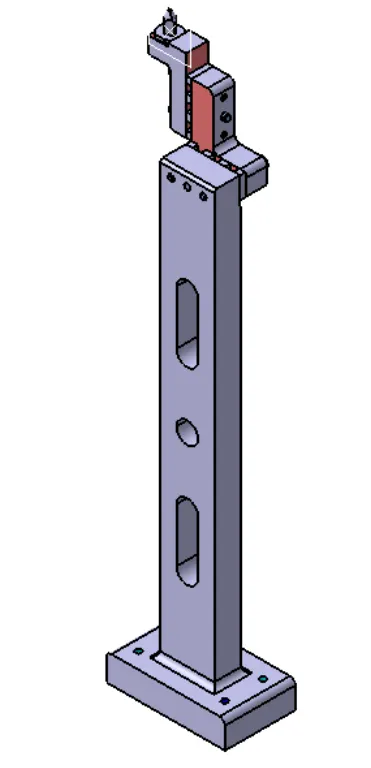
A. RAISER(P00B_Z002_ST01_04_04_RAISER)
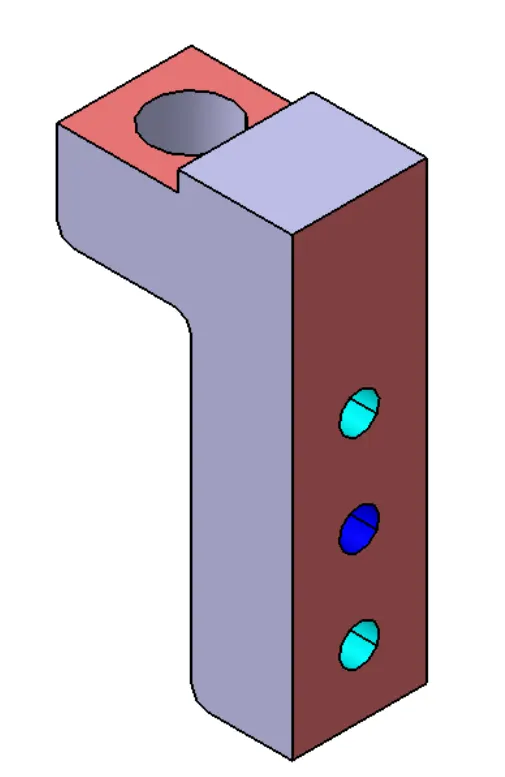
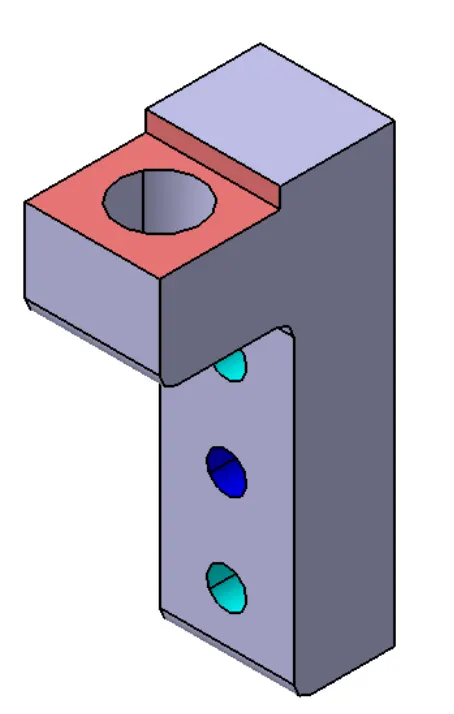
B. L BLOCK(P00B_Z002_ST01_04_01_L_BLOCK)
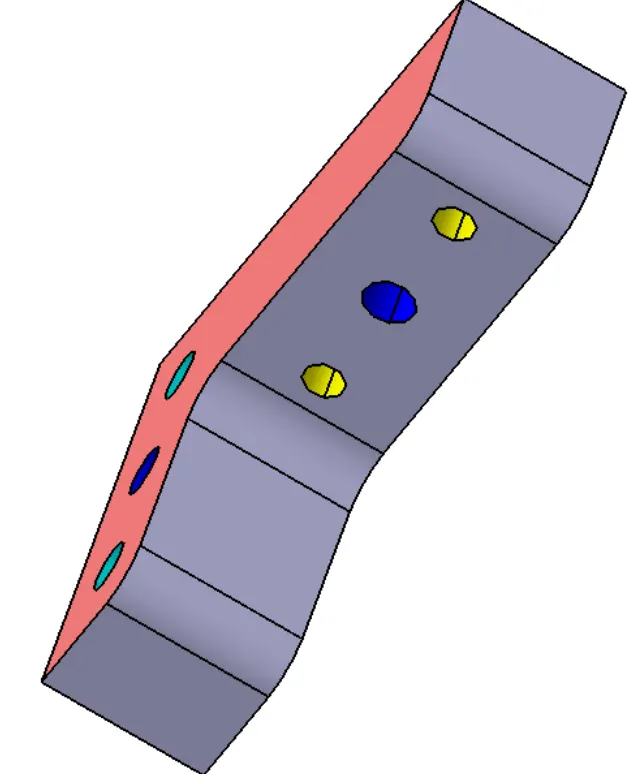
C. PIN RETAINER(P00B_Z002_ST01_04_03_PIN_RETAINER)
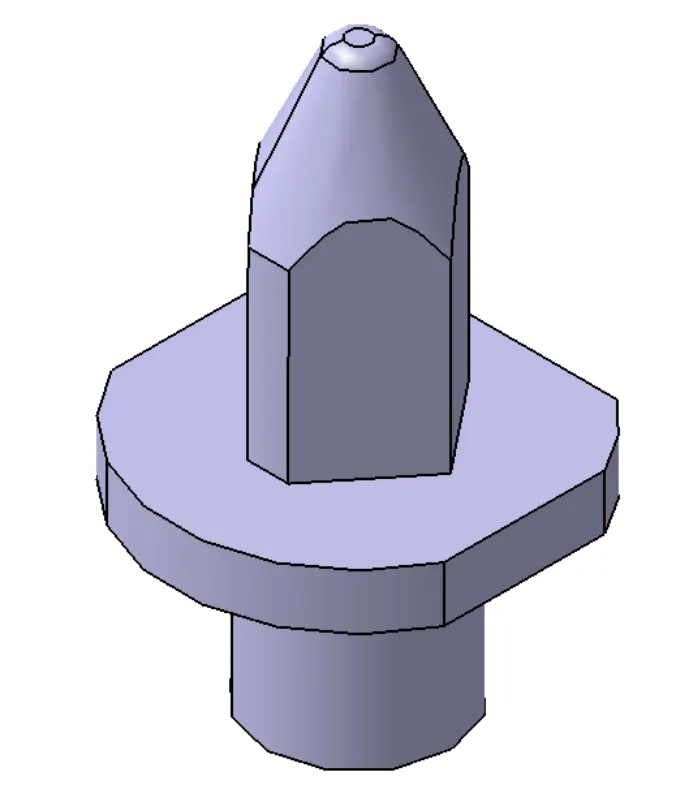
D. PIN(P00B_Z002_ST01_04_02_PIN)
5.CLAMP AND FIXED UNIT _P00B_Z002_ST01_05_00_CLAMP_UNIT_3
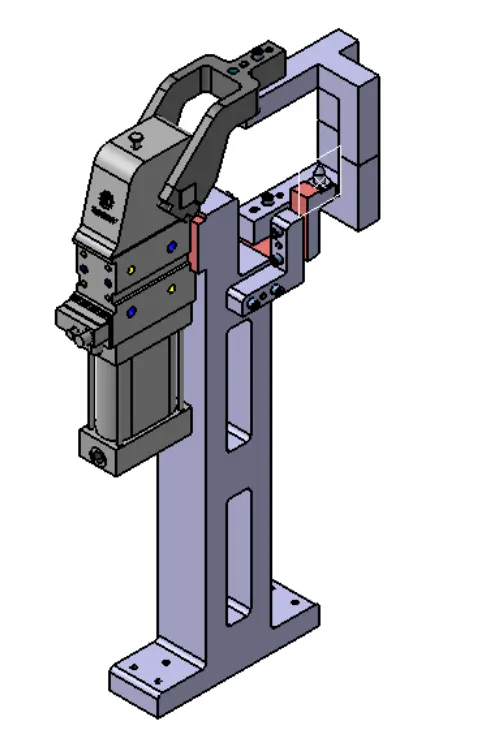
A. RAISER(P00B_Z002_ST01_05_02_RAISER)
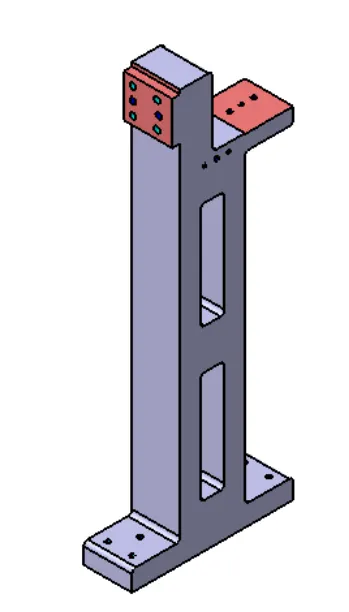
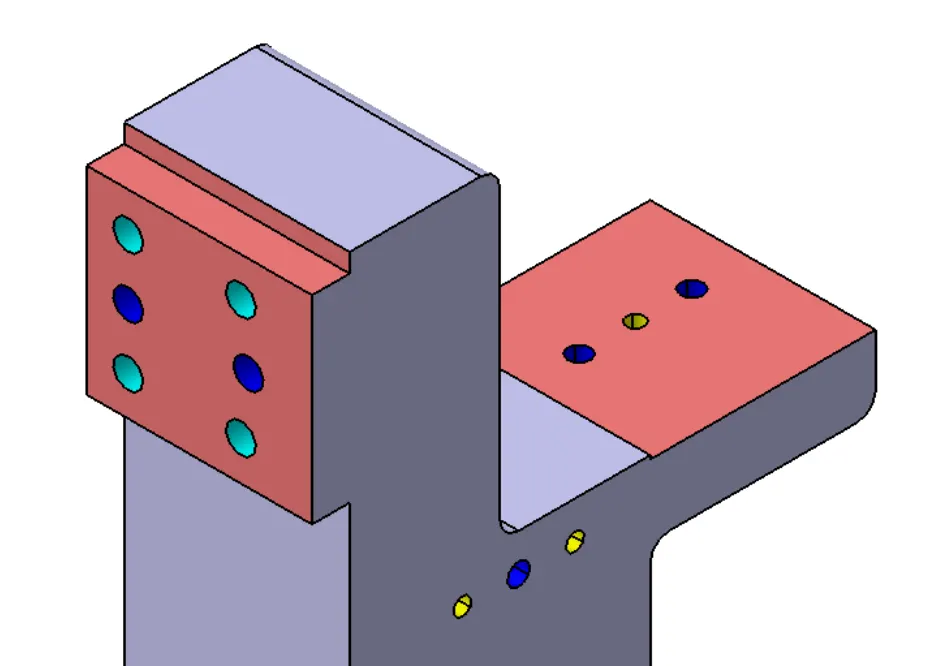
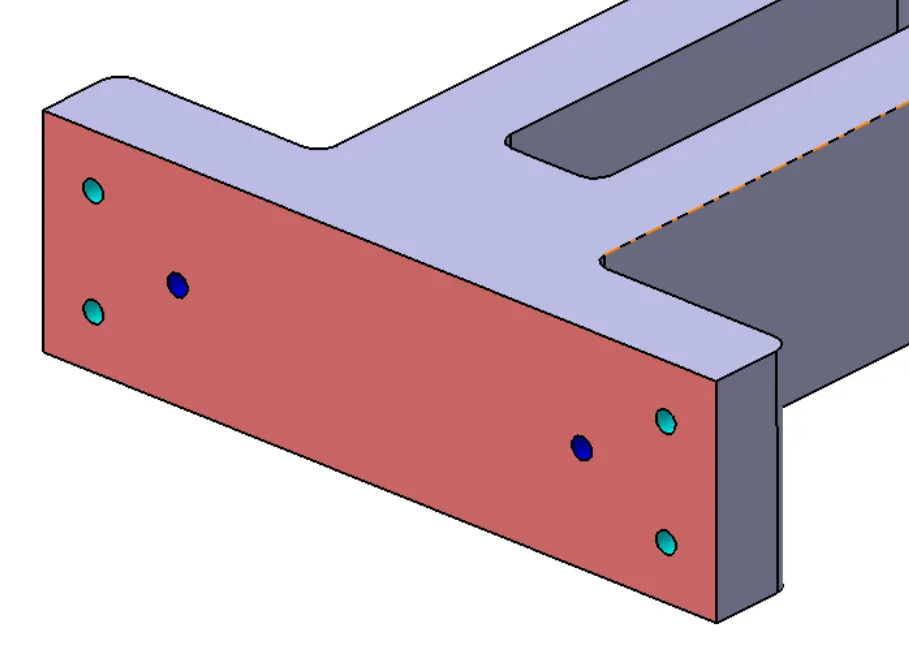
B. REST MYLAR(P00B_Z002_ST01_05_01_REST_MYLAR)
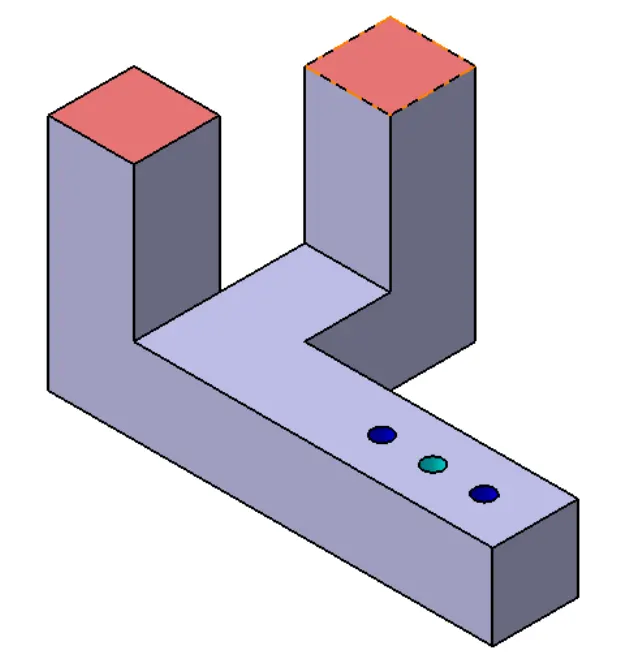
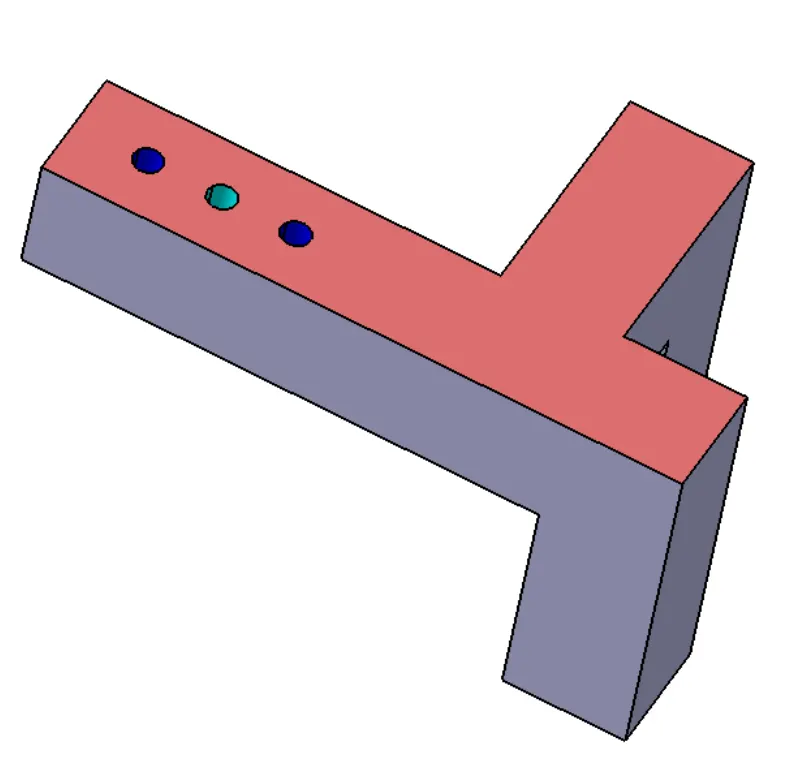
C. L BLOCK(P00B_Z002_ST01_05_04_L_BLOCK)
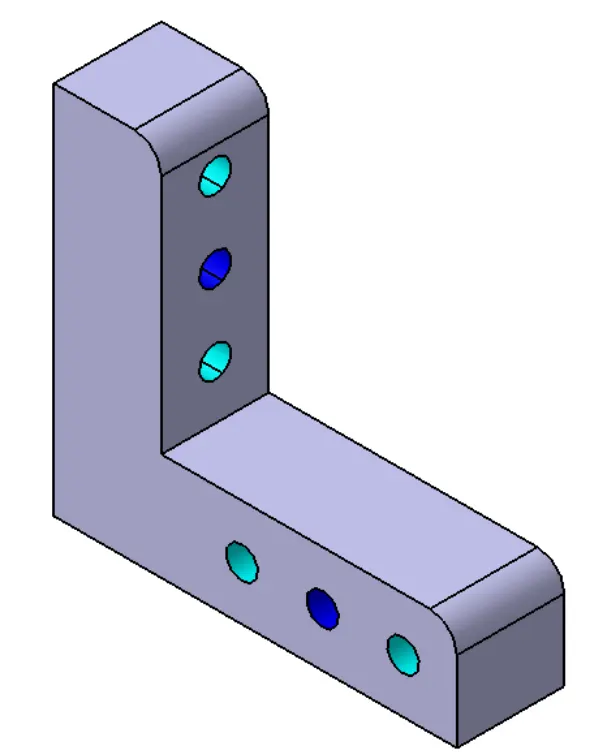
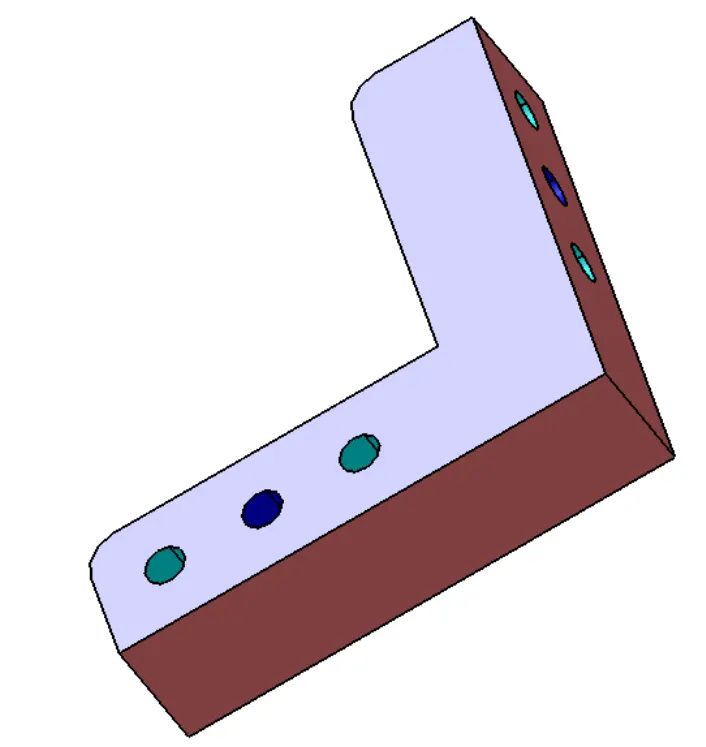
D. PIN RETAINER(P00B_Z002_ST01_05_06_PIN_RETAINER)
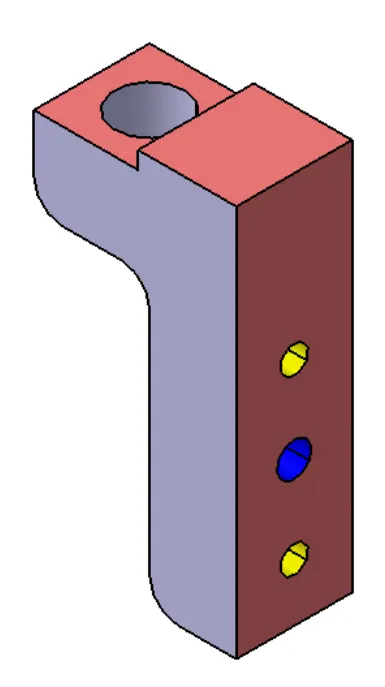
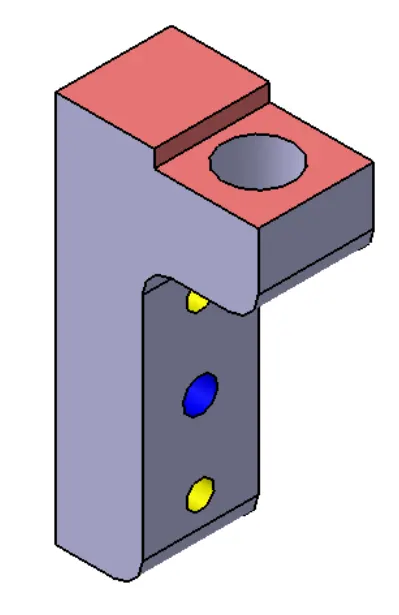
E. PIN(P00B_Z002_ST01_05_05_PIN)
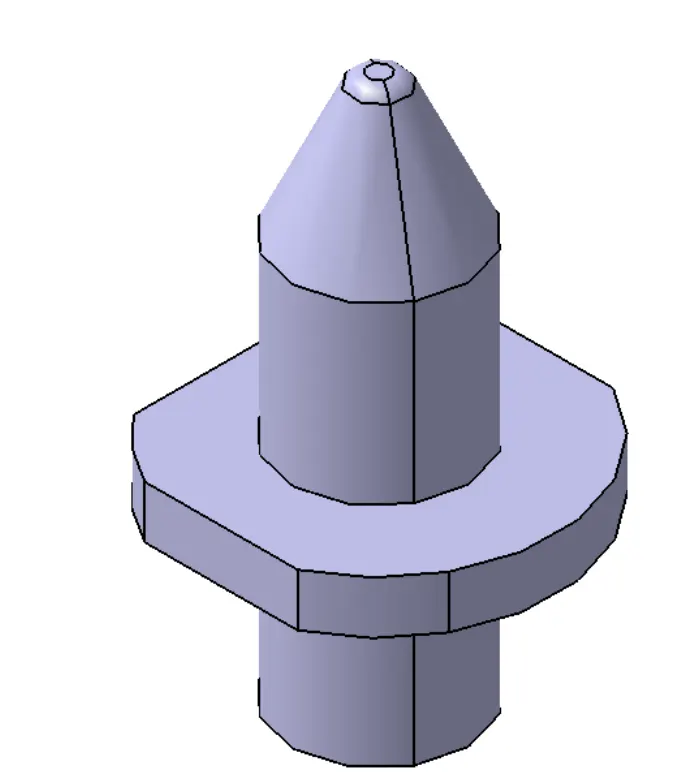
6.REST UNIT_P00B_Z002_ST01_06_00_REST_UNIT_1
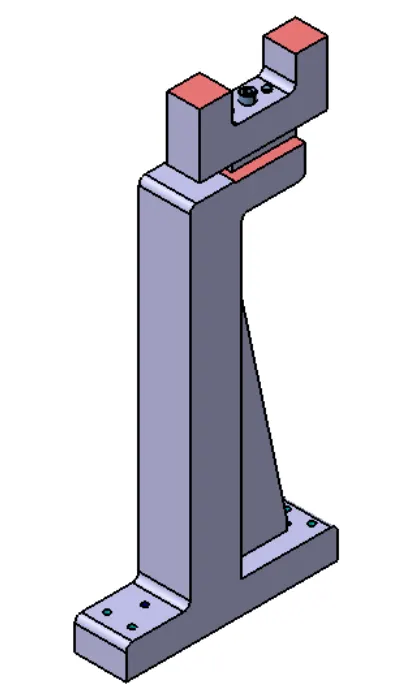
A. RAISER(P00B_Z002_ST01_06_02_RAISER)
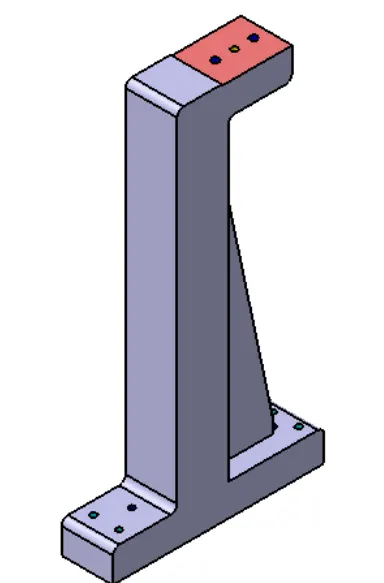
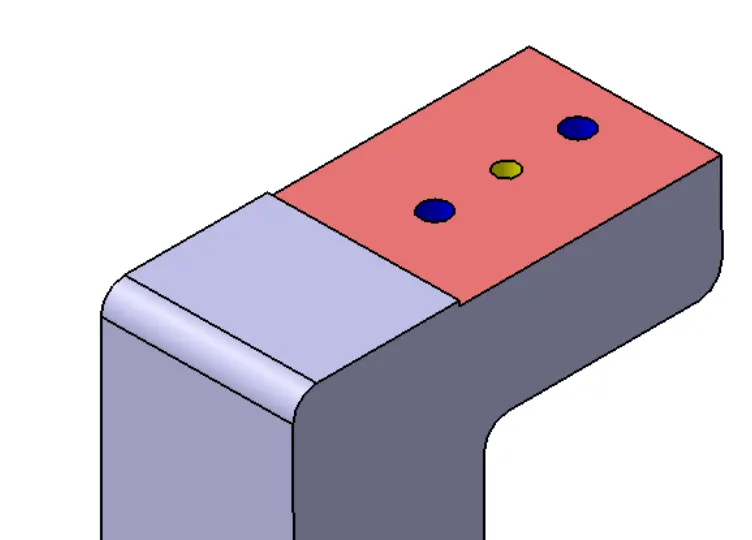
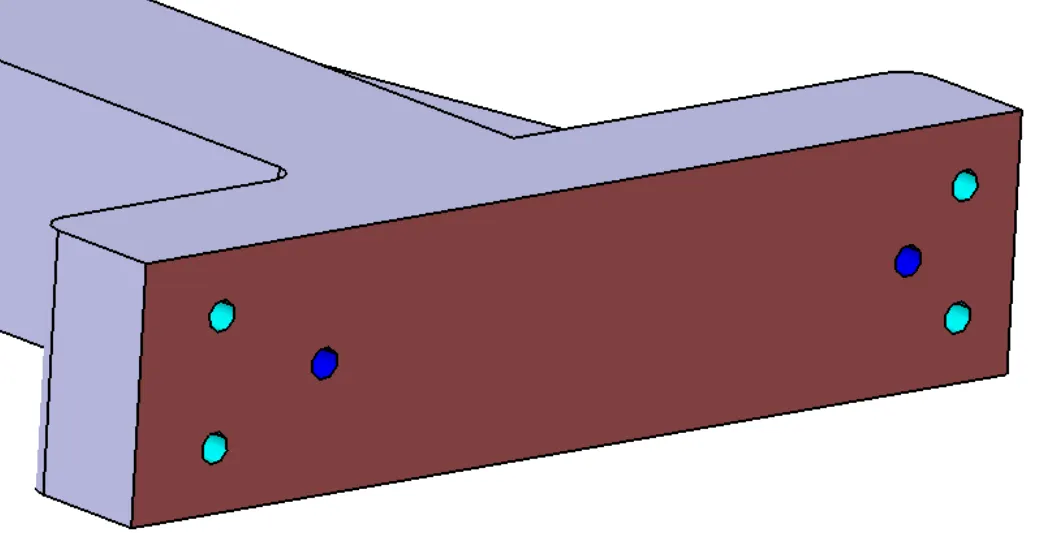
B. REST BLOCK(P00B_Z002_ST01_06_01_REST_BLOCK)
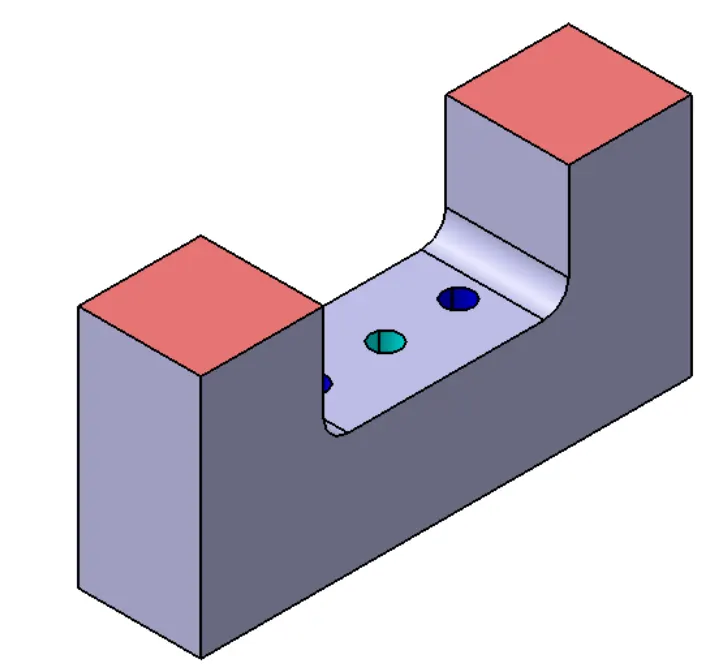
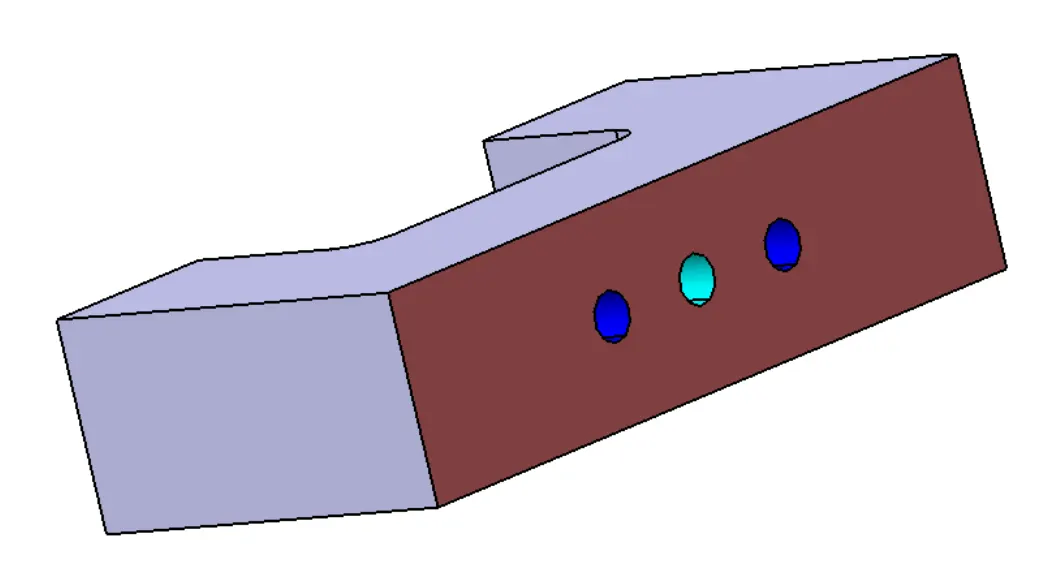
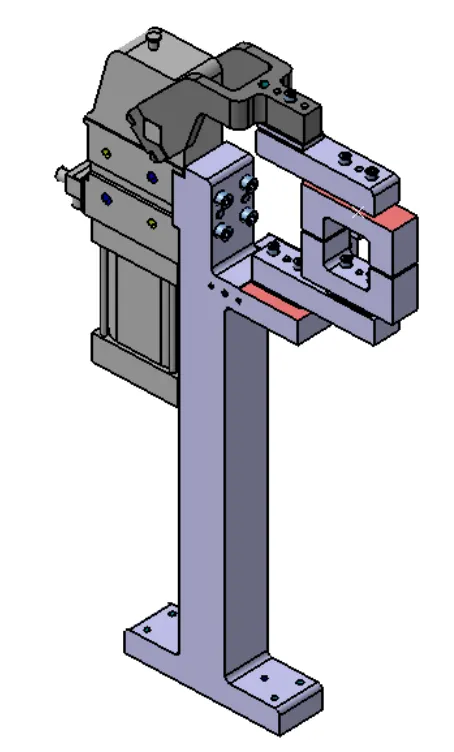
7.CLAMP AND PIN UNIT_P00B_Z002_ST01_08_00_CLAMP_UNIT_3
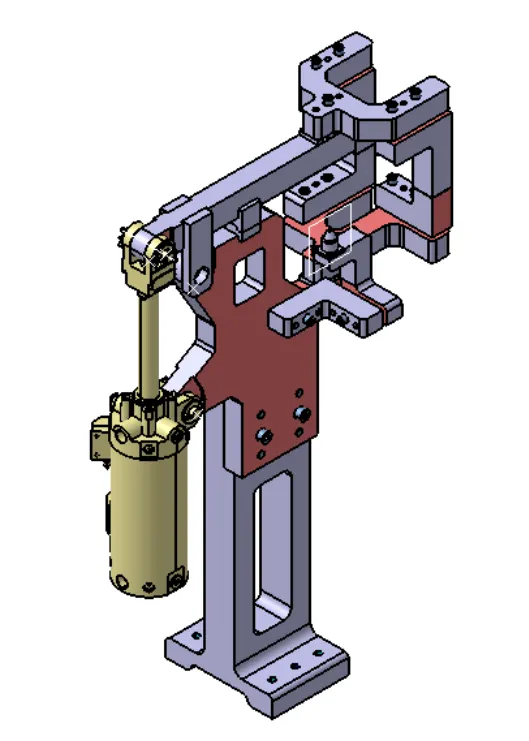
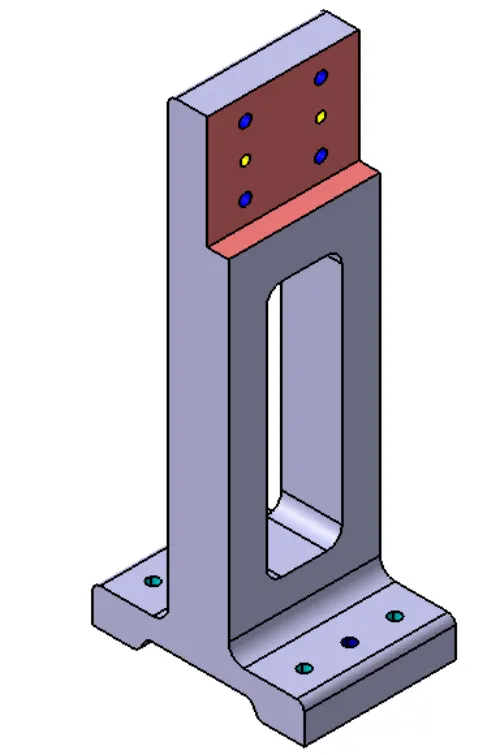
A. RAISER
B. BLADE
C. REST MYLAR
D. CLAMP MYLAR
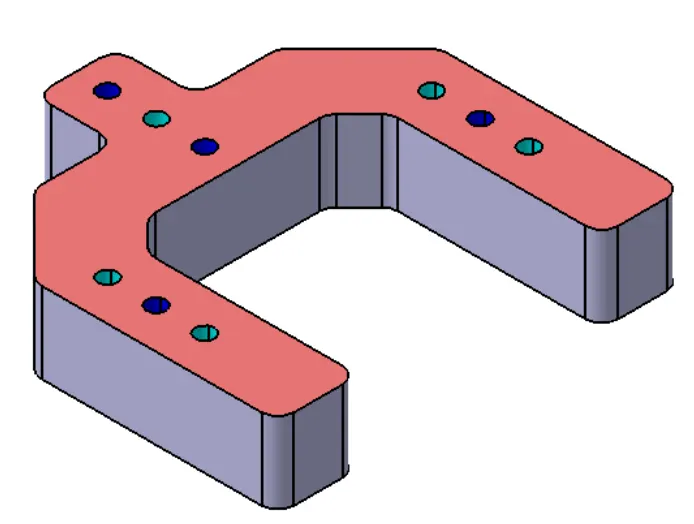
E. CLAMP ARM
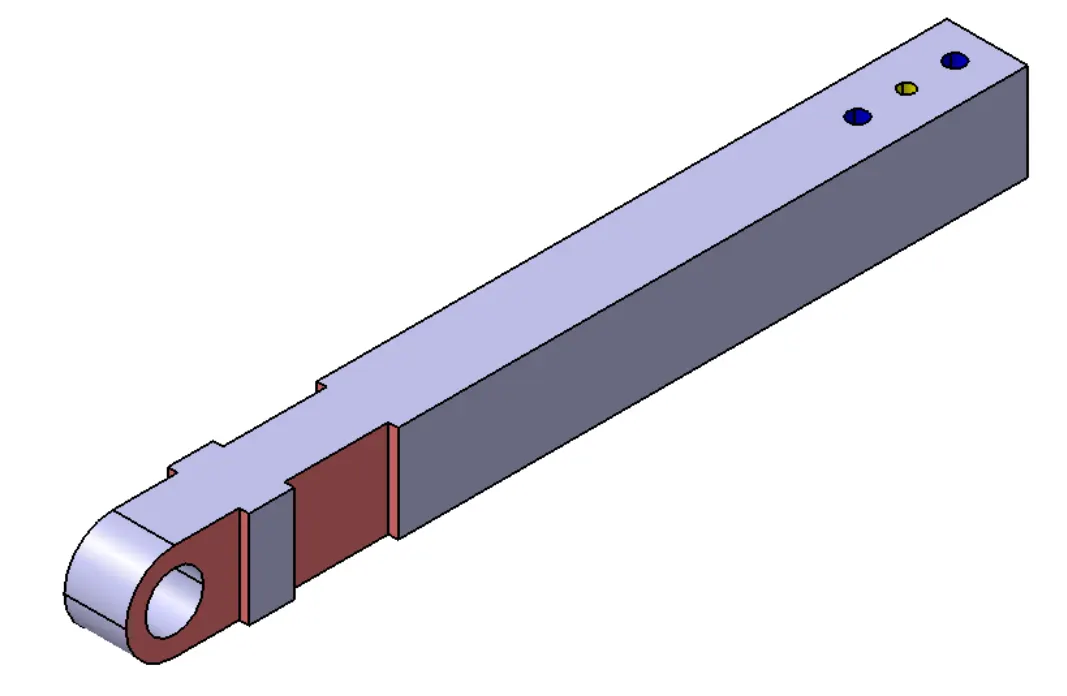
F. STOPPER
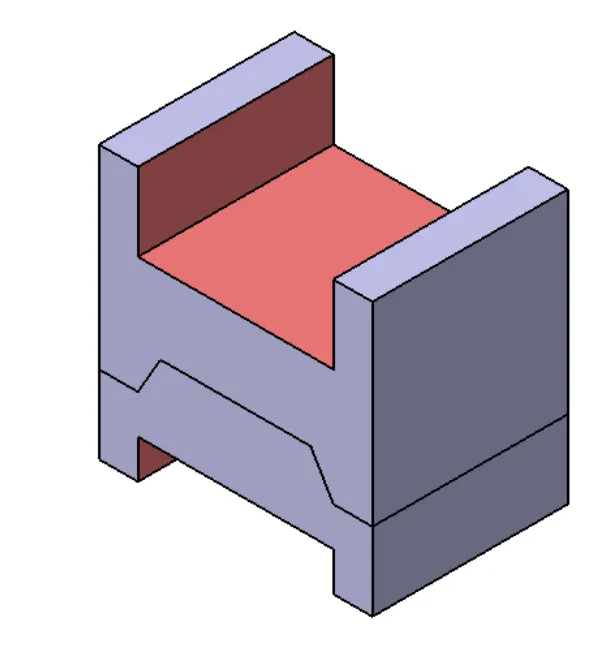
G. CLAMP MYLAR
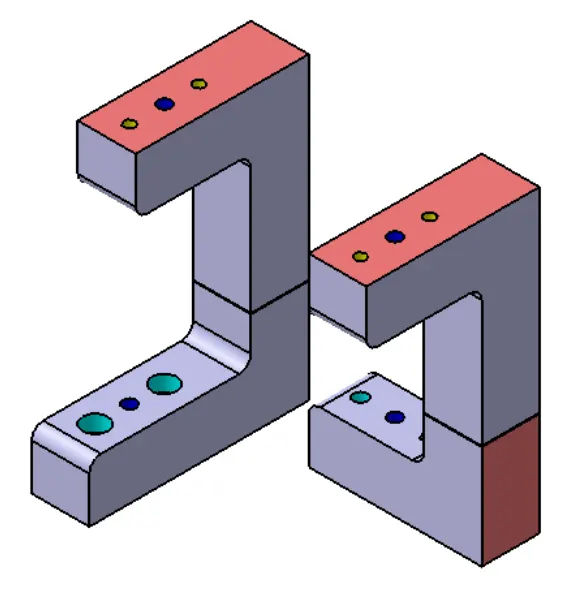
H. L BLOCK
I. PIN RETAINER
J. PIN
ROUGH LOCATORS
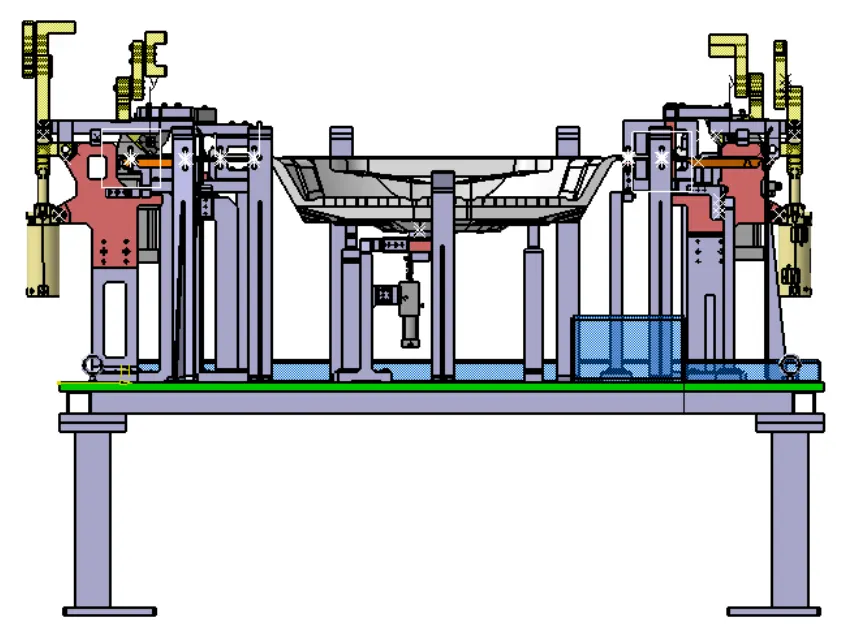
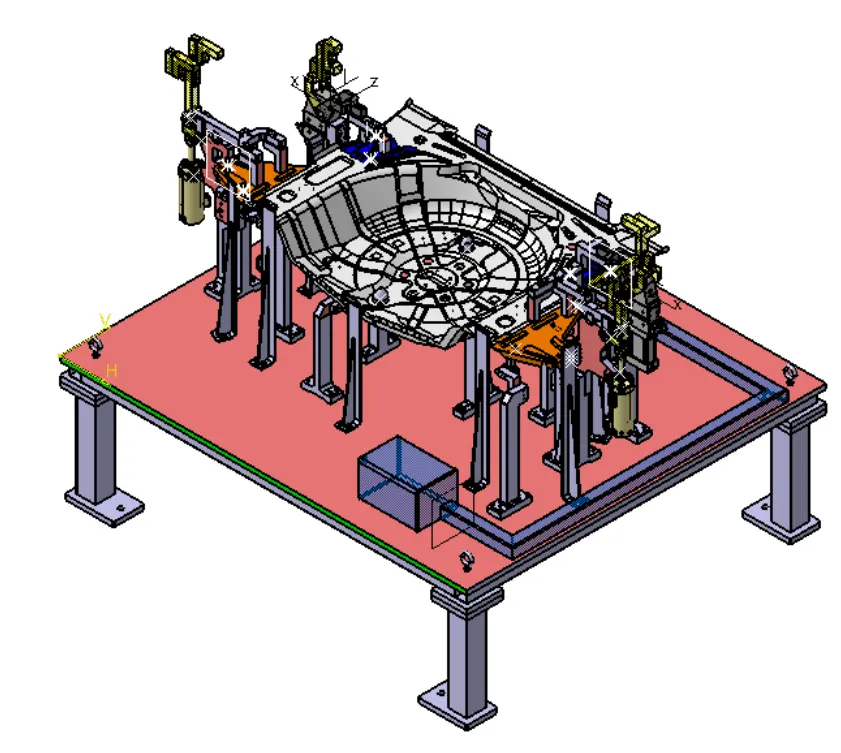
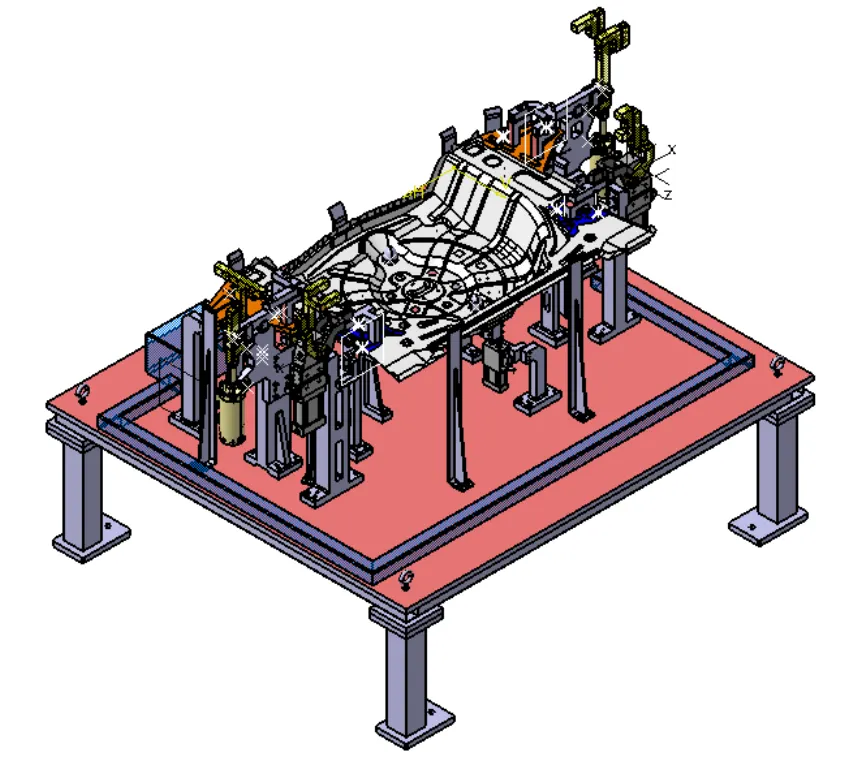
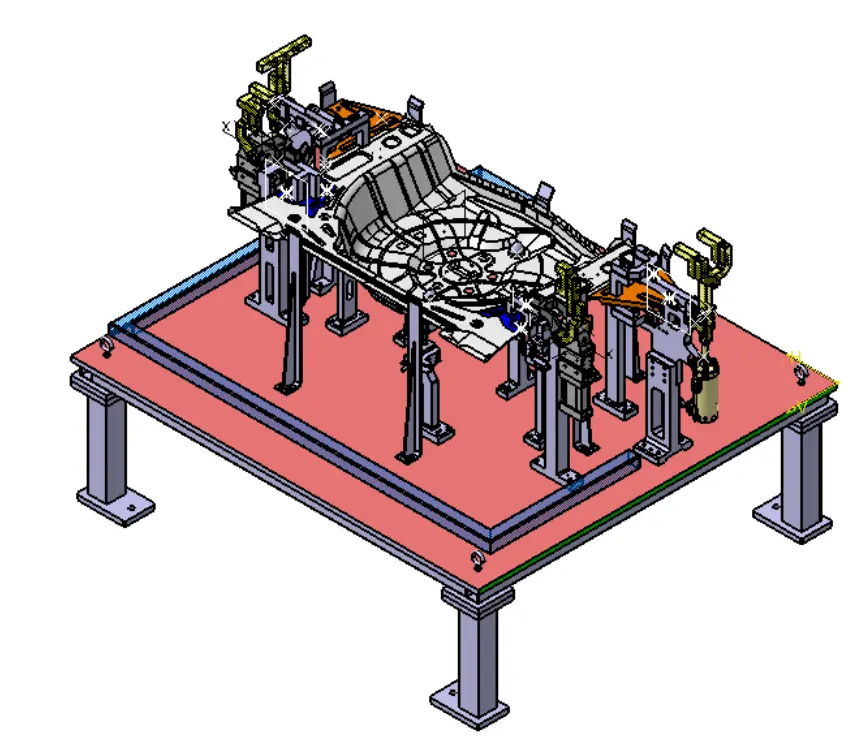
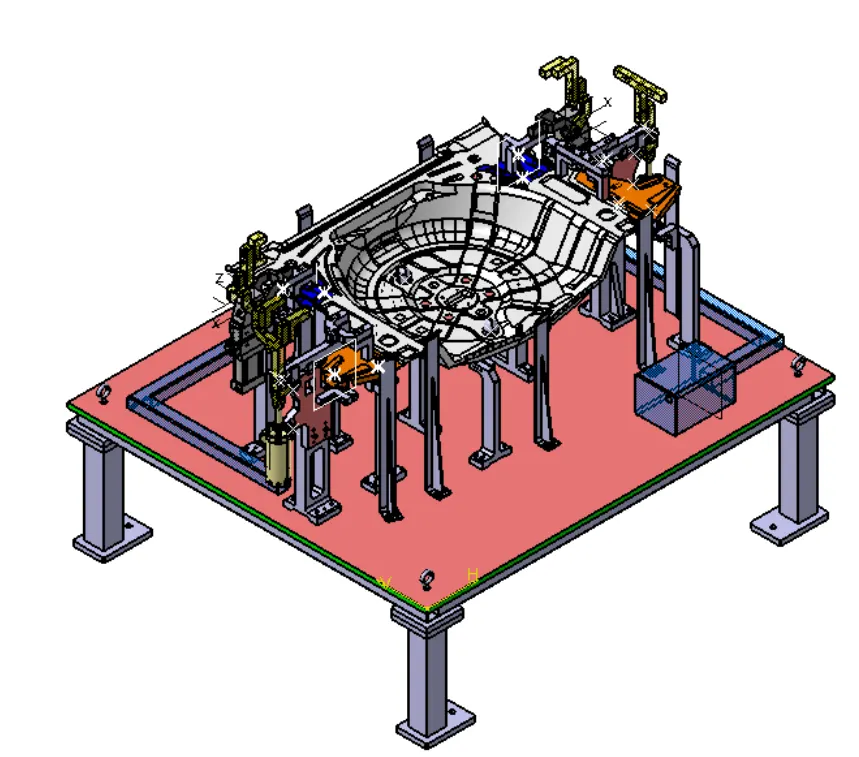
FIXTURE ASSEMBLY
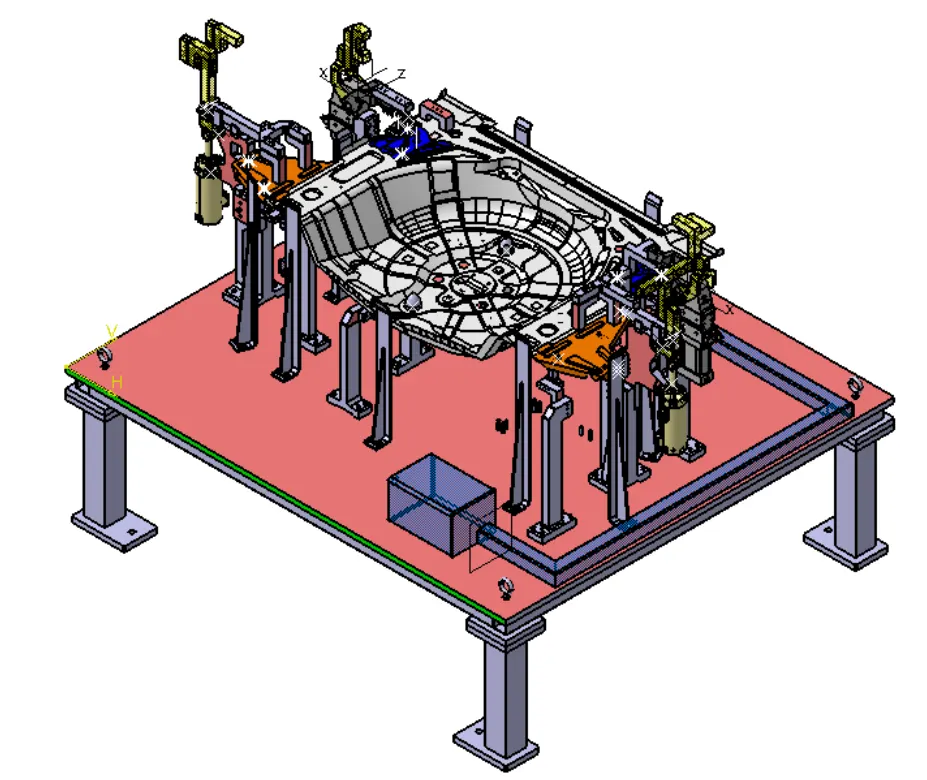
ROUGH LOCATORS
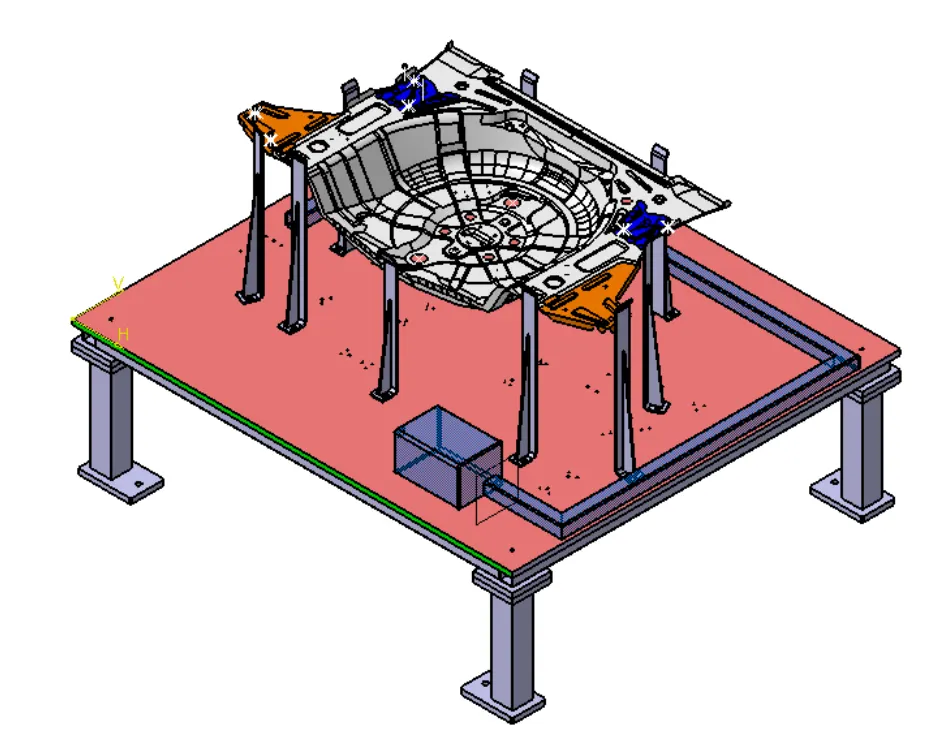
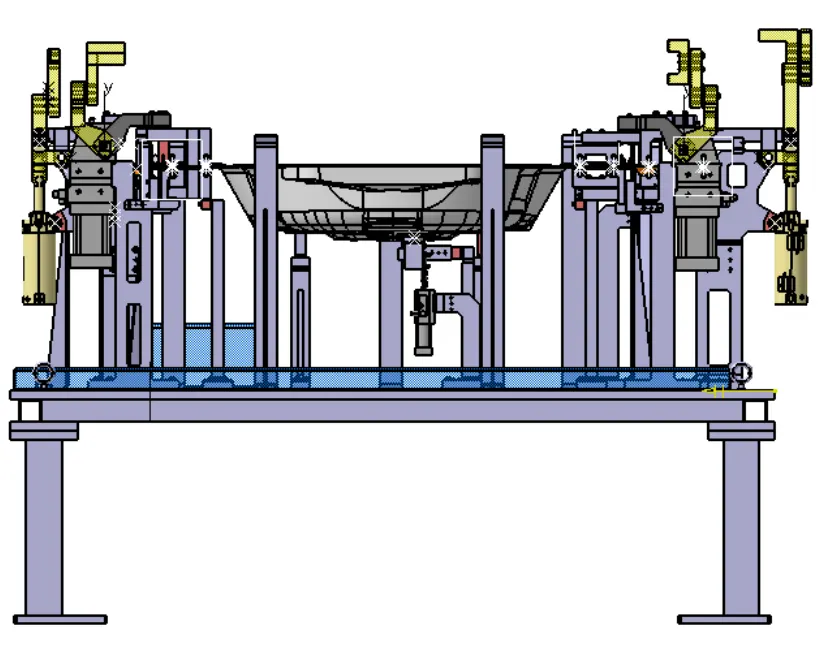
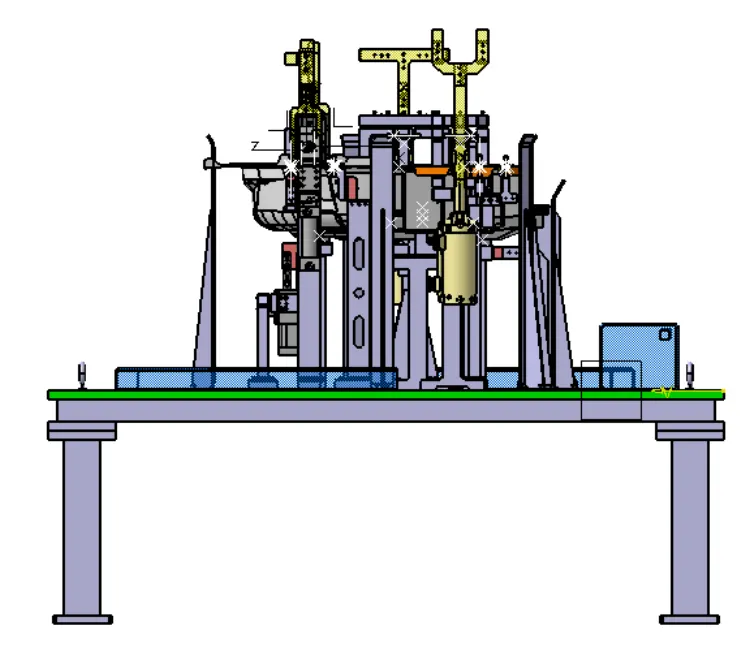
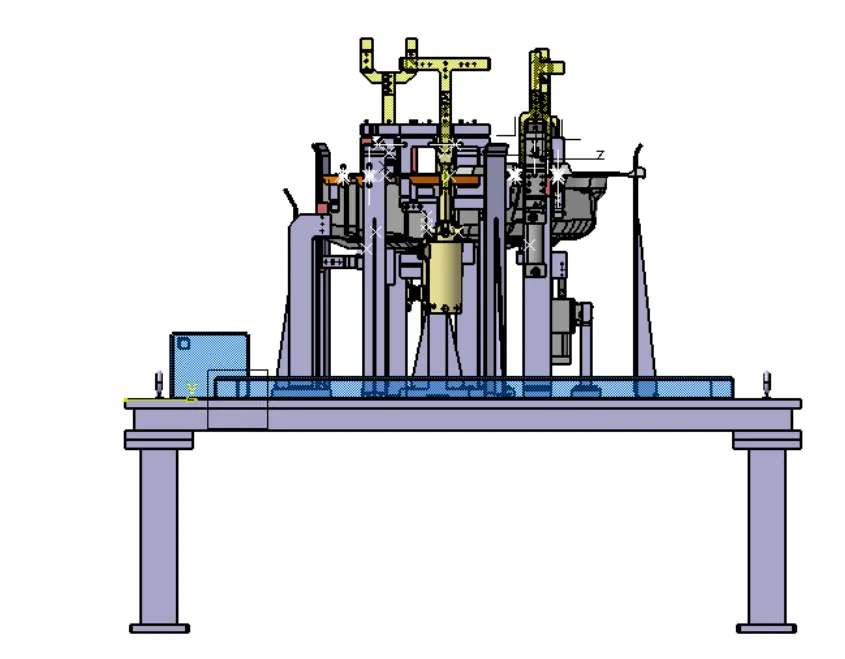
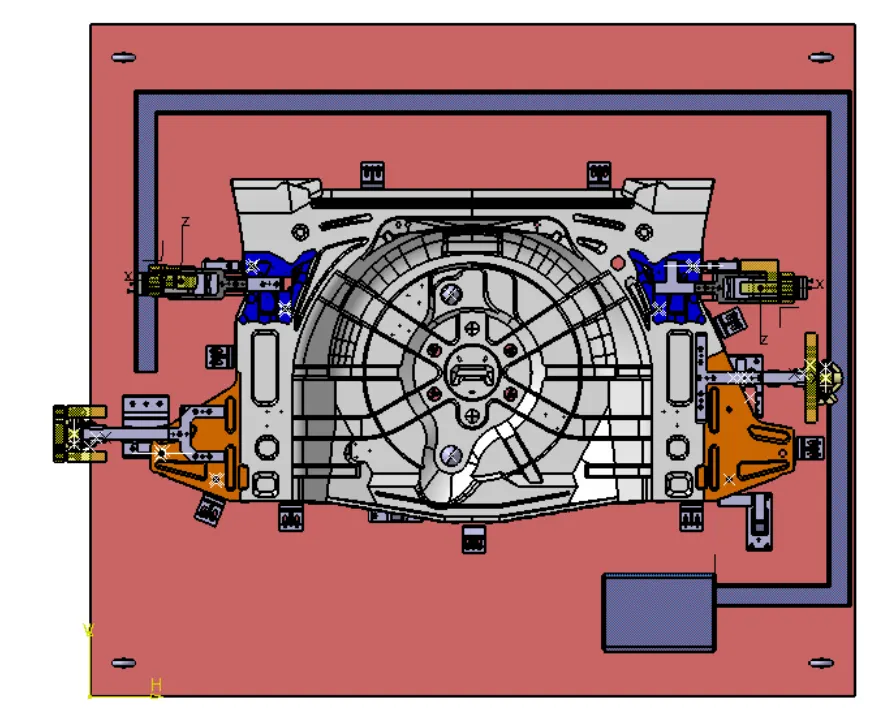
ALL UNITS , ROUGH LOCATORS AND PNEUMATIC CHANEL
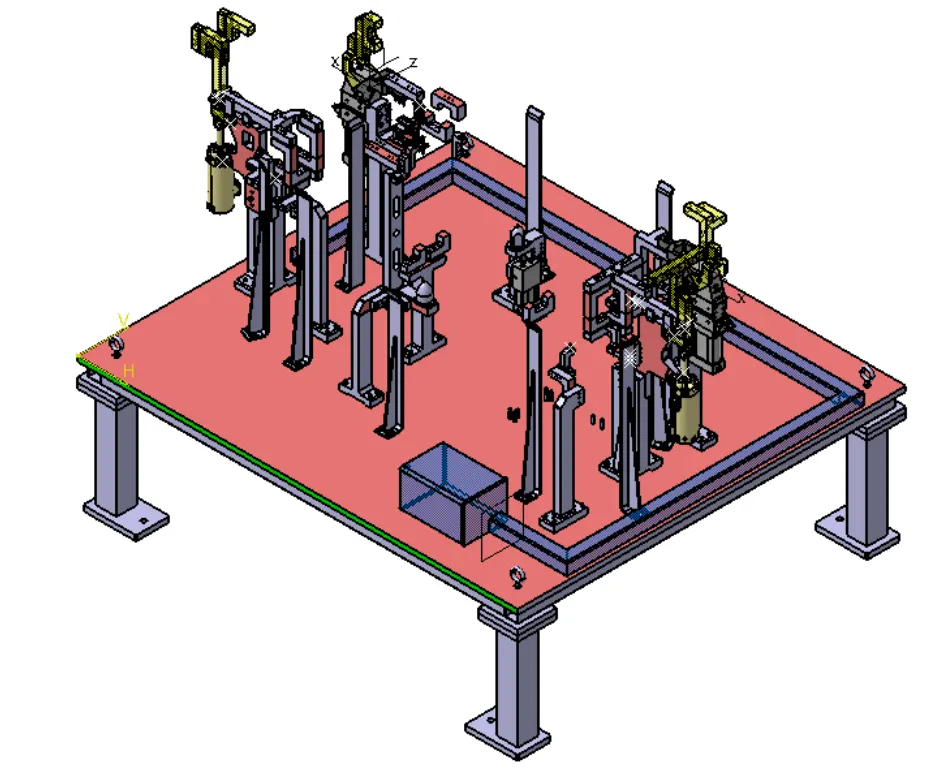
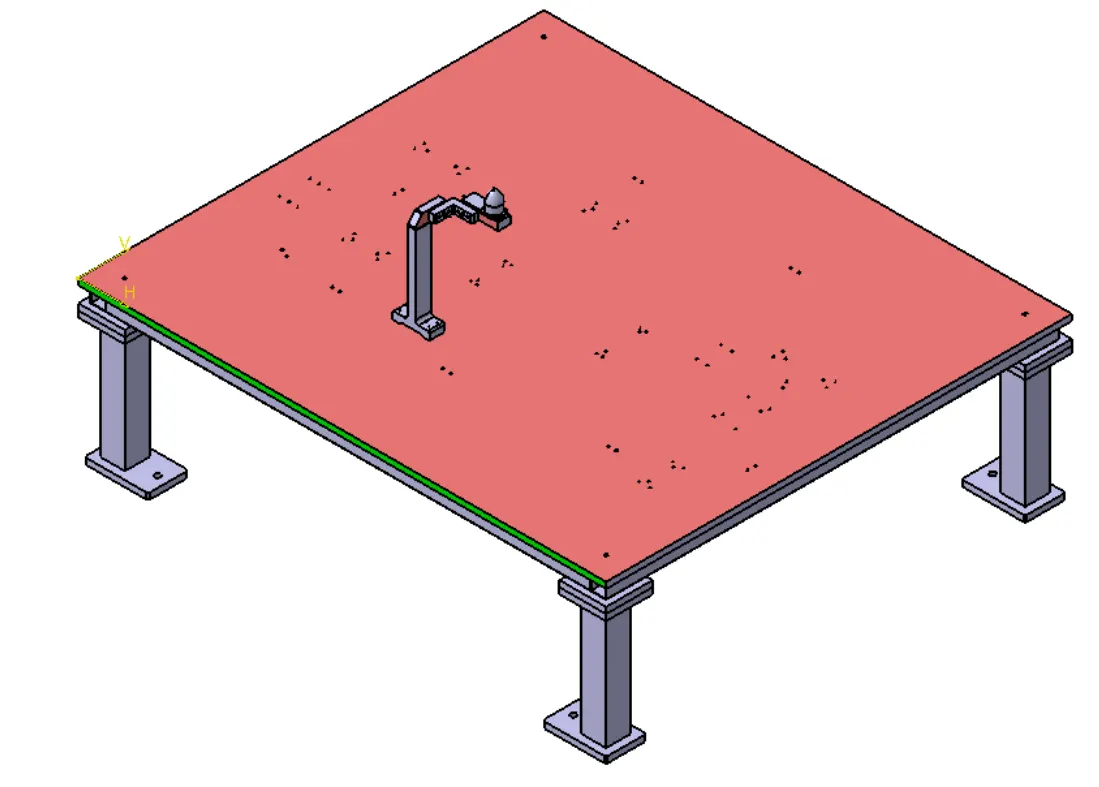
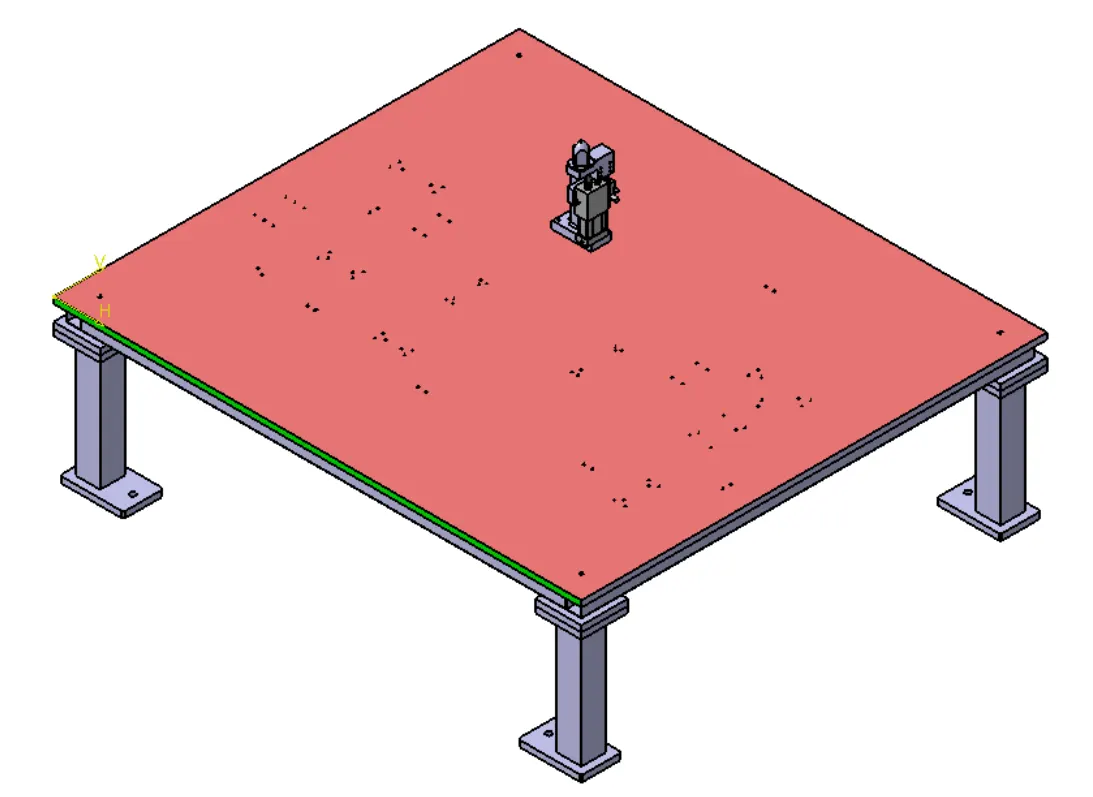
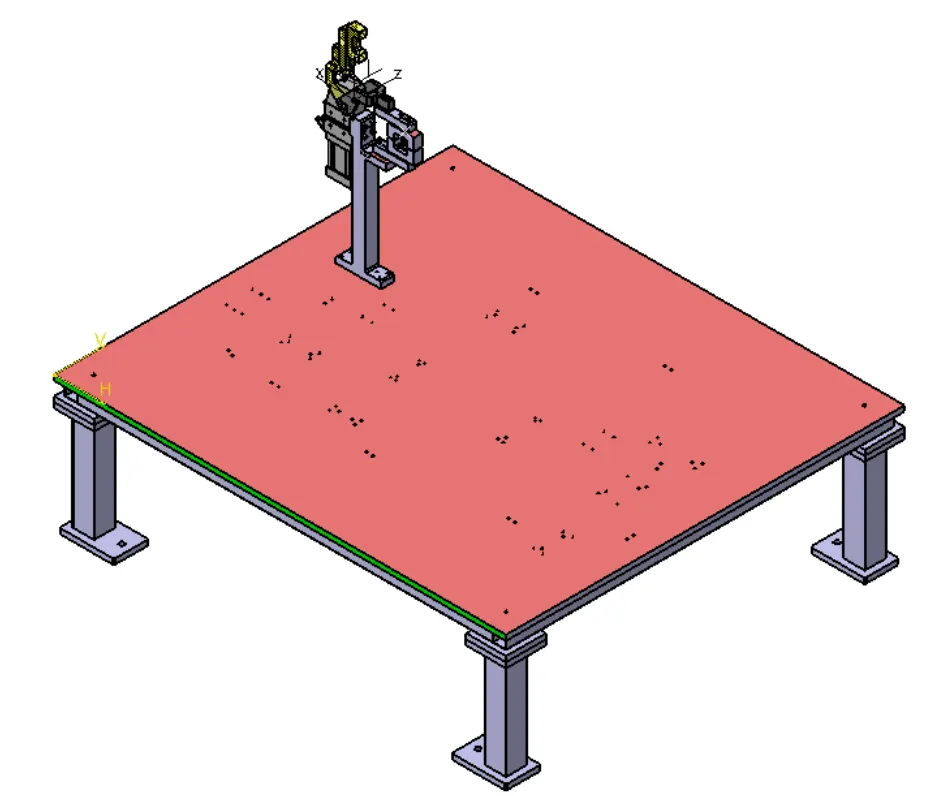
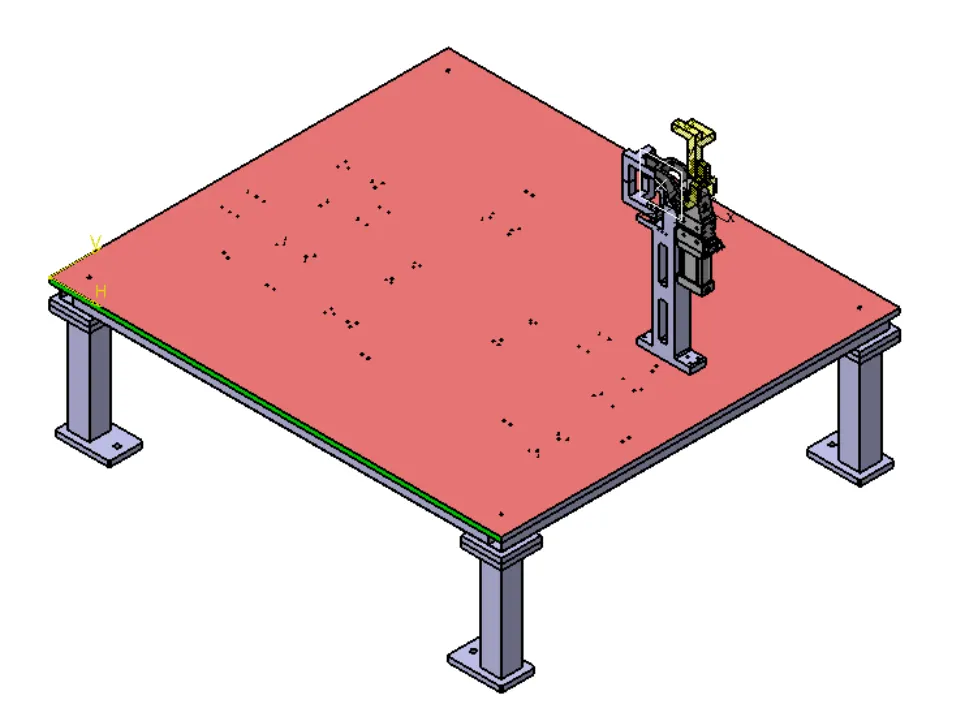
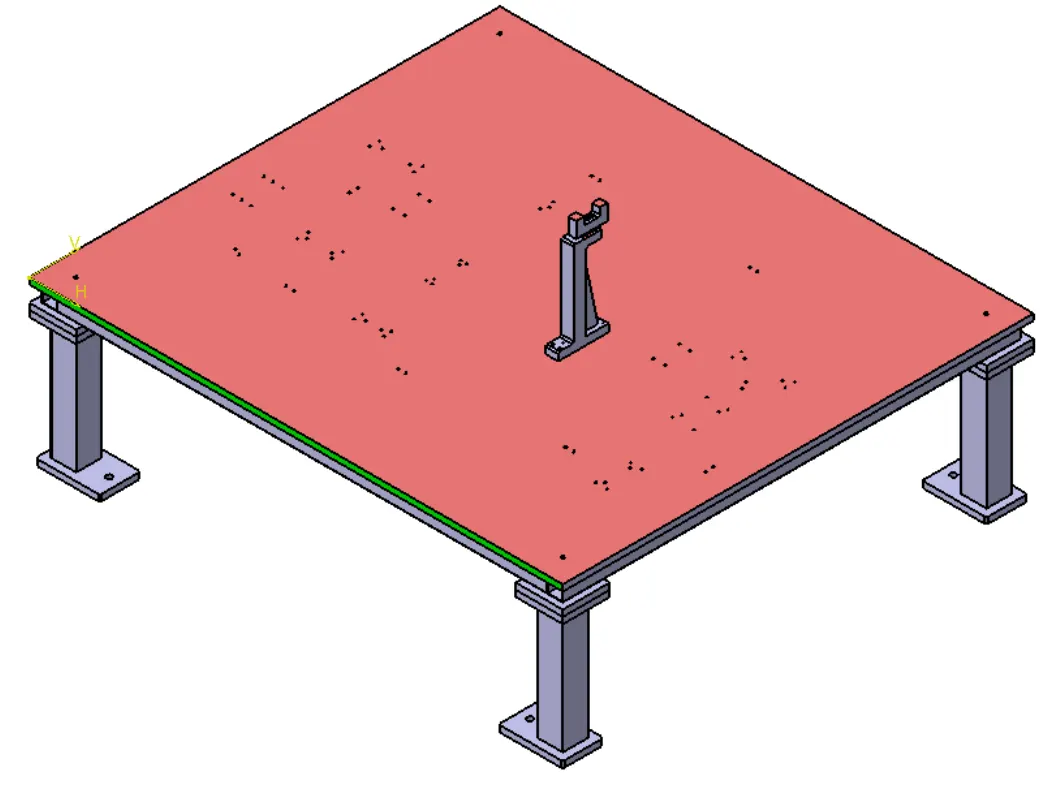
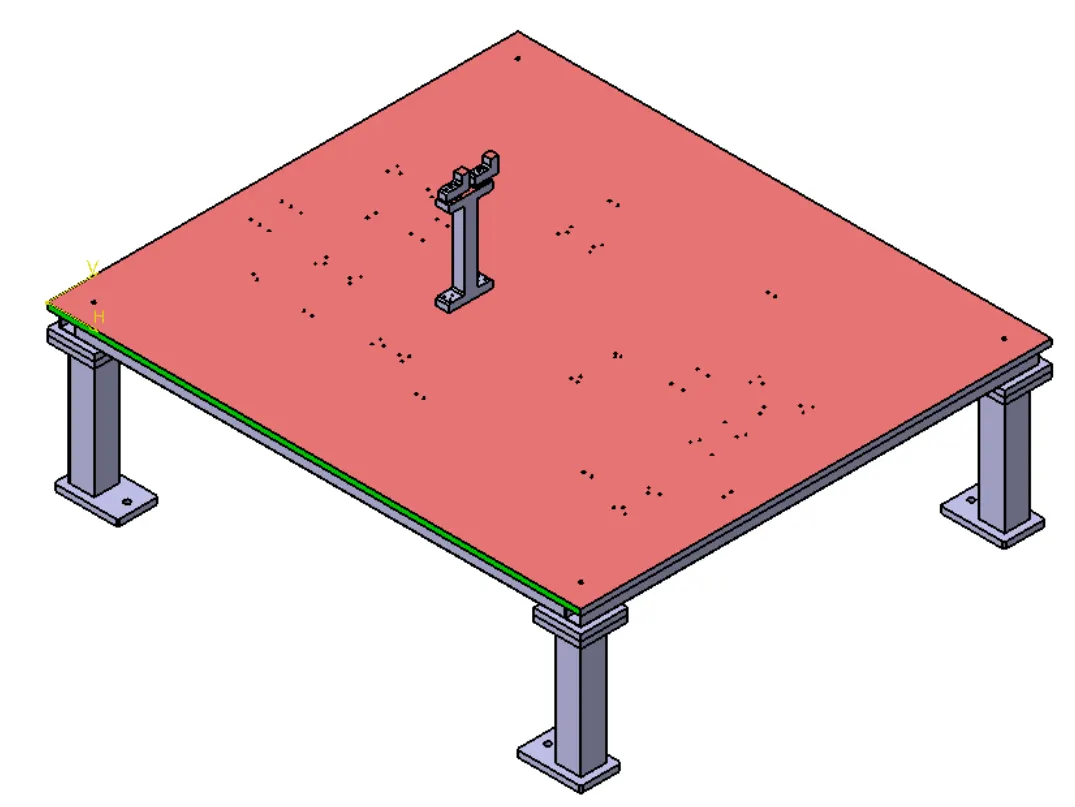
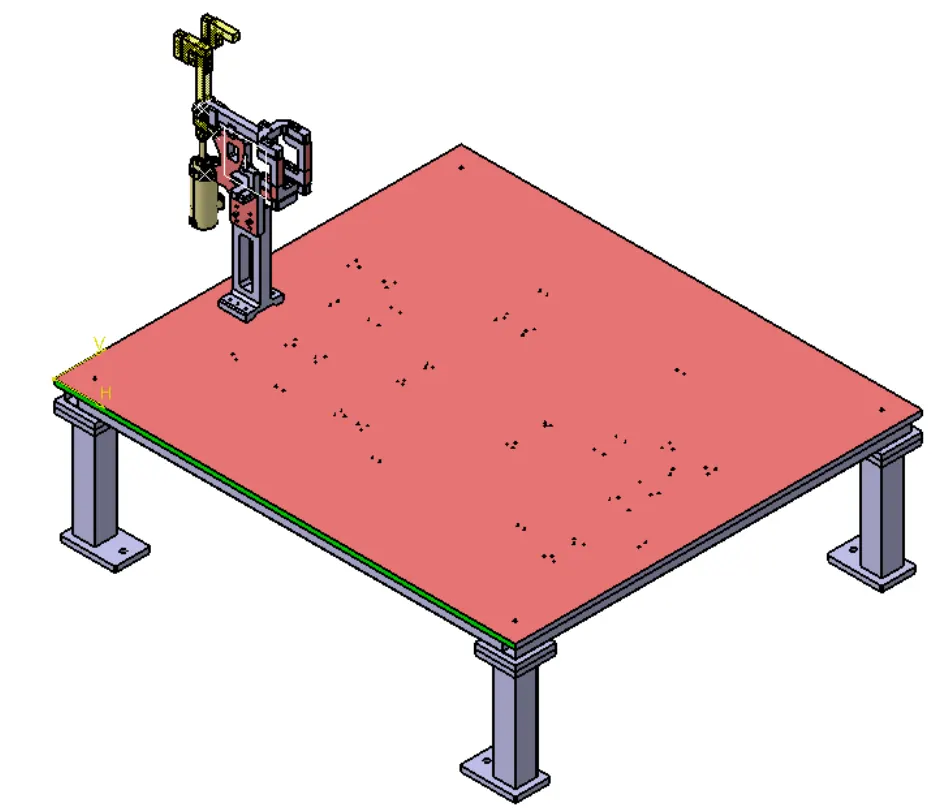
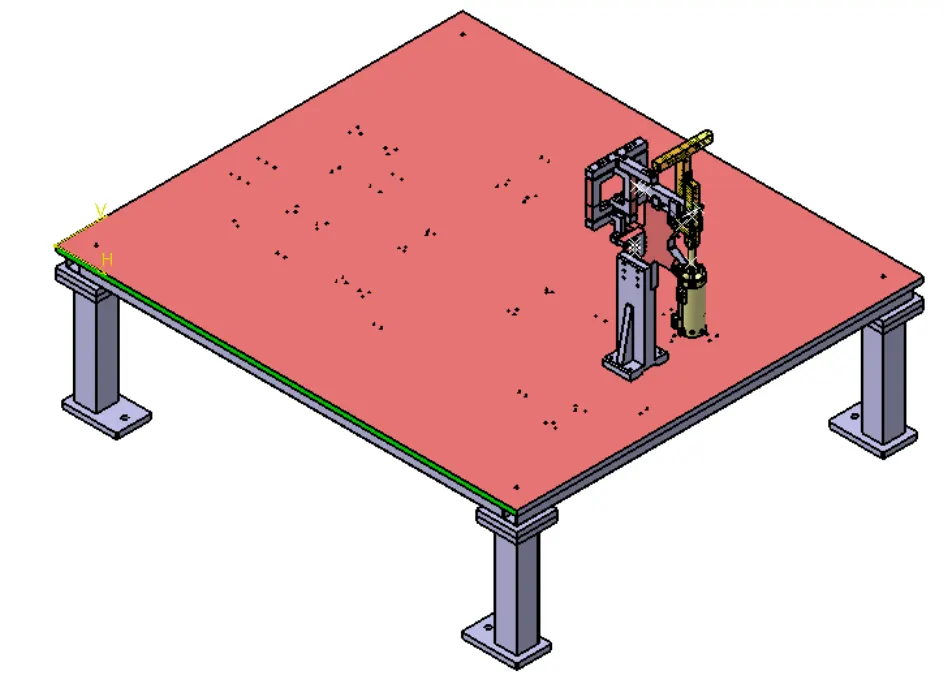
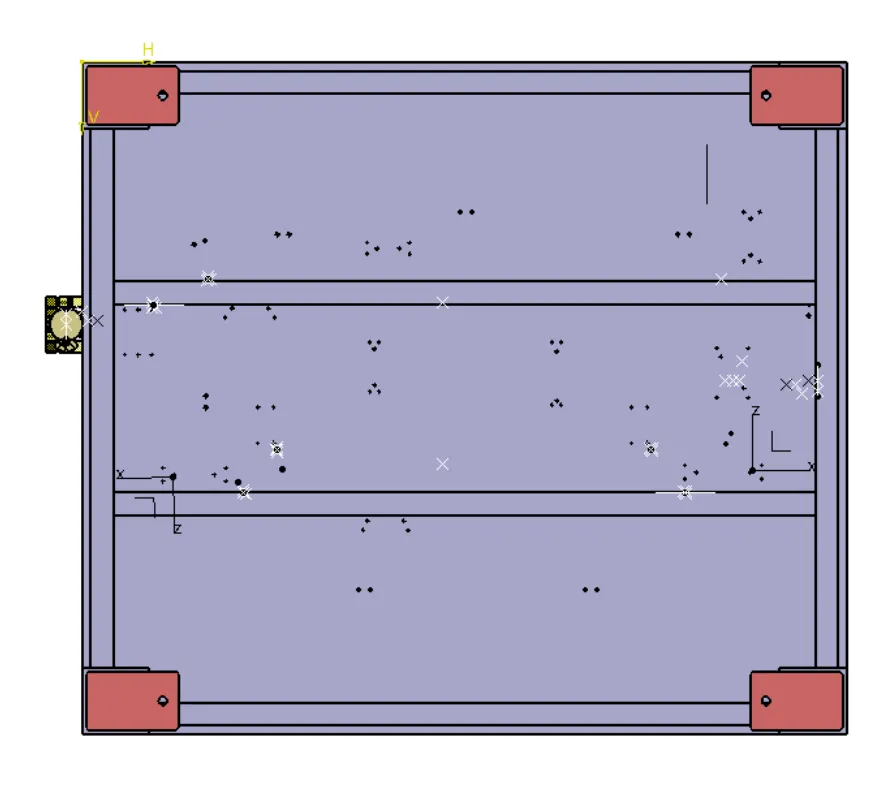
VIEWS
CONCLUSION
- BIW FIXTURE IS SUCESSFULLY 3D FINISHED
- ROUGH LOCATORS ARE CREATED
- PNEUMATIC CHANEL IS CREATED