Week 7- Base Unit Design Challenges 2
Objective:
1. Design a Base Unit for the units designed for the above challenges with all weldments for the given Car Panel.
2. Design the complete Fixture assembly. Make all the 5 Panels given in the CAD data fully constrained with the 3-2-1 principle.
Base Unit:
The base unit is the unit of the fixture which is designed as such so that other units of the fixture can be mounted on it. Apart from these units, other necessary tools like a pneumatic valve box, trunking cable path will also be mounted on the base unit.
The base unit is the fundamental component of the fixture because all other components are mounted over it.so every fixture has a base unit. The base unit design is different according to the panel, Design of clamp system, location system, etc.
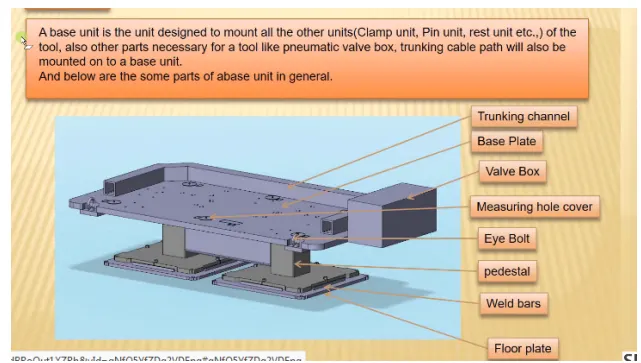
Parts of the Base Unit:
Baseplate
Pedestal
Trunking channel
Valve box
Eyebolt
Floorplate
1. BASE PLATE:
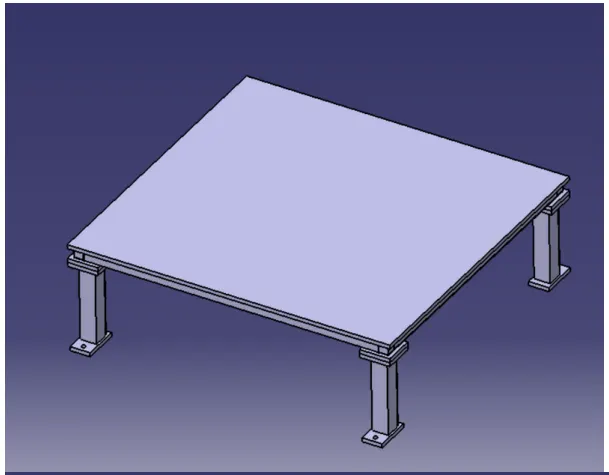
The base plate is a machined plate of 25 to 40mm thickness made of steel and aluminum on which the holes are drilled to mount individual units like clamp unit, pin unit, rest unit, etc.
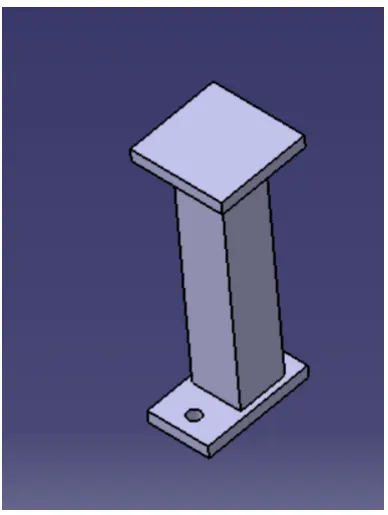
2. PEDESTAL:
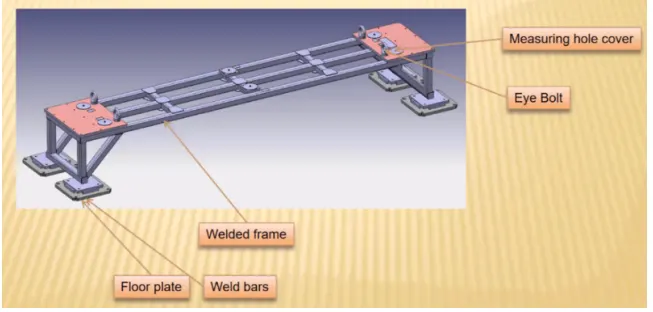
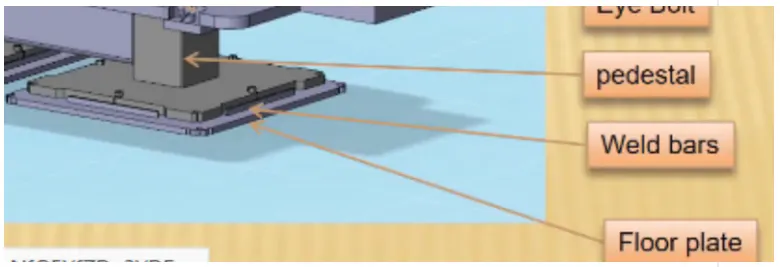
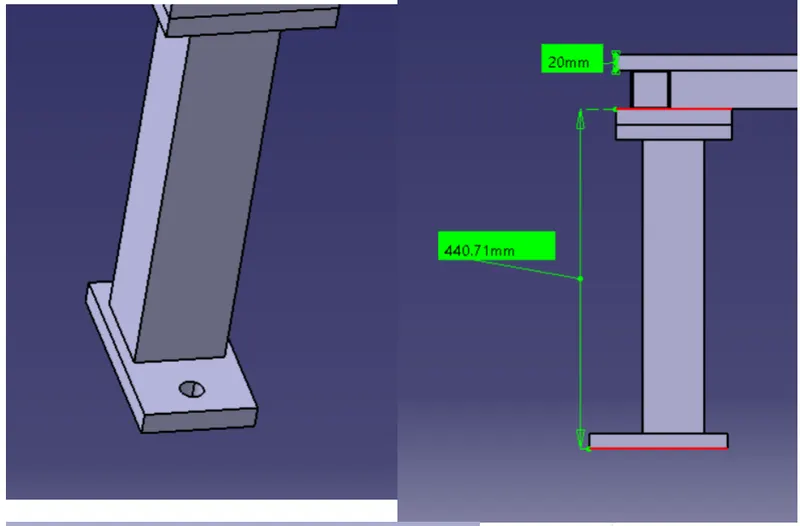
A pedestal is a part that connects the base plate to the floor plate. A pedestal is a standard part in general and in some cases it can be a welded frame integrated with the base plate.
- A standard pedestal can be of different heights and different sizes.
- Depending on the size of the base plate, the number of pedestals varies for load distribution.
- Pedestals are of different types with different inclinations.
3. Trunking Channel:
Trunking Channel is a duct that carries all the electrical and pneumatic connections(wires and pipes) for units of the tool. It has a thickness of a few millimeters.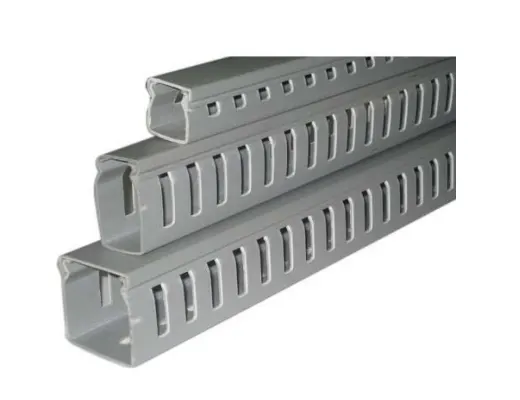
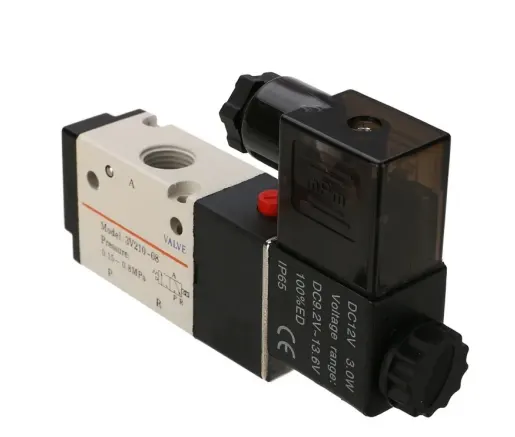
4. Valve Box:
Valve Box is a standard part that contains all the valves for the pneumatic units. The valve box is the box which includes different solenoid valves. The pneumatic fixtures work on air pressure provided to it. So the arrangement of air pressure inlet & outlet is done within this valve box. The trunking channel includes all the pressure inlet cables going to the pneumatic parts of the fixture & protects them from damaging while an operation is in process.
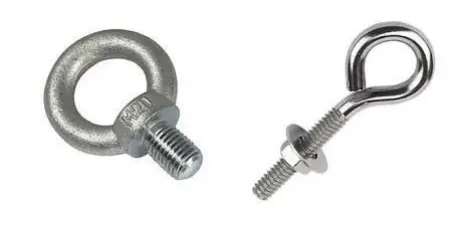
5. Eye Bolts: Eyebolts are used for the transporting of the tool, using lift hooks, fork lift holes will also be provided in some cases for transporting purpose. For example, we usually use M20 bolts that are bolted on the base plate.
When installing lifting eye bolts it is critical to ensure face is in firm contact with the mating surface. These lifting rings are intended for linear pulling loads in the direction of the thread.
They are not intended for use where the load is perpendicular to the thread. This is because in these instances the bolt could unscrew and move or it could be twisted and break.
6. Floor Plate:
The floorplate is grouted to the floor with a fixed bolt on the ground. Floor plates are also called foundation plates.
- There will be a clearance of 10 mm maintained between the pedestal base plate & floor plate.
- This clearance will be used by the leveling screws, for leveling the entire tool.
- Weld bars are be used to weld the positions permanently after leveling is done.
- A weld bar is a plate along the sides of the base plate of the pedestal.
The points need to account while designing a Base Unit:
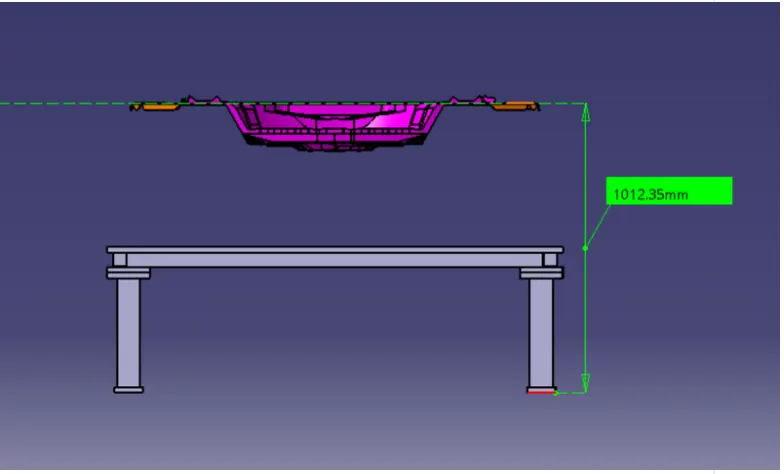
1. Working Height:
- It depends on the nature of the manual or robotic welding fixture.
- For manual fixture working height of 850-1100 mm is needed to be considered, depending upon the working height of the worker standard of specific the country will apply (In few countries human height is higher or lower e.g. US, Japan).
- If the base structure is made with a base plate having a tubular structure welded below it then we can reach to height of 100 mm to ~250 mm. In this case to reach the working welding height we need to provide additional leg structure which may have top and plate welded to the tube.
- Try to study the gun ergonomics properly then design the unit height and then base top height.
2. Base Plate or Welded Structure:
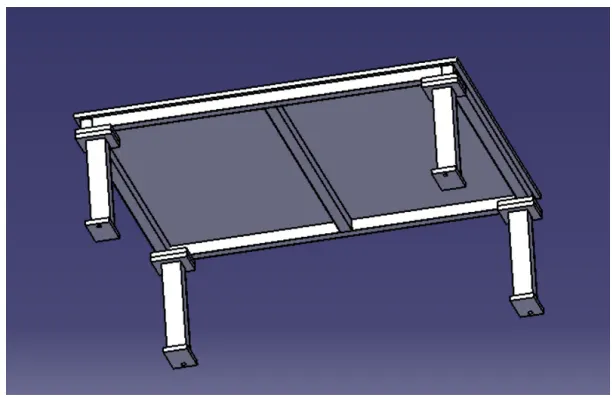
- Depending upon the component size and weight of the total units we can decide whether we need a fabricated base or just a plate.
- Mostly fabricated bases are used made of square or rectangular tubes with plates.
3. Selection of Eye Bolt:
- As designer it is important to know how big base plate or bigger base welded structure will be handled during the fabrication and handling process.
- Depending upon the weight eye bolt size is selected for lifting holes on the base plate.
- Generally, 4 eye bolt provision is made. We also need to select the location of eye bolt considering the rope/ belts used while shifting the structure or complete fixture are not damaging any units (rest, clamp or location units) nearby.
4. Number of Measuring Holes Required:
- We would need 3 holes to define the plane.
- Most of the OEM makes 4 dowel holes at 4 corners and put small aluminum plate marking X, Y &Z coordinates of dowel holes.
- If the base length is too long few OEM's follow the methodology of having dowel holes at 500mm distance
5. Base Plate:
- There are few OEM’s, Line builders use an only thick base plates. Few OEMs recommend thick base plate 40mm or 50mm for the child part assemblies (e.g BMW). 40/50mm plate makes a very heavy structure but some OEM's follow the methodology.
- If we go for a higher thickness it will not bend after machining and will have good flatness.
- The general observation is if we go for 10-12 mm thick plate for large size for e.g. 2mx2m, after machining when we unclamp plate from milling machine theplate will not show good flatness.
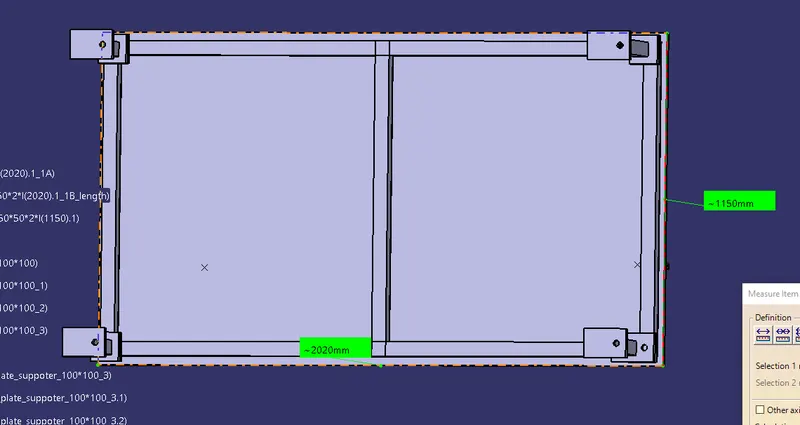
Fundamentals of base plate design:
- A base plate size should cover all the units with its outer periphery including the opening.
- A base plate is preferred to be designed with respect to BCS coordinates.
- A base plate should be drilled with datum holes/ measuring holes in line with a pitch of 100mm in general.
- The number of datum holes depends on the size of the base plate.
- Datum holes should be drilled at nominal values of coordinates and in terms of 50 and 100.
- Datum holes should be drilled with a diameter of 100mm away from other units.
- Datum holes should be covered with cover plates.
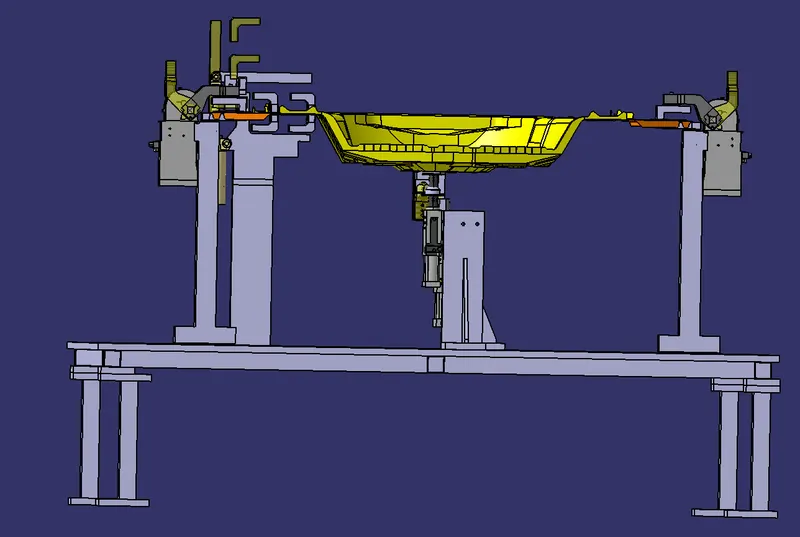
Fixture Assembly:
3-2-1 Principle:
A workpiece free in space can move in an infinite number of directions. For analysis, this motion can be broken down into 12 directional movements or "degrees of freedom". All 12 degrees of freedom must be restricted to ensure proper referencing of a workpiece.
The 12 degrees of freedom all relate to the central axis of the workpiece. Notice the 6 axial degrees and 6 radial degrees of freedom. The axial degrees of freedom permit straight-line movement in both directions along the 3 principle axis shown as X, Y & Z.
The radial degrees of freedom permit rotational movement, in both clockwise & counterclockwise radial directions around the same three-axis.
A rigid body in the plane has 6 degrees of freedom (i.e) The motion of a ship at sea has 6 degrees of freedom.
X+ , X- , Y+ , Y- , ZCW , ZCCW
The purpose of the Fixture is :
1. Resting:
In a fixture, the workpiece should rest in such a way that it doesn’t move or vibrate on the resting blocks.
2. Locating:
The fixture should locate the workpiece such that all the operations to be performed on it are performed without any problem and all of them are performed effectively.
3. Orienting:
The fixture should orient the workpiece such that all the operations to be performed on it are within the reach of the workpiece.
4. Clamping:
A clamp is a fastening device used to hold or secure objects tightly together to prevent movement or separation through the application of inward pressure.
There are many types of clamps available for many different purposes. Some are temporary, as used to position components while fixing them together, others are intended to be permanent.
Achievement of 3-2-1 Principle:
This requires a minimum of three locator blocks to establish the part plane. Three locators or supports are placed under the workpiece. Three locators are usually positioned at the primary locating surface.
The Clamp unit restricts 2 axial movements Upward and downward and the other 2 pin units restrict radial movement. As by the 3-2-1 method, introducing a minimum of 1 clamp and 2 pins will restrict 6 degrees of freedom.
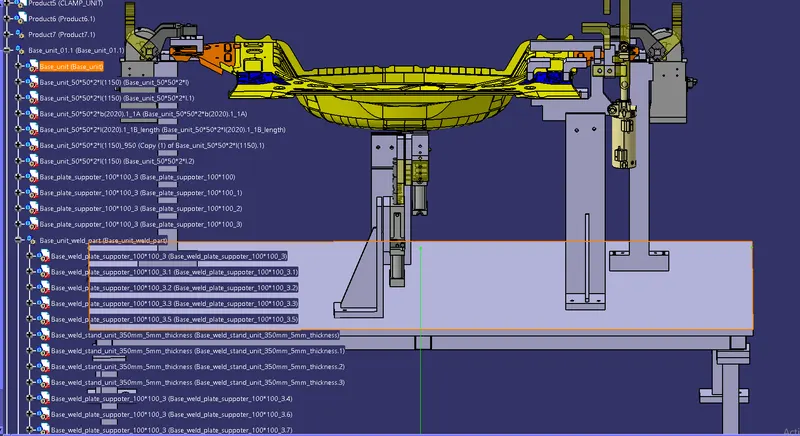
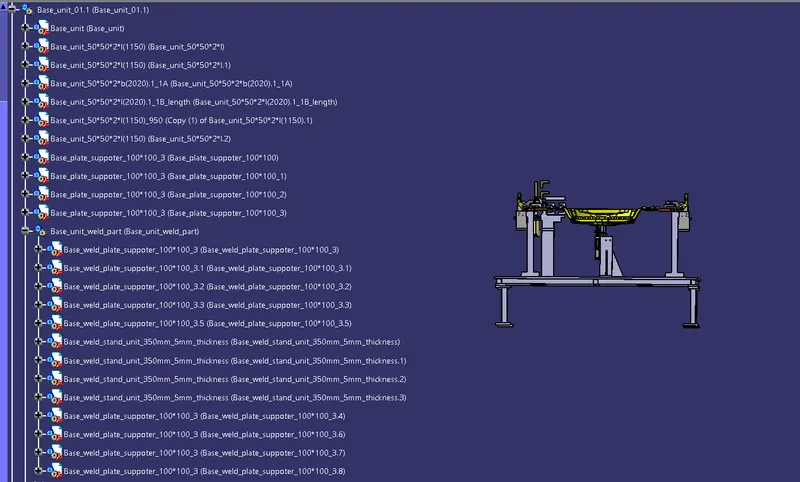
Tree Structure of Base unit: