Week 7:- Base Unit Design Challenges 1
BASE UNIT DESIGN CHALLENGES 1
Q.1)
BASE UNIT
Base Unit
A base unit is the unit designed to mount all the other units (Clamp unit, Pin unit, rest unit etc.) of the tool, also other parts necessary for a tool like pneumatic valve box, trunking cable path will also be mounted on to a base unit.
The Base unit comes in different ranges and sizes, based on the type of loading it supports for the other units that has been placed on the base unit.
Different Panel and surface parts have different
dimensions and its own criticality. The Base unit should be designed in such a
way that, the operations performed on the panel are done smoothly, without
having the adverse effects on the neighboring tools and units.
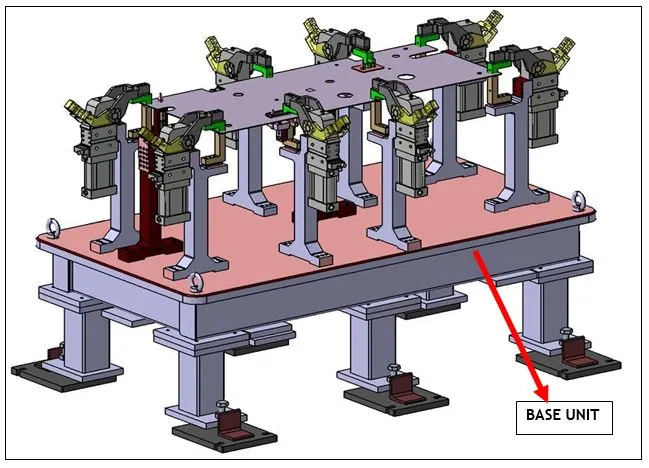
Major parts of Base unit
The major parts of Base Unit are as follows:-
1) Base Plate.
2) Pedestal.
4) Valve Box.
5) Eye Bolt.
6) Floor Plate.
Ø Base Plate
Base Plate is a machined plate of 25 to 40 mm thickness made of steel and aluminium, on to which the holes are drilled to mount the individual units like clamp unit, pin unit etc., of a tool.
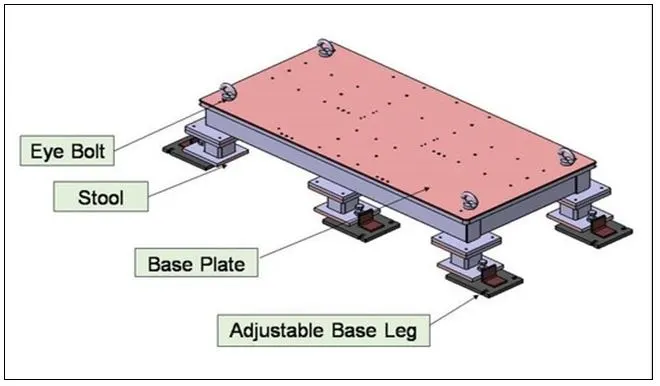
The Base plate is designed as per the requirement and specification called by the client. Based on the complexity of the panel / surface part on which the operations are performed, there are different types of attachments available to perform flexible tasks.
Ø Pedestal
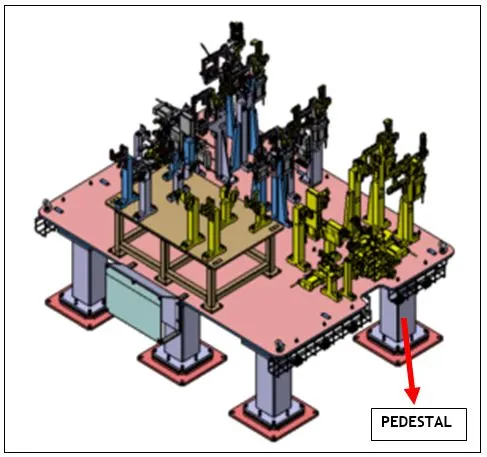
A pedestal is a part which connects the base plate to the floor plate. A pedestal is a standard part in general and in some cases, it can be a welded frame integrated with the base plate.
FEATURES OF PEDESTAL
· A standard pedestal can be of different height and different size.
· Depends on the size of the base plate, the number of pedestals varies for load distributed.
· Pedestal are available in different types with different inclination.
Ø Trunking Channel
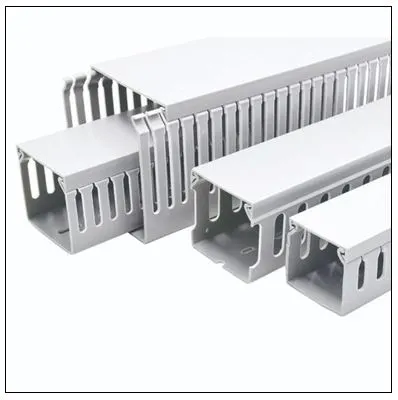
A trunking channel is a duct which accommodates all the pneumatic and electrical hoses and wires for the units of the tool.
The trunking channel makes that, all the cabling and wirings are grouped and laid under the channel, in order to make the base unit free, so that any operating tool performing operation on the panel, doesn’t make contact with the cablings.
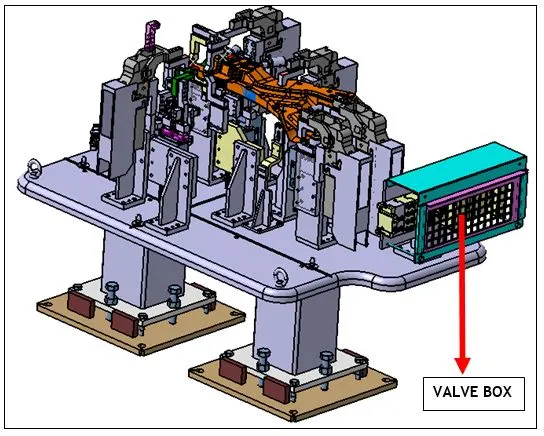
Ø Valve Box
Valve box is standard part which accommodates the pneumatic valves for the units.
A pneumatic actuator comprises of Air-Filter-regulator set, Flow control valves / Directional control valves & solenoid valves for actuating the pneumatic cylinder.
Ø Eye Bolt
Eye bolts are the only bolts, which helps to lift the base unit for shifting purpose.
The eye bolts are on the corner of the base units. The hook of the lifting crane links to the eye of the bolt to make a locking mechanism, so that when the base unit is lifted and in motion from one place to other, the slipping of the base unit should not occur.
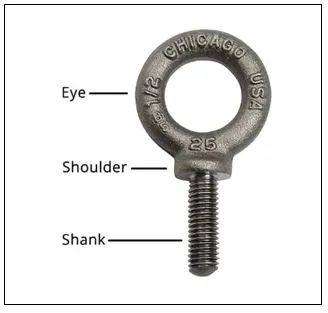
When lifting the base unit, it is common for an eyebolt to be screwed directly into a tapped hole in the structure. In this case, an eyebolt is required that is fully threaded all the way up to the shoulder. When an eyebolt is intended to be inserted through a hole and fastened by a nut on the other side, it is better if there is a shank. A shank is an unthreaded section of the shaft, below the shoulder, which provides a better transfer of load into the surface of the hole and is less likely to crack under a fatigue loading.
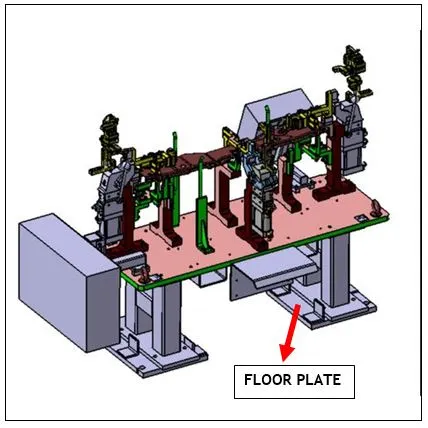
Ø Floor Plate
Floor plate is grouted to the floor with fixed bolt on the ground. Floor plates are also called as foundation plates.
· There is a clearance of 10mm maintained between the pedestal base plate and the floor plate.
· This clearance will be used by the levelling screws for levelling the entire tool.
· Weld bars are to be weld to the positions permanently after levelling is done.
· A weld bar is a plate along the sides of the base plate of the pedestal.
POINTS TO BE CONSIDERED FOR DESIGNING A BASE UNIT
The important parameters that are need to considered while designing the base unit are as follows: -
Ø Working Height: -
Working height depends on the nature of the welding fixture. It may be manual or robotic welding fixture.
For manual fixture, we have to consider the working height between 850-1100 mm, depending upon the height of the worker, who is performing the necessary operation. Different countries have their own pre-defined height standards.
If the base structure is made with a base plate having tubular structure welded below it we can reach to height 100 mm to ~250 mm. In this case to reach the working welding height, we need to provide additional leg support structure which will help in top structure and plate weldment to the tube.
For a designer it is important to know that how big base plate or bigger base welded structure will be handled during the fabrication and handling process. Special care needs to be taken care of flatness if the base size is very long.
Depending upon the weight, the eyebolt size are selected for lifting holes on the base plate. Generally, provision of 4 / 5 / 6 eye bolt are made, based on the magnitude of job done. This eye-bolt helps in lifting the base plate from one place to the other place for movement purpose.
Ø Base plate or welded structure
1.) The base plate can be fabricated by using welding technology on ready-made plates or we can use the readily available standard tubes in round or square shape to fabricate the base plate.
2.) The Manufacturer makes 4 dowel holes at 4 corners and puts small aluminum plate marking X, Y & Z coordinates of dowel holes.
3.) The base unit of the fixture must be strong enough so that deflection of the fixture is as minimum as possible. This deflection of a fixture is caused because of forces of welding, clamping of the workpiece.
4.)The base unit may be built from simple sections so that other units may be fastened with screws or welded whenever necessary. Those parts of the fixture that remain permanently with the fixture may be welded. Those parts that need frequent changing may be held with the screws.
5.)The base unit should cover all the units with its outer periphery including the opening.
The base unit should be parallel to the floor. To make necessary adjustments there should be the provision of height adjusting mechanism. The designing of Swivel Clamp unit is similar to that of a clamp unit. But, one change in the swivel clamp unit is that, the clamp arm is actuated by using the linear acting power cylinder.
Q.3)
Ø DUMP UNIT
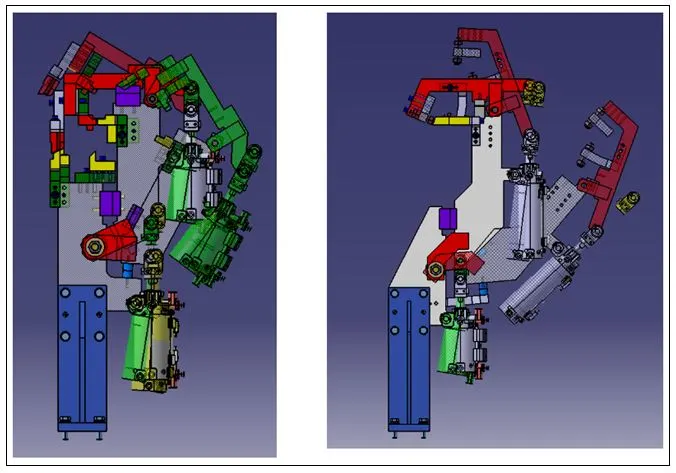
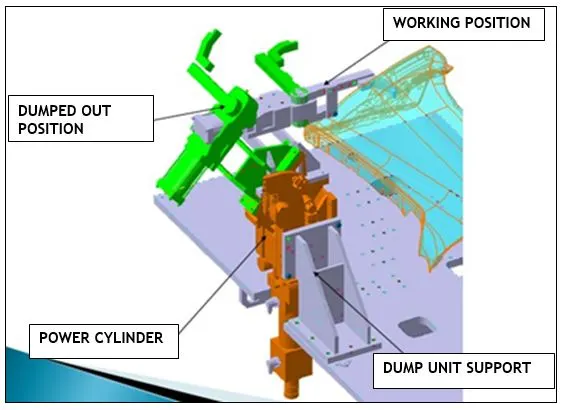
A dump unit is a positioning unit that is used to position car body parts in BIW welding fixtures when there are geometrical constraints that prevent the use of standard positioning units, such as clamp units and pin units.
Dump units are typically more complex and expensive than standard positioning units, but they are necessary in some cases to achieve the required accuracy and precision.
The below images show the complex positioning of the BIW PANELS, to perform the critical operation in precision and accurate manner.
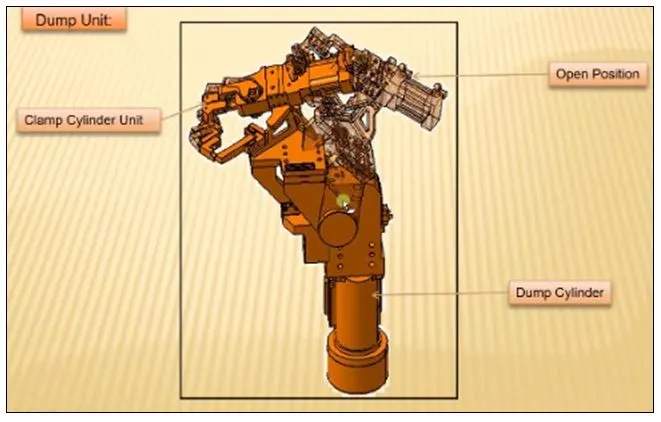
Properties of Dump Unit
Ø To ensure proper resting of the BIW panel, which is being welded and to restrict the motion of the panel the dump unit comes into picture.
Ø To ensure zero rotational of the panel, we have to fix it in correct position her by using pins or side blocks or magnets, to prevent from further movement.
Ø The clamping force delivered by the cylinder, should be such that, when performing operation on the BIW panel, there should be no movement of the clamp arm of the clamp unit.
Ø Dump unit should have right proportion of shimming for adjustment of the BIW panel.
Q.4)
POINTS TO BE CONSIDERED WHILE DESIGNING A DUMP UNIT
The following are the points which have to be considered while designing a dump unit: -
1.) Dump unit requires a quite more of an area, while compared to the other units like clamp unit. Due to the complexity of the dump unit to hold complex parts of BIW panel, the dump unit has to be designed by keeping in view of the working space.
2.) Due to the complex nature of dump unit, one of the major parameters that has to be focused is on the weight of the dump unit.
The Dump unit should be placed on a strong base plate, which can sustain the weight.
3.) The dump units are to be operated by using the pneumatic cylinder. The travel length of the pneumatic cylinder should be sufficient enough to perform the clamping and de-clamping operation with ease, without damaging the BIW panel.
The right amount of air supply pressure to the cylinder will help the linear motion of the piston rod to perform its function efficiently.
4.) The Dump unit design should satisfy the ‘3-2-1 PRINCIPLE ‘of fixture design. It is also known as a six-pin or six-point location principle. In this, the three adjacent locating surfaces of the blank (workpiece) are resting against 3, 2, and 1 pin respectively, which prevent 9 degrees of freedom.
Q.5)
SLIDE UNIT
A slide unit is a positioning unit that is used to position fixtures, weld guns, units, or robots into specific position for performing operations on the BIW panels. It is a common component of body-in-white (BIW) welding fixtures, which are used to hold and position car body parts together during welding.
It contains a sliding bed, which consists the respective fixture unit, which has the respective tool to perform the operations on the BIW panel.
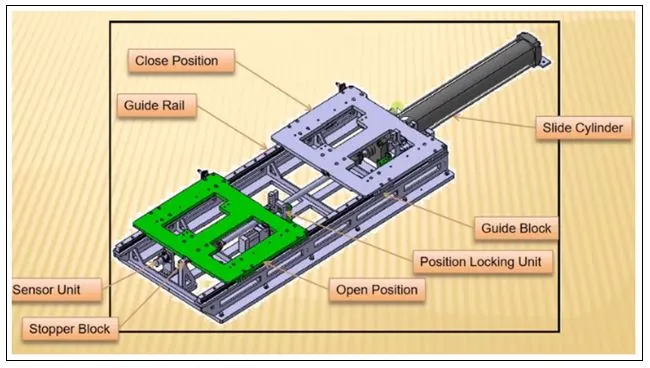
The components of the slide unit are shown below: -
1.) Slide Cylinder
Slide cylinder actuates the guide block to slide on the guide rail to perform opening and closing operation.
2.) Position locking unit
The position locking unit helps to lock the position of the guide block to specific positions, particularly during opening and closing of the guide block.
3.) Stopper Block
The Stopper block limits the overtravel of the guide block. The Stopper is placed on the extreme end of the unit.
4.) Sensor Unit
The Sensor Unit is used to provide the feedback to the ‘sliding cylinder’, to sense whether the Guide block has come to open position or closed position.
The sensor unit like proximity switches are non-contact type sensor units, largely used for providing the feedback signals to the control unit.
Slide units are used in BIW welding fixtures for a variety of purposes, including:
v To position car body parts in the correct location for welding.
v To move car body parts into and out of the welding area.
v To position weld guns in the correct location relative to the car body parts.
v To position robots in the correct location to perform welding operations.
Slide units are a critical component of BIW welding fixtures, as they help to ensure that car body parts are welded together accurately and precisely.
Benefits of using slide units in BIW fixture design:
1.) Accuracy and precision: Slide units provide a very accurate and precise way to position car body parts and weld guns. This is important for ensuring that welds are strong and consistent.
Sliding units are used in BiW fixtures to allow for precision adjustment. These units can be easily moved along their designated axes, enabling the fine-tuning of the fixture’s position. This is crucial for ensuring that the vehicle components align correctly, as even the slightest misalignment can lead to issues in the final product.
2.) Flexibility: Slide units can be used to create a variety of different fixture designs. This makes them a versatile and flexible solution for a wide range of welding applications.
Another advantage of sliding units is their flexibility. They can be adapted to various fixture designs and vehicle models. This adaptability is invaluable in an industry that constantly evolves with new vehicle designs and production techniques. BiW fixture designers can save time and resources by reconfiguring existing fixtures rather than creating entirely new ones.
3.) Durability: Slide units are typically made from durable materials, such as hardened steel, which makes them able to withstand the harsh conditions of a welding environment.
4.) Efficiency: Efficiency is a key driver in automotive manufacturing. Sliding units allow for rapid adjustment and repositioning of fixtures, reducing downtime and increasing productivity. As a result, the assembly line can maintain a steady pace, leading to a higher output of vehicles.
Q.6)
POINTS TO BE CONSIDERED WHILE DESIGNING A SLIDE UNIT
The points to be considered while designing a slide unit is shown below: -
a.) Load capacity: The slide unit must be able to support the weight of the car body part or weld gun that it will be positioning.
Usually, the BIW panel that will be placed on the slide unit, should have the sustainability to carry the weight of the panel. The load of the panel has to be distributed equally across the slide unit, so that overall deformation is reduced while performing operations.
b.) Accuracy and precision: The slide unit must be able to position the car body part or weld gun with the required accuracy and precision.
The slide unit should have the designated locator pins, for placing the BIW panel on it. The locator pins assures that the required degrees of freedom are restricted such that the flickering of the panel doesn’t occurs, while performing the welding operation with accuracy and precision.
c.) Speed: The slide unit must be able to position the car body part or weld gun at the required speed.
d.) Durability: The slide unit must be able to withstand the harsh conditions of a welding environment.
Few of the rigorous welding operations which are performed on the BIW panel requires strong clamping forces and sturdy design of the slide unit to withstand the jolting forces acting upon it. The slide unit should be designed keeping in view with the durability factor.
Overall, slide units are a versatile and effective way to position car body parts and weld guns in BIW welding fixtures. They provide a high degree of accuracy, precision, and flexibility, making them a valuable tool for welding engineers.