Week 6:- Clamp Unit & Pin-Clamp Unit Design Challenge
DESIGN OF SWIVEL CLAMP UNIT AND PIN CLAMP UNIT
OBJECTIVE:
To design three different types of swivel clamp unit with different riser ,blade,and clamp arm for the given car panel and to design a pin clamp unit for the given car panel.
CAR PANEL:
- There are 5 parts in the given car panel, 4 small parts and 1 large part which is main part of the car panel.
- These 5 parts needed to be welded together , for that these parts needs to be fixed using clamp and pin units.
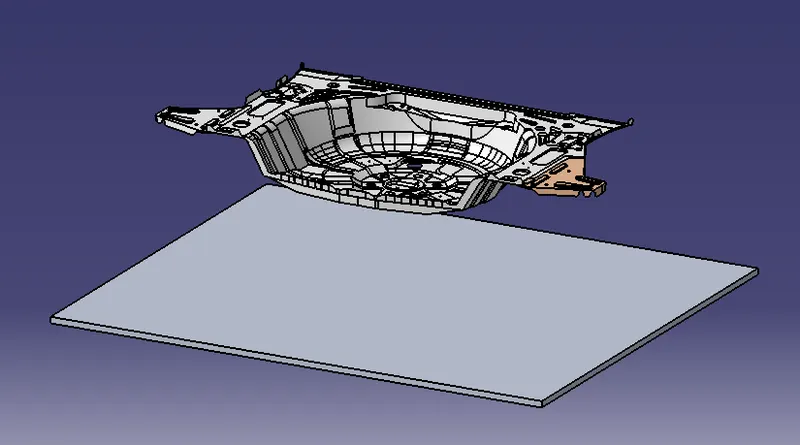
TYPES OF CLAMP UNIT USED TO CLAMP THE CAR PANEL
- Power clamp unit.
- Swivel clamp unit.
To weld these parts ,they must be fixed using 3-2-1 principle:
3-2-1 PRINCIPLE:
- Fixture must correctly locate a workpiece in a given orientation with respect to a cutting tool or measuring device, or with respect to another component.
- Locating and clamping are the critical functions of any work holding fixture.
- A workpiece free in space can move in an infinite number of directions.
- For analysis,this motion can be broken down into twelve directional movements or "degres of freedom".
- All twelve degrees of freedom must be restricted to ensure proper referencing of workpiece.
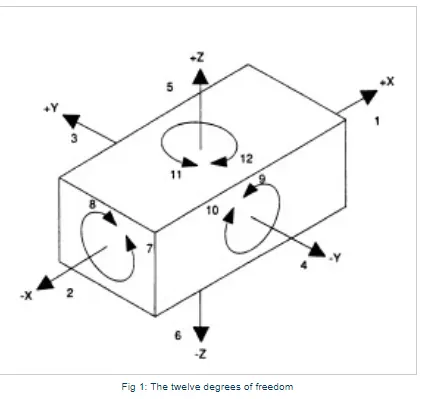
The best and most effective method of part location is reffered to as the 3-2-1 method.
6 Translational degeers of freedom : +x,-x,+y,-y,+z,-z.
6 rotational degrees of freedom:
- C-ROT around X - axsis
- AC-ROT around X- axsis
- C-ROT around Y- axsis
- AC-ROT around Y - axsis
- C-ROT around Z- axsis
- AC-ROT around Z - axsis
If we fix the clamps as per the 12 degrees of freedom listed above,then we can arrest the panel in a fixed position.
6- degrees of fredom are restricted by 2- pin units.
6- degrees of freedom are restricted by 3-clamp units and rest units.
CLAMP UNIT:
Clamp unit is a unit designed to hold /clamp the car panel with NC blocks/mylars / rest by using a pneumatic clamp cylinders .
PARTS OF CLAMP UNIT:
- Mylar/NC block/Finger: Finger is a movable part which is used to hold the car part from top against backup and they are usualy mounted on the clamp arm.
- L-block: L - shaped blocks are used to ount the finger to clamp arm, besides allowing adjustments for locator pin in two directions.
- Shim/Spacer: They allow the finger to be moved to the correct xyz locating and allow the customer to make adjustments to improve the quality of their product.
- Blade: Part onto which the aforeside element are attached to.
- Riser: L- shaped or T shaped tall block which regularly patterened holes to attach the above mentioned parts in modular way blade space.Riser is either a make part or standard part.
- Stopper: The function of stopper is to restrict clamp going beyond the limit.Stopper is mounted between clam arm and rest/blade.Stopper has two parts male and female , when this two parts meets they restrict motion.
CONSIDERATIONS WHILE DESIGINING CLAMP UNIT:
1.STUDY OF PROCESS PLANNING DOCUMENT:
- Process planning document is the document which contains the datas and other informations related to design clamp uniot.
- process documents should contain following informations which are necessary to design clamp unit.
- No. of sheet metal pannels to be welded.
- In this project there are 5 sheet metal parts needs to be joined or welded together.
- Total no. of spots.Weld gun details If its is already recomended by process engineer study it in detials like shape and its type ( c,x or Y)Study the PLP ( principle locating points) data along with the nearby spot data.
2.CAD SOFTWARE:
- If you are using any specific CAD software as per the customer requirement eg. CATIA,UG,FIDES..
- Understand the customer guidelines how to create the fixture,unit,weldment and base fabrictaion.once u have understand the cad software methodology to be followed for design of single part,unit assembly and base then start the design by adding the panel assembly in your fixture or unit assembly.
3.HEIGHT SELECTION:
- Take an overview of the working height if you are having manual welding.For robtic welding it's important to see the working height in consideration of the robtic gun,turntable height if manual loading is done.
4.PANEL SELECTION CREATION:
- Take a section at PLP either in clamp opening direction or normal direction .
- Sections should be normal to the base plate.Panel section through X,Y, or Z direction passing through PLP.
- Section will be finalising the shape of the clamp and rest block.
5.CONSIDERATION OF REST AND CLAMP BLOCK:
- If standard mylar has to be used(few companies make standard height and length of steel blank with few holes and dowels for clamping) then select the proper blank size as per the requirement; consider 5 mm above panel.
6.CLAMP CYLINDER SELECTION:
- Select the clamping cylinder as per the pivot point distance from the PLP.
- You may choose various cylinder 50 dia, 63 dia ,80 dia as per the requirment.
7.RISER:
- As per the company or OEM,Tier 1 standard use the different standards mounting risers.
- Do not forgot to add the 10mm shim (5mm solid+5mm shim pack),in few companies 3 mm shims are used .Make connection plate between riser and mylar.
8.HARDWARES:
- Add all the hardware screws , dowels and washer as per the size.Ensure all these hardwares are easy to dismantel.
9.CLAMP ARM OPEN POSITION:
- Check all the clamp open position and ensure that there is fouling with panels or any other surrounding units.
CLAMP CYLINDER:
- Clamp cylinder can order by giving following inputs to manufacturer.
- Name of the clamp cy;inder is CKG_1B_100Y
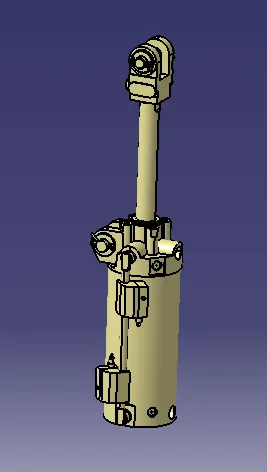
EXPLAINATION:
CKG - SERIES OF CYLINDER
1B - CLEVIS WIDTH=19.5
63 - BORE SIZE
100 - CYLINDER STROKE IN MM
y - END BRACKT i.e. DOUBLE KNUCKLE JOINT(M6 WITHOUT TAP).
SWIVEL CLAMP UNIT 1
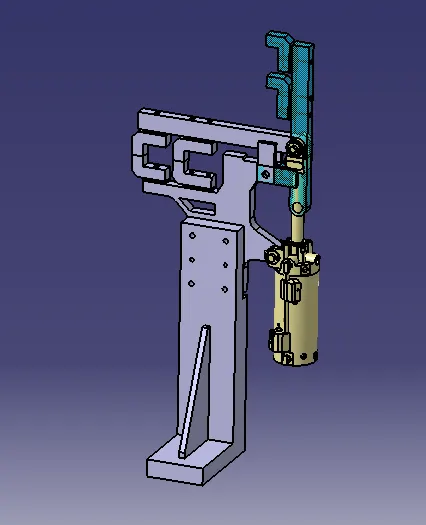
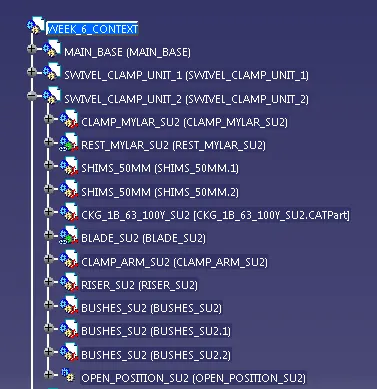
SWIVEL CLAMP UNIT 2
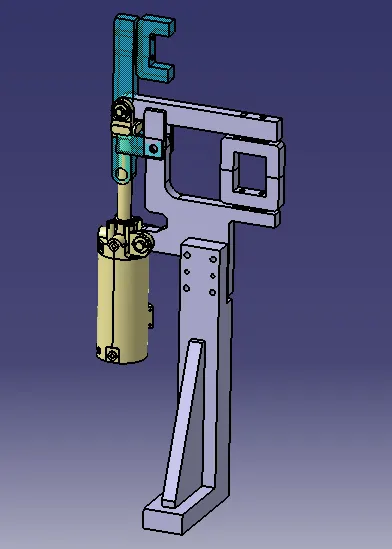
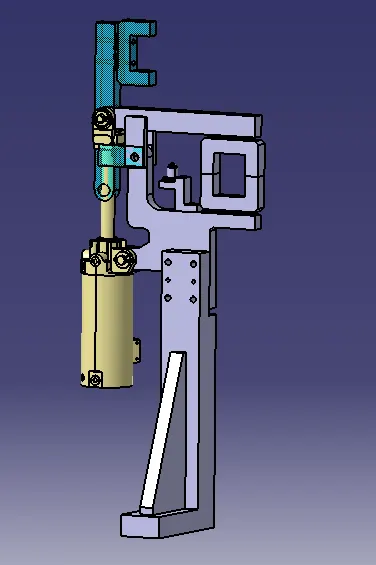
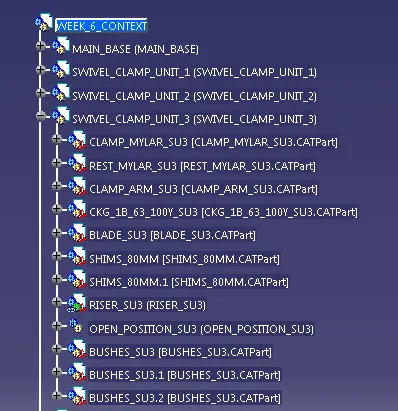
SWIVEL CLAMP UNIT 3
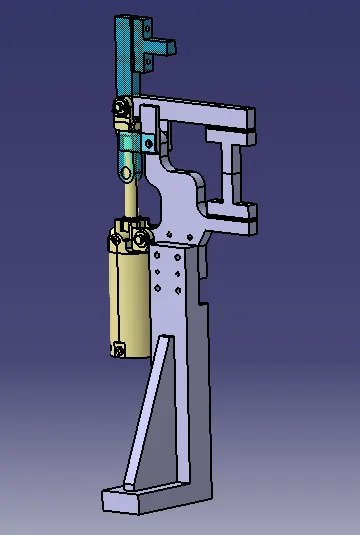
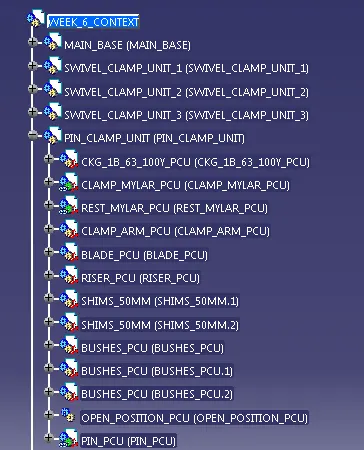
PIN CLAMP UNIT
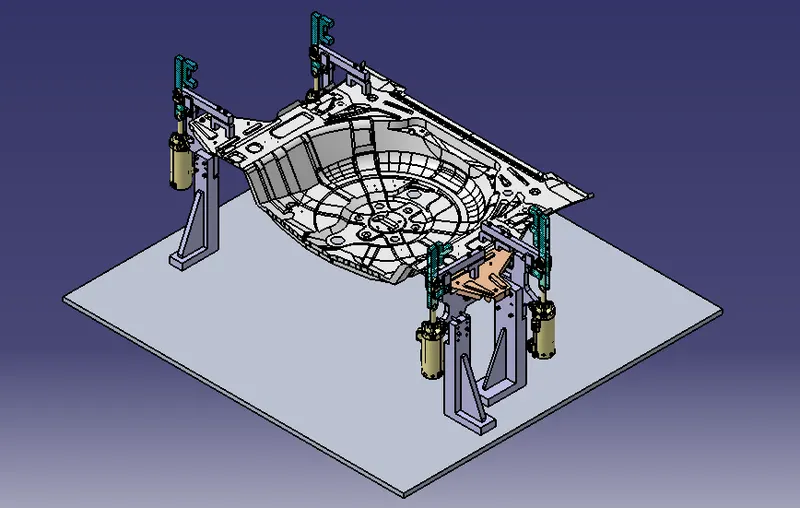
OVERALL MODEL OUTCOME
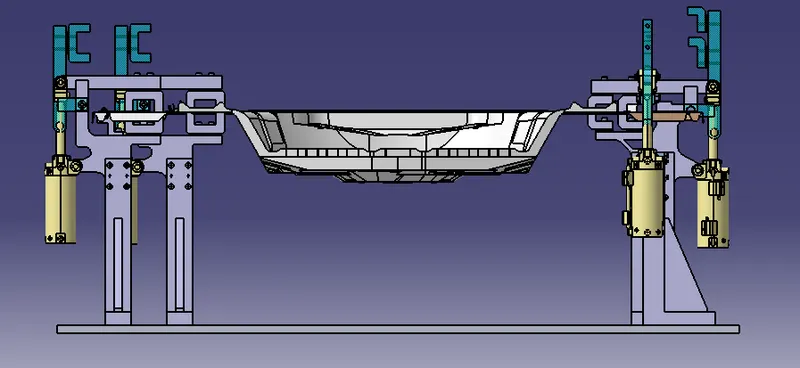
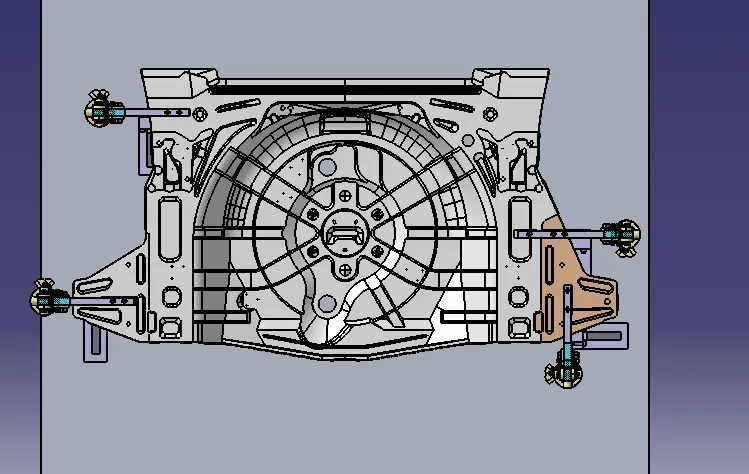
TREE STRUCTURE
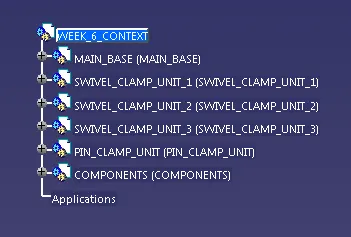
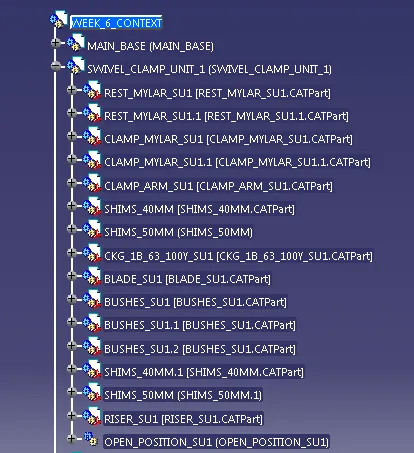
FACTORS SHOULD CONSIDER WHILE DESIGINING CLAMP UNIT:
- Should use standard part as possible i.e.NAAMS standard.
- There should be adequate space between cylinder and other parts like riser,car panel.Because cylinder moves or swing while opening and closing.
- Pin clamp unit is use where two panel or component are located and clamp for welding.
- clamp make in such a way that it it clamp two car panel at once.
- every clamp mylar/NC blocks should have rest mylar or unit.
- clamp unit has shims in only one direction .
- ALL parts should snap and butt properly to eachother .
- Make sure that parts of clamp unit are 10 -12 mm away from the car panel.
- Design tree should structured in way that make part on the top and followed standard part.
- The position of clevies joint pin will be in one line.
- Avoid any clash , It will not rise issue at assembly.
- product should designed in such a way that it will easy to make ,assemble and quality check.
- we should preferably use quick acting clamps.The clamping method must not damage our work piece.
- clamp should open in such a way that clamp arm moves away from the operator.
- There must be adequate clearence for loading and unloading .so that the process becomes fast and easy.The variation in size must be accepted.
- Avoid sharp edges and corner ,they can harm operator and cause to the serious injury .provide chamfer or fillet to the corner.
CONCLUTION:
Hence i designed 3 different types of clevis clamp unit with different riser,blade and pin clamp arm for the given car panel.