Week 3:- BiW Fixture Design Methodologies Challenges
1. Design Methodology:
In this methodology we learn about three design processes, we're going to study how do we proceed while doing a design. And one of the things that we take care of structuring or design tree so we'll be learning how to structure the design tree, and how to name the particular component or particular assembly, or the part of an assembly, which is very easy to read and very easy to understand.
Design methodologies is nothing but the steps followed during the concept designing stages of fixture design.
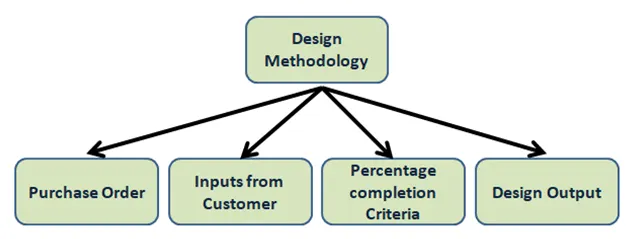
1.Purchase Order:
We start designing after customer gives us purchase order. So, basically it is indication to start designing of particular fixture. Purchase orders can be an essential part of enterprise resource planning system orders. Purchase order is a order from customer for start of the work. After offer has been finalized customer will be releasing the LOI/PO(Purchase Order).
Once PO is released we have to start the work.
After PO from the customer we have to prepare the schedule.
Purchase order is the confirmation document from customer to proceed the committed work for them.
2.Inputs from Customer:
Customer gives us requiremements or specifications of fixture before starting actual design work. So, we have to design fixture by considering all the points of customers.
3.Percentage Completion Criteria:
To complete design in time we have to create schedule or time plan called Percentage Completion Criteria. In this we mention all activities related to design and time required to complete that task like concept design, final finished design and 2D of all units in fixture etc.
4.Design Output:
Design Output consist of lots of data like 3D and 2D documents, VMC IGS files, STEP files, gas-cut or laser-cut files in dwg format and BOM, etc. We have to give these data to our customer as design output.
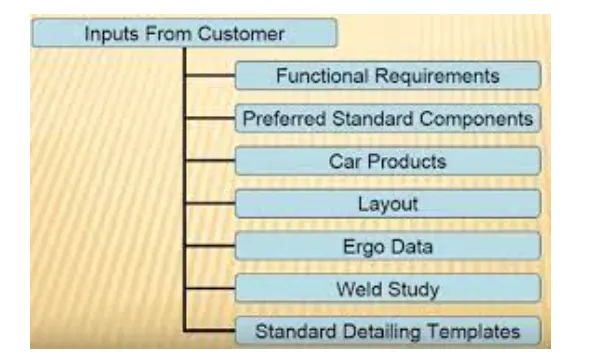
2.Inputs required from the customer to start designing a fixture:
1.Function Requirement:
Generally, function requirement means for what purpose we are going to design fixture like welding, gluing or riveting fixture and inspection fixture.
2.Preferred Standard Components:
While designing fixture, we have to use standard components as much as possible to save time, money and efforts to design, manufacture that non-standard components.
3.Car Product:
It consist of 3D, read files, geometric tolerance and PLP (principle locating points) of fixture.
4.Layout:
Layout is nothing but management of space which helps to understand process or flow of work of entire assembly line.
5.Ergo data:
Every company have standard ergo data and they provide it to fixture designer to design fixture considering that points Ex. height of fixture is decided according to ease while working on fixture. So, we have to design a fixture by considering safety, easy and fool proof design. The ergo data is mainly used to make the operator comfortable which may lead to improve the efficiency in cycle time& production.
Ergo data provides inputs like platform height, maximum & minimum reach from operator to fixture, maximum & minimum height of the fixture, whether the child parts/assemblies are visible while clamping or loading & unloading. Also provises information like loading height, working safety zone of operator, etc.
6.Weld Study:
In this input, customer specify which type of welding (spot or seam) is required to join components according to which we have to design fixture.
7.Standard Detailing Templet:
Customer gives us standard detailing templete, so we can use that to detail or diminesioning components according to that templete.
3.The input we get from "Car Products":
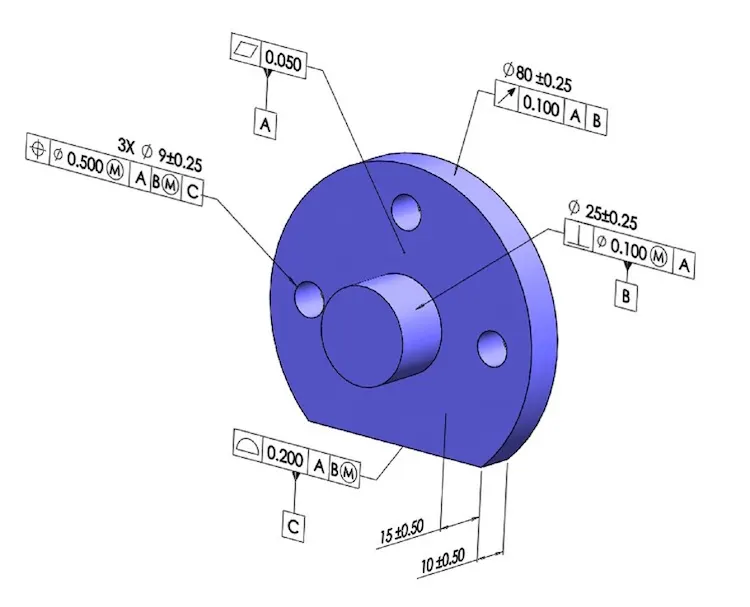
1.GD & T:
Geometric Dimensioning and Tolerancing, is a system for defining and communicating design intent and engineering tolerances that helps engineers and manufacturers optimally control variations in manufacturing processes.
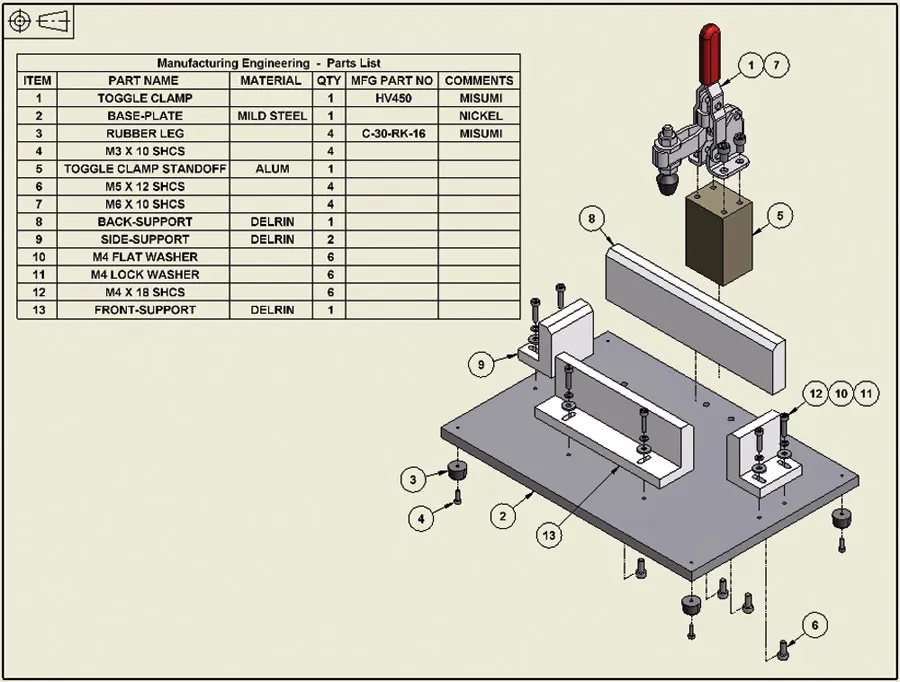
2.Part List:
It states about the parts and assembly style. Part list consist of unique part names of each and every parts in assembly and each part has its own part number which helps while assembly process to identify each and every part in assembly.
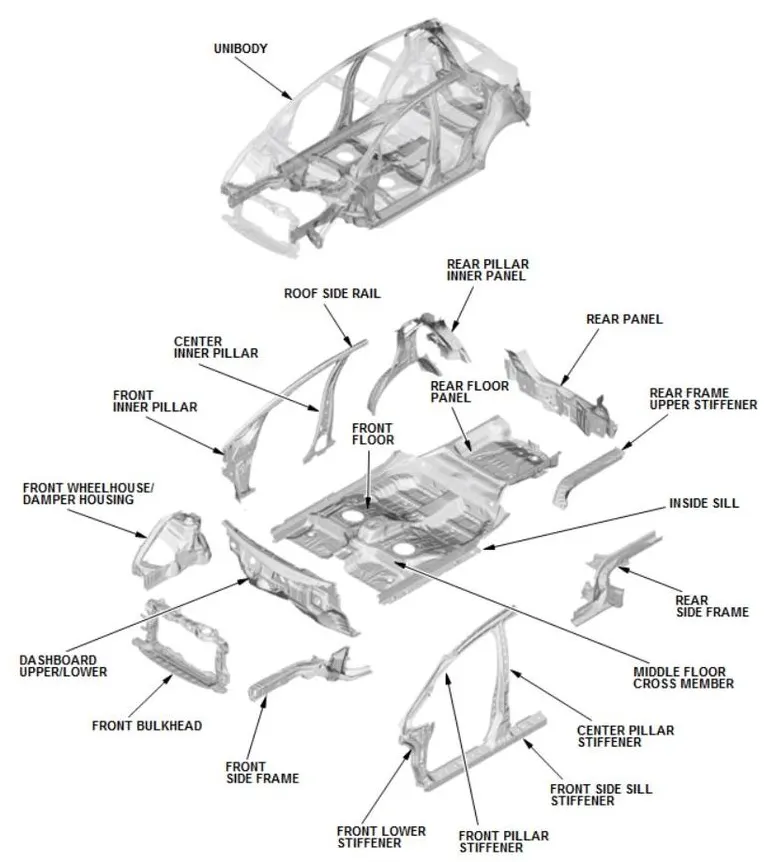
3.Cad Files of Car Part:
3D cad files of parts are necessary while designing fixture.
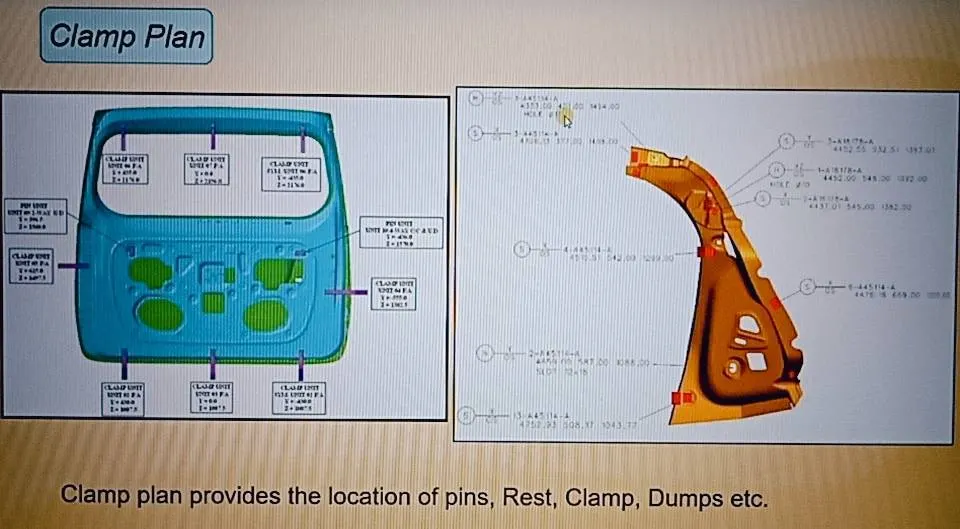
4.Clamp Plan:
Clamp plan provides the information of location of pins, Rest units, clamp unit, Dumps etc. It is the important input from customer.It is one of the important data while designing fixture because clamp plan mentions location of clamps in which component is going to clamp.
5.Product Assembly Process Sheet:
In product assembly process sheet, sequence or stages of assembly of components are given.
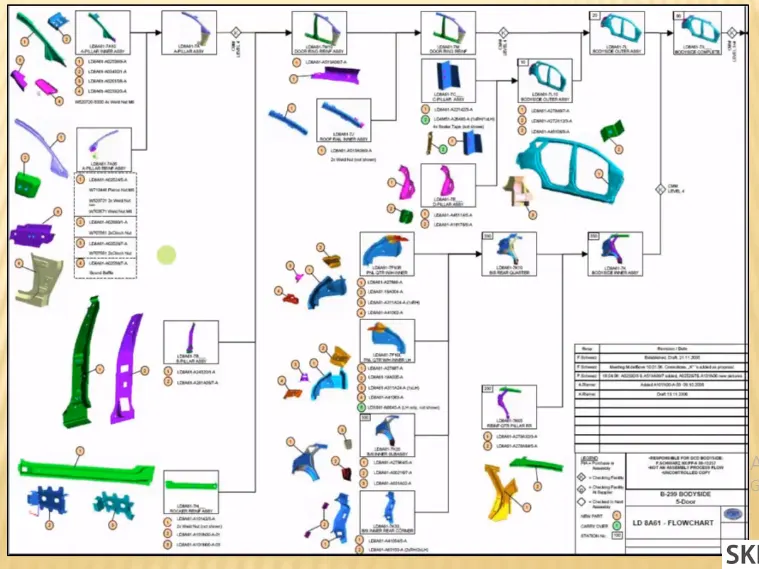
4.Clamp plan:
Clamp plan provides the information of location of pins, Rest units, clamp unit, Dumps etc. It is the important input from customer.It is one of the important data while designing fixture because clamp plan mentions location of clamps in which component is going to clamp.
5.Purpose of a Layout:
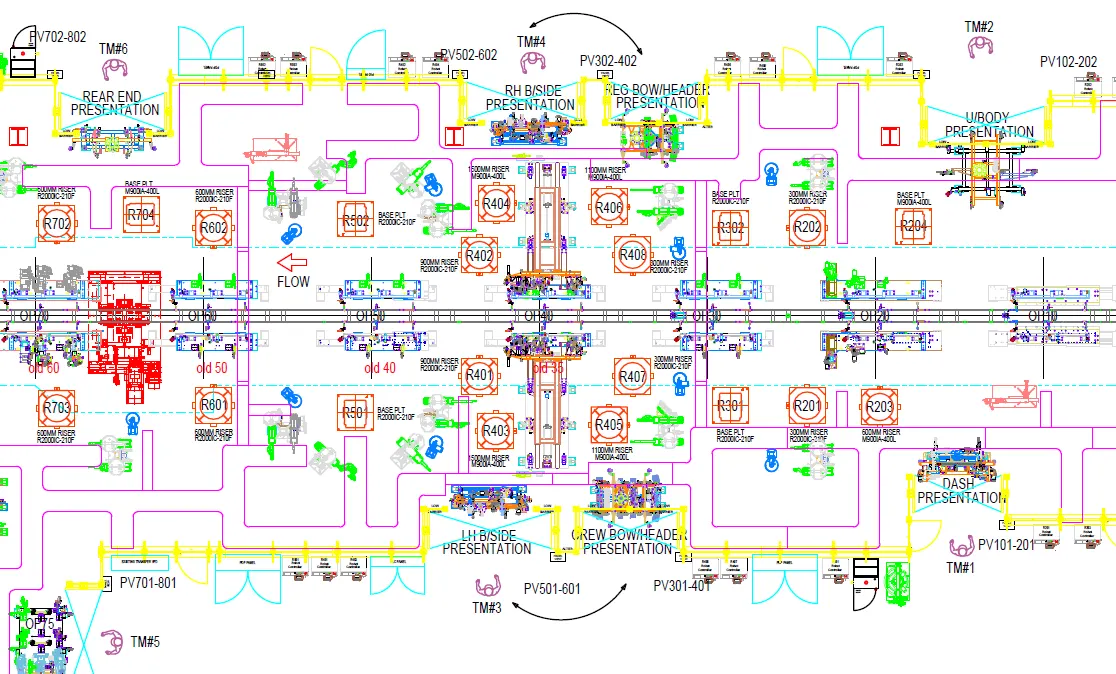
Layout shows the entire assembly plan to understand the process.Layout provides the information of flow of parts, station pitch, robot stations, accessories like tool changers & tip dressers, sub assembly links, plan form height, loading/unloading sequence/height.
Layout is nothing but management of space which helps to understand process or flow of work of entire assembly line. Below image is one of the example of layout.
6.Ergo data:
Ergo data provides inputs like platform height, maximum & minimum reach from operator to fixture, maximum & minimum height of the fixture, whether the child parts/assemblies are visible while clamping or loading & unloading.
Every company have standard ergo data and they provide it to fixture designer to design fixture considering that points Ex. height of fixture is decided according to ease while working on fixture. So, we have to design a fixture by considering safety, easy and fool proof design. Ergo Data is used to reduce human errors, increase productivity, human comfert and safety.
Also provides informations like loading height, working safety zone of operator, etc.
7.Weld study:
Welding engineering is a complex field that requires expertise in many different engineering disciplines. The welding engineer must take advanced courses in metallurgy (including welding metallurgy), material science, mechanics of materials, thermodynamics, chemistry and fundamentals of all welding processes.
Geo weld points:
The Geo weld points are which is planned in the Geo fixture.
These weld will determine the position of the panels as per the given data in drawing.
The geo weld points are represents in red sphere in the weld study inputs given by the customers.
Respot weld points:
The respot weld points are planned in the respot tool.
These weld will determine the strength/stiffness of the panel/components.
The Respot weld points are represent in green spheres in the weld study inputs given by the customers.
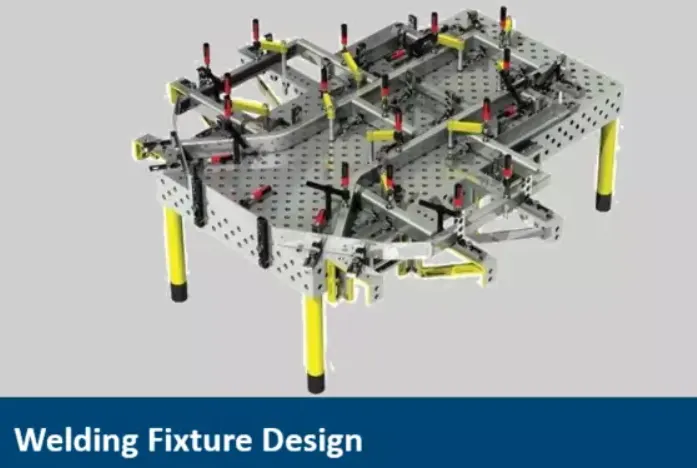
8.What are the criteria for percentage completion in the designing stage?
The percentage completion criteria is followed in the designing stages & dispatch stages of welding fixtures.
This percentage completion criteria is followed to trace the project whether it matches the committed date given to the customer for hand over the projects to them.
Also it helps us to identify the stages in the projects like how much the project is completed and what are the further stages are in pending, to complete which helps us to complete the projects on the committed time and date.
The percentage completion criteria is divided into four stages to identify the percentage of the completion of work.
The four stages of percentage completion criteria are as follows,
- Input & concept design.
- Concept approval & simulation check.
- Design freezing & detailing.
- Check & final dispatch.
1. Input & concept design:
If the project is in the stage of Input & concept design then the percentage completion criteria of the project will be between 0 – 25%.
After the completion of input & concept design then the project will be moved to concept approval & simulation check which is the second stage in percentage completion criteria.
2. Concept approval & simulation check:
If the project is in the stage of concept approval & simulation check then the percentage completion criteria of the project will be between 25% - 40%.
After the completion of concept approval & simulation check then the project will be moved to design freezing & detailing which is the third stage in percentage completion criteria.
3. Design freezing & Detailing:
If the project is in the stage of Design freezing & detailing then the percentage completion criteria of the project will be between 40% - 85%.
After the completion of design freezing & detailing then the project will be moved tp check & final dispatch which the fourth & the last stage in percentage completion criteria.
4. Check and final dispatch:
If the projects is in the stage of check & final dispatch then the percentage completion criteria of the project will be between 85% - 100%.
After the check the project will be finally dispatched successfully to the customer.
9. "Output" in design:
In BIW fixture design or any industry. We don't only just design a particular component and just give the CAD file to the customer, you have to give a lot of documents like 3d documents,2d documents, which is the detailing part, and as well as other factors as well like bom, bom bill of material and other documents as well about this particular component and their standards, all has to be submitted to the customer.
The output is 3D models and the 2D drawing of the tools
1.Unitized Tools
2.Non-Unitised Tools
1.Unitized Tools:
In the unitized tools testing requires two types of drawing sheet,which is one key sheet and layout sheet.
So example of a unitized tools are fixtures,tools So where exactly multiple units are a placed.For example, the entire assembly welding fixtures,where a pin unit,clamp unit,rest unit and the panel, everything is included so that for those things.
Key sheet :
An index of units and their placements on the tool base.It will have an orthogonal view of the fixtures including a numbered balloon drawing mentioning the units.
Layout sheet :
A detailed drawing of individual units to include all of their components.For the Non unitized tool no need of key sheets. As they can stand alone, the drawing can be detailed completely on a layout sheets.
So, it is basically an index of units and placements on the tool base, so the key sheet going to show you the placement and the location of that particular tool on the tool base where exactly the tool is placed. And what is his exact position in a particular place.
2.Non-Unitized Tools:
Tools that can stand alone and can be detailed completely on a layouy sheet.
Non unitized tools are basically tools like Stands and tool changers is also an example of an non unitized tools where you don't need key sheet, you can actually used to layout sheet and complete the entire documentation of the particular component. So this is as known non unitized tools.
The Design Output Should Compile Following Points:
- Approved standard components are to be used wherever possible.
- Design must be as simple & economics as possible.
- Design must be comply with all current safety & ergonomic requirements.
- Design must provide for controlled & damage free handling of product.
- Adequate error proofing provision must be incorporated into each design by proving proximity switches, rough locators, etc.
- The weight of the moving parts must be kept to a minimum while maintaining maximum strength.
10.Structuring a design tree:
Structuring a design tree is very necessary while designing fixture because it help to identify all manufactured part in whole fixture. Every customer company have there own standard. This will help us during design study, manufacturing and inspection to avoid errors.
If we ignore structuring a design tree it will crete confusion to understand design and may errors will appers in fixture.
Steps to structuring a design tree:
Step 1:
Create new à Product à click OK (by clicking ok now you will enter into a product window)
Step 2:
Then right click product in a structure tree à go to properties à rename in part number (As we created a product we have to mention the total assembly name of the fixture) à click ok.
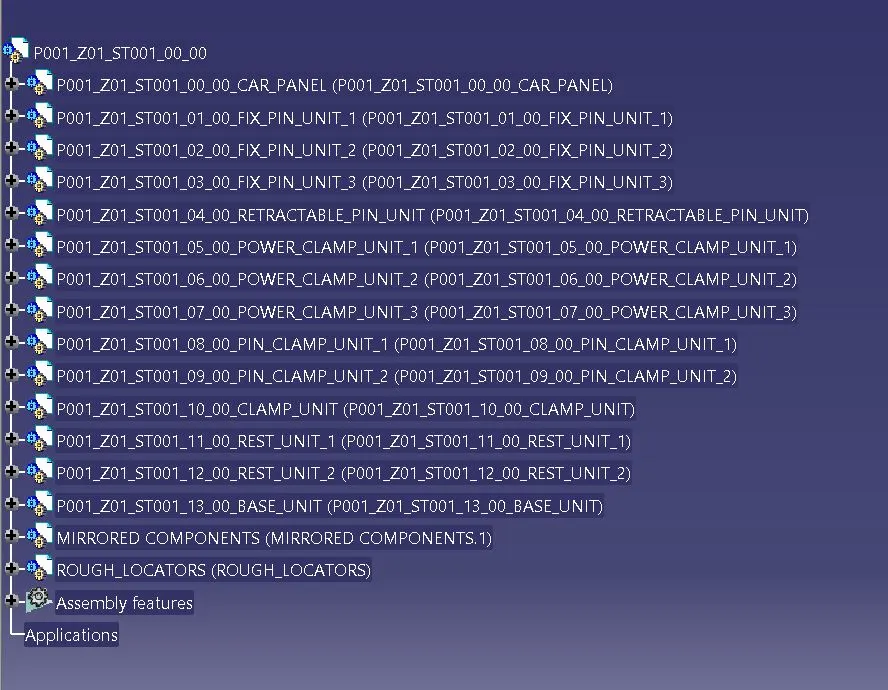
The naming of the assemblies / parts / units have certain standard procedures, which I have clearly explained below.
The product name is title of the fixture. The renamed titled should be à P001_Z03_ST09_00_00_R
P001 – represent the project name.
Z03 – Zone name.
Panel name will also be mentioned in some case.
ST 09 – Station name / J03 – Jig name will be mention sometimes.
00 – unit name.
00 – Part number.
R/L – is representing the right hand side / left hand side of the panel.
The other renamed title explained in video is
H1L_19A_RRFRA_JG3_00_00_R.
H1L_19A – Project name.
RRFRA – Panel name.
JG3 – Jig name/number.
00 – unit name
00 – Part number.
R – Indicates right side.
11.What are Units?
Unit is nothing but a assembly having specific function like clamping, location or resting. In fixture there are number of units. According to 3-2-1 principle of location fixture is designed having two major purpose of clamp and locate the component for which fixture is designed. Image shows fixture consist of different units.
A unit is a device that has a specified function, especially one forming part of a complex mechanism.
A welding fixture is assembly of different types of units.
As name refers, the different units will be only seen in the unitized tool.
5 Types of units
- Rest unit.
- Fixed pin units.
- Retract pin units.
- Rough locator unit.
- Base unit.
1.Fixed pin unit:
Fixed pin unit is a unit designed to locate the car panel using pins.table
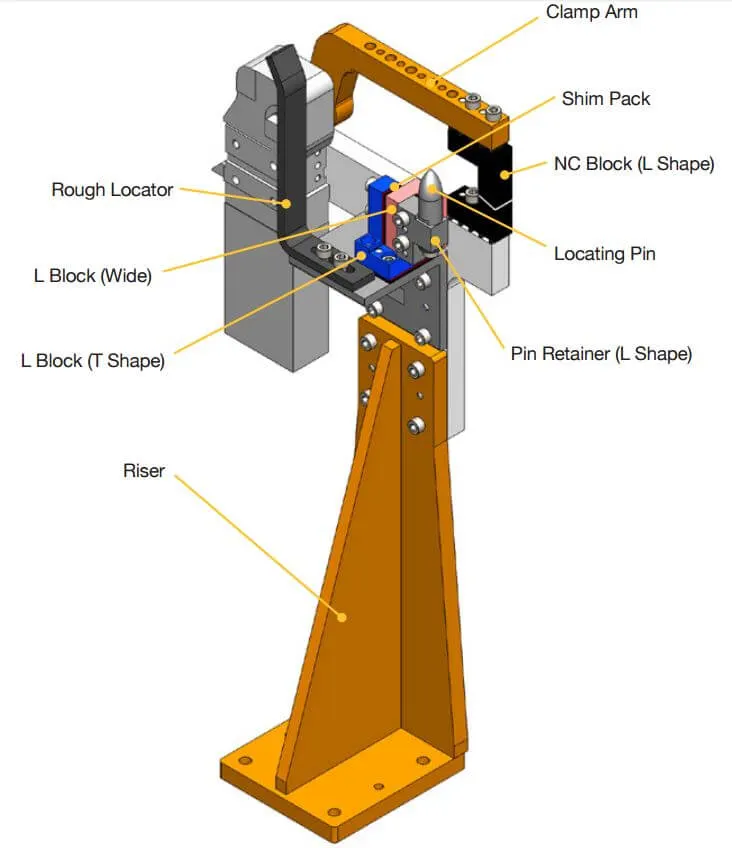
Pin, pin retainer, shims, blocks, blade, riser are the part of fixed pin units.
Pin retainer is used to hold the pin firmly.
Typically, the locating pins are used to locate a body part in a position sufficiently accurate to execute a welding process.
The body part is constrained by a set of appropriately locating pin so total constraint by locating pin should be fully constrained at all times to prevent any movement.
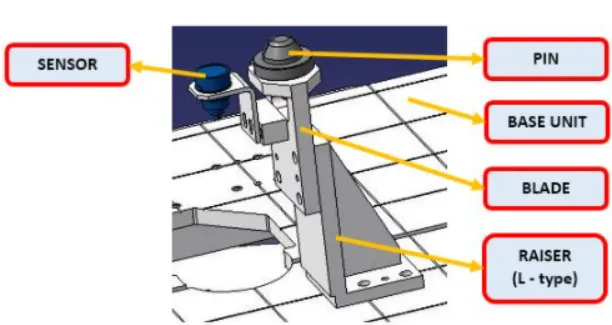
2.Retractable pin unit:
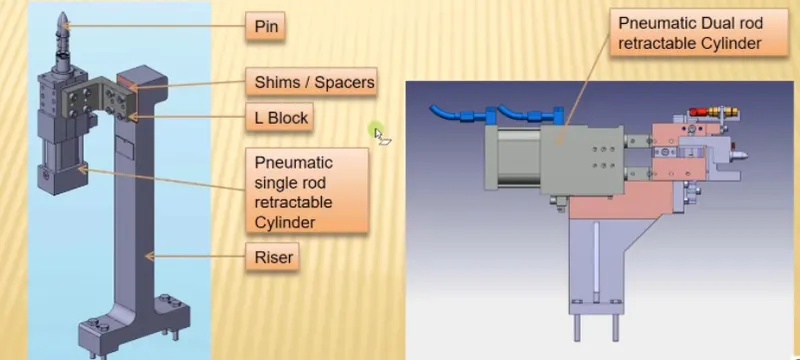
Retractable pin unit is unit designed to locate the car panel using pins, but the entire pin package parts will be mounted on the retractable pneumatic cylinder as shown in below fig 3.
Retractable pin unit is the opposite of fixed pin unit which can be moved up & down also which can be retracted till certain distance.
It is mainly used for unloading the complex panel after welding.
3.Clamping unit:
Clamp unit is a unit designed to clamp or hold the car panel with NC block / Mylars by using a pneumatic clamp cylinder.
Clamping unit is used to clamp the part which is to be welded after location using pin unit.
Clamping is achieved with the help of pneumatic cylinders and clamp arms.
Clamping arm, finger, rest, shims, standard riser, pneumatic cylinder are the parts of clamping unit in general.
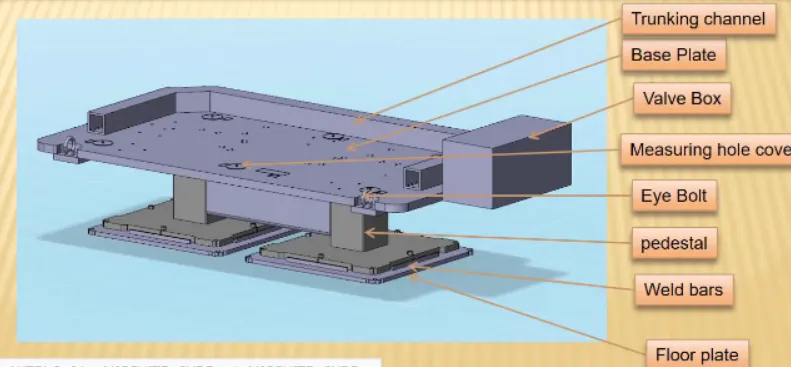
4.Base unit:
Base unit is the unit designed to mount all other units such as clamp unit, pin unit, rest unit etc., of tool, also other parts necessary for a tool like pneumatic valve box, trunk cable path will also be mounted on to be a base unit.
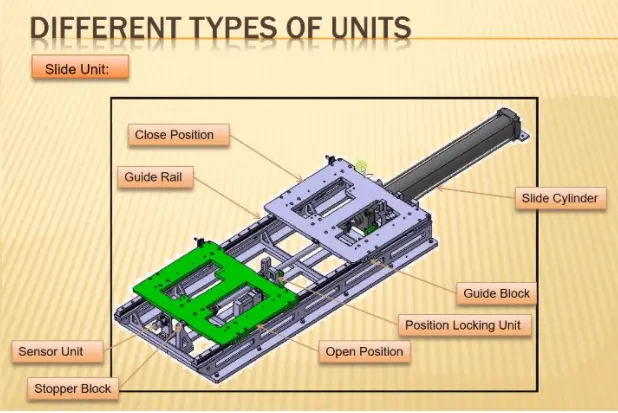
5.Slide unit:
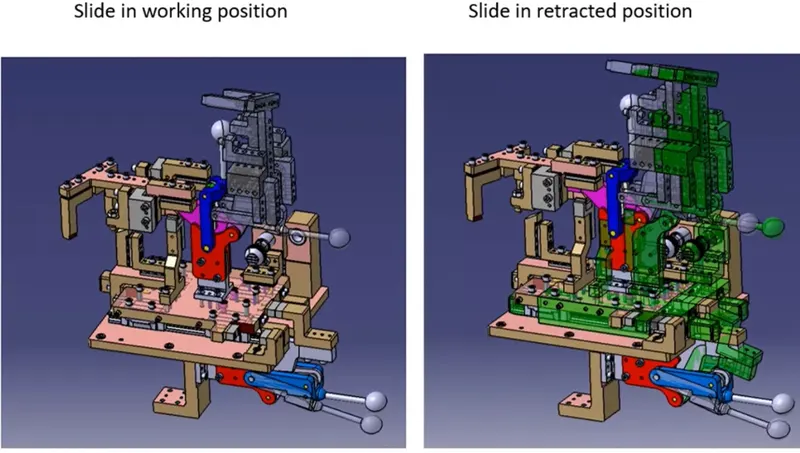
Slide unit is found mostly in complex fixture, where the sliding mechanism will be involved.
This type of unit used when there is some space constraints.
Guide block, guide rail, position lock unit, stopper block, sensors are the parts of slide unit in general.
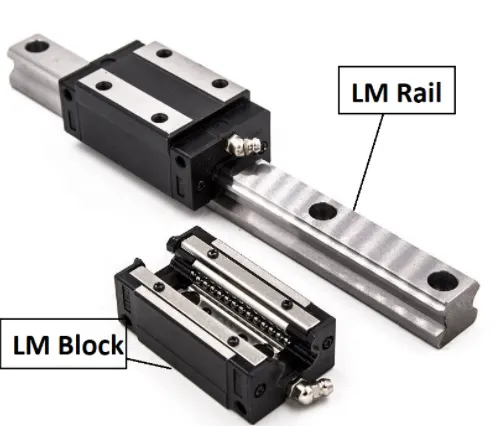
Guide block & guide rail helps to the guide the slide unit. The rail should always be covered to protect against weld spatter & dust by a bellow or a sheet metal cover.
Position lock unit helps the slide to be locked/clamped in the working position.
Stopper block helps to stop/control the entire moving of a slide unit from certain distance, which is placed at the end of the guide rail.
Sensors – The two end limits to be sensed externally by a proximity sensor.
12.Fixed unit:
Fixed pin unit is a unit designed to locate the car panel using pins. Pin, pin retainer, shims, blocks, blade, riser are the part of fixed pin units in general . Pin retainer is used to hold the pin firmly.
Fixed Pin Unit is non movable locating unit which arrest movement of component in fixture.It consist of pin, pin retainer, blade, two way shims or spacer which control X, Y direction adjustment, block and riser.
Purpose of Fixed Pin Unit are as below:
- Main purpose of fixed pin unit is to locate component
- This unit is used arrest 6 degrees of freedom of component
- Two pins are used to locate component. First pin restricts 4 translational motion and other one restricts 2 rotational motion.
13.Different parts of a fixed unit:
- Pin.
- Pin retainer.
- Shims.
- Blade.
- Riser.
1.PIN:
It is used for the location purpose of the panel. Typically, the locating pins are used to locate a body part in a position sufficiently accurate to execute a welding process.
The body part is constrained by a set of appropriately locating pin so total constraint by locating pin should be fully constrained at all times to prevent any movement.
There are dozens of styles of locating pins that can be utilized in a design. One of the most common pins is a stepped pin with either small or large head.
2.PIN RETAINER:
Pin retainer is used to hold the locating pins firmly. Pin retainer is designed to hold the pin in its place and is also used as a rest for the pin. A counter hole drilled on which pin is fit.
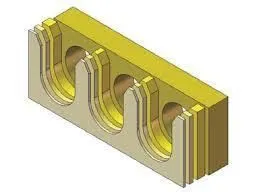
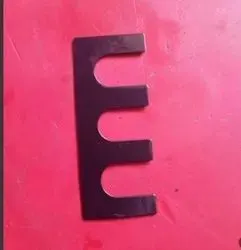
3.SHIMS:
Shims are typically used in order to support, adjust for better fit, or provide a level surface.
Shims may also be used as spacers to fill gaps between parts subject to wear.
Shims are the small parts which comes with the thickness of 0.1mm, 0.2mm, 0.5mm, 1.0mm etc.
These will compensate the stack up tolerance which reflects at the mylars.
We give tolerances to all parts of the fixture. Due to this tolerance the mylars will either lift up moves down from its defined position. To adjust the mylars for getting the defined position we use shims.
Shims will be added above the mylar for adjusting according to tolerance.
4.BLADE:
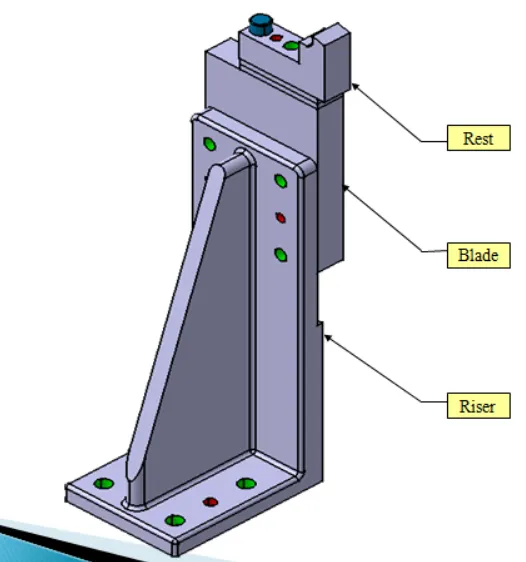
Blade are the plates which are attached to raiser.Blade is also attached or mounted with cylinders, arms etc.
5.Riser:
Riser is the standard part which is used to rise up the height of the while unit. Blades are plates mounted on the riser. Other parts like cylinder, arms etc are mounted on the blade. - Shims are the small part which comes with the thickness of 0.1mm, 0.2mm, 0.5mm etc.
14.Rest units:
Rest unit is unit designed to support car panel using Mylar/ NC block/ rest. Component is rested only, no upper clamp or force applied there.
It is the simplest unit to design because it has fewer parts to design & the purpose is only resting of the car panel. Because of this simplicity the rest unit is combined with other unit to reduce the cost of the overall project.
It can be combined with clamp unit to clamp as well as to rest the car panel. It can be combined with locating unit to locate as well as to rest the car panel. Also locating, clamping & rest unit can be combined together in one unit to reduce cost.
There is no cylinder attached to it. It has rest Mylar, blade & riser & below is different parts of rest unit. Rest unit is also divided into simple support unit, multiple support units & retractable support unit.
15.Basic fundamentals to design a Sensor unit:
Sensor is a device which detect or measure a physical property. The unit which is built to sense the component or car panel using electrical sensors called Unit Sensor. The output signal of sensor is then send to PLC (Programmable Logic Control) for further process. There of different types of sensors such as proximity sensors, laser sensors.
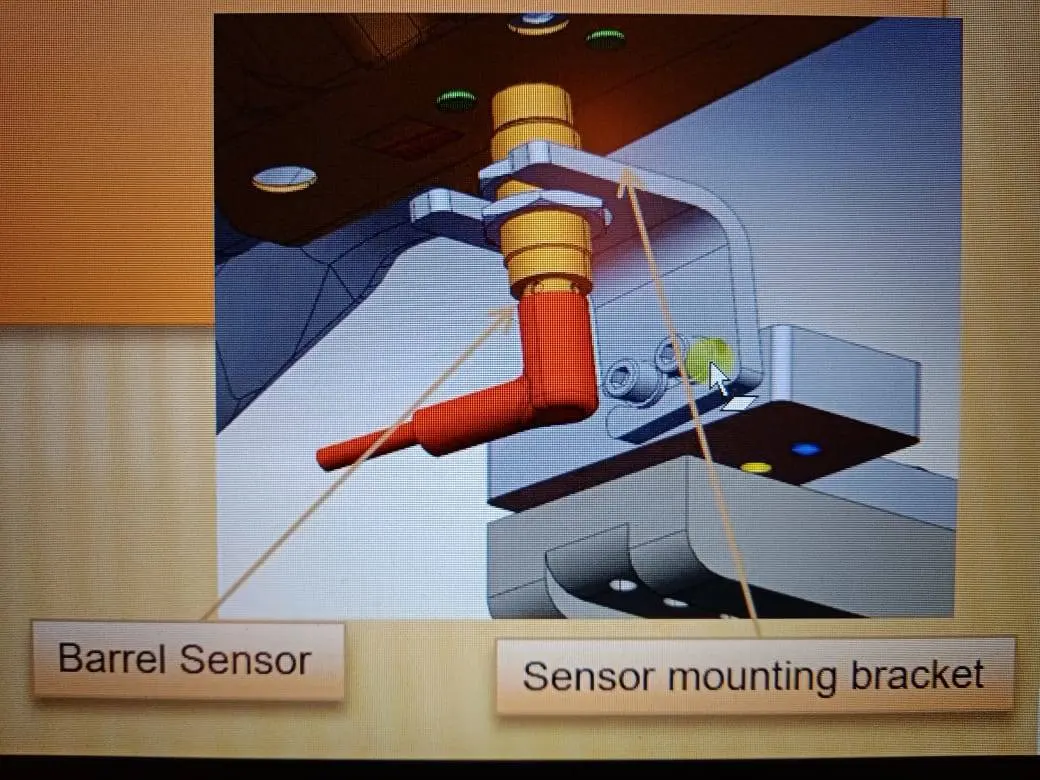
Fundamentals:
Each components which are welded in fixture should be sensed. So, we manufactured or assemble component free from errors. Consider an example of car panel having multiple components to assemble using welding. These multiple components are going to sensed by sensor to assure correct component is placed at correct position.
Types of sensors
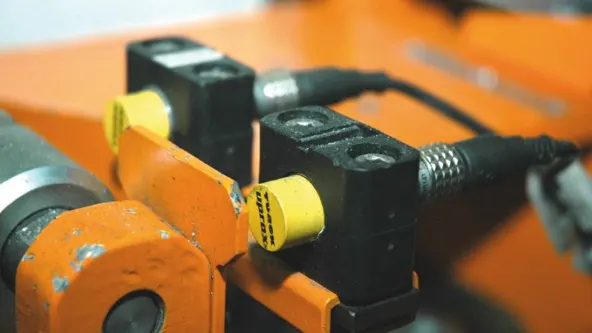
1.Proximity sensor:
A proximity sensor often emits an electromagnetic field or a beam of electromagnetic radiation and looks for changes in the field or return signal.
The object being sensed is often refered to as tge proximity sensors target.
2.Laser sensor:
These laser distance sensors use a focused, coherent light to measure distance to a target object. In factory automation applications, the target is usually a product or a machine elements. They detect any solid object and produce an output proportional to the measured distance – independent of material, color and brightness.
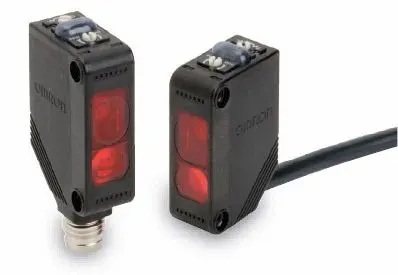
3.Photoelectric Sensor:
A photoelectric sensor or photo eye is an equipment used to discover the distance, absence or presence of an object by using a light transmitter often infrared and a photoelectric receiver.
They are largely used in industrial manufacturing.
There are three different useful types opposed, retro-reflective and proximity sensing.
16.Rough Locator Unit:
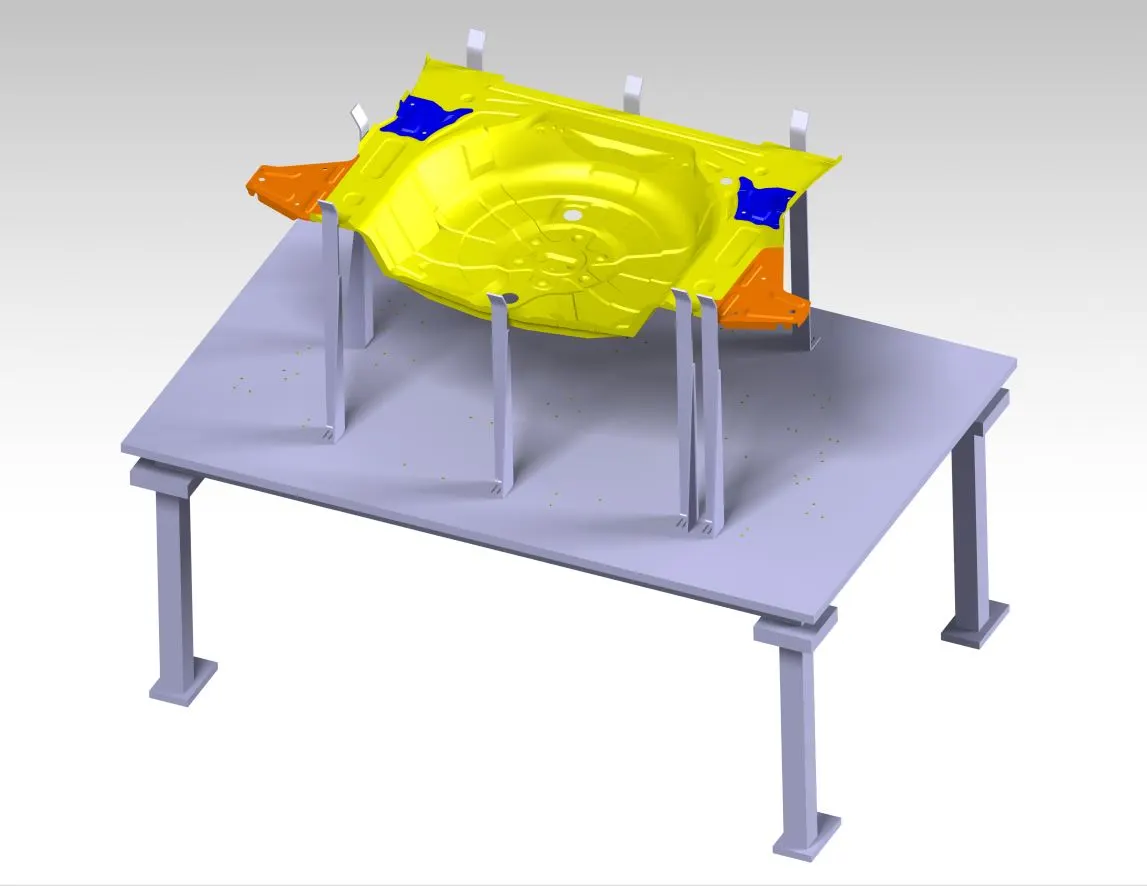
Rough Locator are the parts used to locate component correctly in fixture, basically it guide the operator while loading component in fixture. Figure shows an example of Rough locator and different locators we can used. It may be standard part or we can designed it according to our component.
FUNDAMENTALS:
- They are used to guide the component to load correctly in fixture and placed at the edges of components.
- The angle in locator should be according to component.
- Rough Locator helps component to placed in pins used in fixture to locate component.
- Entry angle should be 30 to 45 degree and rough locator should start guiding component before 10 to 15mm to start the pin engagement.
- For easy adjustmet rough locator mounted on base with two slots in it.
- The direction of slots are in the directon of car panel or component.
17.Base unit:
The Base unit of the fixture should have the mass to prevent vibration and chatter. The base unit may be built from simple sections so that other units may be fastened with screws or welded whenever necessary. Those parts of the fixture that remain permanently with the fixture may be welded.
Base unit is the unit designed to mount all the other unit like clamp unit, pin unit, rest unit, etc. of the tool, also other parts like pneumatic valve box, trunk cable path will also be mounted on to a base unit.
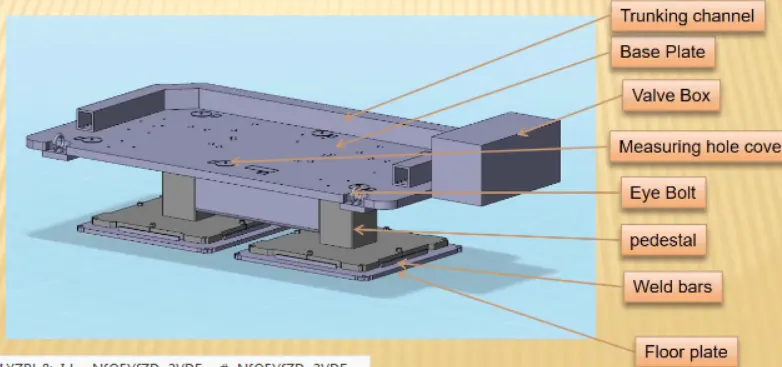
1. Valve box:
Valve box is basically a box which supplies air to all the pneumatic cylinders assembled in the fixture.
Valve box consist of one solenoid valve is used to collect the air from the pneumatic cylinders to valve box.
2. Trunking channel:
Trunking channel is a kind of cable duct, which helps to guide and protect the wirings/tubes used in the fixtures.
3. Measuring hole cover:
In the measuring hole cover the coordinates points are engraved on it.
The hole which mention the coordinates gives the position & placements of the particular units.
The measuring hole helps in CMM inspection & QC inspection.
4. Eye bolt:
An eye bolt is a bolt with a loop at one end. They are used to firmly attach a securing eye to a structure, so that ropes or cables may then be tied to it for lifting purpose.
Eyebolt is used to frag or lift the base unit while relocating.
5. Floor plates:
Floor plates is used to mount the entire base with the floor.
Also it helps to achieve the flatness of the fixture.
18.What is a Dump Unit and what are its functions
Dump units are used when we can not use normal units like clamp unit, pin unit etc. Due to some space constraints.
Dump unit is where you assemble component if you have certain constraint. Here you will have clamp unit, pin unit attached & panel will be assembled. So if you have certain constraint you cannot assemble in normal way.
Dump unit use in different way. It has dump cylinder & complex design. It consists of dump cylinder to perform the operation of clamping & unclamping car panel. A dump unit can have more than one cylinder to perform such operation.
FUNCTION:
Due to space constrain dump unit used in fixture. It has dump cylinder having open and close position for better understanding of design. It also has clamp cylinder used for clamping purpose.Hence this is too complex unit to built.
19.What is a Slide unit?
Slide Units are positioning units used to posiotion fixture, units, weldgun and robots. This unit consist of sliding rail on which entire unit is slide in direction of rails for further operation. Sliding unit consist of open and close position. These sliding unit is commonly used in automotive industry for different similar components. Following is an example of slide unit provided for welding purpose.
Basic fundamentals of slide unit design:
Reverse stroke o 10mm to be considered in both forward & retracted condition.
Cylinder & LM guides to be validate for load & stroke.
Master guideway should be constrained & the subsidiary guideway to be free.
Mechanical hard stop to be considered for both extended & retracted condition.
Shock absorber should be used for both extended & retracted condition to reduce impact load.
Slide to be locked/clamped in the working position.
slide to be locked with a safety pin in the retracted position during transportation.
The two end limits to be sensed externally by a proximity switch.
The design should be checked for screw accessibility, ease of assembly, machinability of parts.