Week 3:- BiW Fixture Design Methodologies Challenges
1.)DESIGN METHODOLOGY :
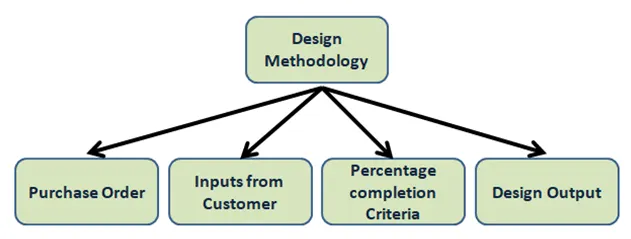
- Design methodology refers to the development of a system or method for a unique situation.Design methodology is the broader study of method in design,the study of the principles, practices and procedures of designing.
- Purchase order - It is the first official document that we will receive from customer side , this document will basically give a confirmation to us that the customer has agreed to our deal and we can start the project .
- Inputs from customer - Inputs from the customer is the demands of the customer that we need to fulfill . inputs like functional requirement , preferred standard components , car products , layout , ergo data , weld study , standard detailing templates . this all details are given by the customer to us .
- Percentage completion criteria - every project is divided into various stages . this stages will be assigned specific percentage value for the time it is needed to be completed , and by analysing these percentage we will come to know how much our project is completed .
- Design output - The design output will be a 3d Part , documents , 2D drawings , bill of materials , key sheet , layout sheet etc will be included in this output .
2.)DESIGN INPUTS REQUIRED FROM CUSTOMERS IN DESIGN FIXTURES:
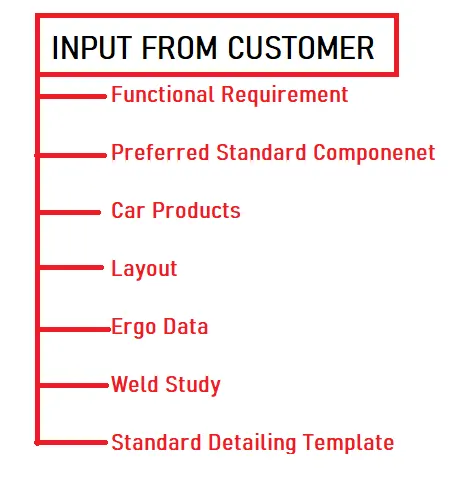
- Functional requirements - It is the first input which will define for what purpose the fixture is being made , whether the fixture is made for welding , hemming , rivetting , inspection etc will be mentioned . this is an important factor as based on this input the entire design and development of the fixture is dependent .
- Preferred standard components - during the development of any project , the team always decides to involve as much as standard parts as possible . as the standard parts are easily and readily available in the market , this will save the time involved in designing the part , which in turn will reduce the cost of the project . ABB, NAAMS , TUNKERS, ZYTRAN , DESTACO etc produce some standard parts which are used in fixture design .
- Car products - It is the input we receive from the customer , this include the 3d cad model data , GD&t of parts , clamp plan , product assembly process sheets etc . these inputs are necessary to begin the project .
- Layout - Layout gives the information about the flow of parts , robot station , tip dressers , tool changers , platform height , loading and unloading sequence etc . layout gives us the understanding of the complete assembly line .
- Ergo data - Ergo data gives the interaction of the human behaviour during the assembly line . it will include data like loading height , safety zone of operator etc.
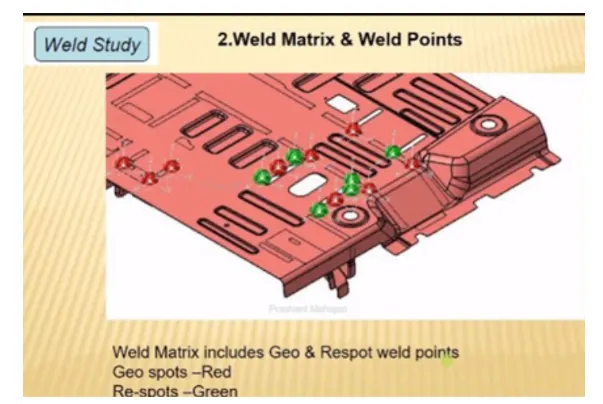
- Weld study - this input will show us how the weld gun will be used for the operation . it will give us report of weld matrix and the weld point positions . this input is necessary as the further development of the fixture will be dependent on this .
- Standard detailing templates - Every company has their own specific standard template used for 2D drawing and drafting. the customer will provide us their templates so that we can incorporate that in our 2d sheets .
3.)INPUT GETS FROM CAR PRODUCTS:
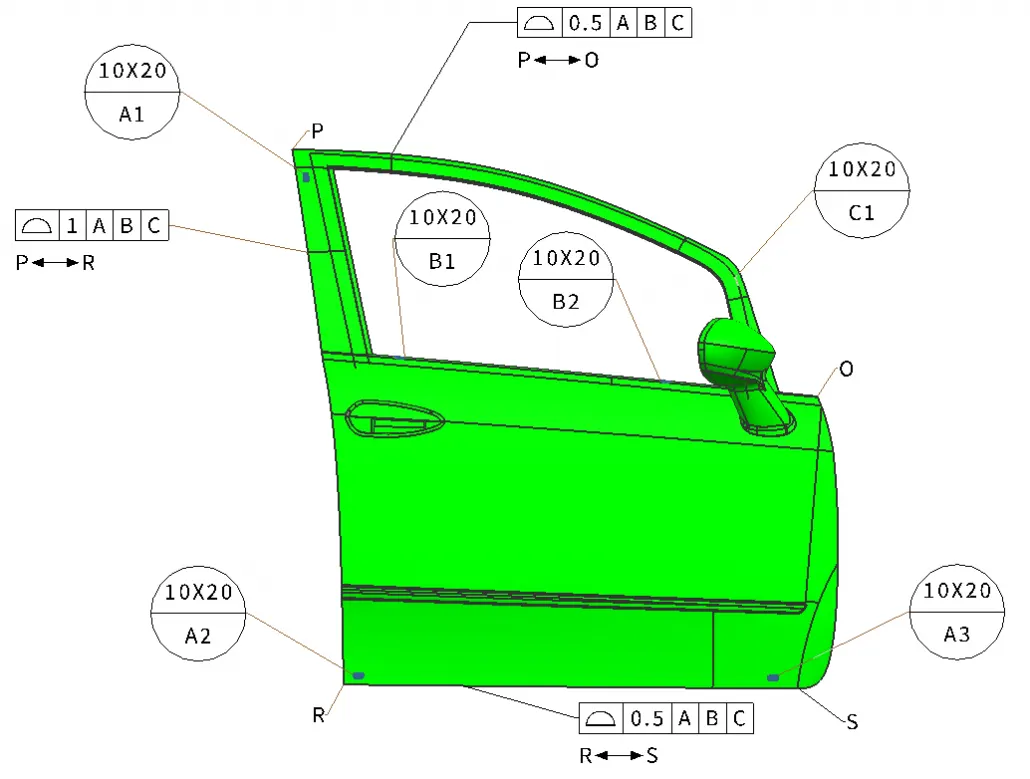
- Geometric dimensioning and tolerance (GD&T) - GD&T will be given of the part for which we need to design the fixture . it will provide information about locating pin , sequence of opening of clamps , rest , dump and slide stroke information .
- Parts list - Part list will give us detailed information about the parts involved in the fixture . it will give us information like part name , part number , thickness of part , quantity of parts etc .
- Cad files - Cad files of the part gives us information of 3d model , design analysis result . this information is very uselful as it will give us an idea on starting to design a fixture .
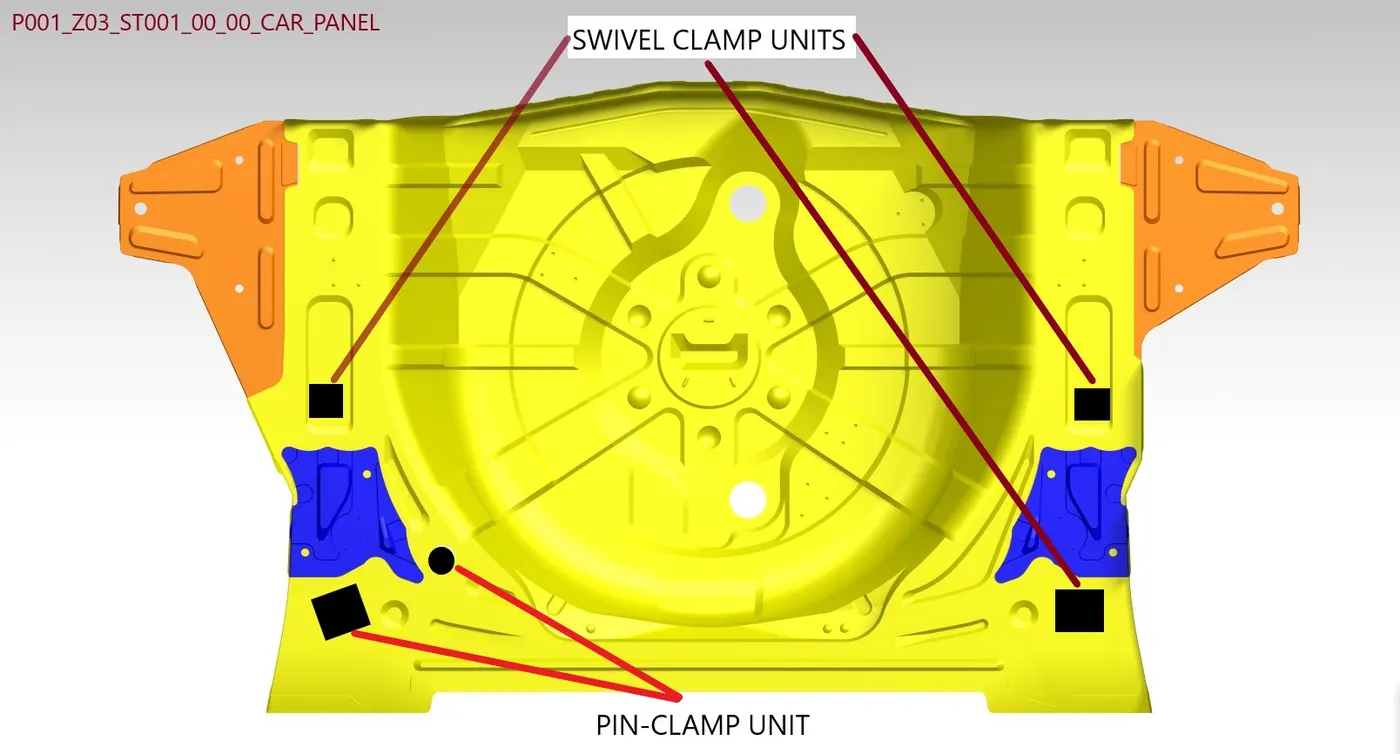
- Clamp plan - Clamp plan is very important information as it will give us idea of places where we have our clamps , pins , dumps , rest etc . we should never change the clamp position unless we ask the customer and they agree to it .
- Product AssemblY- Process Sheet- In product assembly process sheet,sequence or stages of assembly ofcomponents are given.
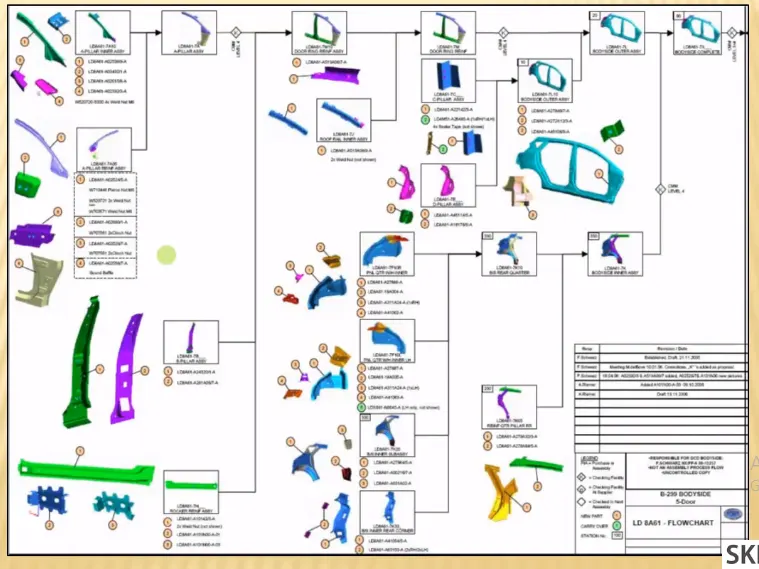
4.)CLAMP UNIT:
- A clamp is a device which is used to hold the workpiece . it is a force actuating mechanism of the fixture .
- A clamp plan is a very important input from the customer , the clamp plan will give us information about area where the clamps will be fixed to ensure proper geometry of workpiece is maintained during the operation .
- clamp plan provides information on location of pins , rest , clamps ,dumps etc . the coordines will also be mentioned in the clamp plan , so the design team can take the coordinates directly and start working on the fixture .
- We cannot change the clamp plan that is given by the customer , we have to inform the customer and if they agree then we can change it .
-
Clamps are nothing but a mechanism or component used to hold or clamp job in fixture sucurely. Clamps are manual type, hydraulic type or pneumatic type depending on customer requirement. Clamp plan mentions or gives thelocation of clamps in which component is going to clamp. We can't change clamplocation without customers approval, first of all we have to take permission from customers side to change clamp location.Clamp plan also provide information regarding location of pins, rest, clamps and dumps.
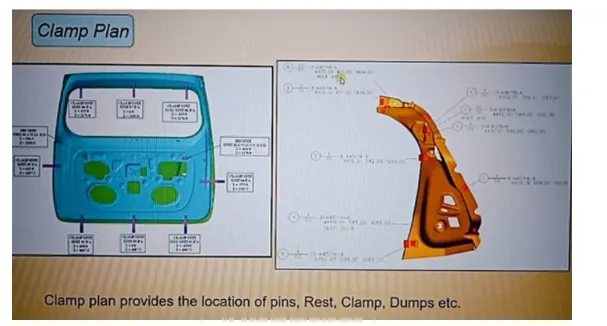
5.)PURPOSE OF LAYOUT:
- Layout Inspection is the complete measurement of all part dimensions shown on the design record. A layout inspection may be required by some customers for all products annually unless another frequency is established in a customer approved control plan. Results shall be available for customer review upon request.
-
The purpose of the layout is to give information about the following:
- Flow of parts
- Station Pitch
- Robot Stations
- Accessories like tool changer and tp dresser
- Subassembly links
- Platform height
- Loading/Unloading sequence/ Heights
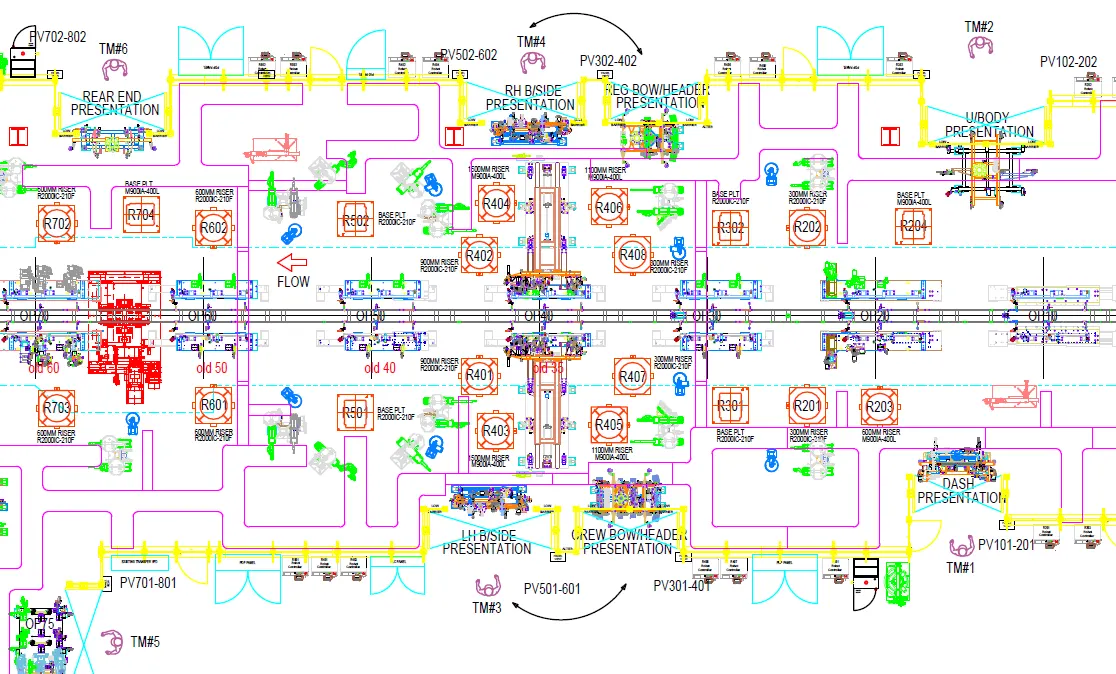
6.)ERGO DATA:
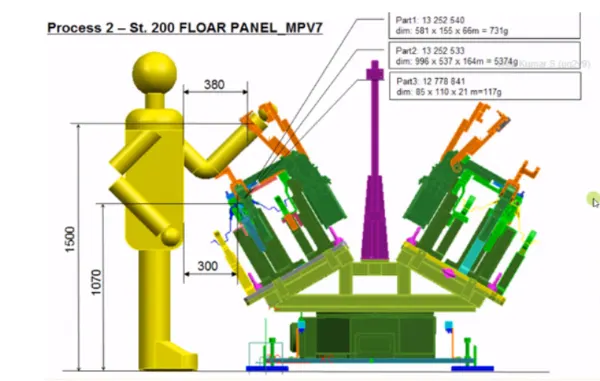
- As same as prfered standards, different companies follow different standards of Ergo data.
- We have to follow the customer standards of Ergo data.
- The inputs of Ergo data will given by the customer mostly in case of manually operated fixtures/manual fixtures.
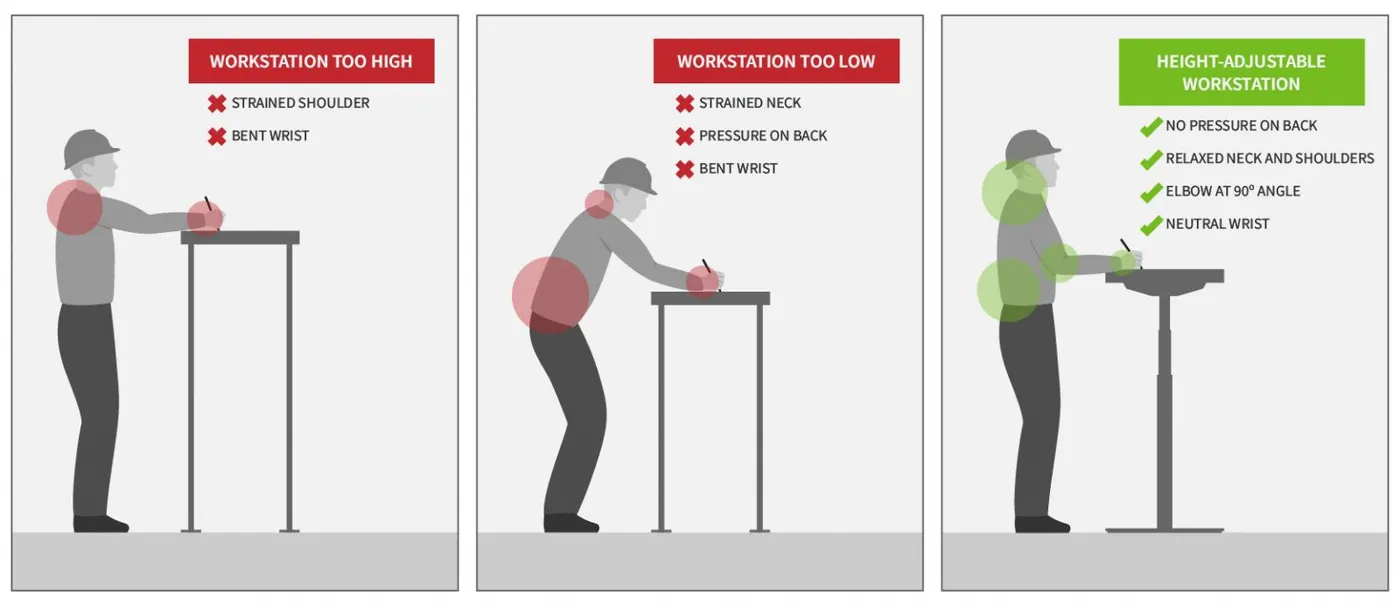
- The Ergo data is mainly used to make the operator comfortable which may leads to improve the efficiency in cycle time & production.
- Ergo data provides inputs like Platform height, maximum & minimum reach from operator to fixture, maximum & minimum height of the fixture, whether the child parts/ assemblies are visible while clamping or loading & unloading.Also provides informations like Loading height, working safety zone of operator.
- Human factors and ergonomics (commonly referred to as human factors) is the application of psychological and physiological principles to the engineering and design of products, processes, and systems. The goal of human factors is to reduce human error, increase productivity, and enhance safety and comfort with a specific focus on the interaction between the human and the thing of interest.
- The final assembly of an automobile involves tasks of complex nature. These processes are on the least priority for automation. Manual labor is best suited for assembly operations with the aid of minimal level of automation. All the processes have to be improved continuously in order to reduce the costs and increase productivity .
- The workers attain various postures, exerts force and works continuously in cycle time to accomplish the assembly task. Working along automobile assembly lines is characterized by repetitiveness.
- Ergo data is studied to identify and quantify ergonomics working postures that contributed to the serious development of muscle skeletal injuries and thus investigated possible contributory their related causes.
Benifits of Ergonomics:
- Improved working condition.
- Reduce physical workload.
- Improved work postures.
- Reduced efforts of certain movements.
- Better reading instrument displays, handling of machine levers & controls.
- Reduced unnecessary information recall efforts.
Below, I have given a basic example of ergonomics in the workstation
7.)WELD STUDY:
Welding is predominantely used in automobile industries and requirements for fixtures that ease the welding process is a continuous development task in any industry.
- Car Body-In-White (BIW) is a complicated steel-structure including 300~500 sheets with complex shape and are assembled by means of welding in a high rhythm through 55~75 robotic work-stations.
- The foremost step taken before starting the design of welding fixture is to arrive at the spot weld locations. The location and orientation of other critical units of the fixture including clamps, locators etc., are decided based on the weld spot distribution. The weld spots for Front door inner panel - side bracket assembly are located as shown in Table 1 with respect to the body line of car.
8.)THE CRETERIA OF PERCENTAGE COMPETION IN DESIGN STAGE:
- The % Completion criteria contain the current status of a task, expressed as the percentage of the task's duration that has been completed. You can enter percent complete, or you can have Project calculate it for you based on actual duration.
-It consist planning of completion of total project. How much days the project will take to complete.
- It is followed in designing stages & dispatch stages of the welding fixture.
- it ensures that how much task that we have decided to complete within the stipulated time is complete or not & how much of it is rest to complete & wheather it is going to be complete or not in given time.
- When a task is first created, the percent work complete is zero percent. If you enter actual work for the task, Project calculates percent work complete as follows:
Percent Work Complete = (Actual Work / Work) * 100
- In a typiacal BIW fixture design we can consider the following criteria of recentage completion,
(a) Input & concept design- 0 to 25%
The design inputs from the customer & after studying those inputs the concept fixture designs are created.
(b) Concept approval & Simulation check- 25 to 40%
The concept design approval from the customer after study of simulation.
(c) Design freezing & detailing- 40 to 85%
After the simulation result if no any changes are required then the design is freezed. After freezing the 2D drwaing which is the detailing part is started.
(d) Check & final dispatch- 85 to 100%
After detailing the quality checking team start inspection of all the data & it will dispatch to the customer if everything is ok.
9.)"OUTPUT" IN DESIGN:
OUTPUT IN DESIGN:
- The output is 3D models & the 2D drawings of of the toos.
- For unitized tools (multiple unit in a common base) requires two types of drawing sheets.
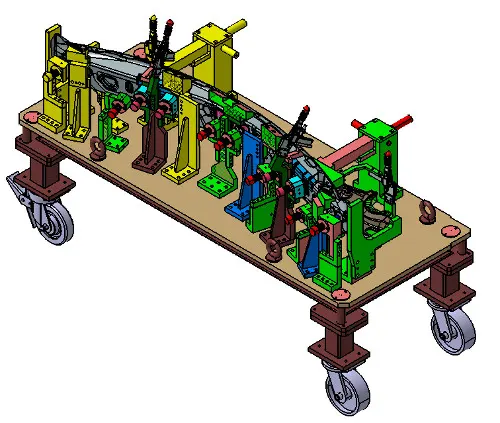
- Example of unitized tool: A tool with multiple units like rest unit, clamp unit, fixed pin unit, rectractable pin unit, rough locator unit, sensor unit, etc. in a common base
- The two types of drawing sheets are,
- key sheet.
- Layout sheet.
a. Key sheet:
- Key sheet gives or shows the index of units & their placements on the tool base.
- It will have an orthogonal view of the fixture including a numbered balloon drawing mentioning the units.
Figure 1. Key sheet
b. Layout sheet:
- Layout sheet shows a detail drawing of individual units to include all of their components.
- For Nonunitized tool no need of keysheets. As they can stand alone, the drawing can be detailed completely on a layout sheets.
Figure 2. Layout sheet
THE DESIGN OUTPUT SHOULD COMPILE FOLLOWING POINTS:
- Approved standard components are to be used wherever possible.
- Design must be as simple & economical as possible.
- Design must comply with all current safety & ergonomic requirements.
- Design must provide for controlled & damage free handling of product.
- Adequate error proofing provision must be incorporated into each design by providing proximity switches, rough locators, etc.
- The weight of the moving parts must be kept to a minimum while maintaining maximum strength.
- Frames & structures are to be simple & sturdy.
- Design clearance & accessibility for routine maintanance & service.
- Motion control must be considered on any moving equipments.
- Designer is responsible to validate clamps & weld guns.
Hence, the output in design are briefed.
10.)Understand by structuring design tree? How does it reduce errors during design process:
Structuring a design tree is very necessary whi e designing fixture because it help to identify all manufactured part in whole fixture. Every customer company have there own standard.This will help us during design study,manufacturing and inspection to avoid errors.If we ignore structuring a design tree it will crete confusion to understand design and may errors willappers in fixture.
A process where all the assemblies and parts are named in a specific standard.Different customers have different set of standards and the structure of design tree.
- Every company,every customer has different standards of their own structure design tree.
- So they will be giving a template on how the structuring and detailing of the design is done. And you have to follow that particular designing or structuring of the tree.
- In the design tree itself if we mentioned that particular name, wherever that part is we can easily know that this part belongs to this zone or This station or this assembly on particular unit. So this helps us to avoid errors during the design study,manufacturing assembly and inspections.
- Structuring a design tree is actually to avoid all the errors, which might come during manufacturing assembly, or either in house inspections as well.
- If the part, or assembly are not named properly, or design tree is not structured properly, it will create confusion to understand the design and may create major possibilities of making an error.
- Every part, every component should be named according to their precedures.
- If we did a mistake or renamed the entire standard parts from the customer as a design part.Now the customer is going to manufacture the entire part again from the scratch, but he already have that product in his itinerary.but extra cost,extra time and not feasible.this is also known as an error which is actually going to increase the cost of the entire assembly as well.
- Naming a fixture or a unit or a part gives the information as to which project zone or assembly do they belong.
- If we name the part properly or name the fixture properly it'll actually tell which unit or which assembly or which zone or in which station it actually belongs.
- It can help us to identify the quantity of items of same types or different types that are being used in an assembly.
11.)UNITS, TYPES OF UNITS:
UNITS
In units they are two types one is unitized tools and non unitized tools.
UNITIZED TOOLS:
Unitize tools are basically tools which are a part of multiple units or multiple tools inside of itThese are the tools which has to be represented by two formats key sheet and layout sheets.unitized tools are basically two types,
- Simple units and
- Complex units.
NON UNITIZED TOOLS:
non unitized tools are basically one unit itself, which is basically don't have any process functionality to it is just to keep component on it as a stable, like grippers turntable stands, etc.
Simple Units:
Simple unit will have a very simple design to it, then the approach of the designing and manufacturing is also will be very simplistic like rest unit.
Rest Unit:
Rest unit is basically a unit where the component is tested, there is no upper clamp to it, there's no force applied to it. There is no cylinder attached to it, it's just, usually it will have a riser a blade and few rest maylers.
Fixed Pin Unit:
fixed pin unit are basically units which has a pin which is already fixed it cannot be moved.
Retract Pin Unit:
Retract pin unit are the opposite to the fixture which can be moved up and down, so it can be retracted till a certain distance.
Rough Locator Unit:
Rough locators are usually used in loading and unloading of that particular panel.
Sensor Unit:
Sensor units are used in actually sensing whether the panel or a particular component is there or not.for example If we are assembling component of nine parts or 10 parts or eight parts, they'll have that many sensors,so that every component will have different its own sensor attached to it.
Base Unit:
Basic unit where all the units has to be mounted.
Complex Units:
Complex unit, like slide unit as an example of a complex units that design in itself a little complex in design.
Slide Unit:
The slide units are basically where the sliding mechanism is involved.
Dump Unit:
Dump unit is basically like a conveyor where you keep all these panels juiced up right as for storage kind.
12.)FIXED PIN UNITS AND THEIR PURPOSE:
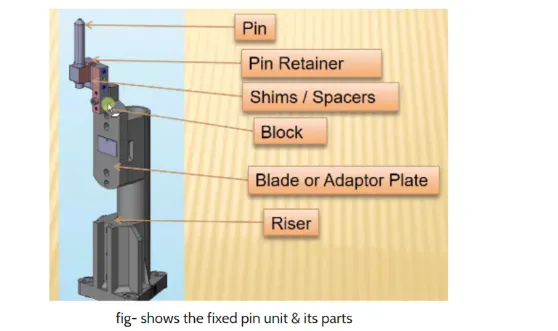
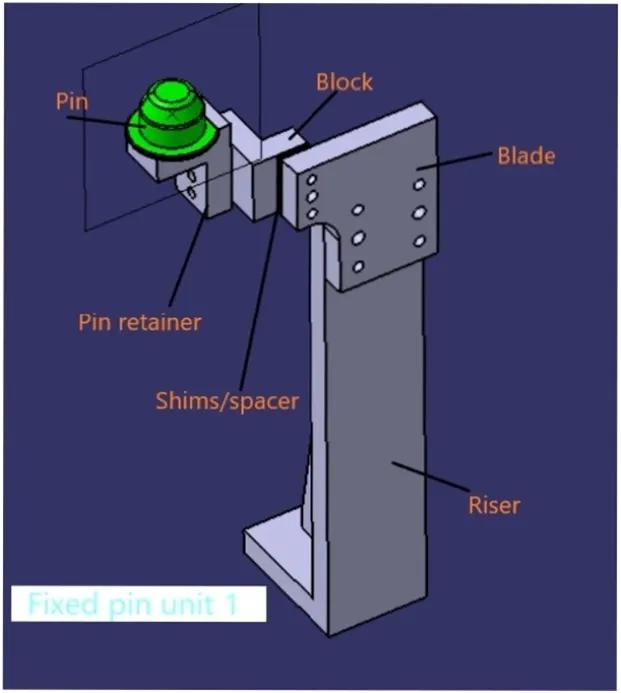
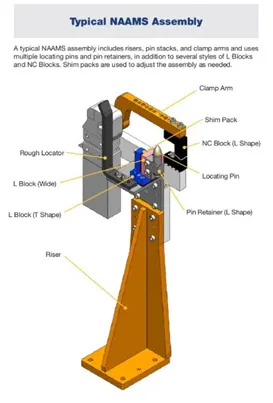
- Fixed pin unit is a non movable locating unit used for proper location of part and it arrests all the movement of part as well. fixed pin unit consist of pin , pin retainer , shims/spacer , block , blade or adaptor plate ,riser . Riser is the part which is used to rise or increase the height of the unit . blades is mounted on the riser . block will be mounted on the blade . shims are small spacers which are used for stack up tolerances . shims are made of various thickness like 0.1,0.2,0.5mm etc . pin retainer will hold the pin . and the pin is used to locate the part and restrict its motion .
- Purpose of fixed pin unit - The main purpose of the fixed pin unit is to locate the car panel and restrict its motion . it is placed following the 3-2-1 principle , so it is necessary to have two pins like 1 pin will restrict 4 d.o.f (4 translational) and the other pin must restrict 2 d.o.f ( 2 rotational) .
13.)DIFFERENT PARTS OF A FIXED UNIT:
Shims:
A shim is a thin and often tapered or wedged piece of material, used to fill small gaps or spaces between objects. Shims are typically used in order to support, adjust for better fit, or provide a level surface. Shims may also be used as spacers to fill gaps between parts subject to wear.
Risers:
Riser is a structure generally used to mount the toggle clamp and rest, clamp mylars and location pin.
- It is not necessary to have one riser where all the parts of clamp or rest or location units are mounted.
- Generally risers are either made of plate fabrication or plate and tube welding together or from single gas cut plate.
Blocks:
Blocks (red for representation) are versatile blocks that can be machined to any desired fixture component. Because they come as a blank block, the possibilities are endless. Adding new tap holes or grinding down to your specifications are quick and simple.
Sensor unit:
Sensor unit is a unit designed to sense the car panel by using electrical sensors, the signal from the sensor will fed to a PLC which is our programmable logic controller and sort of the next process will be executed by this signal.
14.)purpose of making a Rest unit & describe its parts:
- The rest units are designed to rest/support the car panel by using NC blocks/Mylar/Rest
- It is the simplest unit to design because it have less parts to design & the purpose is only resting of the car panel.
- Because of this simplicity the rest unit is combined with other unit to reduce the cost of the overall project.
-It can be combined with clamp unit to clamp as well as to rest the car panel. It can be combined with locating unit to locate as well as to rest the car panel. also locating, clamping & restunit can be combined together in one unit to reduce cost.
it consist following parts,
1) Riser- Riser is the standard part which is used to rise up the height of the while unit.
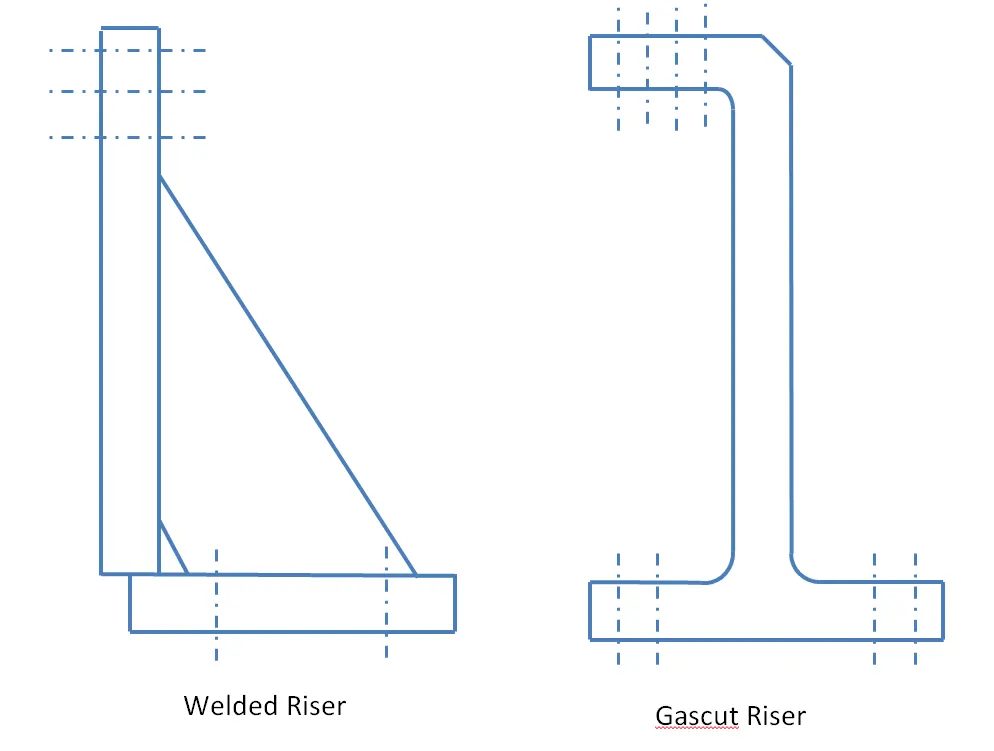
fig-shows the riser
2)Blades - These are plates mounted on the riser. Other parts like cylinder, arms etc are mounted on the blade.
3)Shims- These are the small part which comes with the thickness of 0.1mm, 0.2mm, 0.5mm etc. These will compensate the stackup tolerance which reflects at the panel holding part called Mylars.
Shims are used in one in direction in rest unit which is up & down because it requires adjustment in height only.
4) NC blocks/ Mylar/Fingers- Mylars is the component which holds the panel while operation. These are placed from top side & from bottom side also. The top side Mylars called as Clamping Mylars & the bottom side Mylars called as Resting Mylars. Every clamping Mylars have resting Mylars. It dont allow deformation of the part due to welding stresses.
15.) Basic fundamentals to design a Sensor unit:
Sensor unit:
Sensor unit is a unit designed to sense the car panel by using electrical sensors, the signal from the sensor will fed to a PLC which is our programmable logic controller and sort of the next process will be executed by this signal.
- So our sensors are basically used to sense the particular car panel. Now, the signal which gets from this sensor will be fed to the PLC, the PLC will decide whether the signal from the component or the assembly actually has the particular car panel or not.
- If it does not have it will not execute the next process, and it will stop the entire process that itself until the panel is loaded.
Fundamentals of Sensor Unit Design:
Every single Loose panel, which are being welded in a tool should be sensed.
So every single panel that we are going to assemble in that particular panel.
For example:
- If we are using nine different panels to assemble in one panel. Every single one of those panels should have one sensor attached to it.
- Each panel should be sensed by one or two sensors depending on the size of the panel prefered to be in diagonally opposite ends of the panel.
- If a component is really small,We don't have to use two or three sensors for that you can just use one sensor, which will detect that particular panel.
- If the panel is really big. we will use two sensors towards the opposite directions of each to sense their particular panel.
- So every sensor should be mounted in three directional adjustable ways in general.
- Sensors Detect in Three Different Movements in that first one is upward and downward movement of the sensor.The second one is from left and right movement, and direction so all three directions.
Sensor manufacturers is IFM,Pepperl-Fuchs and Omron, etc.
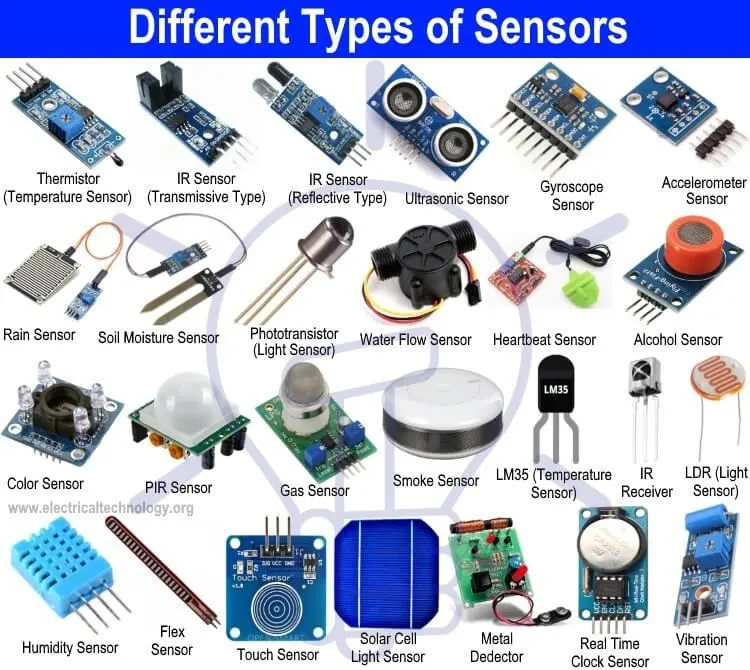
Types of Sensors Used In General
Proximity sensor :
proximity sensor is used in cell phones as well to detect a particular component. So, proximity sensors are range from 5 to 6 mm to 8 to 10 mm.
laser sensors:
Laser sensors are used for bigger sensing the distance.if the component cannot be near the panel. It has to be farther away from the panel, then you will be using laser sensor.
Photo Electric Sensor:
Photo electric sensors this is basically a proximity sensor and this can be utilized as a laser centered sensor and this is an example of a photoelectric sensor.
16.)Rough locator unit & what are the basic fundamentals:
Rough locator :
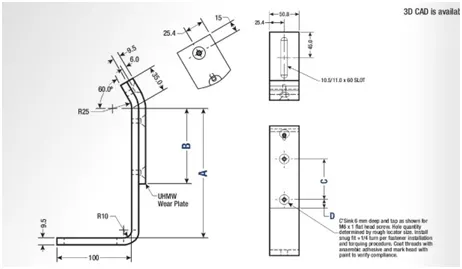
Rough locator is a part which is designed to guide the operator to locate the car panel on the pin accordingly rough locator can be of standard parts or make part.
The locators are used in loading and unloading the pan. These are very handy while orienting the part properly, so it will actually guide the entire the operator to load the panel in a particular orientation.
Fundamentals Of Rough Locator Design-
- Rough Locator should be placed at the edge of the component or car panel,which has to be guided.
- So these are four carriers has to be placed at the edge.These are the edges of the entire panel, where the rough locators are the locating pins. So by these locating pins, you can either restrict the movement of the entire panel as well so placed in the same angle of the car panel edge with a minimum distance of 2 to 5 mm from the edge of the car panel .
- Rough Loacators should not touch the car panel,so that it should not damage the panel by loading and unloading.
- Rough locator should be designed in such a way that the panel will come from top to bottom and then it will be guided in the same direction.
- Rough Locators cannot be in just one angle it should be at the angle where the panel edge is supposed to be.
- Rough locator should start guiding the panel before 10 to 15 mm to the start of the pin engagement is one of the important parameters to consider.
- Rough locators should start guiding the panel downwards, before even the pin unit, engage in the panel.
- Rough Locators should be designed with entry angle for car part entry.
- Rough locators should be designed with two slots to mount for easy adjustments.
- The slots should be in the direction of car part guiding.
17.)Base unit and describe it's parts:
Base unit:
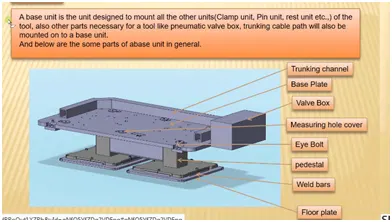
The base unit is a unit designed to mount all the other units like time unit,pin unit , etc. of the tools and also other parts necessary of the tool of pneumatic valve box,trunking cable path will also be mounted on the base unit.
- All the units are basically like clamp unit,pin unit,rest unit And the Rough locators, everything will be mounted on the base unit.
Valve box:
A valve box is basically a box which supplies air to all the other pneumatic cylinders. it's it's a device which includes a lot of other solenoid valves, so it will have one inlet and one outlet and from that one inlet, all the other solenoid valves will be attached to it. And each solenoid valves will have the input, and then again supplied to the separate cylinder, then again the output will be collected, while this solenoid valves, and again given back to the valve box.
Measuring hole covers:
Measuring Hole covers is on the base unit which is for measuring purpose.
Eye Bolt:
It is to drag the entire unit and relocated.
Pedestal :
By this pedestal is for standing the entire unit.
Weld Bars and floor plates:
Weld bars are to mount it to the floor.
18.) DUMP UNIT AND WHAT ARE ITS FUNCTIONS:
Dump unit is a complex unit which is used in places where there is a space constraints or some other constraint . when we have some geometrical constraints and we cannot mount clamp unit, rest unit etc in a normal way then dump unit is used . It consist of dump cylinder to perform operation of clamping and unclamping of car panel .
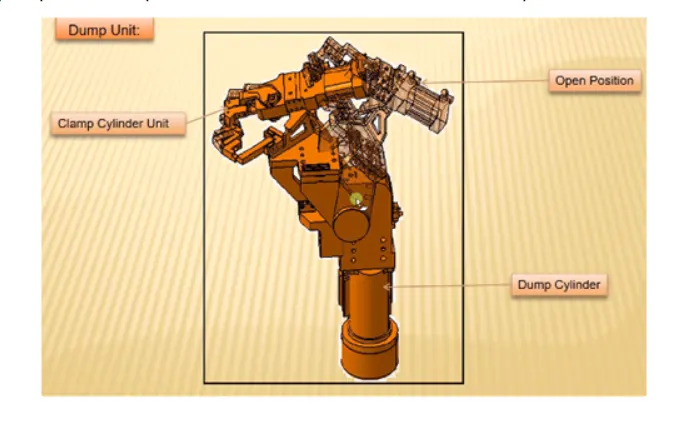
Functions of dump unit -
- When there is a particular constraint and we cannot asssemble component in normal way dump unit is used .
- It has a dump cylinder which performs the opening and closing action . it has a clamp cylinder unit too .
- This dump unit is complex in design and so it is used only in need .
19.)Sliding units :
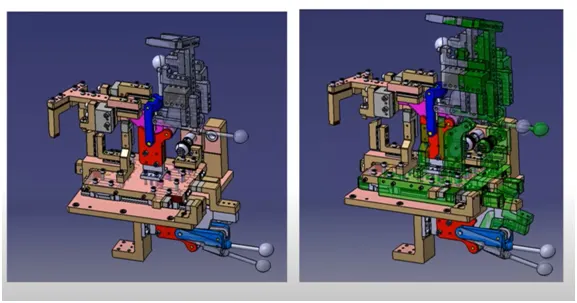
Sliding units are basically used in places where you have a lot of constraints or space constraints, when you cannot use different types of units to design the entire assembly. So, here you will use this sliding Only
Sliding cylinder:
The sliding cylinder has One open position and One closed position, which has to guide rails direction to the entire panel is going to move.
position locking unit :
The position locking unit which will lock the position at that particular point doesn't allow the entire plate to move.
Sensor Unit :
Sensors need to sense whether this entire component has reached here or not.
Stopper blocks :
Stopper blocks as I said initially to control the entire panel moving and it's a moving part.