Week 2:- BiW Fixture Basics Challenge
Question No. 1 - What is the process of project execution activity?
Answer:
PROCESS OF PROJECT EXECUTION ACTIVITY:
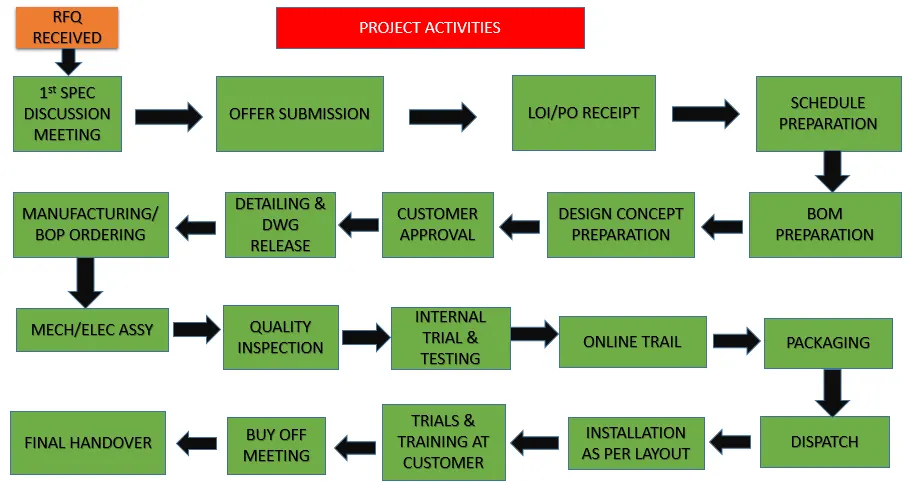
FIG 1. Project Activities
- The above figure shows the process involved in process execution activities.
- It is a general activities which is involved in BIW fixture & Tooling.
- It is a starting phase of every project.
- It starts with basic requirements/RFQ we received from customer.
- As shown in the figure there are various steps involved in project activities, They will be explained in detail below.
1. RFQ:
A request for quotation (RFQ) is a business process in which a company or public entity requests a quote from a supplier for the purchase of specific products or service. RFQ generally means the same thing as call for bids (CFB) and Invitation for bid (LFB).
In this where customer gives the requirement/specification in detail for the given projects in the form of data or documents.
2. FIRST SPEC, THE DISCUSSION MEETING:
After RFQ received, the Technical offer, the commercial offer, the time line of the project, etc., and will be discussed and prepared from outside.
In this time required for data study, 3D design concept, and Simulation validation, quality check, 2D drawing release, Bought outs, manufacturing, Assembly, installation & commissioning will be discussed and prepared in the technical offer.
Based on technical offer, commercial offer will be finalized.
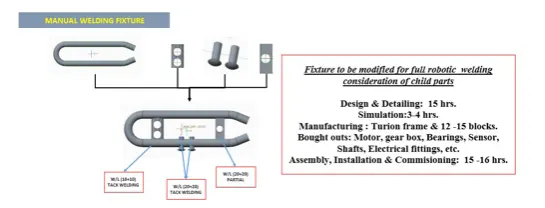
FIG . Basic example of Technical offer for manual welding
3. OFFER SUBMISSION:
After the finalisation in the meeting, the offer will be submitted to costemer end.
Customer will arrange to get offer from other suppliers too.
Based on the technical, cost, quantity, standard and name in the industries the costemer will be finalized the offer.
4.LOI/PO RECEIPT:
After offer has been finalized customer will be releasing the LOI/PO(purchase order).
Once PO is realese we have to start the work.
After PO from the customer we have to prepare the schedule.
5. SCHEDULE PREPARATION:
Once the PO released from customer we will be working on preparation of schedule which be matched our planned commitment in the technical offer / customer required time.
Schedule preparation is nothing but dividing the different activities like kick off meeting, design data study, DAP, Simulate, quality check, 2D detailing, Drawing check, release of BOM, Manufacturing, Bought outs of electrical & mechanical components, assembly of fixture, paint, trial run out, installation and commissioning at customer end etc,
These activities will be traced in the schedule preparation chart.
The date wise schedule should be matched the commited date. Otherwise have to revised the schedule and prepare accordingly by discussing in the meetings.
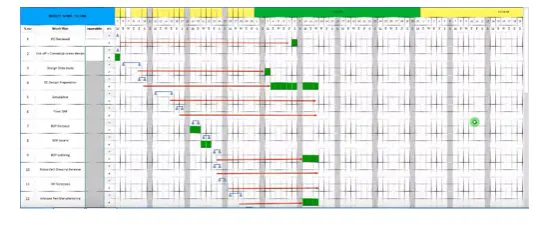
Figure . Example of schedule preparation chart
6. BOM PREPARATION:
Bill of materials like cylinders, motors,etc., which is required for the project are prepared.
7. DESIGN CONCEPT PREPARATION:
Before design concept, we have to study the data of consumer requirement throughly which is carried out in design data study activities.
During design data study, we will be proceed with rough sketches to get a flow while designing concepts.
The concept preparation would include the process like load act on panels, clamping process, which spot should be welded first, travel of the gun.
The weld gun should not collapse while travelling, so by considering this have to make a concept preparation.
To avoid collapses of weldgun or robots during travelling, spot plan will be doneat initial stage.
In design concept preparation, the design of the layout are been prepared at very initial level which gives the information of placements of robots and fixtures.
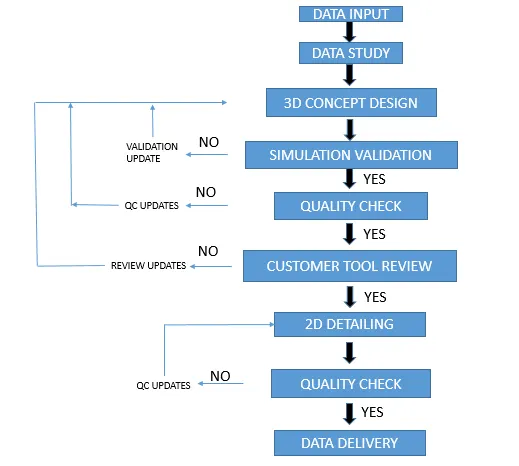
FIG 2. Process involved in Design
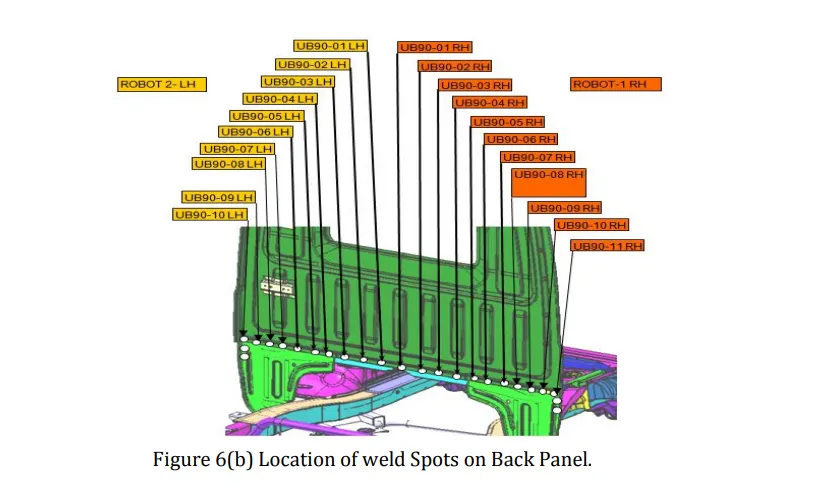
FIG . Location of weld spots and back panel.
Spot plan clears us that how much robots are to be used and the sequence of the spot will be decided along with which robot will be cover certain spot places.
Also cycle time should be considered while preparing concept design.
To calculate the cycle time we should go to cycle time study.
Cycle time study includes : Min. per shifts, no. of shifts, No of days per year, no. of components per year, total number of minutes, efficiency, total no. of seconds, taik time seconds, Avg time per spot, total no of spot, no. of robots placed.
From the cycle time study we can get time taken per spot, time taken for single component, efficiency of production.
If the efficiency is not satisfied we have to do some reconsideration in the design.
8. CUSTOMER APPROVAL:
It is also known as design approval process (DAP).
After design concepts the customer will review the design concepts.
If the design need to be made simple or some other correction needs to be done in concept design will be discussed and after meeting the requirement of customer, they will give approval to the design to go on with furthur activities.
9. DETAILING & DRAWING RELEASE:
Once the customer approved the process, the detailing of the fixture parts which is to be manufactured has been done with giving appropriate dimensions and GD&T symbols.
All the dimensions which is necessary for manufacturing should be included with GD&T in the drawings before releasing the drawing to the manufacturing team.
10. MANUFACTURING / BOP ORDERING:
The mechanical & electrical parts like sensors, cylinders, etc., which needs for fixture are ordered as per design specifications.
11. MECHANICAL / ELECTRICAL:
After the materials ordered received to our end. The quality will check the working conditions and technical specs, which meets our requirement.
After the quality check the mechanical & the electrical parts are assembled as per design.`
12. QUALITY INSPECTION:
After the assembly again the quality check is done.
In this all dimensions, positional accuracy, coordinates are checked using CMM.
13. INTERNAL TRIAL:
After QC check internal trials are made to check the operation of the fixure.
It is a first trial taken inhouse, so we will see by putting the assembly in the fixture whether the seating of assembly/panel suited correctly, whether the clamping operation are done properly, also whether the pins are getting into the holes,etc,.
14. ONLINE TRIAL:
The trial will done in automatic made through control panel.
The process sequence of operations is checked as by the designed way.
15. PACKAGING:
To avoid damage occur in fixtures while transportation which may also leads to affect the aesthetic look & proper function of fixture packaging has been done.
After the trials taken have to get the QC confirmation whether the panels met the standards/specs given by customer also whether the fixture meets the customer standards.
After approval of QC, packaging is been done as per standards certain companies follow certain packaging standards, so the packaging should be one as per customer standards.
16. DISPATCH:
After the fixture has been packed for delivery as per standards.
Its been dispatched to the customer.
17. INSTALLATION AS PER LAYOUT:
As we discussed in design concept preparation, the design of the layout are been prepared at very initial level which gives the information of placements of robots and fixtures.
According to the design the installation & commissioning team will install the fixtures.
18. TRAILS & TRAINING AT CUSTOMER:
Production trails will be taken at customer end.
During technical offer we will be confirmed that n-number of assemblies will be produced within 8hrs/12hrs shifts.
So in customer trial we have to achieve the confirmed quantity of assemblies.
Once it is achieved, training will be given to the operator, staffs, engineers who involved in this process.
The sequence of working process by the fixture will be explained in detail.
The check points which has to be done after placing the panels into the fixture will be made clear to them.
19. BUYOFF MEETING:
After trials and training at customer end, buyoff meeting will be held.
In this meeting customer will give reviews about the fixtures, sometimes customer may need/feels better to do some addition work also. It will be discussed and finalize in the meeting.
20. FINAL HANDOVER:
The fixture and the documents supports the fixtures/production will be haded over.
Documents like poka yoke documents, clamp validation document,ergo sheets,BOM, charts will be delivered and handedover to customers.
Documents will play a vital role in industry, we should always have a proof for our work done. The sequence of quality of work will be seen through the documents.
Every automobile industries will follow some standards to maintain documents as per ISO,IATF.
Now every automobile industries/vendors/suppliers are maintaining the documents as per IATF (International Automotive Task Force).
IAFT - The International automotive task force is a group of automotive manufactures which aims at providing improved quality products to automotive customers worldwide.
Hence, the process of project execution activities are detailed above.
Question No. 2-What are the types of joining processes?
Joining Processes involves joining of two metal parts either temporarily or permanently with or without the application of heat or pressure.
Joining can be done in two types
1)Mechanical joining
2)Metallurgical joining
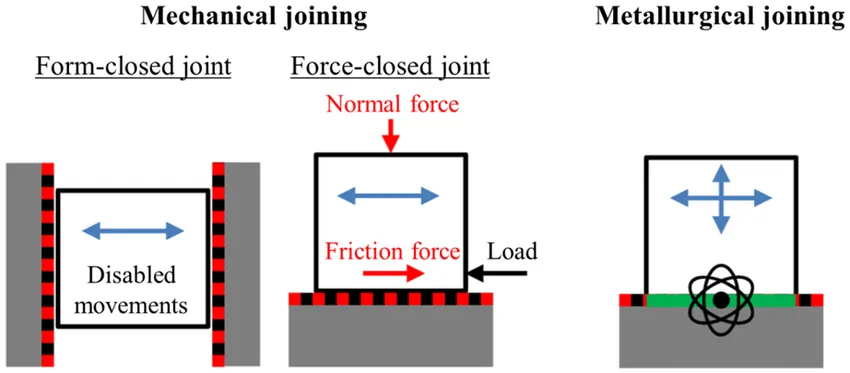
Image 2.0: Mechanical & Metalurgical joining
1) Mechanical Joining:
It is a process of joining using mechanical methods which involves screws, nuts, rivets and bolts etc. The threaded holes employed for mechanical joining are vulnerable to fractures. In ductile materials, the fracture can come from fatigue, while in brittle materials, the fracture can simply result from mechanical overloading. Thus, mechanical joints must be designed with fatigue failure and brittle fracture in mind. In mechanical joints there is a prone to galvanic corrosion. Hence while designing mechanical joints It is to be taken into consideration.
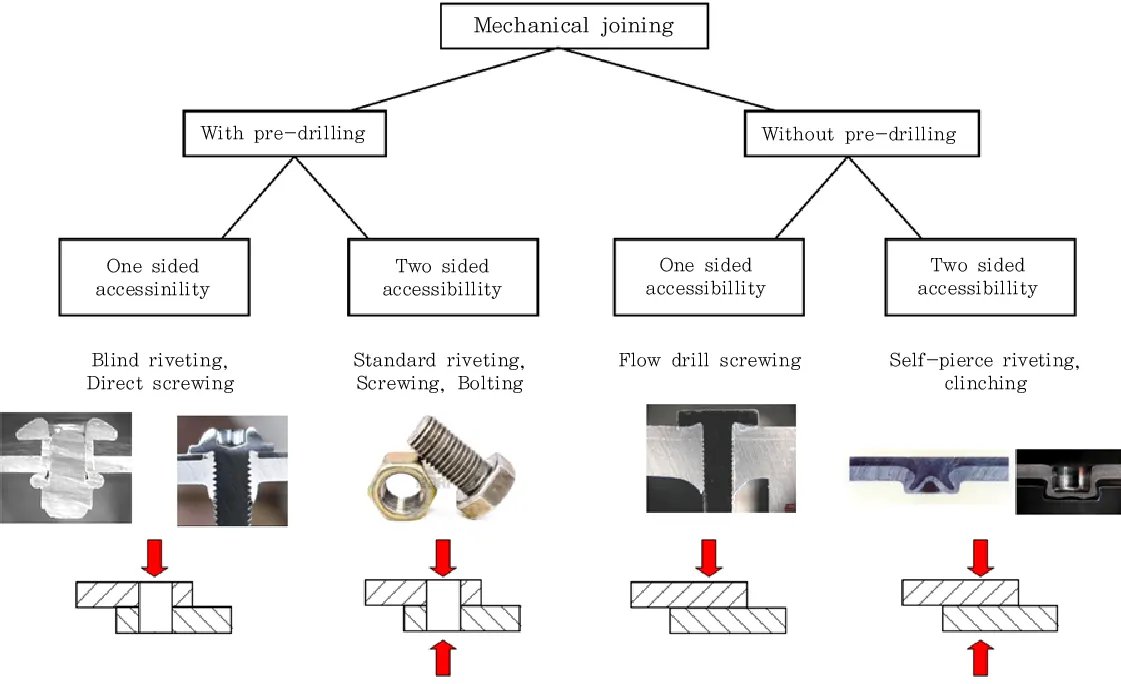
Image 2.1: Mechanical joining
As shown in the image mechanical joining can be classified as with pre-drill and without pre-drill which means with pre-drill have holes and threading in it so that screws, nuts or bolts can be used in this category. where as in without pre-drill forcible drilling or reviting by piercing will be done. The one side or two side accessibility refers in how many sides the mechanical joint can be accessible. for example, if you are using screw and nut it can be accessible from two sides i.e. from top and bottom where as in case of reviting only from the top side is accessible and bottom side it is pierced into the metal.
2)Metallurgical Joining:
It joins two metals involving metallurgical changes in it. Sometimes metals will be fused or heated or filler materials may be added etc. Welding, brazing, diffusion bonding, soldering, adhesive bonding fall into this category.
1) Welding:
Welding is a joining process in which the work pieces are joined by melting/fusion. A common method for welding, known as arc welding, consists of generating an electric arc between an electrode and the work pieces to be welded together.The arc generates enough heat to melt the electrode and the areas of the work pieces were the welding is performed. As the electrode passes over a region while the arc is present, molten metal from the electrode and molten base metal from the work pieces all get mixed together, solidifying to form a strong joint upon cooldown.The electrode contains some flux material, the purpose of which is to stabilize the arc formed by generating gases (carbon dioxide, carbon monoxide, water vapor) that shield the arc from the surrounding atmosphere. some types of weldins are shown in the image below
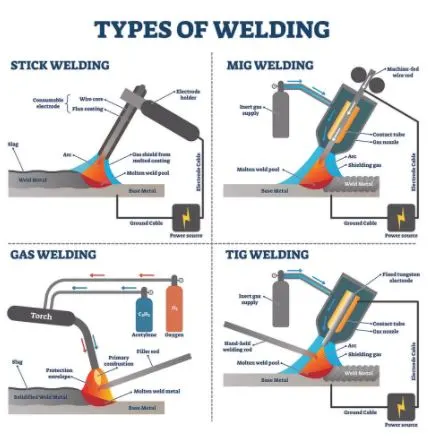
Image 2.2 Types of Welding
2) Brazing
In brazing two work pieces are joined together using a filler material that is sandwiched between them, wherein only this filler metal undergoes melting without causng any melting in workpiece. The temperature for brazing should be high enough to melt the filler material, but not for the work pieces. Materials used as fillers for brazing are those that melt above 450 deg C. Flux is also used during brazing for the purpose of eliminating oxide films from the surfaces of the work pieces and preventing oxidation.This would ensure a good metallurgical bond between the work pieces and the filler once the brazing process is completed.Once melted, the brazing material fills up the spaces between the surfaces being joined, and even manages to get into tight spaces by capillary action. A strong joint is obtained after the brazing material has cooled down.
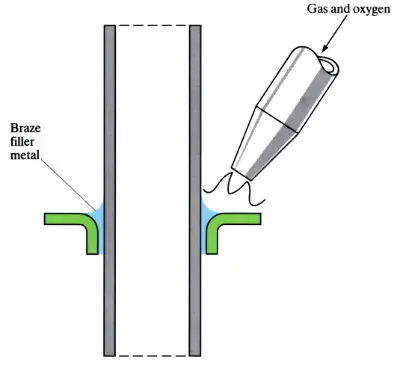
Image 2.3 Brazing
3) Soldering
Soldering is a joining process which is performed at much lower temperatures than brazing. In soldering two work pieces joined together with a filler metal (tin-lead, tin-zinc, lead-silver, and cadmium-silver alloys), such that only this filler metal undergoes melting, i.e., the work pieces do not experience any melting. Brazing materials are those that melt above 450 deg C, so soldering materials would be those that melt at less than 450 deg C. Like welding and brazing, soldering also employs flux materials to clean the surface to be soldered and improve metallurgical bonding. Residues from fluxes, however, must be removed after soldering to reduce the risk of the occurrence of corrosion.
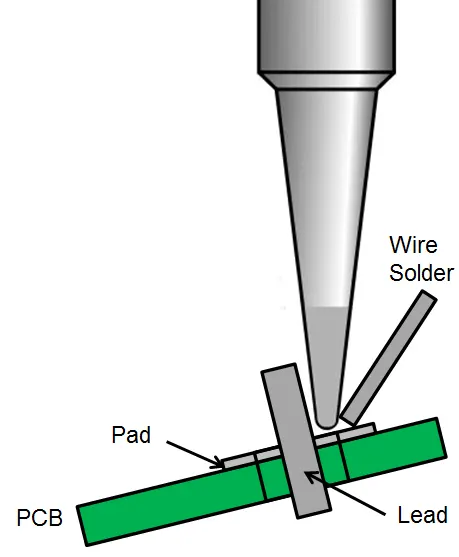
Image 2.4 Soldering
4) Adhesive bonding
Adhesive Bonding uses bonding chemicals or materials known as adhesives. It is used to join polymers and polymer-matrix composites, polymers to metals, metals to metals, and ceramics to metals. Adhesive-bonded joints can withstand shear, tensile, and compressive stresses, but they do not exhibit good resistance against peeling. High adhesive bond strength is achieved if chemical bonds are formed between the adhesive and the base material, or adherent. To improve the adhesive bonding strength, surfaces to be joined by adhesives must be cleaned thoroughly which minimizes the interfacial gap between the adhesive and the adherent. Rough surfaces also improves adhesive bond strength because of the mechanical interlocking.
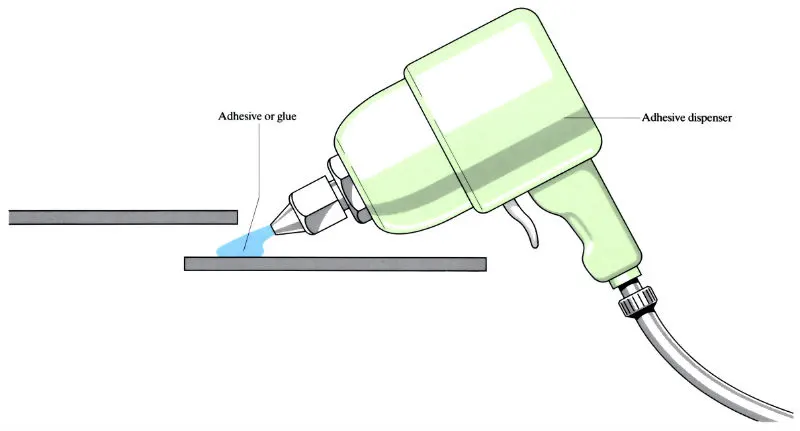
Image 2.5 Adhesive bonding
5) Diffusion bonding
Diffusion Bonding is a solid-state joining process which undergoes macroscopic deformation of workpieces. It is performed at temperatures higher than half the absolute melting point of the base material. Diffusion bonding involves two stages
1) Deformation processes of the surfaces to be joined.
2) Formation of bonds by diffusion-controlled mechanisms such as grain boundary diffusion and power law creep.
Diffusion bonding can be performed with various sizes of metal and ceramic parts.
It is very slow process and it is performed at inert atmospheres to avoid oxidation. this can be done in layers by layers also
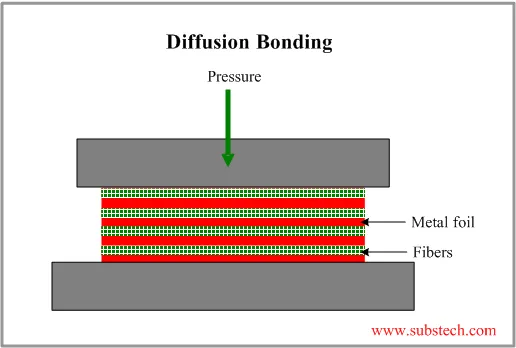
Image 2.6 Diffusion bonding
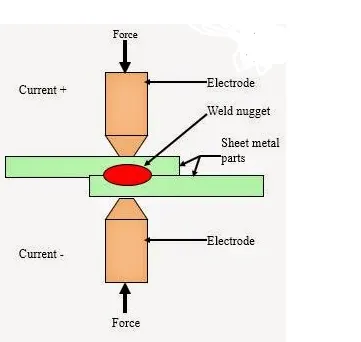
3. Resistance Welding: In this type of joining process two metal workpieces are joined together by applying force to a consumable electrode through which AC or DC current is passing through to create a permanent joint between them. This force should be in moderate because if a high force is applied the sheets might weld due to over-heating and if lesser force is applied workpieces might not be joined and a spot mark is created which leads to a reduction in the life of the product.
- RSW (Resistance Spot Welding): It is the type of resistance welding where two workpieces are joined using a consumable electrode passing through AC/DC voltage and a spot is created at the edges of the part to be joined that leads to a permanent joint between them by application of applied force by the user. eg: Doors, Window panes, etc.
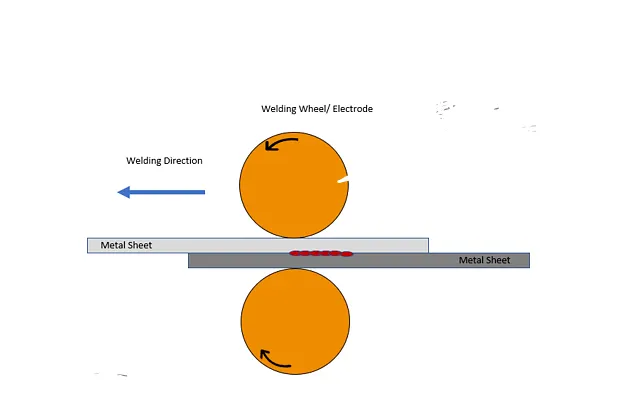
- RSW (Resistance Seam Welding): It is the type of resistance welding where hot-rolled electrodes are used and they both run in opposite directions on that side of the workpieces where they are free. Then some moment is applied at the electrodes and the workpieces' edges get welded in a seam. eg: fuel tanks, radiators, etc.
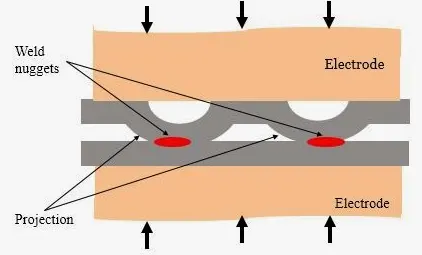
- RPW (Resistance Projection Welding): It is the type of resistance welding where two workpieces are joined using a consumable electrode passing through AC/DC voltage and a projection is created at the welded joint which is of the same projection as that of the part to be joined that leads to a permanent joint between them by application of applied force by the user. eg: welded nuts to a panel in the automotive industry.
4) What is fusion welding & types of fusion welding with its application in the automotive sector?
Fusion welding process uses heat to join or fuse two or more materials by heating them to melting point. The process may or may not require the use a filler material. External application of pressure is not required for fusion welding processes, except for resistance welding, where substantial contact pressure is required during welding for sound joining.
The different types of fusion welding are as discussed below
1) shielded metal arc welding:
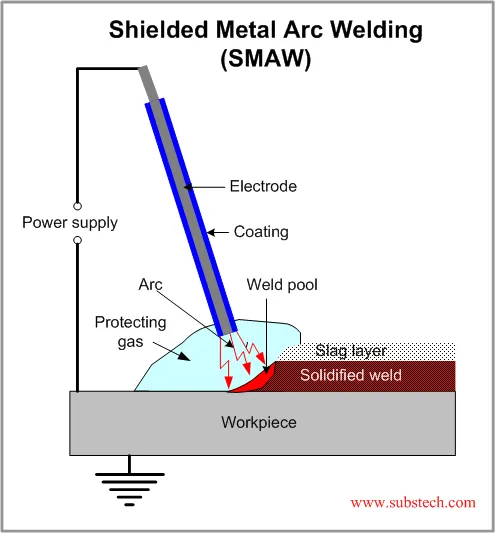
Image 4.0 Shielded Metal arc welding
It is also known as manual metal arc welding, flux shielded arc welding or stick welding that uses a consumable electrode covered with a flux to lay the weld. An electric current either AC or DC is used as welding power supply, That power supply is used to form an electric arc between the electrode and the workpieces to be joined. The workpiece and the electrode melts forming a molten metal pool that solidifies to form a joint. As the weld is laid, the flux coating of the electrode disintegrates, giving off vapors that serve as a shielding gas and providing a layer of slag, both of which protect the weld area from atmospheric contamination.
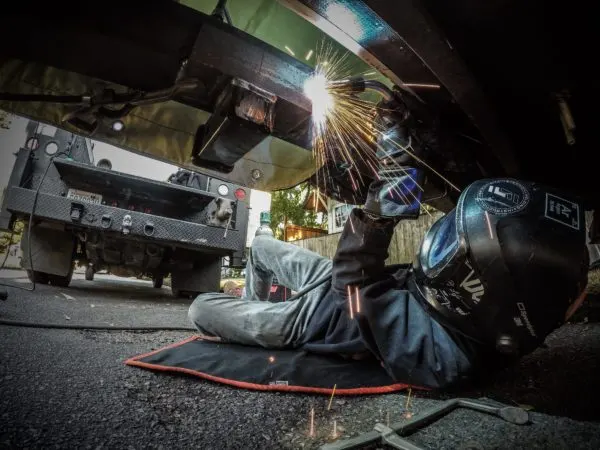
Image 4.0.1 Shielded metal arc welding in automotive industry
This welding is used in the joining of base parts of chassis and doors of the automobiles
2) Metal inert gas welding:
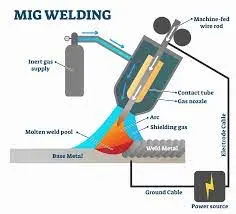
Image 4.1 MIG welding
It is also known as Gas Metal Arc Welding or Metal Active Gas welding in which an electric arc forms between a consumable wire electrode and the workpiece leading them to melt and join. Both use a shielding gas to protect the weld from airborne contaminants, or oxidation in the case of MIG welding. The process can be semi-automatic or automatic. A constant voltage, Direct current power source is most commonly used with GMAW, but constant current systems, as well as AC, can be used. There are four primary methods of metal transfer in GMAW, called globular, short-circuiting, spray, and pulsed-spray, each of which has distinct properties and corresponding advantages and limitations.
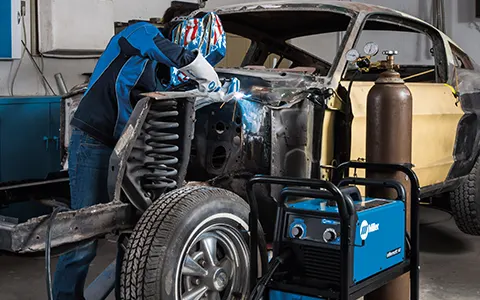
Image 4.1.1 MIG welding in automotive industry
This welding is used in the joining of bone, chassis area and engine parts in automotive industry.
3) Tungsten Inert gas welding:
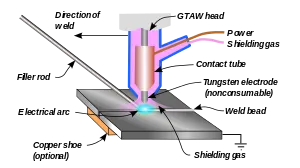
Image 4.2: TIG welding
This is an arc welding process uses a non-consumable tungsten electrode to create the arc between the electrode and the base plate. An inert shielding gas is used to protect from oxidation or other atmospheric contamination. A Constant current welding power supply produces electrical energy, which is conducted across the arc through a column of highly ionized gas and metal vapors known as a Plasma.
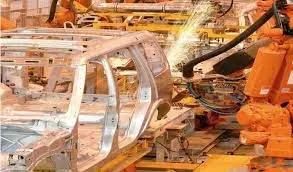
Image 4.2.1 TIG welding in automotive industry
TIG welding is most commonly used to weld thin sections of stainless steel and non-ferrous metals such as aluminium BIW structures of automobile.
4) Plasma arc welding:
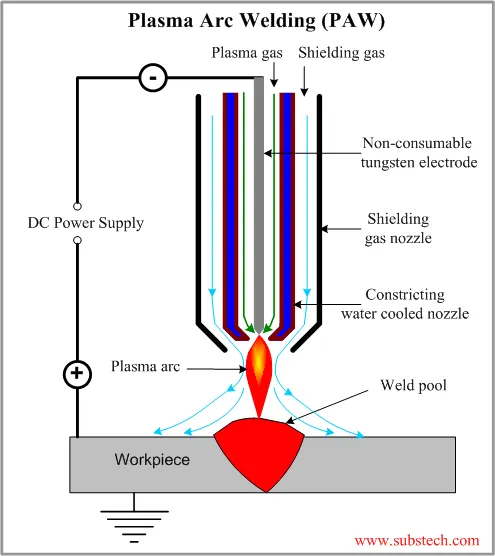
Image 4.3 Plasma arc welding
This process uses an electric arc created between an electrode and the torch nozzle. The electric arc ionises the inert gas (argon) in the chamber creating what is called as plasma. It is then forced through a fine bore copper nozzle that constricts the arc and directs it to the workpiece, allowing the plasma arc to be separated from the shielding gas (mixture of argon and hydrogen).
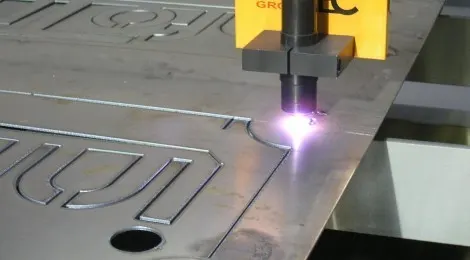
In auto motive industry plasma arc welding/cutting was used for several purposes.
5) What is the 3-2-1 principle?
During metalworking process, it is very much important to locate the parts to be worked relative to the work fixture. Any variation in part location on the fixture adds to the dimensional tolerance that must be assigned to the finished parts. The method of supporting and securing the part in the fixture affects not only dimensional tolerances, but surface finishes as well. Techniques for supporting and clamping must be considered together with the method of locating in order to assure repeatability from part-to-part. The basic principle of fixture is to restrict all degrees of freedom in the desired location and orientation
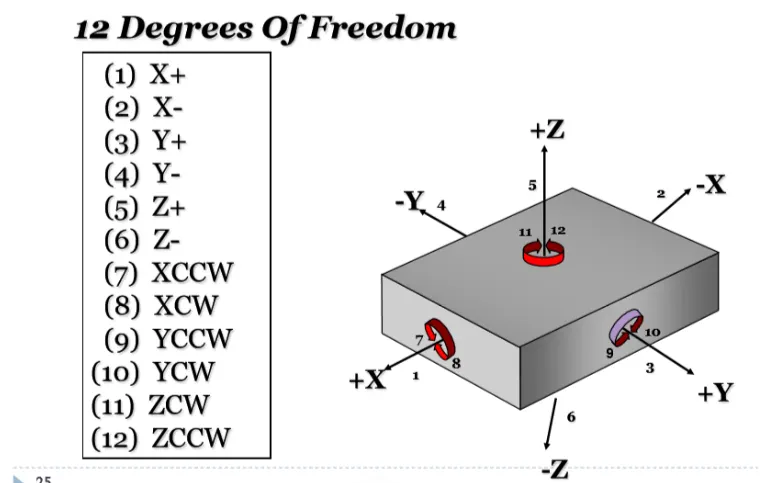
Image 5.0 Degrees of freedom
As shown in the above image degrees of freedom are 12 in that there are 6 translational degrees of freedom and 6 rotational degrees of freedom.
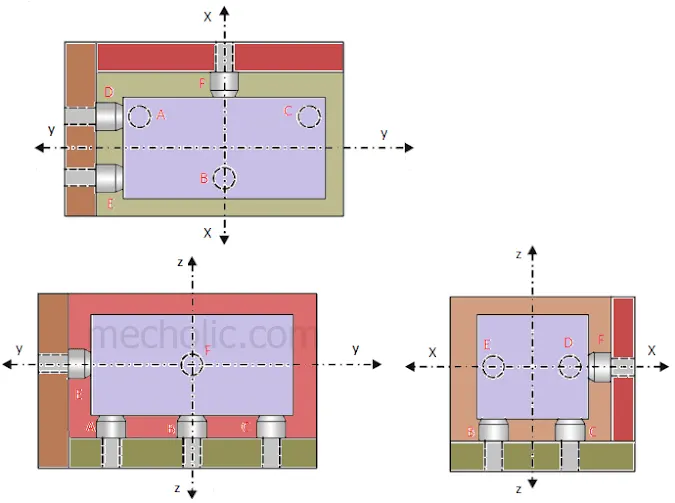
Image 5.0.1 3-2-1 pronciple
Pins A, B, C in the above image on the base plane ( a plane parallel to the plane which contains X and Y axis) restrict the rotation of component about X axis and Y axis. It also limit the downward movement of component along z axis. Ie. 1,2,3,4 and 5 degrees of freedom is restricted. Pins D, E is in plane parallel to the plane containing X and Z axes. It prevents the rotation of component about Z axis (6, 7 degree of freedom) and the movement of the body in along Y axis towards one direction (8 degree of freedom). The last pin F is in a plane parallel to plane contains Y and Z axes. It restricts the movement component along X axis in one direction. Three remaining degree of freedom 10, 11, 12 is unrestricted. It facilitates the loading of the component in the fixture. This three degree of freedom may restrict after loading of component by using clamping devices.
6) Define Body coordinate system?
Body coordinate system is also called as car line or body line. Coordinate system is a reference system Consisting of a set of point, Lines & surfaces used to define position of point in space either in 2 or 3 dimensions
Maintaining X,Y & Z co-ordinates in fixture is a very important factor. We should try that the co-ordinates of locating and clamping points should not be in three decimal (e.g. X=100.124, Y=245.127, Z=450.458). They should be in the whole nos. or max upto 1 decimal . Once these co-ordinates are maintained automatically the BIW base structure is maintained.
All vehicle product drawings are identified numerically relative to three vehicle planes Description shown below.
- (X) It is in width of BIW – 0X is Body Center Line
- (Y) It is in length of BIW – 0Y is Near Front Bumper
- (Z) It is in length of BIW – 0Z is about centre of the wheel
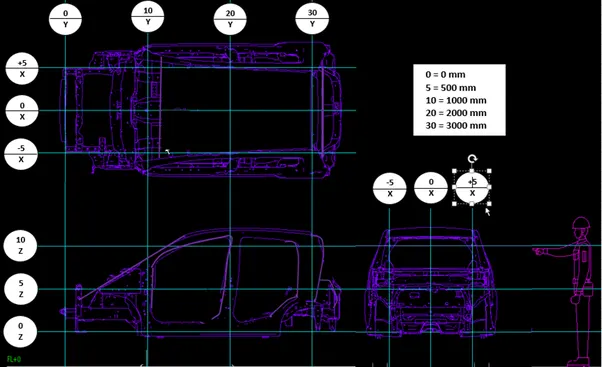
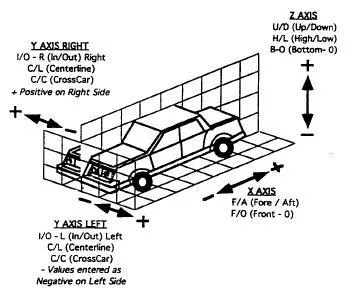
Image 6.0: Typical body coordinate system in BIW and car body
7)Elaborate Body plane system & its essentials?
Body planes are three mutually perpendicular imaginary planes. These are reference planes in automotive car. These are used to define GD & T of all parts in automotive domain. The measurement from body plane to parts are called body plane dimensions.
Body planes are essential for because
- It defines exact position of each product in the vehicle w.r.t a fixed origin.
- It ensures flawless design for assembly.
- While designing lines, all the designs are carried out relative to the bodylines viz.fixtures, Turntables etc.
- It assist in easy location of different parts in the vehicle.
- It aims in creating a standardized system.
- It assist in quality checks.
Image 7.0: Typical body planes of the car
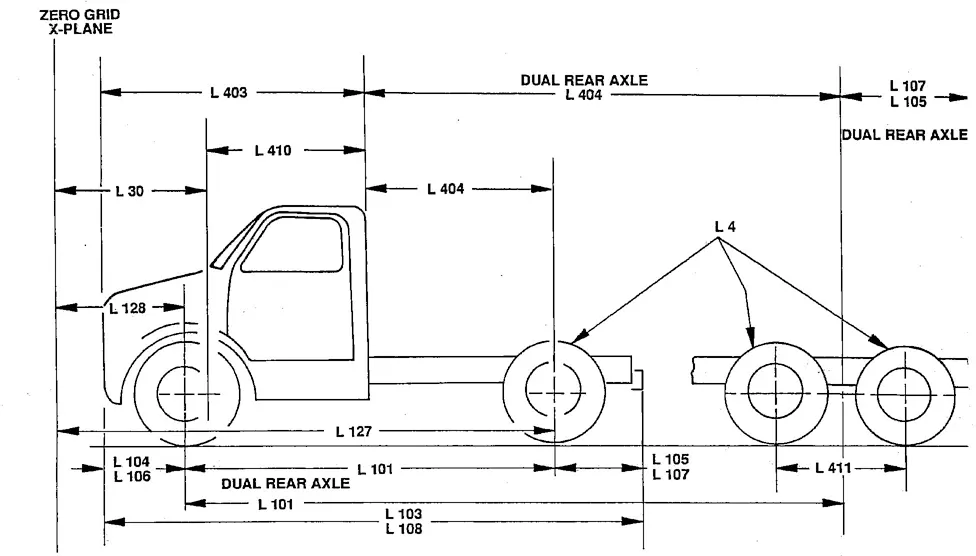
Image 7.1 : Body planes and dimensions measurements using body planes