Week 12 Challenge
Aim: To add Ejector system to the mold assembly complete with back plates and pins. Creating runner gate system and provinding cooling channels.
1. Ejector System:
To eject the plastic component out of the COre blcok, ejectors are required. As the ejectors are on a slope D type ejectors are needed. Ejectors are attached to the ejector plate and hence necassary reliefs are provided to hold all the ejector pins. Reliefs are provided in the core block to guide the pins.
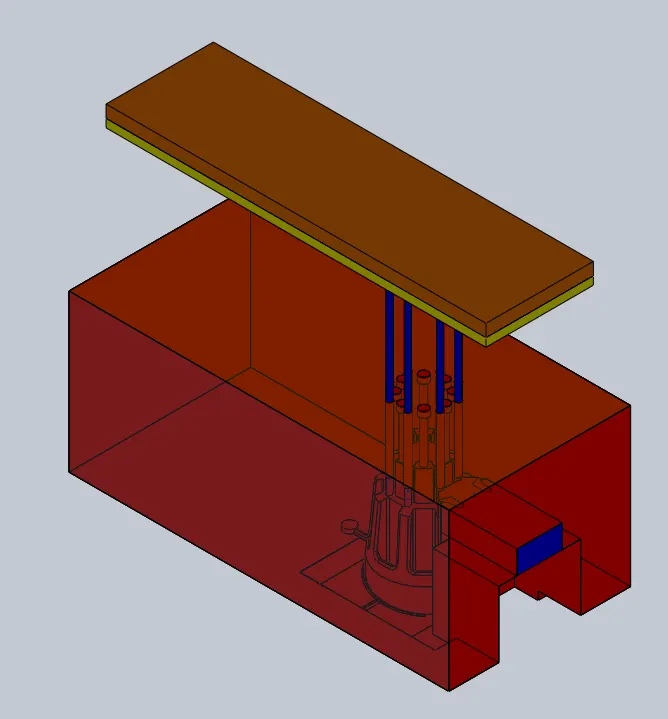
Ejector System
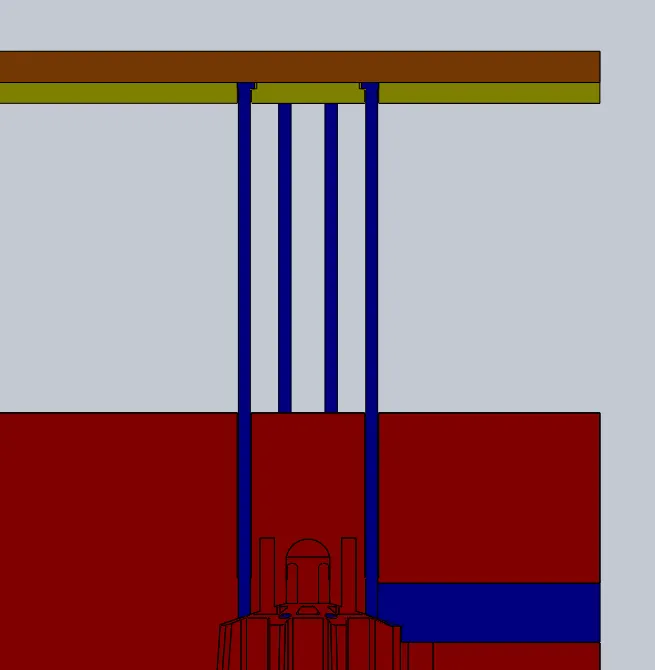
Cross-section of pin with back plate
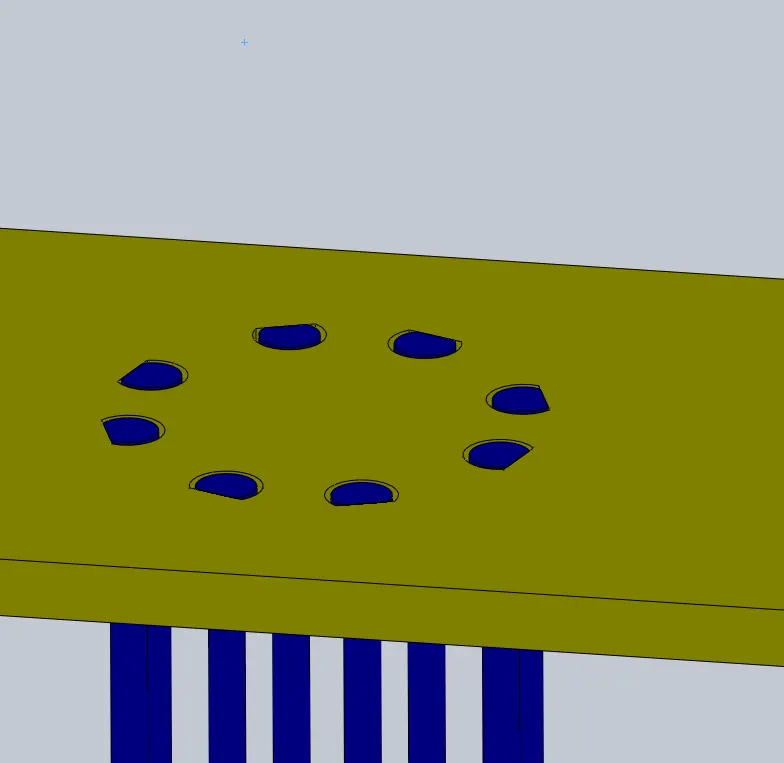
Provision to hold the pins in back plate
2. Runner Gate system:
The Sprue is provided in the cavity block and the inlet is tapered such that it deataches from the cavity block when the core and cavity block separate. The runner and gate is created in the caore block and subtracted from the core block and fillets are provided for proper flow of the molten plastic into the cavity.
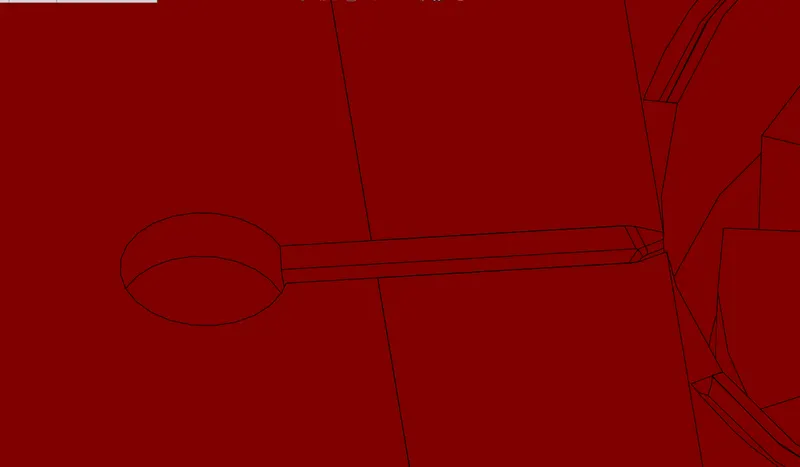
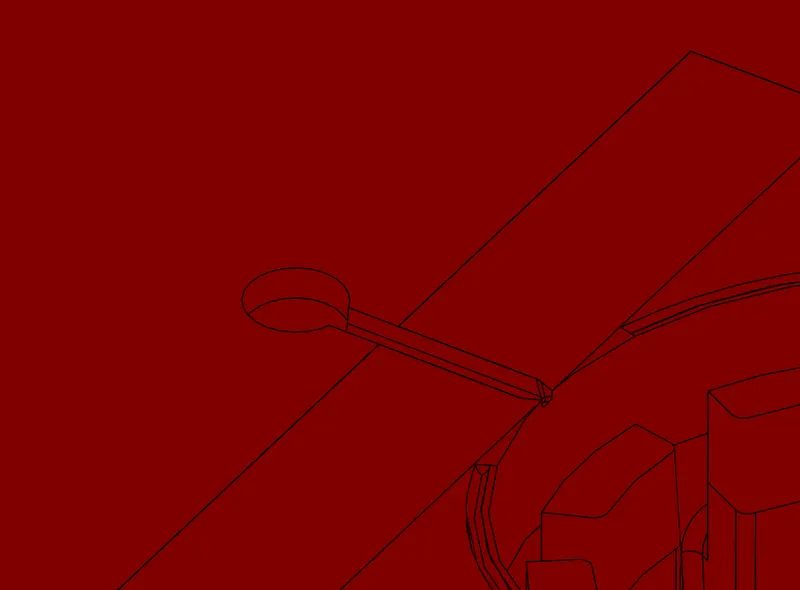
Runner and Gate
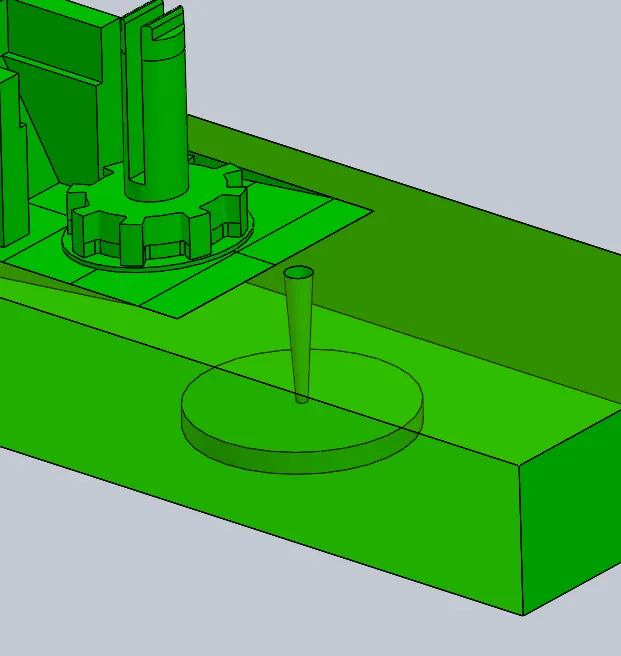
Sprue (Cavity Block)
3. Cooling Channel and Air Vent:
The air needs an outlet when it is filled with the molten plastic. Hence, cooling channels are provided. The cooling channels are provided at the side from where the gate is located. A step is provided so that the plastic doesn't flow over and only air is passed through the air vent.
For the cooling channel a standard sizes are provided and the channels are provided such that it uniformly cools the plastic inside.
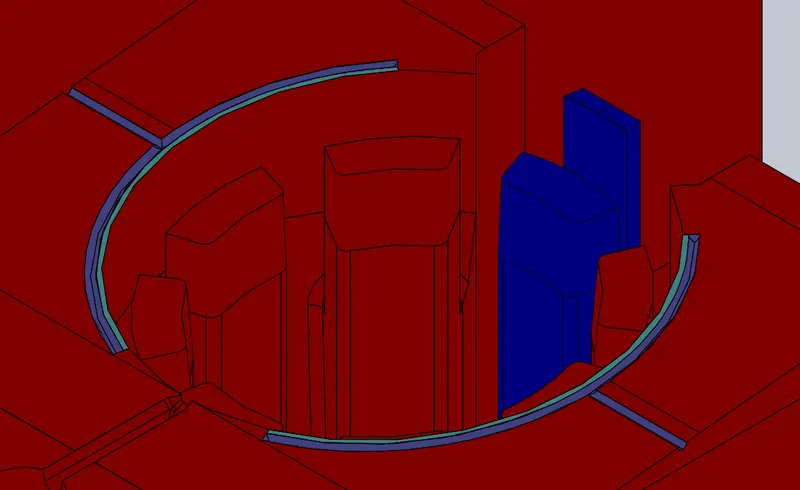
Face in purple (channel to gide air out); Face in blue (Step to stop molten plastic from flowing over).
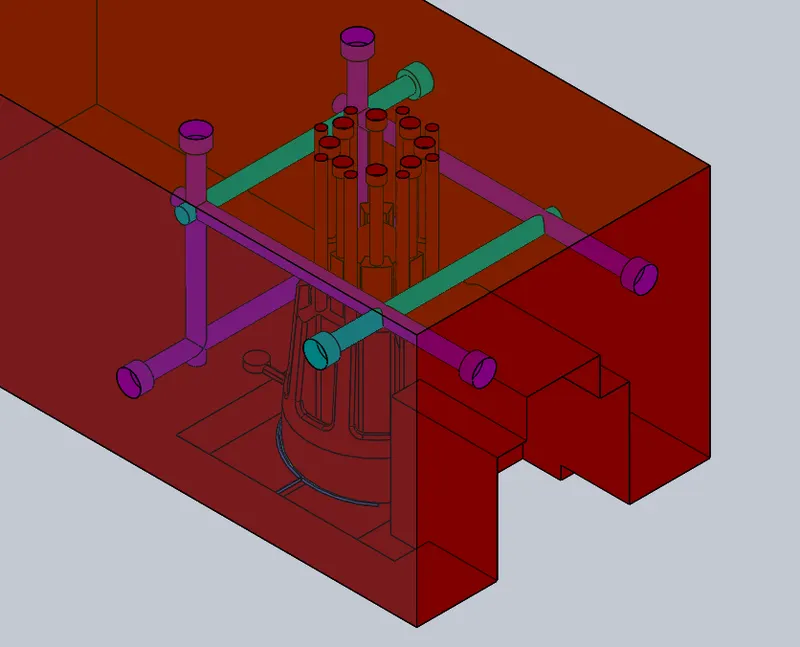
Cooling channels.
4. Assembly:
Since, there are a lot of parts in the assembly for a mold. Sub assemblies are created for each classification. The assembly are divided into,
Mold part: Under which the part to be molded is listed.
Top Part: Under which the cavity block and all the parts associated with the cavity block is listed.
Bottom Part: Under which the core block and all the parts associated with the core block, i.e., silders, inserts are listed.
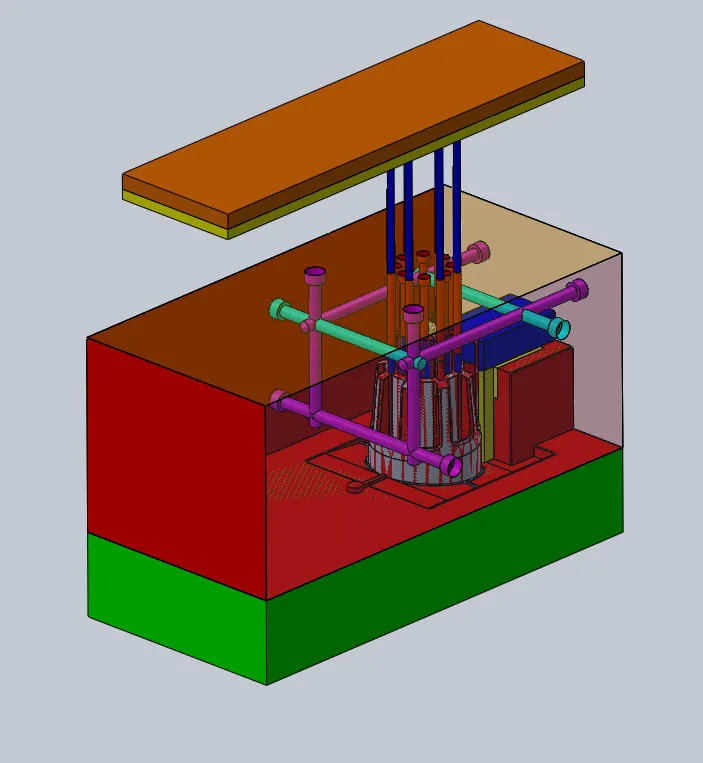
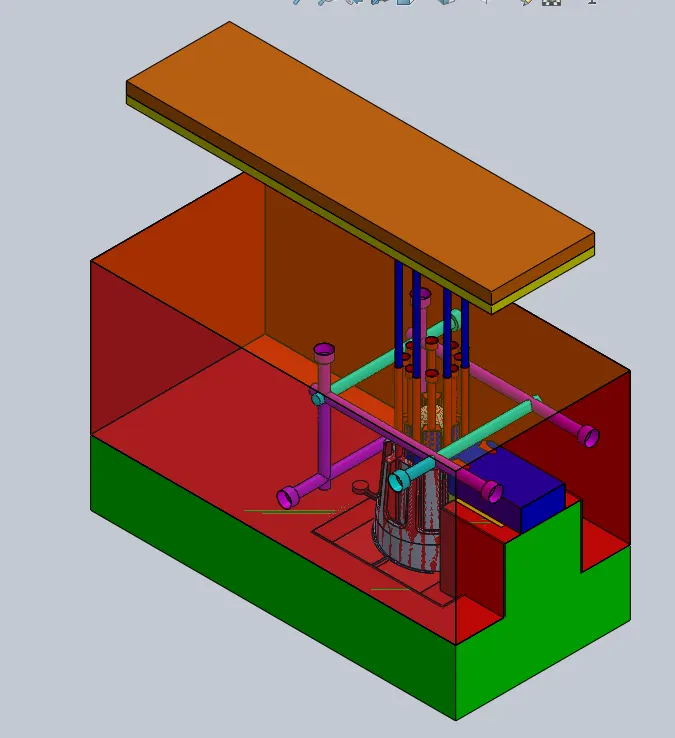
Conclusion: Thus, the ejector system, runner and gate system, air outlet and cooling channels are added to the mold assembly.