Week 10 - Challenge 3 - Door Trim Lower with Engineering Features
Aim:- To Create the Door Trim Lower Plastic component through the given class-A surface.
Requirement:- The creations of locators and heat stakes usnig class A surface.
1. Class A surface
2. Tooling axis using with bisecting method
3. Class B surface
4. Class C surface
5. Closed A,B,C surface body
6. Locators
7. Heat Stakes
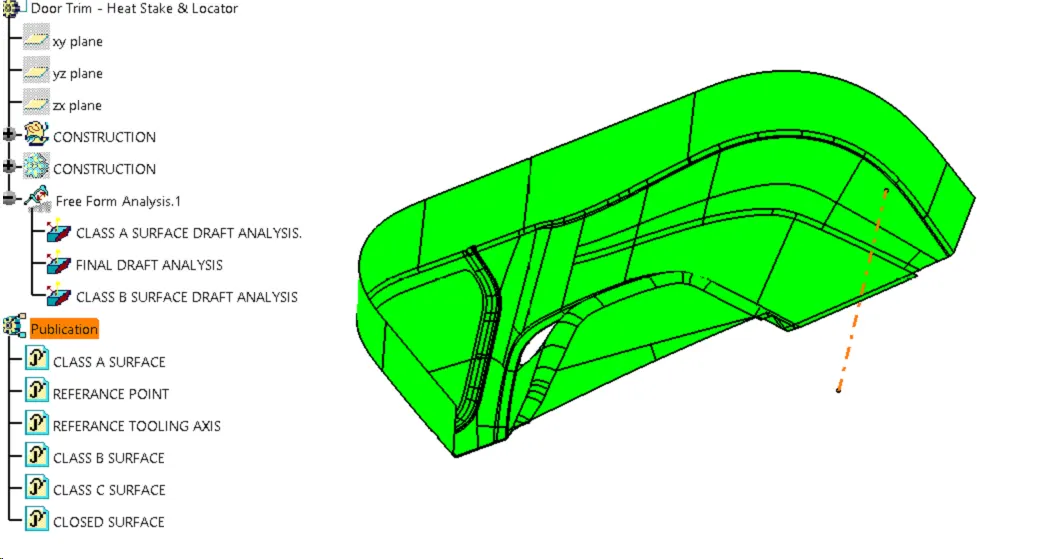
8. Draft Analysis
Referance image of plastic design component
1. Class A surface Its the primary surfce which is use to create plastics component.
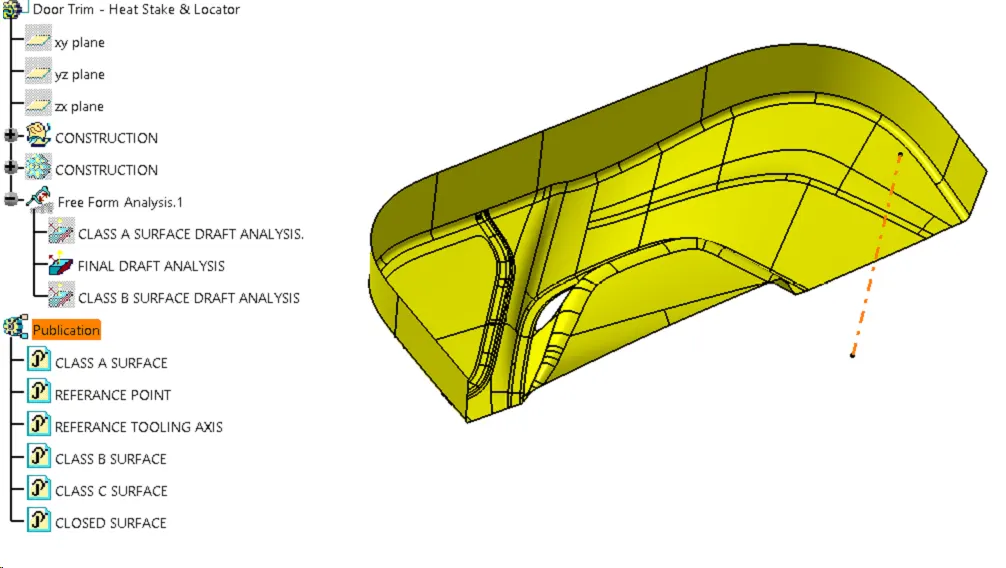
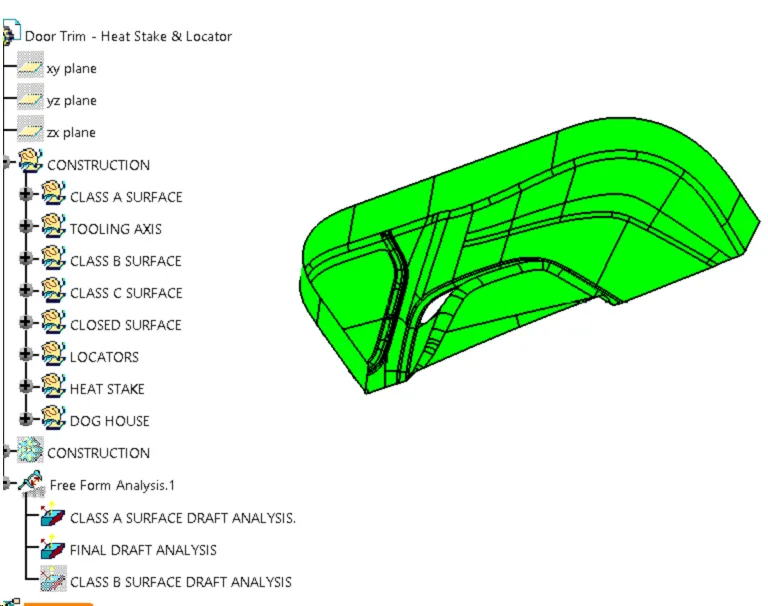
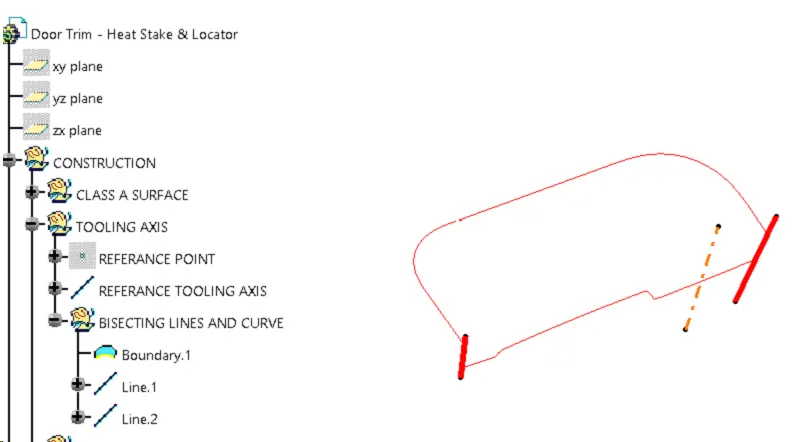
2. Tooling axis using with bisecting method Its the axis at which dies are operate together i.e upper and lower die are come in contact with each other and result is the tooling plastics component & due to the tooling axis component clear the draft angle/analysis. making tooling axis use the bisecting method to clear the draft of plastic design component.
3. Class B surface Its the offset value of class A surface and its 2.5 mm ( consider as per the given in actual body )
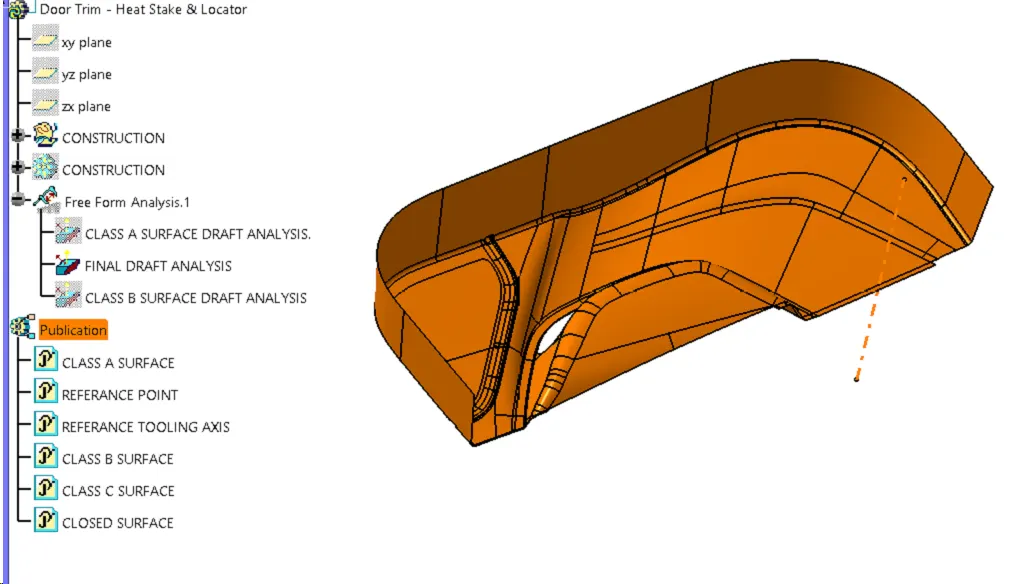
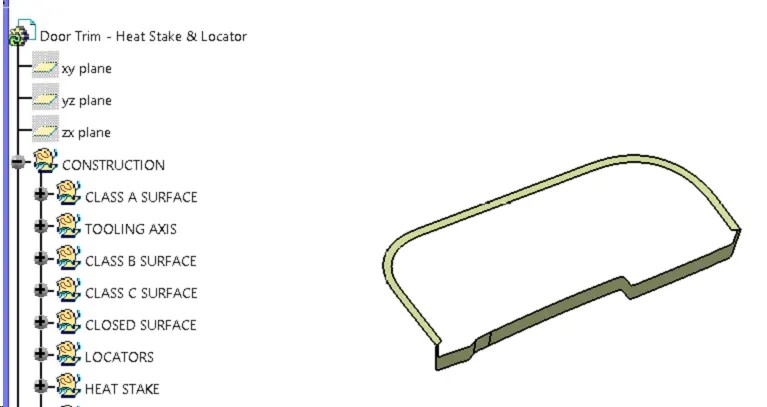
4. Class C surface Its the surface at which two surface are joined together called class c surface.
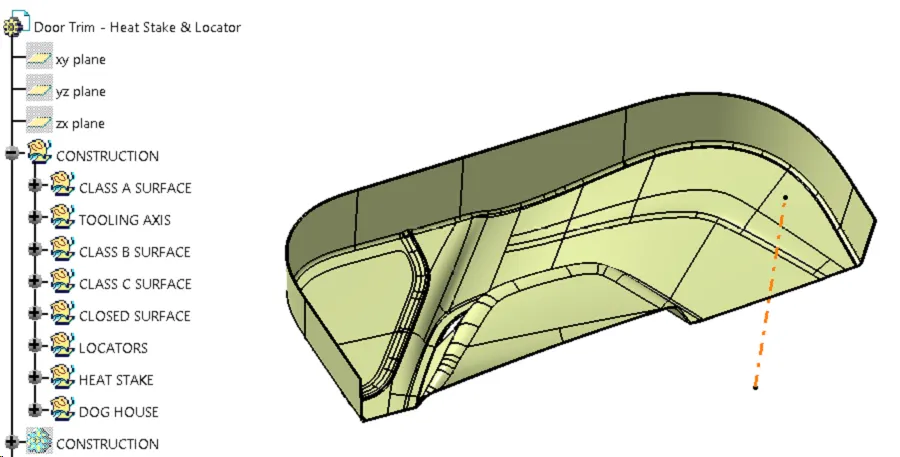
5. Closed A,B,C surface body Its the multiple surfaces like class A surface, Class B surafce & class C surface are joined together.
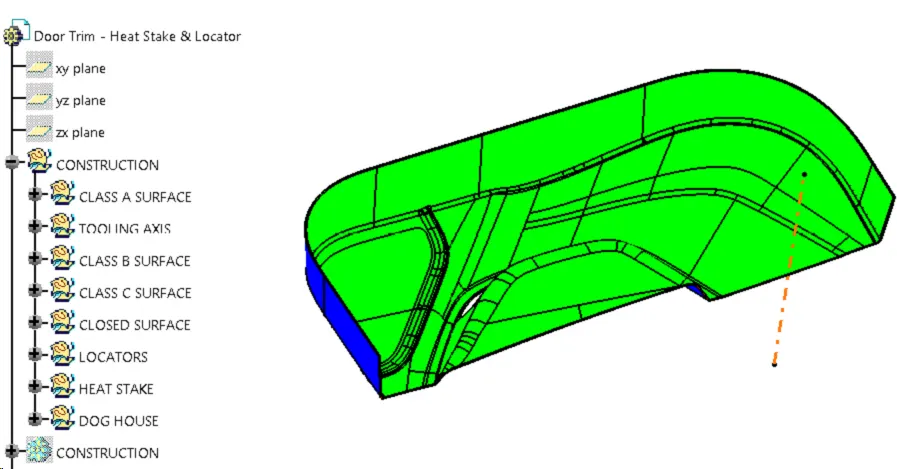
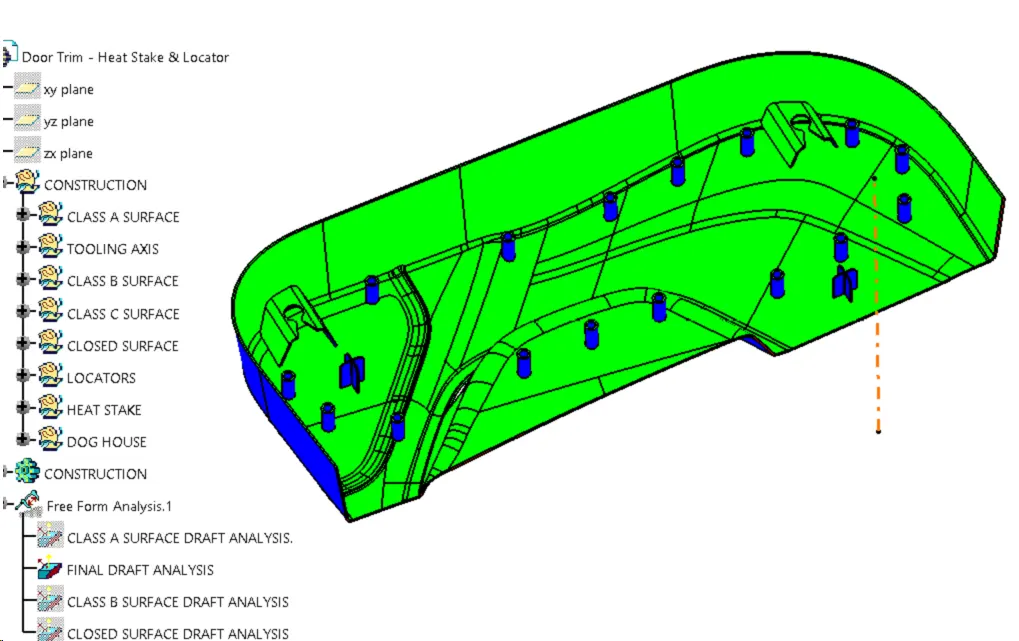
6. Locators Locators are use to place part in assembly and it help to constrain the componet restrict their moment in assembly.
7. Heat Stakes
Its the assembly method which is use to controlled melting and reforming plastic stud or boss to capture or lock onother plastic or metal component of an assembly in place. The plastics stud protrudes through a hole in the component to be locked in place the heated thermal tip contacts the top of the stud which melts and fill the volume of the tip cavity to produce heat locking the component in place of manufacturing of thermoplastics component. below are the given advantages of heat stakes.
Simplifications of machinery
Reduced cost of machinery
Multiple fastening points
Allows higher density of welds compared to hot air cold form or ultrasonic welding
8. Draft Analysis
Draft
The draft is the amount of taper moulded or cast part perpendicular to the parting line. draft angle are a desing consideration that makes it much easier for a part to release cleanly from a mould A draft angle is calculated as a degree measurment ( less often, an inch or millimeter measurment ) from vertical axis of a mould & it helps account of thermoplastic shrinkage. a partical reality of the injection moulding process for most materials.
Draft angles are generally a requirement of injection moulding design (though there are select few soft material, like nylon that can get away with angle of zero) The draft should be a part of the design manufacture and all stakeholders & contributors should be aware of its need at the out side of the design process. This includes product designers, design engineers etc & this allows considerations for desing requirement to be taken into account. Any draft is better then no draft.
Importance of draft
By accounting for thermoplastic shrinkage during the cooling process, draft angles significantly reduce friction between the finished, cooled part and the side of the mould, Not only does this create a much easier release process, but it also offers several other benefits, depending on the design of the part which is as follows:
Reduces the chance of damage to the part due to friction during the release.
Reduces wear and tear and chances of damage to the mould.
Ensures a uniform, smooth, unscratched finish when required. • Ensures the integrity and uniformity of other surface finishes and textures.
Reduces overall cooling time by lessening or eliminating the need for unconventional ejection setups.
Most, if not all, of these benefits, offer either direct or indirect overall production cost reductions.
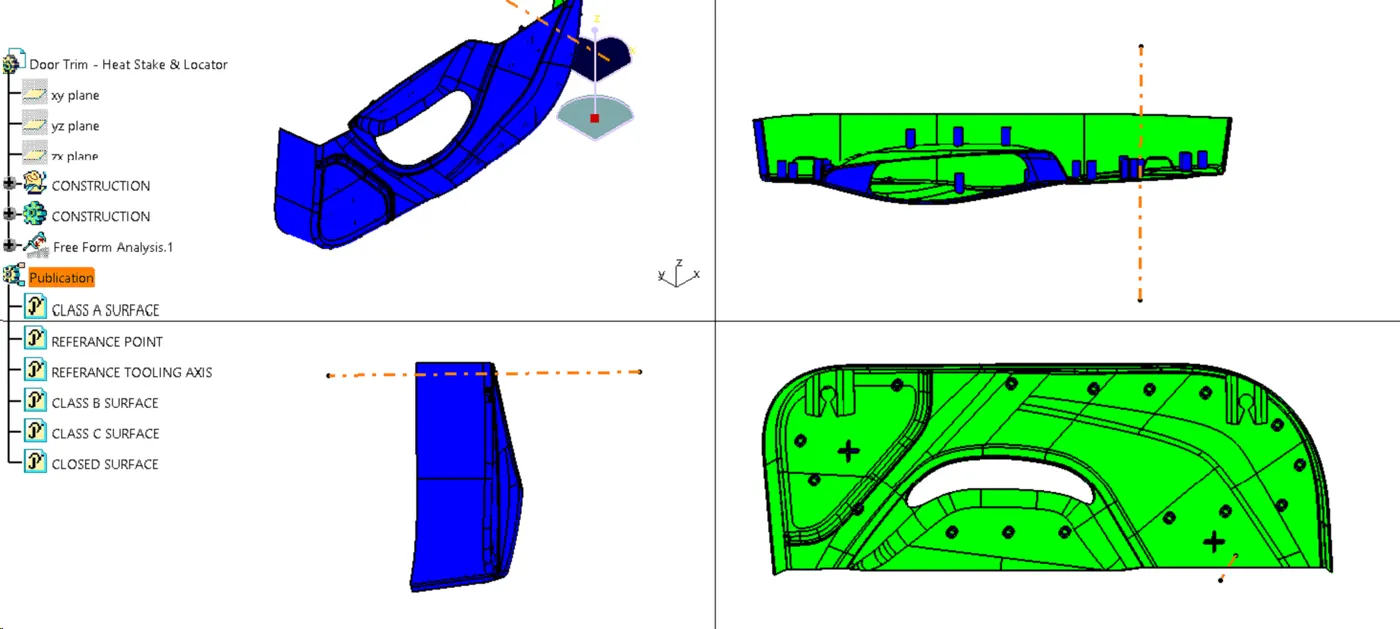
Conclusion In this way we have successfully created heat stakes and locators for arresting the plastics component.