Week 8:- 3D Finishing Challenge 2
Aim:
To perform 3D finishing and create rough locators for the assembly fixture.
Introduction:
It is the process where the fixture is checked in various parameters like hole concentricity, machining area marking, resolving clashes etc. This is the stage in the process where the position of the rough locators is also identified. This process precedes the 2D detailing and design testing of the fixture.
Positioning rough locators:
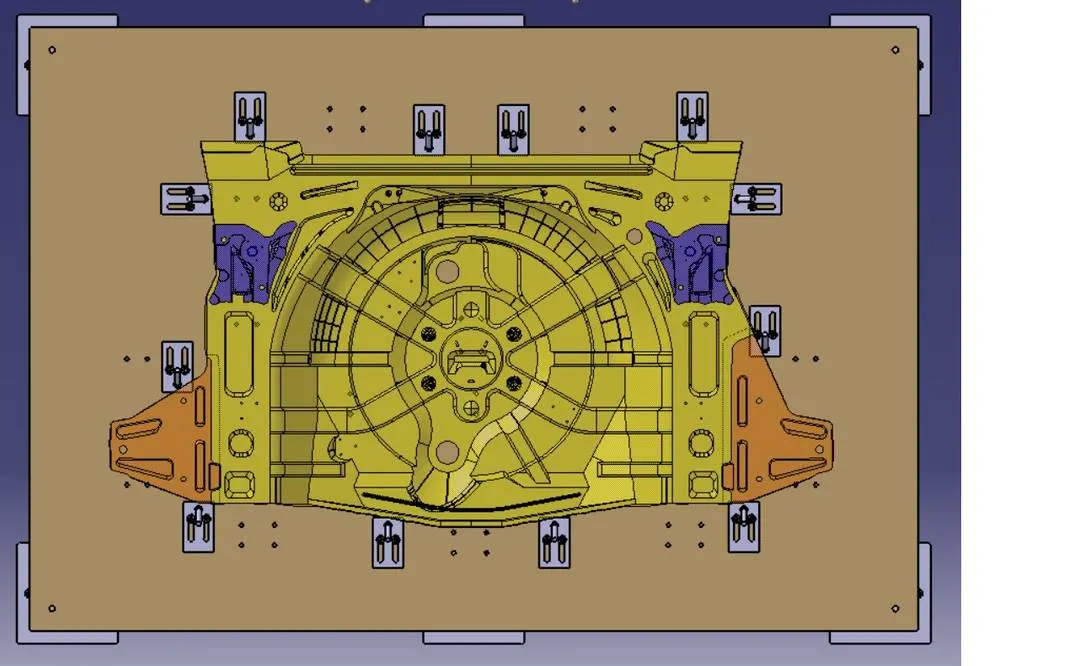
Rough locators are used in allowing the movement of the panel easily into the fixture. They allow with the proper poka-yoke of the fixture.
A minimum of 2mm distance between the panel and rough locator. The entry of the locator should be 10-15 mm above the panel surface. Rough locators may be a rod or flat type.
Checking for clashes:
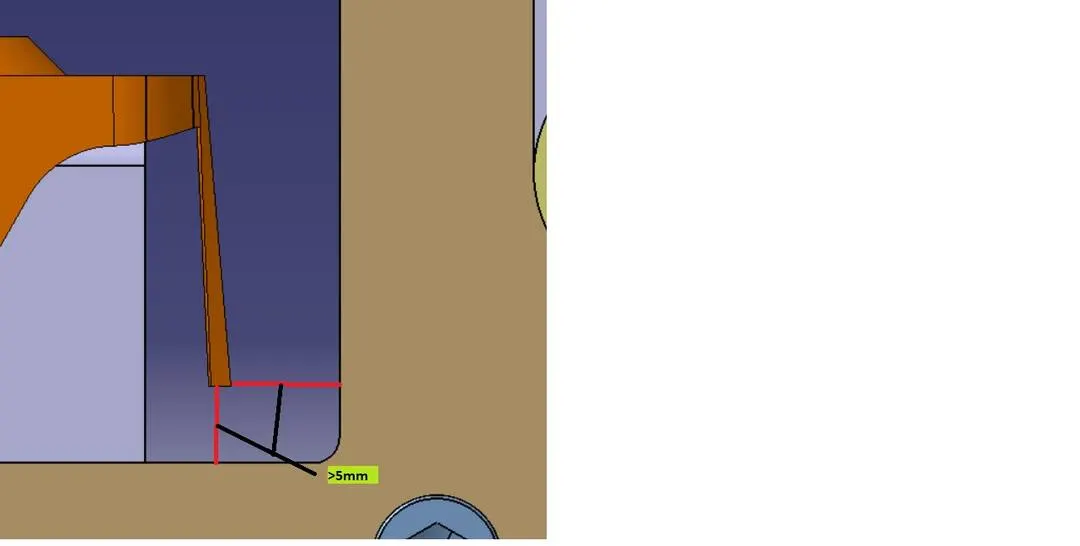
All the parts in the fixture are checked for clashes between one another and the panel. Checking must also be done for panel engagement and disengagement. Space should also be provided for the movent of the welding tool.
Checking nominality and concentricity:
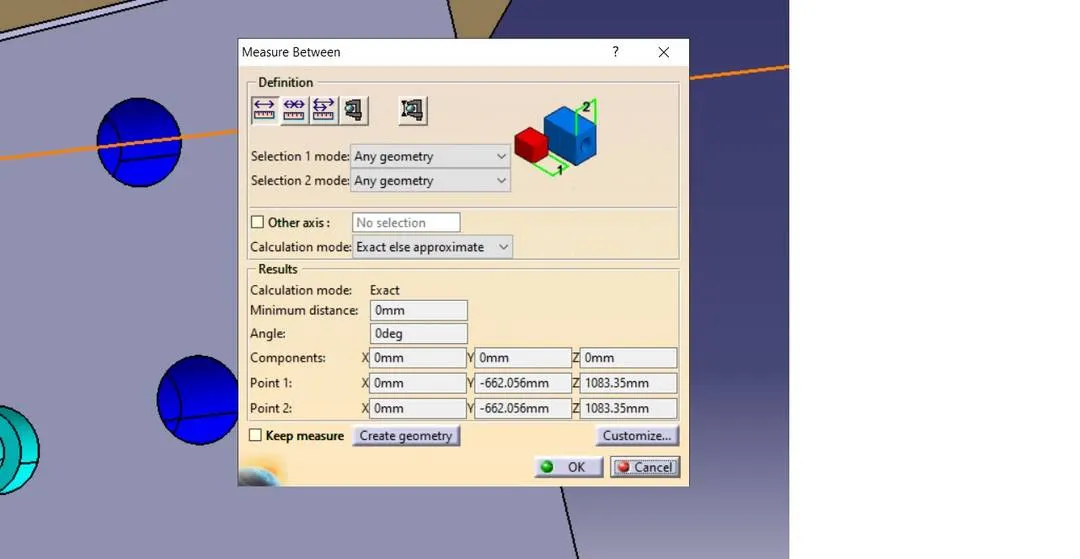
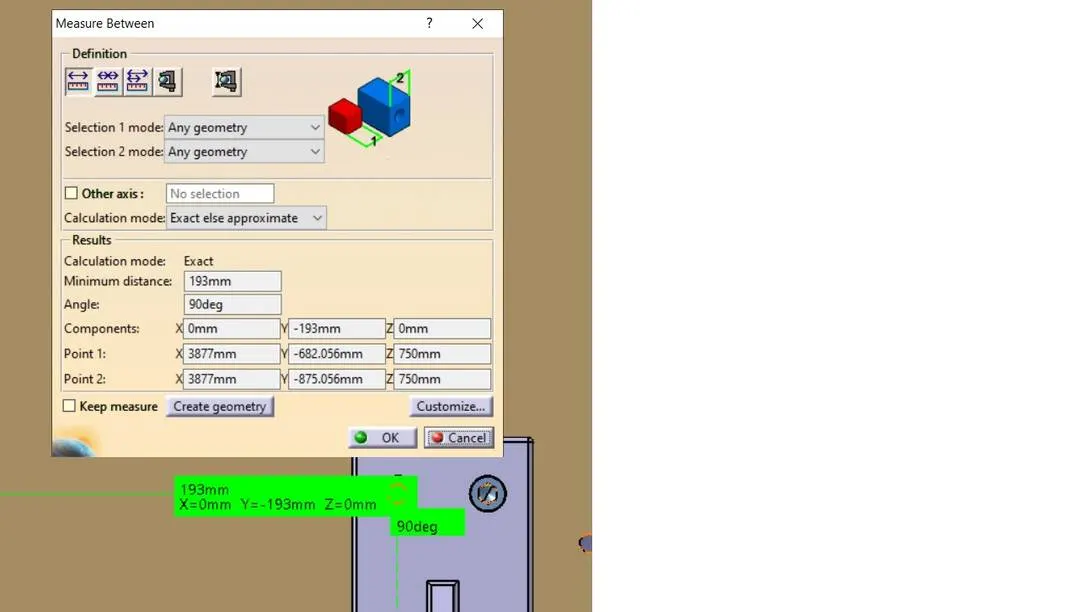
The design dimensions of the fixture must be made nominal if possible and all the holes in the fixture should be checked for concentricity and their respective hole sizes.
Fastener selection and implementation:
The required fasteners are selected as per load requirements and customer preferences.
Machining area definition:
Once the fixture is designed the faces requiring machining must be marked with a standard colour. Machining is done to allow proper mating of parts and only on required parts to reduce machining costs.
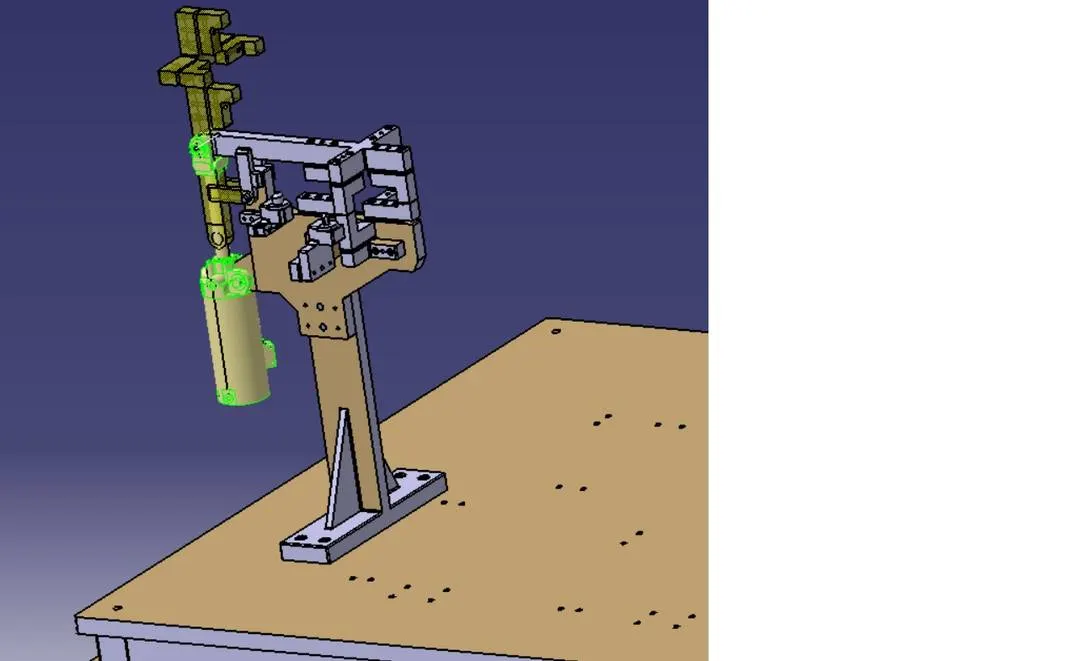
Hole colouring standards:
Hole colouring is done to identify the type of hole used in different parts of the 3D design of the fixture.
| Cyan |
Normal hole |
| Yellow |
Threaded hole |
| Blue |
Dowel hole |
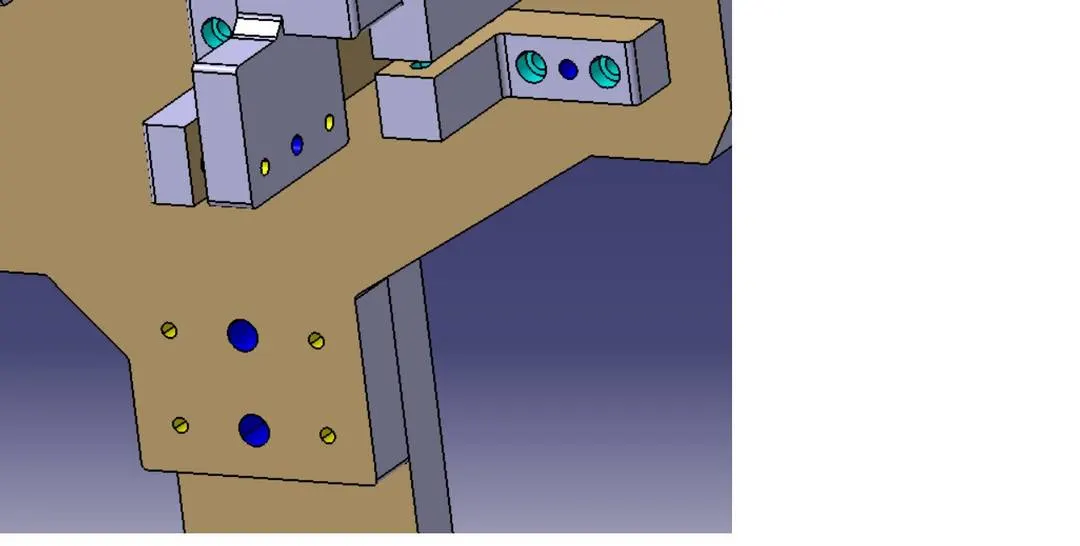
Proper renaming and arrangement of parts in the tree:
The individual assemblies and parts should be properly named as per customer requirements and proper design tree arrangement must be carried out to easily identify the different parts of the fixture.
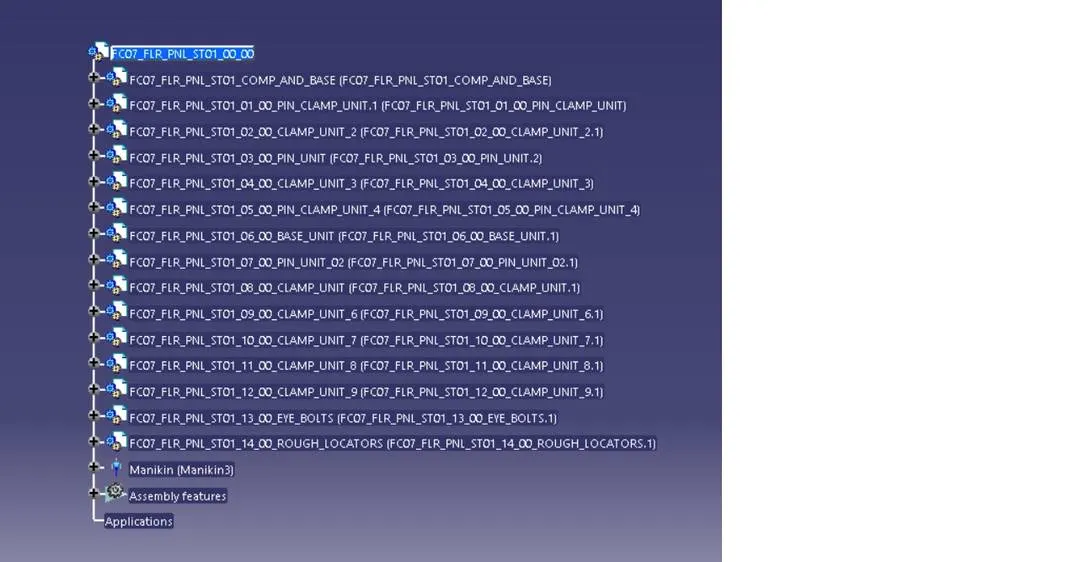
Pin Unit:
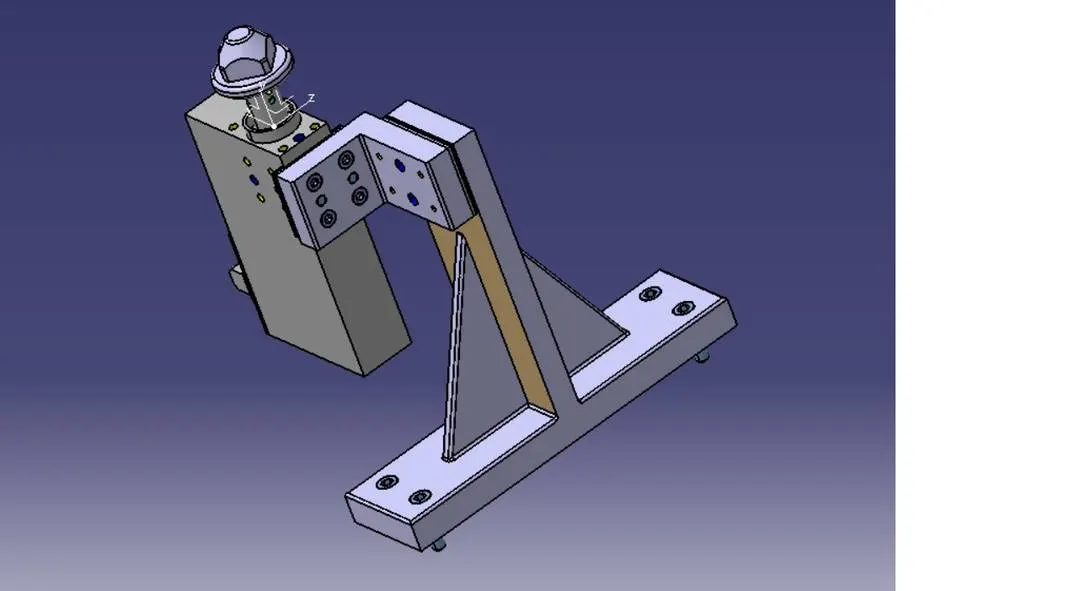
Clamp Unit:
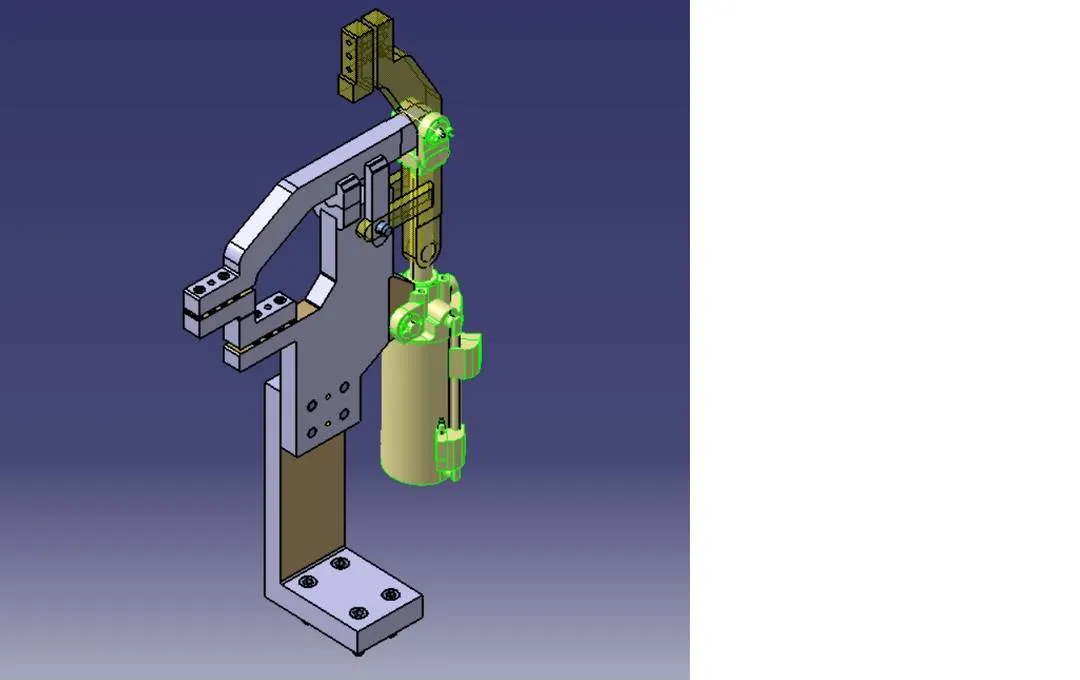
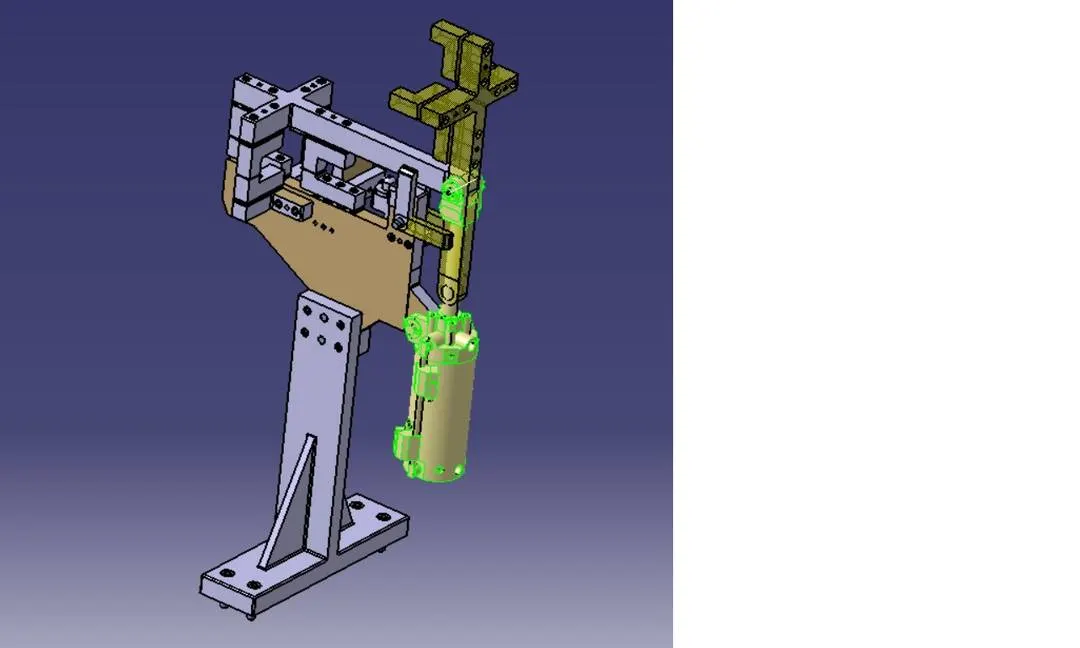
Pin-Clamp Unit:
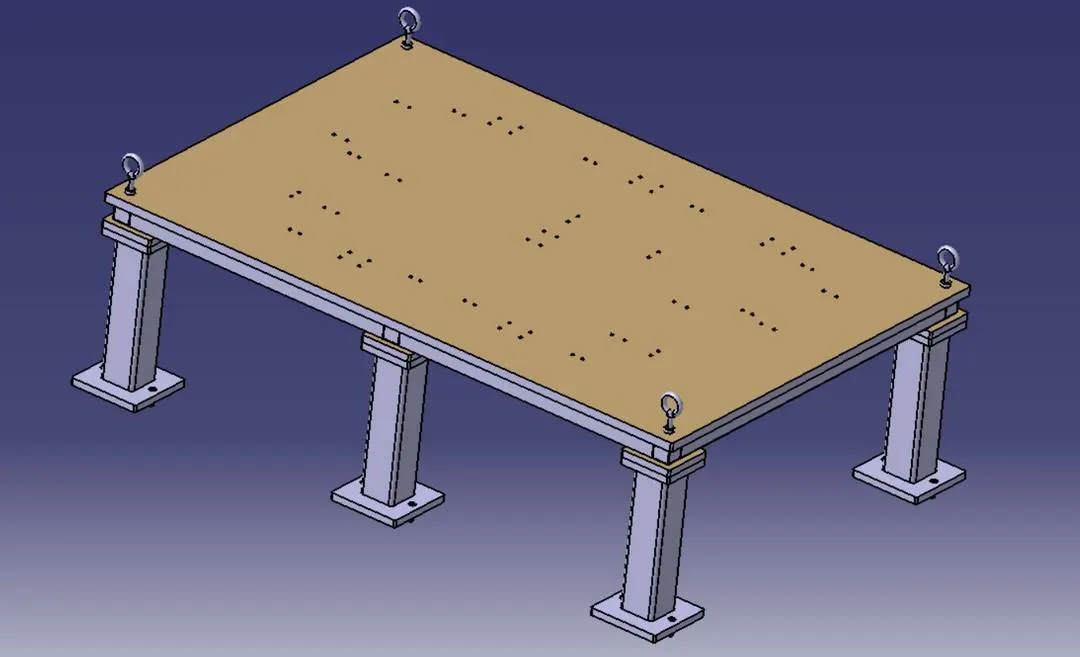
Base unit:
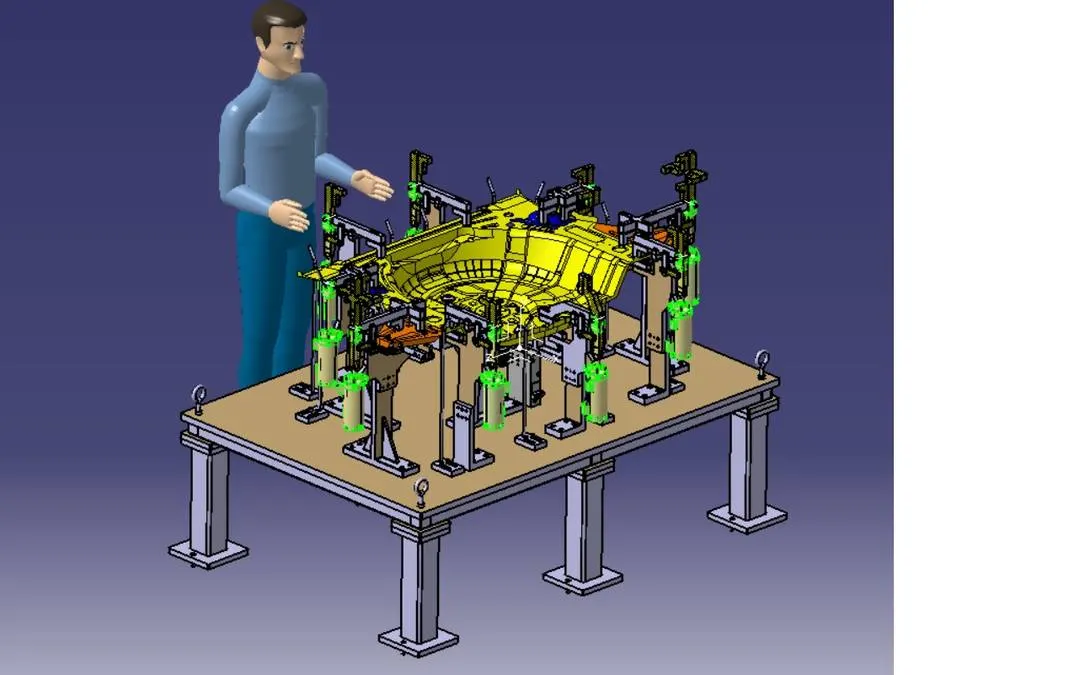
Fixture Assembly:
Conclusion:
Thus the fixture is designed and final 3D finishing processes are carried out as required and 2D detailing processes may now be carried out.