3D Finishing
Aim/ Introduction:
Perform 3D finish for all units of assembly design. Create rough locators for assembly.
Theory:
3D Finish
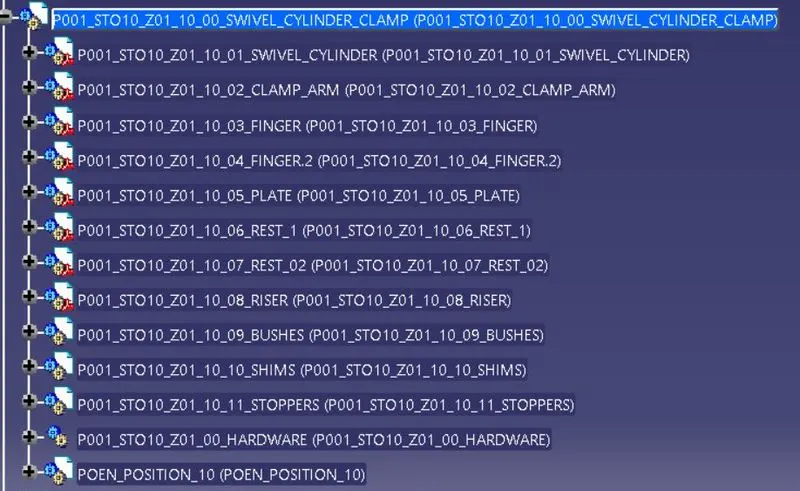
3D finish is a process where the design is being completely finished & to be ready for final simulation & 2D detailing. The following points are taken into consideration while finishing the design
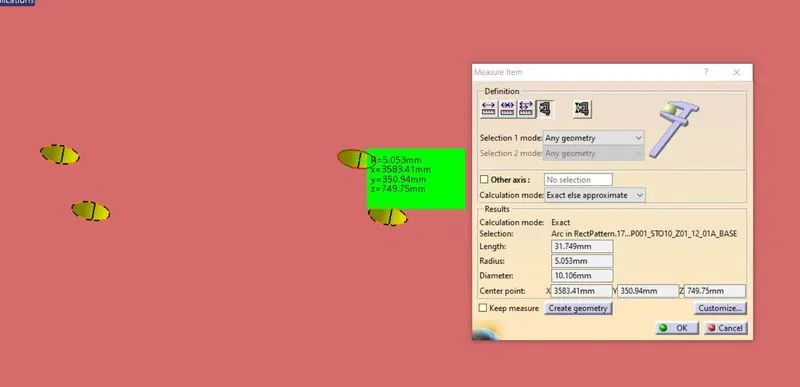
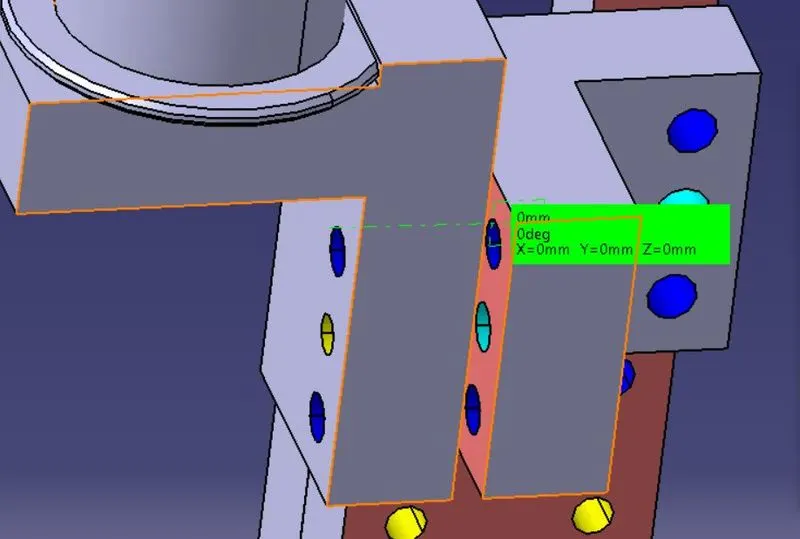
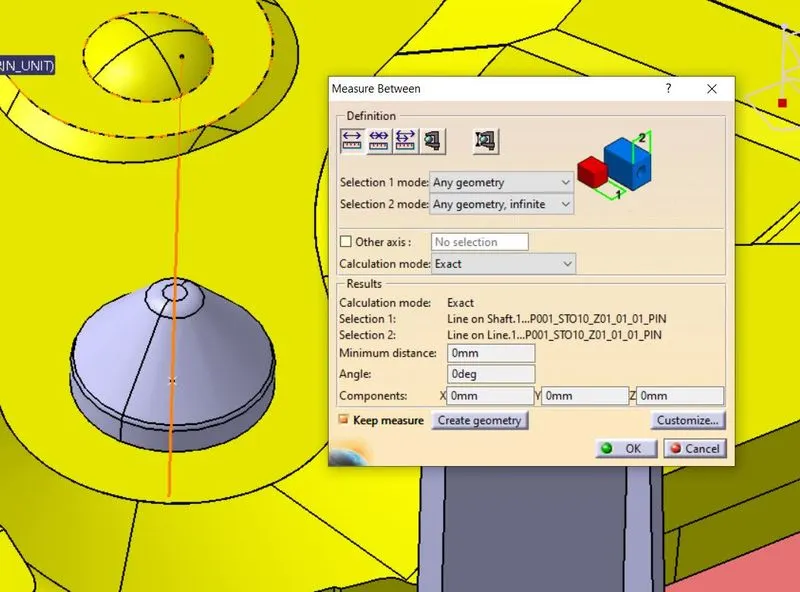
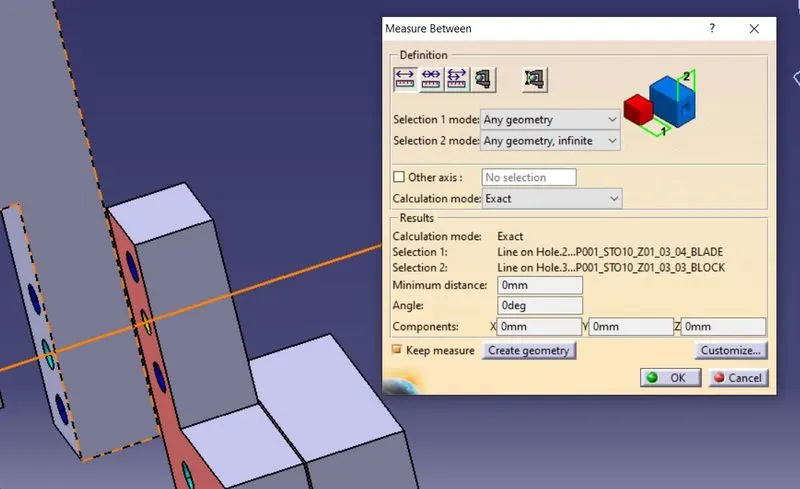
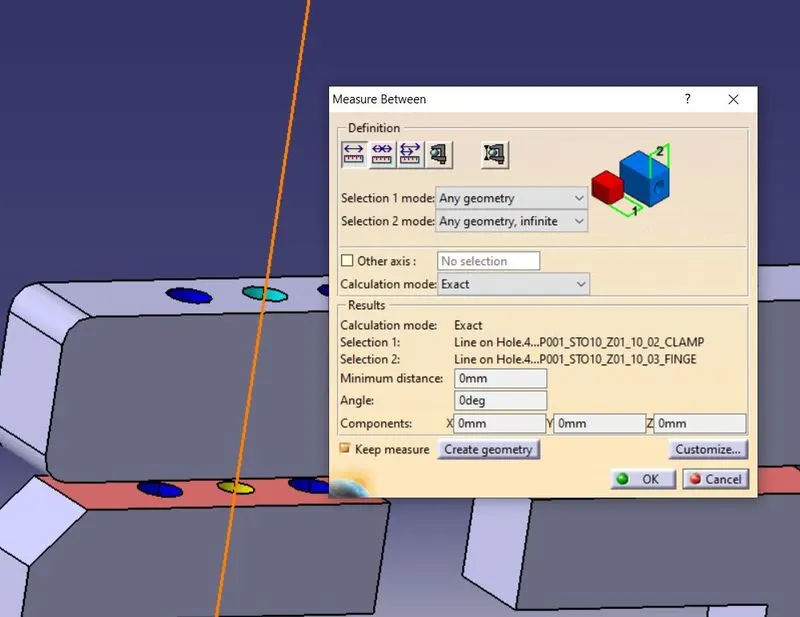
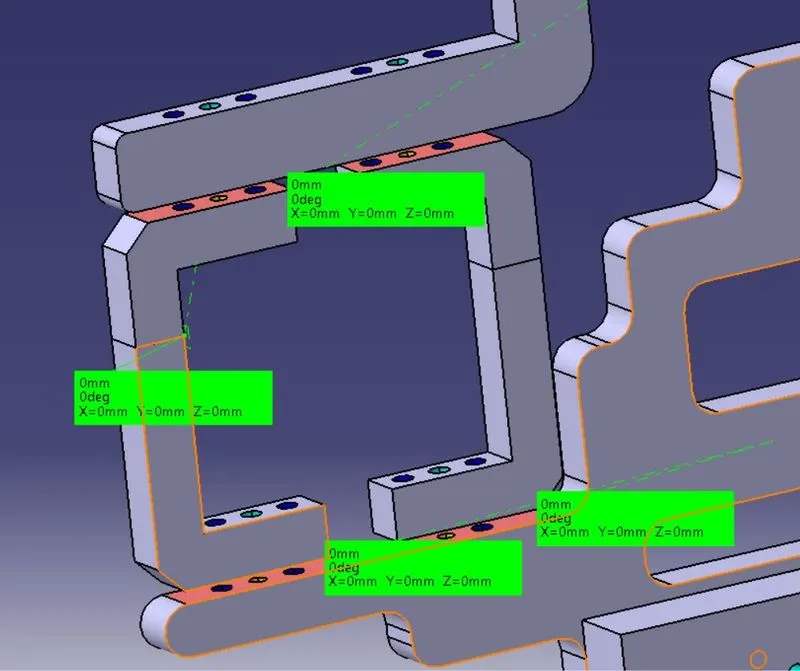
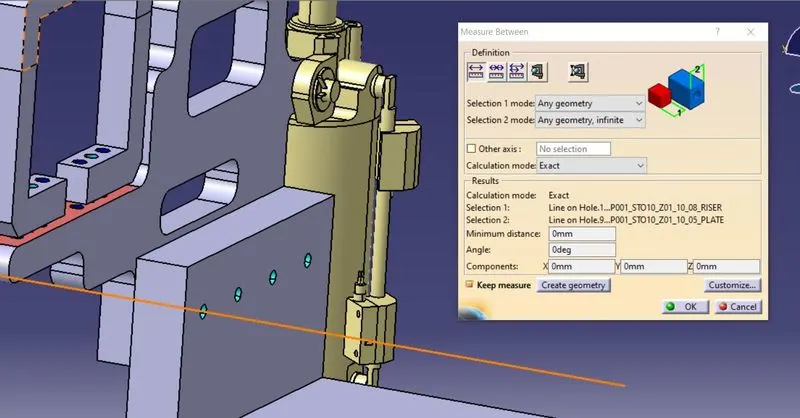
Hole concentricity & hole sizes
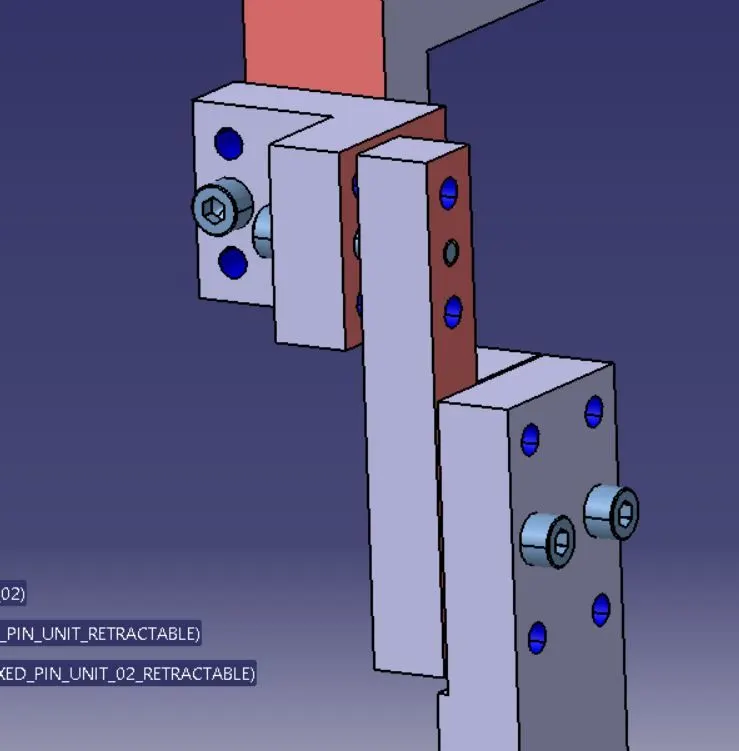
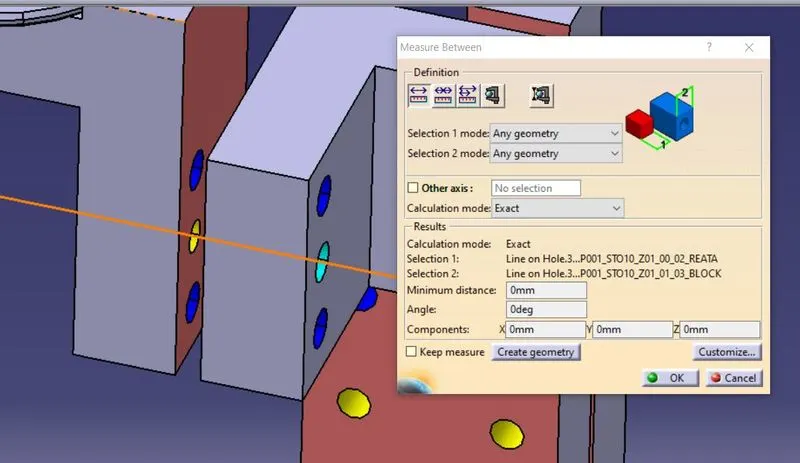
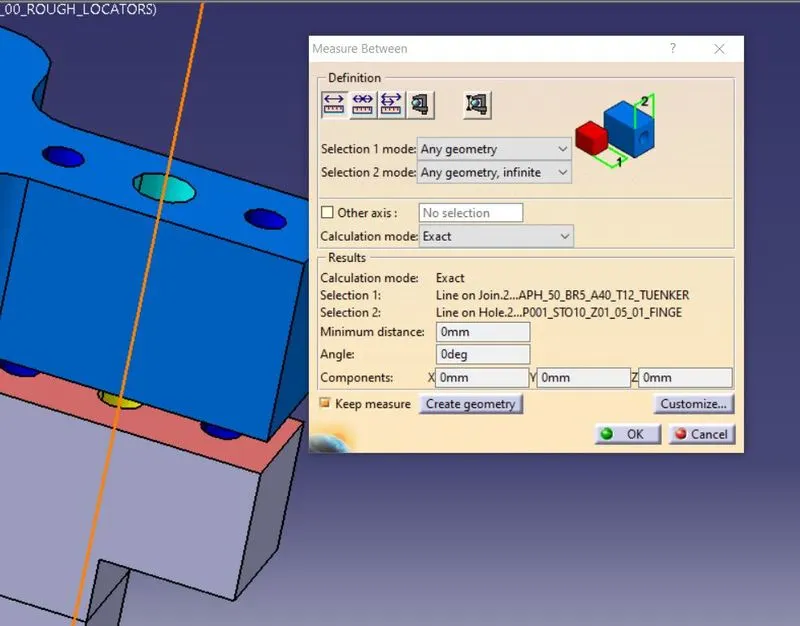
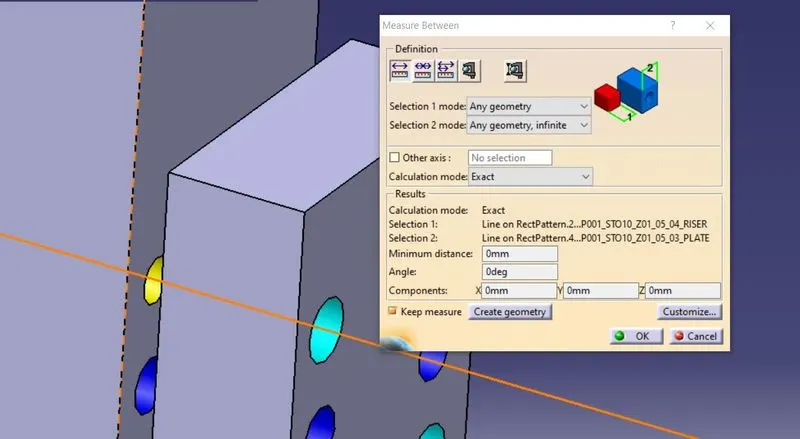
All parts holes concentricity & holes sizes are checked for easy assembly while finishing the parts.
Machining area.
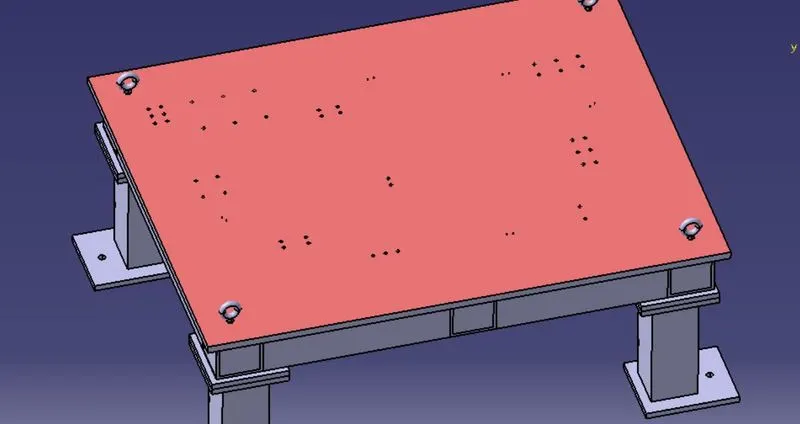
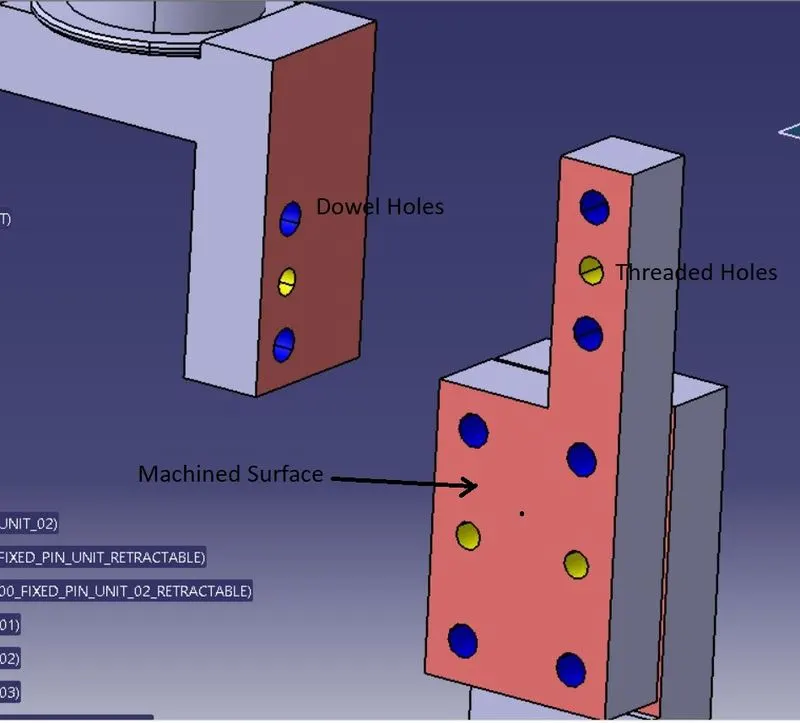
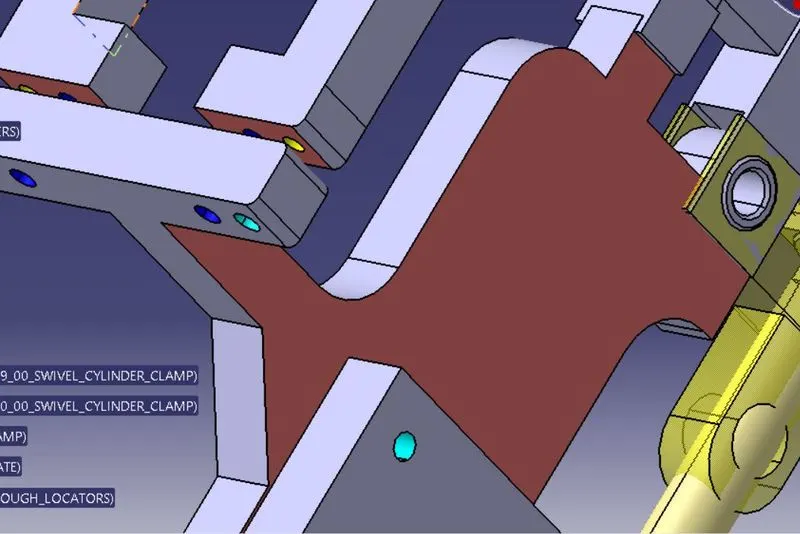
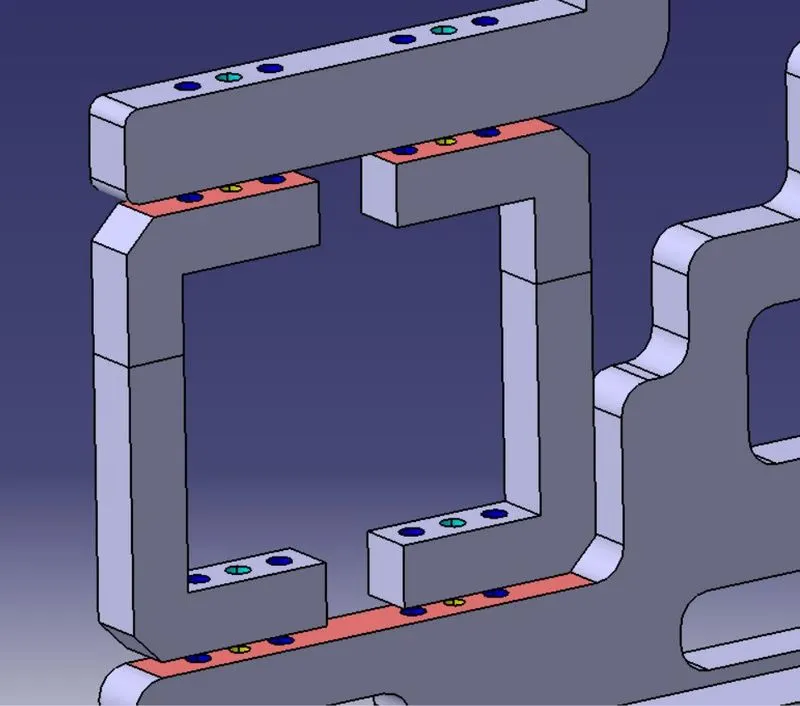
The machining area in every part should be defined & the machining area should be highlighted by using standard color code. Machining is to be done on parts to properly mount with mating parts. Machining only on desired faces reduces cost & saves time also machining increases the accuracy of dimension. So before going to simulation or detailing machining area should be defined.
Nominality
All units dimension should be maintained nominal to facilitate easy assembly of the unit.
Holes coloring standard
In 3D finish holes, coloring should be done because it helps to identify what type of hole it is? It depends on customer standards. The customer specifies colors
Hole coloring standards used in this project :
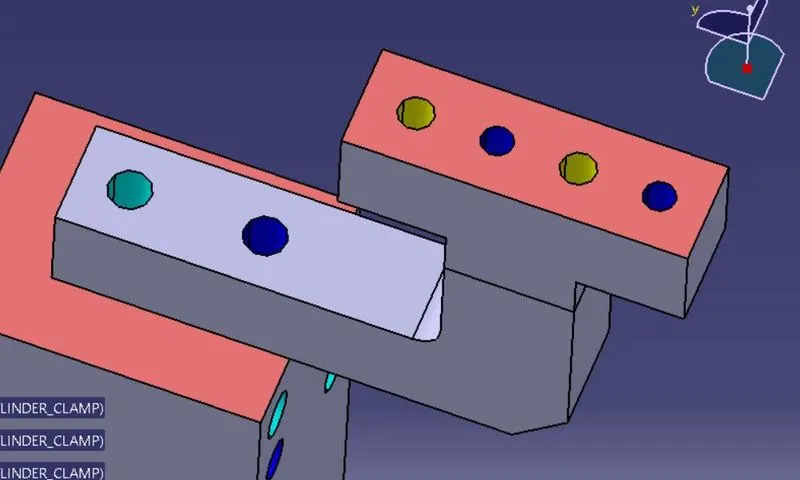
Dowel holes - Blue color.
Threaded holes – Yellow color.
C. bore or simple holes - Cyan green color.
Pneumatic lay-outing
The pneumatic layout is a collection of different pneumatic pipes which work as an inlet to the pneumatic cylinder. It should be done properly for proper functioning of the units.
Gaps checking:
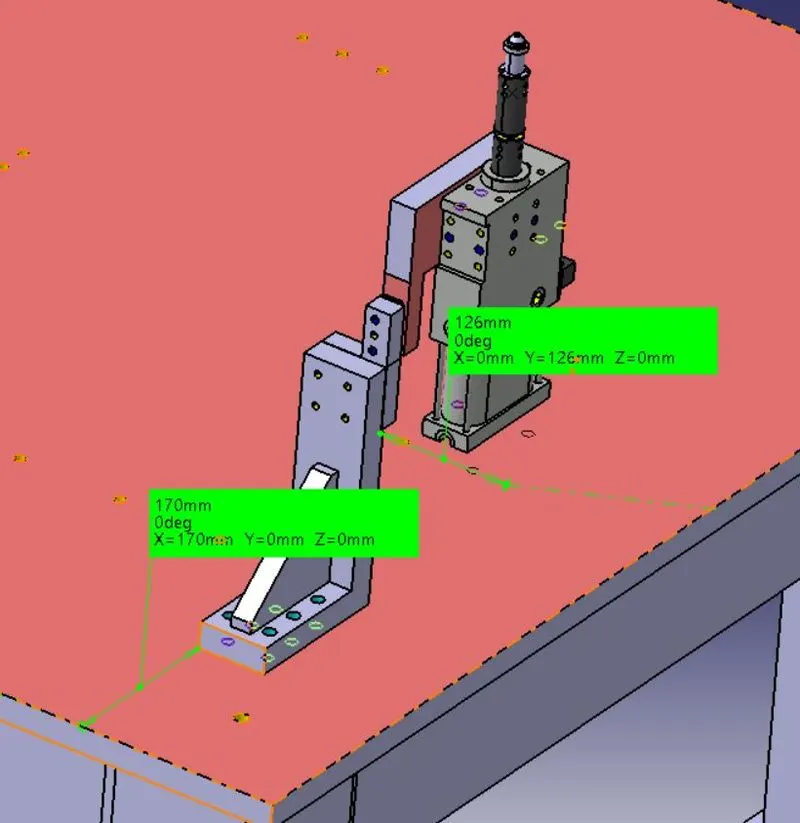
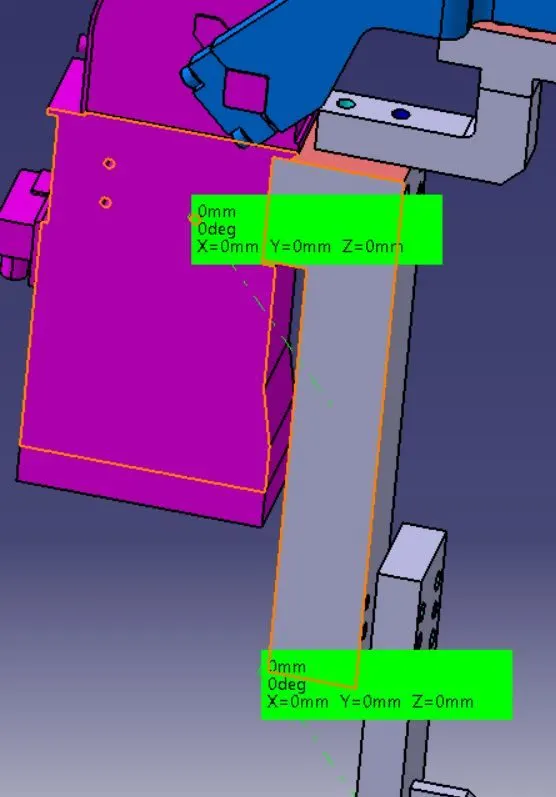
The gaps between the different units were checked to ensure the proper individual working of different units.
Fasteners implementation
Fasteners should be implemented in all units as per the requirement & load on the part
Avoiding clash between different parts
A proper gap should be maintained between units to avoid the clash between the different units.
Mylar splitting as per panel profile
Mylar splitting as per panel profile should be confirmed while finishing the design.
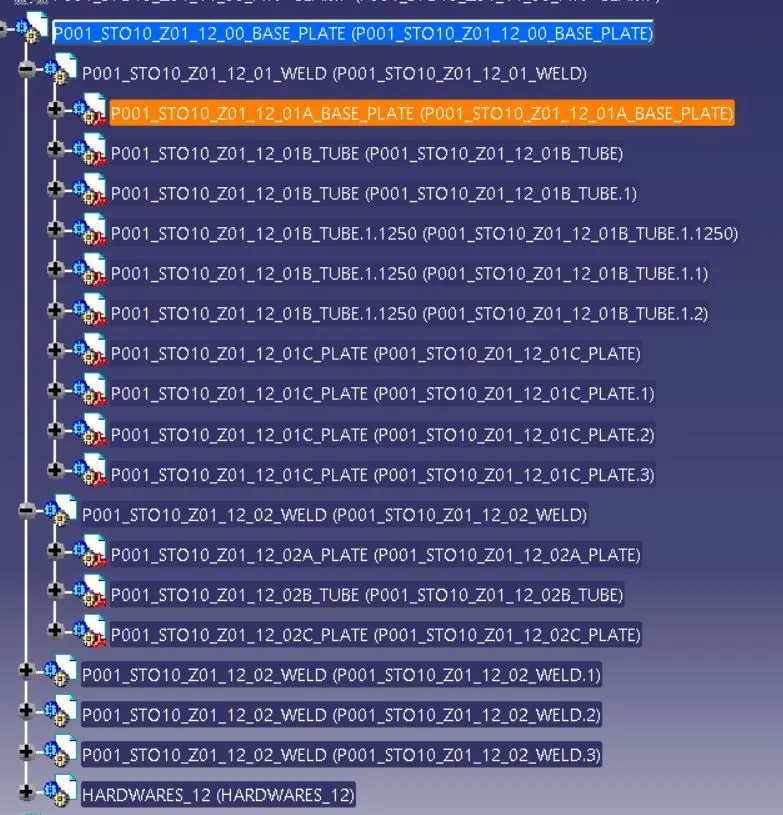
Proper renaming of parts/ assemblies as per the standard
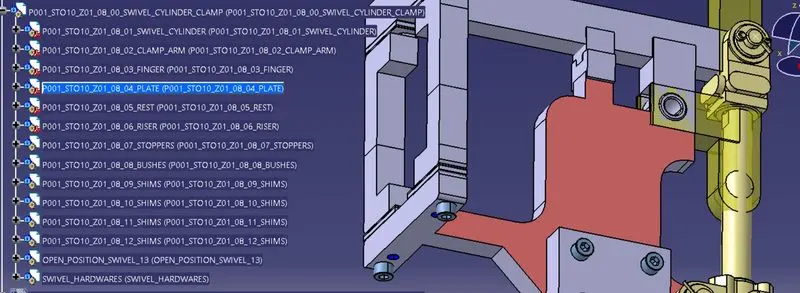
Proper renaming of parts & assemblies should be done while finishing the design hence we can identify each & every part easily with unique identification.
Fixture Assembly:
Structuring the tree:
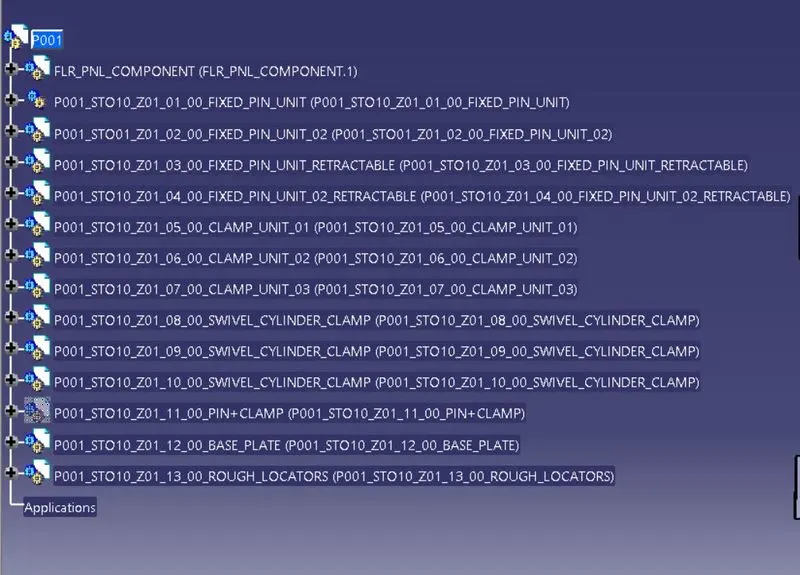
Base Unit(P001_STO10_Z01_12_00_BASE_PLATE)
| Checking parameter | Action |
| Renaming & structuring of the design tree | Checked |
| Nominality of holes | Checked |
| Hole coloring standard | Marked |
| Machined area | Marked |
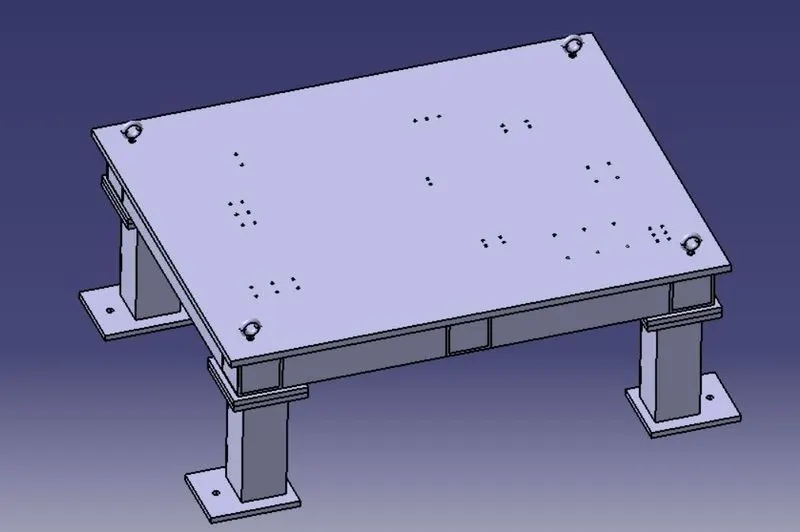
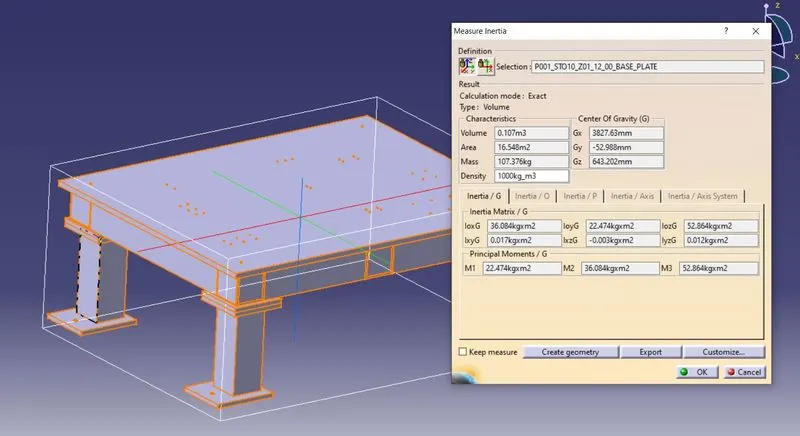
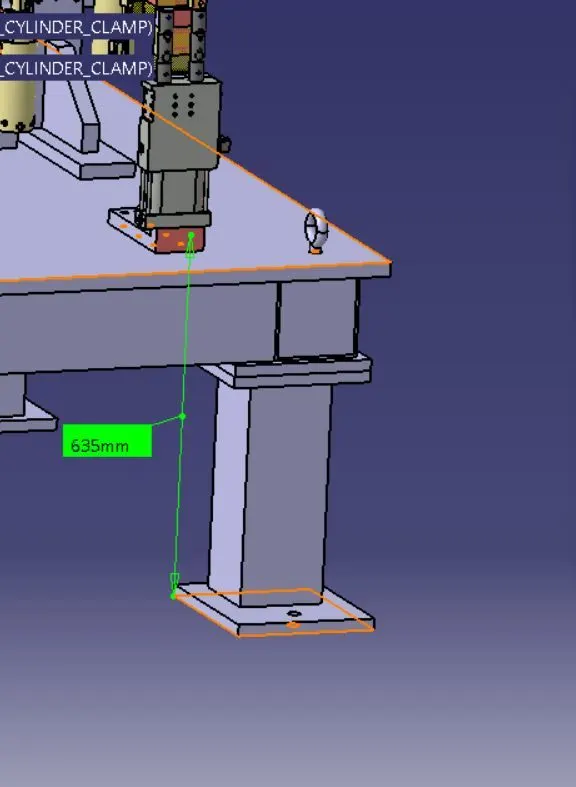
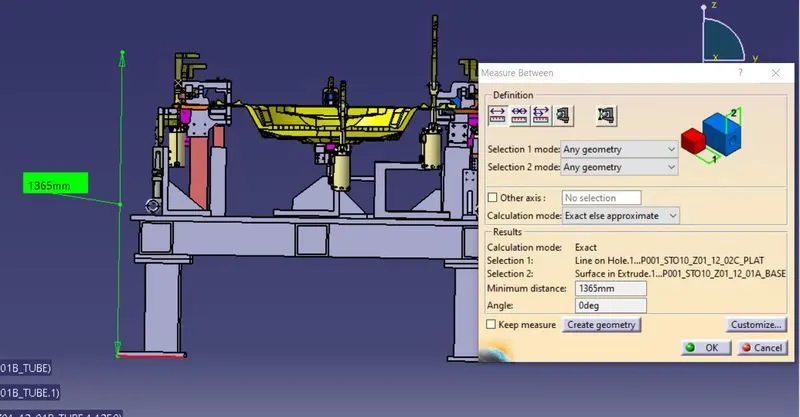
Machined Surface:
Holes Normality:
Hole coloring standard:
Dowel holes - Blue color.
Threaded holes – Yellow color.
C. bore or simple holes - Cyan green color.
Tree Structure:
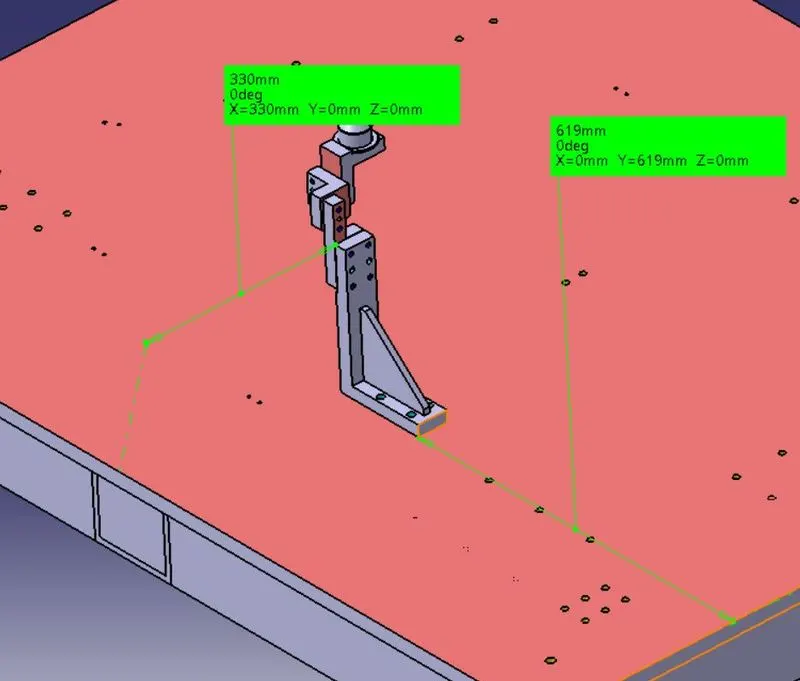
Rough locators(P001_STO10_Z01_13_00_ROUGH_LOCATORS)
Rough locator Design:
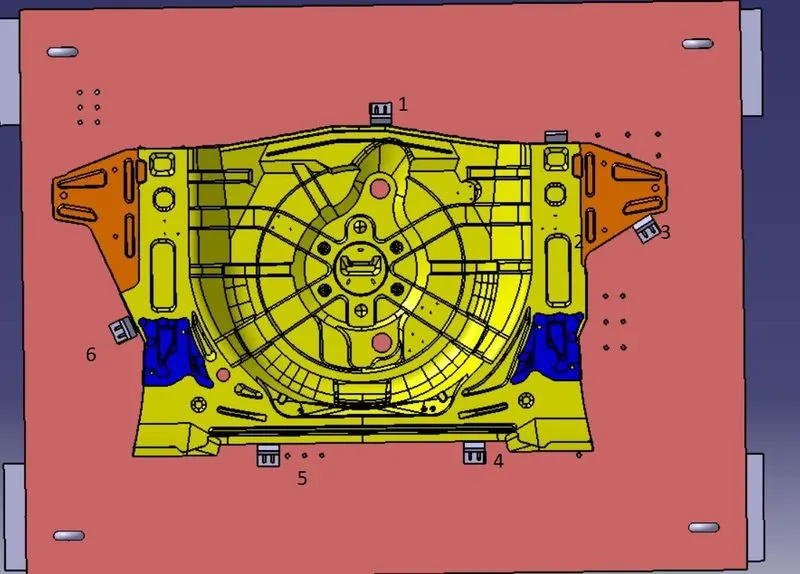
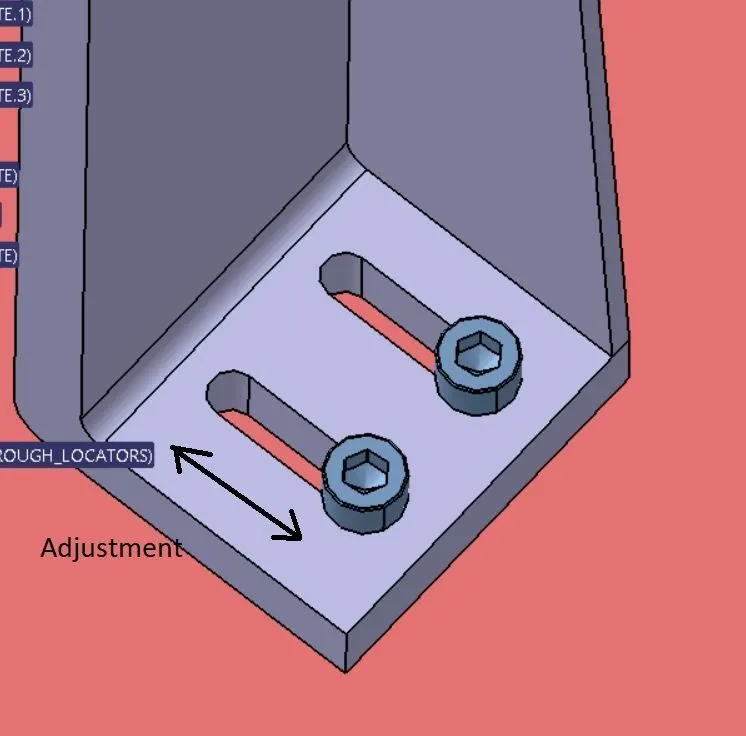
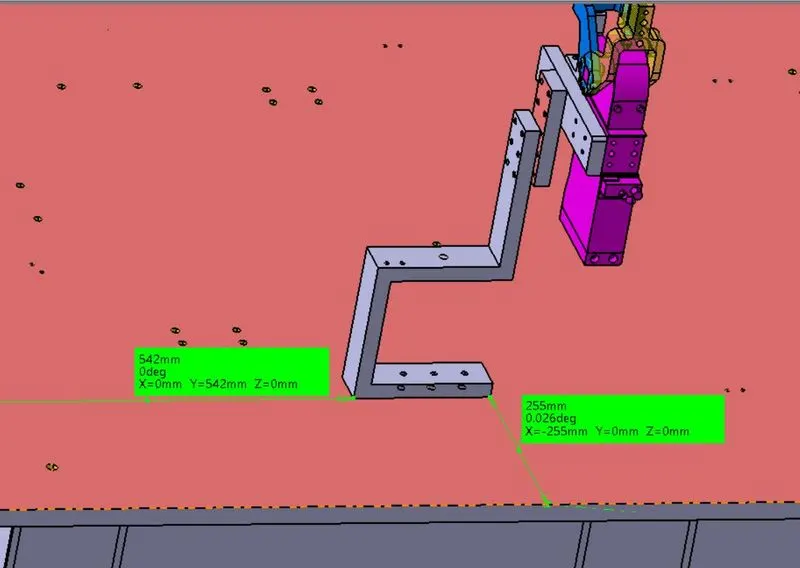
Rough locators are usually used in the loading & unloading of particular parts. The rough locator unit is apart designed to guide the operator to locate the car panel on the pins accordingly. They have a slot for adjustment.
Fundamentals of rough locator design
Rough locators should be placed at the edges of the car panel, which it has to guide using locating pins one can easily restrict movement of the entire car panel.
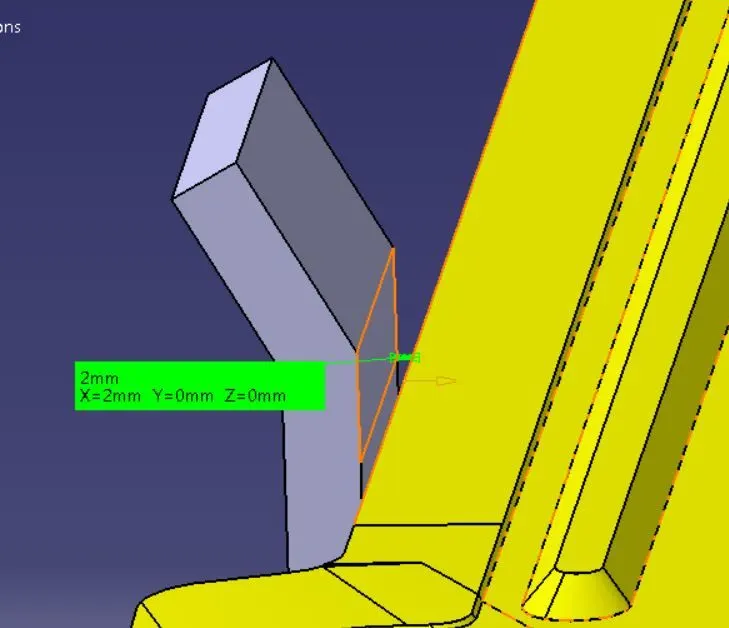
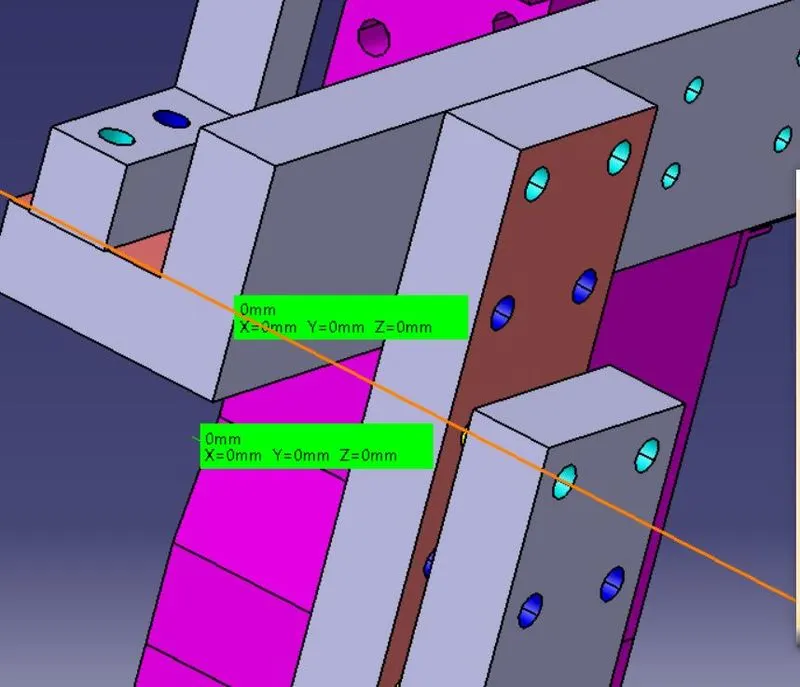
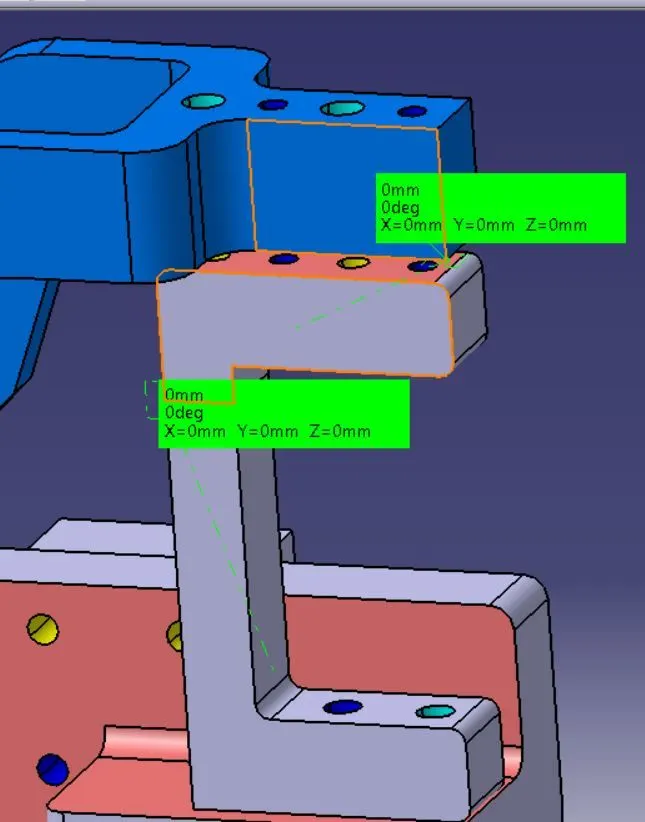
A rough locator has to be placed at the same angle of the car part edge with a minimum distance of 2.5 mm from the edge of the car part, so it should not damage panel.
Rough locators should guide the panel before 10 to 15 mm. to the start of the pin engagement.
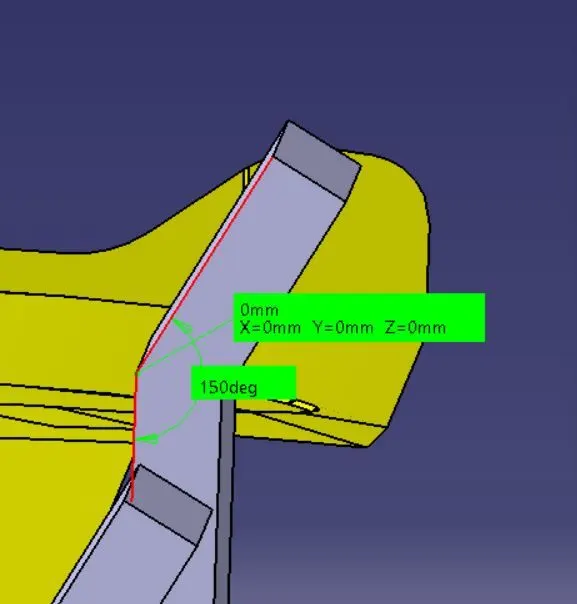
A rough locator should be designed with an entry angle for the car panel. Generally, it ranges between 30-45 degrees.
Rough locators should guide the panel in pin arresting direction in general
Rough locators should be designed with two slots to mount for easy adjustment. (In general). The slot should be in the direction of car panel guiding
Pin Unit (P001_STO10_Z01_01_00_FIXED_PIN_UNIT)
| Checking parameter | Action |
| Renaming & structuring of the design tree | Checked |
| Nominality of holes | Checked |
| Hole coloring standard | Marked |
| Machined area | Marked |
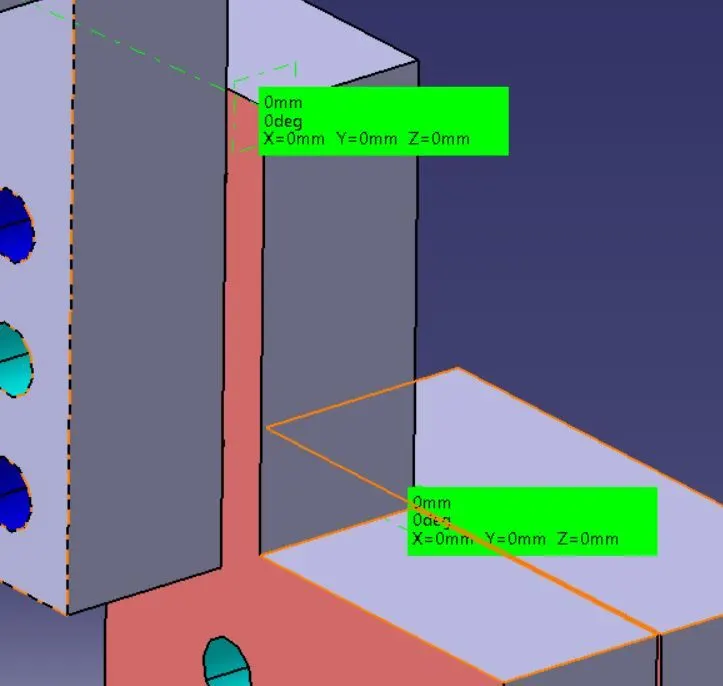
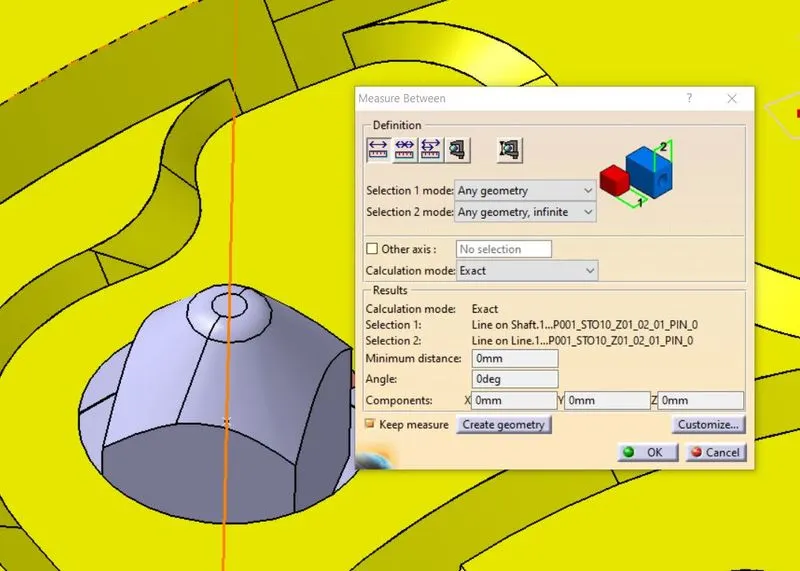
| Concentricity of Holes | Checked |
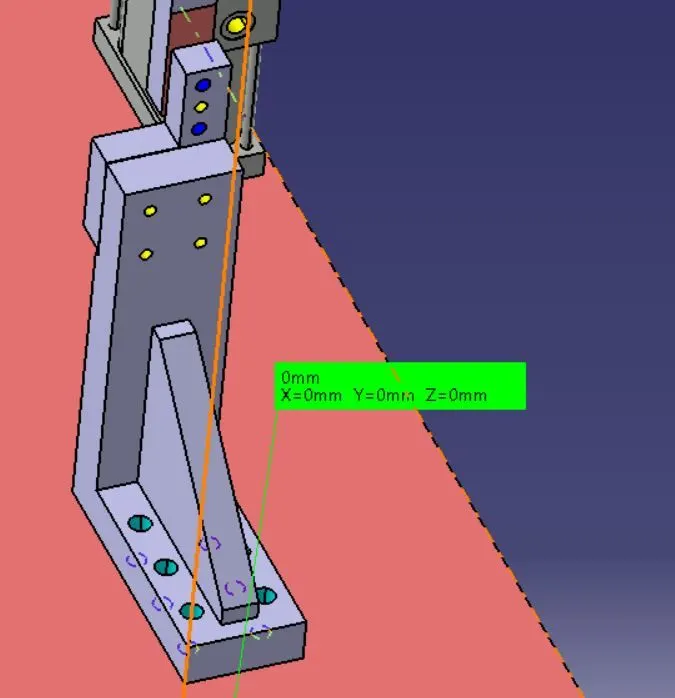
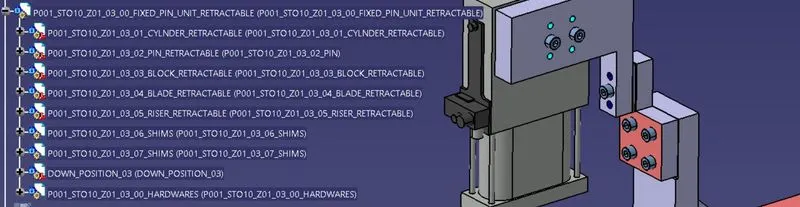
Retractable Pin Unit(P001_STO10_Z01_03_00_FIXED_PIN_UNIT_RETRACTABLE)
| Checking parameter | Action |
| Renaming & structuring of the design tree | Checked |
| Nominality of holes | Checked |
| Hole coloring standard | Marked |
| Machined area | Marked |
| Concentricity of Holes | Checked |
FIXED_PIN_UNIT_02_RETRACTABLE(P001_STO10_Z01_04_00_FIXED_PIN_UNIT_02_RETRACTABLE)
| Checking parameter | Action |
| Renaming & structuring of the design tree | Checked |
| Nominality of holes | Checked |
| Hole coloring standard | Marked |
| Machined area | Marked |
| Concentricity of Holes | Checked |
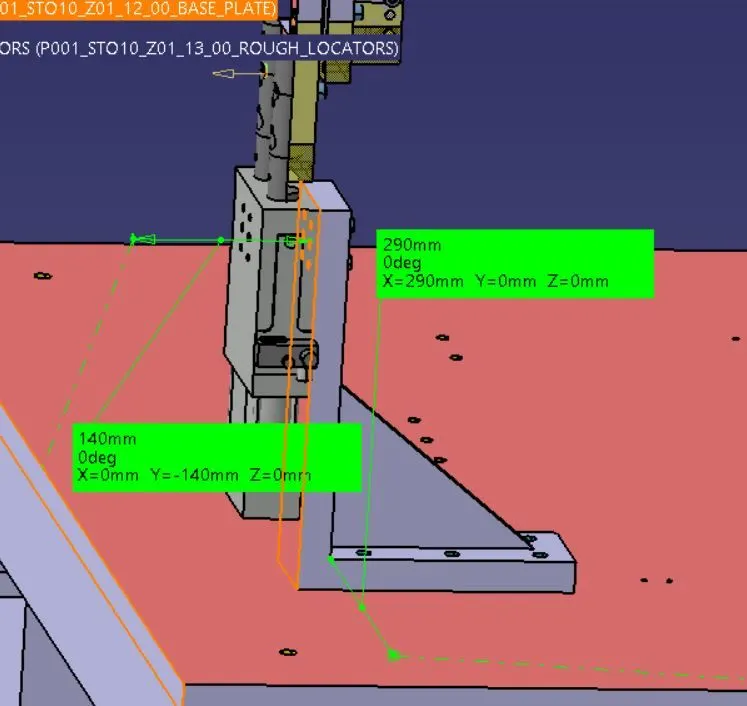
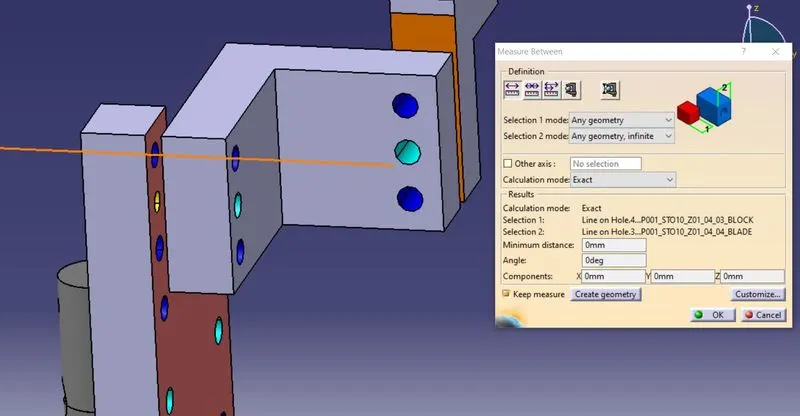
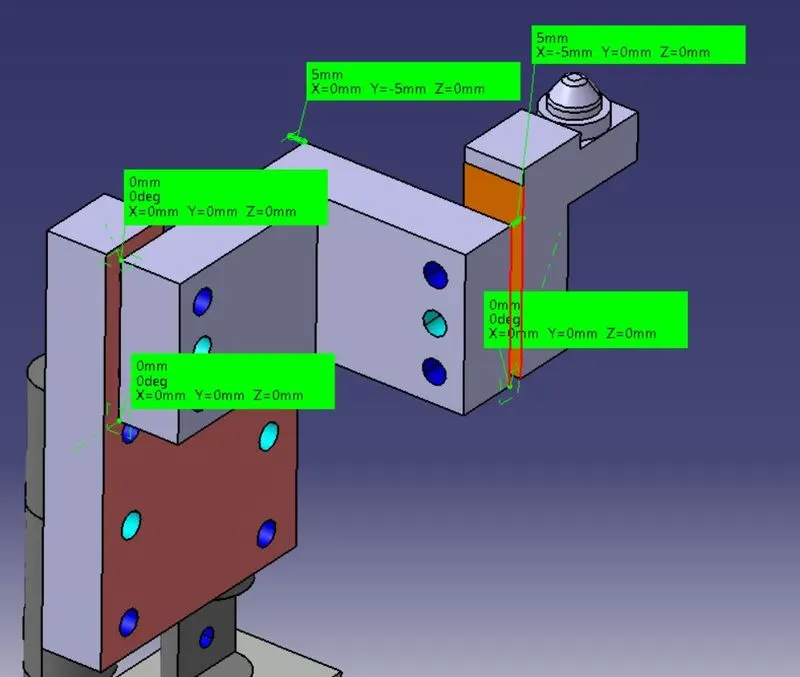
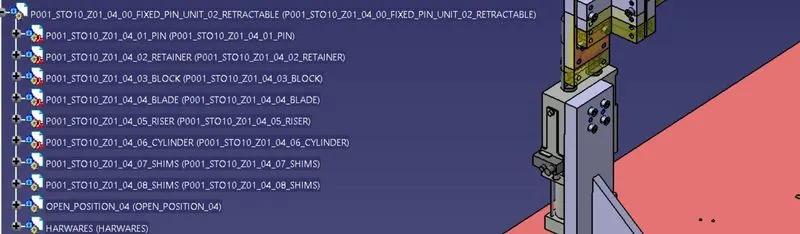
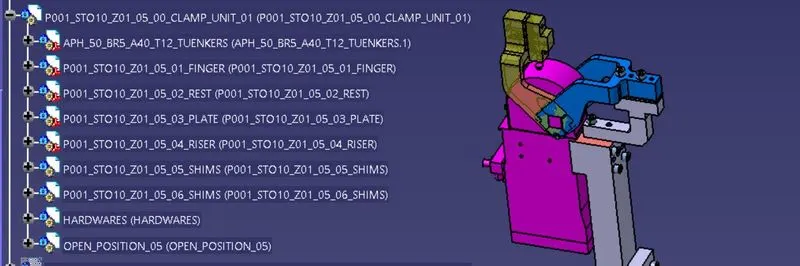
Clamp Unit(P001_STO10_Z01_05_00_CLAMP_UNIT_01)
| Checking parameter | Action |
| Renaming & structuring of the design tree | Checked |
| Nominality of holes | Checked |
| Hole coloring standard | Marked |
| Machined area | Marked |
| Concentricity of Holes | Checked |
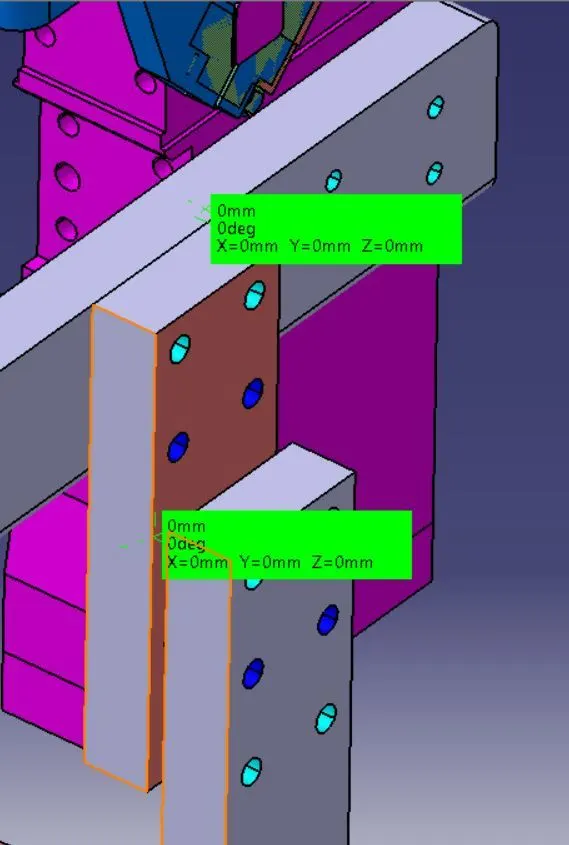
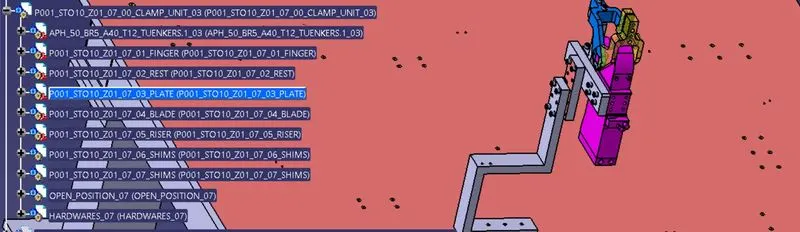
CLAMP_UNIT_03(P001_STO10_Z01_07_00_CLAMP_UNIT_03)
| Checking parameter | Action |
| Renaming & structuring of the design tree | Checked |
| Nominality of holes | Checked |
| Hole coloring standard | Marked |
| Machined area | Marked |
| Concentricity of Holes | Checked |
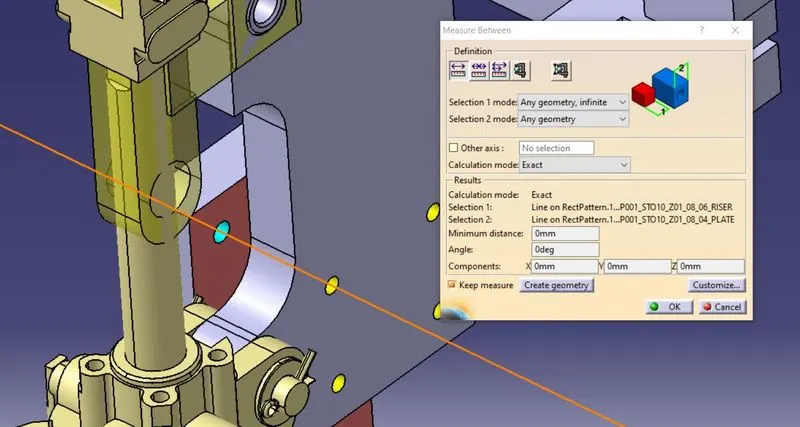
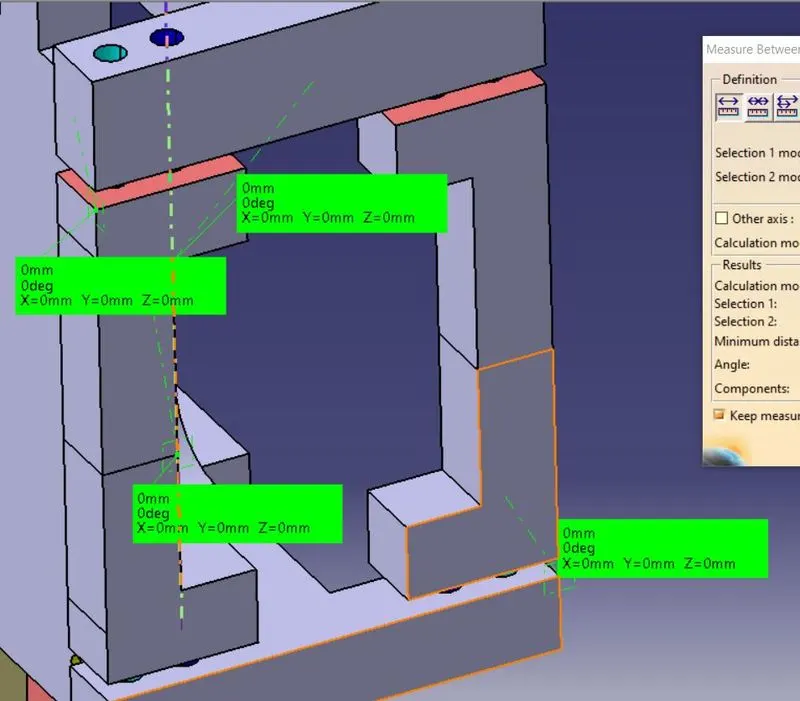
SWIVEL_CYLINDER_CLAMP(P001_STO10_Z01_08_00_SWIVEL_CYLINDER_CLAMP)
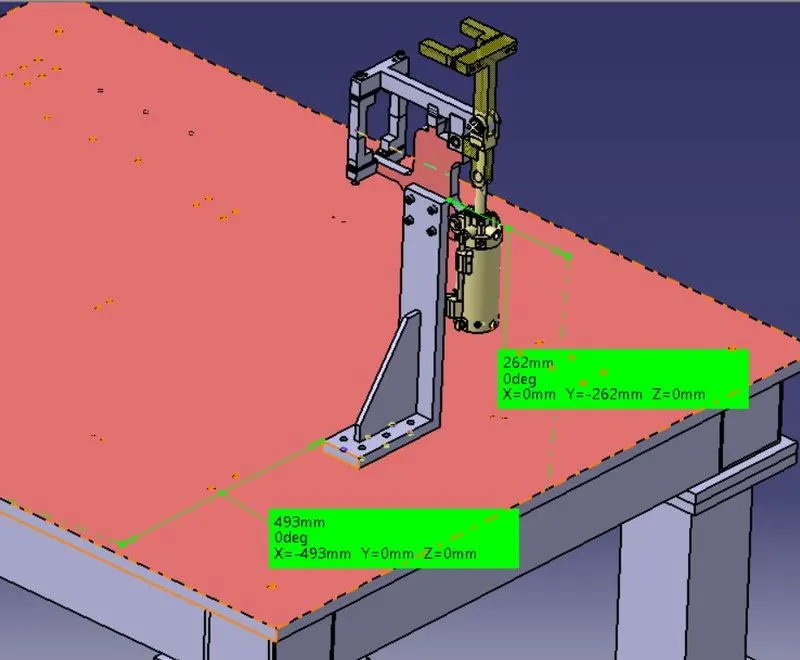
| Checking parameter | Action |
| Renaming & structuring of the design tree | Checked |
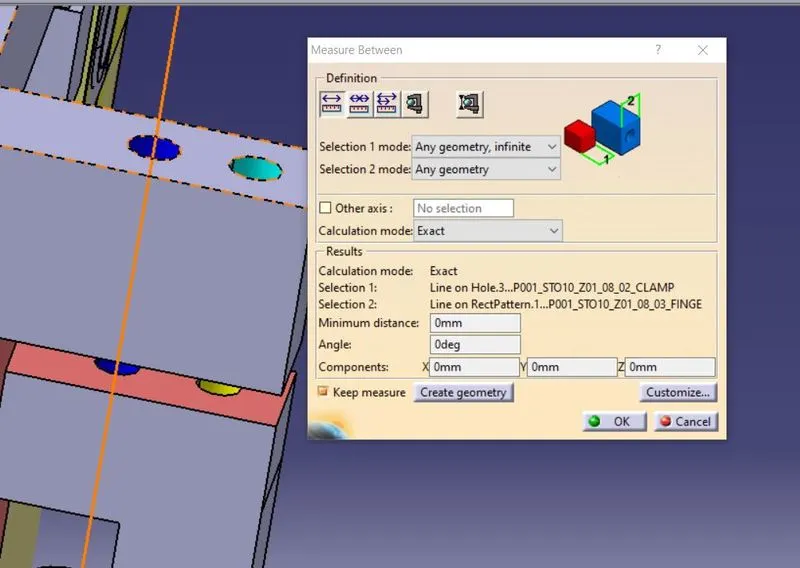
| Nominality of holes | Checked |
| Hole coloring standard | Marked |
| Machined area | Marked |
| Concentricity of Holes | Checked |
SWIVEL_CYLINDER_CLAMP 02 (P001_STO10_Z01_10_00_SWIVEL_CYLINDER_CLAMP)
| Checking parameter | Action |
| Renaming & structuring of the design tree | Checked |
| Nominality of holes | Checked |
| Hole coloring standard | Marked |
| Machined area | Marked |
| Concentricity of Holes | Checked |
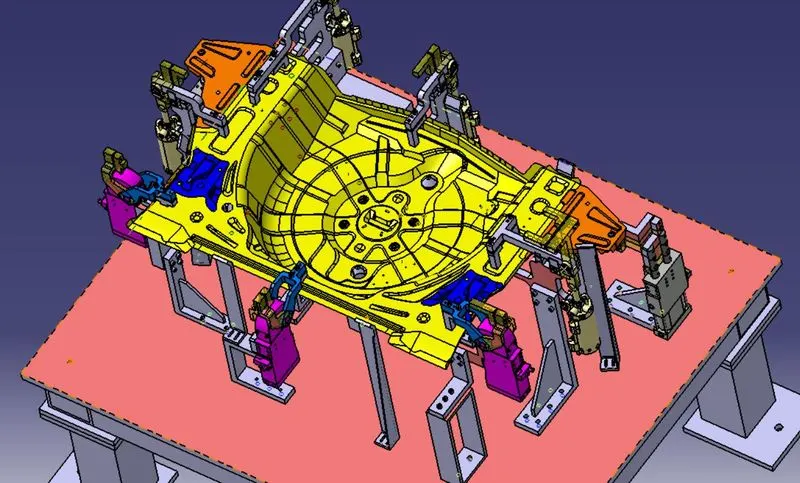
Final assembly:
Conclusion:
Design of rough locators for the Fixture, and perform 3D finish for all the Units (including Pin Units) is carried out successfully.