Design of a Base Unit for Fixture
DESIGN OF BASE UNIT OF A FIXTURE
OBJECTIVE: To design a Base unit with all weldments for the given car panel.
ABSTRACT: In automotive industry, a lot of processes are followed to make a single panel and further operations are performed on that panel and other panels to get an automobile. The role of BIW fixture design engineer is to make fixtures for the panels so that they can be worked on. A fixture is a work holding device that holds support and locates the work piece in a desired position to perform any operation. For automotive industry, a fixture is an assembly of different units like rest pin units, fixed pin units, retractable pin units, Clamp unit, rough locator units, sensor units, base unit etc. In this project I have focused on designing the base unit for the given car pane with necessary design considerations. In addition, I have carried over the previously designed unit for the same panel here. This report contains basic definition and explanation of the fixture, units its parts and process followed to design the base unit.
SOFTWARE USED: CATIA V5
INTRODUCTION:
FIXTURE: A fixture is a work holding device that holds support and locates the work piece in a desired position to perform any operation. Thus the main purpose of the fixture is to hold and support the work piece during machining operation and to provide repeatability, accuracy and interchangeability in the manufacturing of the products.
A BIW fixture is an assembly of units. A unit is a device which has unique function and is a component of a fixture. Components of units differ from unit to unit. In general a BIW fixture consists of following units:
- Pin unit
- Clamp unit
- Rest unit
- Rough locator unit
- Sensor unit
- Base unit
The ultimate aim of a fixture is to hold the work piece and prevent its movement. This is achieved by 3-2-1 principle which states that the six locators are sufficient to restrict the required degree of freedom of any work piece. In this, motion is restricted using clamps and locators. A three-pin base can restrict five motions and six pins restrict nine motions. Let us understand 3-2-1 principle in detail.
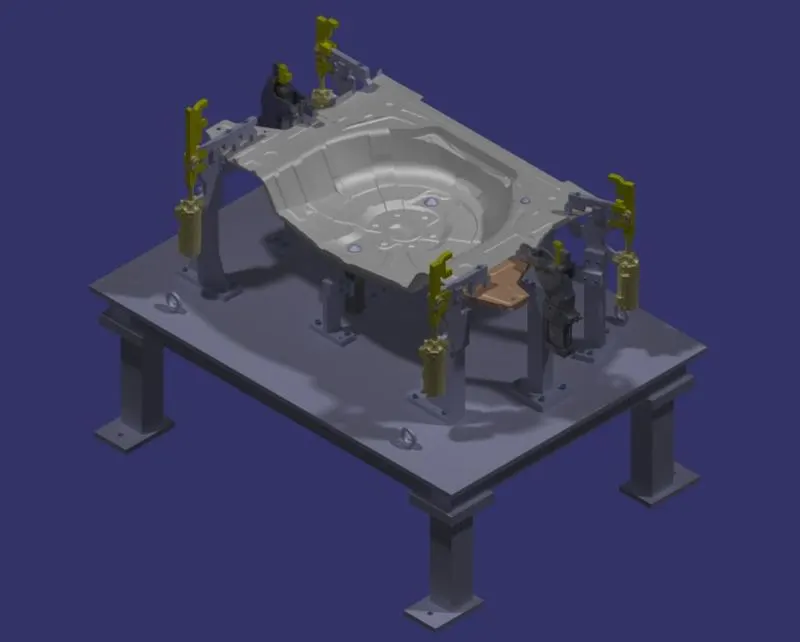
FIG. FIXTURE DESIGNED FOR THE PROJECT
When any work piece is not clamped or held, it can move or rotate in any direction and along any axis. We can list its movements as:
- Translational motion along x-axis.
- Translational motion along y-axis.
- Translational motion along z-axis.
- Rotational motion along x-axis.
- Rotational motion along y-axis.
- Rotational motion along y-axis.
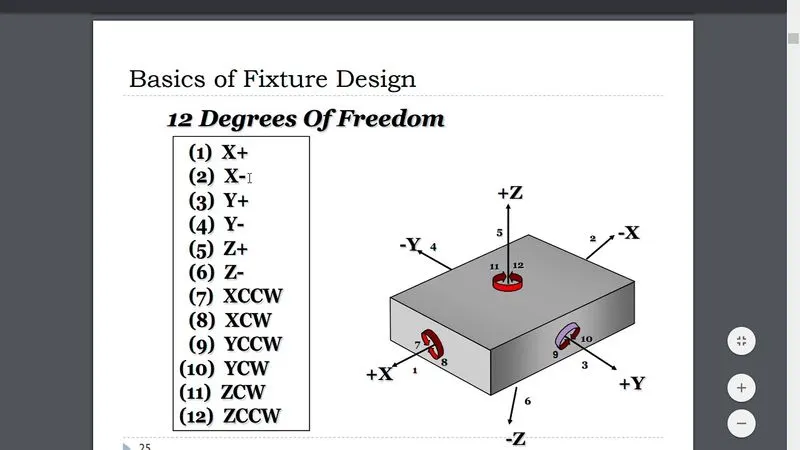
FIG. DEGREES OF FREEDOM
These are not just 6 but 12 as its motion will be along positive and negative directions and along clockwise and counter clockwise direction. But if we were to perform any operation on that work piece we must restrict the movements in order to perform the task without any mistakes. This can be achieved by 3-2-1 principle. In 3-2-1 principle we make use of locating pins in the given order to fix it on a fixture:
- 3 pins are located on the bottom side of the component. These pins constrain the translational motion of the body in z direction and rotational motion along x-axis and y-axis. Thus 3 degrees are restricted. But the body still can rotate along z-axis and translate in x-axis and y-axis.
- 2 pins are located on the back side of the component. These pins constrain the translational motion along x-axis and rotational motion along z-axis. Thus we have constrained 5 degrees in total. But translation along y-axis is still possible.
- 1 pin located on the adjacent side of the 2 pins we can constrain the last degree that is translation along y-axis.
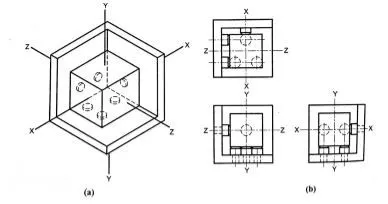
FIG. LOCATING PINS
Thus, a fixture locates the work piece with the help of its various units, Pin unit and clamp unit in general. All the degrees of freedom are restricted using these two units. In clamp unit, we use clamping Mylar and Rest Mylar to locate the panel. Here we are doing following things:
- Restricting the upward and downward motion that is movement along z-axis.
- Restricting clockwise and counter clockwise rotation along x-axis.
- Restricting clockwise and counter clockwise rotation along y-axis.
Thus out of 6, we are restricting 3 degrees of freedom when we clamp the panel. Similarly, when we locate the panel with locating pins we:
- Restrict the translational movement along x-axis.
- Restrict the translational movement along y-axis.
- Restrict the rotational movement along x-axis.
- Restrict the rotational movement along y-axis.
PIN UNIT: As the name suggests, these units have a pin which are used to locate the work piece. During the entire course of study I have designed two types of pin unit which are fixed pin unit and retractable pin unit.
Fixed pin unit: This type of pin unit does not have freedom to move as it an assembly of rigid structures. It consists of following parts:
- Locating pin
- Pin retainer
- L block
- Two way shim packs
- Blade
- Riser
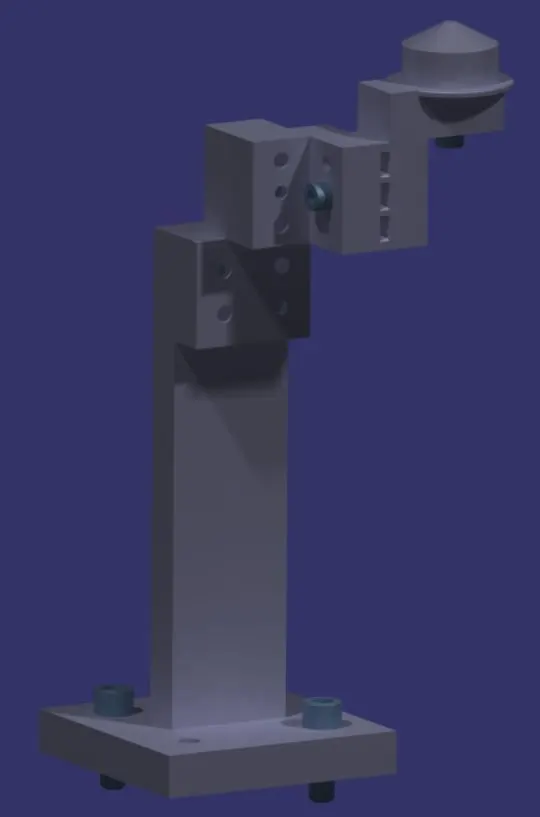
FIG. FIXED PIN UNIT DESIGNED FOR THE PROJECT
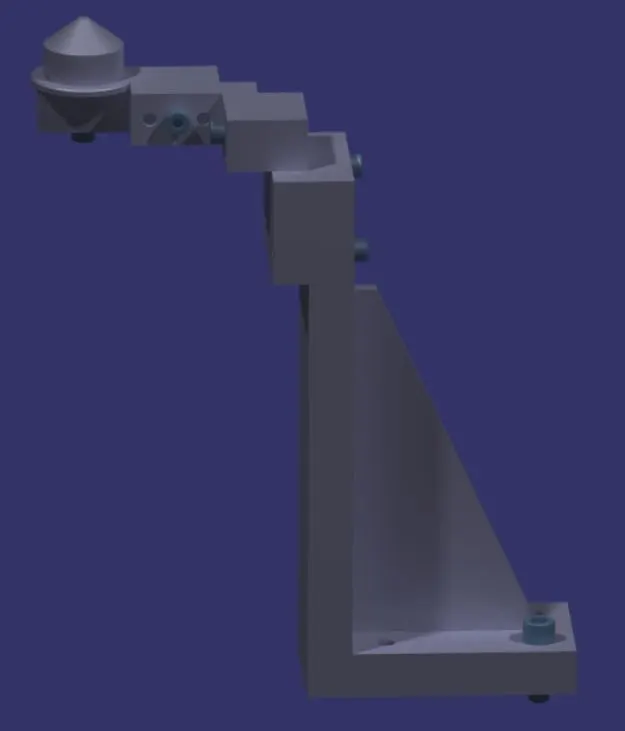
FIG. FIXED PIN UNIT DESIGNED FOR THE PROJECT
Retractable pin unit: This type of unit has the freedom to move up and down as the combination of locating pin, pin retainer, L block or locating pin alone or locating pin and pin retainer is mounted on the retractable cylinder. It consists of the following parts:
- Locating pin
- Pin retainer (Optional)
- L block
- Two way shimming
- Blade (Optional)
- Retractable cylinder
- Riser
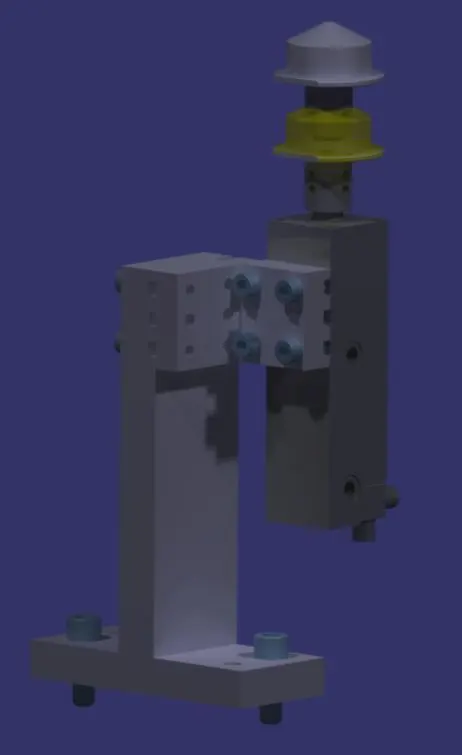
FIG. RETRACTABLE PIN UNIT DESIGNED FOR THE PROJECT
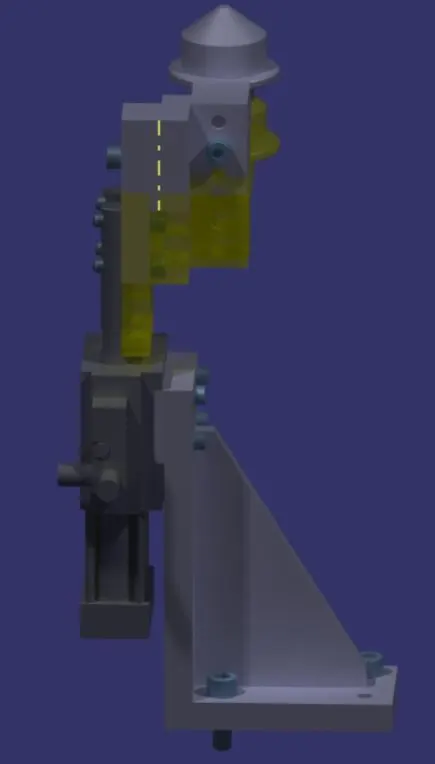
FIG. RETRACTABLE PIN UNIT DESIGNED FOR THE PROJECT
REST UNIT: The sole purpose of these types of units is to let the panel rest on it. It does not use any clamping force or any other force to fix the panel on it. This is a simple unit and can be combined with other units like pin units and clamp units. It consists of following parts:
- Rest Mylar (NC block)
- Shim pack
- Blade
- Riser
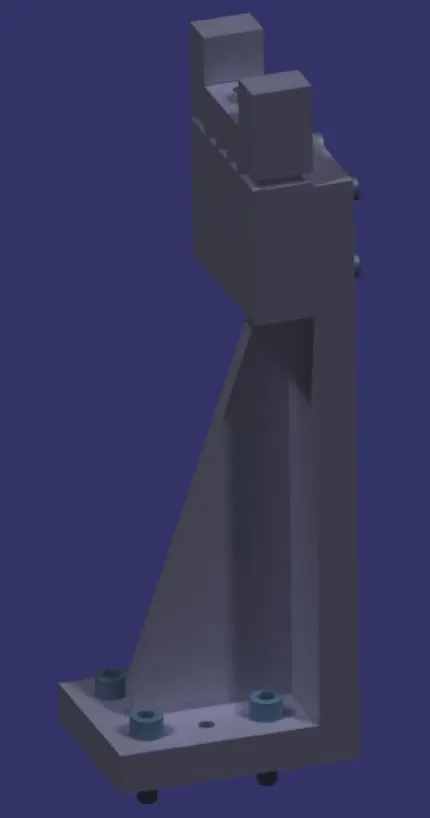
FIG. REST UNIT DESIGNED FOR THE PROJECT
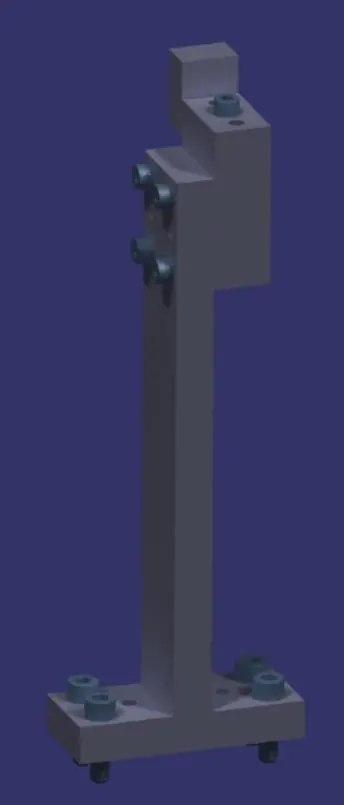
FIG. REST UNIT DESIGNED FOR THE PROJECT
CLAMP UNIT: A clamp unit is used to hold the panel at desired location and prevent it from unnecessary movements. A clamp plan is provided by the customer, which helps us to design the clamp unit as it consists of the location of clamping. In the course of study I have designed powered clamp unit, swivel clamp unit and pin-clamp unit. The purpose of all the clamp units is same they just differ in the parts used.
Powered clamp unit: This type of unit uses pneumatic powered cylinder. It consists of following parts:
- NC blocks
- Clamp arm (Standard)
- Pneumatic clamp cylinder
- Shim pack
- Blade (Optional)
- Riser
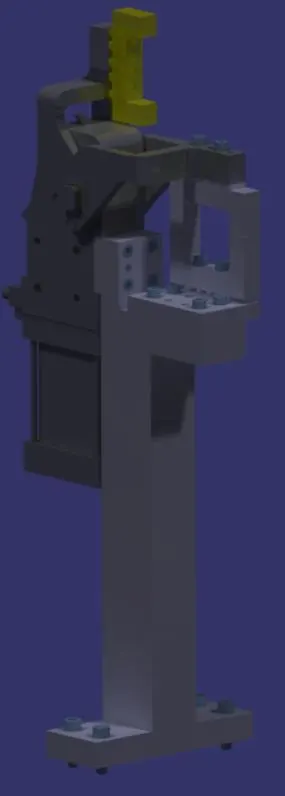
FIG. POWERED CLAMP UNIT DESIGNED FOR THE PROJECT
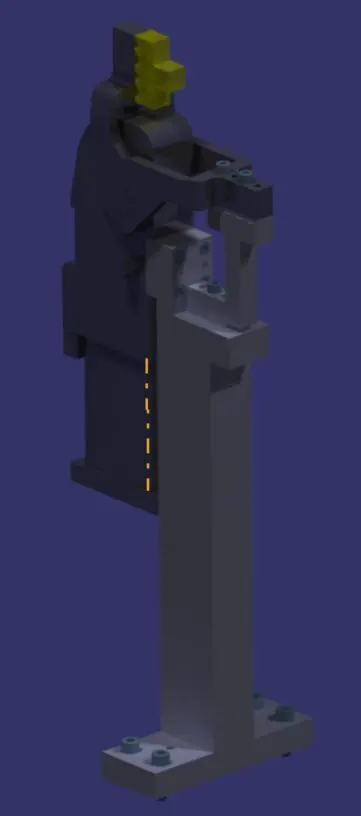
FIG. POWERED CLAMP UNIT DESIGNED FOR THE PROJECT
Swivel Clamp unit: This type of unit uses swivel cylinder. It consists of following parts:
- NC blocks
- Clamp arm (Make part)
- Swivel cylinder
- Blade
- Stopper
- Weld plates
- Shim pack
- Riser
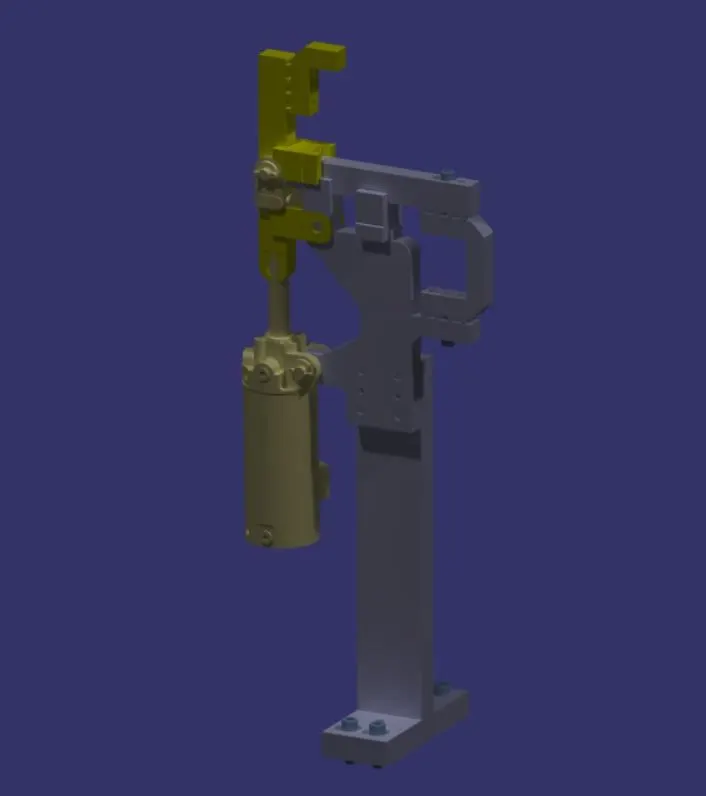
FIG. SWIVEL CLAMP UNIT DESIGNED FOR THE PROJECT
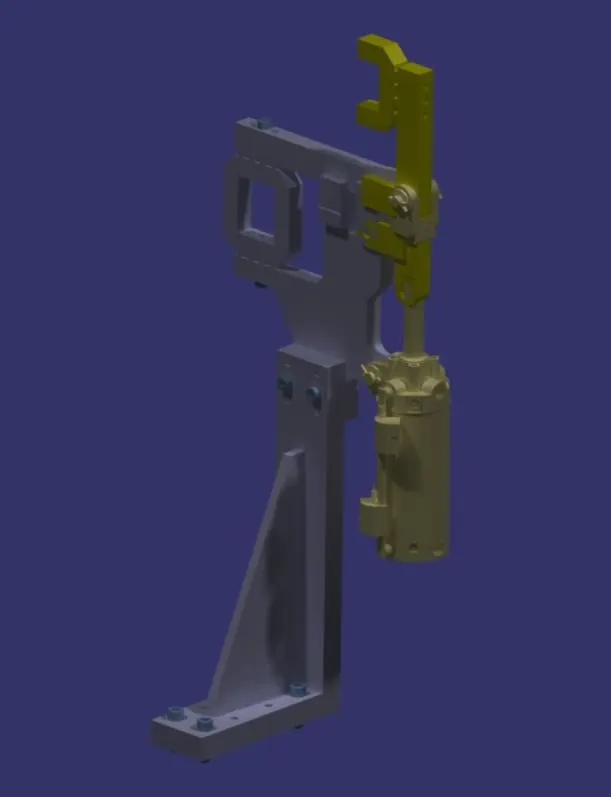
FIG. SWIVEL CLAMP UNIT DESIGNED FOR THE PROJECT
Pin-Clamp unit: This unit is just a combination of pin unit and clamp unit. This can have various combinations. I have designed fixed pin unit with swivel cylinder. It consists of following parts:
- Locating pin
- Pin retainer
- L block
- Blade (Different for pin unit and Clamp unit)
- Shim packs
- NC blocks
- Clamp arm (Make part)
- Swivel cylinder
- Weld plates
- Stopper
- Riser
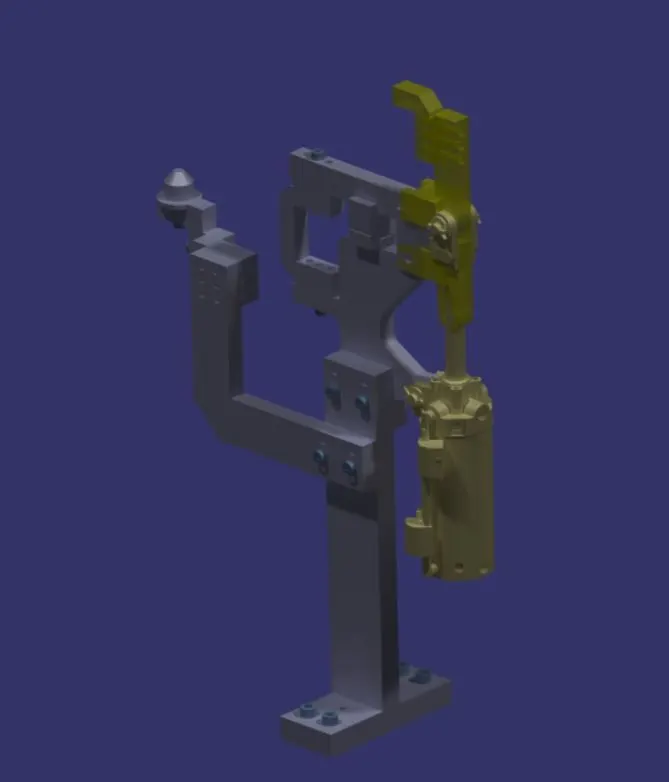
FIG. PIN-CLAMP UNIT DESIGNED FOR THE PROJECT
BASE UNIT: Base unit is the unit of the fixture which is designed as such so that other units of the fixture can be mounted on it. Apart from these units, other necessary tools like pneumatic valve box, trunking cable path will also be mounted on the base unit. It consists of following parts:
- Base plate
- Pedestal
- Trunking channel
- Valve box
- Eye bolt
- Floor plate
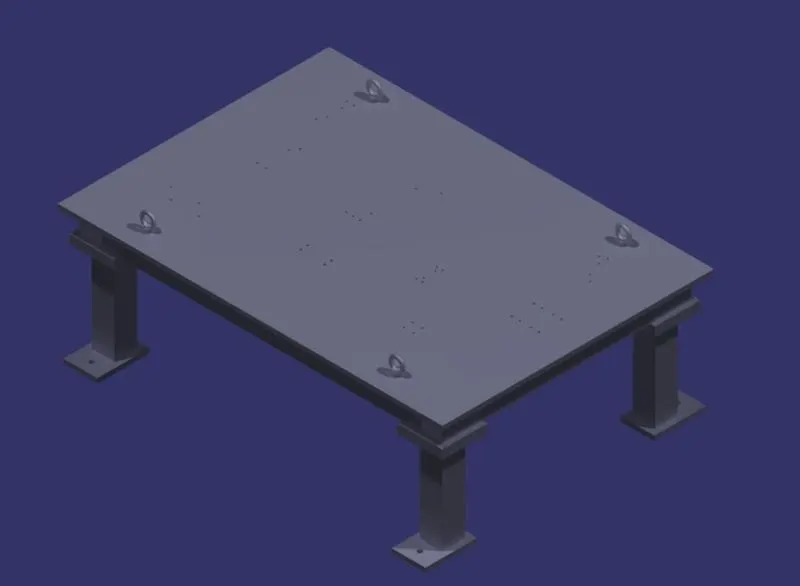
FIG. BASE UNIT DESIGNED FOR THE PROJECT
WELD STUDY: Weld study is provided by the customer beforehand to convey the information such as the type of weld gun to be used, location of weld matrix and weld points. Type of weld gun used for the operation depends on the size and the thickness of the part. As the customer has already decided these things so it is easy for him to do this study and provide us the data so that we can make use of this for designing purposes. Weld location and weld matrix has data of geo spot and weld spots. This data tells us exactly where and which type of weld will be applied. It shows the geo spots and re-spots with spheres with different colors.
CLAMP PLAN: The customer provides the clamp plan which consists of the position of the clamp, pins, rests and dump etc. It has the exact coordinates of these components and in addition it also has the hole’s dimensions and tolerances. As this is a critical input data, it must not be modified on own. In case the spot for weld and the clamp position is nearby and it may create problem later and there is need to change the position of the clamp, the same must be done so with the permission of the customer as it will be easy for the customer to make changes from his side also.
ABOUT THE COMPONENTS USED IN THE UNITS
Locating pin: They are used for controlled, fine tolerance positioning of a work piece. For example, a pallet that is moved along one axis, where the drive mechanism is not accurate and stable enough to place it in a position sufficiently accurate to execute a particular process, the use of locating pins may be the best solution. Usually two locating pins are enough to properly locate the work piece on one plane. We should also consider the following points while choosing the locating pins:
- Pin should engage 3-5mm from car part entry surface.
- All pins should be accommodated with 2-way adjustable shims irrespective of direction of arresting.
- Round pins should be used in case of 4-way arresting of car part if the hole is round.
- Round pins can be used in 2-way arresting of car part if the hole is slotted.
- Diamond pins should be used in case of 4-way arresting of car part if the hole is slotted.
- Diamond pins can be used in 2-way arresting of car part if the hole is round.
The Diamond Shape is a critical feature that helps with machining inaccuracies and smoother locating operation. When two round head pins are installed onto one plate, the distance between two mounting holes must be extremely precise and even then, the work piece will not be placed on the base as easily as it would with the use of a diamond shape pin.
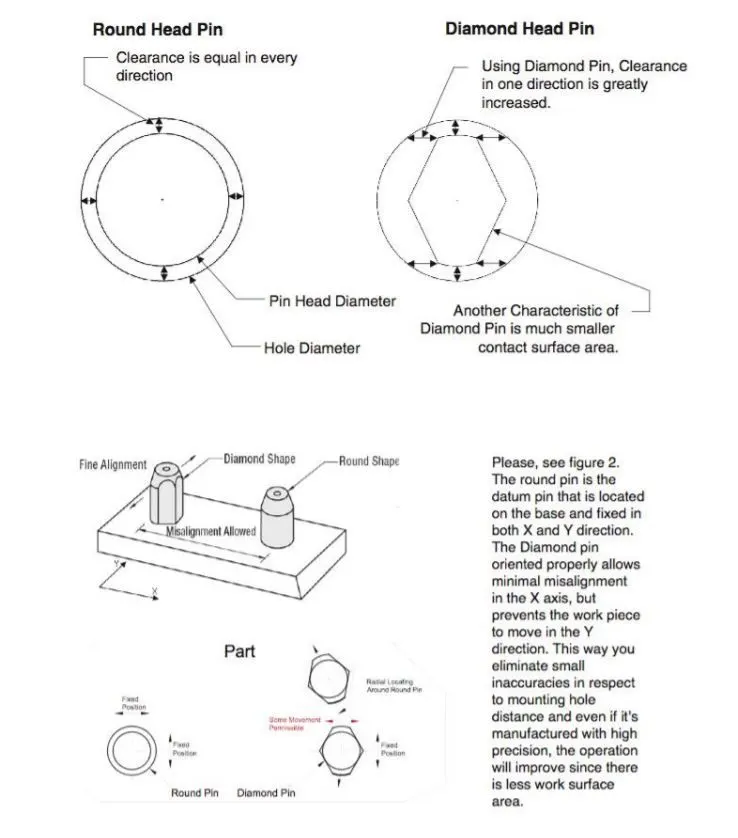
FIG. DIAMOND HEAD AND ROUND HEAD PIN
Typically, locating pins are manufactured from hardened tool steel such as O1 heat treated to 60-63Rc or from case hardened carbon steel (1045 with 45-50Rc). In some cases, soft 300 series or hardened 400 stainless is used in assemblies where no rust is accepted. Please, remember that pins made out of soft materials will wear out much faster than harden pins.
There is a variety of coatings that can be chosen based on your application. In corrosive environments, a hard chrome, Dicoat or TiCN coatings can help extend the life of the pin since they provide non-corrosive and hard layer that can be as hard as 3000 Vickers. A variety of insulating coatings or materials can be used in case of welding applications. KCF stainless steel coat is one surface treatment that provides great insulation and prevents weld build-up between the work piece and the surface of the pin.
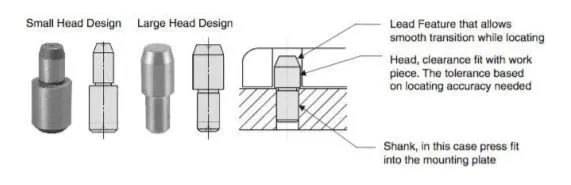
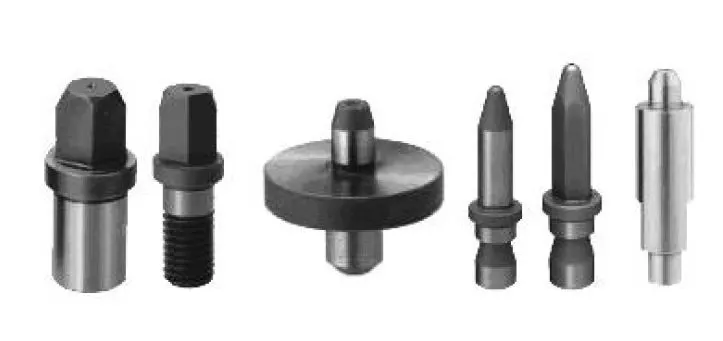
FIG. TYPES OF PINS
Pin retainer: A pin retainer is a part which holds the pin in position. It can either be a make part or a standard part. Usually the material used for making pin retainer is Steel / ASTM A-36. Pin retainers can be of two types:
HORIZONTAL PIN RETAINERS: Horizontal pin retainers are used to extend a straight plane with a perpendicular locating pin. These come with either 3 or 4 hole configuration with tapped and untapped hole variations. All the locating pin hole for horizontal pin retainers are 16mm in diameter.
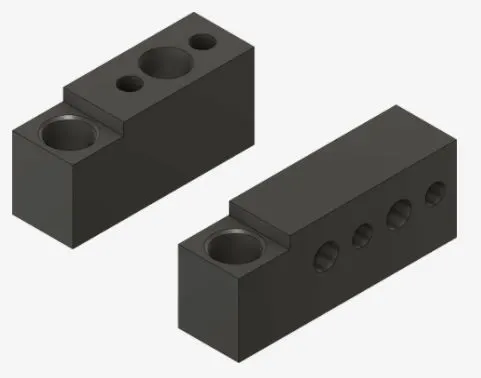
FIG. HORIZONTAL PIN RETAINER
VERTICAL PIN RETAINERS: Vertical pin retainers help to extend plane while placing the locating pin parallel to the original plane and block. Pin holes are bored to 16mm in diameter.
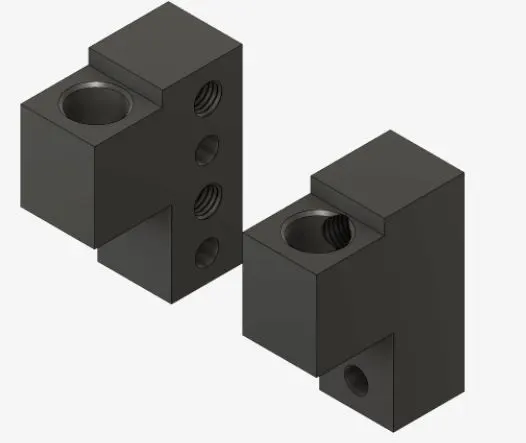
FIG. VERTICAL PIN RETAINER
Following things are kept in mind while making a pin retainer:
- Pin retainer should have a hole with a fit on which the pin will be fixed.
- The pin mounting surface of the pin retainer should be a fine machined surface.
- The pin mounting surface of the pin retainer should have a step to lock the rotation of the pin.
- The mounting surface of the pin retainer to the blocks should be a machined surface.
- The pin retainer will be fixed to a block or a L-block to the riser with 2 dowel holes and at least with one screw hole to maintain the tolerance.
NC block/Mylar: NC blocks or popularly also known as Mylar is the ones which hold the panel. It prevents the panel from deforming while welding. They always come in pairs. Top Mylar is known as clamping Mylar and bottom Mylar is known as resting Mylar.
Few points to remember about Mylar:
- Generally Mylar clamping block clamp cross section (the area which in contact panel) is considered as 20mmx20mm.
- Most of the OEM's /Tier 1 prefer Mylar to have 5mm allowance material for machining. Most of Mylar is CNC machined if it is clamping 3D profile.
- Depending on the angle of cross section, Mylar will be having shimming either in one direction or in 2 directions. General Thumb rule is if the section is inclined more than 15 deg or clamping surface is 3D profile then 2 direction shimming is provided. The reason being simple mathematics. Equation of inclined line/ plane will be having 2 parameters to controls and we control with shimming in 2 directions. Less than 15 deg does not mean that there are not 2 parameters. These are their but they are neglected if angle is less than 15 deg.
- Clamping or holding of Mylar depend upon various OEM or Tier 1 stand. Various options are available. 2 screws and 2 dowel OR 1 screw and 2 dowels. Size of dowel or screw selected as per the customer input or existing experience. Mostly M10 screw, Diameter 8mm dowel or M8 and Diameter 6mm dowels are selected.
- Tolerance of dowel is made as per the customer or Tier 1 guidelines. Keep simple rule in mind, if you are removing Mylar then should have loose /sliding fit. D10 or F8 depending upon guidelines.
- Mylar’s material can be C45, Teflon, Aluminum or S-Grun as per the customer requirement. Generally, S-Grun Mylar are made of more thickness.
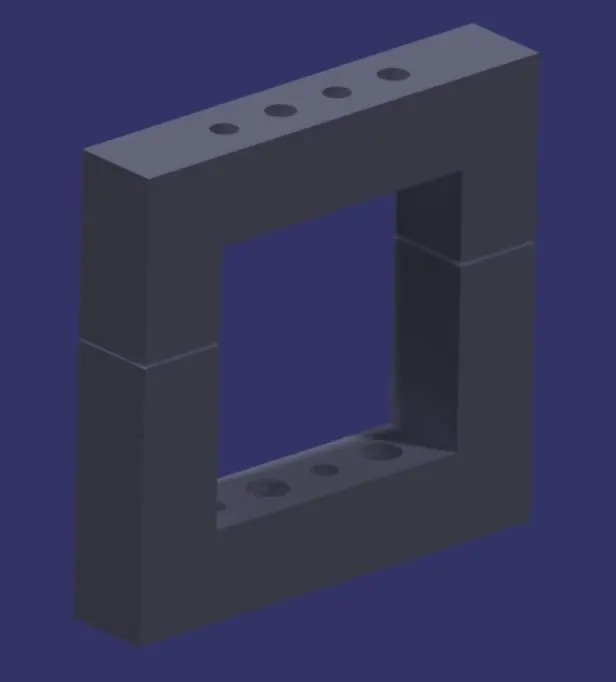
FIG. MYLAR DESIGNED FOR THE PROJECT
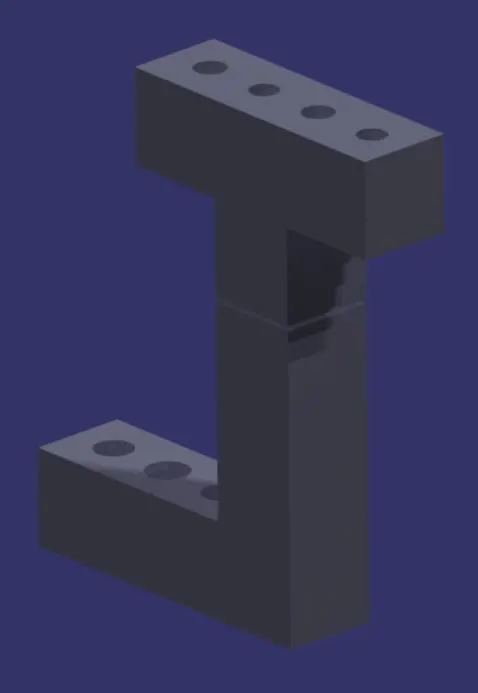
FIG. MYLAR DESIGNED FOR THE PROJECT
Shim: Shims are washers or thin strips of material used to align parts, make them fit or reduce wear. Shims are designed to fit in between blocks and fixtures to provide support or reach a dimension required in the assembly.
Few points to know about Shim:
- Typically designed in a U shape matter so that they can fit between mounting screws. This shape helps to make them easy to install and remove or replace.
- Designers will use shims individually or as packs of 5, 6, or 7 pieces. Thicknesses range from 0.25mm to 2mm.
- Many assemblies require a tolerance to be hit in relation to a length or height; shims allow designers to hit these tolerances. They can be stacked between NAAMS NC blocks, L blocks, or pin retainers.
- They come in a variety of sizes and styles. The material is typically very thin so that they can accommodate smaller to larger tolerances.
- NAAMS specification for the material is an SAE cold rolled steel.
- Different widths of the shims can have different surface treatments either yellow zinc dichromate, black oxide, or none. Yellow zinc dichromate surface treatment is used for corrosive resistance and acts as an anti-rust primer. Black oxide coating is also for corrosion resistance.
- Generally shim is used as a pack with 2*0.5mm, 2*1mm, 2mm shims.
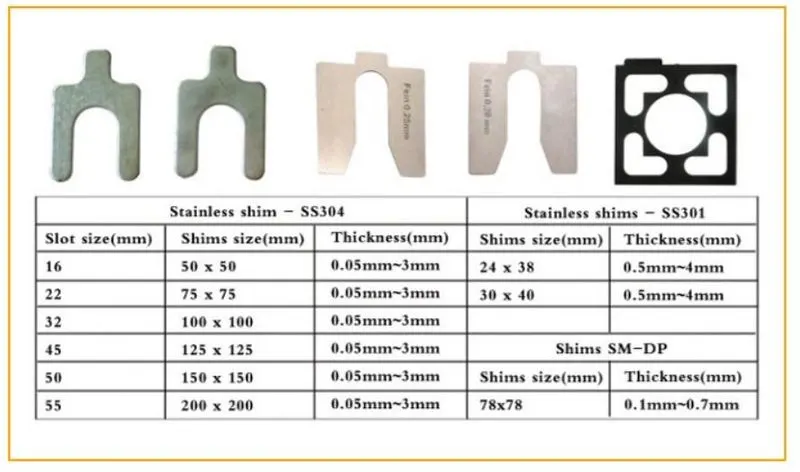
FIG. STANDARD SHIM
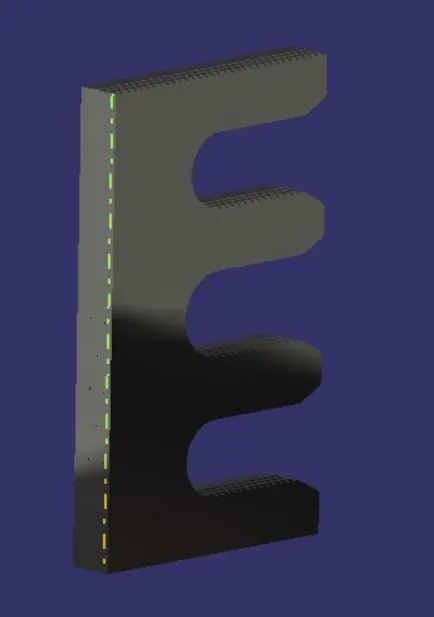
FIG. SHIM PACK DESIGNED FOR THE PROJECT
Block/L-block: These parts are mainly used to accommodate the shimming direction as per fundamental in general. In some cases they are used for other design feasibility.
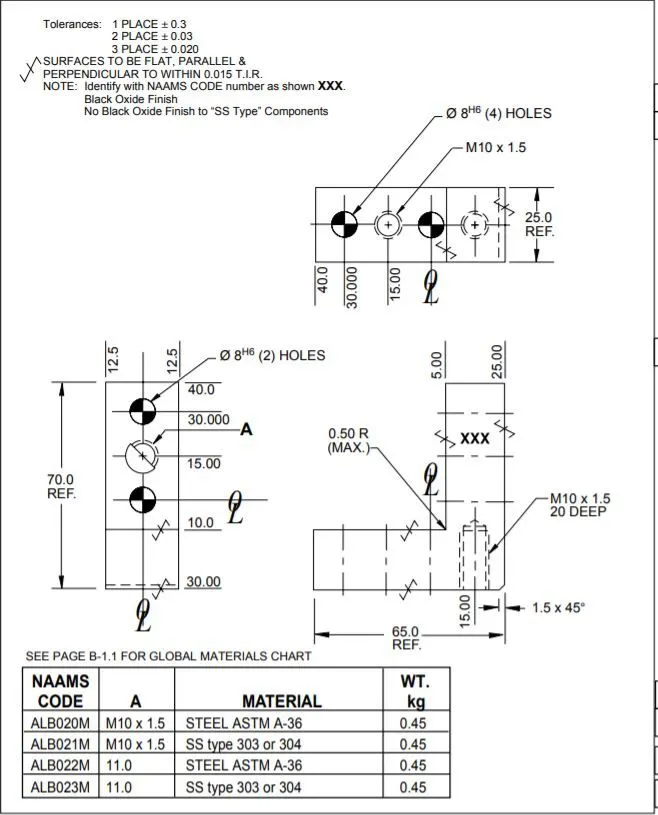
FIG. STANDARD L BLOCK
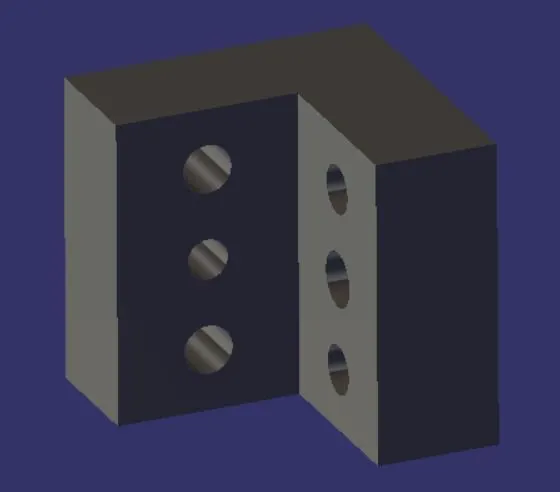
FIG. L BLOCK DESIGNED FOR THE PROJECT
Blade: Blades are the plates which are attached to the riser and other components like cylinder, arm etc are mounted on it. It can either be a standard part or a make part.
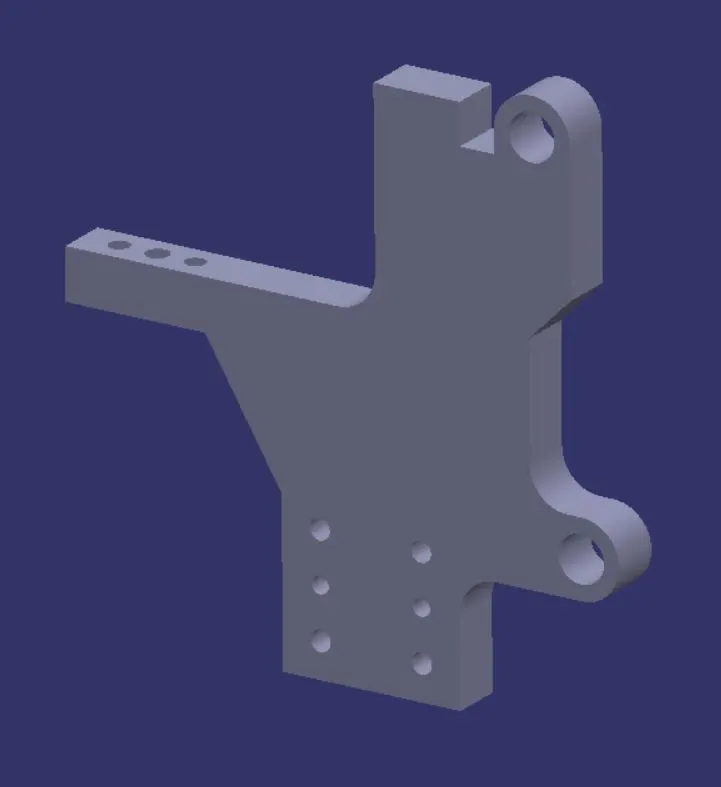
FIG. BLADE DESIGNED FOR THE PROJECT
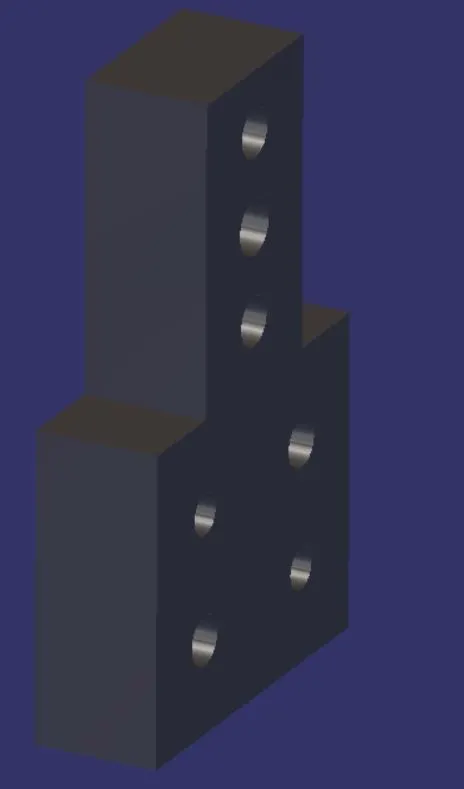
FIG. BLADE DESIGNED FOR THE PROJECT
Riser: Riser is a structure generally used to mount the toggle clamp and rest, clamp Mylar and location pin and to give height to the assembly. It is not necessary to have one riser where all the parts of clamp or rest or location units are mounted. Generally risers are either made of plate fabrication or plate and tube welding together or from single gas cut plate.
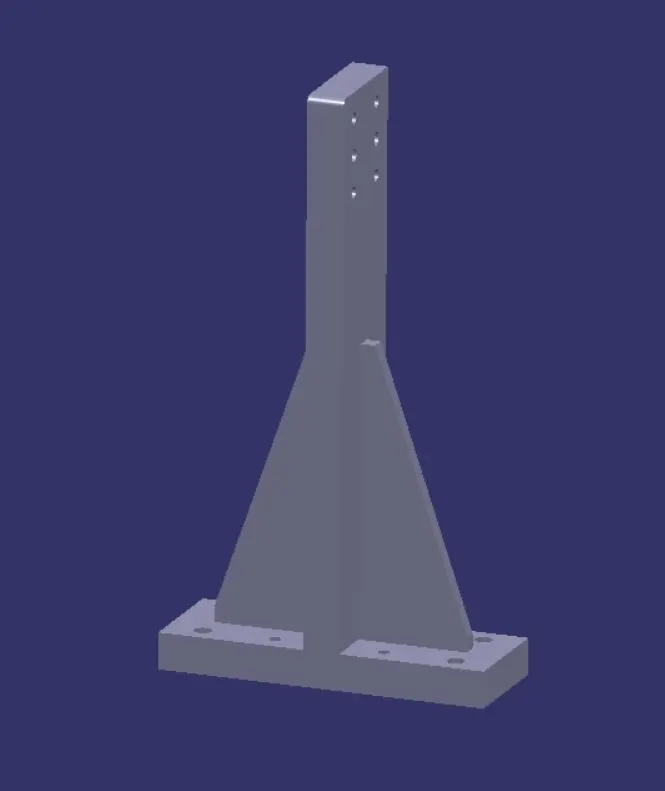
FIG. RISER DESIGNED FOR THE PROJECT
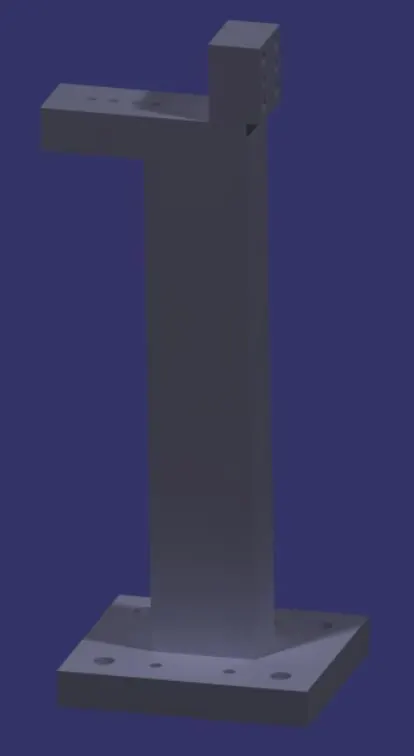
FIG. RISER DESIGNED FOR THE PROJECT
BASE PLATE: Base plate is a machined plate of 25 to 40mm thickness made of steel and aluminum on which the holes are drilled to mount individual units like clamp unit, pin unit, rest unit etc.
Fundamentals of base plate design:
- A base plate size should cover all the units with its outer periphery including opening.
- A base plate is preferred to be designed with respect to BCS coordinates.
- A base plate should be drilled with datum holes/ measuring holes in line with a pitch of 100mm in general.
- Number of datum holes depends on the size of the base plate.
- Datum holes should be drilled at nominal values of coordinates and in terms of 50 and 100.
- Datum holes should be drilled with diameter 100mm away from other units.
- Datum holes should be covered with cover plates.
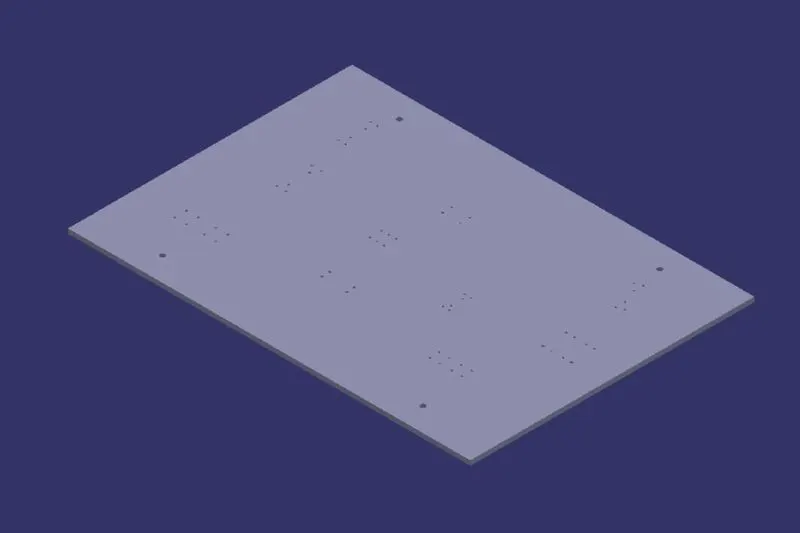
FIG. BASE PLATE DESIGNED FOR THE PROJECT
PEDESTAL: A pedestal is a part which connects the base plate to the floor plate. A pedestal is a standard part in general and in some cases it can be a welded frame integrated with the base plate.
- A standard pedestal can be of different height and different sizes.
- Depending on the size of the base plate, the number of pedestal varies for load distribution.
- Pedestals are of different types with different inclinations.
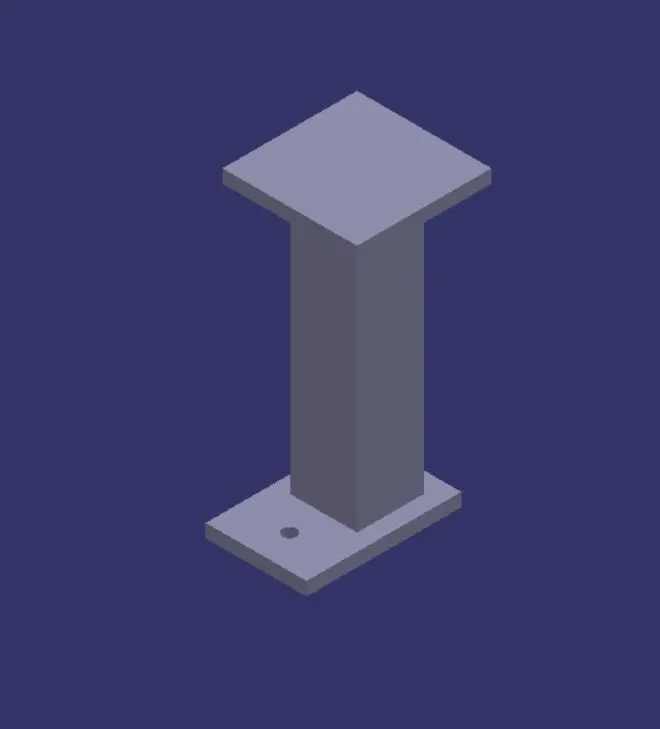
FIG. PEDESTAL DESIGNED FOR THE PROJECT
TRUNKING CHANNEL: A trunking channel is a duct which accommodates all the pneumatic and electrical houses and wires for the units if the tool.
VALVE BOX: Valve box is a standard part which will accommodate the pneumatic valves for the units.
EYE BOLT: Eye bolts are used for transporting the tool using lift hooks. Fork lift holes will also be provided in some cases for transporting purpose.
- When installing lifting eye bolts it is critical to ensure face is in firm contact with the mating surface.
- These lifting rings are intended for linear pulling loads in the direction of the thread.
- They are not intended for use where the load is perpendicular to the thread.
- This is because in these instances the bolt could unscrew and move or it could be twisted and break
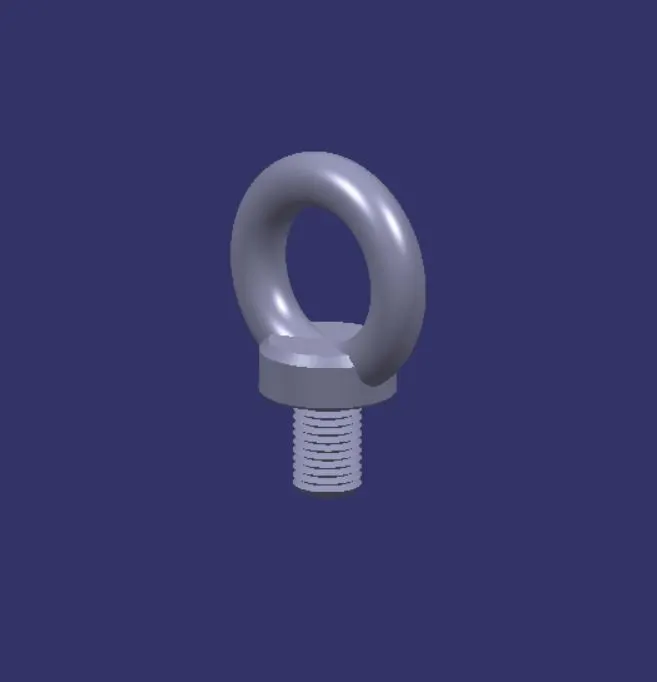
FIG. STANDARD EYE BOLT
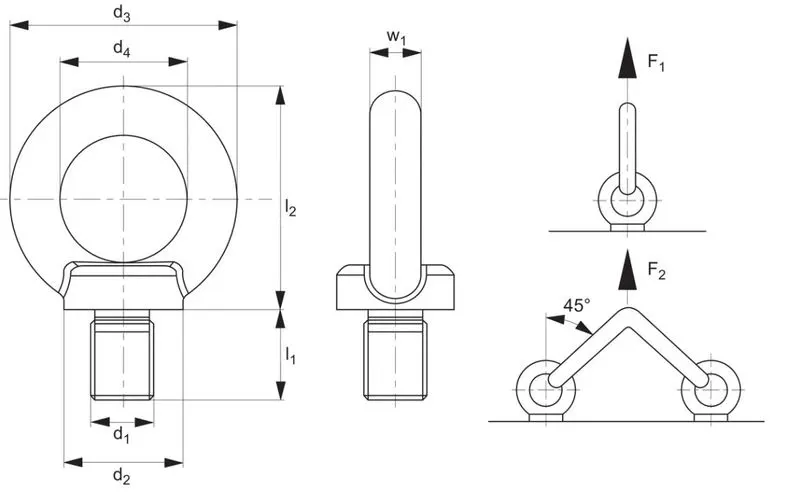
FIG. STANDARD EYE BOLT
FLOOR PLATE: Floor plate is grouted to the floor with fixed bolt on the ground. Floor plates are also called as foundation plates.
- There will be a clearance of 10mm maintained between the pedestal base plate and the floor plate.
- This clearance will be used by the leveling screws for leveling the entire tool.
- Weld bars are used to weld the positions permanently after leveling is done.
- Weld bar is a plate along the sides of the base plate of the pedestal.
Clamp arm: It is a device that mounts on the cylinder and attaches to the clamp Mylar. It is used to open and close the clamp unit. This can be a standard part or make part. For Swivel clamp unit and pin-clamp unit I have designed same type of clamp arm with varying lengths and for powered clamp unit I have used standard clamp arm downloaded from Tüekners website.
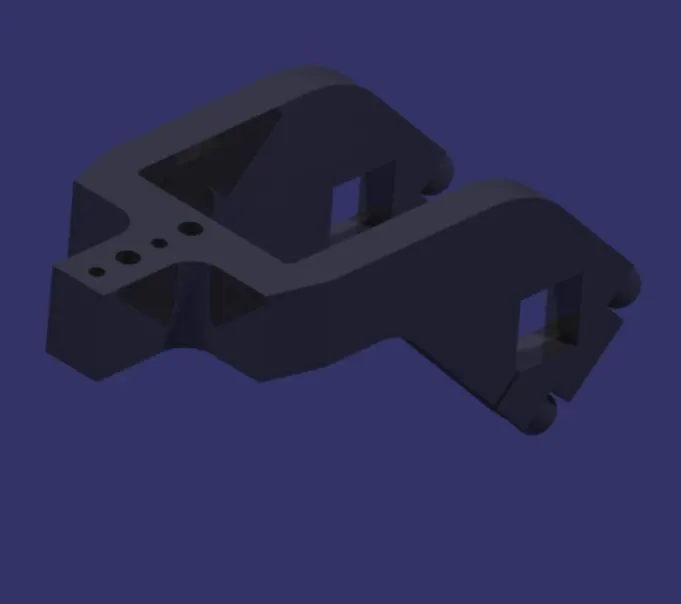
FIG. STANDARD CLAMP ARM
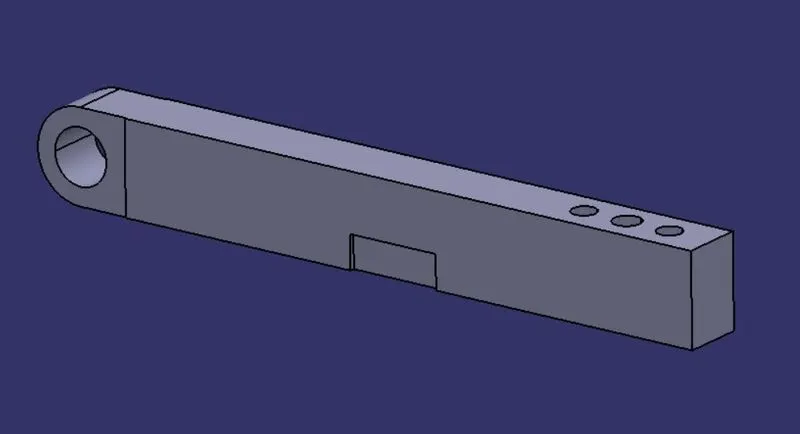
FIG. CLAMP ARM DESIGNED FOR THE PROJECT
Retractable cylinders: These are the standard parts used in Retractable pin unit. These standard cylinder CAD files were downloaded from Tüenkers website. I have used the below two cylinders in design:
SZK_30_8_T12_TUENKERS: Pneumatic Cylinder in aluminum block design with precision guide of the piston rod, secured against rotating. Compact housing made from high-strength aluminum with mounting options on several sides. Drive mechanism with circular-section cylinder for thrust forces and extraction forces of approx. 350/250 N. Total stroke 40 mm. Integrated inductive sensing system (T12).
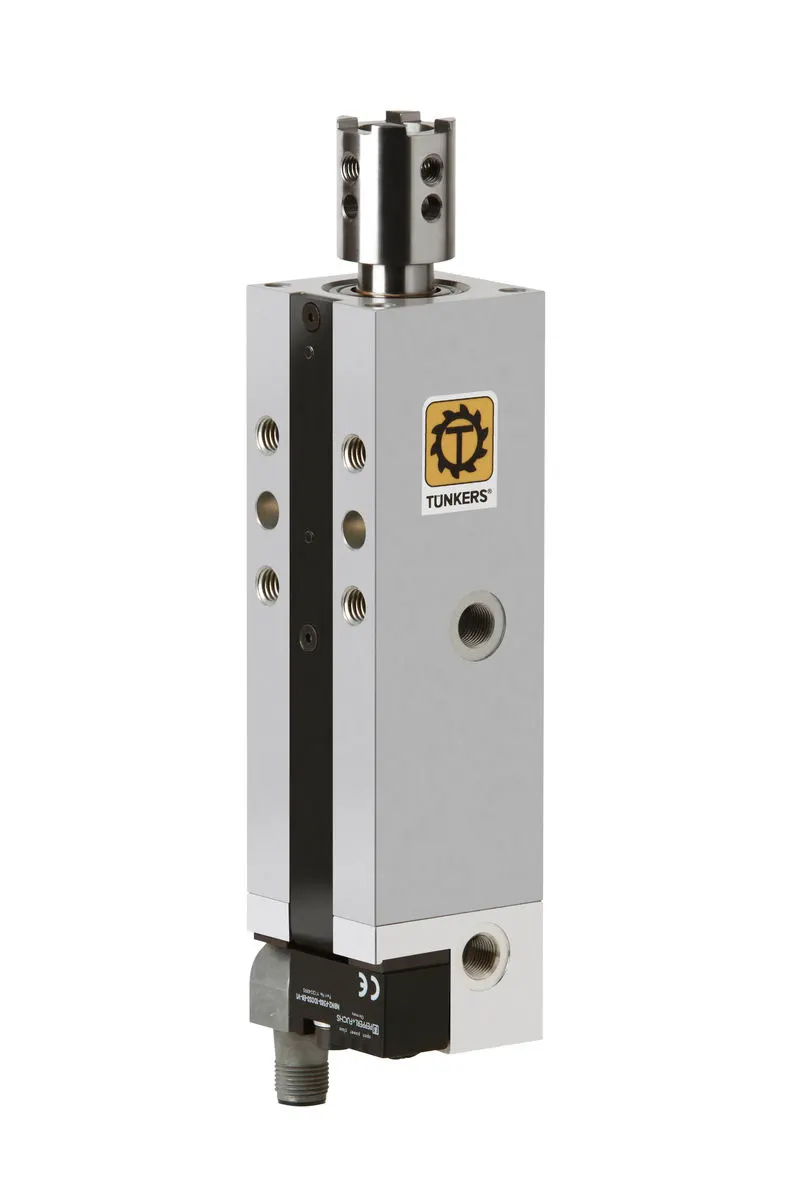
FIG. STANDARD RETRACTABLE CYLINDER
SZKD_40_BR4_A23_T12_TUENKERS: With dual non-rotating rods, Flat housing/tubing in high strength Aluminum, Flat oblong cylinder Ø 40 mm for push and pull forces of 600/400 N, Simultaneously moving rods in Bronze / Graphite Bushings, Integrated position sensing.
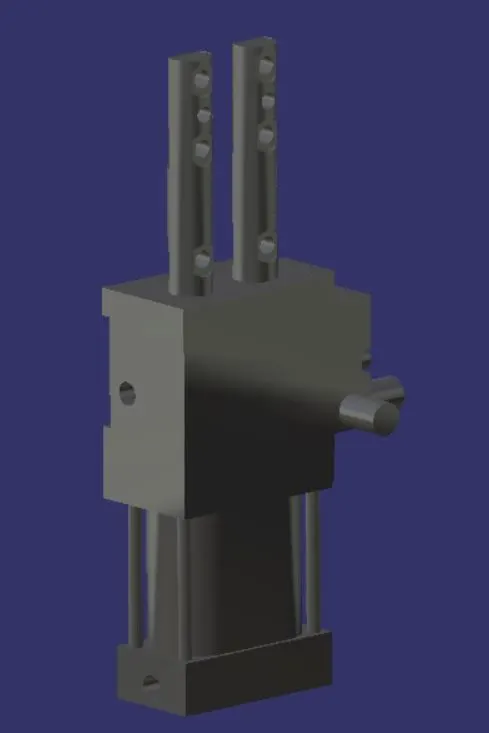
FIG. STANDARD RETRACTABLE CYLINDER
Pneumatic Cylinder: It is used to open and close the parts fixed to the clamp arm fixed to the clamp body. They are in general of 40, 50, 63 and 80 bore capacity. Horizontal clamp mounting opens up to 135 deg. Vertical clamp mounting opens up to 105deg.
V 50.1, 63.1, 80.1 BR3 Vario Clamp: Vario clamp with toggle joint mechanism and continuously adjustable opening angle, Over-centre-lock, Enclosed aluminum housing, Oval-shaped cylinder in the sizes 50, 63, 80, Forked clamping arm, standard hole pattern for adapting contour blocks, Continuously adjustable opening angle 5°-135°, optional: Weld immune inductive sensing of closed and opened position (T12).
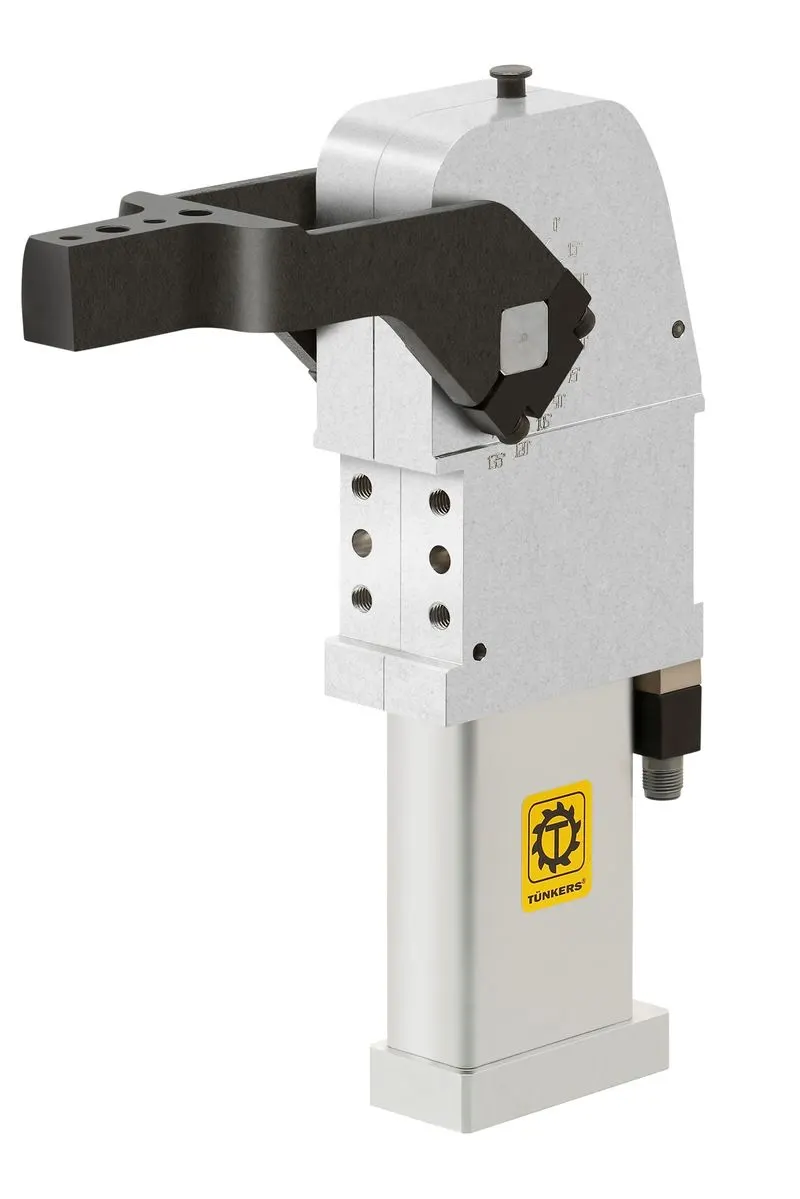
FIG. STANDARD PNEUMATIC POWERED CYLINDER
VU_63_BR2_A05_T12_135_GRAD_TUENKER: Vario clamp, Naams version, for clamping of medium and large body panels with stepless adjustable opening angle, integrated toggle lever mechanism, self-holding type. Enclosed aluminum housing, flat oval cylinder in sizes 50, 63, 80. Fork shaped clamp arm with standard hole pattern for receiving contour pieces. Opening angle variable from 5 ° -135 °. Options: - Inductive sensing, weld immune for open and closed position (T12) - Hand applied version.
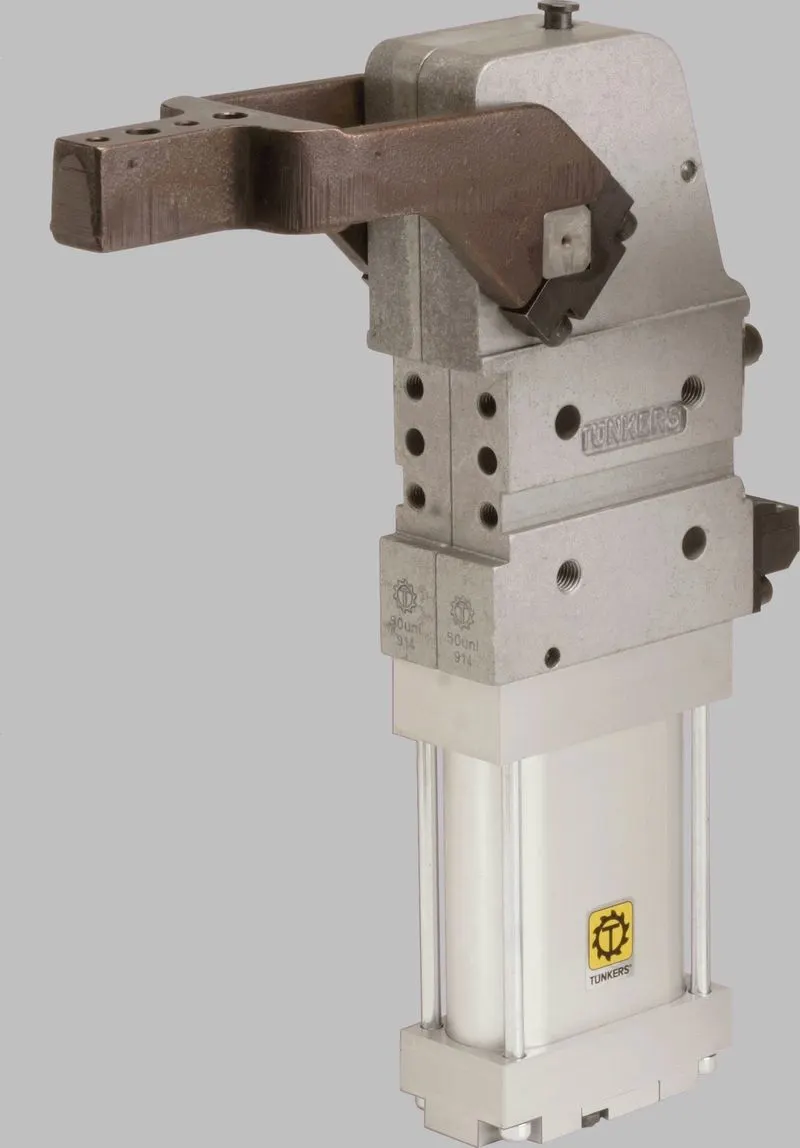
FIG. STANDARD PNEUMATIC POWERED CYLINDER
U_63_BR5_Z_A00_T24_3_TUENKERS: Variable high-performance clamp for clamping of medium and large-sized car body components with continuously adjustable opening angle and new force optimized knee lever mechanic. With the same force as a Vario Clamp, smaller cylinder diameters are used and so the air consumption is reduced by 30%. Enclosed aluminum housing, oval-shaped cylinder in the sizes 50, 63 and 80. Fork shaped clamp arm with standard hole pattern for adapting contour blocks. Continuously adjustable opening angle in the range of 5° to 135°. New two-parts switch for easy replacement.
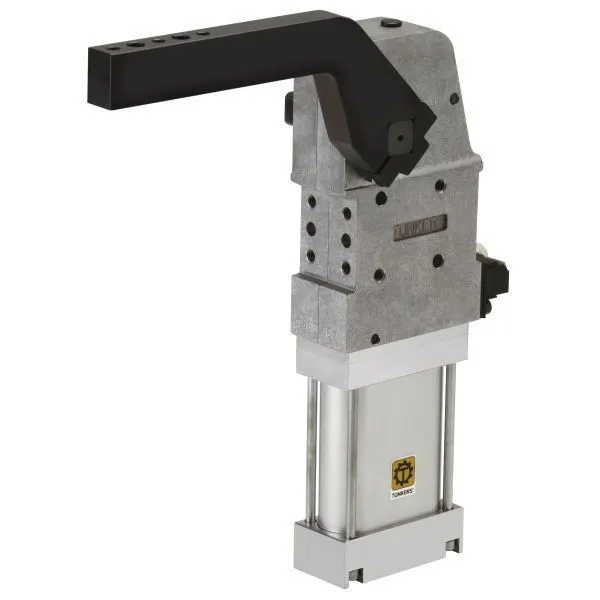
FIG. STANDARD PNEUMATIC POWERED CYLINDER
Swivel cylinder: For this project I have used Clevis clamp cylinder.
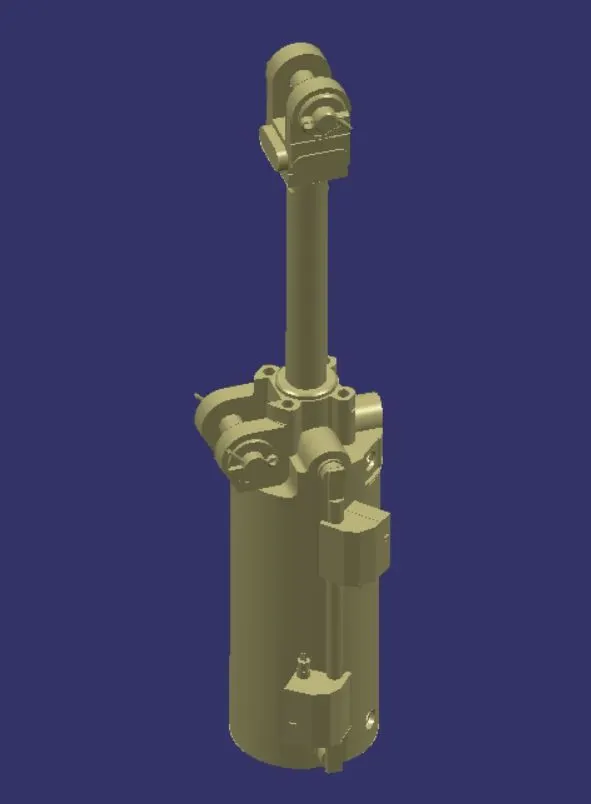
FIG. STANDARD SWIVEL CYLINDER
DESIGN APPROACH:
Carry over the units from previous projects: As the main focus of this project is to design the base unit for the given panel, I have carried over the previously designed units like powered clamp units, swivel clamp units, pin-clamp units, retractable pin units and rest units from the previous projects to this project and renamed them accordingly. A few edits were carried out on the units like changing the position and editing accordingly.
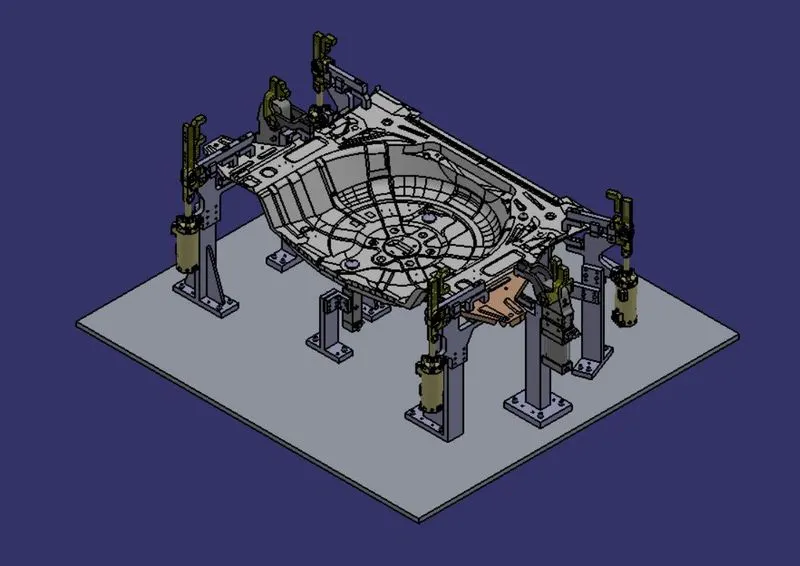
FIG. CARRIED OVER UNITS
Improving the input: The input is shown below. As it came with a surface model of base plate it had to be changed with our design rules. So the surface model of the base was hidden and a new base plate was designed which covered the periphery of all the units. As previous units had the base with respect to the surface model and the new base plate also is exactly similar to the surface model, no further changes were required.
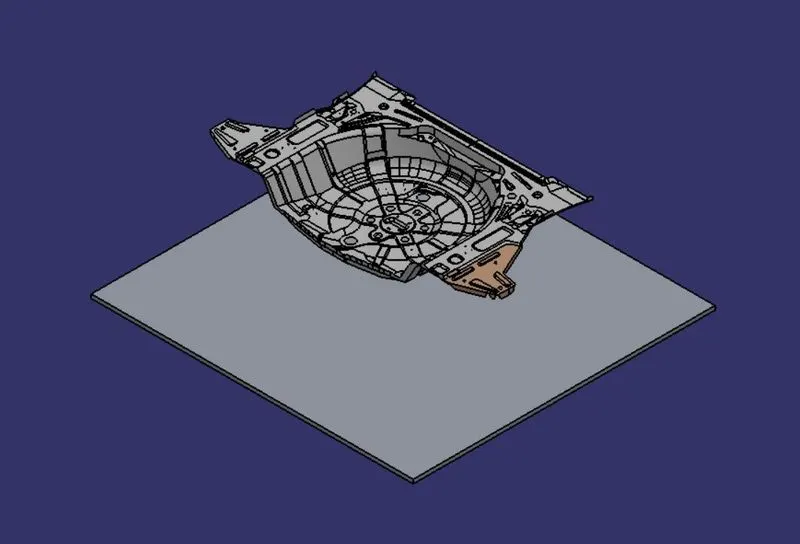
FIG. PROVIDED INPUT
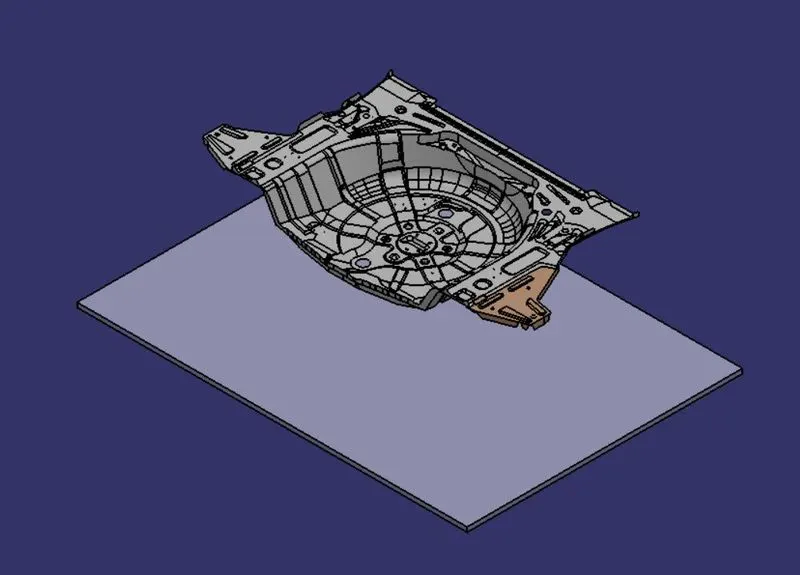
FIG. IMPROVED INPUT
Creating holes on the base plate: The base plate is to mount all the units on it with the help of M10 or M12 fasteners. The units were designed with necessary mounting clearance holes. The same threaded holes were later created on the base plate taking reference from the previously created holes. M24 holes for 4 eye bolts were also created.
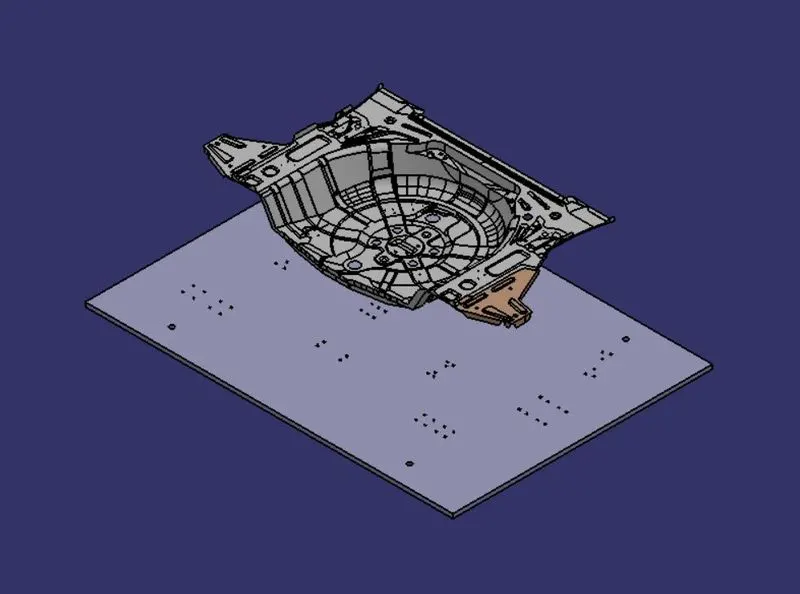
FIG. HOLES ON BASE PLATE
Designing weldments: As the thickness of the base plate is not much so we will have to increase the strength of the base unit by welding tubular structure beneath it. Hence a proper structure consisting of and tubular pipes of 100*100 with 5mm thickness placed below the base plate followed by weld plates placed properly below the tubes.
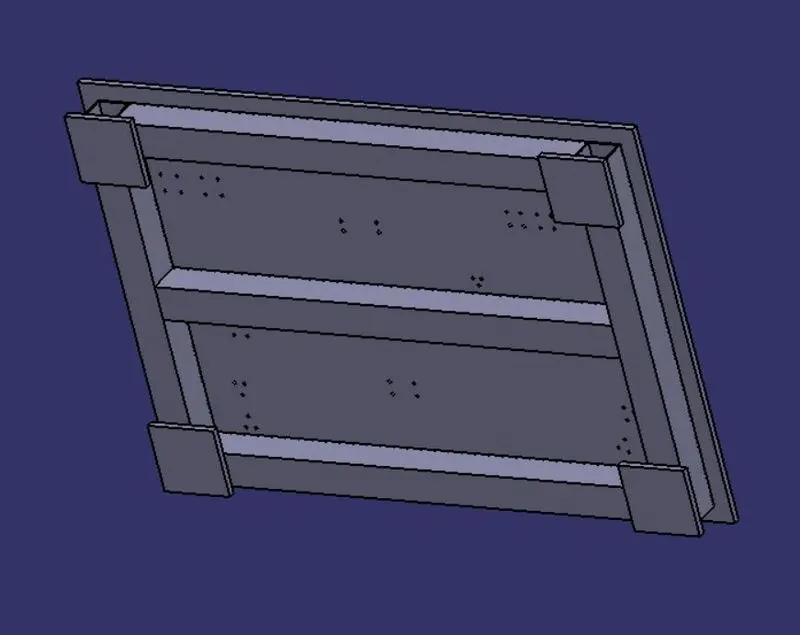
FIG. WELDMENTS
Designing pedestal: The pedestal consists of a weld plate, square tubes and mounting plates. This assembly is welded to the structure below the base plate. Square tube of 100*100 with 10mm thickness is used. The length of the pedestal is around 500mm and the entire base unit is within the limits of 850mm to 1200mm.
FIG. FINAL BASE UNIT
FINAL ASSEMBLY:
FIG. FINAL FIXTURE
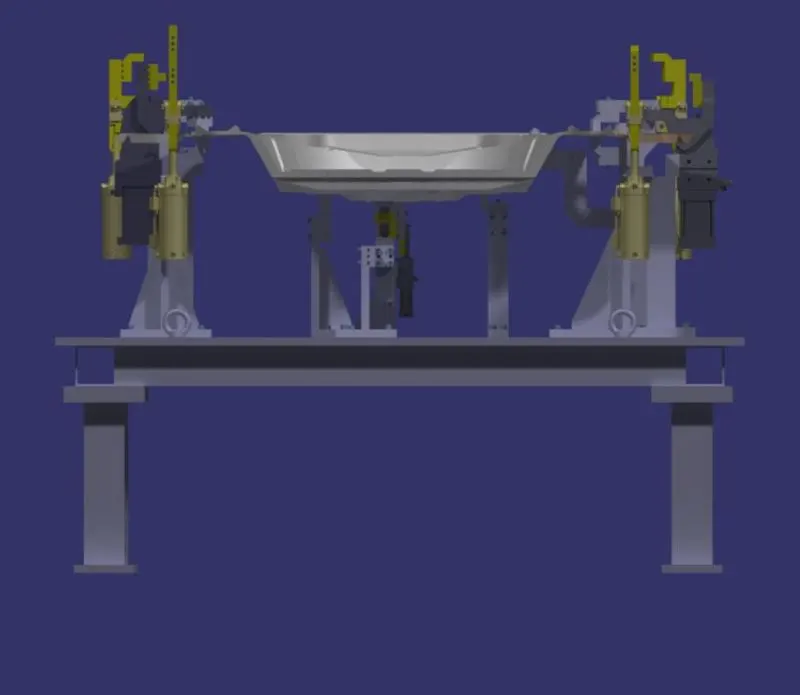
FIG. FINAL FIXTURE
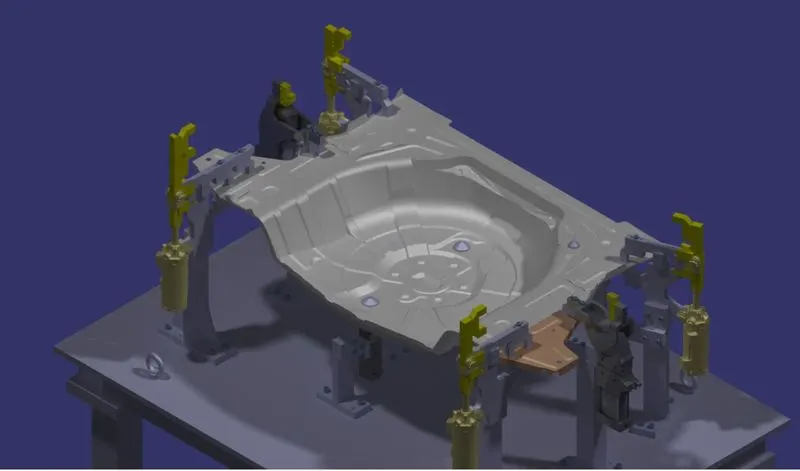
FIG. FINAL FIXTURE
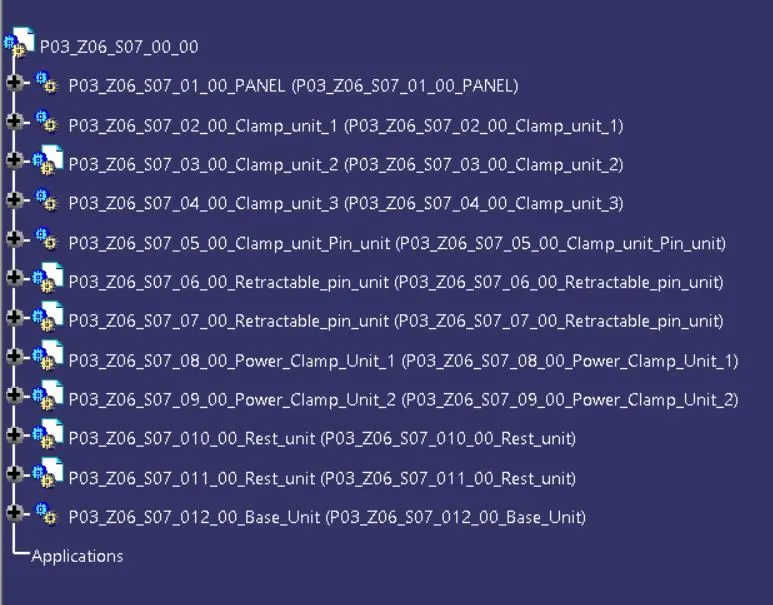
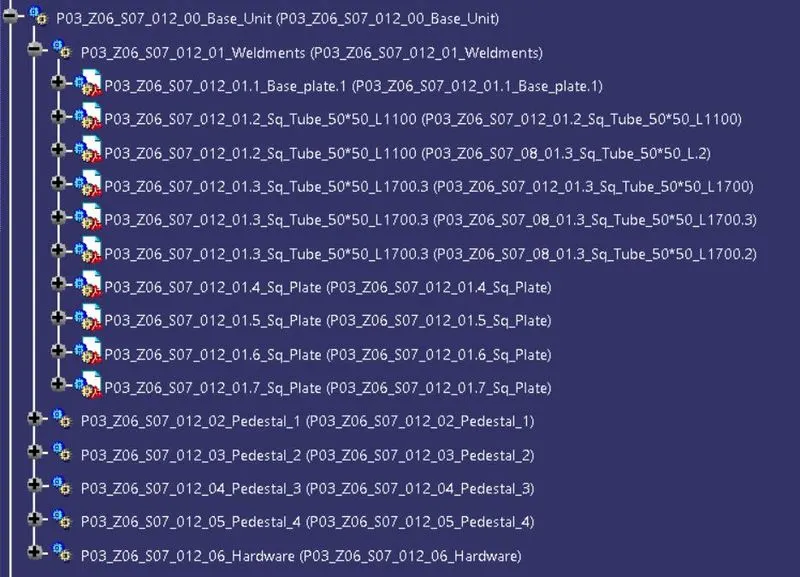
DESIGN TREE: In order to maintain a presentable CAD model with non chaotic and easy to understand project, we must maintain the design tree with proper naming. This is usually provided by the comapany. In this project I have followed the following naming:
PROJECT NUMBER_ZONE NUMBER_STATION NUMBER_UNIT NUMBER_PART NUMBER_PART NAME