Week 3:- BiW Fixture Design Methodologies Challenges
DESIGN METHODOLOGIES:
In this methodology we learn about three design processes, we're going to study how do we proceed while doing a design. And one of the things that we take care of is structuring or design tree so we'll be learning how to structure the design tree, and how to name the particular component or particular assembly, or the part of an assembly, which is very easy to read and very easy to understand.
Design methodologies are nothing but the steps followed during the concept designing stages of fixture design. The various stages of design methodologies are,
1. Purchase order.
2. Inputs from customers.
3. Percentage of completion criteria.
4. Design outputs.
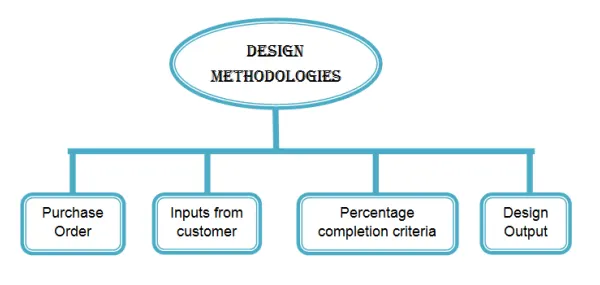
1. Purchase Order:
A purchase order (PO) is a commercial document and the first official offer issued by a buyer to a seller indicating types, quantities, and agreed prices for products or services. It is used to control the purchasing of products and services from external suppliers. Purchase orders can be an essential part of enterprise resource planning system orders. A purchase order is an order from a customer for the start of the work. After an offer has been finalized customer will be releasing the
LOI/PO(Purchase Order).
Once PO is released we have to start the work.
After PO from the customer, we have to prepare the schedule.
A purchase order is the confirmation document from the customer to proceed with the committed work for them.
2. Inputs from customers:
The inputs from the customers are as below,
Functional Requirements:
The purpose or the function of the fixture will be given as inputs from the customers like what are the process the fixture is going to do i.e welding, riveting, gluing, or whether it is a checking fixture, etc.
Preferred standards:
As we know different companies follow different standards, we will be following the standards, we will be following the standards followed by the customers. By following standards, the time of designing and manufacturing of parts will be saved, which will be automatically minimizing the time of the projects. As for the standards parts, they can be easily replaced from the used fixture to the new fixture which reduces the cost.
Car products:
The inputs we get from car products are GD&T, part list, cad files of car part, clamp plan, product assembly process sheet.
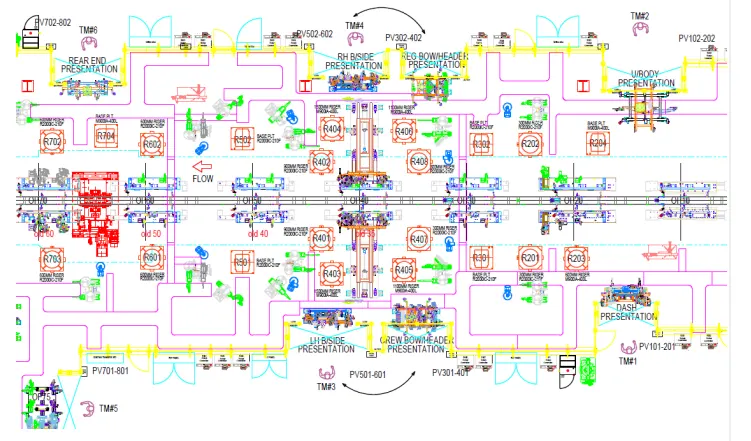
The layout: shows the entire assembly plan to understand the process. The layout provides the information of flow of parts, station pitch, robot stations, accessories like tool changers & tip dressers, sub-assembly links, platform height, loading/unloading sequence/height.
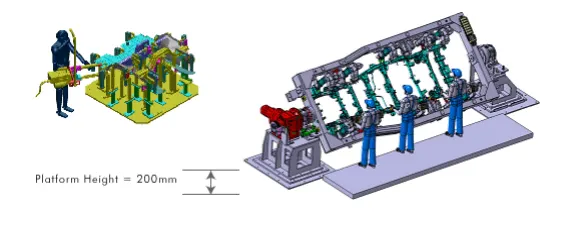
Ergo Data: As same as preferred standards, different companies follow different standards of ergo data. We have to follow the customer standards of ergo data. The inputs of ergo data will be given by the customer mostly in the case of manually operated fixtures/manual fixtures. The ergo data is mainly used to make the operator comfortable which may lead to improved efficiency in cycle time& production. Ergo data provide inputs like platform height, maximum & minimum reach
from operator to fixture, maximum & minimum height of the fixture, whether the child parts/assemblies are visible while clamping or loading & unloading. Also provides information like loading height, working safety zone of the operator, etc.
Weld study: Weld study is the important inputs given by the customer. It gives details about the study of particular guns that we use for welding. Also, the dates like no/ of weld, the position of weld in the components will be given. In short, the weld study includes weld gun details, weld matrix & weld points.
Standard detailing templates:
These inputs include the detailing templates of 2D cad drawing as per the customer standards. So, we have to follow the detailing templates as per the customer
standards.
3. Percentage of completion criteria:
Percentage completion criteria are basically scheduled. What time that we can complete the entire process again this is more detailed. So when we are going to complete the in entire design, then we're going to move on to simulation on all these subcategories would be considered in percentage completion criteria like a probability to when we can complete the entire fixture design.
It is followed in the designing stages & dispatch stages of welding fixtures. It helps to track or identify how many tasks completed & how much to go further for completing a fixture.
Inputs & concept design – 0 to 25%
Concept approval & simulation check – 25 to 40%
Design freezing & detailing – 40 to 85%
Check & final dispatch – 85 to 100%
The above-mentioned percentage are the percentages of stage-wise completion criteria of the projects.
4. Design Output:
In BIW fixture design or any industry. We don't only just design a particular component and just give the CAD file to the customer, we have to give a lot of documents like 3d documents,2d documents, which is the detailing part, and as well as other factors as well like bom, bill of material(BOM) and other documents as well as this particular component and their standards, all has to be submitted to the customer.
Question 2) What are the inputs required from the customer to start designing a fixture?
The inputs required from the customer to start designing a fixture:
1. Fundamental requirements.
2. Preferred standard components.
3. Car products.
4. Layout.
5. Ergo – data.
6. Weld study.
7. Standard detailing templates
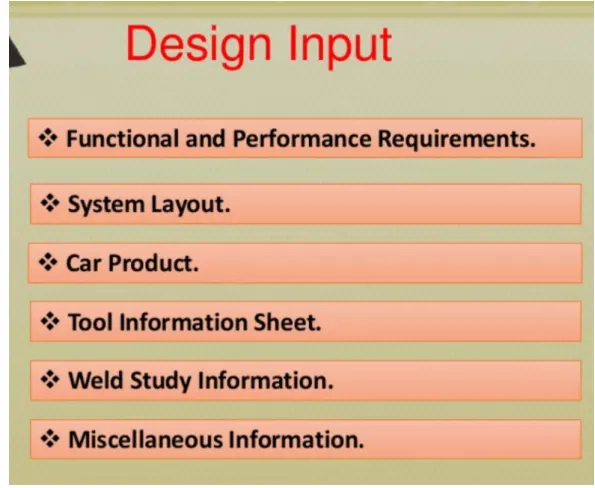
1. Functional Requirements:
The purpose or the function of the fixture will be given as inputs from the customers like what are the process the fixture is going to do i.e welding(spot or seam weld), gluing, riveting, hemming, or whether it is a checking fixture or a storage racks, etc.
It is one of the basic requirements to get from the customer to start designing a fixture.
2. Preferred standards:
As we know different companies follow different standards, we will be following the standards, we will be following the standards followed by the customers. By following standards, the time of designing and manufacturing of parts will be saved, which will be automatically minimizing the time of the projects.
As for the standards parts, they can be easily replaced from the used fixture to the new fixture which reduces the cost.
Some of the preferred standard components used in BIW fixtures are given below,
1. Standard like ABB, NAAMS, DESTACO, ZYTRAN, TUNKERS are used in the design & manufacturing of fixtures.
2. Standard parts like Risers, L-blocks, retainers, pins, NC blocks, Shims, etc.
3. Components like clamps, cylinders, slides, switches, sensors, etc.
4. Weld guns, Tip dressers, Tool changers, etc. tip dressers are to sharpen the tip of the tools whereas tool changes are used in robots to do various processes.
As robots are too costly, tool changers are used.
ABB – It is a Robots manufacturing company.
Some examples of a description of standard robots are Robust IRB 7600 robots, which can hold the panels securely and accurately in place while IRB 6640 robots perform the welding.
The welding line is installed at great wall motors (GWM) recently opened an internationally acclaimed automotive plant in Tianjin, China. One of the factory’s most highly publicized and productive manufacturing lines is the ABB welding line, which comprises among other things a fleet of
ABB robots and patented ABB framing and hemming technologies.
3. Car Products:
The inputs we get from car products are: GD&T, part list, Cad files of car part, Clamp plan, product assembly process sheet.
a. GD&T: It provides information of locating pins, rest, clamp, damp & slide unit information of each station. Also includes the information of the sequence of openings of clamps, dumps & slide stroke information.
b. Part lists: It gives the lists of parts that are going to assemble in the fixture. The list contains the information of part number, part name, revision of fixture, part thickness, etc.
c. Clamp plan: Clamp plan provides the information of the location of pins, Rest units, clamp unit, dump, etc. It is the important input from customers. The clamp plan/position should not be changed without the knowledge of the customer.
d. 3D cad file: The 3D model of the car part will be given to the customer. From that 3D model, we will be developing our fixture design process. The 3D cad file will be in the format of a step file (STP) or IGES file (igs).
e. Product assembly process sheet: It gives the information of stage-wise assembly process like how the parts move from one assembly process like how the parts move from one assembly station to another after the completion of the joining process.
4. Layouts: The layout shows the entire assembly plan to understand the process. The layout provides the information of flow of parts, station pitch, robot stations, accessories like tool changers & tip dressers, sub-assembly links, plan form height, loading/unloading sequence/height.
5. Ergo Data: As same as preferred standards, different companies follow different standards of ergo data. We have to follow the customer standards of ergo data. The inputs of ergo data will be given by the customer mostly in the case of manually operated fixtures/manual fixtures.
The ergo data is mainly used to make the operator comfortable which may lead to improved efficiency in cycle time & production.
Ergo data provide inputs like platform height, maximum & minimum reach from operator to fixture, maximum & minimum height of the fixture, whether the child parts/assemblies are visible while clamping or loading & unloading.
Also provides information like loading height, working safety zone of the operator, etc.
6. Weld Study: Weld study is the important inputs given by the customer. It gives details about the study of a particular gun that we use for welding.
Also, data like No. of weld, the position of weld in the components will be given. In short, the weld study includes weld gun details, weld matrix & weld points.
Generally, weld points will be given in spheres.
7. Standard detailing templates:
These inputs include the detailing of 2D cad drawing as per the customer standard.
So we have to follow the detailing templates as per the customer standards
Question 3) What are the inputs we get from car products?
Inputs we get from car products include;
1. GD&T.
2. Part lists.
3. 3D cad file.
4. Clamp plan.
5. Product assembly process sheet.
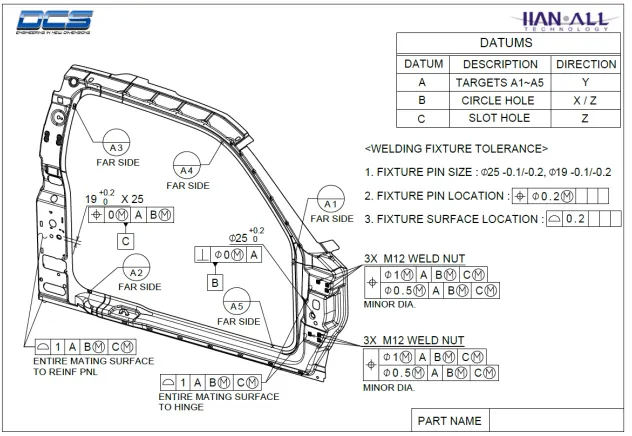
1. GD&T: Geometric Dimensioning & Tolerance.
It provides information on locating pins, rest, clamp, damp & slide unit information of each station. Also includes the information of the sequence of openings of clamps, dumps & slide stroke information.
Tolerance important:
Assemblies – Parts will often fit together if their dimensions do not fall within a certain range of values.
Interchangeability – If a replacement part is used, it must be a duplicate of the original part within certain limits of deviation.
The relationship b/w functionality and size or shape of an object varies from part to part.
When to use GD&T:
When part features are critical to a function or interchangeability.
When functional gaging is desirable.
When datum references are desirable to ensure consistency between designs.
When standard interpretation or tolerance is not already implied.
When it allows a better choice of machining processes to be made for the production of a part.
Datum in GD&T:
A datum is a theoretical exact plane, axis, or point location that GD&T or dimensional tolerances are referenced to you can think of them as an anchor for the entire part, where the other features are referenced from A DATUM feature is usually an important functional feature that needs to be controlled during measurement as well.
2. Part lists:
It gives the lists of parts that are going to assemble in the fixture. The list contains the information of part number, part name, revision of fixture, part thickness, etc.
3. 3D cad files:
The 3D model of the car part will be given to the customer. From that 3D model, we will be developing our fixture design process.
The 3D cad file will be in the format of step file (stp.) or IGES file (igs.) or sometimes it may be in a part file (part).
4. Clamp plan:
The clamp plan provides the information of the location of pins, rest units, clamp unit, dump, etc.
It is the important input from customers. The clamp plan/position should not be changed without the knowledge of customers.
It gives the detail of the exact position of the clamping units.
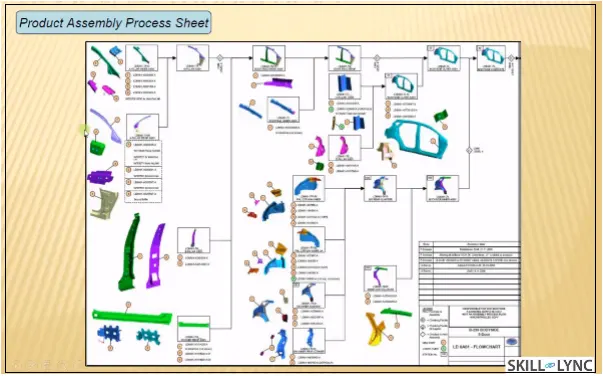
5. Product assembly process sheet:
It gives the information of stage wise assembly process like how the parts move from one assembly to another after the completion of joining process
It shows the sequence of operations/process to be done in a part of a panel.
Also what is the parts to be joined with the panel will show in sequence.
From this sheet, we can trace out the pending process which has to further go on for completion of part.
From this product assembly process sheet designer can understand the sequence for designing the fixtures.
Question No.4 – What is the clamp plan?
Clamp:
A clamp is a fastening device used to hold or secure objects tightly together to prevent movement or separation through the application of inward pressure.
Essential requirements of clamps:
All clamps must fulfill four essential requirements. They are,
1. The workpiece must be held rigid while undergoing operations.
2. The time required for loading / unloading the tool must be as short as possible, which means the clamping device must be quick acting.
3. when subjected to vibration, chattered, heavy pressure the clamping must be positive.
4. The clamp must not damage the workpiece.
Clamp Plan:
- Clamp Plam is a very important to input that we get in the car products is where exactly we can place those clamping units are the particular pin Units.
- we should never change the position of the particular clamp or the pin, which is given in these data.
- we can change our design a little bit here or there, but we should not change the input design data about the clamp position or the pin position.
- In the Clamp plan, there is a clamp unit, pin unit and it is more detailed. It also gives the exact location of y and Z coordinates designing as well you can just input these coordinates and we can start designing from there.
- If the three coordinates, whole diameter, and everything are already given to design the entire future design phase, and it is sometimes ministry as well. It happens that another thought position, also given very close to the clamp, or the clamp location. So always ask to whether you have changed the clamp position.
- we should never change the vent position or the clamp position without asking it So always be vary about these situations So the tool might get damaged or the department gets damaged so for that itself need to clarify once again before doing any changes in the clamp.
Question No.5 – What is the purpose of the layout?
THE PURPOSE OF THE LAYOUT:
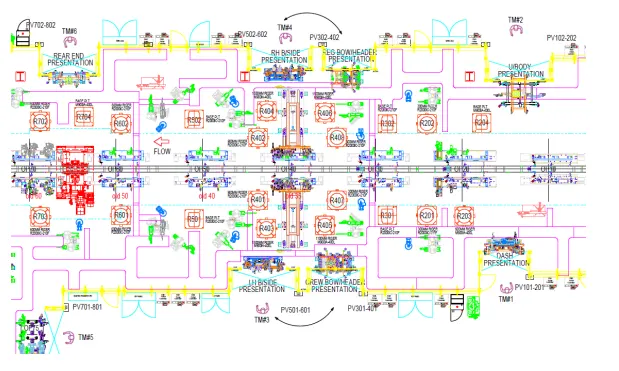
The purpose of the layout is to understand the information about where the fixture & robots are been placed, the working area covered by the robot, what are the fixtures assigned for the robots to do the process, etc. layout shows the entire assembly plan to understand the process.
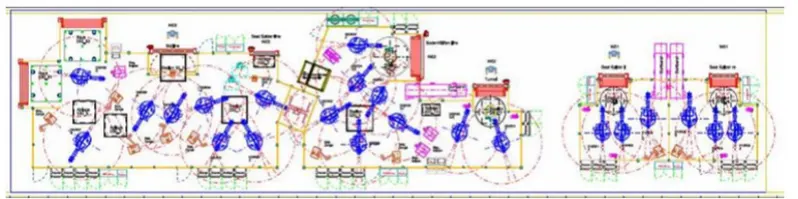
The circle around the robot is the swept area of the particular robot which shows the reachability of the robots particularly with the confine circle.
The layout provides the information on the flow of parts, station pitch, robot stations, accessories like tool changers & tip dressers, sub assembly links, platform height, loading/unloading sequence/height.
The layout sheet will give you information about all the fixtures are placed, the robots are going to work on it.
In the layout sheet, the circle around the robot is called the Trapped Area of that particular robot.
So, this is basically the reachability of the robot which is confined to the particular circle.
The flow of parts: It shows the flow of the parts/panel in the assembly line or shop floor like how components move from one station to another station after the completion of the process.
Station pitch: The distance between two stations is known as station pitch. It shows the space constraints between the two stations, which shows in the layout.
Robot stations: It shows the position where the robots & their accessories are placed, which is shown in the layout.
Sub-assembly link: The subassembly link is nothing but the link between the assembly fixtures & the main assembly line. It shows that how the sub-assembly
fixtures are linked with the main assembly line.
The main purpose of the layout is to understand the entire plan of the assembly line.
The layout providing the above information like the flow of parts, station pitch, robot stations, etc used to understand the working process of robots, what are the fixtures assigned for the robots, space constraints, etc.
By considering the layout, the designers can develop the concept sketches of fixtures without any clash in the assembly lines.
One of the main purposes is to get the information about the space constraint which helps to develop the robotic cell without any clash during working.
Question No.6 – What is Ergo-data?
ERGO DATA: Ergo data is nothing but the data or inputs which give the human factors engineering data, between the operator & his working environment. Before detailing about ergo data we should know about ergonomics in detail.
ERGONOMICS: Ergonomics also known as human engineering & human factors engineering is the scientific study of the relationship between man and his working environments.
OBJECTIVES OF ERGONOMICS:
The fundamental objective of the study of ergonomics is to optimize the integration of man & machines so as to improve productivity & accuracy.
In short, the objective of ergonomics is designing for human use & optimizing working & living conditions.
Two main objectives of ergonomics are:
1. To enhance the efficiency and effectiveness with which the work is carried out so as to increase the convenience of use, reduce errors & increase in productivity.
2. To enhance certain desirable human values including safety, reduced stress & fatigue, and improved quality of life.
Ergonomics involves the design:
1. A workplace suitable for the worker.
2. Machinery & controls, so as to minimize physical strain on the worker to enable the improvement in the efficiency.
3. An environment for performing a task most effectively and conducive.
4. A conducive task & work organization.
Benefits of Ergonomics:
- Improved working conditions.
- Reduce physical workload.
- Improved work postures.
- Reduced efforts of certain movements.
- Better reading instrument displays, handling of machine levers & Controls.
- Reduced unnecessary information recall efforts.
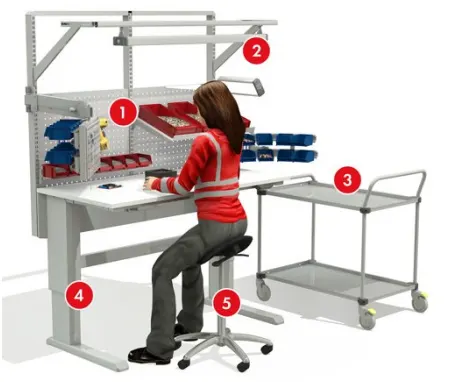
- Below, I have given a basic example of ergonomics in the workstation.
ERGO DATA:
- Ergo data is nothing but the data or inputs which give the human factors engineering data, between the operator & his working environment.
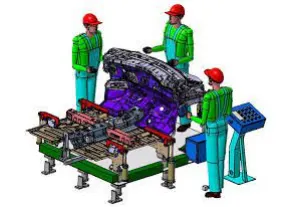
- Ergo data is most needed while there is a need for manual operator/operation.
- Ergo data will be given from customers as per their standards. Every customer follows different ergo data standards.
- As per customer standards, we have to consider the ergonomics in the fixture while designing.
- From ergo data we get the details or inputs related between the operator and his working fixture.
- The ergo data is mainly used to make the operator comfortable which may lead to improved efficiency in cycle time & production.
Question No.7 – What do you understand by weld study?
WELD STUDY:
Weld study is the important inputs from the customer.
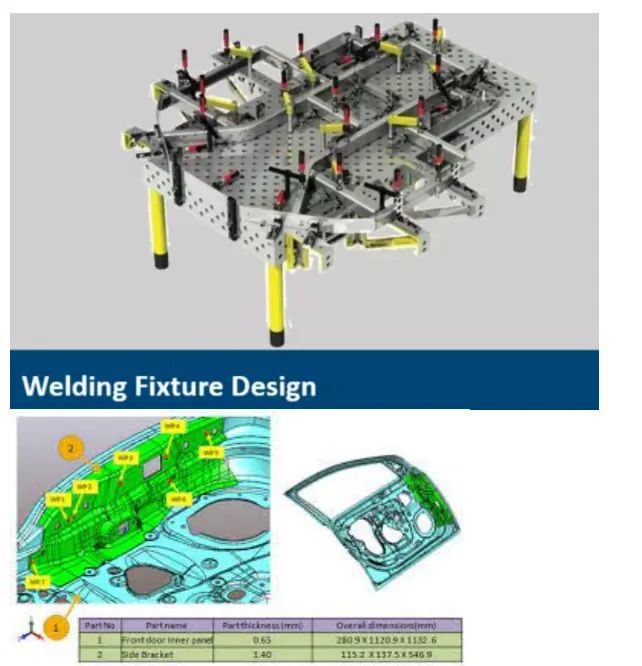
It gives the study of particular gun that we use for weld, No. of spots to be welded, sequence of weld, the position of weld in the components.
In short, the weld study includes weld gun details, weld matrix & weld points.
Generally, the weld points will be given in spheres.
The red sphere represents the Geo spot weld points whereas the Green sphere represents the Respot weld points. The weld points are classified as,
1. Geo weld points:
The Geo weld points are which is planned in the Geo fixture.
This weld will determine the position of the panels as per the given data in the drawing.
The geo weld points are represented in the red sphere in the weld study inputs given by the customers.
2. Respot weld points:
The respot weld points are planned in the respot tool.
This weld will determine the strength/stiffness of the panel/components.
The Respot weld points are represented in green spheres in the weld study inputs given by the customers.
Question No.8 – What are the criteria for percentage completion in the designing stage? Explain in detail?
The percentage completion criteria is followed in the designing stages & dispatch stages of welding fixtures.
This percentage completion criteria is followed to trace the project whether it matches the committed date given to the customer for hand over the projects to them.
Also, it helps us to identify the stages in the projects like how much the project is completed and what are the further stages are in pending, to complete which helps us to complete the projects on the committed time and date.
The percentage completion criteria is divided into four stages to identify the percentage of the completion of work.
The four stages of percentage completion criteria are as follows,
1. Input & concept design.
2. Concept approval & simulation check.
3. Design freezing & detailing.
4. Check & final dispatch.
1. Input & concept design:
If the project is in the stage of Input & concept design then the percentage completion criteria of the project will be between 0 – 25%.
After the completion of input & concept design then the project will be moved to concept approval & simulation check which is the second stage in percentage completion criteria.
2. Concept approval & simulation check:
If the project is in the stage of concept approval & simulation check then the percentage completion criteria of the project will be between 25% - 40%. After the completion of concept approval & simulation check then the project will be moved to design freezing & detailing which is the third stage in percentage completion criteria.
3. Design freezing & Detailing:
If the project is in the stage of Design freezing & detailing then the percentage completion criteria of the project will be between 40% - 85%.
After the completion of design freezing & detailing then the project will be moved tp check & final dispatch which the fourth & the last stage in percentage completion criteria.
4. Check and final dispatch:
If the project is in the stage of check & final dispatch then the percentage completion criteria of the project will be between 85% - 100%.
After the check, the project will be finally dispatched successfully to the customer.
Question No.9 – Brief about output in design?
Output In Design:
In BIW fixture design or any industry. We don't only just design a particular component and just give the CAD file to the customer, you have to give a lot of documents like 3d documents,2d documents, which is the detailing part, and as well as other factors as well like bom, bom bill of material and other documents as well about this particular component and their standards, all has to be submitted to the customer.
The output is 3D models and the 2D drawing of the tools.
1. Unitized Tools
2. Non-Unitised Tools
1. Unitized Tools:
The unitized tools testing requires two types of a drawing sheet, which is one key sheet and a layout sheet.
So examples of unitized tools are fixtures,tools So where exactly multiple units are a placed. For example, the entire assembly welding fixtures, where a pin unit,clamp unit,rest unit and the panel, everything is included so that for those things.
Key sheet - An index of units and their placements on the tool base.It will have an orthogonal view of the fixtures including a numbered balloon drawing mentioning the units.
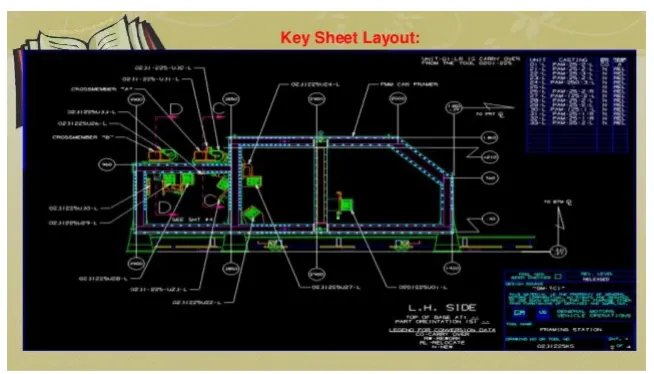
Layout sheet - A detailed drawing of individual units to include all of their components.For the Non unitized tool no need of key sheets. As they can stand alone, the drawing can be detailed completely on layout sheets.
So, it is basically an index of units and placements on the tool base, so the key sheet going to show you the placement and the location of that particular tool on the tool base where exactly the tool is placed. And what is his exact position in a particular place.
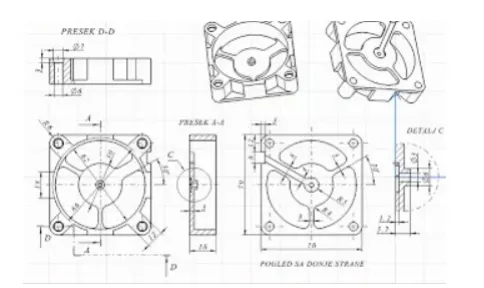
2.Non-Unitized Tools:
Tools that can stand alone and can be detailed completely on a layouy sheet.
Non unitized tools are basically tools like Stands and tool changers is also an example of an non unitized tools where you don't need key sheet, you can actually used to layout sheet and complete the entire documentation of the particular component. So this is as known non unitized tools.
The Design Output Should Compile Following Points:
1. Approved standard components are to be used wherever possible.
2. Design must be as simple & economics as possible.
3. Design must be comply with all current safety & ergonomic requirements.
4. Design must provide for controlled & damage free handling of product.
5. Adequate error proofing provision must be incorporated into each design by proving proximity switches, rough locators, etc.
6. The weight of the moving parts must be kept to a minimum while maintaining maximum strength.
7. Frames & structures are to be simple & study.
8. Design clearance & accessibility for routine maintenance & service.
9. Motion control must be considered on any moving equipments.
10. Designer is responsible to validate clamps & weld guns.
Question No.10 – What do you understand by structuring a design tree? How does it reduce errors during the design process?
Structuring A Design Tree: Structuring a design tree implies to process where all the assemblies & parts are named in a specific standard. Different customers have a different set of standards to structure a design tree.
It is an important process that helps us to identify a specific part or assembly as to which project, tool/unit, it belongs to.
This helps us to avoid errors during design, manufacturing, assembly, inspection, etc.
If the parts or assemblies are not named properly or the design tree is not structured properly, it will create confusion to understand the design & may create major possibilities of making an error.
The naming of a fixture or a unit or a part gives the information as to which project or zone or assembly do they belong.
It can help us to identify the number of items of the same types or different types that are being used in the assembly.
While start designing a fixture, the first unit will be the base unit.
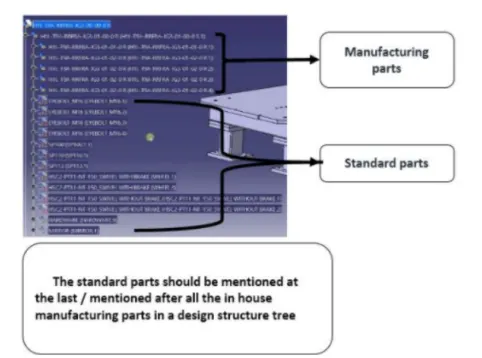
In the structure tree, all the manufacturing parts should be first and the standard parts should be at the last.
A structure tree helps to study or understand the parts in the assemblies easily.
Steps to structuring a design tree:
Step 1: Create new à Product à click OK (by clicking ok now you will enter into a product window)
Step 2: Then right click product in a structure tree à go to properties à rename in part number (As we created a product we have to mention the total assembly
name of the fixture) à click ok.
The naming of the assemblies / parts / units have certain standard procedures, which I have clearly explained below.
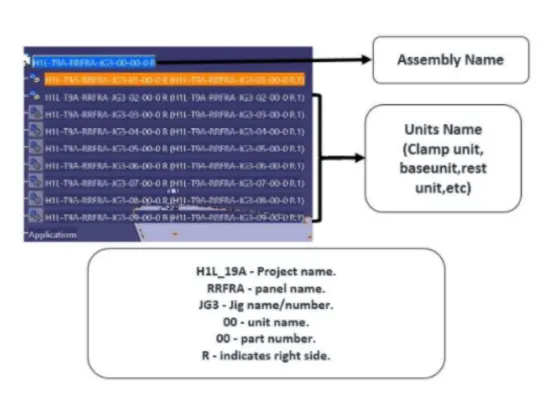
The product name is title of the fixture. The renamed titled should be à P001_Z03_ST09_00_00_R
P001 – represent the project name.
Z03 – Zone name.
Panel name will also be mentioned in some case.
ST 09 – Station name / J03 – Jig name will be mention sometimes.
00 – unit name.
00 – Part number.
R/L – is representing the right hand side / left hand side of the panel.
The other renamed title explained in video is
H1L_19A_RRFRA_JG3_00_00_R.
H1L_19A – Project name.
RRFRA – Panel name.
JG3 – Jig name/number.
00 – unit name
00 – Part number.
R – Indicates right side.
Question No. 11 – What is units? Mention 5 types of units?
A unit is a device that has a specified function, especially one forming part of a complex mechanism.
A welding fixture is an assembly of different types of units.
SIDE, FIXED , BASE, BUMPED,REST units