Week 11 - Final project
AIM:
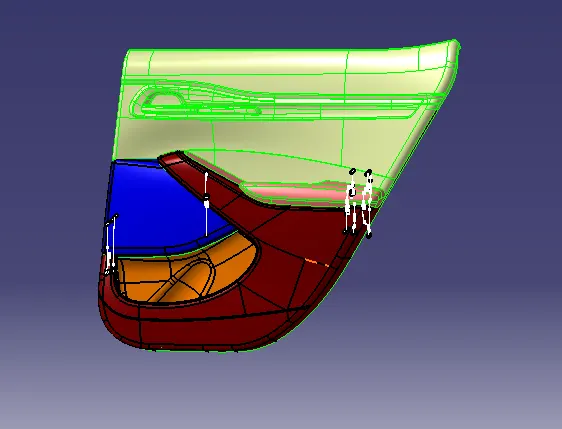
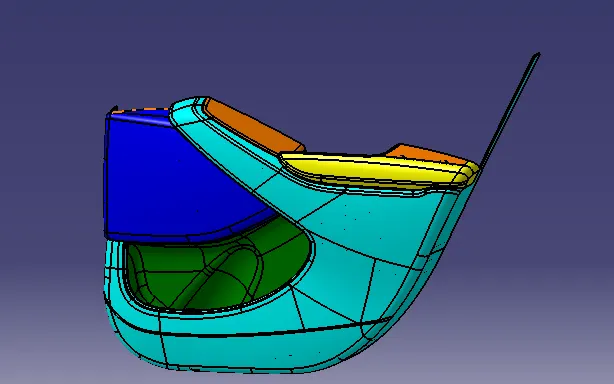
To create a CAD model considering the OEM standards from the Class-A surface of a Door Panel.
INPUT CLASS A SURFACE:
INTRODUCTION:
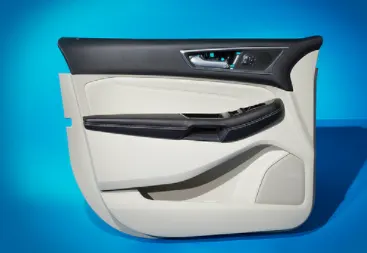
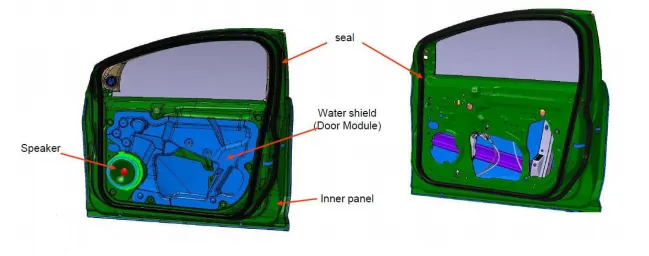
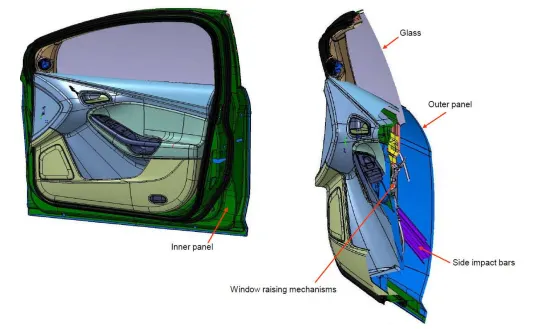
Door panels serve as an interface between the interior of the car and the inner workings of the door, and between vehicle occupants and the door. They are expected to meet a variety of design specifications regarding safety, aesthetics, and functionality. In addition, they are expected to continue the material theme of the dashboard and pillars while concealing intricate electrical and mechanical components for operating locks, windows, and other features. The door panel has evolved from a simple two-part system of latch and simple winding mechanism to a more sophisticated enclosure. Doors currently have an inner full-width panel consisting of electronic windows, central locking system, and speakers. These panels typically consist of a foamed core covered with either textiles or plastics.
Overview of Door Trim Panel:
Class-A Surface:
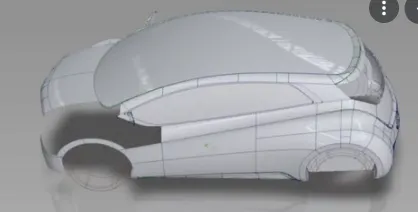
A-class surfaces are those aesthetic/ free form surfaces, which are visible to us (interior/exterior), having an optimal aesthetic shape and high surface quality. Mathematically class-A surfaces are those surfaces which are curvature continuous while providing the simplest mathematical representation needed for the desired shape/form and does not have any undesirable waviness. Products are not only designed considering the functionality but special consideration is given to its form/aesthetics which can bring a desire in one’s mind to own that product. This is only possible with high-class finish and good forms. This is the reason why in design industries Class-A surfaces are given more importance. In automotive design, a class-A surface is any of a set of freeform surfaces of high efficiency and quality.
Although, strictly, it is nothing more than saying the surfaces have curvature and tangency alignment – to ideal aesthetical reflection quality, many people interpret class A surfaces to have G2 (or even G3) curvature continuity to one another (see free form surface modelling). Class A surfacing is done using computer-aided industrial design applications. Class-A surface modellers are also called "digital sculptors" in the industry. Industrial designers develop their design styling through the A-Surface, the physical surface the end user can feel, touch, see etc.
Class-B surface:
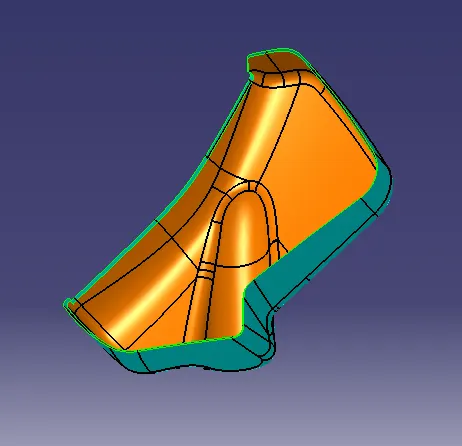
Class-B surfaces are the secondary surfaces that can be seen sometimes, but are less important, such as the
inside of your glovebox, ash tray, etc. These must be smooth and "error-free" as well, but are not held to the
standards that class-A surfaces are.
Class-C surface:
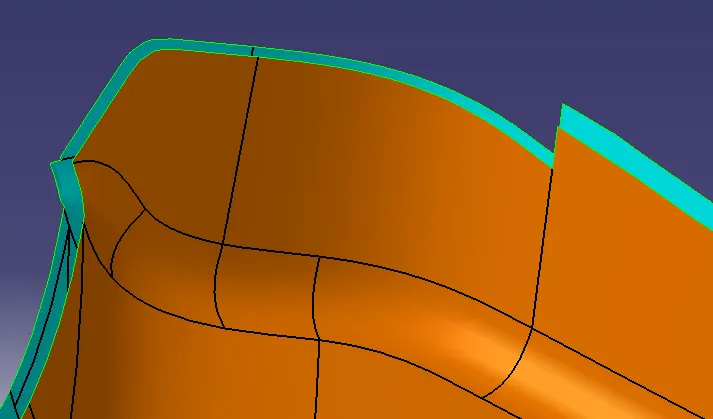
Class C surfaces are the backside surfaces that can have tool marks, flash and other imperfections without hurting appearance, function, etc.
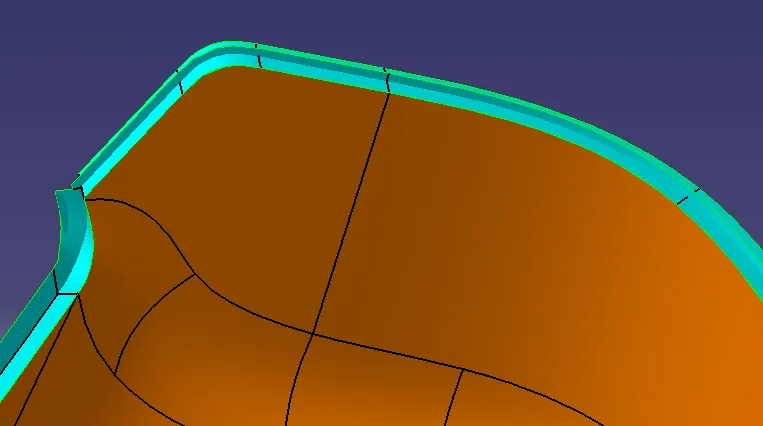
Plastic Part:
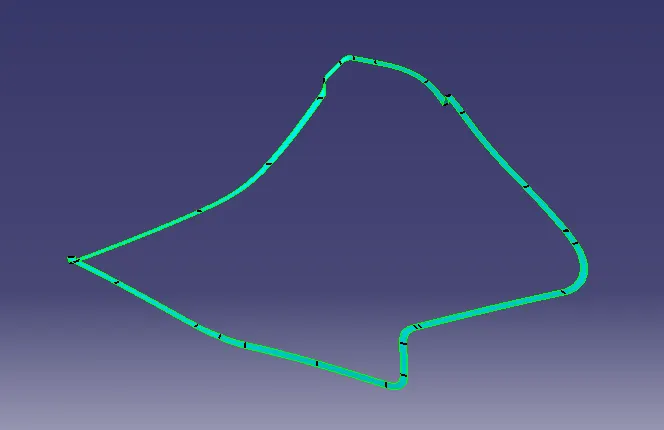
When designing parts for injection molding the manufacturing process is an important consideration.Injection
molding is a process in which solid thermoplastic resin pellets are melted, injected into a mold, and then cooled back to a solid state in a new form. During both the injection and cooling stages of the manufacturing process,there are several factors that may affect the quality of the final product and the repeatability of the manufacturing process. Although it is not always possible to follow all recommendations, outlined on the following pages are some of the most fundamental guidelines when designing parts for injection molding.
Injection Molding Materials:
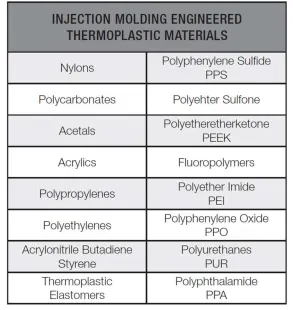
Materials Selection: Many types of thermoplastic materials are available. Selection depends on the specific
application. The chart below shows some of the most common materials being used.
Theory:
Ribs:
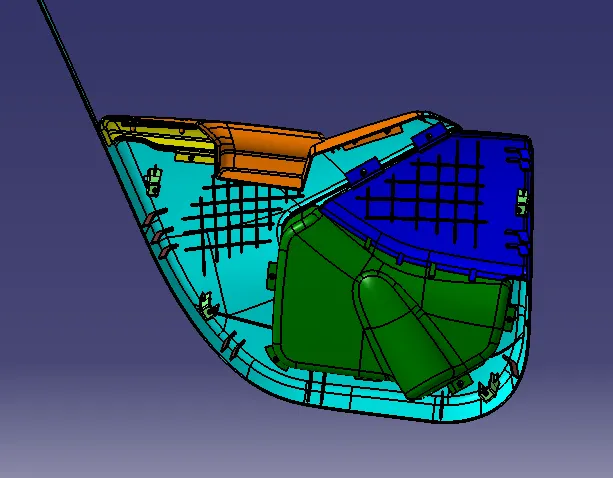
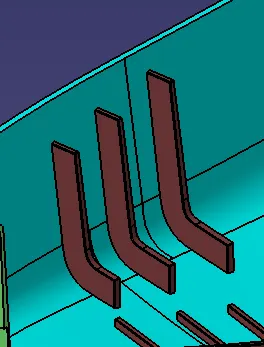
Ribs are reinforcements,ususally thin, wall-like features added to the part to add internal support to walls or other features like bosses. In a similar fashion, gussets are support features that reinforce areas such as walls or bosses to the floor. Ribs provide stiffness and strength in molded parts without disturbing the thickness. They also help in Locating & arresting components of an assembly, Providing alignment in mating parts, Acting as stops or guides for mechanisms.
A well-designed rib will overcome the disadvantages like Increasing part weight and cost,Production cycle time required and appearnce of sink marks.
Ribs are also used as Covers, cabinets and body components with long, wide surfaces. They are also used as Frames and supports.
Ribs design features 5 main criticalities:
1. Thickness.
2. Height.
3. Location.
4. Quantity.
5. Manufacturability.
1) Rib Thickness:
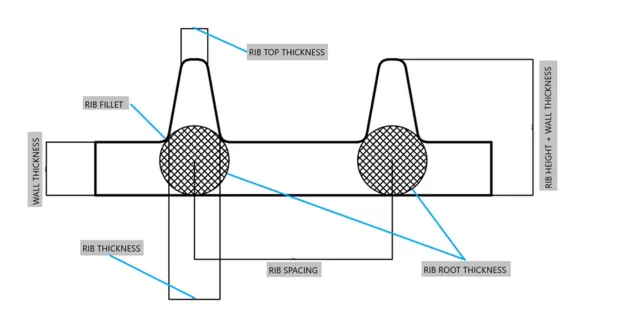
Ribs should be designed to be 50-60 percent of the nominal wall thickness. Thicker ribs are more prone to create sink marks on surfaces.Rib Thickness should be 0.5 * Wall Thickness and the Top part of the Rib should have a thickness of 0.75mm minimum.
2)Rib height:
Rib height is nominally supposed should be 5 times the wall thickness.Taller Ribs can cause problems during producton as unfill can happen.Rib Height= 5 * Wall Thickness.
3)Rib spacing: Ribs should be placed at a distance atleast twice the wall thickness.Rib Height/Rib width ratio = 3:1 –steel.
Rib Height/Rib width ratio = 2:1 –preferred
4)Rib draft:
A minimum of 0.5-degrees draft is sugested to ensure proper ejecton of the part.Rib draft = 0.5 to 1 degree.
5)Rib fillet:
Fillets are used at feature intersections to increase rib strength.Typically,Rib fillet = 0.125 * Wall Thickness.
6)Rib Root Thickness:
It is the thickness at the intersection of the Rib and Wall of the plastic component.Typically,Rib Root Thickness = (0.3 to 0.5) * Wall Thickness
Boss:
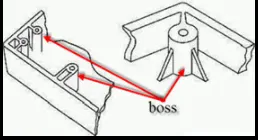
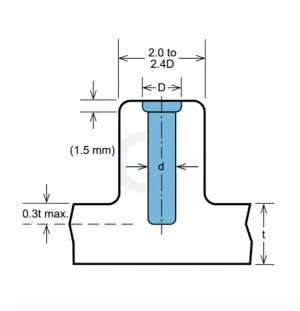
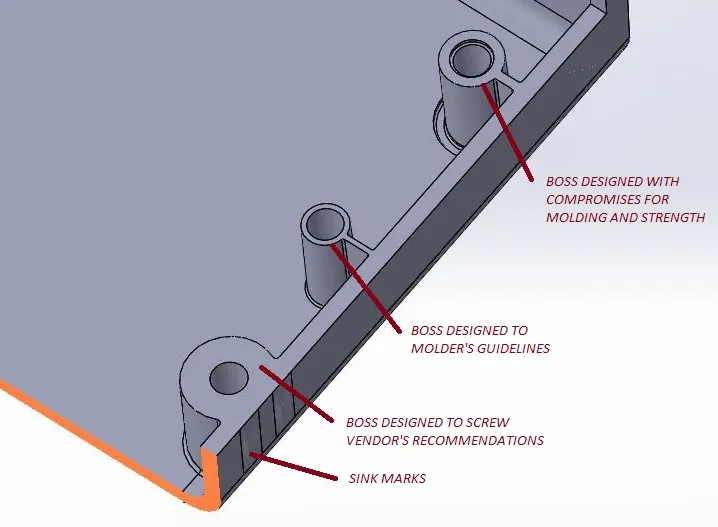
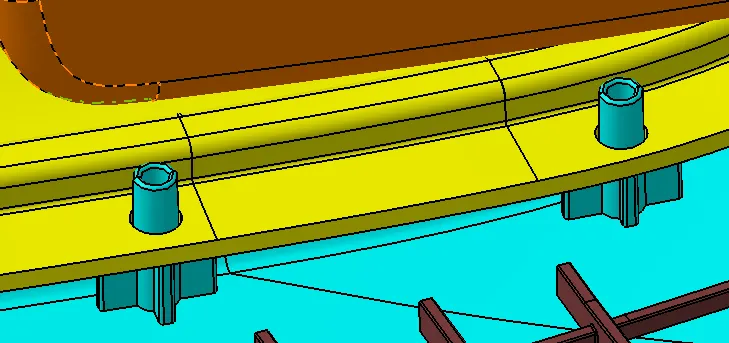
Bosses are used to facilitate the registration of mating parts, for attaching fasteners such as screws, or for accepting threaded inserts.Wall thicknesses for bosses should be less than 60 percent of the nominal wall to minimize sinking. However, if the boss is not in a visible area, then the wall thickness can be increased to allow for increased stresses imposed by self-tapping screws.
The base radius should be a minimum of 0.25 X thickness. Bosses can be strengthened by attaching gussets. At the base or by using connecting ribs attaching to nearby walls.
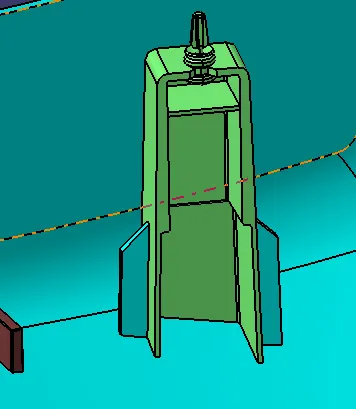
Dog House:
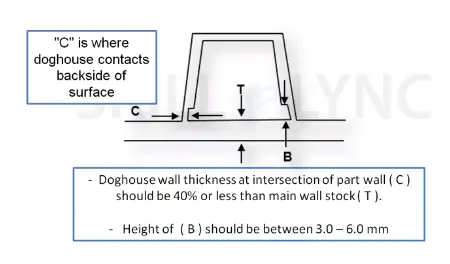
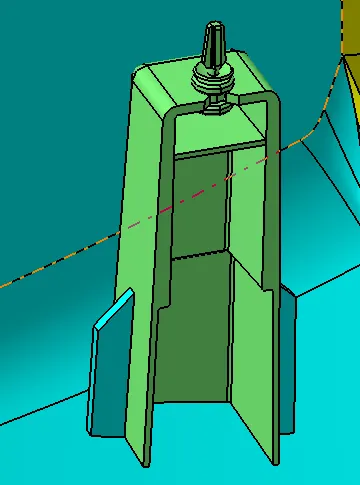
Dog house is an engineering feature used in plastic trim design. Dog houses are used as supporting features.
Sometimes other engineering features like snaps; locators etc. are mounted on them to increase their strength. Dog houses are subjected to draft analysis to prevent breakage of the component during ejection from mould cavity. Dog house and other engineering components are built on a B-surface. Dog houses are used as supporting feature. Dog houses are subjected to draft analysis to prevent breakage of the
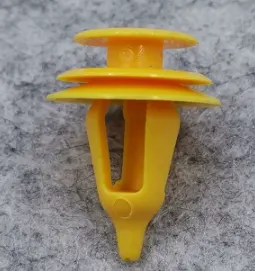
component during ejection from mould cavity. Dog house and other engineering components are built on a B-surface. Dog houses keeps hold of Push pin clips that are mounted on them to snap the mating parts.
Heat Stakes:
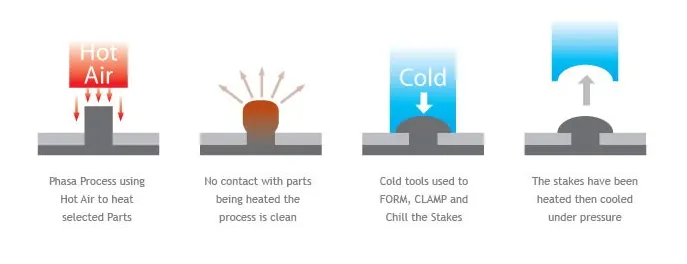
Heat staking process is described as a pulsed heat process used to join two or more parts out of which at least one is made of plastic, heat staking involves deforming the plastic material using heat and force at a set process time. The bond is made by partly de-forming the plastic part to fix the other. Therefore, the process makes it easy to bond metal to plastic, which is why it is commonly used in high volume/low cost applications like automotive, IT and consumer appliances.
Locators:
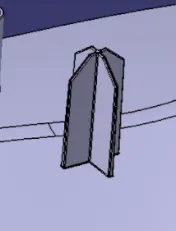
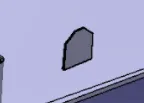
Locators are those features that locate 2 mating parts during assembly. Locators are fixed to the Base part and the mating part is inserted through the Locator. These locators also help in resisting the DOF of a part, Hence making he part motionless in the desired way.
There are 2 types of locators used commonly. 2 way locators and 4 way locators.These two locators are helpful in their own way to locate and resist the DOF.
Design Procedure:
At first, The given Input Class A surface is split into the different parts of Door,such as:
1) Lower Subtrate
2) Map Pocket
3) Bottle Holder
4) Arm Rest
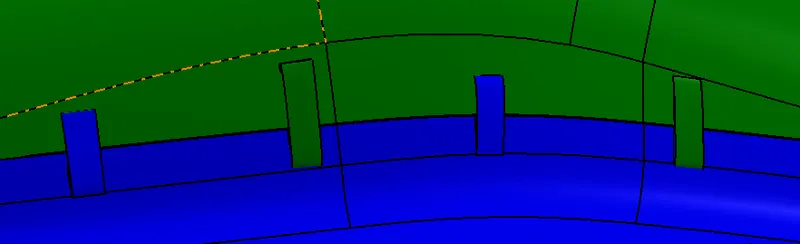
These class A sufaces are put in seperate Geometrical sets and are worked upon one by one. Class B surfaces are generated. Class C surfaces are generated wrt the Tooling Axis and a respective draft angles are given. B side Engineering features such as Heat Stakes, Ribs, Dog Houses, Push Pins and Flanges are made are required places.
Result:
Hence the given Class A surface is converted into an Industrial standard Door of an Automotive.