Week 11 - Final project
Aim: Is to Design a Car door Plastic components placed in the car door panel by following the design standards used in the Industries. The Reference Designs for the Mechanical designing team of the Plastic components are drawn initially by the Class A surface defined by the Concept Sketch team as well as by the Styling Class A using Alios software and in reference to Class A the Part Body with thickness is designed by the Designing Team.
Factors to consider before choosing a material for the component, they are
- Ease of manufacture.
- Cost effectiveness.
- Material Physical and mechanical properties.
- Is of availability in the society.
- Suitability to the surrounding change of environment.
- Reliability.
- Easy to handle.
- Eco friendly.
Types of Plastic:
Thermoset Plastic: Thermoset type of plastics are the plastics which are non-usable once it is moulded to the required shape, if it is reheated to transform into a new plastic product is impossible and it becomes irregular in the form of shape and properties. Example - Bakelite which is used as an sausage handle which is black in colour, Trolley wheels, Polyester, epoxy resin etc
Thermoplastic: Thermoplastic is the type of plastic which is used and recycled to transform into a new product without affecting its properties. Thermo means temperature where the plastic is heated every time to change into a new product. Example - Low density and high-density Polyethylene type of plastic commonly known as grocery bags, nylon, PVC etc.
Advantages and Disadvantages of Thermoset type of Plastic,
Advantages:
- Is hard as concrete where Set (like concrete) meant to say it is Rigid material.
- Is having higher the melting point as compared to thermoset.
- Is used in Handles of Sause pan, Epoxy is used as resin, Polyester for Clothing.
- Will not change its shape as per the change in the surrounding environment.
- Non-corrosive.
- Non-toxic while in use.
- Cost effective.
- Thickness of material can vary from minimum to maximum.
Disadvantages:
- It will not revert back to its original shape if it cannot be molded to new shape once it heated beyond its melting temperature.
- They cannot be molded to very small thickness whereas used in grocery bags.
- Brittle material where it will break to high load.
- toxic when it is heated to melt into paste.
Pros of Thermoplastic.
- The thermoplastic products are reverted back to new products with new shapes and same material properties by melting beyond its melting point temperature.
- The thermoplastic material is with low melting point temperture compared to Thermoset type pf material.
- Low density and high density type of plastic products are used for grocery, packaging plastic materials, containers, Nylon as ropes, PVC for pipes.
- Fast processing
- No chemical reactions occur during application processing.
- Resists Humidity and other harsh environments.
Cons of Thermoplastic,
- Limited serve temperature performance.
- It tends to form weaker adhesive bonds.
The Following Methods used to Produce Plastics:
Thermoset Type Plastic:
- In general, thermoset products are made through liquid molding processes.
- The polymers and other agents are fed into tanks or barrels, where they are heated to a liquid state and mixed. Then the liquid polymers and other agents are injected into a mold cavity.
- As the material cools and hardens to the configuration of the cavity, it goes through a curing process where the polymers cross-link together.
- That process forms an irreversible chemical bond that prevents the risk of melting, softening, or warping when or if the finished product is subjected to high heat or corrosive environments. This makes thermosets perfect for high-heat applications and outdoor use.
There are two primary liquid molding processes used to produce thermoset plastics:
- Reaction Injection Molding.
- Resin Transfer molding.
Thermoplastic:
- Thermoplastic sheets are manufactured from raw materials, including polymer resins, colorants, and additives, depending on the specific formulation required.
- Raw materials are blended to exacting standards to ensure uniformity throughout the batch and consistency between batches.
- Once the raw materials are blended, they are heated, pressed through an extrusion die, and drawn into a sheet through a set of rollers. While the sheet is still warm, it passes through additional roller sets to reach the desired thickness and specified surface texture.
- As the sheet travels down the line, it cools and is cut to size. This process ensures dimensional stability and a uniform thermoplastic sheet.
Thermoplastics are characterized by their pliability above a specific temperature, and ability to re-solidify upon cooling. This allows them to be easily shaped and molded without changing the properties of the thermoplastic material.
Types of Thermoplastic:
Thermoplastic material classified as polypropylene, polyethylene, polyvinylchloride, polystyrene, polyethylene terephthalate and polycarbonate.
- Acrylonitrile butadiene styrene (ABS) is a thermoplastic used to manufacture:
- Sports equipment.
- Toys (for example LEGO® blocks).
- Various automobile parts
- Polycarbonate is used to make:
- CDs and DVDs.
- Drinking bottles
- Food storage containers
- Eyeglass lenses.
- Polyethylene is probably the most common thermoplastic and is used to make:
- Shampoo bottles.
- Plastic grocery bags.
- Bullet-proof vests
- Polypropylene is used to make:
- Fibre for yarn and fabric.
- Film for packaging or many other shapes.
Types of Thermoset Plastic:
Thermoset type of Plastic, they are
- Epoxy resin.
- Polyester resin.
- Glass reinforced type of plastic.
- Carbon fibre plastic.
- Melamine Formaldehyde.
- Silicones
- phenolic
- Alkyd
ABS:
ABS stands for Acrylonitrile Butadiene Styrene,
Acrylonitrile - This component contributes to ABS chemical resistance & heat stability
Butadiene: This component delivers toughness & impact strength to ABS polymer
Styrene: It provides rigidity & processability to ABS plastic.
Overall:
- High rigidity
- Good impact resistance, even at low temperatures
- Good insulating properties
- Good weldability
- Good abrasion and strain resistance
- High dimensional stability (Mechanically strong and stable over time)
- High surface brightness and excellent surface aspect
Plastic Components used generally in Automobiles:
These engineering polymers are thermoplastics, and they have good chemical and temperature resistance; provide strength, toughness, and stiffness and resist wear and abrasion.
Parts in Automobile industries they use Nylon as material are,
Manifolds
Fuel pipes
Nylon Clay hybrid (NCH) which provide barrier against vapor emission.
Door and tailgate handles.
Exterior mirrors.
Front-end grilles. Fuel caps and lids.
Wheel covers and trim.
Nylon fibers are exceptionally strong and elastic and stronger than polyester fibers. The fibers have excellent toughness, abrasion resistance, and are easy to wash, and to dye in a wide range of colors. The filament yarns provide a smooth, soft, and lightweight fabric of high resilience.
Filler:
Filler materials are particles added to resin or binders (Plastics, composites, concrete) that can improve specific properties, make the product cheaper, or a mixture of both. The two largest segments for filler material use is elastomers and plastics.
Fillers with properties:
- Calcium carbonate (CaCO3): It. brings for final plastic products brighter and glossier surface.
- Kaolin: Is mainly used in plastics for its anti-blocking characteristics as well as an infrared absorber in laser marking. It increases impact strength and heat resistance.
- Wollastonite (CaSiO3): This filler can improve moisture content, wear resistance, thermal stability, and high di-electric strength.
- Glass: Glass fibers are used to increase the mechanical properties of the thermoplastic or thermoset such as flexural modulus and tensile strength.
Additives: A substance added to something in small quantities to improve or preserve it.
The most common polymer additives are stabilizers, plasticizers, lubricants and flame retardants.
- Stabilizers are added to prolong the useful life of a polymer formulation by protecting it from thermal and light-assisted oxidation.
- Plasticizers: Plasticizers are additives used in the production of plastics to reduce the attraction between polymer chains, thereby increasing the flexibility and durability of the resulting plastic. The most common Plasticizers are phthalate esters, which are used primarily in the manufacturing of products made from PVC, including shower curtains, upholstery, flooring, and food containers.
- Lubricants are the substances, which work between surfaces in relative motion to prevent friction and wear
- Flame retardants are chemicals that are applied to materials to prevent the start or slow the growth of fire.
Materials Used in Automobile with respect to the Components:
The 10 Automotive interior components and the materials used are,
- Truck trim - Steel.
- trunk - Steel
- door panels - Fibre
- Instrument panel - Acrylonitrile-butadiene-styrene (ABS), ABS/polycarbonate alloys, polycarbonates, polypropylene, modified polyphenylene ether (PPE) and SMA (styrene-maleic anhydride) resins
- Glove box - Stainless steel, Carbon fibre, polycarbonates, polypropylene
- center console - Carbon fibre
- Headliner - tricot knit fabric
- Ac register - Polyurethane and phenolic insulation panels.
- SOS switch - Bakelite and Ebonite
- Control knob - Stainless steel
The 10 Automotive Exterior components and the materials used are,
- Spoilers - Is made from ABS plastic, which is mixed with granular fillers to make the spoiler stiffer.
- Automotive lighting - Acrylonitrile-butadiene-styrene (ABS), polycarbonates, polypropylene.
- Bumper - Steel, fiberglass composite, plastic or aluminium
- Wheel arch - fibrous layer comprising of thermoplastic bicomponent filaments
- A pillar - Steel, Aluminium.
- Cover wheel bright work - High-grade sheepskin fabric.
- Silencer - Stainless Steel
- Protector - Stainless steel.
- Wheel trim - zinc coated steel with a hardness of 40 HRC
- Wiper - Blade of Aluminium and attached with rubber.
There are 5 types of thermoplastic molding, they are
- Extrusion moulding: The extrusion moulding, hot melted plastic is pressed through a shaped hole to create a lengthy shaped plastic part. This customizable shape that the liquid plastic gets pressed through is called a die. This die is custom made for the particular outcome that is desired. It is almost like pressing dough through a press to make shaped cookies. The other forms of plastic moulding also use extrusion so get the raw liquid into the moulds, the difference here is that other methods use the moulds to make the desired shape and here the extrusion itself is making the shape with the use of the die’s shape.
- Compression molding: This method involves the raw liquid plastic being poured into a heated mould and then being compressed together to form the desired shape. The high temperature of the entire process ensures good strength in the final product. The process is finished off by cooling the liquid plastic so that it keeps its form before being trimmed and removed from the mould.
- Blow modling: With blow moulding, the custom plastic parts come out hollow and thin walled. This method is ideal for when the plastic part must have uniform wall thickness. This is very similar to the process of glass blowing. The machine heats up the raw plastic until it becomes liquid and then injects air into it like a balloon. The plastic is blown into a shaped mould and as it gets bigger it presses against the mould walls and it starts to take its shape. After the liquid balloon fills the mould it is cooled to keep its shape. The process is very fast and can produce up to 1400 pieces in a 12-hour work day.
- Injection Moulding: Injection Moulding is fairly similar to extrusion moulding. The difference here is that with injection moulding the melted plastic is injected directly into a custom mould. The injection is under high pressure so that the mould is filled, and a solid part is made. As with the other methods, after the mould is filled, the plastic is cooled as to keep its new shape and then the mould is opened.
- Rotational molding: This method involves the resin or liquid being placed inside the mould and then being rotated at high speeds. The liquid then evenly covers the entire surface of the mould to create a hollowed part with all the walls evenly thick. After the mould is cooled and the liquid plastic has taken its new form it is then taken out of the mould.
Project:
Class A surface:
Class A surface refers to those surfaces which are VISIBLE and abide to the physical meaning, in a product. This classification is primarily used in the automotive and increasingly in consumer goods.
Class A surface of Car Door panel:
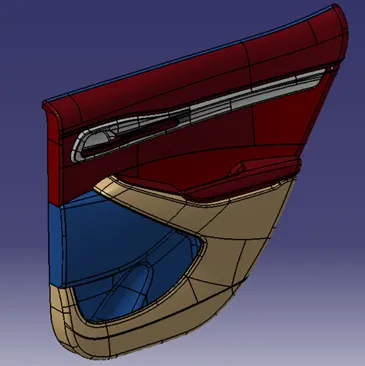 figure 1
The Class A surfaces of Car door Plastic components from the Styling team used are,
- Lower substrate.
- Arm rest.
- Mat Pocket.
- Lower Substrate:
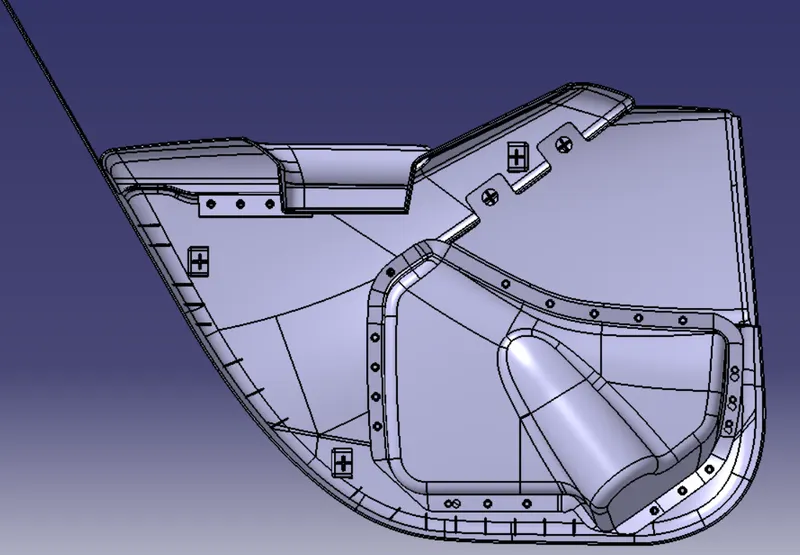
- The Lower substrate portions from the Class A surface (as shown in figure 1) is extracted by the extract command as shown in figure 2.
- The extracted Class A surfaces are Joined by using Join Command to pile up the pieces into a single surface body. As shown in figure 3.
- Observe the defects in the Class A surface once after it is Joined into a single surface body, the damaged portions need to be repaired by using the required surface workbench commands and by using Boundary command observe the open brackets in the Joined surface body i.e Class A, if the boundary is defined only at the boundary of the Class A then it is a damage free Surface as shown in figure 4.
- The Class C surface is Swept in the required directions from the boundary of the Class A using Sweep command and where,
Profile Type – Line
Subtype – Either “With Reference surface” or the “With draft direction”.
Angular Degree between the Class C surface with respect to the Boundary should be 3o and
Length of Class C surface should be more than the Actual thickness between the Class A and B as shown in figure 5.
- The Class B surface is attained by Offsetting the Class A surface to 2mm (in case of Plastic Components) by using Offset Command as shown in figure 6.
- Then the Class A surface is trimmed or joined with Class C surface to be a single surface body called as “Joined Class C surface with Class A” as shown in figure 7.
- Unhide the Class B surface in orange colour as shown in figure 8.
- The Class B surface in Orange colour is joined with “Joined Class C surface with Class A” surface body by using trim command to trim off the unwanted extra surfaces from the boundary of Class B as shown in figure 9.
- Then we obtain a closed Surface body and in order to check whether the surface body is closed or not, use Boundary command and select the Body if the Pop-up message appears saying “the selected body is closed, and it has no boundary” then it is a closed surface body and if there are any open space available in the body then Popup message will not appear as shown in figure 10.
- Then Change the workbench from “Generative Shape Design” to “Part Body” to create the Solid Part Body using the Closed Surface Command as shown in figure 11.
- The Heat stakes are created on the Solid Lower substrate to join the dissimilar material either it can be a metal or the Plastic component or any other material and usually the Heat stakes are created on the Thermoplastic component. Whenever two or more components need to be attached to one another, and at least one is made of a thermoplastic, a combination of heat and pressure can be used to reform the plastic to the many shapes or profiles to retain or join the parts together as shown in figure 12.
- To avoid Sink marks on the 4- and 2-way locators, Doghouse is created on the Lower substrate solid body to join the neighbour part body which is of few distance apart. The Doghouse will avoid the sink marks on the Locators of length more than the limit and the doghouse will build a strength to the base of Locators as shown in figure13 and Locators and Doghouse are created by following design standards used for plastic components. Ribs not only avoids the Contraction of Plastic parts i.e, but Ribs also increases the fatigue life and gives strength to the Parts as well and they are designed by the following Standards as shown in figure 13.
- 4-way and 2-way locators with Doghouse is as shown in figure 14.
- The Following standards used for the Locators, Doghouse and Ribs is as follows,
- Doghouse guidelines:
Draft, Doghouse walls, Part surface, Bottom of Doghouse, Wall thickness and Height and width.
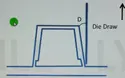
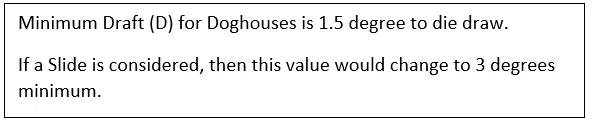
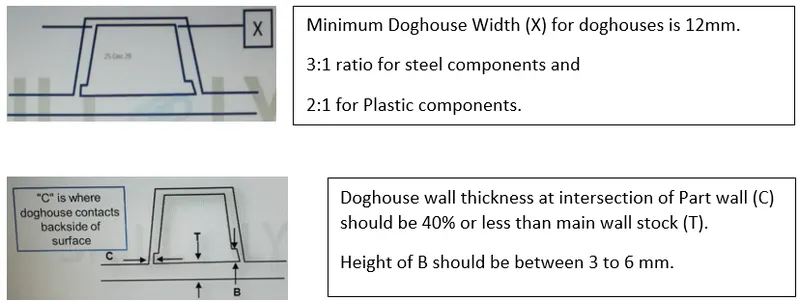
Rib: Ribs not only avoids the Contraction of Plastic parts i.e, but Ribs also increases the fatigue life and gives strength to the Parts as well.
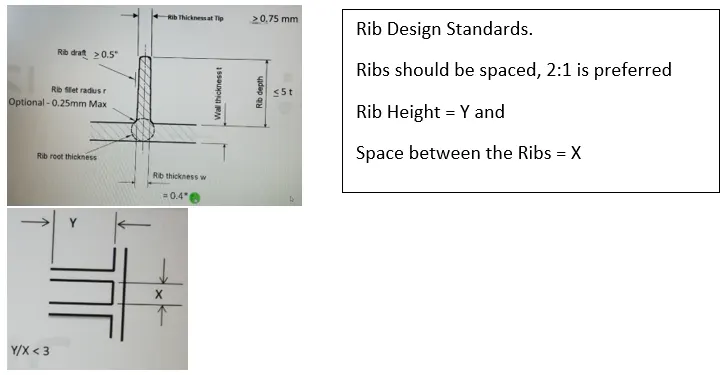
4-way Locator on Doghouse:
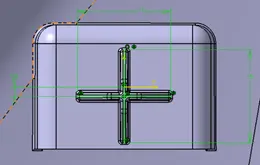
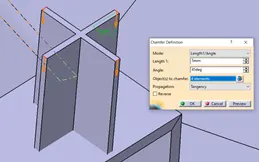
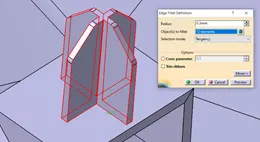
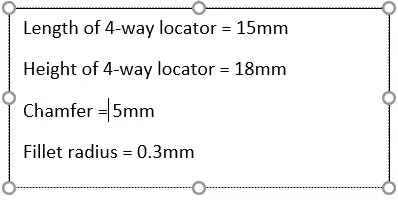
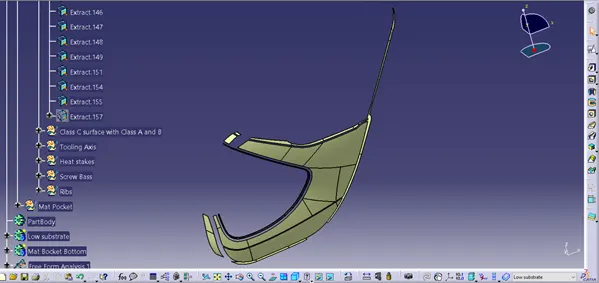
Figure 2: Extracted Surfaces in Pieces
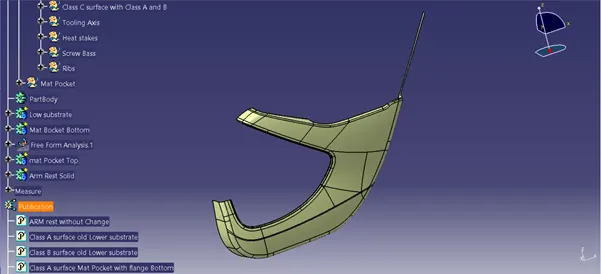
Figure 3: Joined by using Join Command
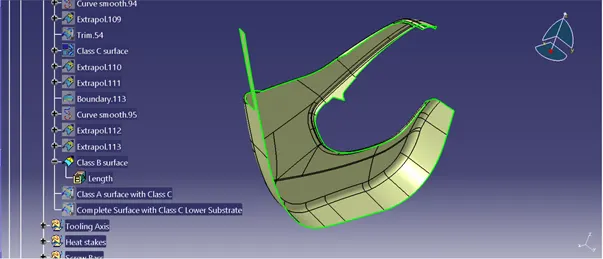
Figure 4: Using Boundary Command on Class A surface
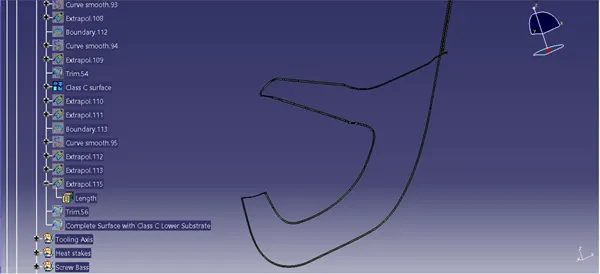
Figure 5: Class C surface
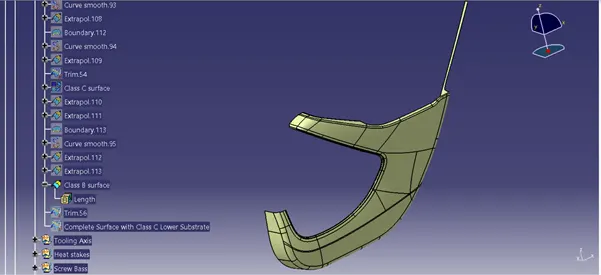
Figure 6: Class B surface by offsetting a Class A surface to 2mm
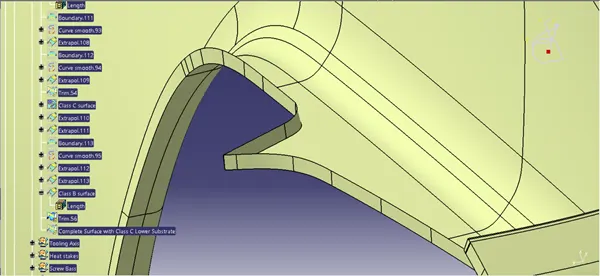
Figure 7: Class A surface is Joined by using Trim or Join Command
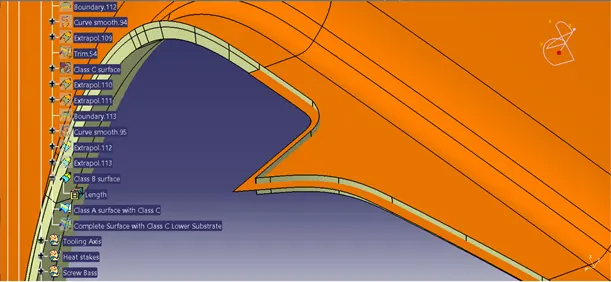
Figure 8: Class C and Class A surface with Class B(in orange colour)
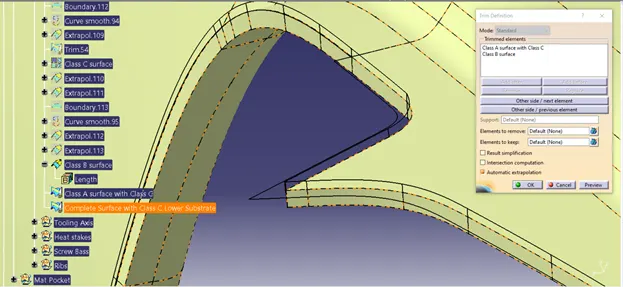
Figure 9: Class B is connected to surface with Class C and A using Trim command
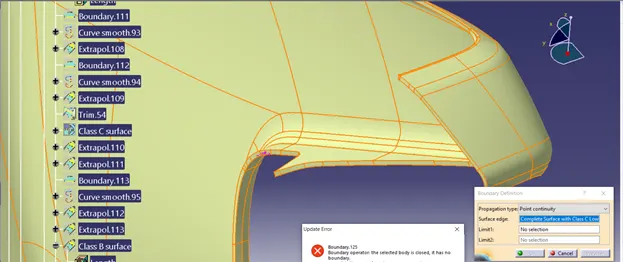
Figure 10: Closed surface
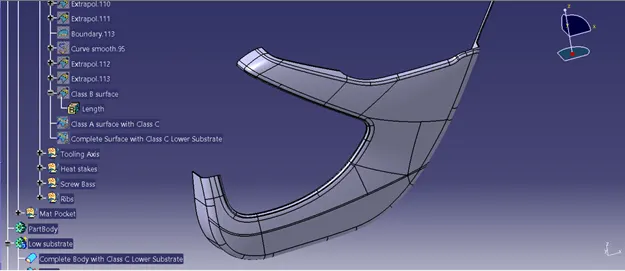
Figure 11: Solid Lower Substrate
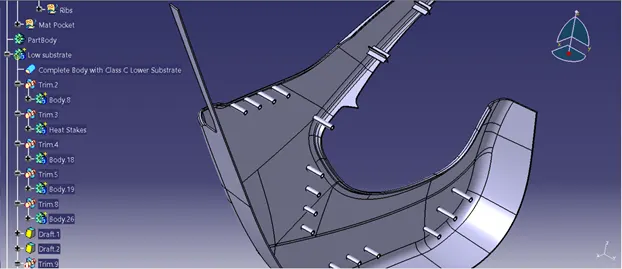
Figure 12: Heat stakes on Lower substrate
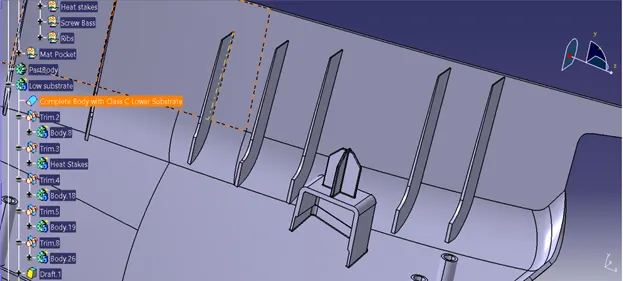
Figure 13: Ribs with Doghouse on lower substrate
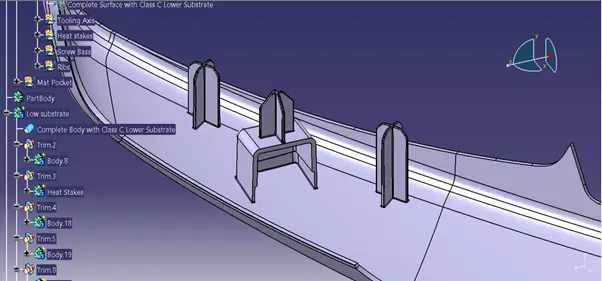
Figure 14: 4 – way locators and Doghouse on Lower substrate
- Arm Rest: A Feature provided on Car door Panel, to support a arm and is made up of Plastic.
- The Arm rest portions from the Class A surface (as shown in figure 1) is extracted by the extract command as shown in figure 15.
- The Arm rest portion is divided into two parts initially as part 1 and Part 2 in order to design the parts in an ease way.
- The extracted Class A surfaces are Joined by using Join Command to pile up the pieces into a single surface body. As shown in figure 16.
- Observe the defects in the Class A surface once after it is Joined into a single surface body, the damaged portions need to be repaired by using the required surface workbench commands and by using Boundary command observe the open brackets in the Joined surface body i.e Class A, if the boundary is defined only at the boundary of the Class A then it is a damage free Surface as shown in figure 17.
- The Class C surface is Swept in the required directions from the boundary of the Class A using Sweep command and where,
Profile Type – Line
Subtype – Either “With Reference surface” or the “With draft direction”.
Angular Degree between the Class C surface with respect to the Boundary should be 3o and
Length of Class C surface should be more than the Actual thickness between the Class A and B as shown in figure 18.
- The Class B surface is attained by Offsetting the Class A surface to 2mm (in case of Plastic Components) by using Offset Command as shown in figure 19.
- Then the Class A surface is trimmed or joined with Class C surface to be a single surface body called as “Joined Class C surface with Class A” as shown in figure 20.
- Unhide the Class B surface as shown in figure 21.
- The Class B surface is joined with “Joined Class C surface with Class A” surface body by using trim command to trim off the unwanted extra surfaces from the boundary of Class B as shown in figure 22.
- Then we obtain a closed Surface body and in order to check whether the surface body is closed or not, use Boundary command and select the Body if the Pop-up message appears saying “the selected body is closed, and it has no boundary” then it is a closed surface body and if there are any open space available in the body then Popup message will not appear as shown in figure 23.
- Follow the same procedure for Part 2 as well.
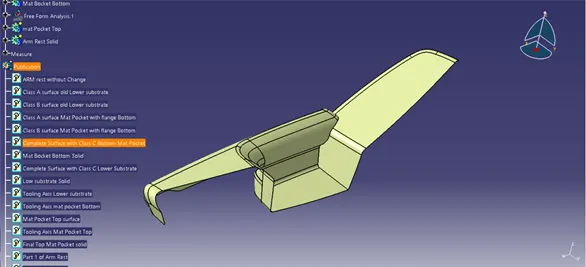
Figure 15: Extracted surfaces in Pieces
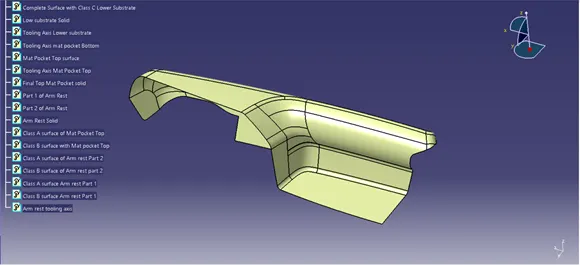
Figure 16: Class A surface
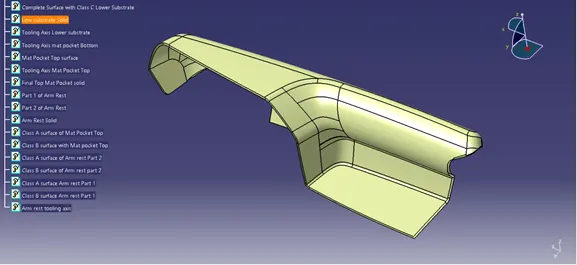
Figure 17: Class A surface (Bottom surface) and Class B surface (Top surface)
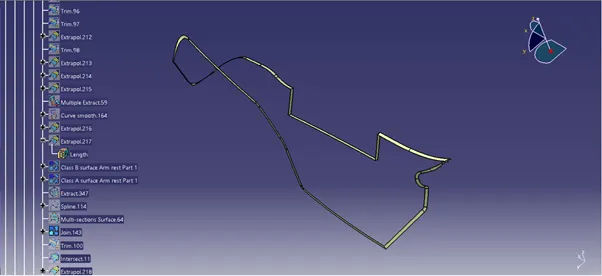
Figure 18: Class C surface defined from the boundaries of Class A
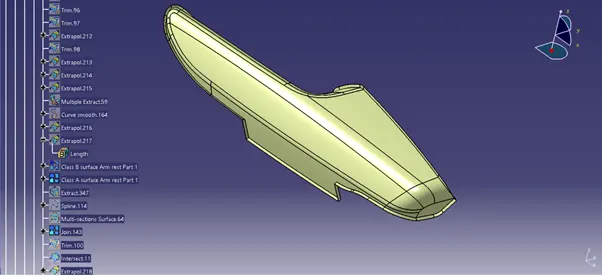
Figure 19: Class C surface joined to Class A surface using Trim command
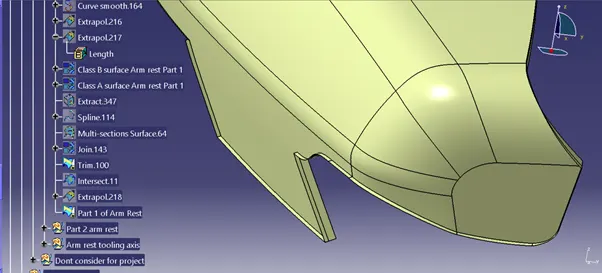
Figure 20: Class B boundaries are extrapolated beyond the Class C surface
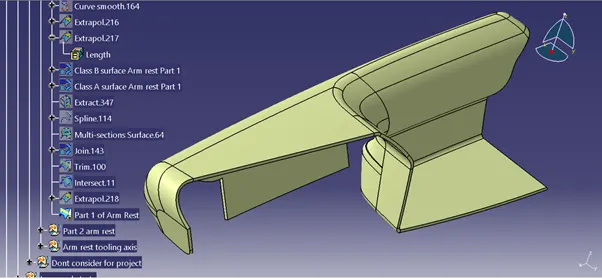
Figure 21: Closed surface
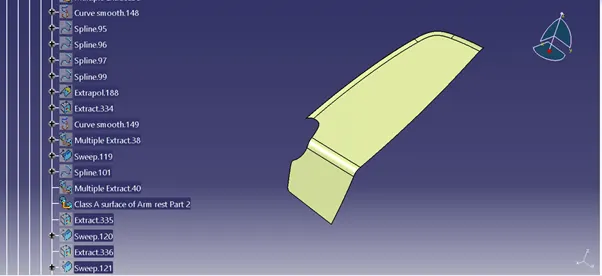
Figure 23: Class A surface
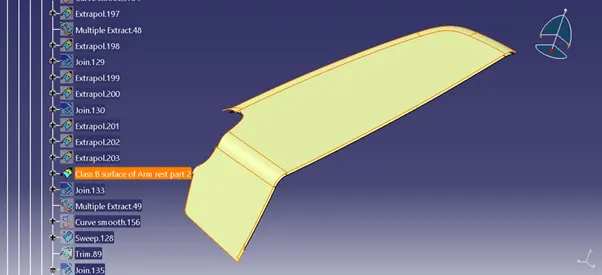
Figure 24: Class A surface (Bottom surface) and Class B surface (Top surface)
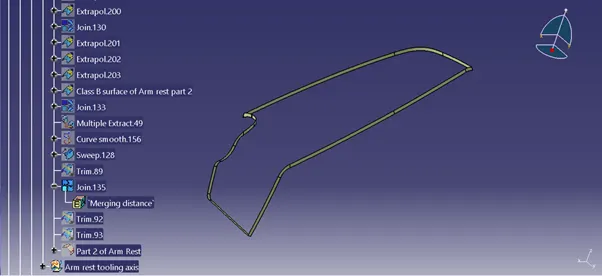
Figure 25: Class C surface defined from the boundaries of Class A
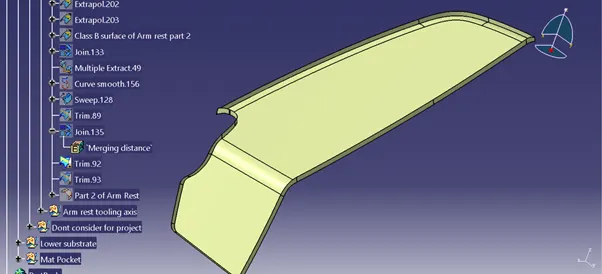
Figure 26: Class C surface joined to Class A surface using Trim command
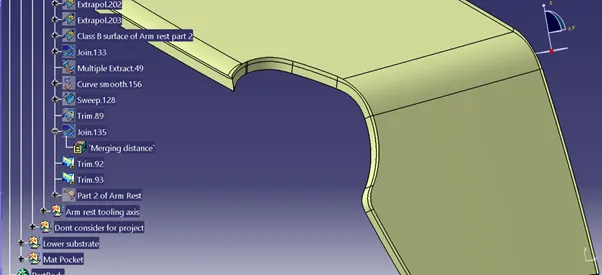
Figure 27: Class B boundaries are extrapolated beyond the Class C surface
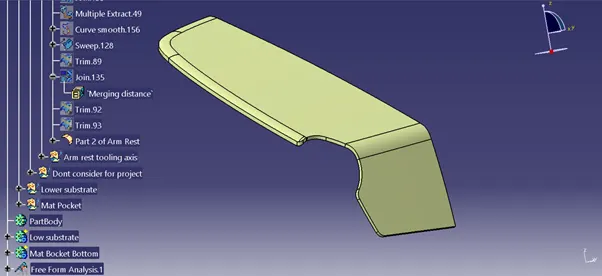
Figure 28: Closed surface
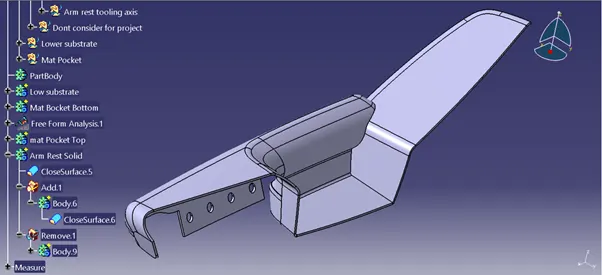
Figure 29: Part 1 and Part 2 solid body is connected with each other using Boolean operation and even the Heat Clearance drawn on the flange of Arm rest.
Mat Pocket: Is the Feature given in the Car door panel which helps to keep the things like water bottle, eatables or anything which suits inside.
- The Mat Pocket portions from the Class A surface (as shown in figure 1) is extracted by the extract command.
- The Mat Pocket portion is divided into two parts initially as part 1 and Part 2 in order to design the parts in an ease way as shown in figure 30.
- The extracted Class A surfaces are Joined by using Join Command to pile up the pieces into a single surface body. As shown in figure 31.
- Observe the defects in the Class A surface once after it is Joined into a single surface body, the damaged portions need to be repaired by using the required surface workbench commands and by using Boundary command observe the open brackets in the Joined surface body i.e Class A, if the boundary is defined only at the boundary of the Class A then it is a damage free Surface as shown in figure 31.
- Draw the Flanges on the Class A surface as shown in figure 32, where the flanges would provide space to create a Clearance Hole for the Heat stakes to pass into and also to join the Lower substrate with Mat Pocket Bottom Portion and in the other end Mat pocket Top and Bottom portions as well.
- Then the Flanges defined with respect to the surface of Class A is joined with Class A by using Trim command as shown in figure 33
- The Class C surface is Swept in the required directions from the boundary of the Class A flange using Sweep command and where,
Profile Type – Line
Subtype – Either “With Reference surface” or the “With draft direction”.
Angular Degree between the Class C surface with respect to the Boundary should be 3o and
Length of Class C surface should be more than the Actual thickness between the Class A and B as shown in figure 34.
- The Class C surface is then joined with Class A surface with Flange by using trim command as shown in figure 34.
- The Class B surface is attained by Offsetting the Class A surface to 2mm (in case of Plastic Components) by using Offset Command as shown in figure 35.
- The Class B surface is joined with “Joined Class C surface with Class A (from figure 33)” surface body by using trim command to trim off the unwanted extra surfaces from the boundary of Class B as shown in figure 36.
- Then we obtain a closed Surface body and in order to check whether the surface body is closed or not, use Boundary command and select the Body if the Pop-up message appears saying “the selected body is closed, and it has no boundary” then it is a closed surface body and if there are any open space available in the body then Popup message will not appear as shown in figure 37.
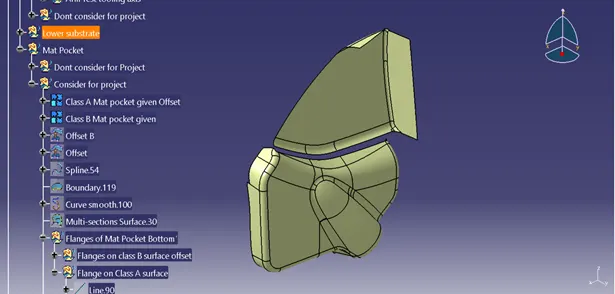
Figure 30: Mat Pocket Part 1(Bottom surface) and Part 2(Top surface)
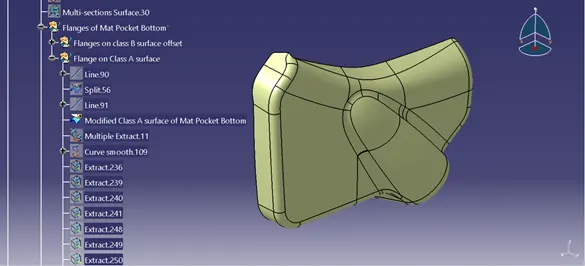
Figure 31: Mat Pocket Bottom Class A surface
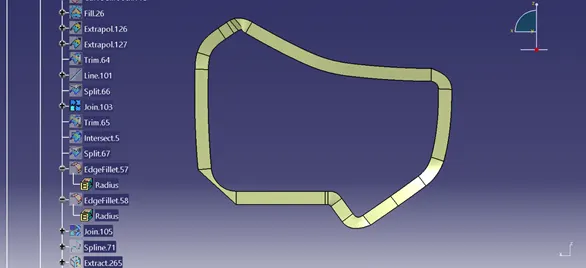
Figure 32: Flange created with respect to Class A surface
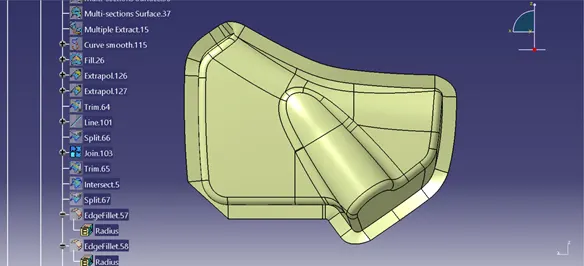
Figure 33: Flange is Joined with Class A surface using Trim command
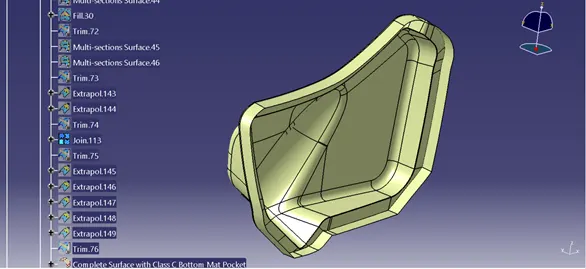
Figure 34: The Class C surface is drawn with respect to Flange and also connected using trim Command
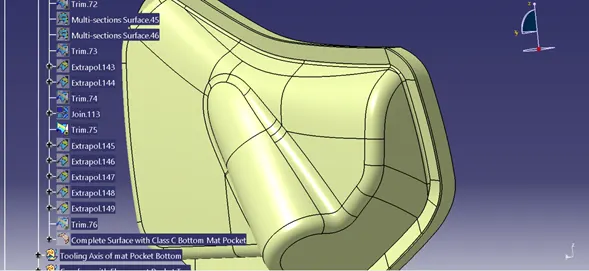
Figure 35: Unhide The Class B surface and extrapolate the boundary of Class b beyond Class C
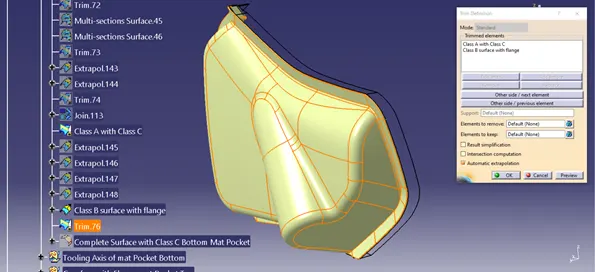
Figure 36: Trim the unwanted surface of Class B with respect to Class C surface
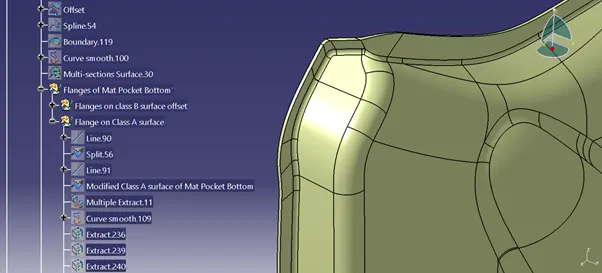
Figure 37: The Close surface
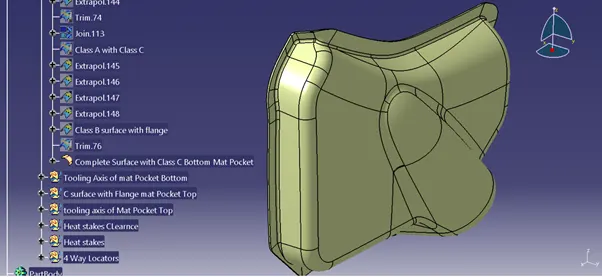
Figure 37: The Close surface
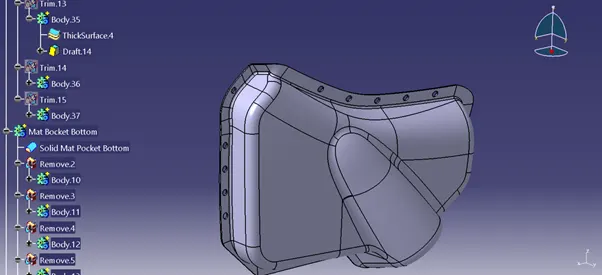
Figure 38: Solid Mat Pocket
Top Mat Pocket Portion:
Follow the same procedure as above, here the flanges are created directly on the Class A surface then offset the Class A to create a Class B surface. Refer figures from 39 – 45.
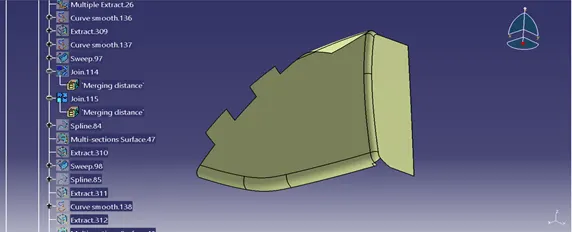
Figure 39: Mat Pocket Bottom Class A surface with Flange
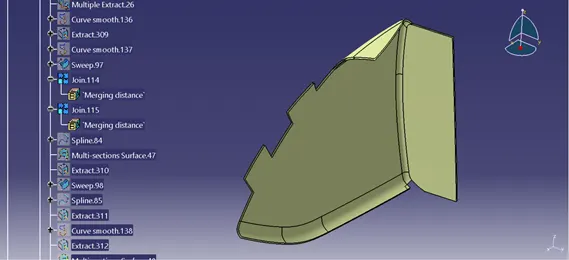
Figure 40: Class A and Class B surface
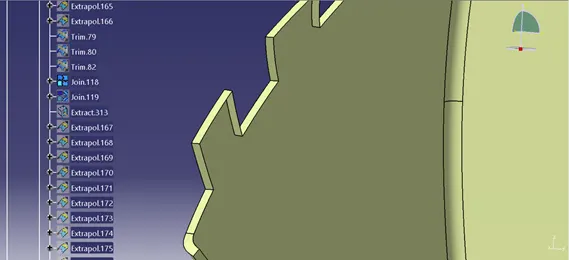
Figure 41: The Class C surface is drawn with respect to class A and connected using trim Command
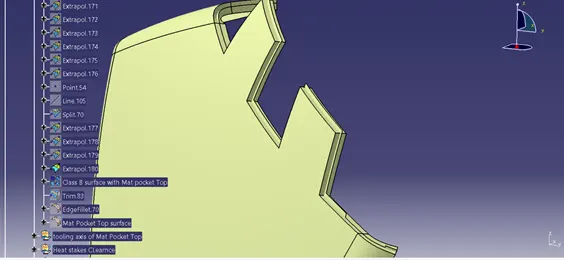
Figure 42: Unhide The Class B surface and extrapolate the boundary of Class B beyond Class C
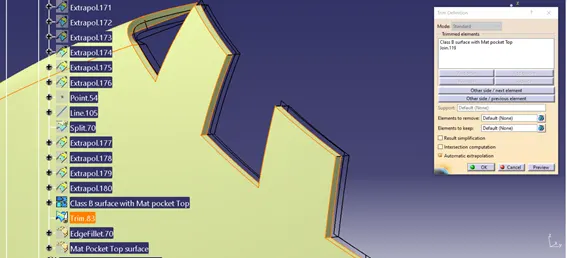
Figure 43: Trim the unwanted surface of Class B with respect to Class C surface
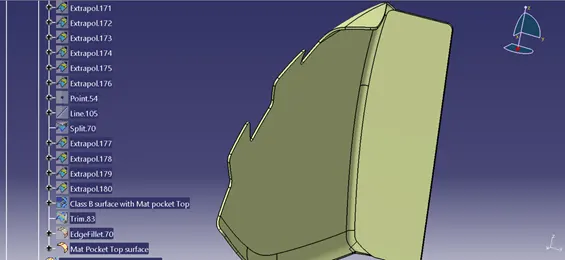
Figure 44: Closed surface
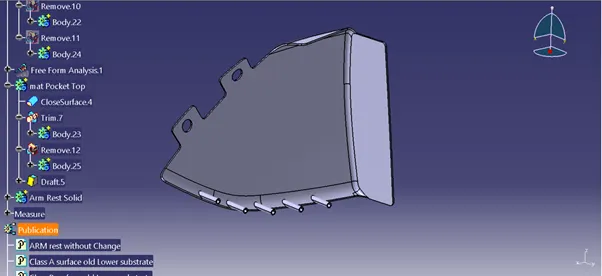
Figure 45: Solid Body of Mat Pocket Top
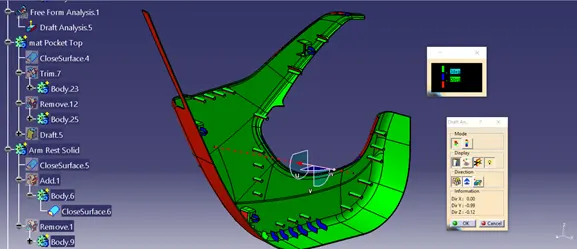
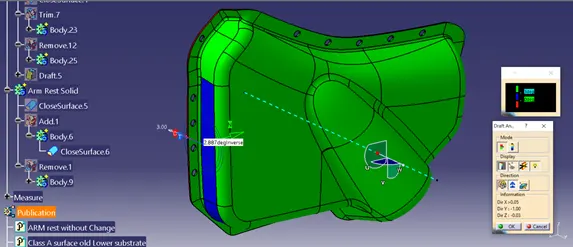
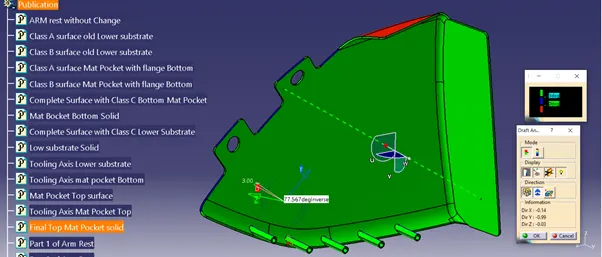
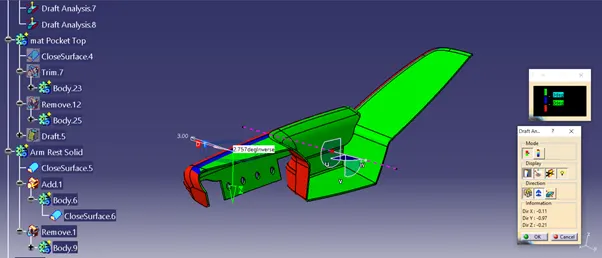
Draft Analysis Images:
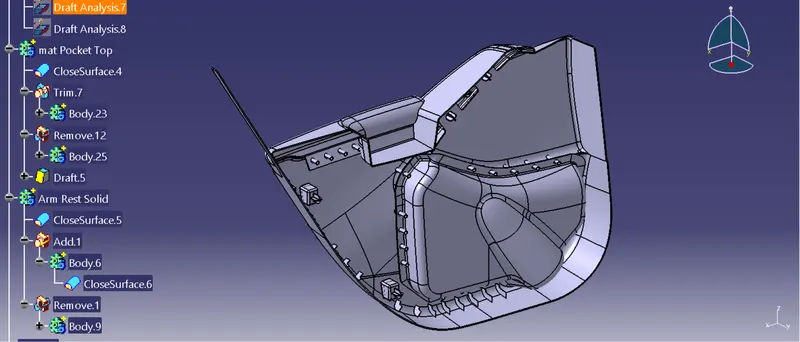
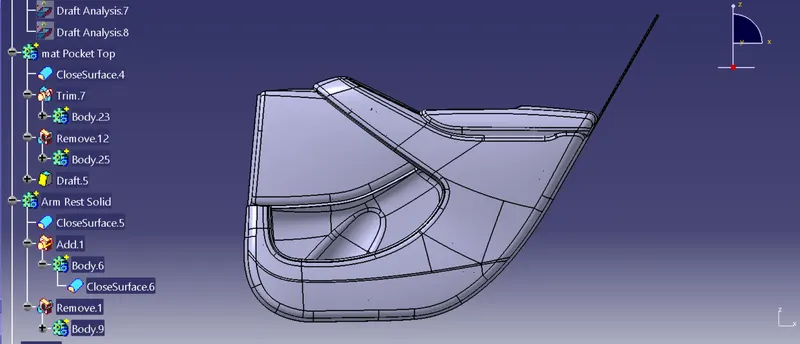
1.Low substrate:
2.Mat pocket Bottom:
3. Mat Pocket Top Portion:
4. Arm Rest:
Complete Arrangement of Lower substrate, Arm rest and mat Pocket,