Week 1:- Introduction to BiW and Fixtures Challenge
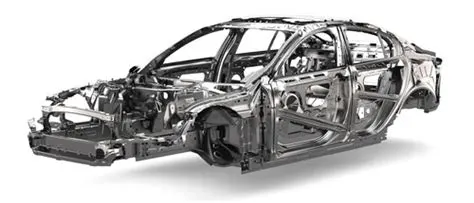
Body in White (B.I.W.) refers to the welded sheet
metal components which form the vehicles structure to which
the other components will be married, i.e ., engine, chassis,exterior and interior trim.
Body in White or BIW refers to the stage in automotive design or automobile manufacturing thambi (ekg8o) in which the car body sheet metal(including doors, hoods, and deck lids)
has been assembled or designed but before the components (chassis, motor) and trim(windshields, seats, upholstery, electronics, etc.) have been added
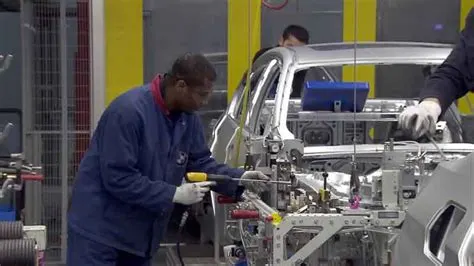
BIW is the stage in automotive design or automobile manufacturing in which the car body sheet metal component are been assembled by welding and by other joining process.
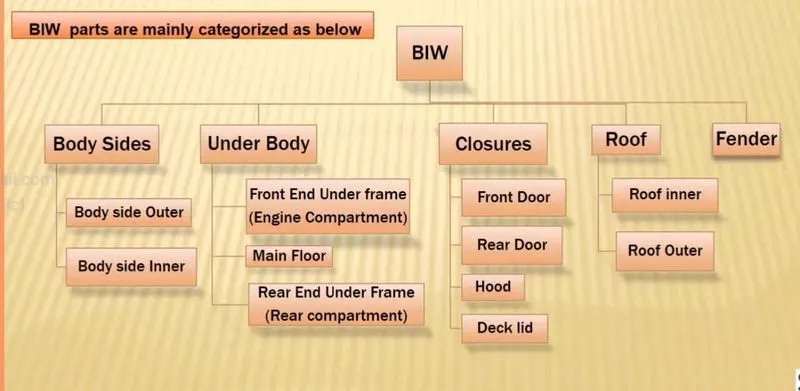
BIW PARTS
BIW Nomenclature
A system of names used in the classification of an art or science or other field or subject. A naming system peculiar to a social group.
Here the namnings are given for Automobile parts.
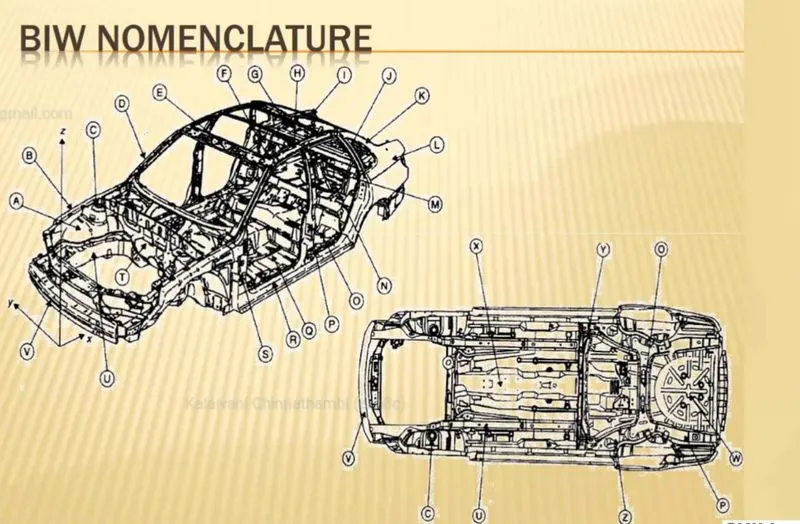
UK Description US Description
A Inner wing panel Motor compartment side panel
B Upper wing member Motor compartment upper rail
C Suspension tower Shock tower
D Upper 'A'-pillar A'-pillar or windshield pillar
E Windscreen header rail Windshield header or front header
F Roof stiffener Roof bow
G Rear parcel tray Package shelf
H Cantrail Side roof rail
I Backlight frame Backlite header or rear header
J "C'-pillar C'-pillar
K 'D'-pillar ' D'-pillar
L Rear quarter panel M Boot floor panel Rear quarter panel
M Boot floor panel Rear compartment pan
N Rear seatback ring Rear seatback opening frame
O Rear seat panel Rear seatback panel
P 'B'-pillar 'B'-pillar or center pillar
Q Floor panel Floor pan
R Sill Rocker or rocker panel
S Lower 'A'-pillar Front body hinge pillar (FBHP)
T Dash panel Dash panel
U Engine (longitudinal) rail Motor compartment lower rail
V Front bumper Front bumper
W Spare wheel well Spare tire well
X Centre (longitudinal) tunnel Tunnel
Y Rear seat cross-beam # 4 crossbar
Z Rear suspension support beam # 5 crossbar
Fixture: A fixture is a device which holds the work piece to be processed (Welded), by using 3-2-1 principle.
In general a welding fixture (tool) consist of number of units together to hold the car panel, and is mounted on a base unit.
Welding fixtures are normally designed to hold and support the various components (work pieces) to be welded. It is necessary to support them in a proper location which is capable of preventing distortions in work pieces
during welding. For this the locating elements need to be placed carefully, clamping has to be light but firm, placement of clamping elements has to be clear of the welding area and the fixture has to be quite stable and rigid to
withstand the welding stresses.
Types of fixtures:
Below are the general types of BIW fixtures:
1.Production Fixtures - mass production purpose
2.Pre production operation fixtures(PPO) - For initial batch production to study the feasibility.
3. Checking fixtures - For car panel geometric inspection purpose.
Principle of Fixture Design:
For a fixture designer, the major portion of design time is spent deciding how to locate the work piece in the fixture.
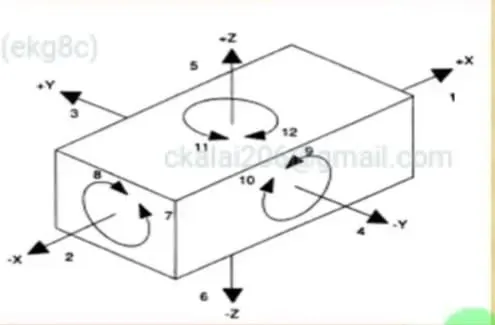
For any free body there are total of twelve degrees of freedom as below:
6 translational degrees of freedom: +X, - X, +Y, - Y, +Z, - Z
And 6 rotational degrees of freedom:
Clockwise around X axis (CROT-X)
Anticlockwise around X axis (ACROT-X)
Clockwise around Y axis (CROT-Y)
Anticlockwise around Y axis (ACROT-Y)
-Clockwise around Z axis (CROT-Z)
-Anticlockwise around Z axis (ACROT-Z)
You must fix all the 12 degrees of freedom in order to locate the work piece in the fixture. So, 12 degrees of freedom of the workpiece need to be fixed & thus we can achieve zero degrees of freedom for the workpiece.
BIW STATIONS
Tool: A tool is a fixture which consists of a number of units together to hold a car part in general.
Types of tools:
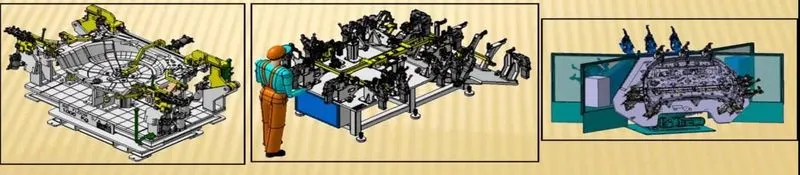
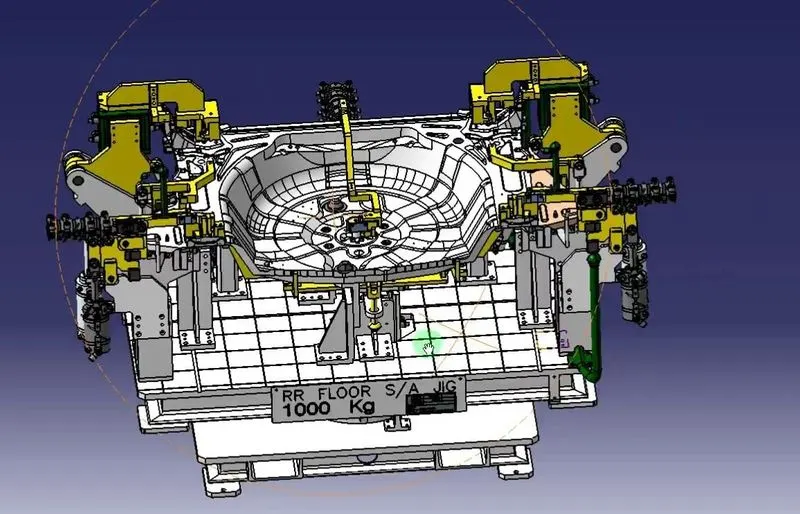
Geo Tool: A geo tool is a fixture in which the geometry of the panels which are welded together is defined accurately. The pin tolerance for a geo pin will be of closer tolerance i.e. 0.15 in general.
For example:
Consider panel hole size 20mm, the pin diameter should be 19.85
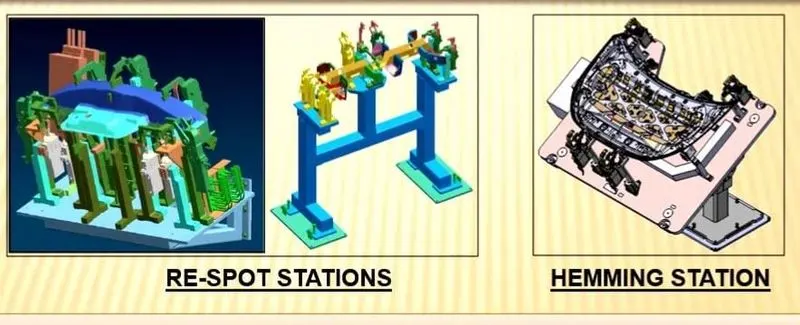
Re-spot Tool: A re-spot tool is a fixture in which the remaining weld spots which are not achieved in geo tool are welded for the pre welded panel from the geo tool.nambi (ekgbc) The pin tolerance for a re-spot pin will be of tolerance with -0.28 in general.
For example:
Consider panel hole size 20mm, the pin diameter should be 19.72
Checking Stations: A Checking Station tool is a fixture which is used to check the automotive parts or assemblies, ensuring all the coordinates, relative dimensions & positions as per the tolerances.
A checking station can be a gauge type, fixed type and automated checking fixtures.
A Checking gauge is a tool where a work piece is held & various measuring gauges are introduced to ensure the dimensions & repeatability.
A fixed type checking fixture is used where the work piece is fixed with clamps & pins & a CMM machine is used which measures the coordinates of different points of the panel or assembly,
compares it with the nominal values & gives a report.
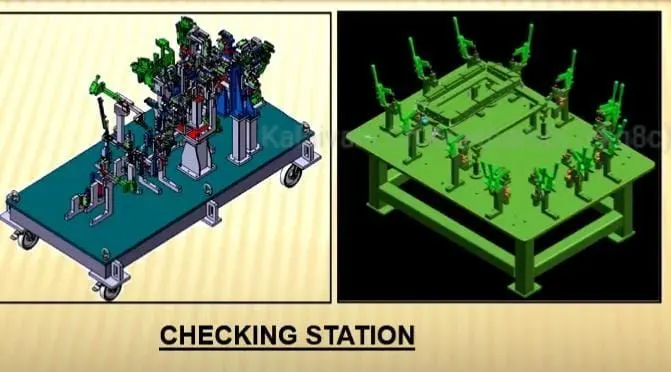
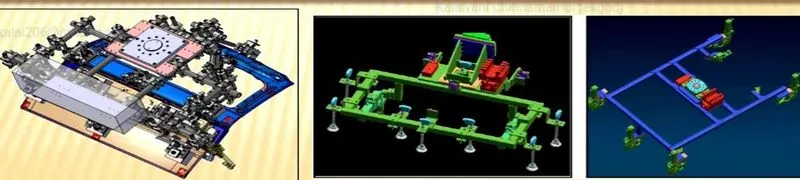
Gripper: A Gripper is a device or a fixture which holds the car panel, and is fixed to the manipulating end of a robot or an end effector. Also know as EOAT - End Of Arm Tooling.
Types of Grippers:
Material Handling Gripper (MH): Material Handling gripper are designed for handling the car panel from one tool(Station) to other tool(Station)
Process Gripper: Process gripper are designed for handling the car panel from one tool(Station) to otherk ool(Station), And in addition to that it undergoes process like pedestal welding, pedestal riveting, Gluing, sealing, etc.
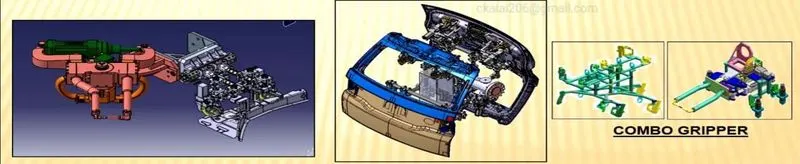
Combo Gripper: Combo grippers are designed for handling the car panel from one tool(Station) to another tool(Station), Also with a combination of weld gun at another side of the gripper for welding.
Gripper + Weld Gun
Dual Gripper: Dual grippers are designed for handling the car panel from one tool(Station) to another tool(Station), With two sided grippers.
Gripper + Gripper
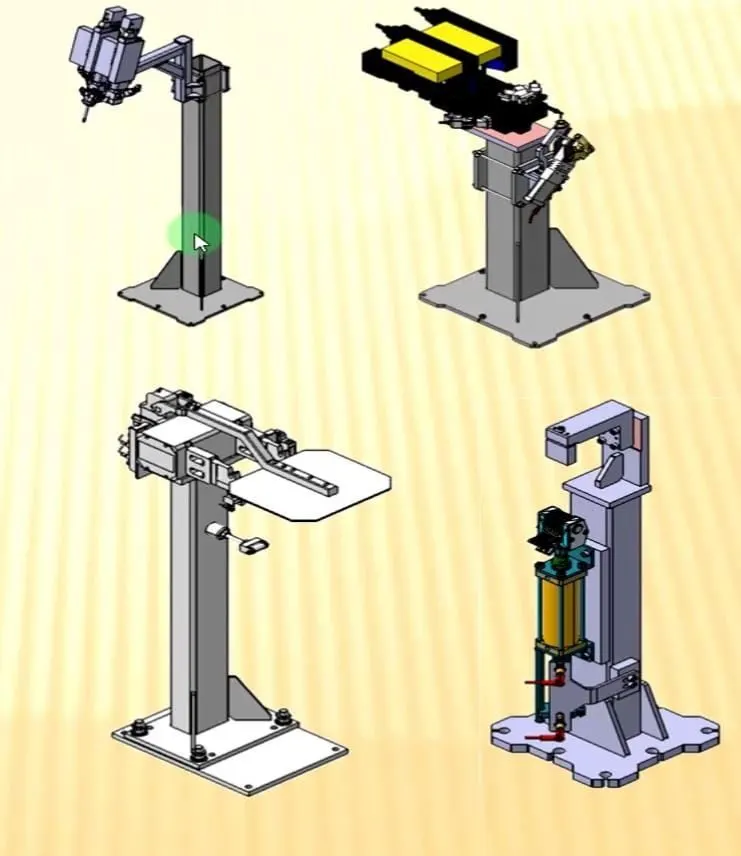
Stands and types of stands
Gluing and sealer stand: Gluing gun or sealer gun is fixed to a welded or a standard stand which is grouted to the floor permanently.
Docking stand: When robots are selected for multi tasking like material handling & welding , which cannot carry both due to some limitations ( payload capacity of the robot or space constraint) the robot will drop and pick the gripper or gun after completing the respective operation with the help of Docking stands.
Date stamp stand: The panel will get the date embossed on to it, with the date stamping device mounted on this date stamp stand.
Take out Trolley: Take out trolley is used to take the car panel out of the robotic working cell between the cycle for inspection purpose.
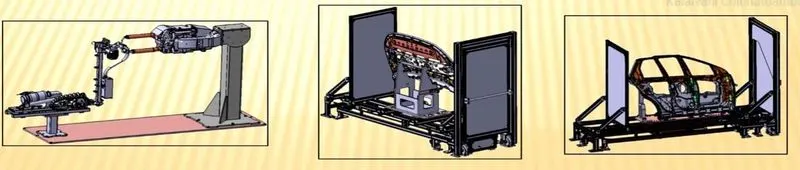
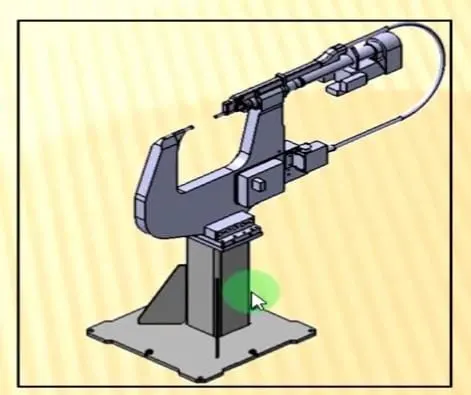
Basic Terminologies used in BIW Fixture
NC/MYLARS/FINGERS
PLP
X BLADE RISERS
SHIMS
ROUGH LOCATORS
HARDWARES
CMM
UNITS
NUMBER PLATE
CO-ORDINATE PLATE
NAME PLATE
CLAMP ARM
PIVOT
CLASS 'A' SURFACE/SKIN SURFACE
REED SWTCHES
SENSORS