Hood design-Week 2
Hood Design
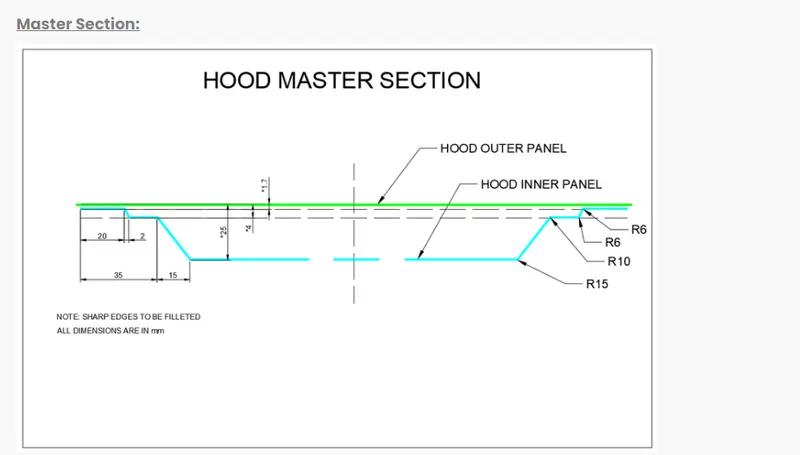
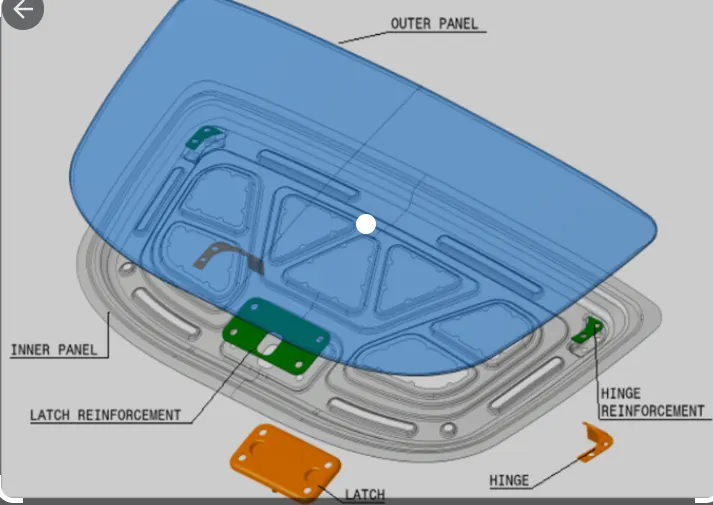
Aim: Design the Hood outer panel, inner panel, and the necessary reinforcements by following the Master section mentioned with the design parameter explained in the videos. Submit an assembly of the Hood inner panel, outer panel, latch, hinge, and reinforcements.
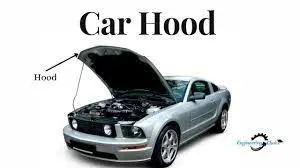
The hood (North American English) or bonnet (Commonwealth English) is the hinged cover over the engine of motor vehicles. Hoods can open to allow access to the engine compartment or trunk (boot in Commonwealth English) on rear-engine and some mid-engine vehicles) for maintenance and repair.
Styles and materials
On front-engined cars, the hood may be hinged at either the front or the rear edge, or in earlier models (e.g. the Ford Model T) it may be split into two sections, one on each side, each hinged along the centerline.
Hoods are typically made out of the same material as the rest of the bodywork. This may include steel, aluminum, fiberglass, or carbon fiber. However, some aftermarket companies produce replacements for steel hoods in fiberglass or carbon fiber to make the vehicle lighter.
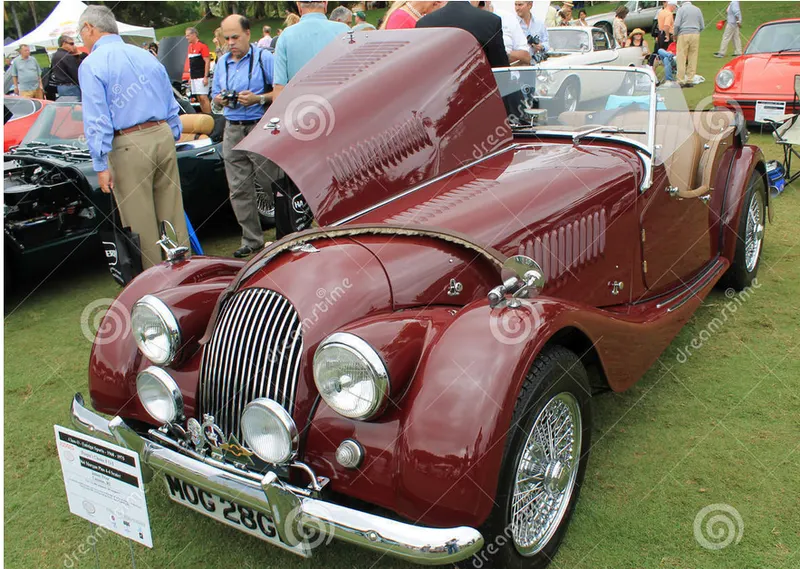
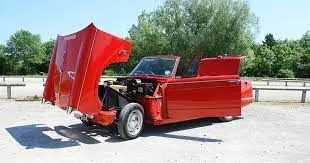
A further variant combines the bonnet and wheel arches into one section and allows the entire front bodywork to tilt forwards around a pivot near the front of the vehicle (e.g. that of the Triumph Herald).
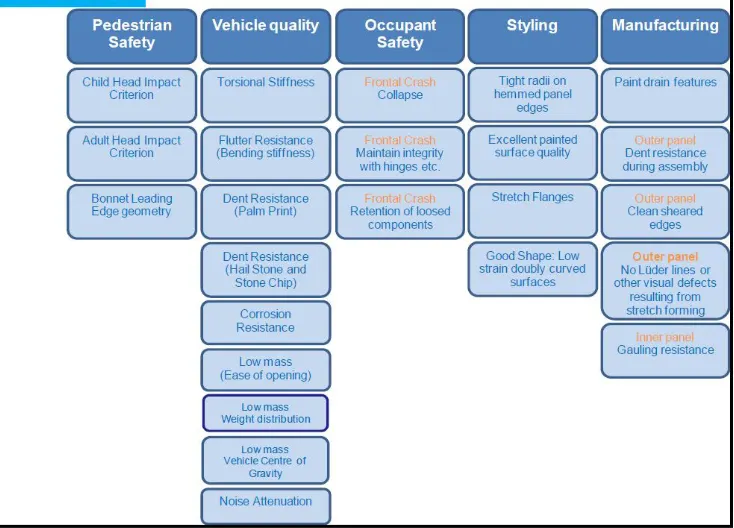
ENGINE HOOD: Hood which is also called ENCON, serves as an access panel to ENGINE COMPARTMENT of an automobile. It is an assembly made of OUTER and INNER PANELS to meet various safety & design requirements. Following are the design considerations involved to design hood,
1. PEDESTRIAN SAFETY.
2. VEHICLE QUALITY.
3. OCCUPANT SAFETY.
4. STYLING.
5. MANUFACTURABILITY.
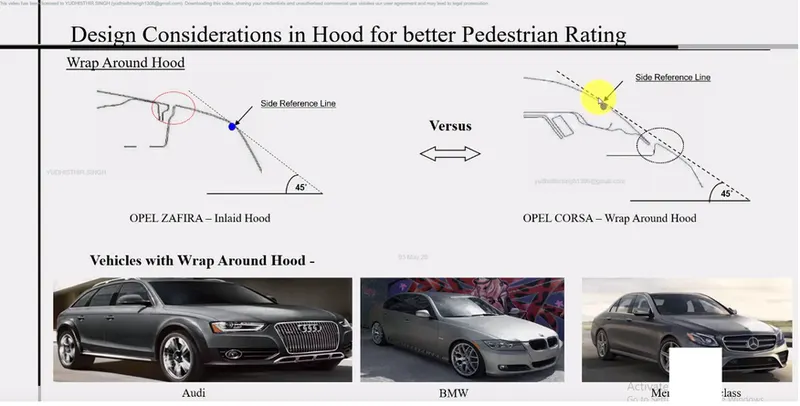
1. PEDESTRIAN SAFETY: Pedestrian safety is always a factor involved in the design of the hood. This is achieved by proper selection of material that can readily deform avoiding risk during impact, providing emboss to inner panels, etc. This is one of the major factors for a vehicle to have better safety ratings.
2. VEHICLE QUALITY: This involves how best the hood can be designed to have better quality in terms of torsional stiffness, dentb resistance (Hailstone and stone chippings), corrosion resistance, better weight distribution, and noise attenuation.
3. OCCUPANT SAFETY: The design consideration must include the impact caused due to FRONTAL CRASH COLLAPSE. Under such a scenario it is expected that the HOOD maintains its integrity with hinges and also retains any of the loosed components from engine compartments.
4. STYLING: Better surface quality (A-class surface finishing), Tight radii on hemmed panel edges & low strain between curved regions of the inner and outer panel.
5. MANUFACTURABILITY: The design should be always considered for Manufacturability e.g. embossing on the inner panel should have sufficient draft angles provided for the punching tool to flow in and flow out.
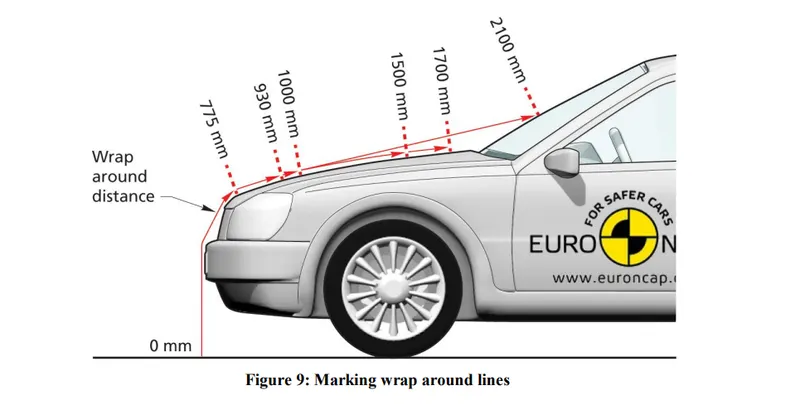
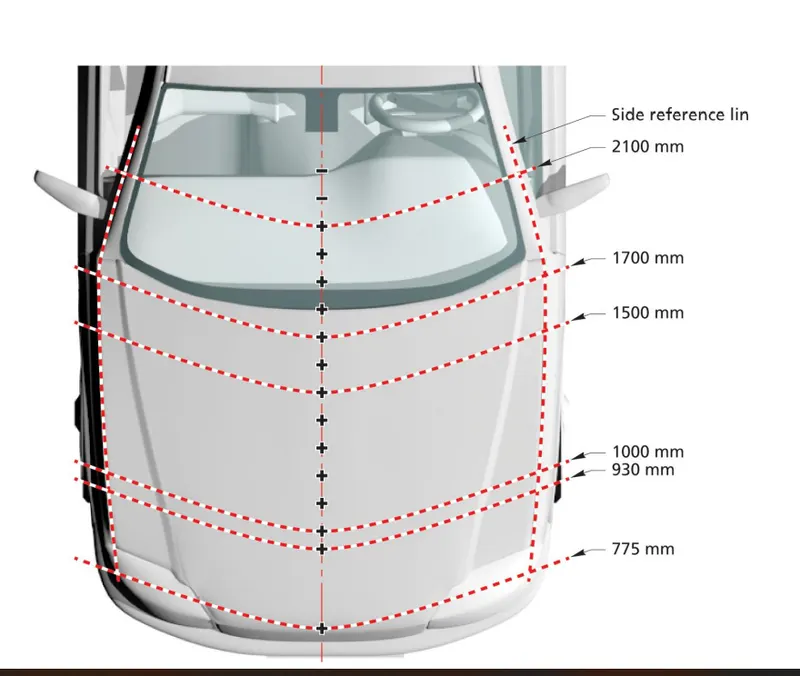
- Marking Wrap Around Distances
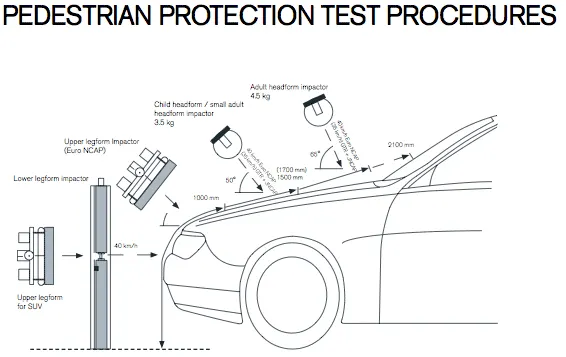
The headform test area is defined as the outer structure that includes the upper surface of all outer
structures. It includes, but is not limited to, the bonnet, wings, windscreen scuttle, wiper
arms/spindles, windscreen frame, A-pillars, and roof. It is bounded by the geometric trace of the
1000mm wrap-around line in the front, the Bonnet Side Reference Lines, and the 2100mm wrap-around distance (WAD).
- Begin at the vehicle centreline.
Place the end of a flexible tape measure or graduated wire on the floor vertically below the front face of the bumper. - Wrap the tape or wire over the bumper, bonnet windscreen, and roof ensuring that it is maintained in a vertical longitudinal (X, Z) plane and that its end is still in contact with the ground.
- The tape should be held taut throughout the operation, vertically below the front face
of the bumper, see Figure - Mark on the bumper/grille, bonnet top, windscreen, A-pillars, and/or roof the wrap-around distances of 775mm, 930mm, 1000mm, 1500mm, 1700mm, and 2100mm. These are the geometric traces described on the outer surface of the vehicle by the end of the flexible tape or wire 775mm, 930mm, 1000mm, 1500mm, 1700mm, or 2100mm long, when it is held in a vertical fore/aft plane of the car and traversed across the front of the bonnet and bumper.
Impact-absorption bonnet and bumpers
Mazda uses various methods to reduce injury to pedestrians in the event of a collision.
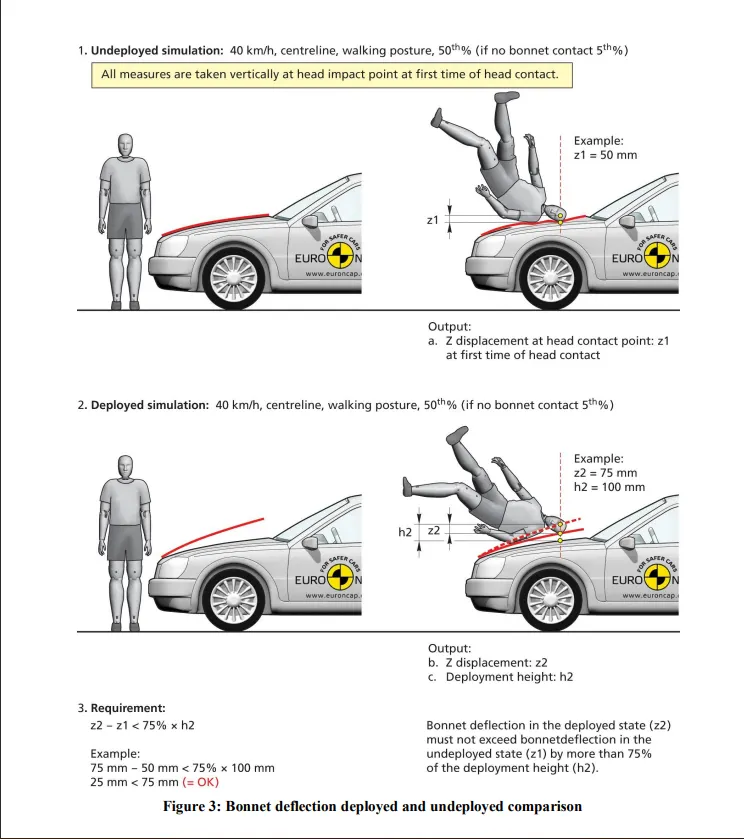
The Impact Absorption Bonnet mitigates the impact to a pedestrian's head in a pedestrian accident.
Active Bonnet is designed to mitigate the shock to the head in the event the vehicle collides with a pedestrian. Designed to activate with a defined speed range, the system causes the rear end of the bonnet to pop up when an impact exceeding a certain threshold is detected, creating a shock-absorbing space between the bonnet and the engine.
Energy absorption materials are used in the front part of the vehicle which hits pedestrians' knees to mitigate the severity of pedestrian's knee injuries. Also, stiffening reinforcement is placed at the bottom of the bumper to better prevent pedestrian's legs from going under the vehicle. In anticipation of an accident, the shape of the bonnet is carefully designed to reduce the damage to the pedestrians' knees, which are an important part of the body for walking.
How Active Bonnet works
Bonnet Side Reference Line
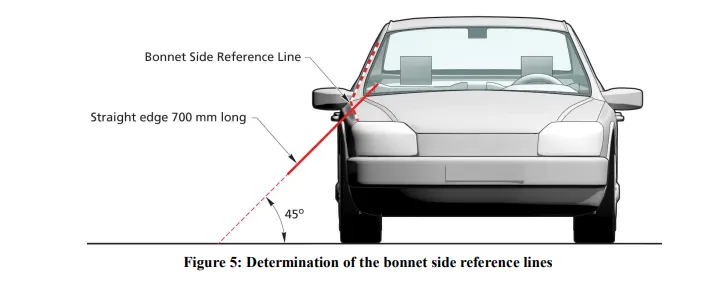
The Bonnet Side Reference Line is defined as the geometric trace of the highest points of contact between a straight edge 700mm long and the side of a bonnet, as defined in Section 3.3.1 and A-Pillar, when the straight edge, held parallel to the lateral vertical plane of the car and inclined inwards by 45is traversed down the side of the bonnet top and A-Pillar, while remaining in contact with the surface of the body shell, any contact with door mirrors is ignored. See Figure 5. Where multiple or continuous contacts occur the most outboard contact shall form the bonnet side reference line.
Figure: Determination of the bonnet side reference lines
Fix a straight edge that is 700mm long at 45 to the vertical. With this edge in a plane parallel to the lateral vertical plane of the car, position the straight edge at the front of the front wing and in contact with, the bonnet.
- Mark the uppermost point of contact of the straight edge and wing.
- Pull the straight edge away from the wing, move it towards the other end of the vehicle by
not more than 100mm, and then back into contact with the wing. - Mark the uppermost point of contact of the straight edge and wing
Data to be used:
Hood Thickness Information
- Outer Panel Thickness = 0.75mm
- Inner Panel Thickness = 0.75mm
- Reinforcement Thickness = 1.5mm
Master sketch:
- Embossing:
The metal sheet embossing operation is commonly accomplished with a combination of heat and pressure on the sheet metal, depending on what type of embossing is required. Theoretically, with any of these procedures, the metal thickness is changed in its composition.
The metal sheet is drawn through the male and female roller dies, producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet. The pressure and a combination of heat actually "irons" while raising the level of the image higher than the substrate to make it smooth. The term "impressing" refers to an image lowered into the surface of a material, in distinction to an image raised out of the surface of a material.
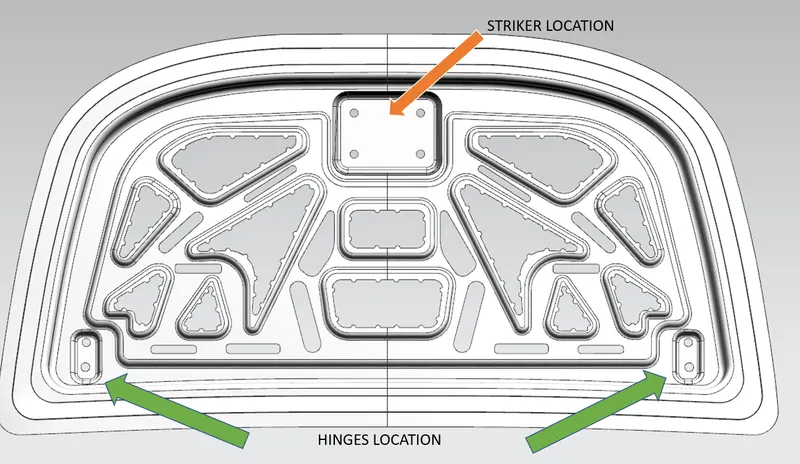
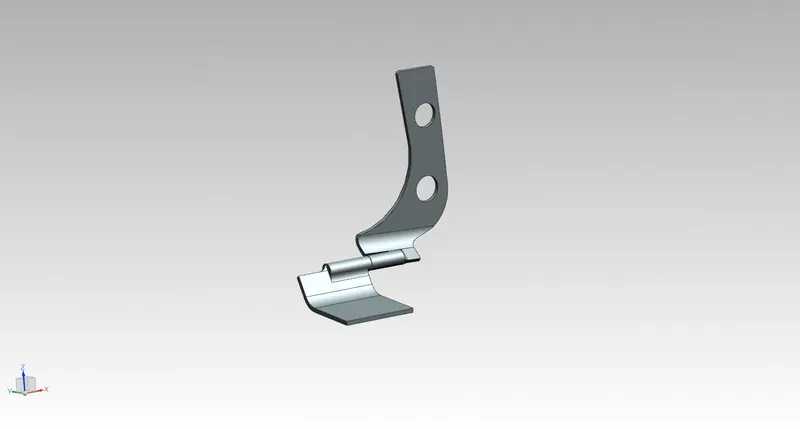
Hinges are used to join two parts together while allowing them to rotate relative to each other. They typically have two flat faces, known as leaves. One leaf is attached to each of the parts being joined.
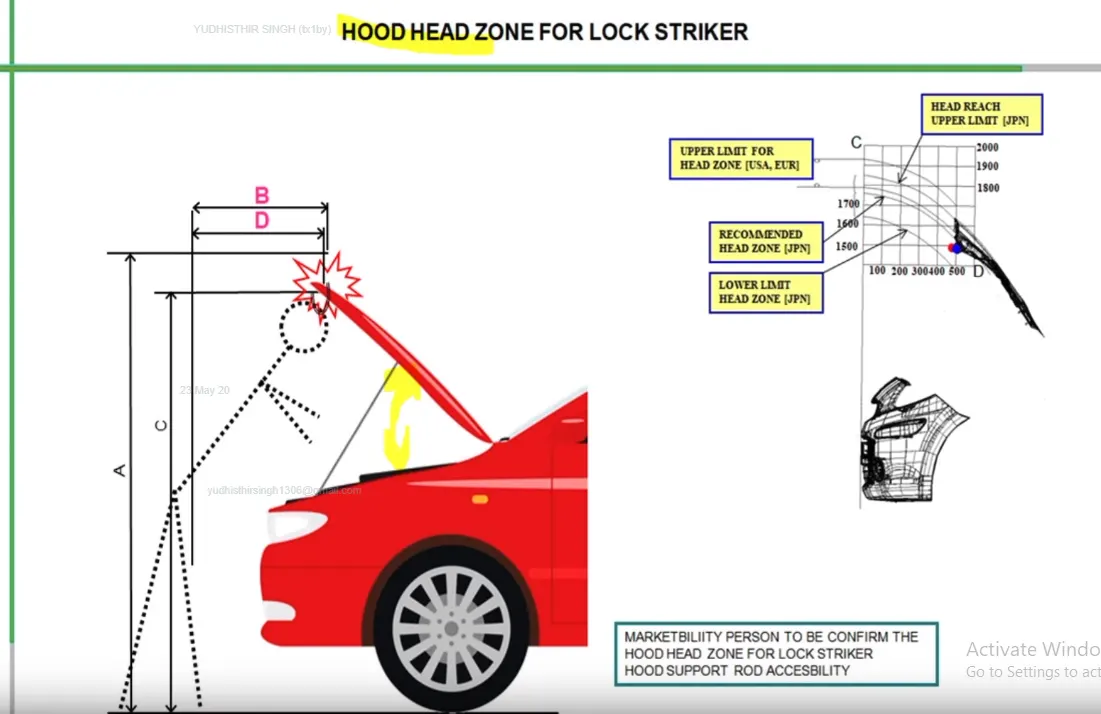
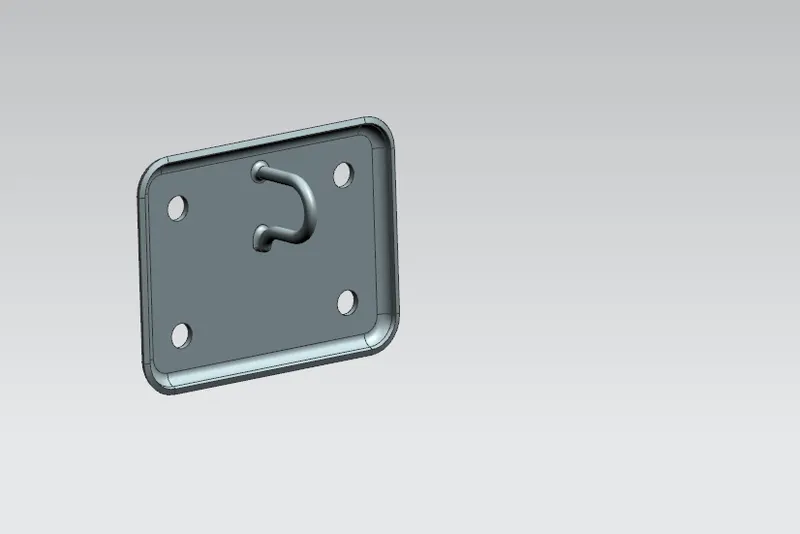
Hood striker It bolts to the underside of the hood at the front. It engages the hood latch when closed.
For the term hood striker may also exist other definitions and meanings, the meaning and definition indicated above are indicative not be used for medical and legal or special purposes.
and follow design rules as per master section provided in challange data.
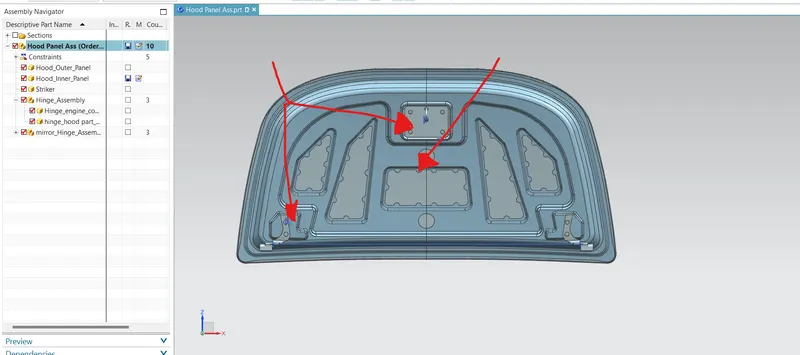
- Reinforcements:- The reinforcements are provided to add material to inner panel to provide extra strength to hood to compensate for loss of strength near component installation region.
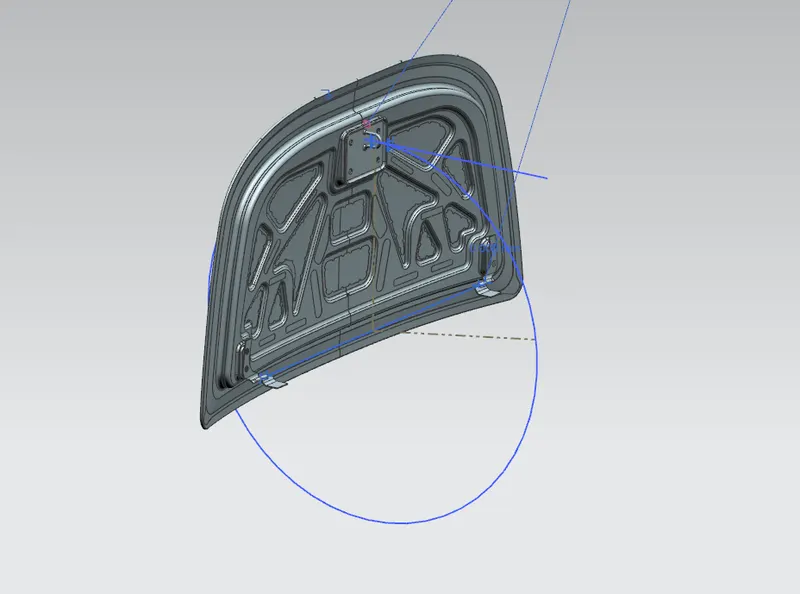
- Latch Trajectory: It is the path along which the hood rotates during opening and closing movement.The striker in the hood follows a perticular path while opening or closing the hood.which is along circumference of a circle with center at hinge axis.this path is nothing but the latch trajectory.It is a very important aspectrs in hood design ,in order to decide hinge,latch and striker installation points.
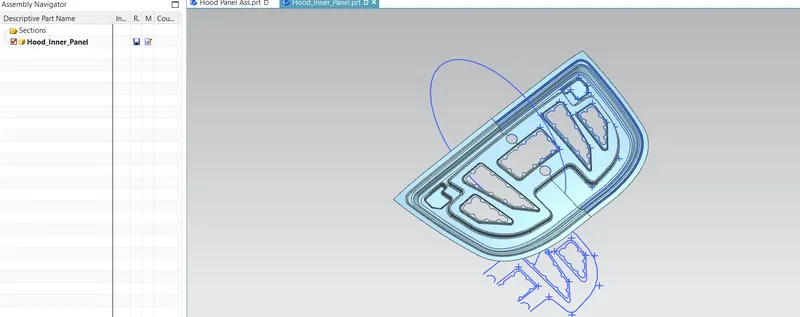
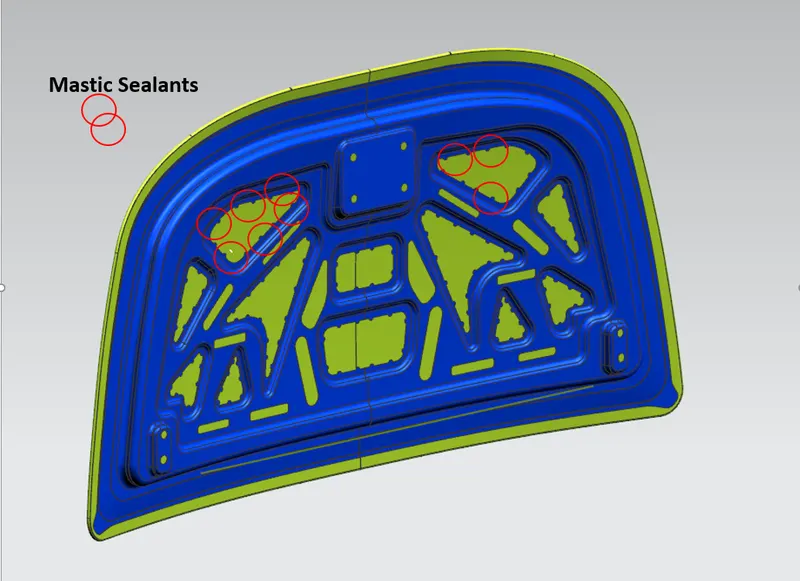
- Mastic sealant:- Mastic sealant helps to loaclly improve strength of the hood.It is generally a hard rubber part,which is intriduced as a paste between inner and outer panel of the hood , which will get hardened insuide furnace.Every mastic point will have tendency to improve the local strength in around 80mm diameter. considering this , the mastic points are positioned such that most of hood region is coverd.
- Design Methodology:-
- First the inner panel is designed from given master section using the various commands and features.we creates the embossinbg using the offset surface from the original master section . similarly we create the cuts on the the emboss by sketching and using trim surface option.
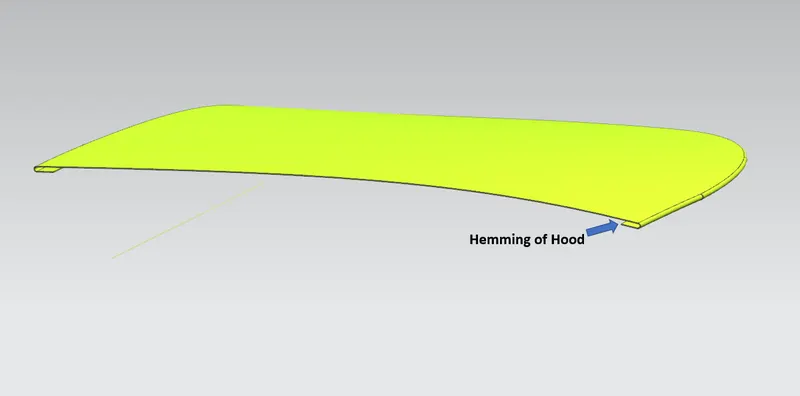
- Then the outer panel is designed from same master section. here we are supposed to provide the hemming the outer panel. The parametersog the hemming take as per given values.
- Now on the inner panel, the embossing for hinge and striker are produced by considering their respective dimensions and assembly positions.First the emboss for hing is created and then by fixing the hinge into position. we draw an axis passing through both axis to commen axis and then position of striker such that it will move along circumference of a circle and whose center is nat a midpoint to commen axis.Thus,position of striker is decied and we canb create emboss for same.
- Data provided
outer panel thickness-0.75mm
inner panel thickness- 0.75 mm
reinforcements thickness - 1.5 mm
Sheetmetal Operations in car Hood Manufacturing Process:
- Deep Drawing:-
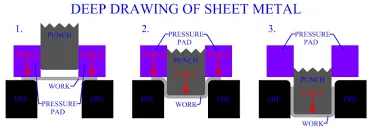
It is sheet metal forming process in which a sheet metal blank is radially drawn into a forming die by mechanical action of punch .The process is considered deep drawing when the depth of the drawn part exceeds its diameter.
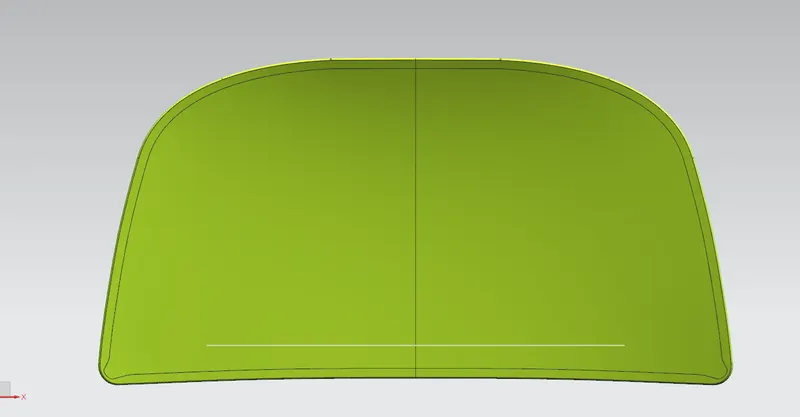
External Skin or Outer Panel of Car Hood to cover the Engine and Protect the Engine as well as Aesthetic of a car
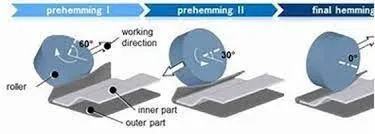
Hemming
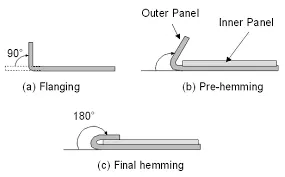
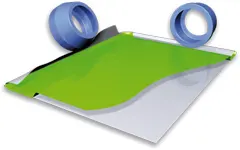
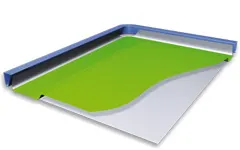
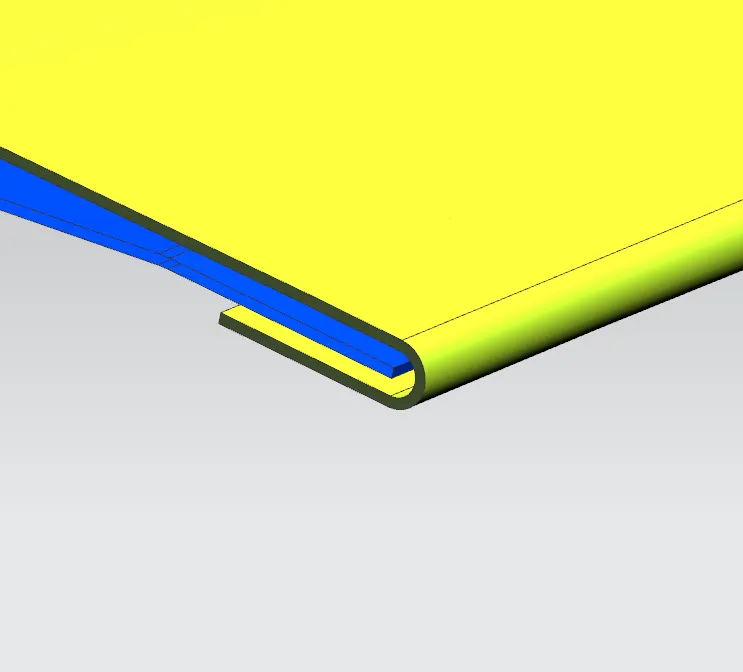
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
The accuracy of the hemming operation is very important since it affects the appearance of the surface and surface quality. Material deformations, which occur during the hemming process, can lead to dimensional variations and other defects in parts. Typical hemming defects are splits or wrinkles in the flange, material overlaps in the corner areas or material roll-in. This is why it is important to use simulation tools in order to, on the one hand, better understand the hemming process and, on the other hand, significantly reduce the number of “trial and error” loops during tryout und production.
HOOD ASSEMBLY:
1.HOOD OUTER PANEL:
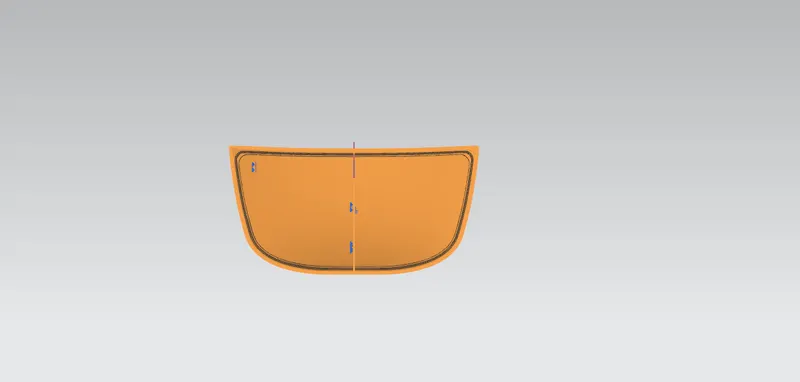
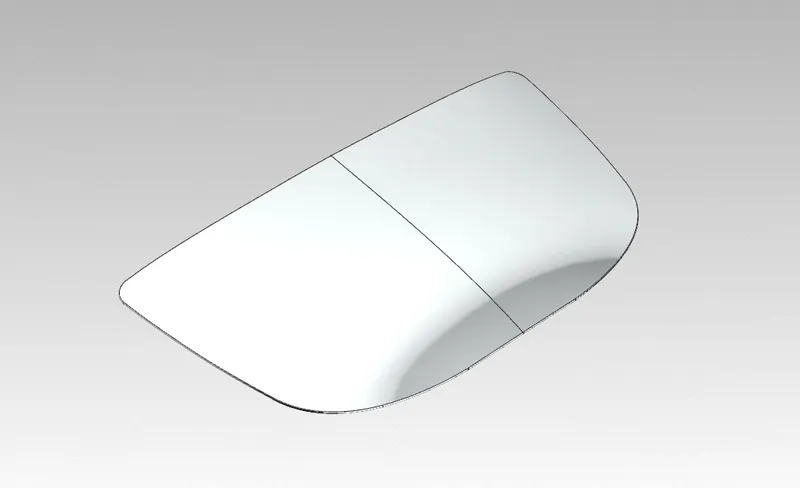
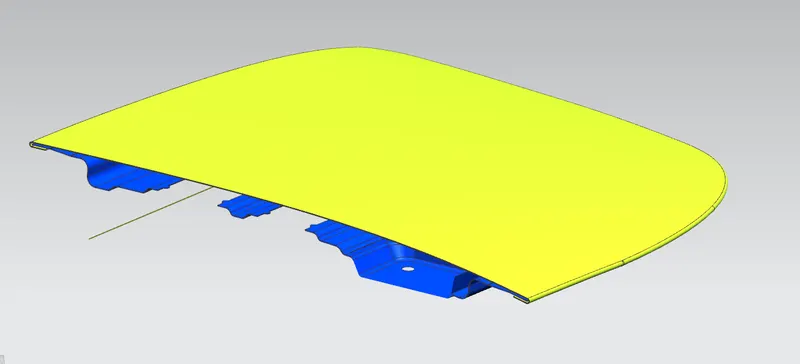
Hood outer panel provides aesthetic look to the vehicle.It is the styling team who provides the skin for the outer panel. The shape, position and size of the hood should satisfy the safety norms. So while designing the hood we should give more importance to pedestrian safety. The outer panel is attached to the inner panel by hemming. So, it is necessary to provide required hemming flange and reliefs for the hemming operation. We also provide mastic sealants between outer panel and inner panel to reduce vibration.
2.HOOD INNER PANEL
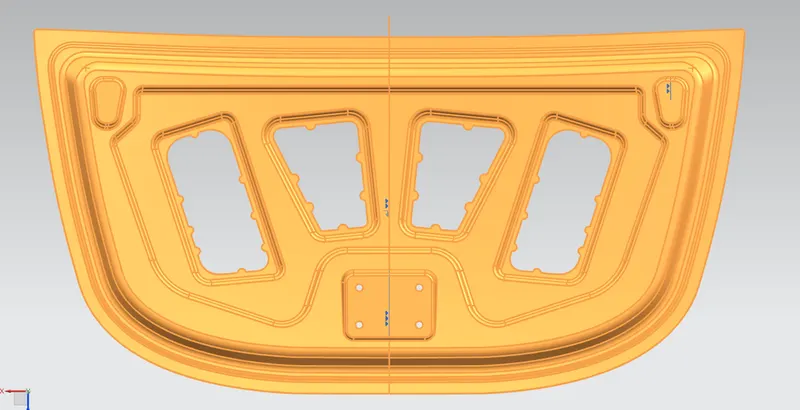
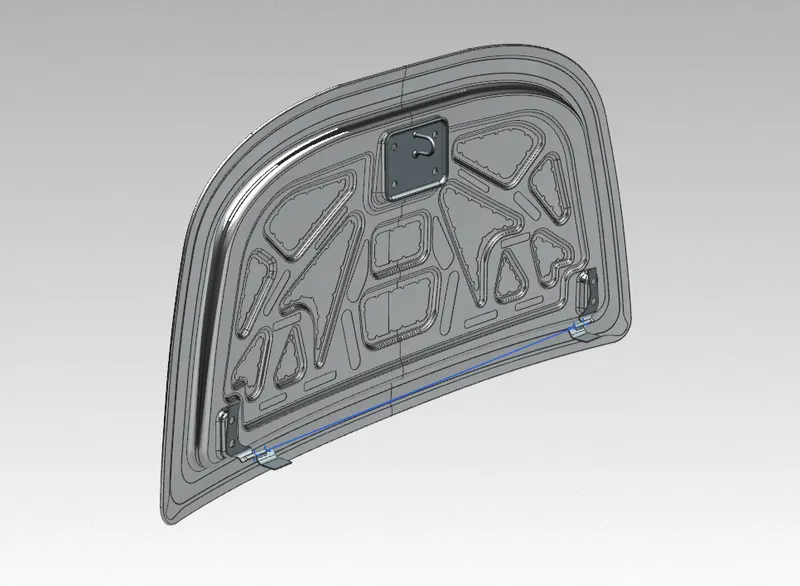
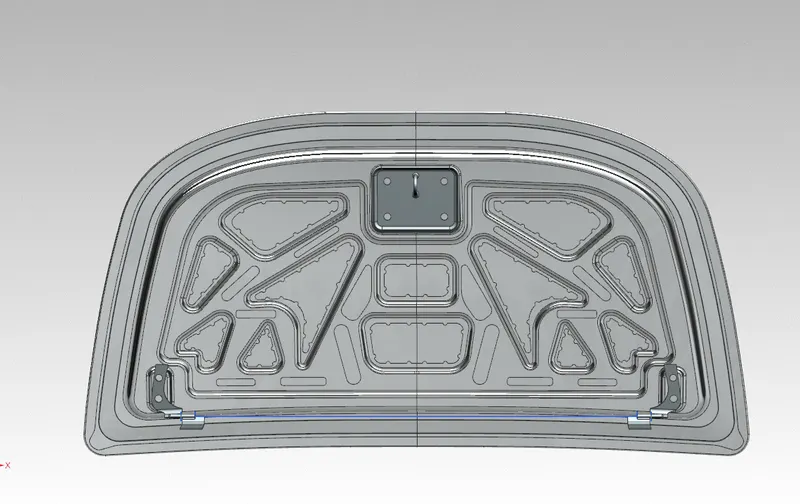
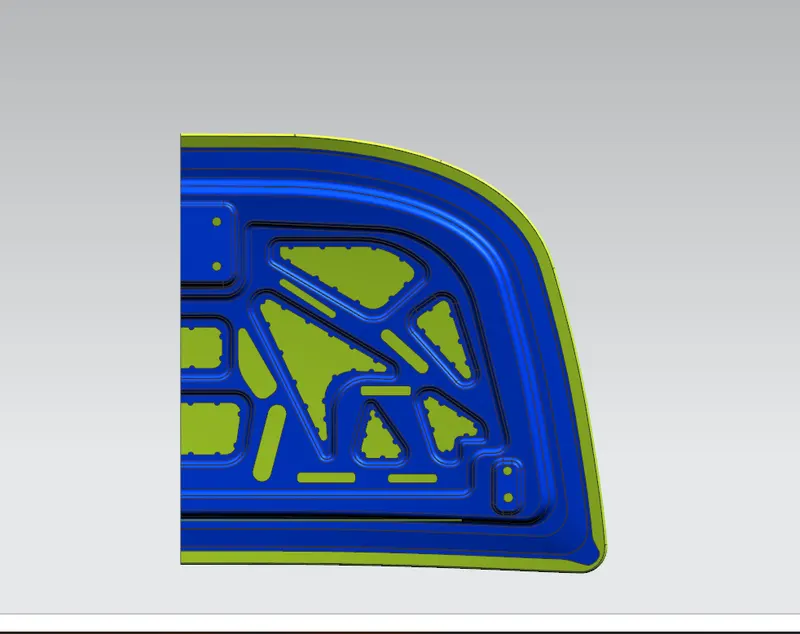
Inner panel is the part that gives strength and rigidity to the outer panel. The master section represents the initial emboss shape and size. Then we provide the emboss for the latch and hinge elements after fixing the location.
3. STRIKER AND HINGES REINFORCEMENT
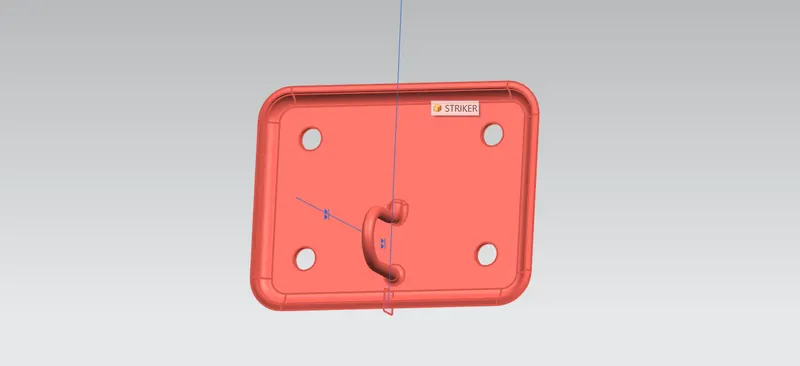
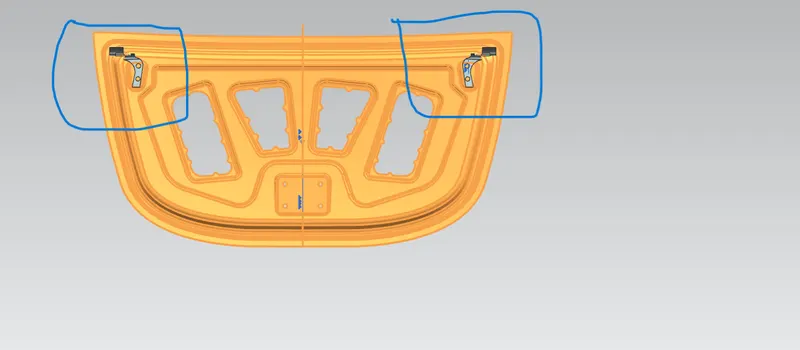
Reinforcements are provided according to the design requirements. Mainly it is provided at the hinge and latch regions to improve the strength locally. Usually thickness of reinforcements will be higher than that of the inner panels and the value varies according to cost and requirement. According to the design requirement here it is given 1.5mm thickness to both hinge and latch reinforcements.
4. LATCH TRAJECTORY
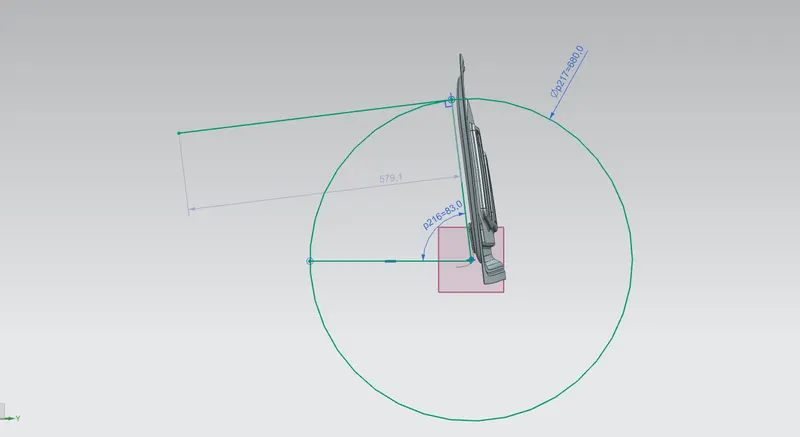
Latch trajectory is given by the circle drawn from the hinge axis point. Hinge axis point is the centre point of the hinge axis. First, we can fix either the latch or the hinge. If we have fixed the hinge position then we should plot the Trajectory circle for the latch. For proper mating condition the striker axis through the tip of the striker should be tangential to the latch trajectory.
5.RELIEF POINTS ON THE EDGES
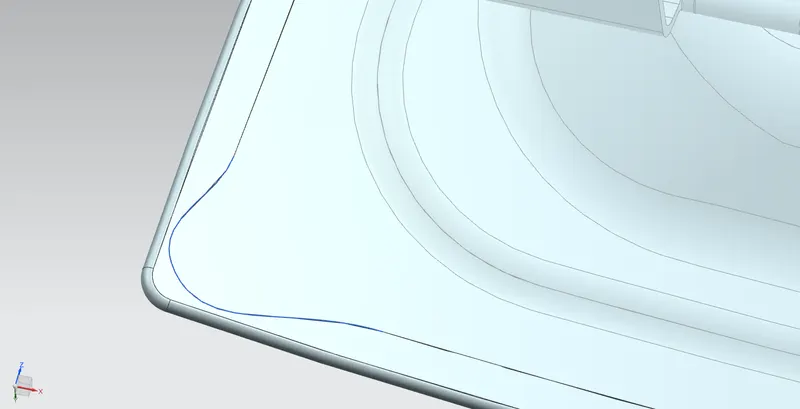
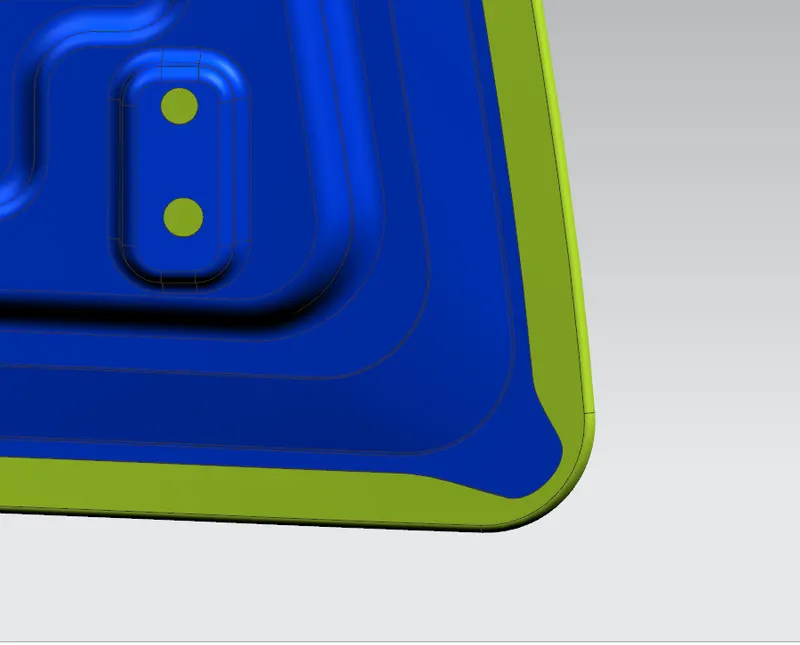
Relief ponts provides the strenth to the outer panel which has lost due to hemming process.
6.HEMMING
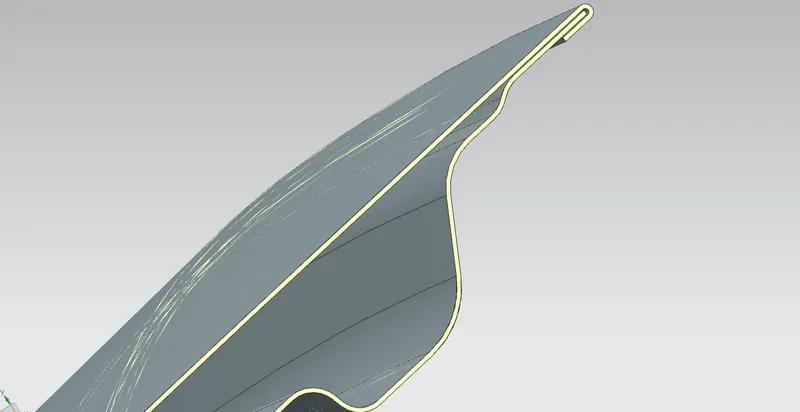
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
The accuracy of the hemming operation is very important since it affects the appearance of the surface and surface quality. Material deformations, which occur during the hemming process, can lead to dimensional variations and other defects in parts. Typical hemming defects are splits or wrinkles in the flange, material overlaps in the corner areas or material roll-in. This is why it is important to provide required reliefs at the corners.
7. MASTIC POINTS:
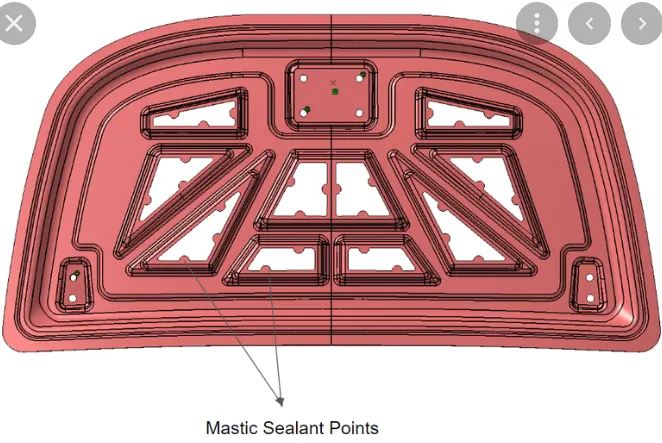
Hood commonly possess large surface area and hemming can only be provided through its boundary. We cannot use other joining techniques like welding, riveting etc because they leave marks on the outer panel which spoil its aesthetic appearance. So, mastic sealants are used to stick the inner surfaces of outer panel and inner panel. Mastic sealants are elastic compound that behave like rubber. It is applied between the inner and outer panels at specified spots. Each spot of mastic sealants has its effect around a circular region of 80mm diameter. Thus, the mastic points are arranged in such a way that it covers the areas away from the hemming which are more vulnerable to vibrate.
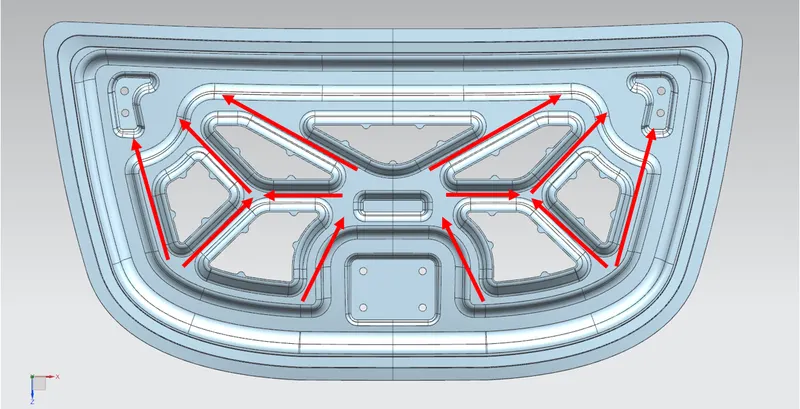
8. EMBOSSES:
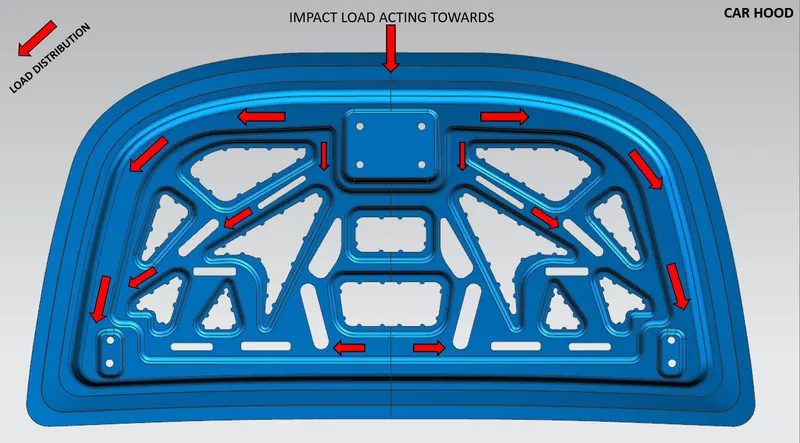
Throughout the inner panel we provide different embosses. We can increase the stiffness of the inner panel through these embosses. The shape and size of the embosses also determines the direction of the force distribution resulted from frontal collision. The force should be always distributed away from the passengers. Here in the figure the embosses are designed in such a way that the force is directed to either sides of the car.
9.DEEP DRAWING
Deep drawing is one of the most widely used processes in sheet metal forming. Apart from its use in many other sectors, it is applied in the automotive industry for the manufacturing of car body parts. The deep drawing process is a forming process which occurs under a combination of tensile and compressive conditions.
Sheet metal blank is radially drawn into a forming die by the mechanical action of a punch. It is thus a shape transformation process with material retention. The process is considered "deep" drawing when the depth of the drawn part exceeds its diameter. This is achieved by redrawing the part through a series of dies. The flange region (sheet metal in the die shoulder area) experiences a radial drawing stress and a tangential compressive stress due to the material retention property. These compressive stresses (hoop stresses) result in flange wrinkles. Wrinkles can be prevented by using a blank holder, the function of which is to facilitate controlled material flow into the die radius.
DESIGN CONSIDERATIONS OF A CAR:
STEPS FOR HOOD DESIGN:
First we need to download the skin data from given link.
Then from outer panel we need to take the inner panel skin data by offsetting it to 0mm and we should hide the outer panel to work on inner panel.
Then we have to work on inner panel according to the master section by creating embosses for hinges and striker.
Then by using hinge axis we need to draw a latch trajectory.
For removing sharp corners we should use blends wherever it is required.
Then we need to do the hemming and give relief points on the edges to strentghen the hood .
finally thicken the component by 0.75mm to covert it to sheetmetal.
There are various types of hemming operations:
- Conventional die hemming
- Roll hemming
Body Sealer
-
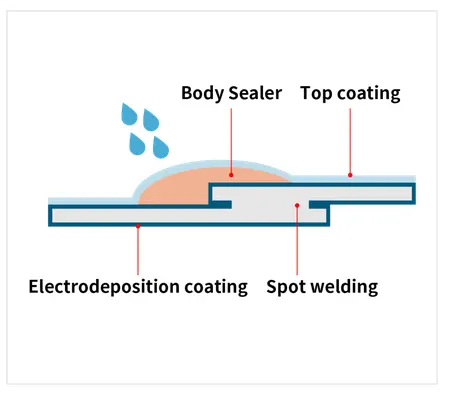
Body sealers that provide manufacturers with truly waterproof, dustproof, and corrosion‐proof solutions for automotive body joints that are susceptible to environmental threats. These one‐component PVC sol/acryl sol sealing materials accommodate multiple wet-on-wet coating applications without requiring the time and expense of oven curing between coats. These sealers are tough on the elements, yet easy on your team—and your bottom line.
Distinct Benefits
- Protection at its best. Body Sealer keeps dust and moisture out, preserving the integrity of steel panels inside and outside of the automobile cabin. It puts a durable, rustproof coating on vulnerable steel plate edges, virtually eliminating corrosion.
- Ultimate application flexibility. Body Sealer can be applied manually or robotically during the paint process, then cured in the paint shop’s baking oven.
- Excellent adhesion. Our body sealer is engineered to provide exceptional adhesion, including bonding securely to electrodeposition coatings.
- Tailored to your needs. Sunstar’s flexible design allows for the material’s properties and performance characteristics to be optimized for each working environment, application, coating, and working condition. Custom specifications can be set to further fine‐tune coating properties and assure exceptional paint finishing for your shop.
- Excellent compatibility. Our Body Sealer systems are highly compatible with virtually all adherents and paints and are cured in conventional OEM paint shop baking ovens one time (no need for curing between each applied coating). Achieving excellent results is easy when everything works together.
Mastic Adhesive
Sunstar’s mastic adhesive was developed specifically to bond exterior automotive panels to the vehicle’s inner panel structure, such as on roofs, doors, and hoods. This one‐component synthetic rubber sealer remains elastic after curing to reduce panel flapping and to prevent panel distortion
Distinct Benefits
- Great application flexibility. With minimal stringing effect, our mastic adhesive provides controlled application for consistent performance during robotic application. The easy-to-handle formula can also be applied with a handgun or pump.
- Excellent adhesion to oily steel plates. Mastic adhesive can be applied directly to oily steel plates without pre‐treating the metal, creating a strong and permanent bond.
- Ideal for aluminum panel bonding. Our mastic adhesive is suitable for a variety of metals and is an excellent choice for assemblies where aluminum and other alloys are used.
- A formulation for virtually every need. Mastic adhesive is available in a range of hardness and foam expansion ratios to provide optimal performance for each application.
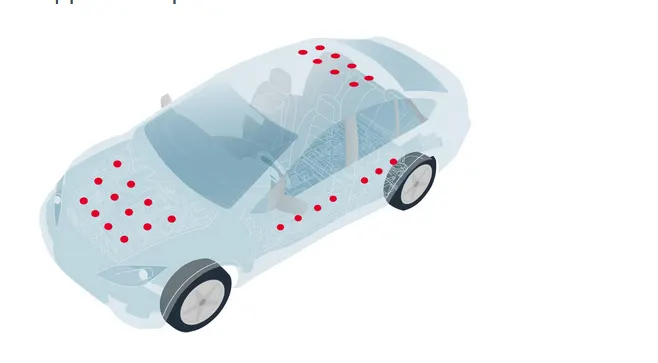
Location of Mastics on Hood
Position of Hinges
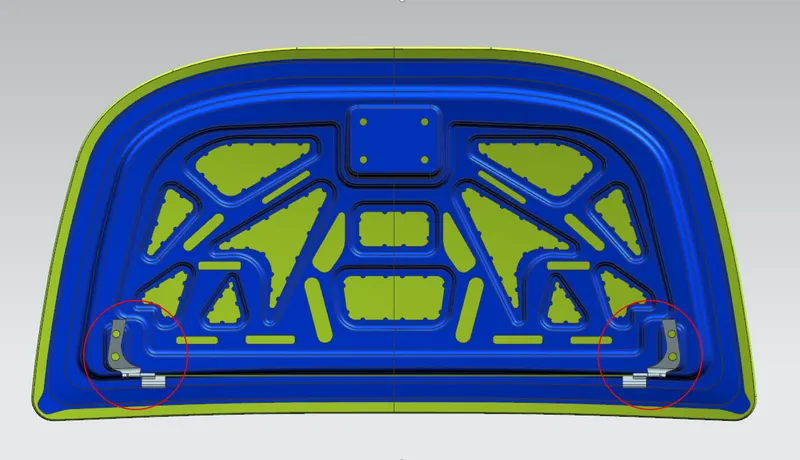
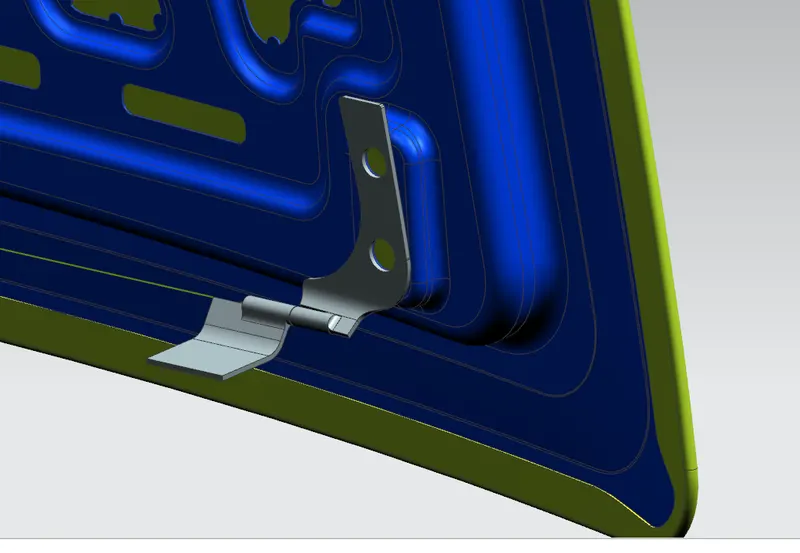
Positioning Striker and Hinges using Proper geometry and angle