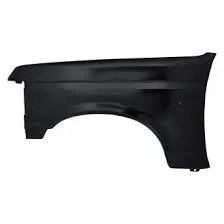
The first step: open straight snips plate: first select applicable cold coiling specification, cold coiling is opened flat; Then according to production material specification, will open cold coiling after flat and be cut into into the iron plate of corresponding size; Finally the iron plate after shear is cleaned to iron filings;
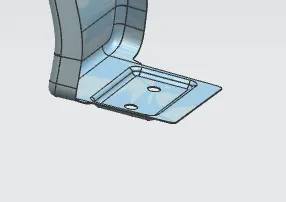
Second step: oil pressure, punch press: first iron plate is extended; Secondly to its trimming and punching; Then to its flanging and shaping; Finally after shaping completes, then carry out one-off hole-piercing; Completed the making of lappet plate body 1;
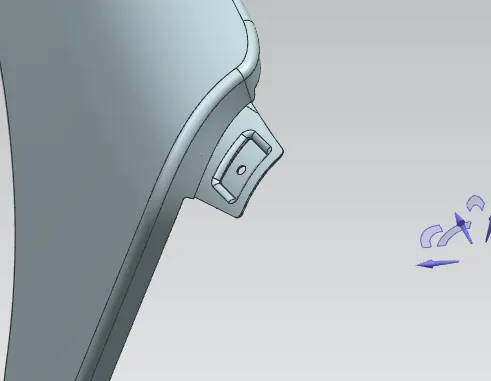
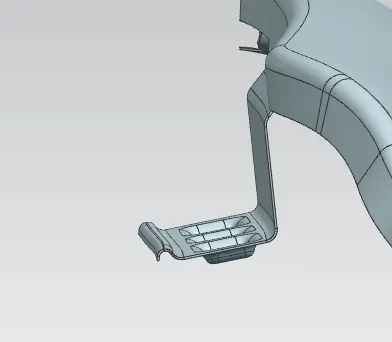
The 3rd step: the 1 smallclothes 2 of processing lappet: first iron plate is stamped out to required outline blank (blanking); Then to completing the further moulding of iron plate of outline blank; Finally it is carried out to punching;
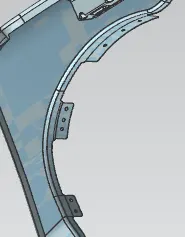
The 4th step: panel beating assembly welding: first 1 smallclothes 2 are carried out to spot welding M63 nut; Then 1 part point is welded on lappet; Finally lappet body 1 and 1 smallclothes 2 are carried out to sanding thorn and ending.
The trimming of described second step, punching can replace by Radium art.
The flanging of described second step, shaping can be replaced by punch press punching, steel seal technology generations.
The processing technology of automobile fender of the present invention is simple, production efficiency is high; Lappet plate body and smallclothes can separate machined, reduced the time of waiting for; Improved the operating efficiency of producing.
Embodiment recited above is described the preferred embodiment of the present invention, not the spirit and scope of the present invention is limited.Do not departing under the prerequisite of design concept of the present invention; various modification and improvement that this area ordinary person makes technical scheme of the present invention; all should drop into protection scope of the present invention, the technology contents that the present invention asks for protection, is all documented in claims.