Design of Passenger Car Rear Door considering FMVSS regulations for Rear visibility Criteria
Abstract:
A door is a hinged part which is used for entry and exit of the vehicles. Back doors are one of the type doors of the vehicle which are located next to the passenger seat which provides access to the luggage compartment. In most of the cars, these back doors are operated with the help of gas stay which in turn reduces the effort required to lift open the door. Some luxury cars have powered backdoor which in turn is driven by an electric motor. This kind of system is also called a powered trunk lid system. Hatchback or station wagons are sold as 3 door or 5 door models. In this case, the rear hatch is classified as door this is because it enters the passenger compartment. The naming is mainly used in Europe countries. In case of safety, the back door designed should meet the safety requirement for the rear collision.
Unlike other types of doors, the exterior side of the vehicle door contrasts in its design and finish from its interior side (the interior part is typically equipped with a door card (in British English) or a door panel (in American English) that has decorative and functional features.The exterior side of the door is designed of steel or other material like the rest of the vehicle's exterior. In addition, its decorative appearance, typically colored with a design, is intended to match with the rest of the vehicle's exterior, the central purpose being to add to the overall aesthetic appeal of the vehicle exterior.
A vehicle typically has two types of doors: front doors and rear doors.
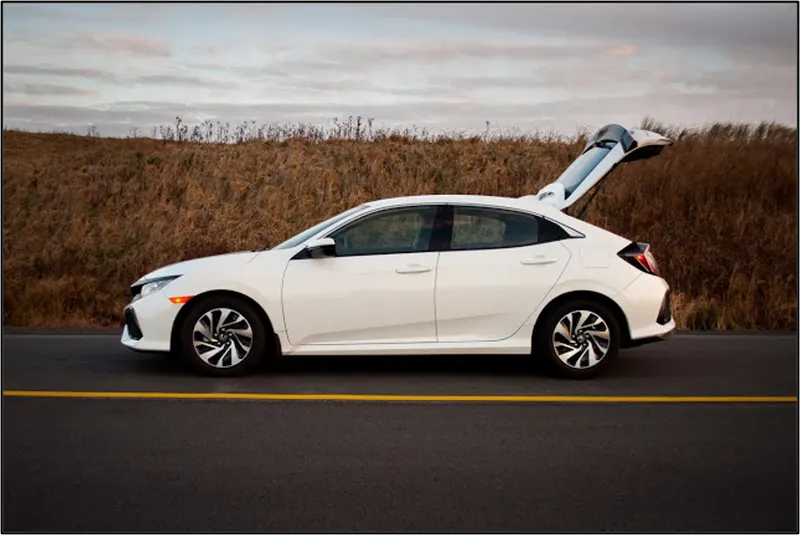
Types of Backdoor based on working positions:
The door or opening of a cargo area may be hinged at the top, side & bottom. If the door hinged in the bottom it is called as a tailgate.
- Top mounted
- Side mounted doors
- Bottom type
Top mounted:
This type of back doors is used in a station wagon, pickup trunk and some of the spot utility vehicles. Today's modern cars use top mounted tailgating system which are both powered and also gas stay supported. These top mounted tailgates provide greater rear visibility compared to side mounted or backdoor which have center pillars in it.
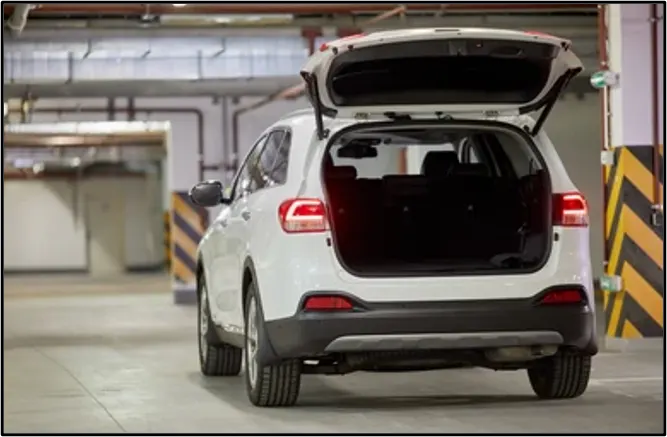
Side Mounted Doors:
As the name signifies the side mounted doors are the one which is used in the van type MPVs, SUVs, pickup truck vehicles. These side mounted doors or barn doors are a lot easier compare to top mounted doors. These doors are generally smaller in size and can be easily accessed. These doors are more convenient for the goods handlers for long pipe and lengthy components where one door is kept open. These door also save accidental head impacts. It is a lot easier to load and unload items in the side mounted doors.
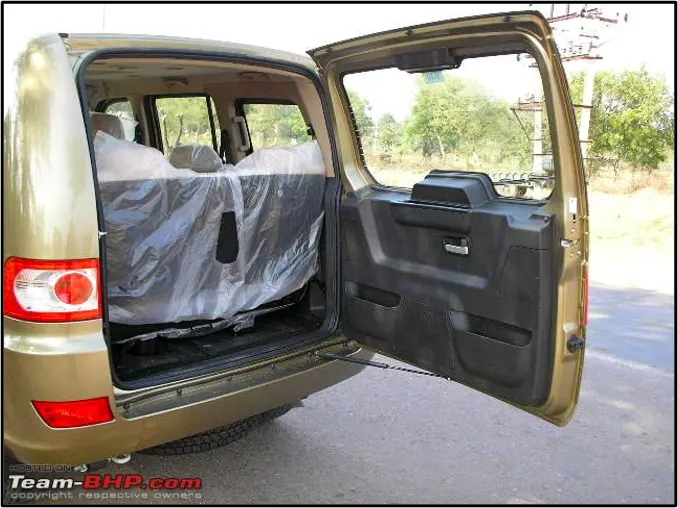
Bottom type:
This bottom type type backdoor system are used in the car type such as car, pickup truck and some luxuary SUVs. These are the most convenient type of back door in which the bottom split is used as a support or even as a table for the tour going people.
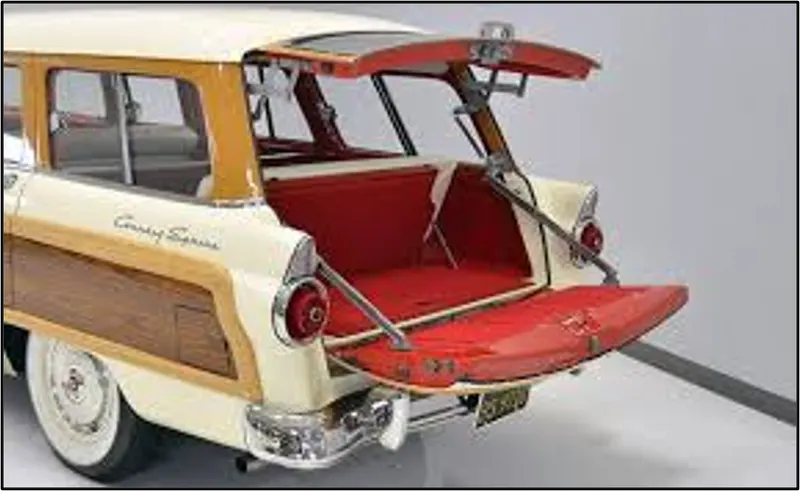
- Support Rod and Gas Stay
There are two types of support is there,
- Gas stay
- Support rod
1.Gas stay
spring stays are designed to be used on upward lifting doors, once you have opened the door slightly the spring will push the door to the fully open position, Euro fit stock various size springs depending on the door size requirements. This is mostly used for where the car bonnet weight is heavy.Struts contain nitrogen gas under pressure and some oil to damp movement and to lubricate the seals.
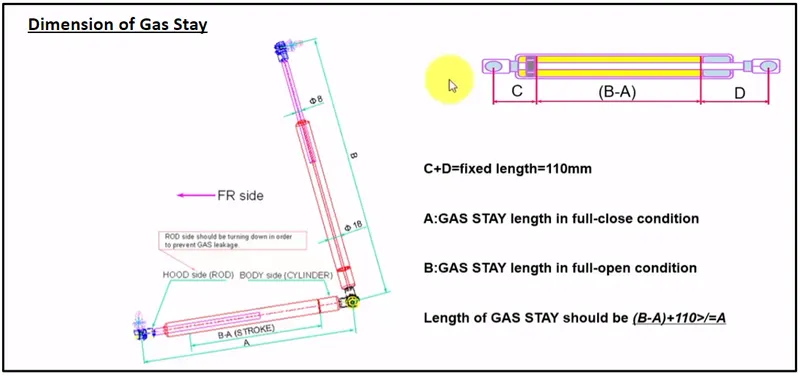
- Support Rod
1)Support Rod can be mounted with grommet side on the engine compartment of Body and rod locking hole on hood or vice versa.
2)Grommet and the clip of the rod are standard parts.
Support rod is used to increase the support force, automatic buffering, stable and reliable, strong load-bearing capacity, safe use, not easy to fall, avoid hot hands, support the engine more easily, and balance the force without shaking.
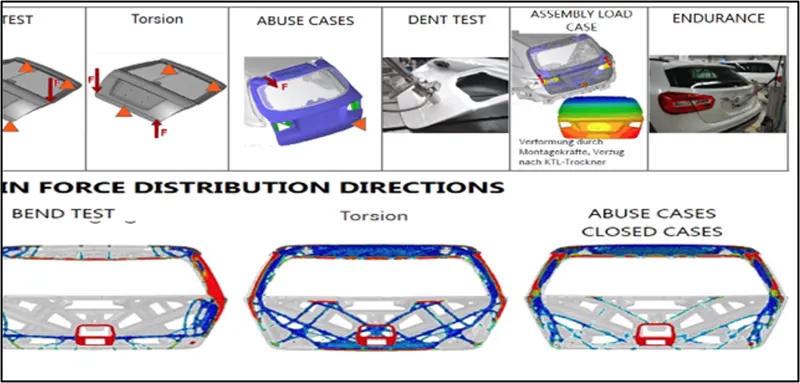
Load Case Analysis:
- Bend Test
- Torsion Test
- Abuse cases
- Dent test
- Assembly Load Cases
- Endurance test
Tooling Axis:
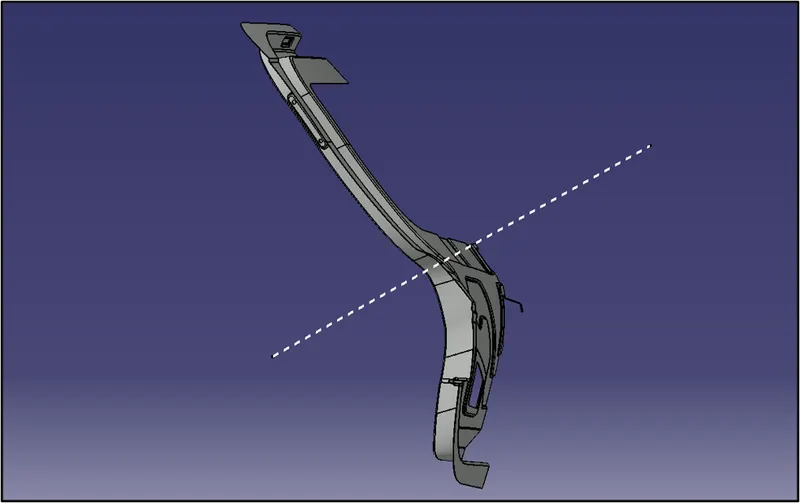
Tooling axis is nothing but the direction in which the Core and Cavity Opens and Closes.Design Engineer works is to Analyse the Class A Surface and find out the best possible tooling direction keeping in mind all the draft angle is with respect to the tooling axis so that the Component can be easily ejected from the moulds.
Latch and Striker tajectory:
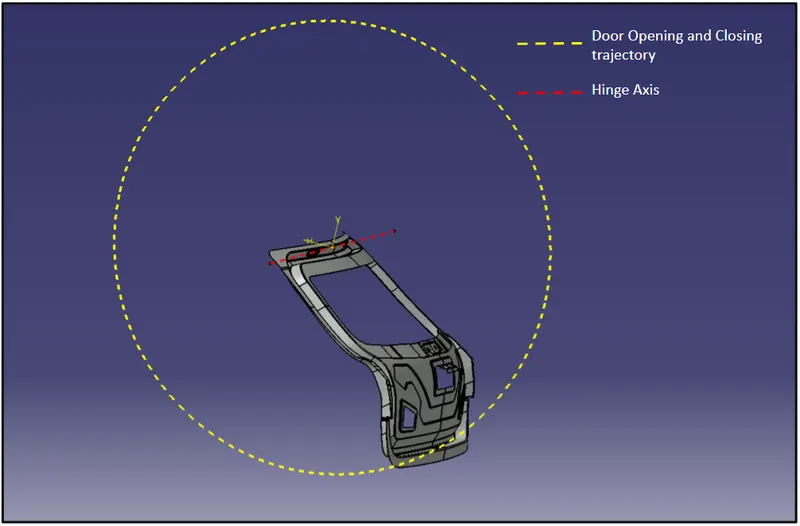
To define the opening and Closing Trajectory, the hinge and Latch are positioned based on the Hinge axis and Trajectory. The Circle drawn should perpendicular to the Latch’s Striker to satisfy the condition. Based on the Rotation trajectory the Hinge Axis, Latch Striker and predefined Gas Stay are correlated for smooth kinematics of door opening and closing.
Based on the type of Gas Stay, Door Weight and Kinematics the distance between the Gas Stay and Hinge axis is 60-90mm and an angle of 85-90.
Materials and manufacturing method
The materials used for manufacturing of front hood it was carbon fibre/epoxy. The balanced woven fabrics Twill 2X2 by 200g/m2 were used. The distribution layers were [90/0 ±452/90/0].
For the matrix L285 epoxy resin and hardener 286 from Lange-Ritter (Germany) was used. The mixing ratio according to the company prescription was 100:40 parts by weight. The epoxy blocks were used to obtain the front hood mould. There was milling by CNC machines. To have a sufficient sealing surface of the vacuum bag the borders of the mould were extended by 100 mm. Two moulds were manufacturing, one for exterior of the hood and one for back part (Fig. 5). The surface of the moulds was mechanical processing by glass paper sanding by 1000 grit.
Deep drawing is one of the most widely used processes in Hood manufacturing. Apart from its use in many other sectors, it is applied in the automotive industry for the manufacturing of car body parts.
The deep drawing process is a forming process which occurs under a combination of tensile and compressive conditions. A flat sheet metal blank is formed into a hollow body open on one side or a hollow body is formed into a hollow body with a smaller cross-section.
Deep drawing processes are divided into three types:
- Deep drawing with tools
- Deep drawing with active means
- Deep drawing with active energy
In the automotive industry, deep drawing is usually carried out using rigid tools.
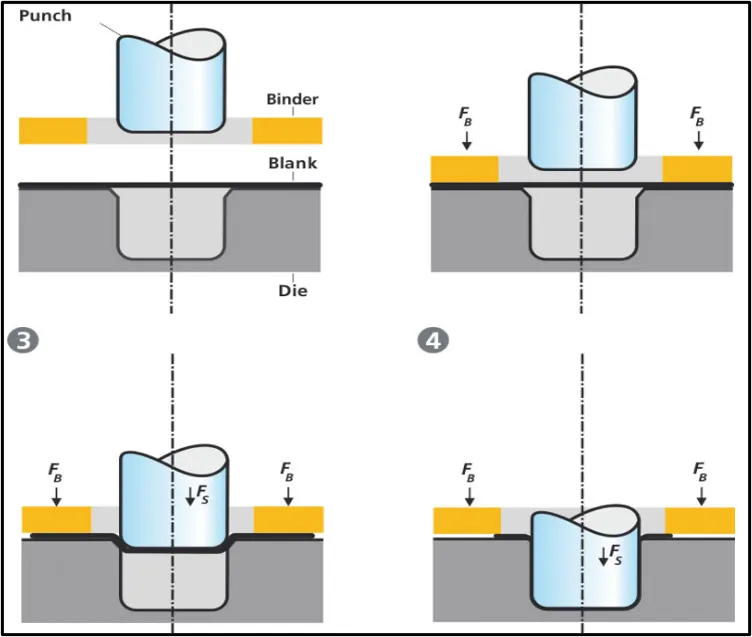
- The figure illustrates the deep drawing process. The rigid tools consist of a punch, die and binder. In deep drawing, the plate holder closes after the metal sheet blank has been inserted.
- Next the sheet is clamped between the die and the binder. This process slows down the flow of the sheet while it is being drawn and thereby prevents wrinkles from forming under the binder. The punch stretches the sheet over the die radius and forms it in the die. The amount of punch force necessary for forming is thereby continually increased up to the lower dead center of the punch.
- Whereas in pure deep drawing there is no reduction of sheet metal thickness, forming is achieved in stretch forming purely as a result of a decrease in sheet metal thickness. Stretch forming is extensively used for the forming of only slightly curved parts with low depth of draw (e.g. roofs, doors).
- When drawing complex car body parts in practice, there is usually a combination of stretch and deep drawing involved. It is necessary that the sheet metal is stretched as well as possible without reaching the material’s limits (e.g. splits, wrinkles).
- There are approximately 300 to 400 sheet metal parts which fit together to form the body of a car. In order to manufacture high quality sheet metal parts optimally for their particular use, specialized software simulates the complete deep drawing process.
Spring back Effect:
Springback is the geometric change made to a part at the end of the forming process when the part has been released from the forces of the forming tool. Upon completion of sheet metal forming, deep-drawn and stretch-drawn parts spring back and thereby affect the dimensional accuracy of a finished part.
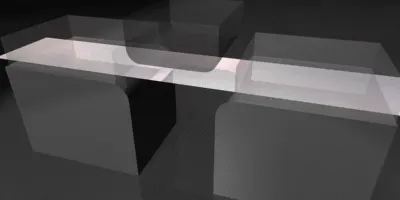
Through the application of new materials, the number of problems increases. Forming parts made of these materials are more affected by springback than parts made from conventional deep-drawn steel. Concerning classic sheet metal defects such as splits and wrinkles, strain in the sheet metal is decisive. If springback occurs, such models are not enough to predict a deformation. In this case, the stresses are decisive and a considerably higher accuracy is crucial.
During the development of tools, springback is compensated by software in order to remove the part from the tool straight away in the required dimensions. Intense tryout loops, which occur at a very late stage in the development of the tool, are reduced to a minimum. Simulation software can not only detect springback early on, it can also compensate for it. In this way, tooling processes are improved and manufacturing costs are significantly decreased. Springback compensation thus minimizes the risk of costly changes to tools or processes later on.
Trimming:
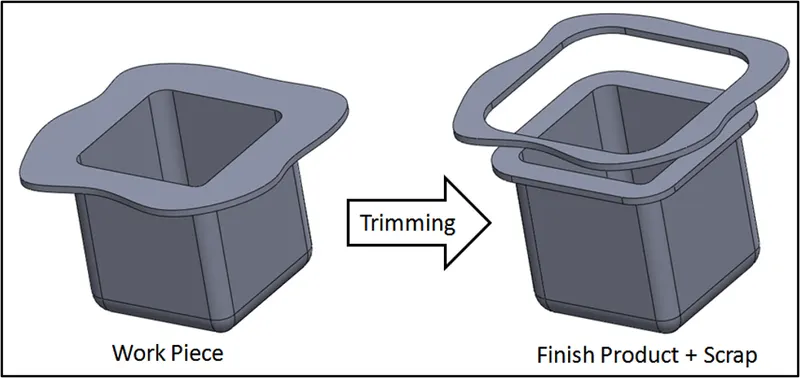
In the Trimming process,excess metal that is necessary to draw the part is cut away from the finished part.
Hemming:
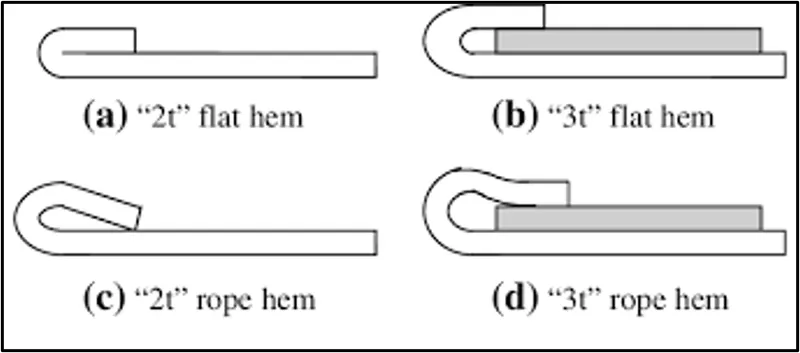
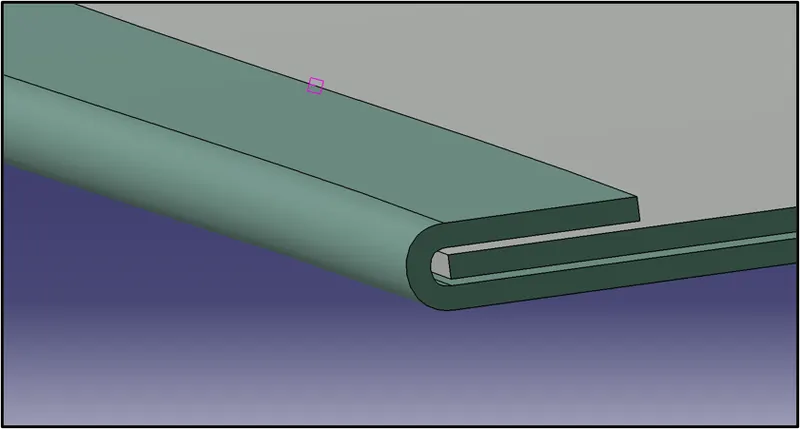
Hemming is a sheet metal forming process in which sheets are joined by bending it usually to 180°. Automotive body panels and automotive parts such as deck-lids, trunk-lids, doors, hoods and tailgates are formed by hemming process.Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
Design of Car Tail Door using Catia V5
- Class A surface refers to those surfaces which are VISIBLE and abide to the physical meaning, in a product. This classification is primarily used in the automotive and increasingly in consumer goods.the Class A Surface will be given by Styling team.
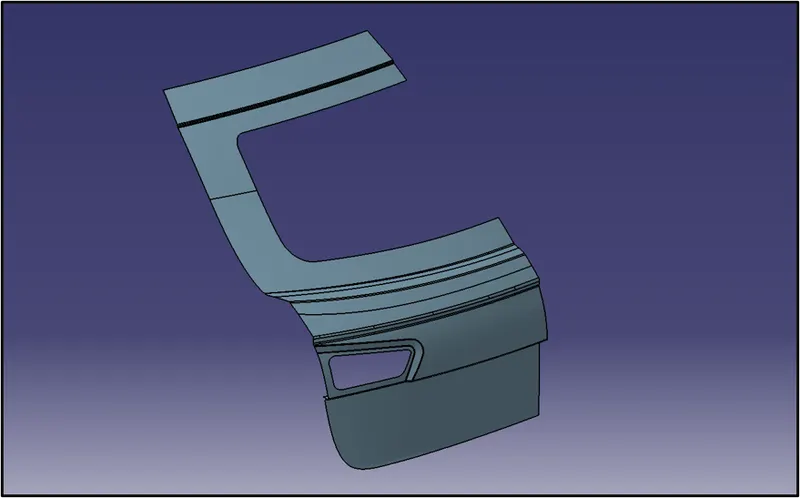
- By using the A class surface and Master section the Inner panel of the hood has been designed as follows:
Design of Back Door consists:
1.Upper Outer Panel
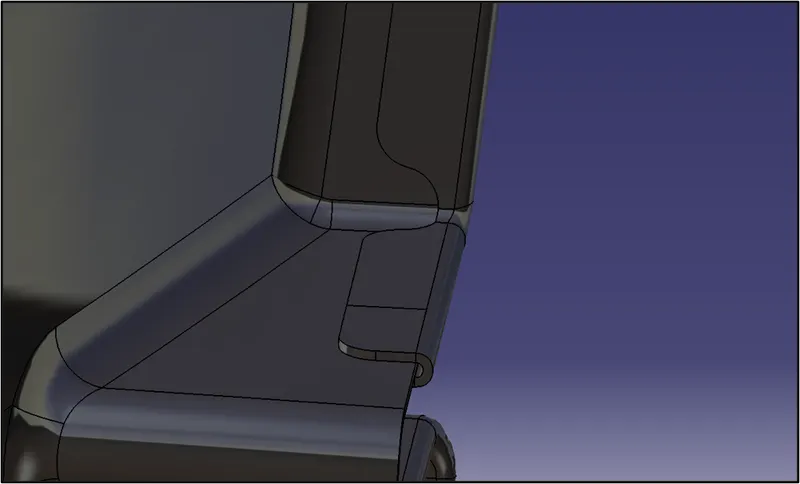
Design of outer panel is mainly inspired by aesthetic but there is some engineering also to it. Here main purpose of outer panel is to cover the inner panel to provide aesthetic look at the same time Panel must be curve & sleek so that it behave aerodynamically and air hitting from front reflect from it efficiently. So here rather than using seam and spot welding we use hemming method to join outer and inner panel. Hemming is a type of folding or wrap-around process in which roller bend and press the extrapolated flange in a way that it holds the inner panel firmly, then a sealant is also provided in between them under folds to get water tightening.
While hemming we provide relief around corner as it helps in easy hemming or undistorted hemming while roller took turn around any corner.
It’s thickness is also 0.75 mm maximum
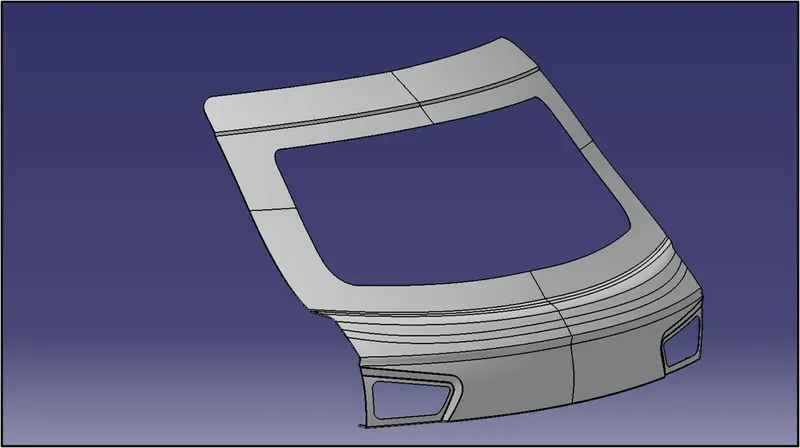
In order to join the inner panel with the outer panel we have provided the hemming in the outer panel where the spot welding or laser brazing takes place.
Hemming is a sheet metal forming process in which sheets are joined by bending it usually to 180°. Automotive body panels and automotive parts such as deck-lids, trunk-lids, doors, hoods and tailgates are formed by hemming process.Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
2.Lower Outer panel
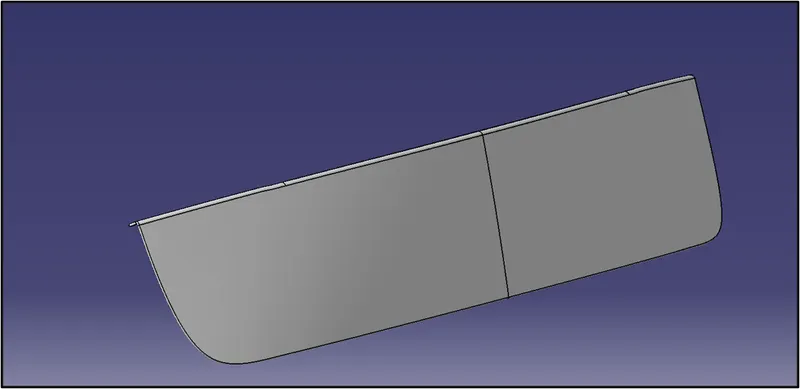
3.Inner Panel
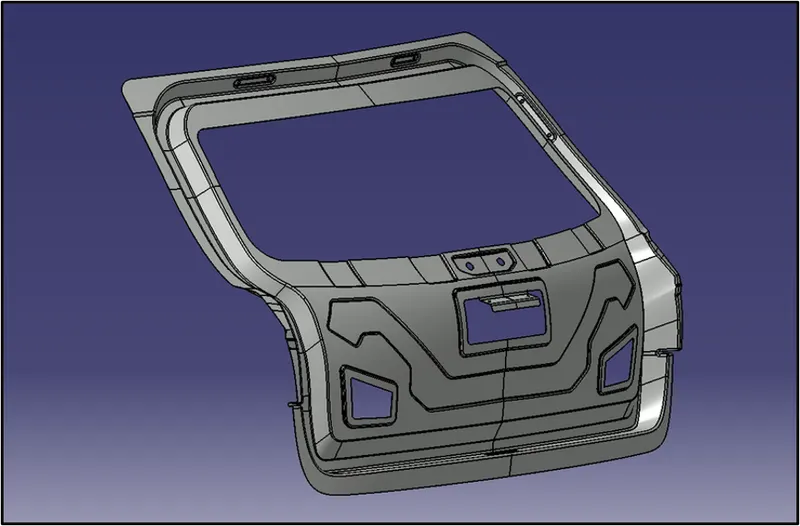
For the Inner Panel we have provided the Embosses to increase the strength of the panel locally.
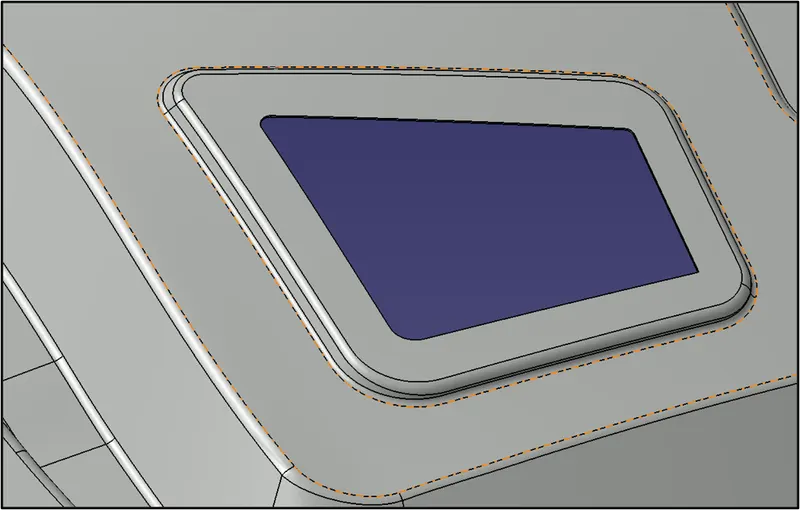
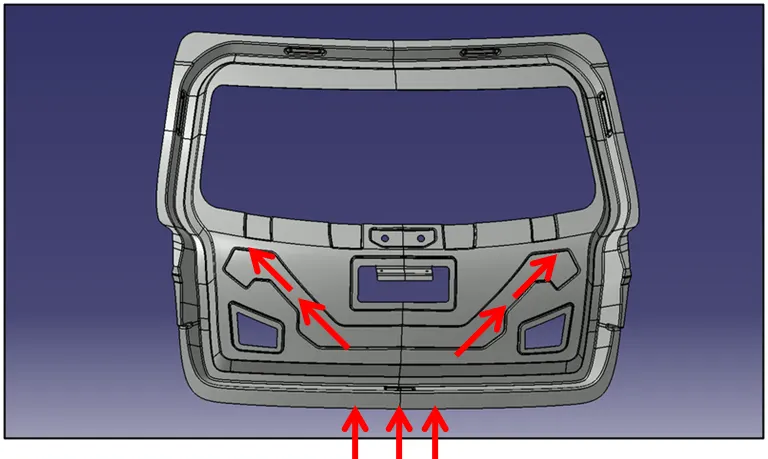
Embosses has been given to create extra strength in inner panel and embosses design needs to be inspired by force dissipation phenomena like here I have made embosses in a way if any object hit from front most of the force will get dissipated by its design towards the upper left & right corner so that less force reach at occupants end.
Distribution of force in case of collision:
The inner panel is designed in such a way that in case of collision ,the impact force must goes in outward direction ,so that the impact on the driver and front passenger must reduce.
Hinge and hinge reinforcement:
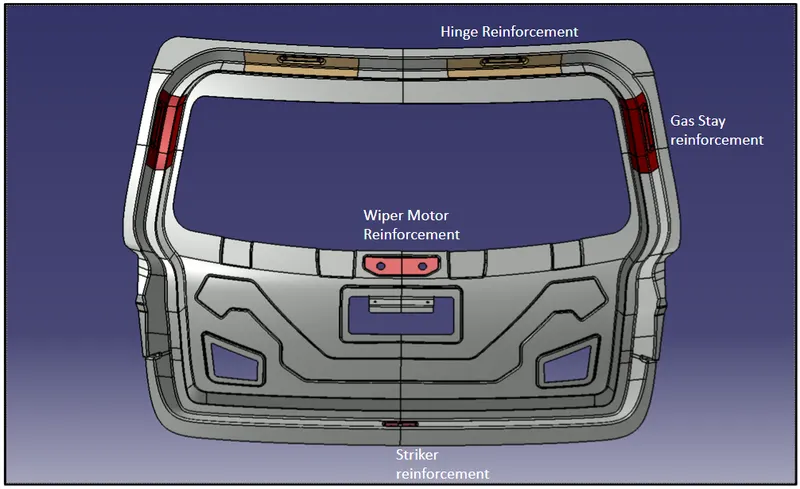
Hinge is a mechanical bearing that connects two solid objects typically allowing only a limited angle of rotation between them it has one degree of freedom. So here hinge is providing rotation to backdoor about it’s own axis and also keep it connected to the roof portion.
So while creating space for hinge we need to provide emboss there, because of emboss and hole its strength got affected so to compensate that we provide hinge reinforcement.
Hinge reinforcement has thickness around 1 to 1.5 mm to provide reinforcement to hinge embossed region.
Draft Analysis
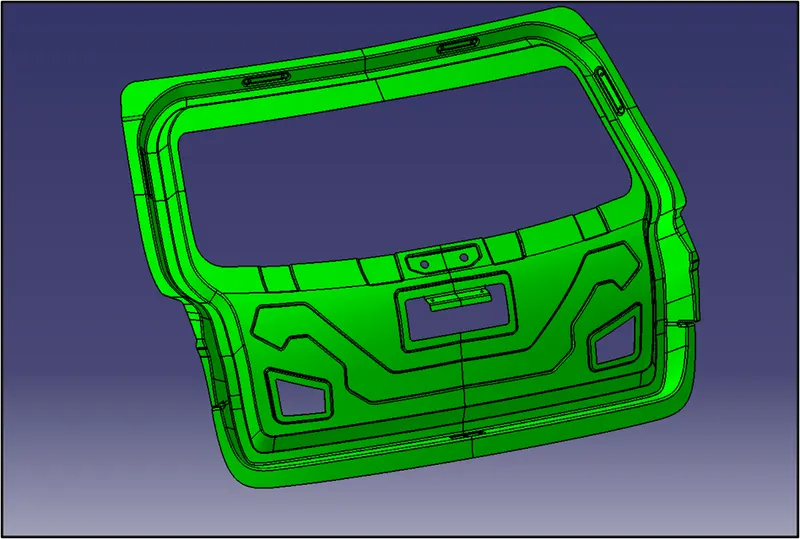
Parts Cannot be ejected from the tool if it is at 90 degree surface.for the reason,A small Draft angle is to be provide for each and every surface s of the Component in order to easy removal of component from the moulds without any defects.Draft is the angle in which the part is tapered to aloow it to release.Most of the part require minimum 7 degree to 10 degree however 7 degrees are widely accepeted in sheetmtal component design.Draft Analysis is the technique used to analise weather our designed product are manufacturable with required conditions or not.
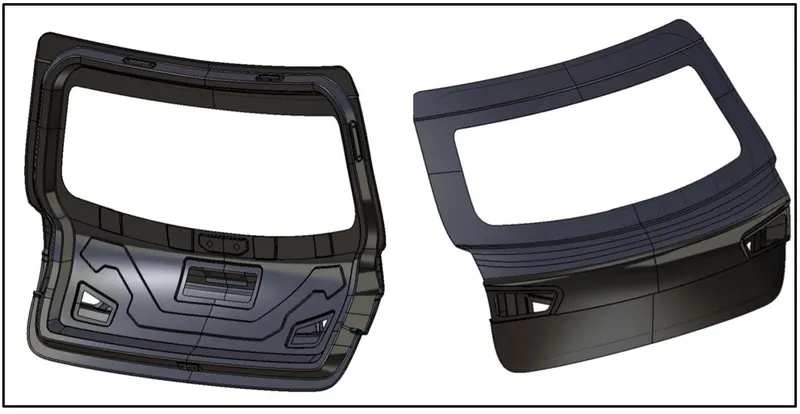
Final Design:
Conclusion:
Thus the Car hood is designed using the given A Class surface and given mastersections as well understood the design parameters to be considered for the hood design.