Design of backdoor
Design of Back Door
Abstarct
This report presents the design and assembly of the car’s Backdoor (Tailgate) along with the justifications being carried out.
Objective
To Design a car’s backdoor in NX CAD using the given master section and design parameters.
Introduction
An automobile back door or Tailgate is the panel that covers the boot (or trunk) of an automobile. It enables access to the main luggage compartment. A hinge allows the boot lid to be raised, while devices such as springs or gas cylinders hold it up in the open position The Backdoor is an assembly of many parts such as inner panel, outer panel upper, outer panel lower, and Reinforcement. The inner panel is attached to the outer panel using mastic sealant.
Components
- Backdoor upper panel outer
- Backdoor upper panel lower
- Backdoor inner panel
- Left side hinge reinforcement
- Right side hinge reinforcement
- Left side gas stay reinforcement
- Right side gas stay reinforcement
- Latch and striker reinforcement
- Wiper motor reinforcement
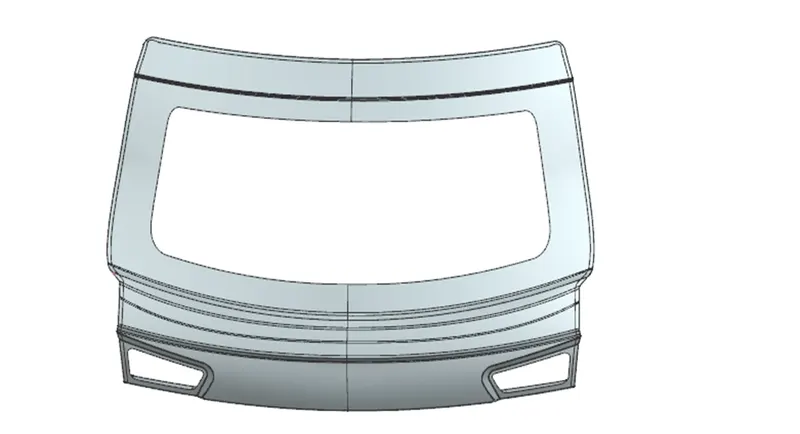
Backdoor upper panel outer
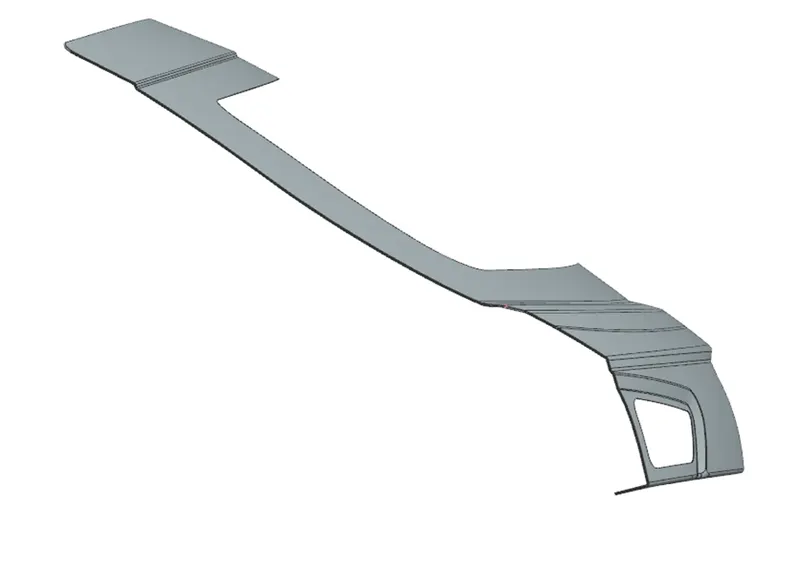
Backdoor outer panel lower
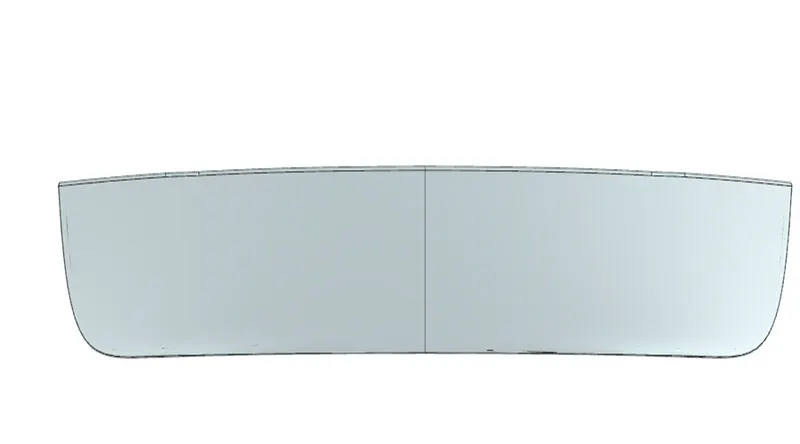
Backdoor inner panel
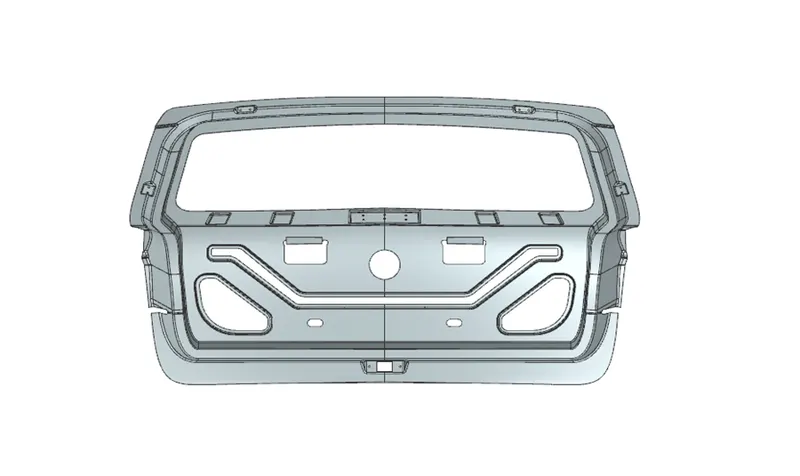
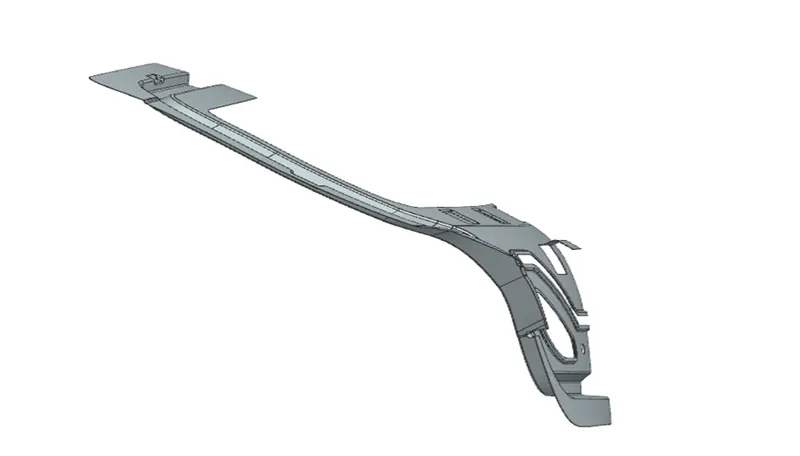
Left side hinge reinforcement
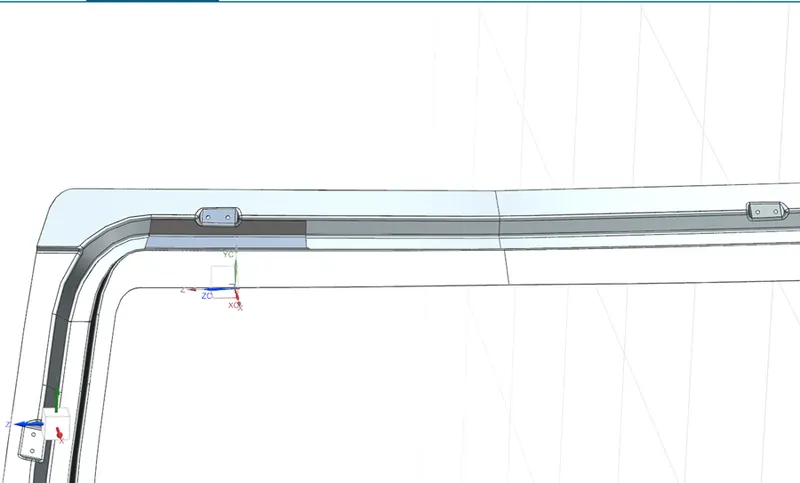
Hinge reinforcement right side
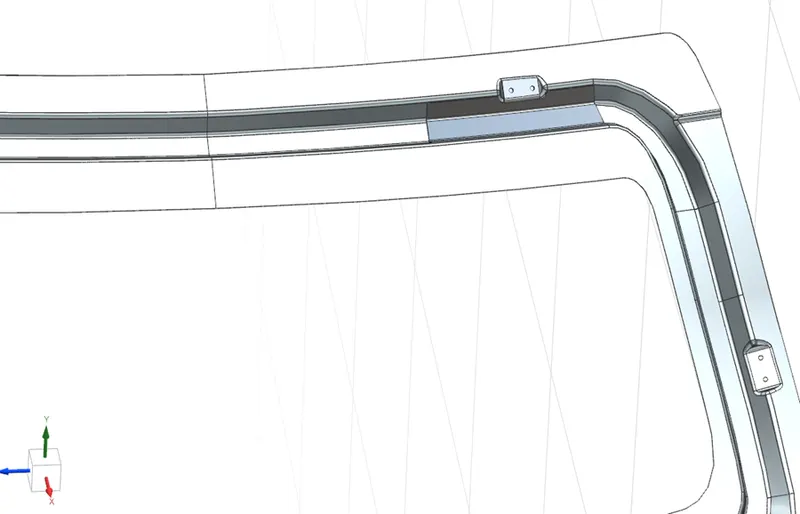
Left side gas stay reinforcement
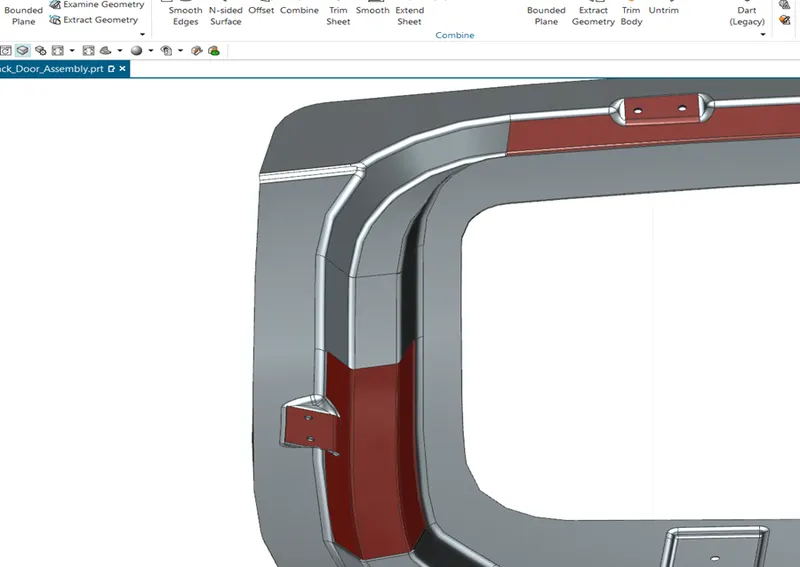
Right side gas stay reinforcement
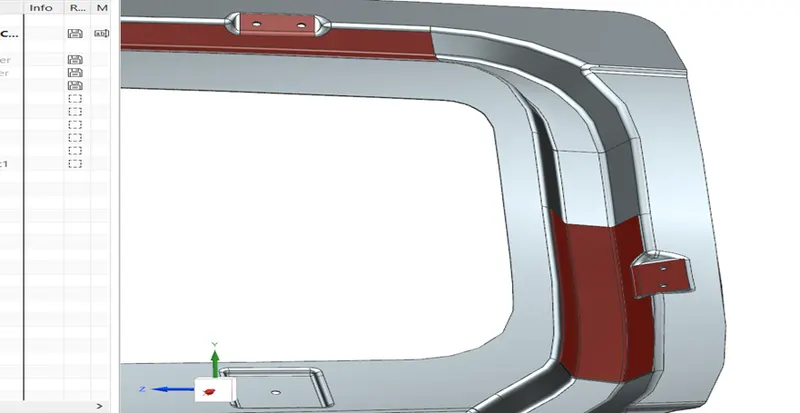
Wiper motor reinforcement
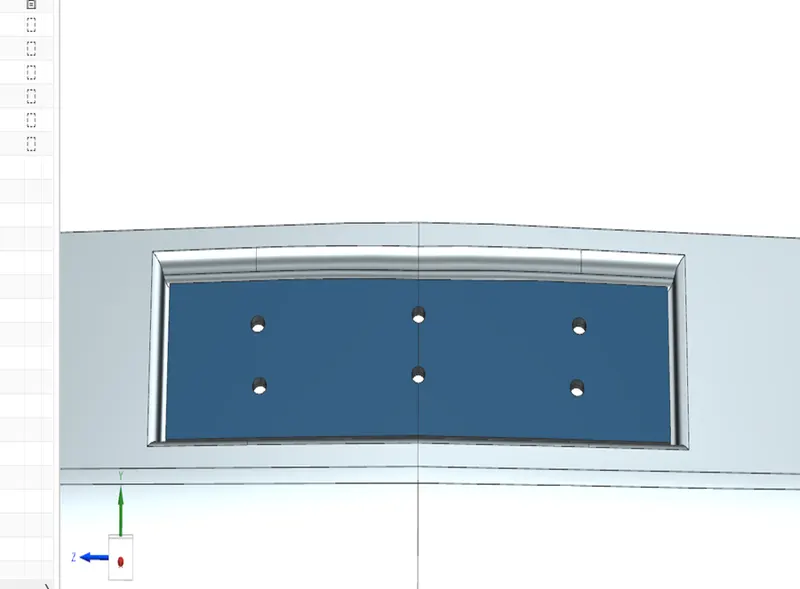
Latch and striker reinforcement
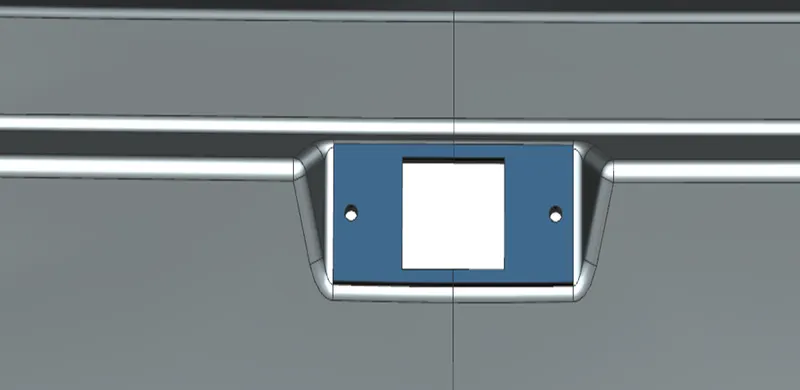
Mastic sealant region
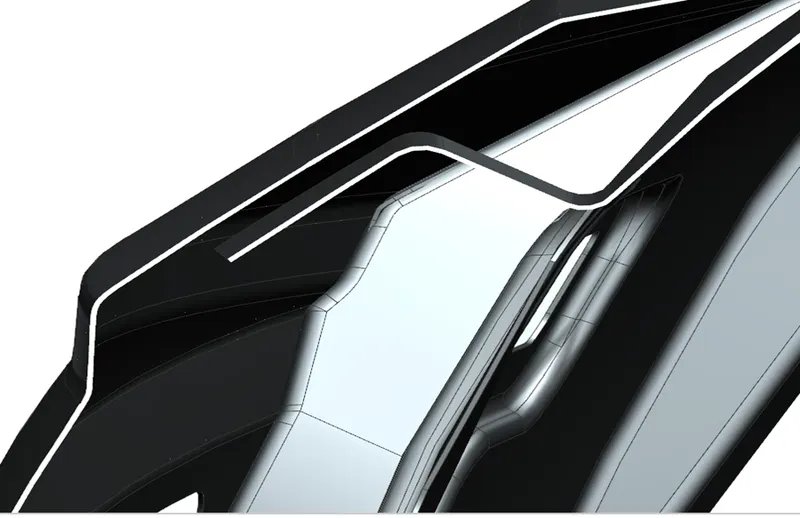
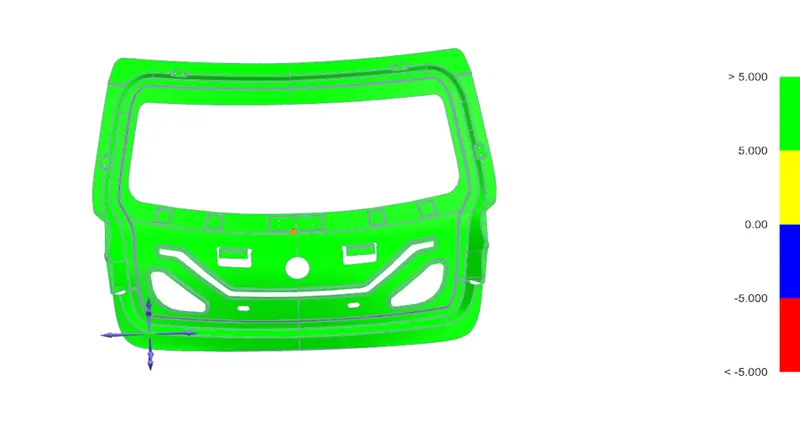
Draft Analysis
The design has been analyzed using the draft analysis tool in NX CAD with having 5-degree allowance.
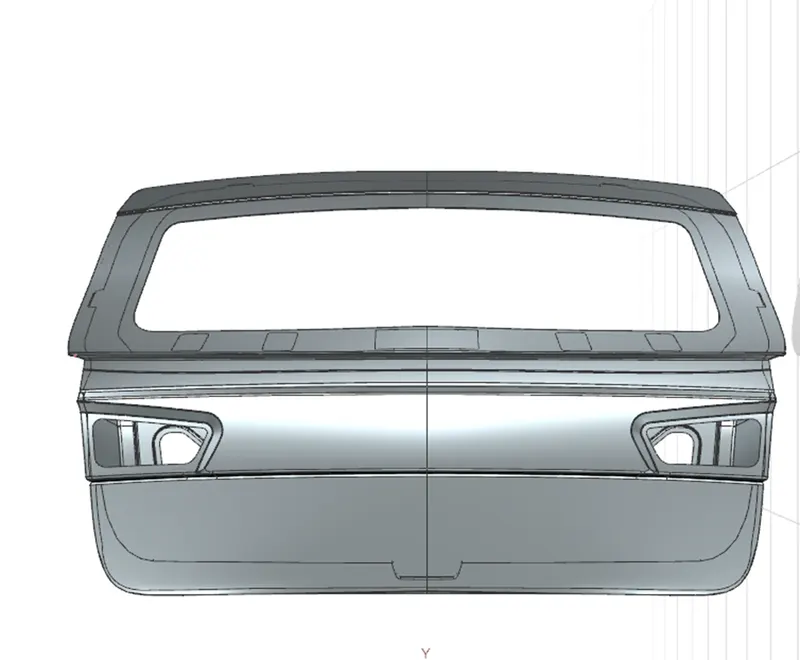
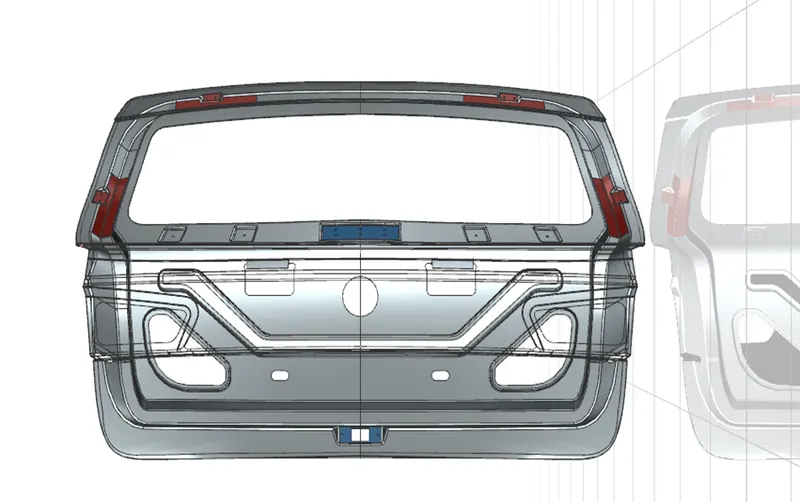
Final Assembly
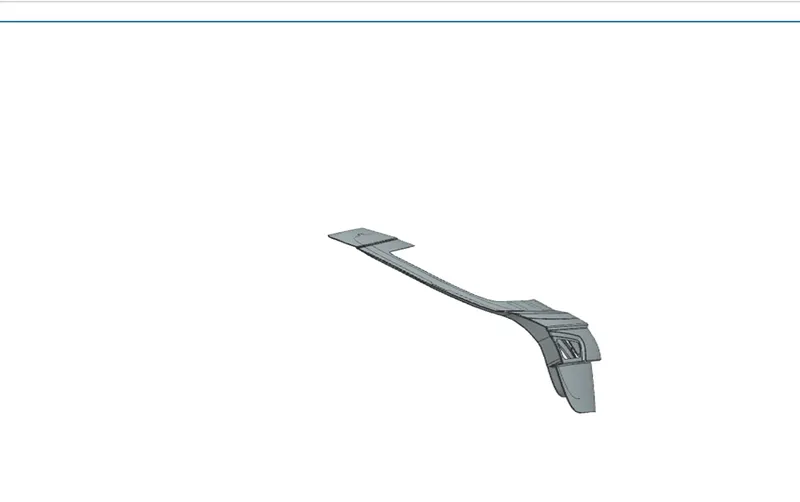
Features used in designing
- Offset surface - The Offset Surface command to create an offset of one or more existing faces.
- Offset in face - To create offset curves on one or more faces from connected edges or curves on the surfaces.
- Trim Sheet - To trim sheet bodies to intersecting faces and datums, and projected curves and edges.
- Trim body - To trim one or more target bodies using a face or plane.
- Edge blend - The Edge Blend command to round sharp edges between faces.
- Face blend - The Face Blend command to add tangent blend faces between two or three sets of faces.
- Emboss - The Emboss Sheet command to modify a sheet body by adding faces of a solid body, as if the solid body was pressed into the sheet body.
- Sew - The Sew command to join two or more sheet bodies into a new single sheet body.
- Thicken - The Thicken command to offset one or more connected faces or sheets into a solid body.
- Project curve - The Project Curve command to project curves, edges, or points that are external to the sketch, onto the sketch along the normal of the sketch plane.
- Extrude - The Extrudecommand to create a solid or sheet body by selecting a section of curves, edges, faces, sketches, or curve features and extending them a linear distance.
Back door manufacturing process
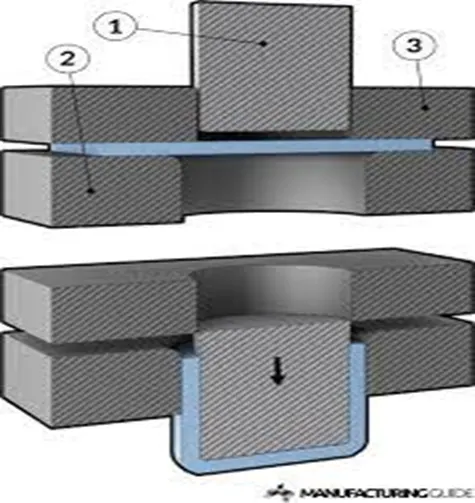
1.Deep drawing:
Deep drawing, is a sheet metal forming process in which a sheet metal blank is radially drawn into a forming die by the mechanical action of a punch. It is thus a shape transformation process with material retention. The process is considered “deep drawing” when the depth of the drawn part exceeds its diameter. In the Quintus denomination of deep drawing a flat sheet, metal blank is formed over a rigid, shape-defining, movable tool half, pushed against a flexible rubber diaphragm, which is supported by uniform hydrostatic oil pressure. The process results in scratch-free parts regardless of the sheet thickness or complexity of the tool, including undercuts. High forming pressure ensures close tolerance parts direct from the press with little or no secondary hand work required.
2.Hemming
Hemming is a technology used by the automotive industry to join inner and outer closure panels together (hoods, doors, tailgates, etc.). It is the process of bending/folding the flange of the outer panel over the inner one. The accuracy of the operation affects significantly the appearance of the car’s outer surfaces and is, therefore, a critical factor in the final quality of a finished vehicle. The Hemming process can be carried out in diverse vehicle components: closures (Hood, doors, tailgates), sunroof, fenders, wheelhouses, and in special applications such as fuel lid, brand, and special parts. Both the outer perimeter and the inner frame of the part can be hemmed.
There are two types of hemming operations
- Tabletop hemming
- Roll hemming
Tabletop hemming
In tabletop hemming or conventional die hemming process, the flange is folded over the entire length with the hemming tool.
Roll hemming
In the roller hemming process, a robot guides a small roller across the flange to fold a sheet onto itself or onto another sheet. The process is oriented to low-volume automotive applications, providing a distinct advantage in manufacturing closures and subassemblies with developed flanges.
Result
Final Assembly of the Back door