Week 8:- 3D Finishing - Challenges 1
3D Finishing
What do you understand by the 3D finish process?
3d Finish is a process where the design is being completely finished and to be ready for final simulation and 2d detailing.
A- While finishing the design the nominality is checked which ensures the easy assembly of all the units. The hole concentricity and hole sizes are checked which ensures the assembly of different parts.
B- The gaps between the different units are checked to ensure the proper individual working of different units. Design the rough locators, which help to load a panel in correction orientation.
C- Design the pneumatic lay-outing for pneumatic connection. Gun study is the major and most important part of 3d finishing.
D- Selection of sensors, Solenoid valves as per the requirement and implementation in design.
E- Fasteners are implemented as per the hole size and the standard color codes as per the customer requirement are applied to differentiate the type of hole whether its dowel hole, Threaded hole, or clearance hole.
F- Renaming of the assembly and the part is done to give every part a different identity so everyone can identify in which assembly this part is going to be fit.
G- After doing all these things the model is sent for simulation and 2d detailing.
What are the points need to be taken care of while finishing the design?
A- Hole Concentricity and Hole Sizes:All part holes concentricity and hole sizes are checked for easy assembly while finishing the parts.
B- Machining Area:The machining area in every part should be defined and the machining area should be highlighted by using a standard color code. Machining is to be done on parts to properly Mount with mating parts. Machining only on desired faces reduces cost and saves time. And also Machining increases the accuracy of dimension. So before going to simulation or detailing machining area should be defined.
C- Nominality:All unit dimensions should be maintained nominal to facilitate easy assembly of the unit.
D- Holes Colouring Standard:In a 3D finish, hole coloring should be done because it helps to identify what type of hole it is. It depends on customer standards. Customer-specific color like:
The dowel hole should be given blue color.
The threaded hole should be colored yellow.
Counterbore, open hole should be given cyan blue color.
E- Pneumatic Lay outing:The pneumatic lay outing is a collection of different pneumatic pipes which work as an inlet to the pneumatic cylinder. It should be done properly for the proper functioning of the units.
F- Gaps Checking:The gaps between the different units are checked to ensure the proper individual working of different units.
G- Fasteners Implementation:Fast should be implemented in all the units as per the requirement and load on the part.
H- Avoiding Clash Between Different Parts:A proper gap should be maintained between units to avoid clashes between the different units.
I- Mylar Splitting as Per Panel Profile:Mylar splitting as for panel profile should be confirmed while finishing the design.
J- Proper Renaming of Parts or Assemblies as Per the Standards:Proper renaming of parts and assembly should be done while finishing the design and hence we can identify each and every part easily with Unique Identification.
What are rough Locators & what is their use?
- A rough locator is a part designed to guide the panel, to locate the car panel onto the pins accordingly. A rough locator can be of standard part or a make part.
- Rough locators also work as Poka-yoke. Poka-yoke is a Japanese concept used for mistake-proofing.
- Rough locators are also used to help to locate the workpieces in the automation process. Locating refers to the desired location where you want the workpiece to be when it is getting worked on either by a person or a team or a robot.
- The accuracy of the locating components directly affects the consistency and how the final product will come out. This is why these components are essential to our setup.
- It can be also called fool proofing method. Because without a rough locator the part cannot be loaded incorrect position.
- The rough locators are set accordingly to the angle of the respective panel and hence the part can be loaded in a defined direction and orientation only.
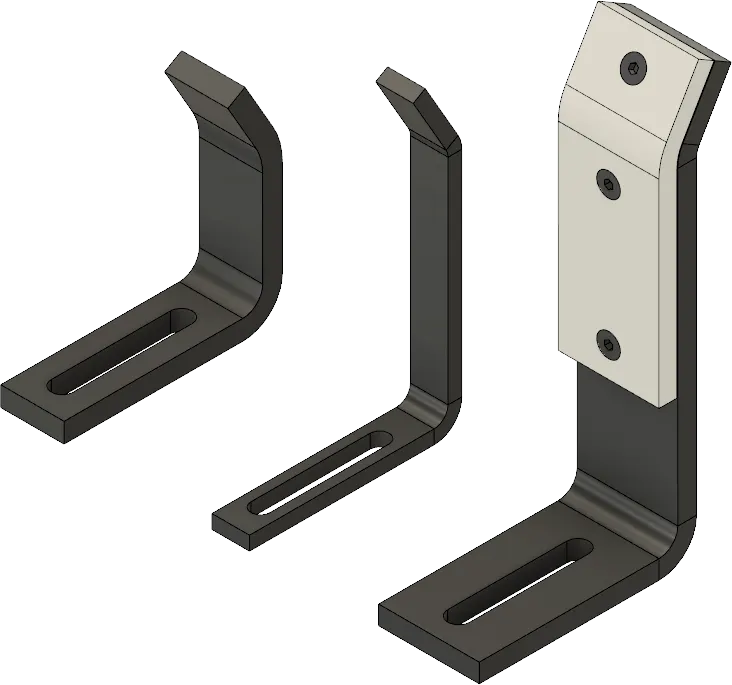
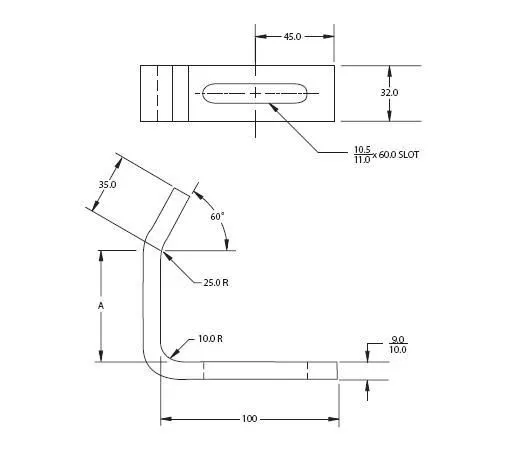
What are the points you need to consider while designing a rough locator?
- Rough locators should be placed at the edges of the car panel, which it has to guide.
- Rough locators has to be placed in the same angle of the car part edge with a minimum distance of 2-5 mm from the edge of the car panel.
- Rough locators should guide the panel in pin arresting direction.
- Rough locators should start guiding the panel before 10 to15mm to the start of the pin engagement.
- Rough locators should be designed with entry angle for the car panel. Generally it ranges between 30-45 degree.
- Rough locators should be designed with two slots to mount the easy adjustments.
- The slots should be in the direction of car part guiding.
- Rough locators must be designed with slots for ease of adjustment.
- Rough locators should have minimal part contact so that the operator can load the part to work location with ease. Excessive part contact may cause difficult part loading and unloading.
What is the gun study process?
- Welding is predominantly used in automobile industries & requirements for fixtures that ease the welding process is a continuous development task in any industry.
- Car Body-In-White (BIW) is a complicated steel structure including 300-500 sheets with complex shape & are assembled by means of welding in a high rhythm through 55-75 robotic work stations.
- The foremost step taken before starting the design of welding fixture is to arrive at the spot weld locations.
- The location & orientation of other critical units of the fixture including clamps, locators etc., are decided based on the weld spot distribution.
- It includes information of weld gun detail, weld matrix & weld points. There are two types of weld points geo weld point & re-spot weld point.
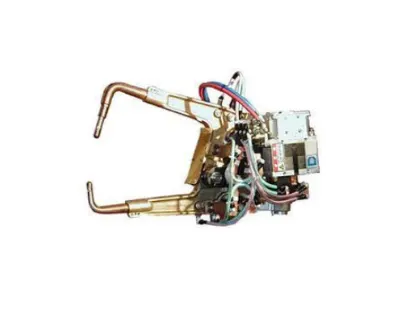
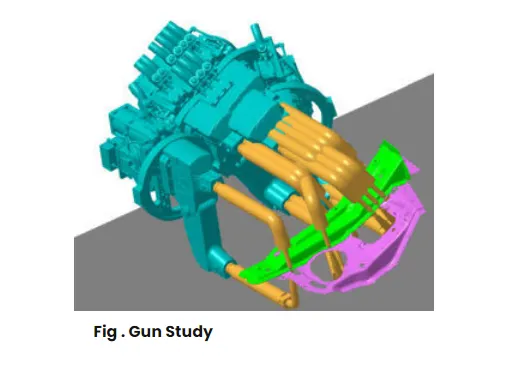
In the automobile business, welding is a procedure that is frequently used, and standards for the welding process are constantly being improved. Welding is used to put together the sophisticated construction known as Car Body-in-White (BIW). Establishing the location of the spot welds is the first step before designing a welding setup. The weld spot distribution dictates the positioning and orientation of other crucial fixtures components like clamps and locators. The weld matrix and welding position are shown in the figure above, along with the spot welding tool that will be utilised.
Weld spots will come in two varieties: geo weld points and respot weld points. In the first stretch, the geo weld locations are welded, and in the second stretch, the respot welded places are welded. Gun studies comprises learning about the weld gun, a portable device used for semiautomatic welding of parts and components. The weld gun will be used for the operation according on the part's size, thickness, and other factors. If the welding gun hits the fixture unit, the fixture is redesigned or moved, which validates whether the welding gun is falling or not. If the cannon hits the fixture unit, the fixtures are changed, but the weld spot locations are kept the same.
What re the points need to consider during the gun study?
The number of weld spots on the panel and the amount of time needed to spot each weld define the overall time needed to complete all of the weld spots. The axis of the weld spot in the direction of welding must be parallel to the weld surface. We can simulate each model's behaviour in the work cell over time if we have one or more device models and want to programme them. Each device's instructions are coded using sequences.
The sequence establishes how the devices will move, be used, and function. Based on the location of each tag point in relation to the home location, the type, speed, and acceleration of the motion can be used to determine the cycle time for each device connected to the sequence. In this way, the robot cycle time is correctly calculated. In order to make sure that the welding process is collision-free, a simulation is run once all of the devices have been sequenced.
What is pneumatic routing?
Pneumatic systems must be effective and leak-free. Sometimes they aren't because of improper tube line routing brought on by a lack of knowledge, a lack of planning time, or even both. Planning the route of tube lines takes time, but it can be quite beneficial, especially in systems that are complex. After sizing the tube line and choosing the required fittings, routing should be designed as the following stage of system design.Clamping should be considered when designing routing. Proper clamming follows logically from appropriate design. It is frequently possible to clamp together many lines. Think on maintenance and troubleshooting: concentrate on logical design and prevent crossed lines. Reduce the possibility of users climbing or standing on plumbing by designing the tube line routing.
What is the solenoid valve?
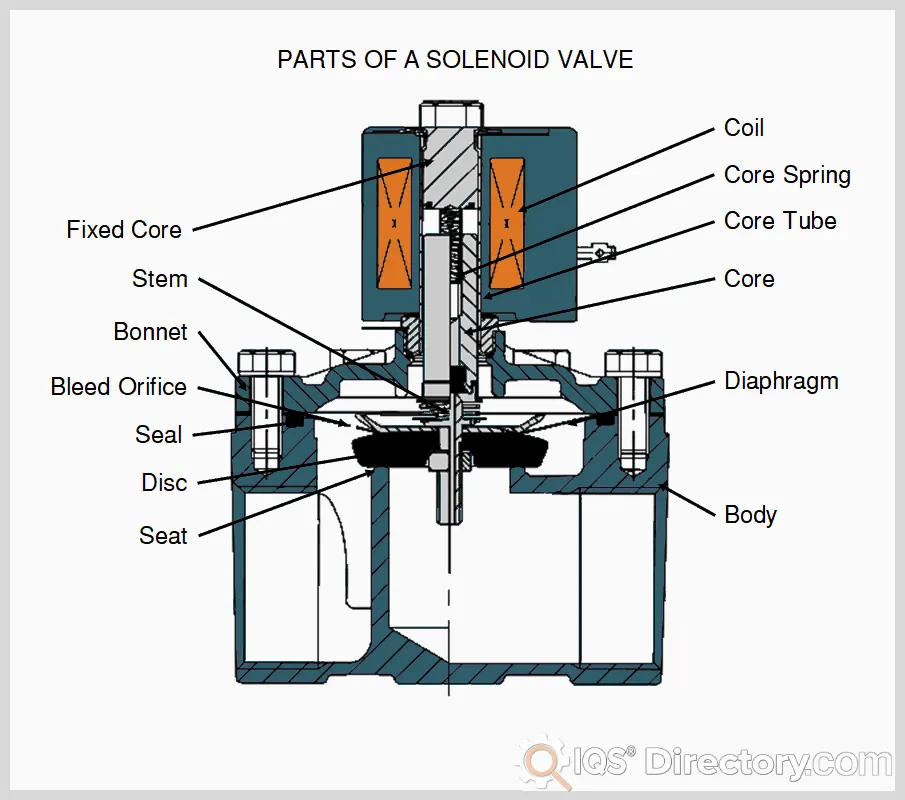
Solenoid valves are used to actuate the air flow in the cylinders as per the sequence through a manual or PLC-operated system.It is a mechanical device used to control or regulate the flow of fluid.A solenoid valve is an electrically controlled valve. The valve features a solenoid, which is an electric coil with a movable ferromagnetic core (plunger) in its center. In the rest position, the plunger closes off a small orifice. An electric current through the coil creates a magnetic field. The magnetic field exerts an upwards force on the plunger opening the orifice. This is the basic principle that is used to open and close solenoid valves.
What is the valve bank?
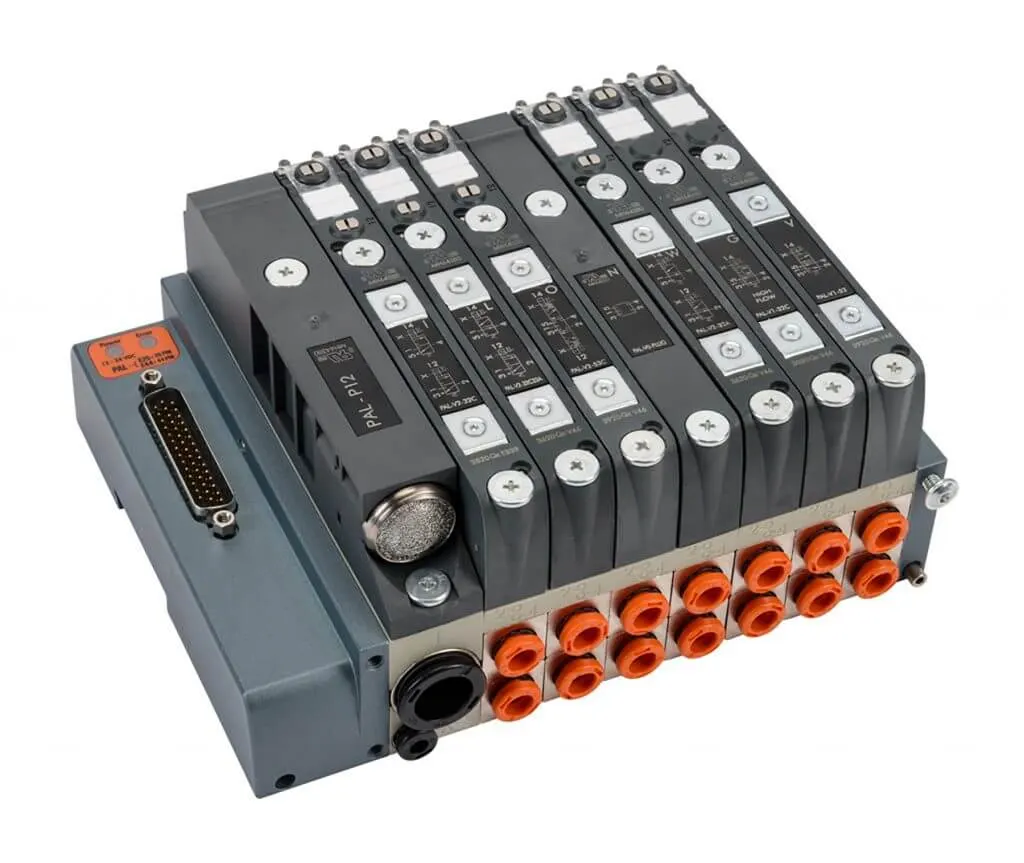
These valve banks are laterally arranged between a connection block and an end plate, all held together and hydraulically connected via a tie rod. The connection block, with inlet for pressurised oil and outlet for the return, is available in differing versions: With/without pressure limiting
valve or as an adapter to mount the valve bank on hydraulic power units. The galleries for pressurised oil and return run through all sub-plates and connect the mounted valves in parallel.
What is sensor & brief about its application in automation?
Sensor is a device which detects or measures a physical property and records, indicates, or otherwise responds to it. A unit designed to sense car panel using electrical sensors is called sensor unit. The from the sensors is send to the PLC so the next process is executed by this signal. The sensor is very sensitive & easily damagable part so sensor cover is provided to the sensor for safety purpose.
Sensors in Automation:
In the industrial automation, sensors play a vital part to make the products intellectual and exceptionally automatic. These permit one to detect, analyze, measure and process a variety of transformations like alteration in position, length, height, exterior and dislocation that occurs in the Industrial manufacture sites.
What are the types of the sensor?
The following are the various types of industrial sensors commonly used in automation:
- Temperature Sensor
- Proximity Sensor
- Accelerometer
- IR Sensor (Infrared Sensor)
- Pressure Sensor
- Light Sensor
- Ultrasonic Sensor
- Smoke, Gas and Alcohol Sensor
- Touch Sensor
- Color Sensor
- Humidity Sensor
- Tilt Sensor
- Flow and Level Sensor
We will see about few of the above mentioned sensors in brief. More information about the sensors will be added subsequently. A list of projects using the above sensors is given at the end of the page.
What are the fundamental points that need to consider while designing or selection of sensor?
-Sensor unit is design to sense the car panel,by using electrical sensors which are being welded tool.
-The signal form sensors will be feed to PLC and so the next process will be executed.
-Each panel should be sensed by 1-2 sensor depends on size of panel,preferred to be in digonal opposite ends of panel.For example if 10 panels are in assembly,so there should be atleast 10 sensors used.
-Sensor should be used to prevent accidents.
-Every sensor should be mounted in 3-directions adjustable way in general.
-Some major sensor manufactures are IFM,SICK,OMRON etc.