Week 1:- Introduction to BiW and Fixtures Challenge
1.BIW-BODY IN WHITE
BIW is the basically car or automobile welded sheet metal parts to form a structure of the vehicle . It is in the form of primers applied condition. Hence it appears like white color
It is used to connect the all the parts of the vechile parts like Engines,Gear box,Differencials, Roofs,Lamps ,Bumbers,it also help full to rooting wires almost the wholes weight vehicle part are sitting on this structure only
these are very large and complicated struture hence the these are divieded into the varies parts that are list down below of
- Under body
- Body sides
- Closures
- Roof
- Fenders
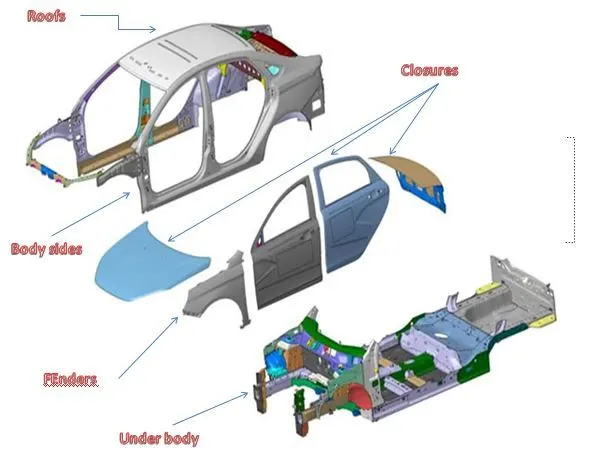
Under Body
This is bottom side of body that is carries a more weight in the struture. Most of part are mounted in this part likes Engines,Clutched,Gear boxes,petrol tanks,cooing systems,Gear Shifting Assemblys,fly wheels,power transmission shafts,ets
Side Body
This Inner and Outer side of the body like that is shown in figure
closers
It is normally likes open and close types it always connected in hinges for example Doors,Hoods,dickys,etc
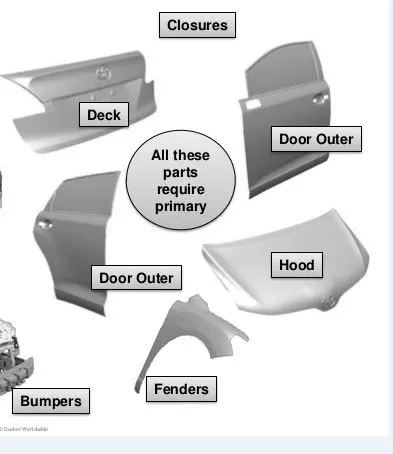
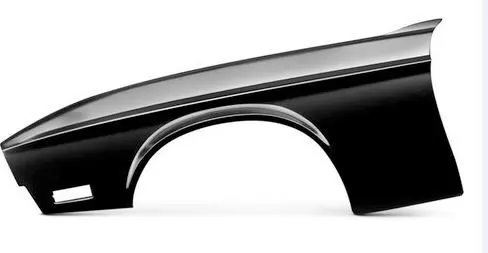
Fenders
It is very smooth surface edges of the car body. It gives the good look of the cars
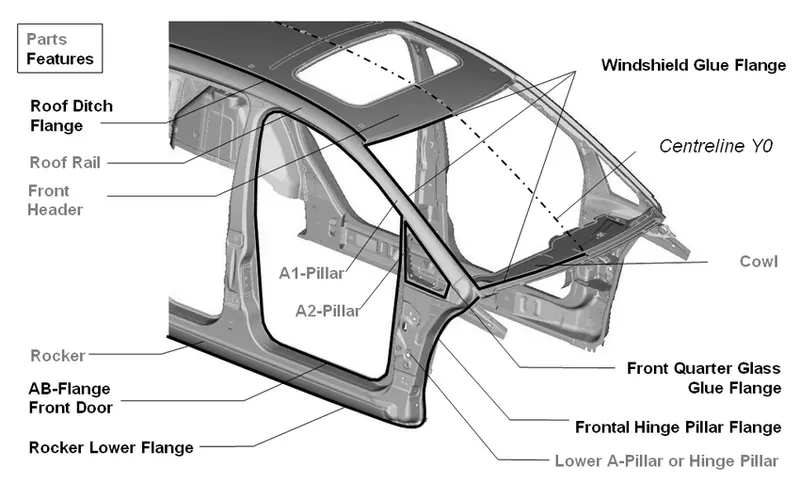
Roofs
It is the top of the car struture it carries some of the wire rootings hoods some cars have top door space , front door space ,windshield glus flange, roof ditch flange , back wind shield space
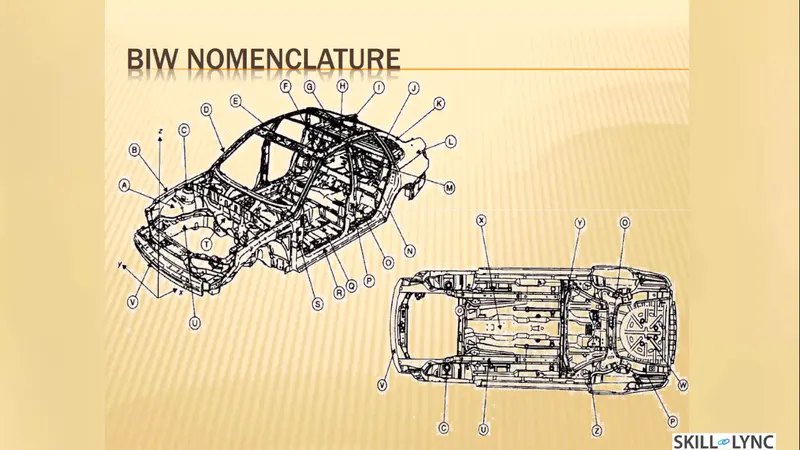
2.BIW NOMENCLATURE
- The biw nomenclature is the list of part that is in the assemble condition or exploded views.
- That is used to identify part which position which component will come.
- this is used assemble part easier and it is pictorical reprasentation of the no of parts
- IT represented my alphabets(A TO Z) OR IN NUMBERS(1 TO 26)
The belows are the biw nomenclature of biw parts
| ALPHABETS | UK(DESCRIBTION) | US (DESCRIBTION) |
| A | INNER WINK PANEL | MOTOR COMPONENT SIDE PANEL |
| B | UPPER WING MEMBER | MOTOR COMPONENT UPPER RAIL |
| C | SUSPENSION TOWER | SHOCK TOWER |
| D | UPPER A PILLER | A PILLER OR WINDSHIELD PILLER |
| E | WIND SCREN HEADER RAIL | WIND SHIELD HEADER OR FRONT HEADER |
| F | ROOF STIFFNER | ROOF BOW |
| G | REAR PARCEL TRAY | PACKAGE SHELF |
| H | CENTER RAIL | SIDE ROOF RAIL |
| I | BACK LIGHT FRAME | BACKLITE HEADER OR REAR HEADER |
| J | C PILLER | C PILLER |
| K | D PILLER | DPILLER |
| L | REAR QUARTER PANEL | REAR QUARTER PANEL |
| M | BOOT FLOOR PANEL | REAR COMPONENT PAN |
| N | REAR SEAT BACK RING | REAR SEAT BACK OPENING FRAME |
| O | REAR SEATBACK PANEL | REAR SEAT BACK PANEL |
| P | B PILLER | B PILLER OR CENTER PILLER |
| Q | FLOOR PANEL | FLOOR PAN |
| R | SILL | ROCKER OR ROCKER PANEL |
| S | LOWER A PILLER | FRONT BODY HINGE PILLER |
| T | DESH PENEL | DASH PANEL |
| U | ENGINE RAIL | MOTOR COMPARTMENT LOWER RAIL |
| V | FRONT BUMPER | FRONT BUMPER |
| W | SPARE WHEEL WELL | SPARE TIRE WELL |
| X | CENTER TUNNEL | TUNNEL |
| Y | REAR SEAT CROSS BEAM | #4CROSS BAR |
| Z | REAR SUSPENSION SUPPORT BEAM | #5CROSSBAR |
3.WHAT IS FIXTURE AND ITS TYPES ?
Fixture is device is used to hold the work without any moment in it.Based on the work condition fixtures are made by veries material like harden materials like Tool steels ,Soft Materials low carbon steels , other then matal like plastic material PU,Derlin,pvn,ppv etc..
Fixtures are used to manufacturing product Quicker , Easier , and also Quality also good.there are varies types of fixture design is there are based on the Pnuematic Actuators , Hydroulic Actuators, electric actuators . These fixture are made of veries kind mechanism are used to clamp the product with out any damage of the component . fixture is main used in automobile industries production line .
Fixture are made big revalution in the veries kind Industrial Manufacturing sectors.it increases the production quantity . it makes complicated work to so easy. it reduces the human effects , and its save humen energies , simplifies works , it reduces the production time , it negulates human errors , and more on
These are also catagariesbased on process like welding fixture, screwing fixture , reviting fixture , pressing fixture , checking fixtures , persing fixture
Types of Fixture
- Prodution Fixture
- Pre production Fixture
- Checking Fixture
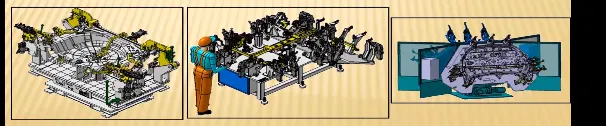
- Production Fixture
This kind of fixture mainly used to mass produce of product .they are various kind of production fixture is here that based on the process of it work
Welding Fixture :
this kind of fixture are used for various welding process like
- TIG
- MIG
- LASER WELDING
- AUTOMATIC HYDROGEN WELDING
- STRIK WELDING
- ELECTRO SLAG
- ENERGY BEAM WELDIND
- PLASMA ARC WELDING
Based on the welding process and welding we made the fixture
if it is a automatic fixture we are going to the elecrical actuators , pnuematic actuator , motor like induction motor weathar need accuracy go stepper motors or servo based fixtures,
there are more things inside that that are
- Pnuematic cylinders
- Read switch
- Pressure Regulators
- Sensors (there are lot verties of sensor available in market)
- clamps mechanisms
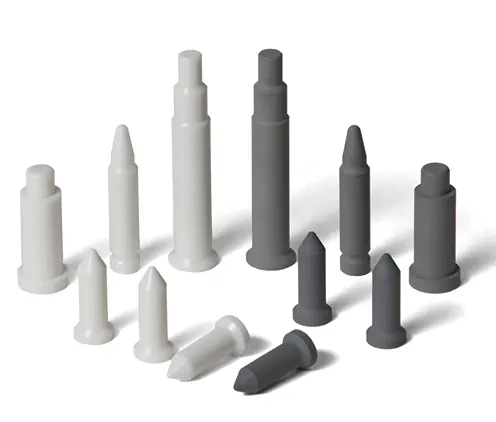
- geo pins
- re locating pin
- profile locator
- welding electrodes with its assessoeries
Screwing Fixture:
This fixture are used screwing the component to join two parts together
Reviting fixture:
It is same like that screw fixture
Glueing fixture
2. Pre-processing Fixture
Before made mass prodution fixture they are made some trial fixture chacking every things of this fixture before it will goes for mass producttion it cycle time is more then the production fixture
3. Checking Fixture
checking fixture are used to check the component weather it is exact dimension OR not . there are based on the gauge fixture and cmm fixture cmm stands for co ordinate measureinf machine this fixture used to check the gd & t of the component .
4. What is the basic principle of design the fixture
Basic Principles of Fixture Designing :
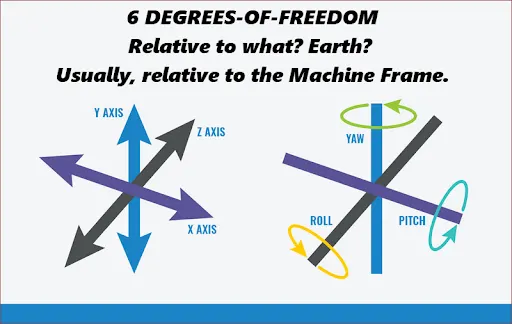
when we start to design the fixture we need to arrest the fixture by all the side without any moment in that fixture. hence we follow the principle 3-2-1 Principle whatis that mean for that when ever the body is in space it has 6 degrees of free dom it may be a 12 but mainly we need to arrest the 6 degrees of free dom
what is that 12 degress of freedom are '
6 translational motion
6 rotational motion
6 translation are
- X positve translation motion
- X negative translation motion
- Y positve translation motion
- Y negative translation motion
- Z positve translation motion
- Z negative translation motion
6 rotational motion
- X clockwise rotation
- X anticlockwise rotation
- Y clockwise rotation
- Y anticlockwise rotation
- Z clockwise rotation
- Z anticlockwise rotation
wnen we place the oneside face on wall means it arrest the 2 Rotational motion and 1 translational motiol . place the onther bottom face on the ground means it will arrest the two degree of freedom like 1 Rotional motion and 1 near motion and remainning one degrees of freedom is available that is also arrested by anther side of the part to arrest three degrees of freedom
When ever working on the fixtures these kind think to arrested must other wise acciedent may accure during the machinnig process.
to accure the zero desgree of freedom.
5. Elabrate Types of BIW Stations ?
Assembly lines are divided into verious zone under that varius station are come.We cannot able made a part into single part it will makes the product cast too higher hence we made three different zones roof zone , under body zone , fender zone , body side zone ,fenders zone. this is further divided into the various stations .
The time are based on the this zone we can ablw to get some time cycle that will get a knowlege of the all thos e things . these zone furhter divided in to the station because of the size of the product we can sub assemly wise make some station to make product to easy for the manufacturing .
Types of biw stations :
- Tool
- Grippers
- Stands
- miscellaneoues
1.Tool
Tools are used to assembly or able location of component that helps to locating the component accurate dimentions.
there four kind tools are here . There are
- Geo tools
- ReSpoted Tool
- marriege Tool
- Former Tool
A. Geo Tools :
A tool is used to geometeric dimension of the component that will not change its geometric dimension of after the welding or working done by the station this cycle is based on the location of the component it reduces the wastage level or craap product level
B. ReSpoted Tool :
Respot to also the geomateric it will cover the other then the geometer tool because the it will spoted more location for example geo metric tool is able to cover the 15 spots there remainng part have 150 sport means it will be covered by those spots geometeric tools castly then the respot tool
C. Marriage tool :
Marriage tool is defind as two or more tool combined to form a single tool it may be a gang tool
D.Former Tool :
The function of the marriage tool is comes under the framer tool only
2.Grippers :
Grippers are used to pick the component from one place to anther place
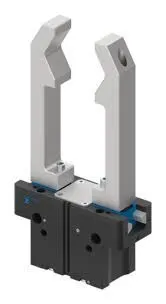
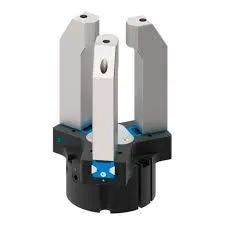
The Various Types of Grippers are
- Material Handling Grippers
- Process Grippers
- Combo grippers
A.Material Handleing Gripper :
These gripper are use to handling the thinks from one place to anther places these grippers are more useful to reduces the human effects
B.Process Grippers :
These grippers used to handle processes like welding , screwing , reviting , glueing , drilling , reaming , tapping , broaching , milling ,etc....
C.Combo grippers :
Combo Grippers are used to both Material handling as well as the Process handling
3.Stands :
Stands are used to hold the product or tool the will handle by the robo hands
there are verious types of stands are
- glues gun stands
- welding gun elesctrode stands
- pedestal stand etc....
4.Miscellaneous
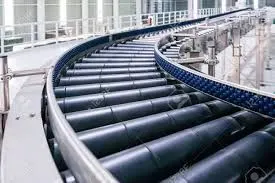
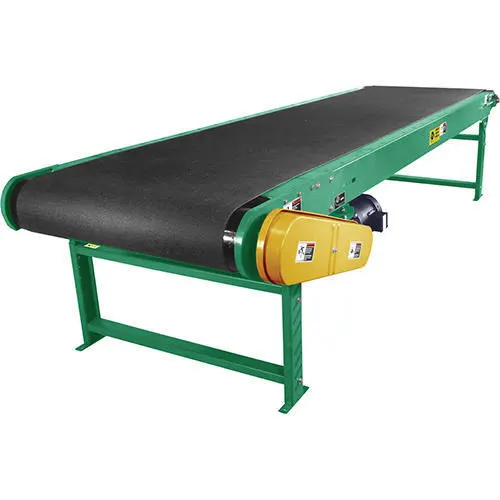
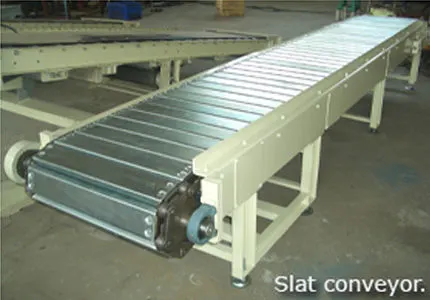
Conveyors , material stand or product stand ,take out trallies these are call as miscellanious
there are various types of convoyer is there belt conveyor , roller conveyer , chain conveyer
6.What are the basic terminologies used in the BIW fixture?
what is terminalogy means when ever constructing fixture there are lot of thinks needed to added on that and what kind think are more important that is called as the terminalogy. fixture made lite weight these terminalogies helps to reduces the weight of the fixture too. the fixture terminalogy are
- Mylers
- Principle locating Point
- Blades
- Raisers
- Shims
- Rough Locator
- Hardwares
- CMM
- Units
- Number plates
- Co-ordinates
- Clamp plates
- Name plates
- Clamp arms
- Pivot points
- Class A surface
- Reed switch
- Sensors
Mylors
Hardwares
Hardwares are nothing screws and nuts are called as hardwares basically fastners are called as the hardwares
CMM
CMM is nothing it Co ordinated Measuring Machine the small ball types needle that touch to identify the sufaces of the component that will be programed by softwares . Basically that ball types needs are called as Probes that willbe control by the servo motors x,y and z axis Co-ordinates
Units
there
- pin unit
- calmping unit
- assembly unit
Number Plates
Co-ordinates
Each and Every fixture must have co ordinate holes that is used to measure CMM of the fixture points this will be the start point of the cmm co ordination
Clamp plates
clammping plates are used to clamp and hold the work piese proper condtion
Name plates
Names plate contains fixture name , its parts numbers , company name fixture designed all are engraved
Clamp arms
clamp arms used to swing the clamps back and forth
Pivot points
clamps rotates above its axis of this pivot points
Class A surface
the component surface is the face of the part means that surface must have clear suface the is no mark on that surface on that sufaces area we used derlin block or plastic material avoid those scranch and marks
Reed switch
Read switch is used to identify the weather cylinder is in clamping condition or not that will be identify by reed switches
Sensors