Design of backdoor
Design of Backdoor
Objective: To design Back door of car using the given Class ‘A’ surface.
Introduction
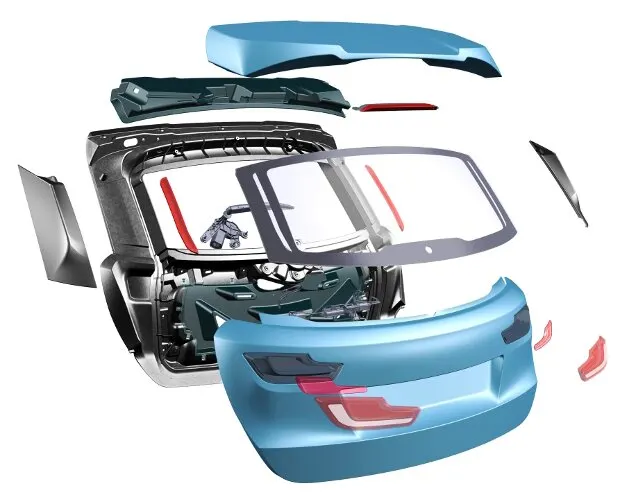
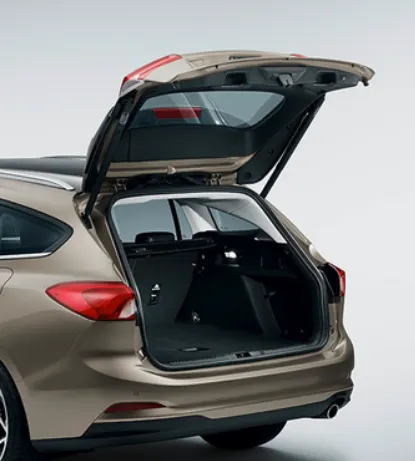
It is a hinged board or door at the rear of the vehicle that can be moved up or down during loading and unloading.
Back Door is also referred as 'Hatch' or 'Tailgate' or 'Trunk-lid' or 'Boot-door'. Its the rearmost part of the vehicle which gives access to the trunk and has mounts for tail lamps, hinges, wiper motor, gas stayetc
Functions of the Backdoor:
- It protects the occupants and luggage from getting damaged.
- It houses assembly of tail lamps, wiper motor and other components.
- It serves as entry and exit point for luggage/passengers.
- It houses windshield glass which helps in rear visibility.
- Parking sensors, rear view camera are mounted on it.
Types of Backdoor
- Top mounted
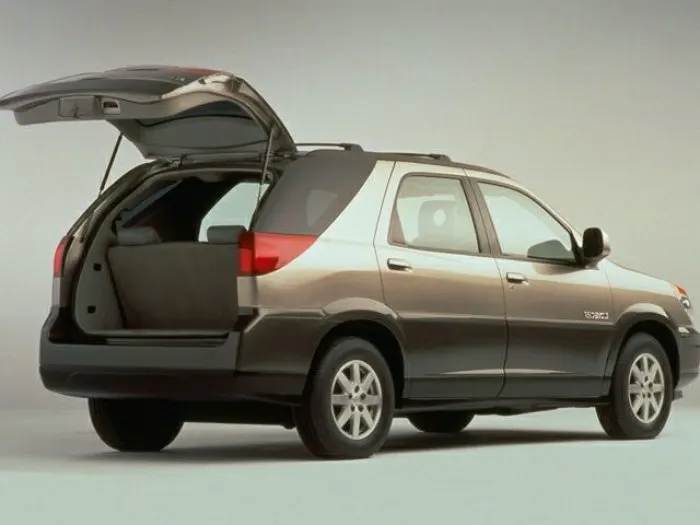
These type of back doors are used in a station wagon, pickup truck and some other sports utility vehicles. Today’s modern cars use top mounted tailgating systems which are both powered and also gas stay supported. These tailgates provide greater rear visibility compared to other types.
- Side mounted
It is generally used in van type MPVs, SUVs, pickup truck vehicles. These side mounted door/barn doors are a lot easier compared to top mounted ones. These doors are generally small in size and can be easily accessed. These doors are more convenient for the goods handlers carrying lengthy objects, long pipes where one door is kept open. It also saves accidental head impacts. It is a lot easier to load /unload things in vehicles having side-mounted doors.
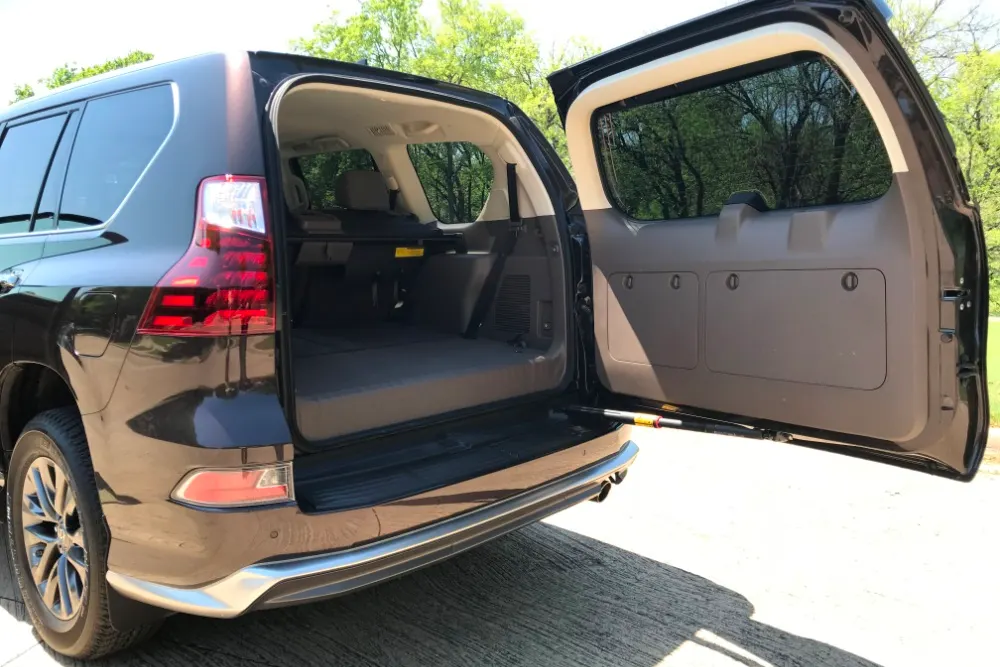
- Bottom mounted
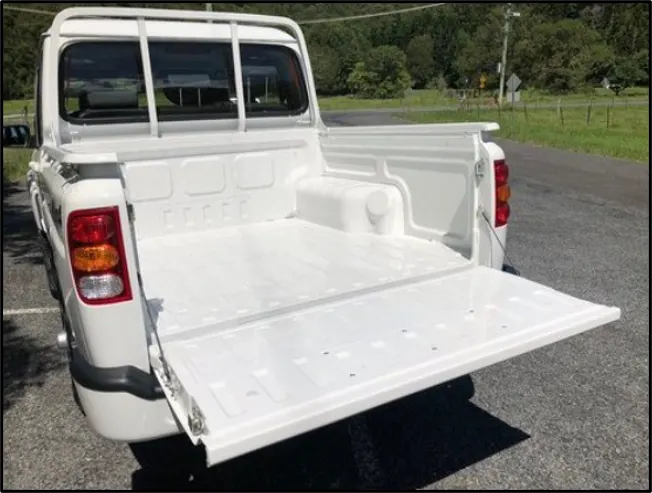
Bottom type or split type backdoor system is used in estate type cars, pickup trucks and some luxury SUVs. These are most convenient type of backdoor in which the bottom split is used as a support or even as a table for the touring people.
Materials Selection:
The selection of material plays a major role in determining the overall weight of the back door. The common materials used are Steel & Aluminum. The density of Steel is higher than Aluminum thus adding more weight to the door. The material used in the manufacturing of the backdoor depends upon the budget of the car, most low cost vehicles use steel as it is cheaper compared to Aluminium. Another aspect to be noted is that, if casted Aluminum parts are used instead of deep drawn steel parts there is no need of reinforcements and the overall weight of the car is reduced by approximately 5-10kg thus increasing the performance of the vehicle. Also the draft angle for casted parts is around 3 degrees while for deep drawn parts is around 7-10 degrees which helps in increasing the luggage/ cabin space.
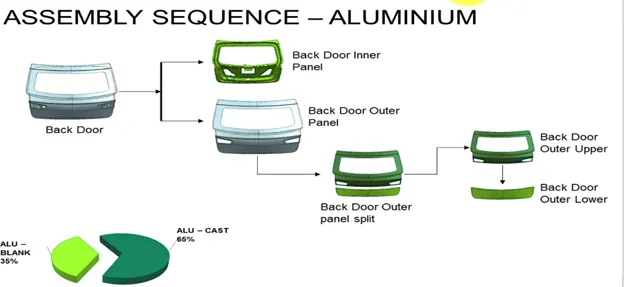
Fig. above shows possible no. of parts in aluminium backdoor
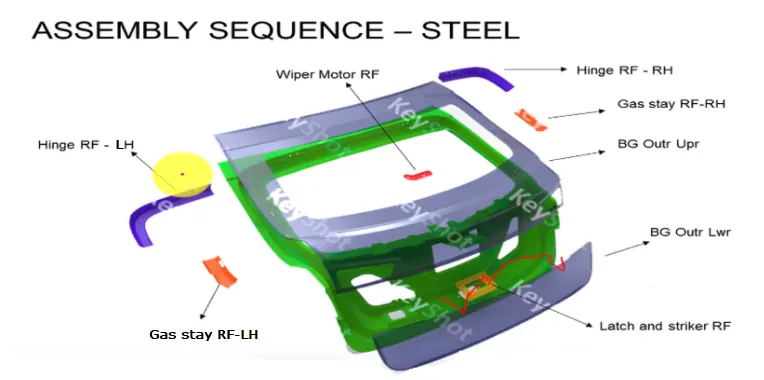
Fig. above shows possible no. of parts in Steel backdoor
The below table gives a comparative information about Steel and Aluminium.
| Aluminium | Steel | |
| Parts | Parts are casted | Parts are stamped |
| Reinforcements | Reinforcements can be neglected | Reinforcements are necessary |
| Thickness | Thickness can be varied | Thickness should be uniform |
| Weight | Lighter in weight | heavier in weight |
| Cost | Costly as compared to Steel | Cheap as compared to Aluminium |
| No. Of components | Less No. of components | More No. of components |
Components to be designed:
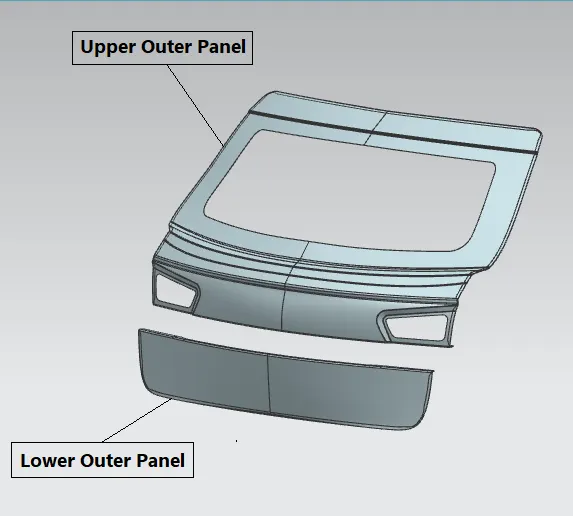
1) Outer panel
It is the outer styling skin surface of the back door. It is provided with multistage coatings which has property of scratch resistance, rust prevention etc. It is wrapped around the inner panel through hemming process.
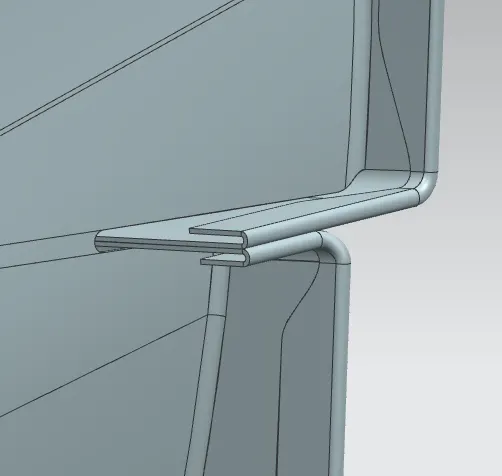
Hemming: Hemming is a forming operation in which the edges of the sheet are folded over another part in order to achieve a tight fit. Usually hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges. In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
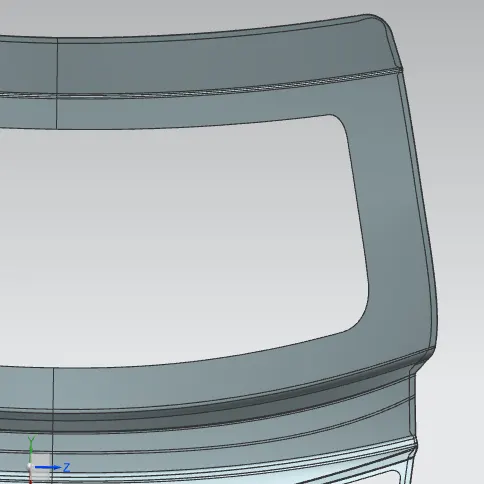
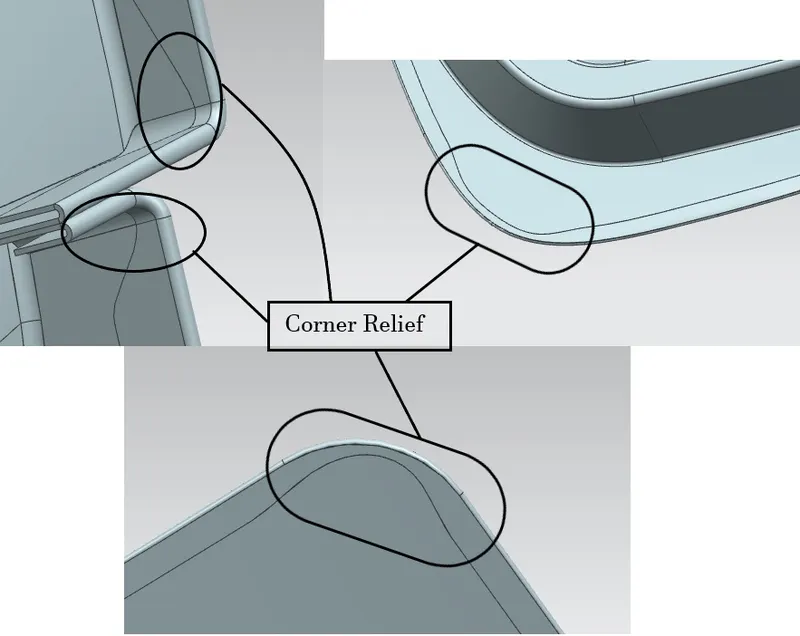
Corner Relief: During hemming process multiple rollers are used which causes vibrations and stress concentrations at the some locations due to which design intent of the panel shouldn’t be changed (i.e the panel should spring back to original formation after roller is removed). But most of the time that is not the case at corners so to avoid that situtaion reliefs are provided at corners.
2) Inner Panel
The inner panel is one of the most important components of backdoor assembly. It provides strength and helps in dissipation of forces outside the part with the help of embosses made on it. It helps in mounting of accessories like hinges, wiper motor, gas stay, latch & striker etc.
The inner panel is produced by either casting or through Deep drawing process.
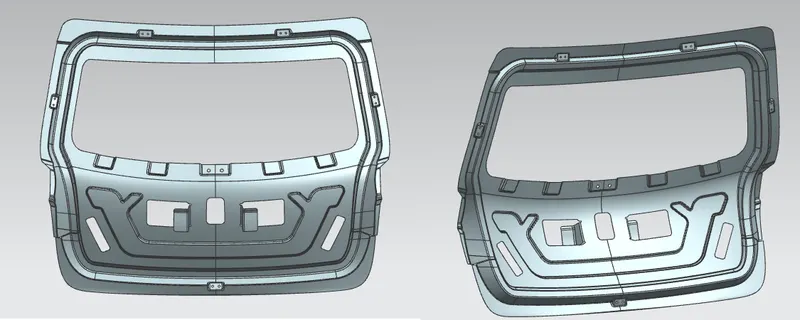
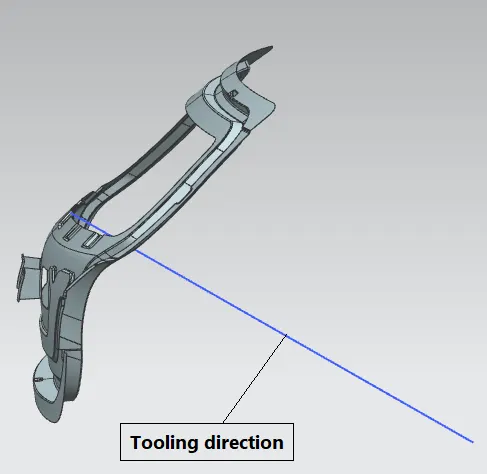
Mostly aluminum part is casted, steel inner panel are manufactured by deep drawing process. If deep drawn, there must be a tooling direction through which that panel must be deep drawn.
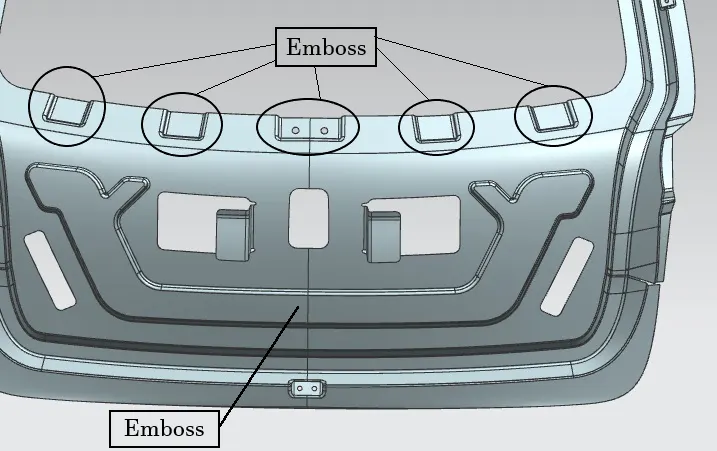
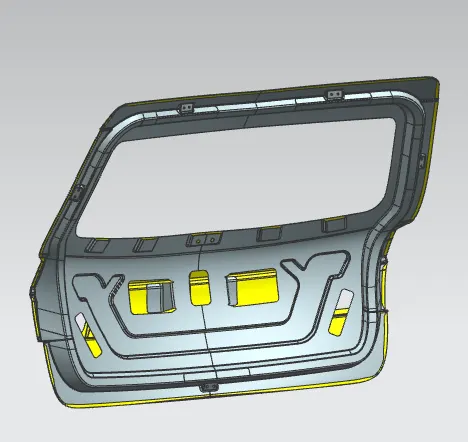
Embosses: It is provided to give extra strength to sheet metal panel and to help dissipate forces/energy towards a specific direction. Here embosses (Y/V emboss) are designed in such a way so as to direct them towards the outer end of the backdoor as shown in the image.
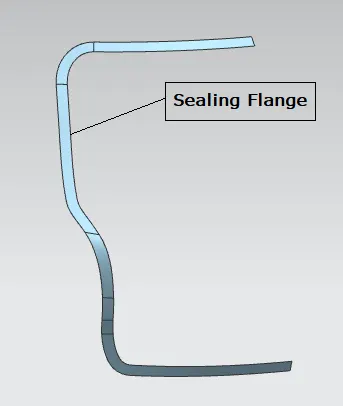
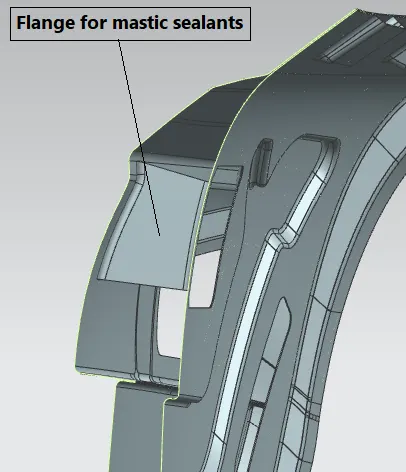
Sealing Flange: It is that section of the inner panel which enables the backdoor to sit over the rear body side of the car. Its design is important as it decides how a backdoor is mounted on the rear body side of the car and also restricts any external matter to enter inside the vehicle.
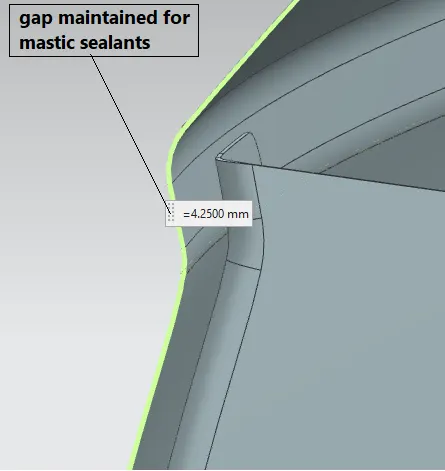
Mastic Sealants: As we know the outer panel gives the aesthetic look to the vehicle, so we can’t use bolting or spot welding or any other joining technique which damages the aesthetic looks of the panel. Thus mastic sealants are used for joining the Inner panel elements with outer panel. A maximum gap of 5mm is to be maintained in between parts where mastics are to be applied.
Reinforcements
Reinforcements are generally placed to increase the strength of the panel in localized areas which is relatively small compared to sheet metal parts for absorbing loads imposed thereon and dissipating such loads throughout the panel assembly to help maintain rigidity of the panel assembly. The reinforcements are usually 1-1.5mm thick as opposed to 0.75mm thick panel used in this part.
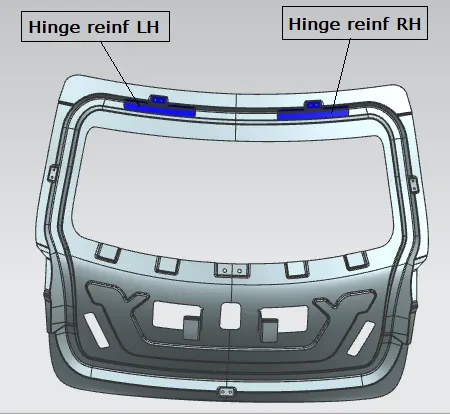
- Hinge reinforcements
Hinge is a pivot mechanism which supports the total weight of the backdoor. So reinforcements are added for strength and rigidity.
- Gas stay reinforcements
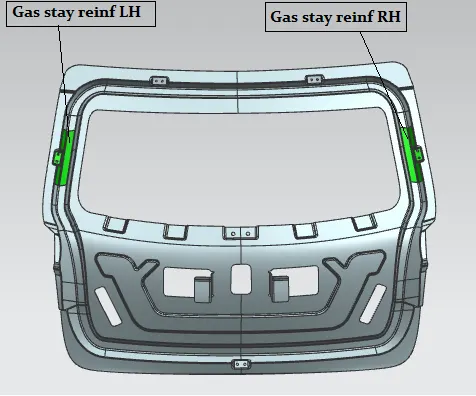
Gas stay is used to lift the backdoor automatically and is used to support the backdoor in its open position. It can be of Two types Semi-automated and fully automated.
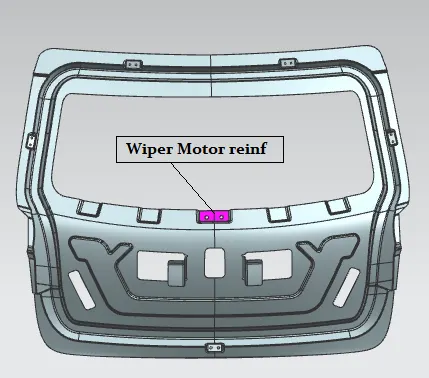
- Wiper Motor reinforcement
Wiper is used to wipeout the dust particles/water on the windshield glass which affects the rear visibility. It is actuated by the motor which is mounted on the inner panel. Due to vibration and heat of the motor, inner panel gets deformed which results in loss of strength & rigidity of the panel thus leading to poor NVH. So reinforcement is provided to avoid these conditions.
- Latch and Striker reinforcement
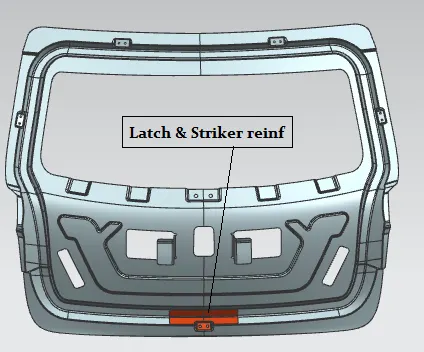
In the bottom part of the panel emboss is created for placemnet of latch and striker assembly. There is over slamming and abusing while opening and closing of the door, thus arising the need for reinforcement to be placed.
Positioning of Latch & striker/ Latch Trajectory:
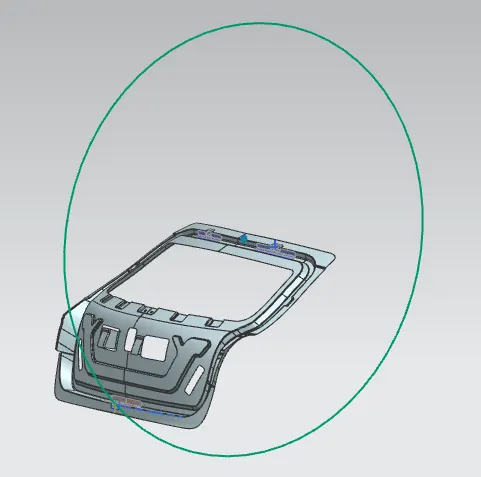
Backdoor is the swinging part which rotates about hinge axis. The position and orientation of latch striker is important for proper opening and closing of the backdoor. The positioning is done by sketching a circle with center as the axis of the hinge which passes through the striker at appropriate position with respect to inner panel.
Design considerations
- Rear visibility
- Boot space & accessibility
- Sealing Flange
- Support structures like hinges and gas stays.
- Mounts for wiper motor, tail lamps and other wiring loops
- Rear crash regulations
- Joining techniques such as hemming, spot welding etc.
- Gap and flush requirements
Assembly:
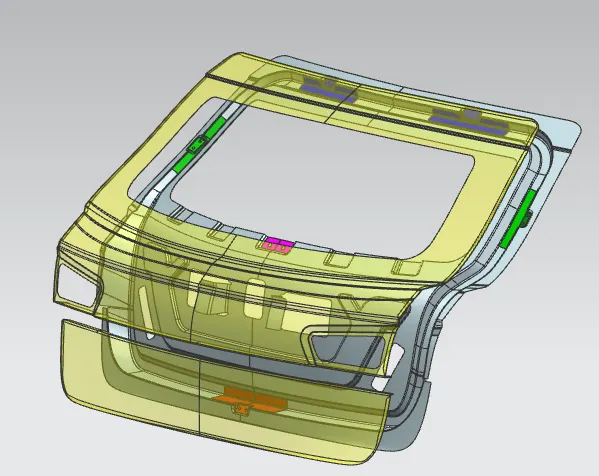
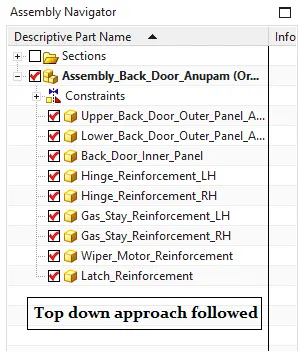
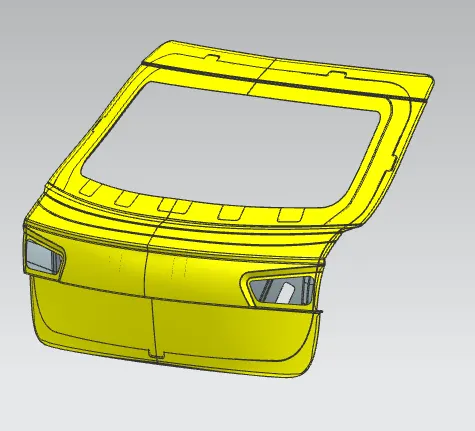
In this assembly Top down approach was followed wherein from given styling surface the inner panel was created using various tools/commands in NX. After that others parts were modelled as per the requirements one by one.
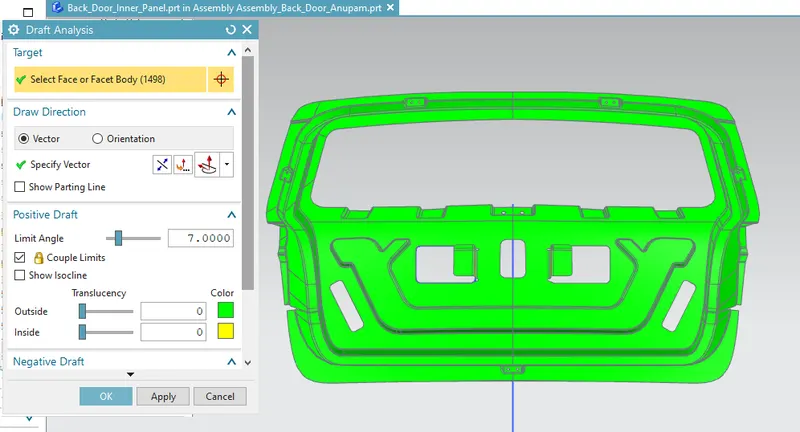
Analysis: Draft analysis
Every part which is manufactured from press tool or other forming tools require some positive draft on the faces which are parallel to the tooling direction. If we don’t give draft (Zero Draft) or give negative drafts on these faces it will stick to the mould surface and when the mould is in motion it will destroy surface thus reducing its surface finish. Thus Draft Analysis command enables us to detect if the part we have drafted can be easily ejected or not. It also give insights about the critical zones, so that appropriate changes in the design can be made if needed.